Engineered High-Integrity Metric Titanium Fasteners
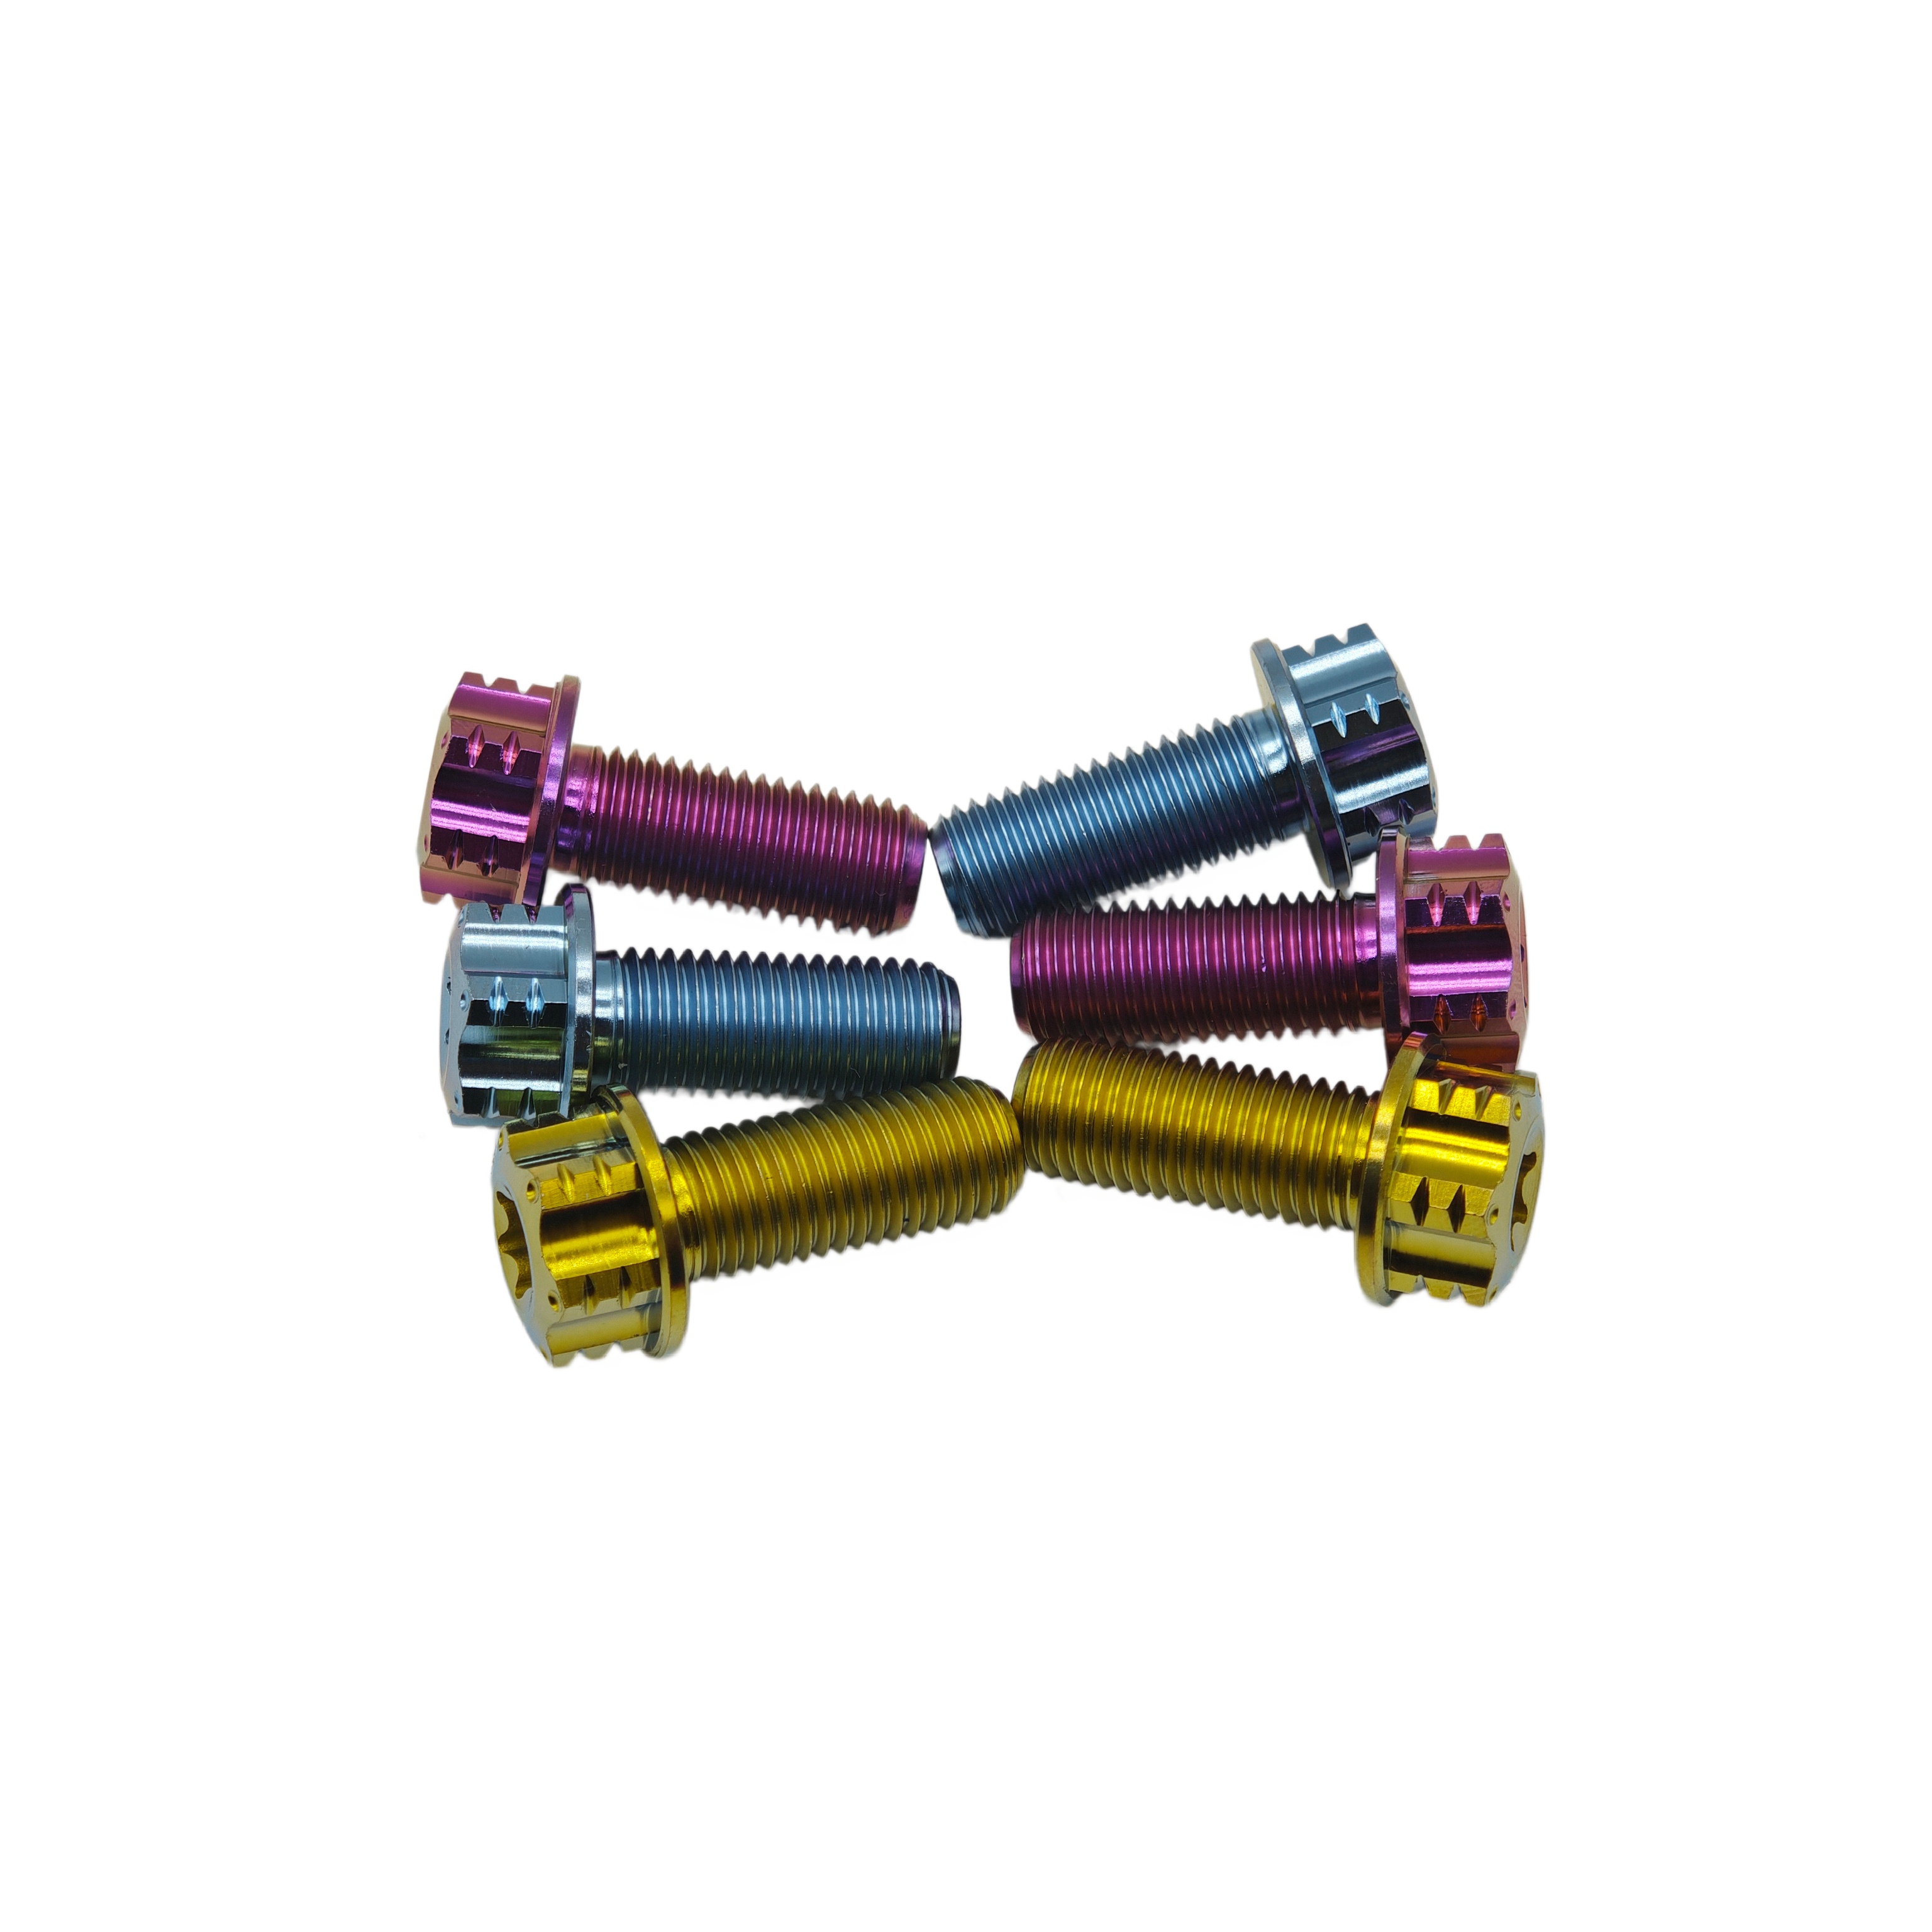
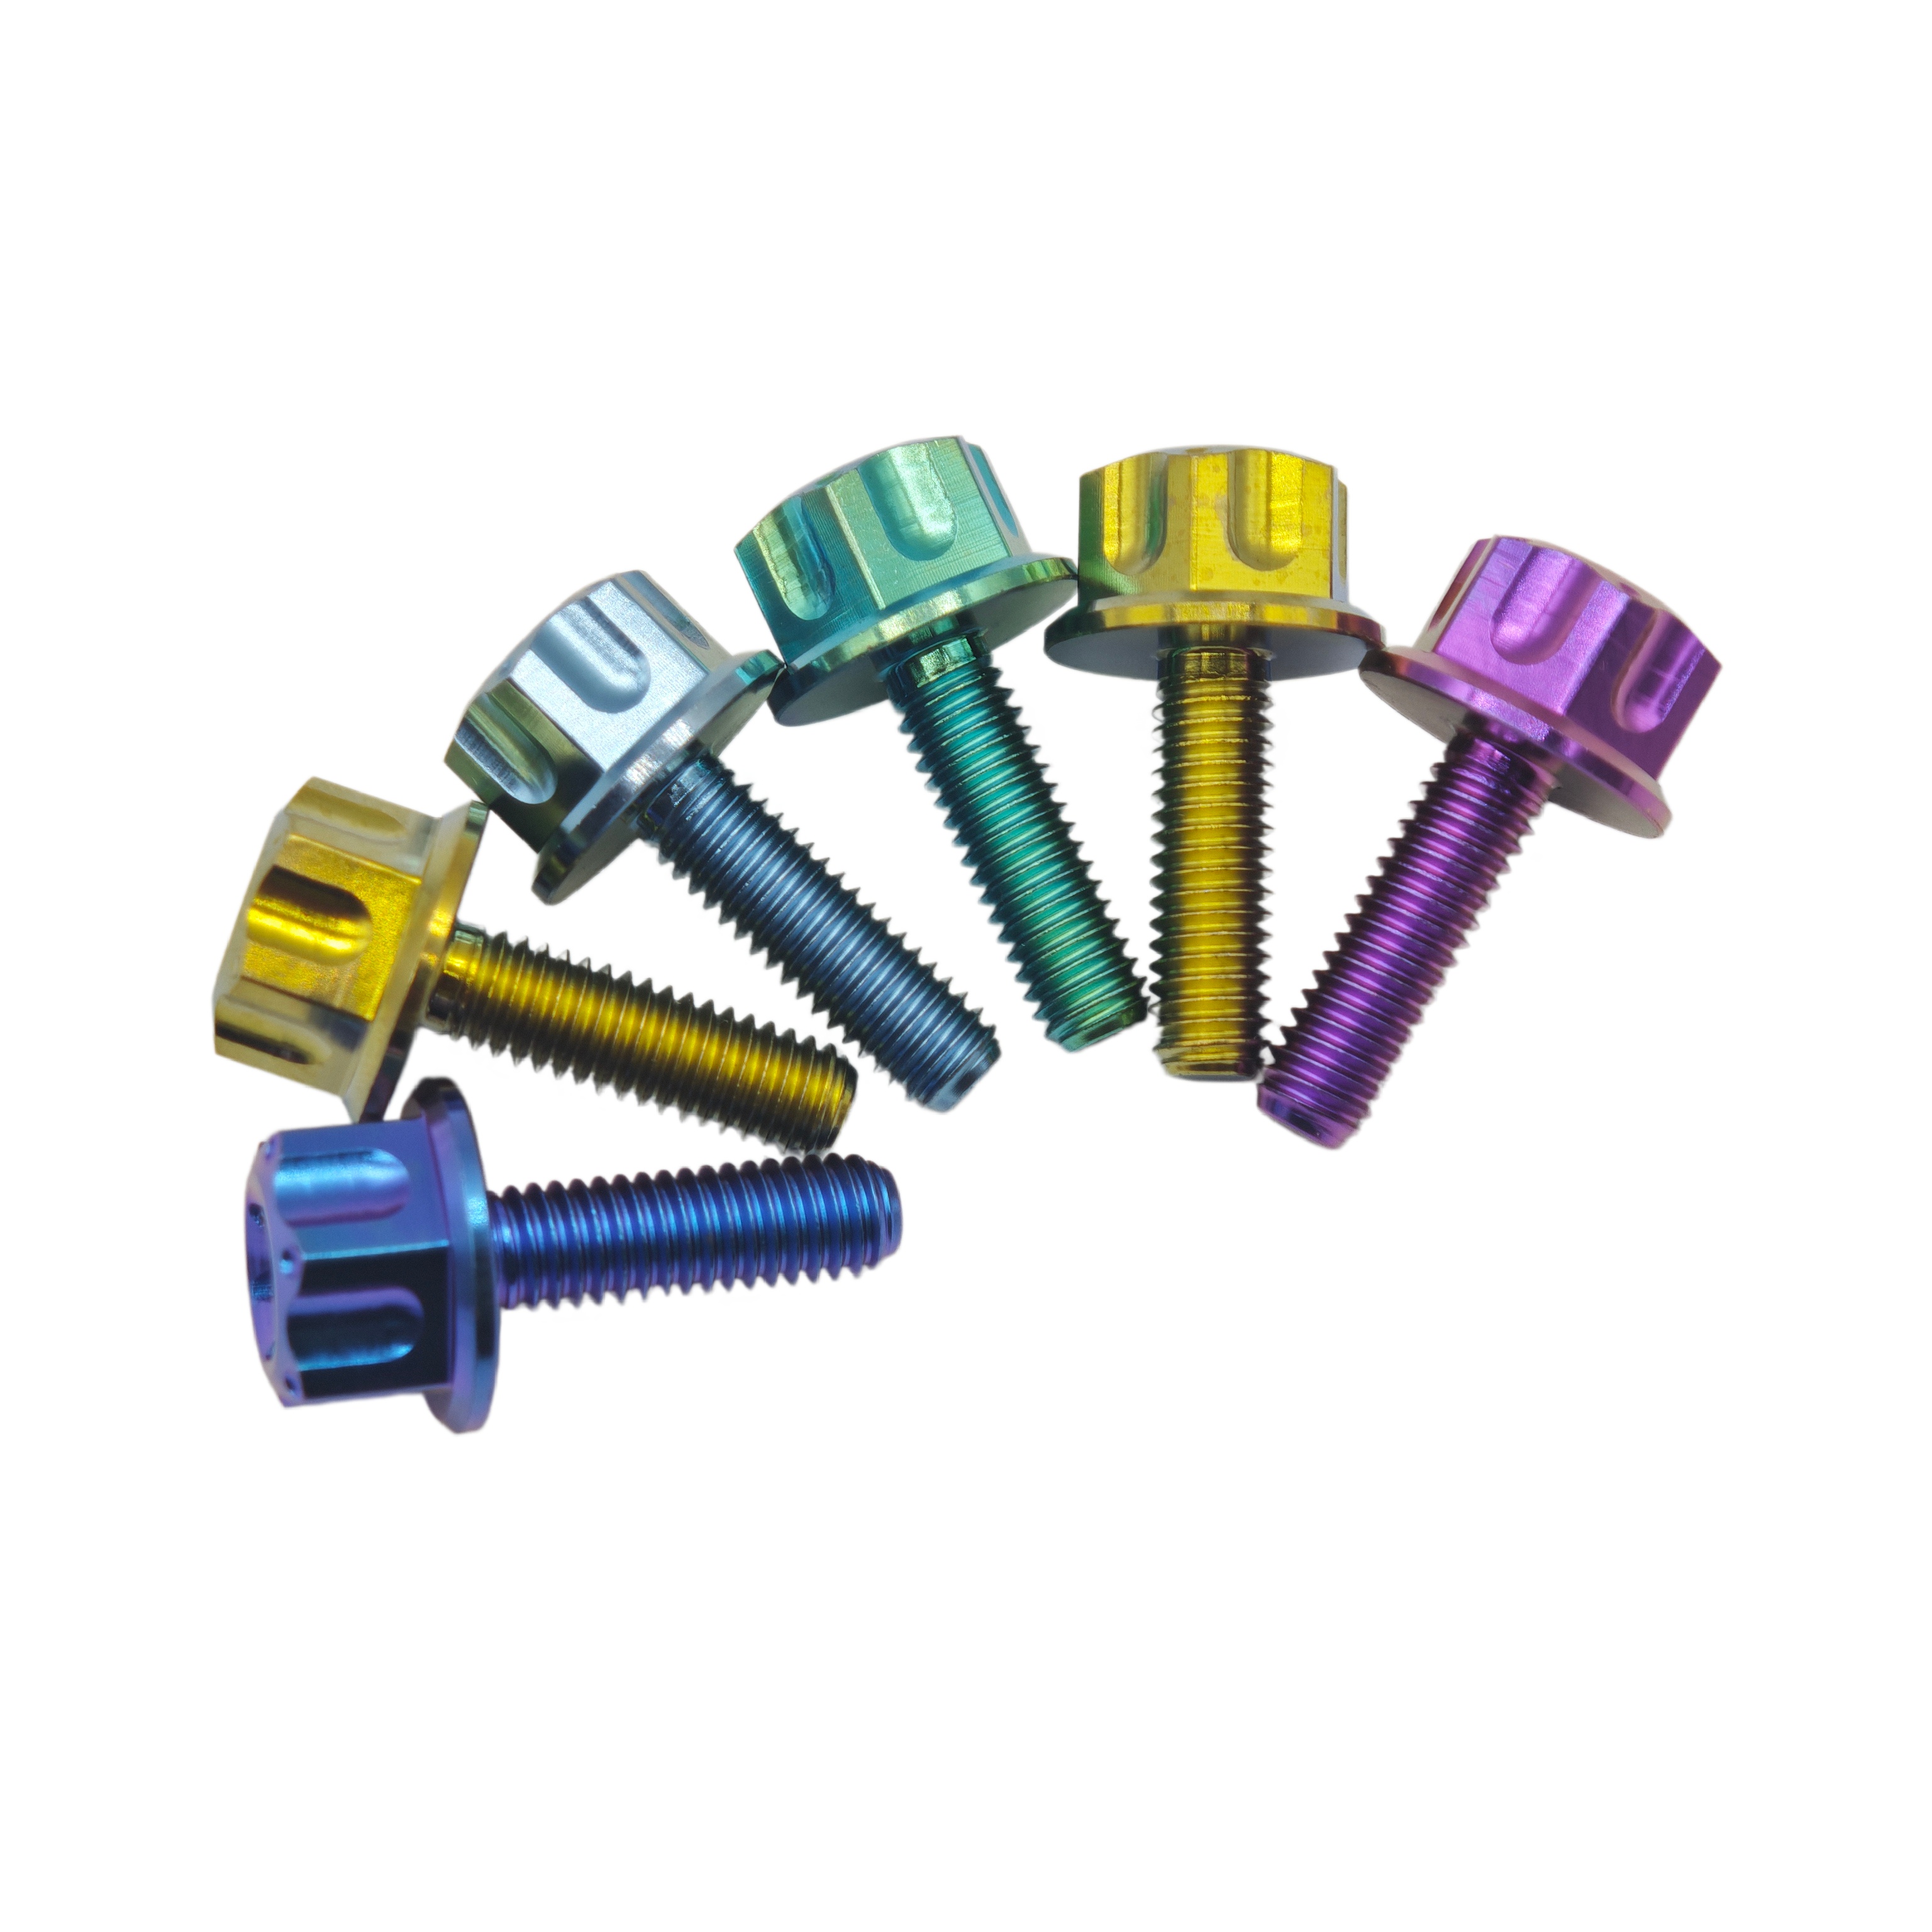
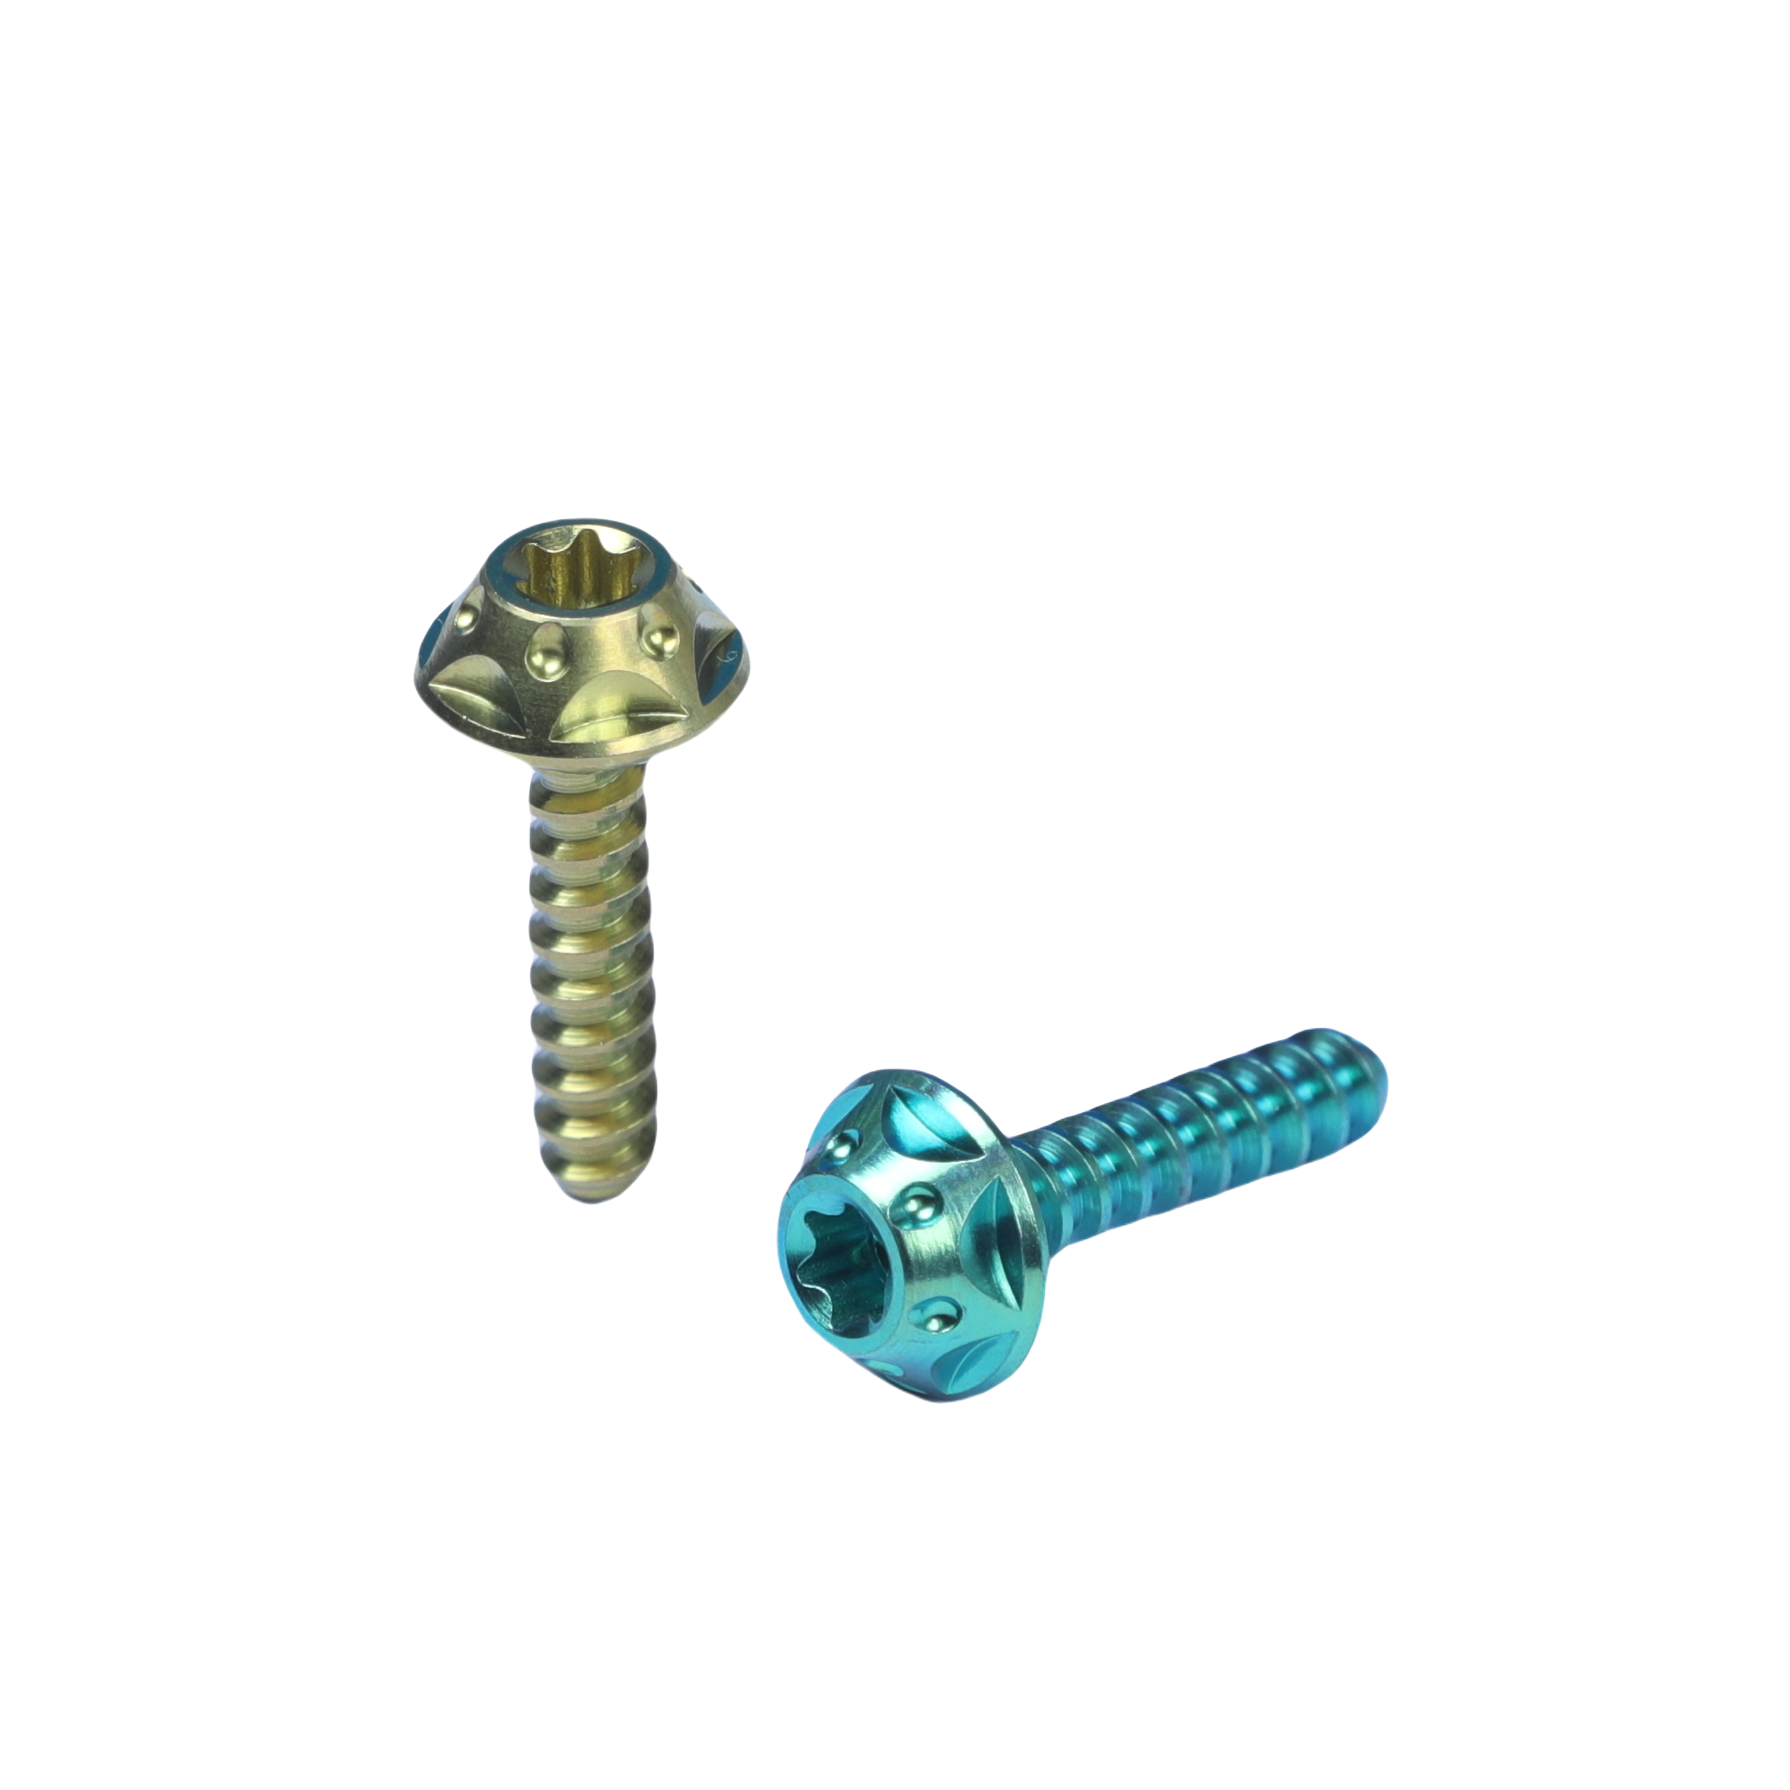
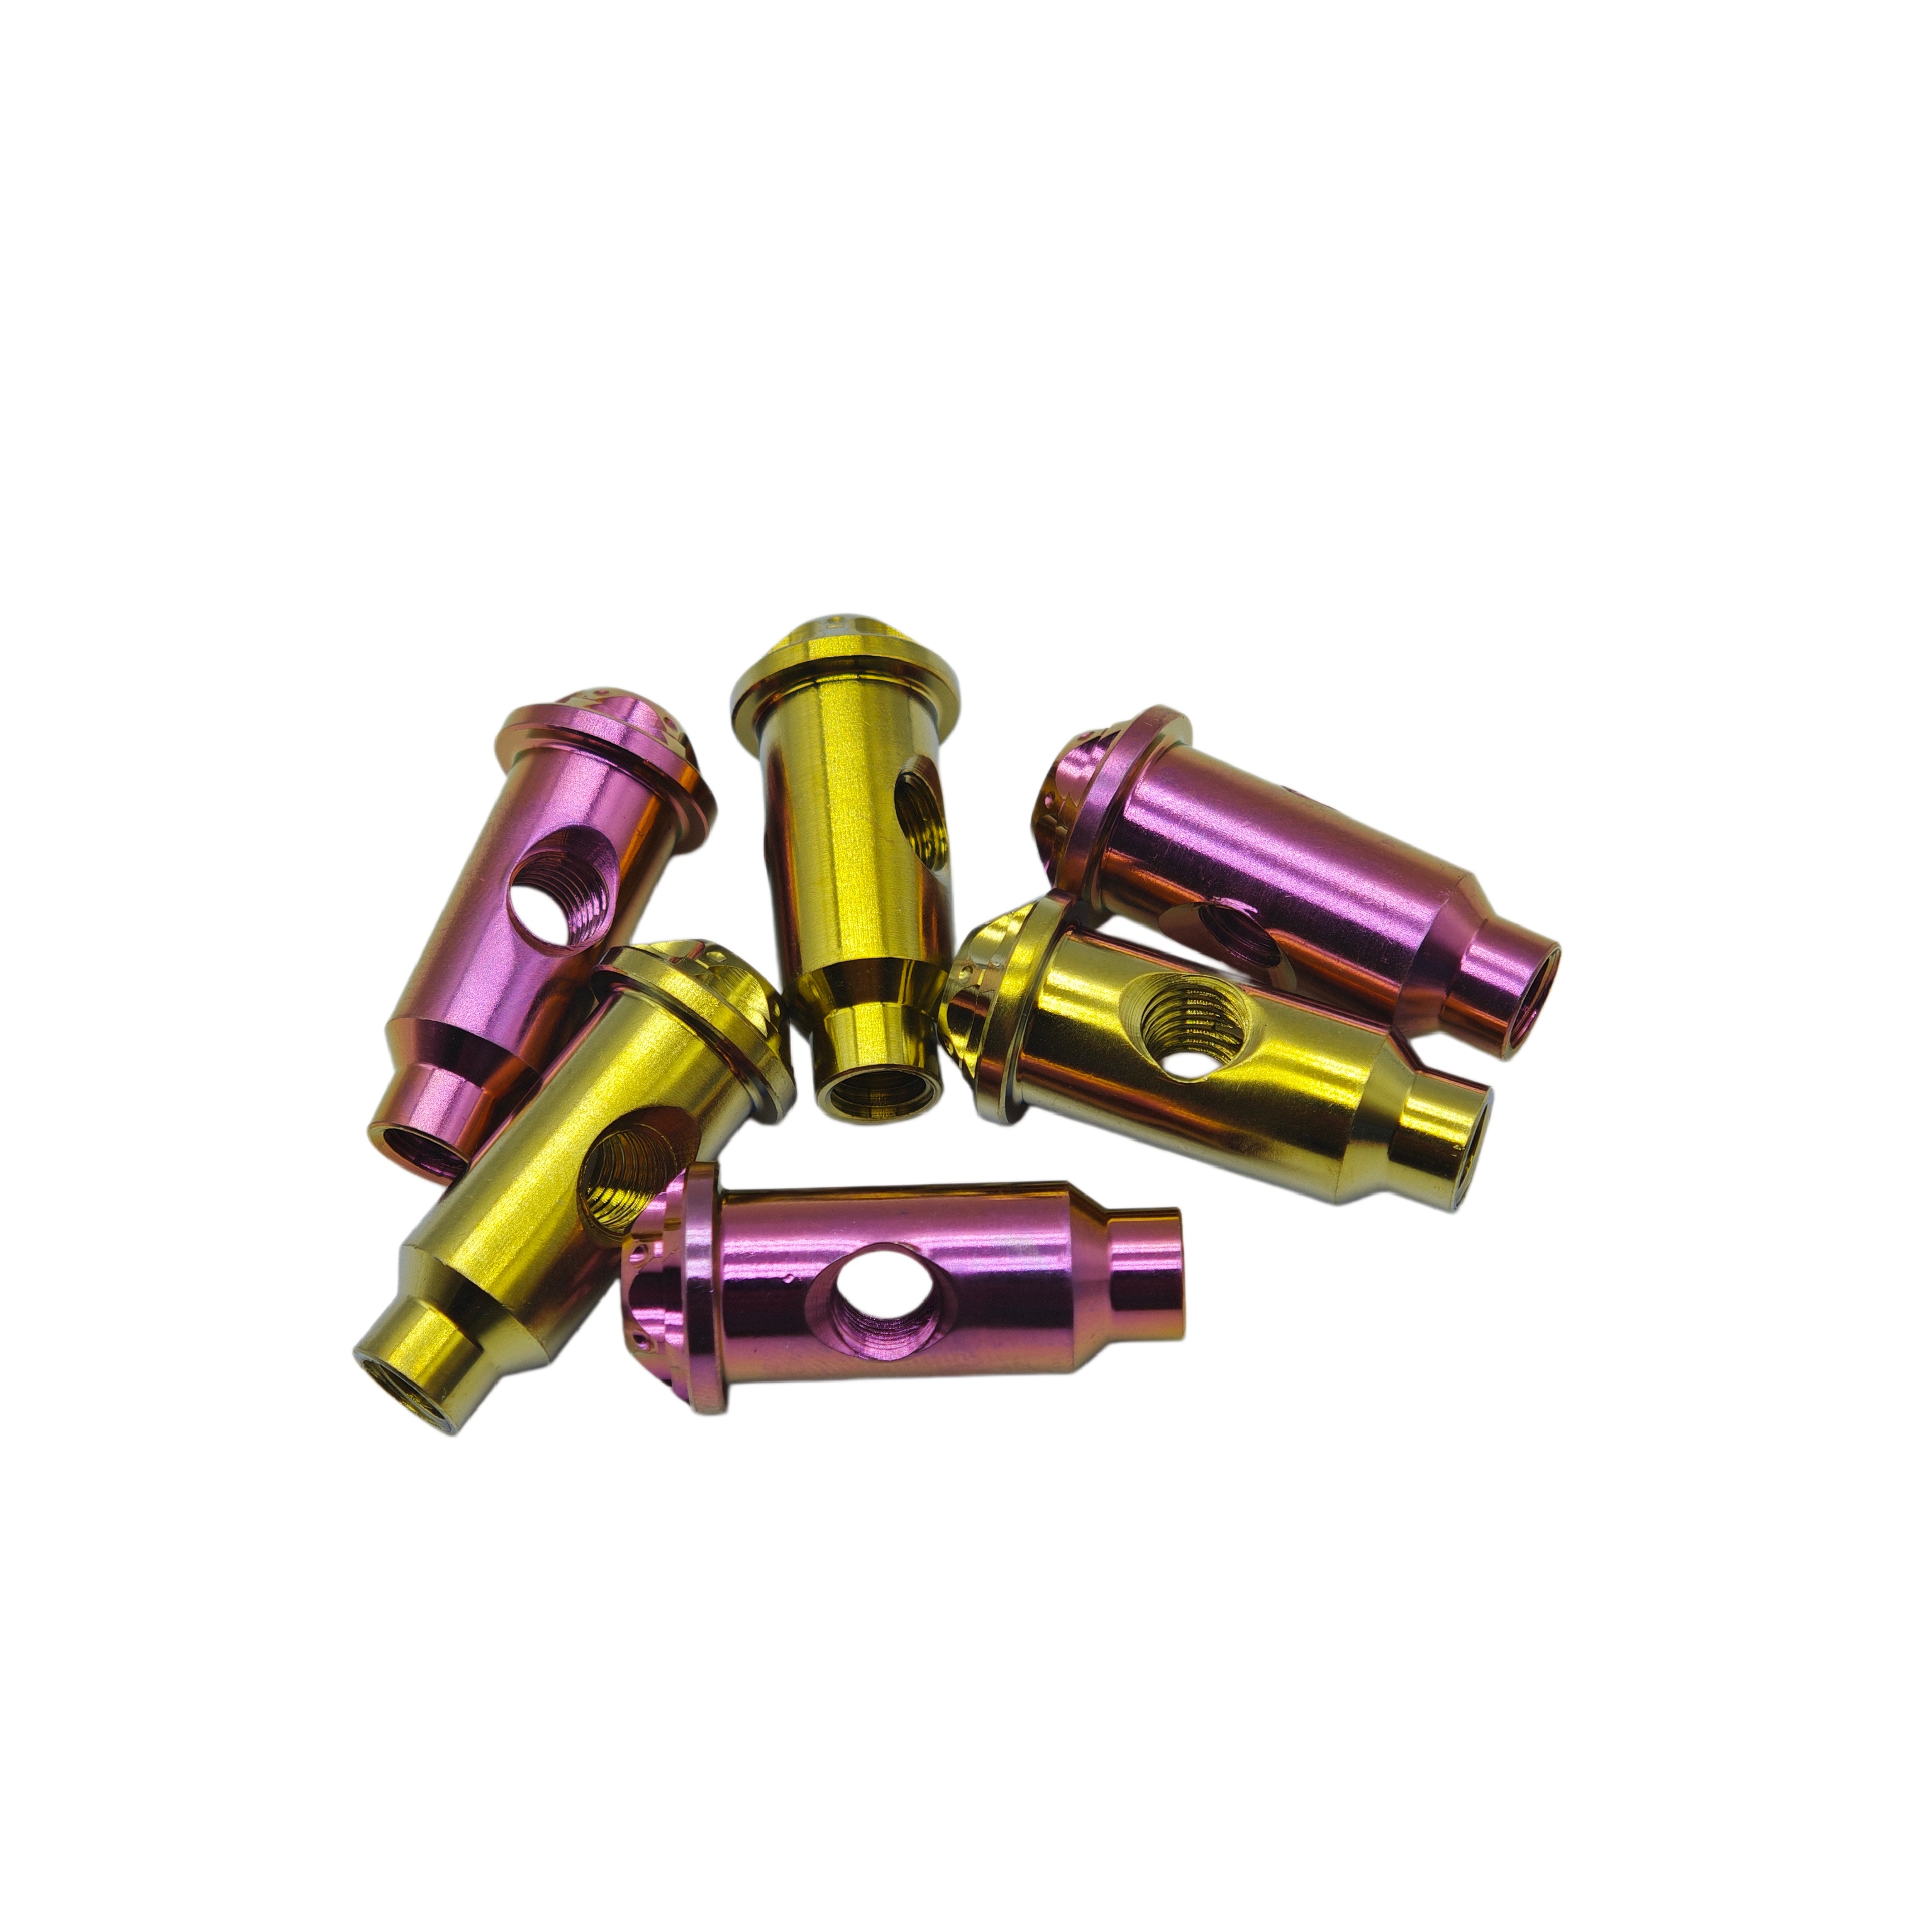
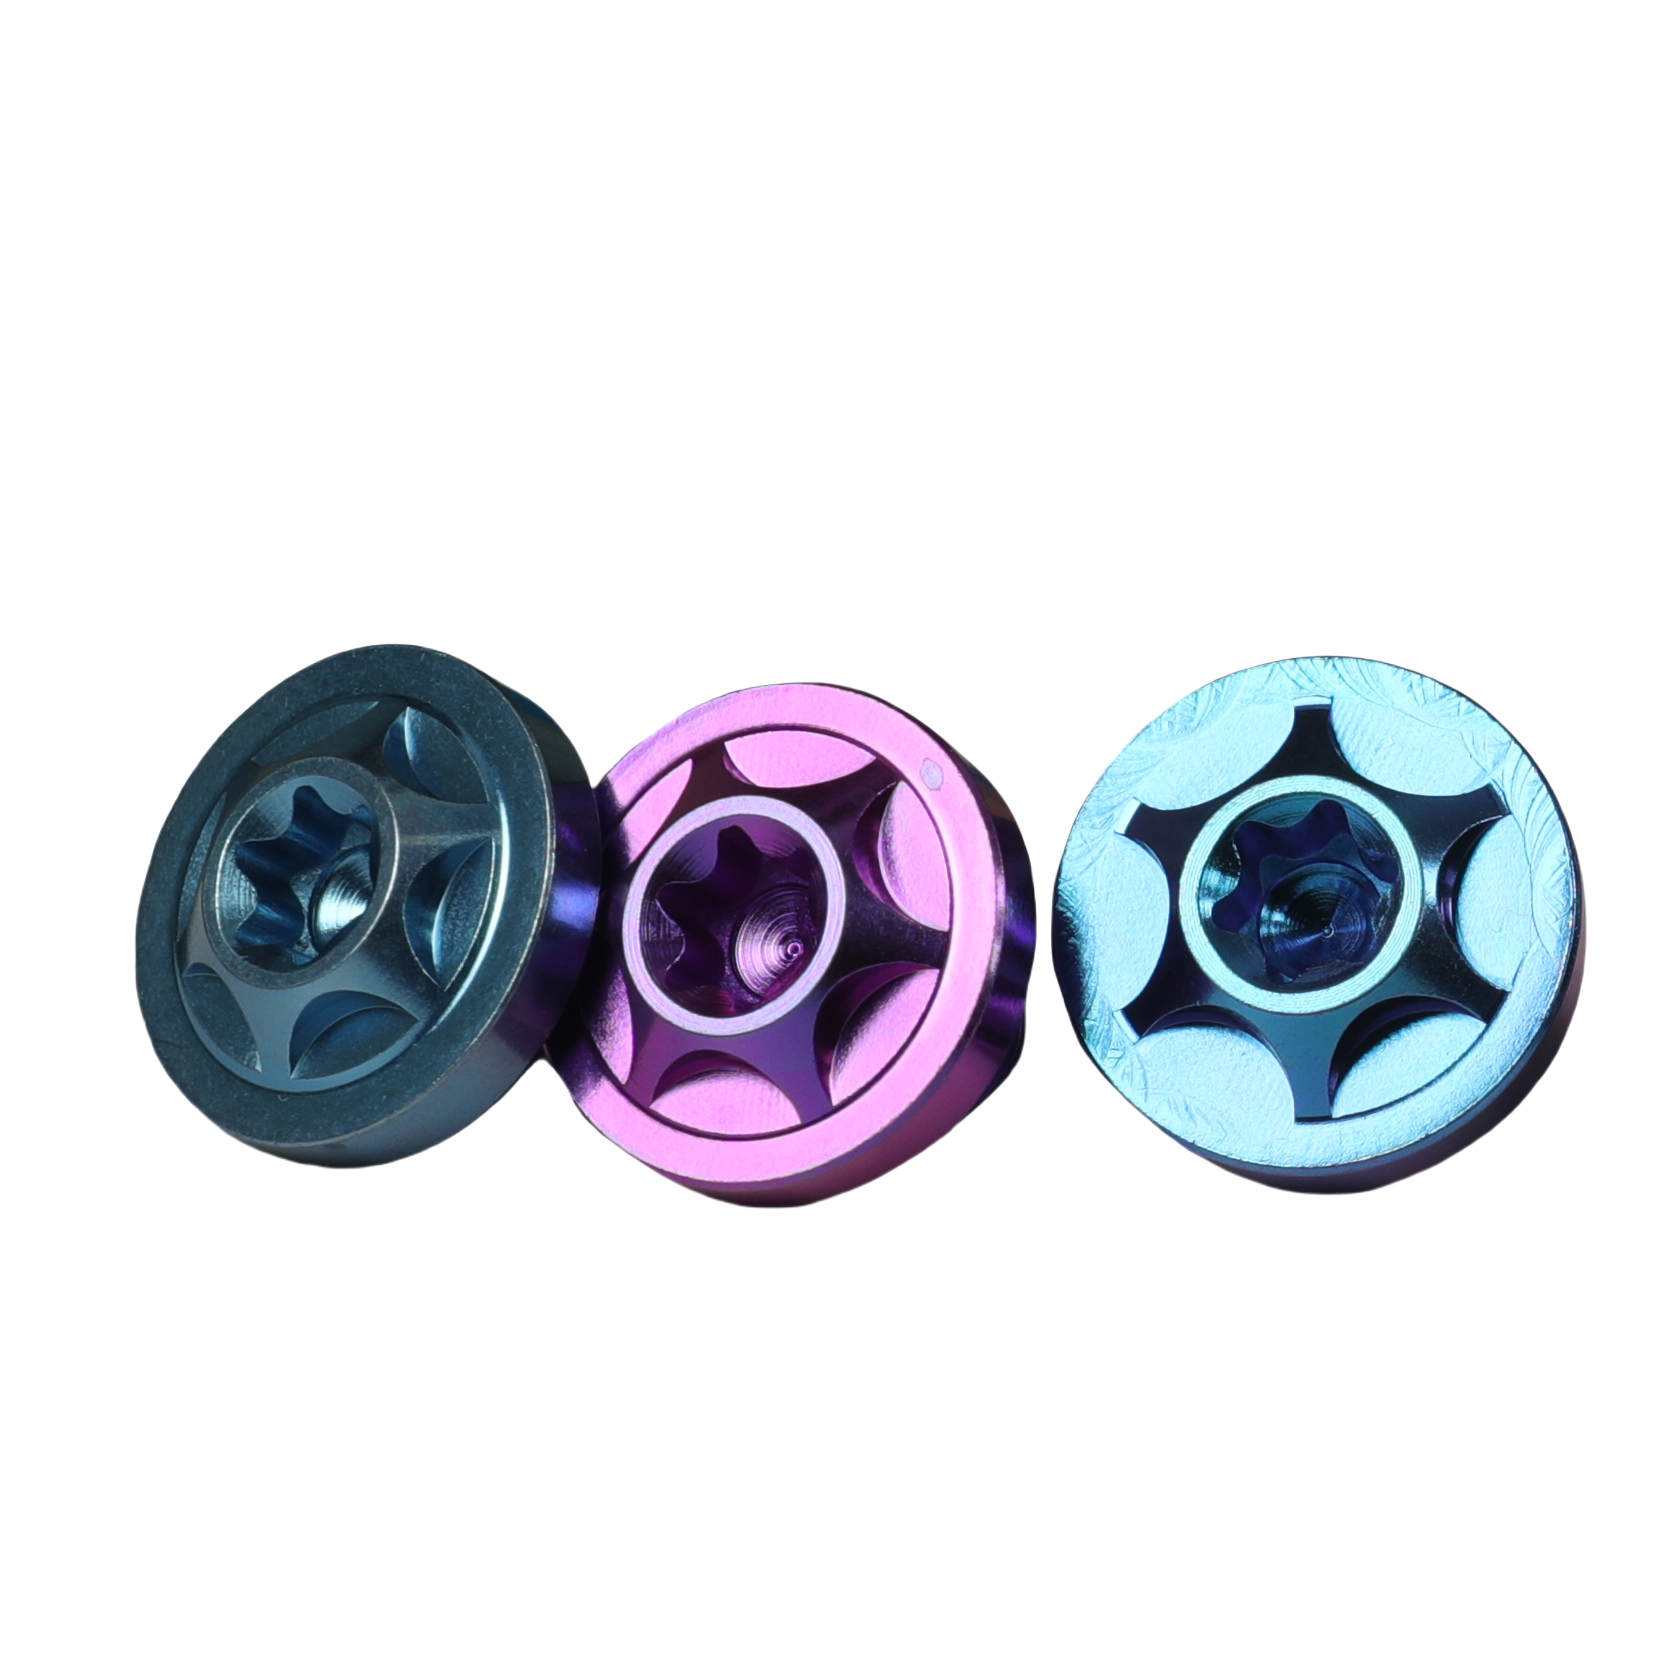
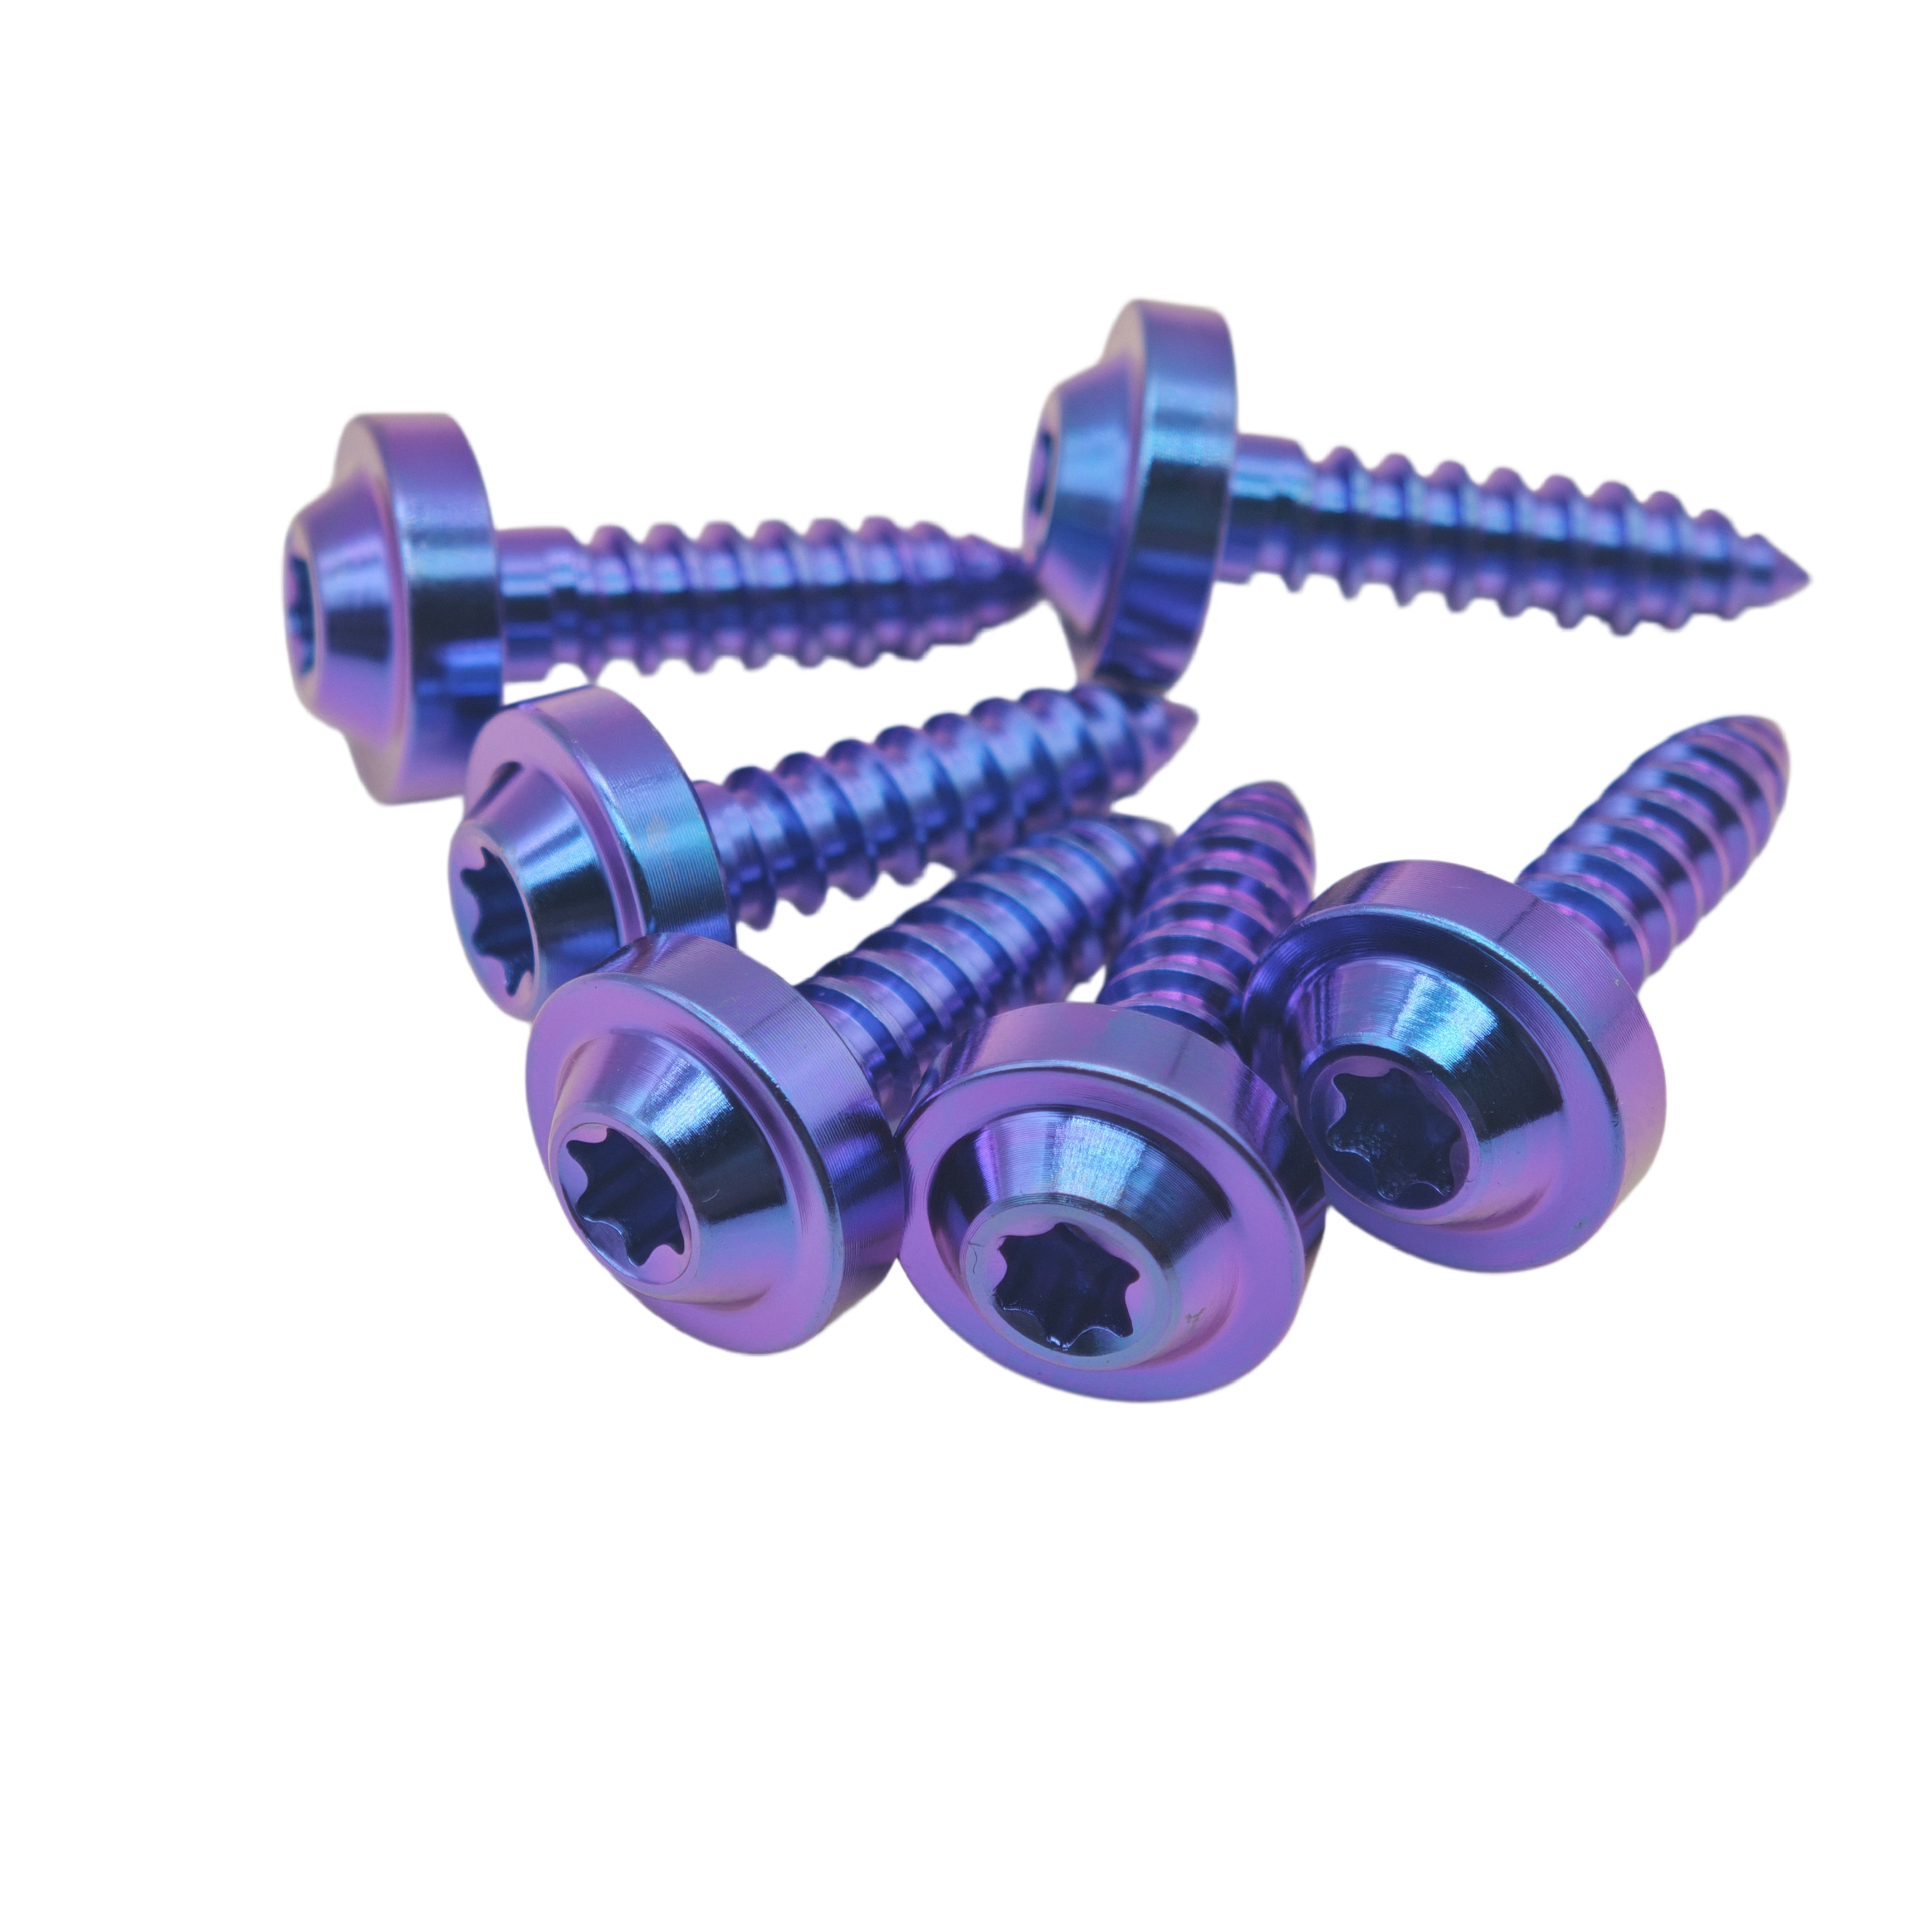
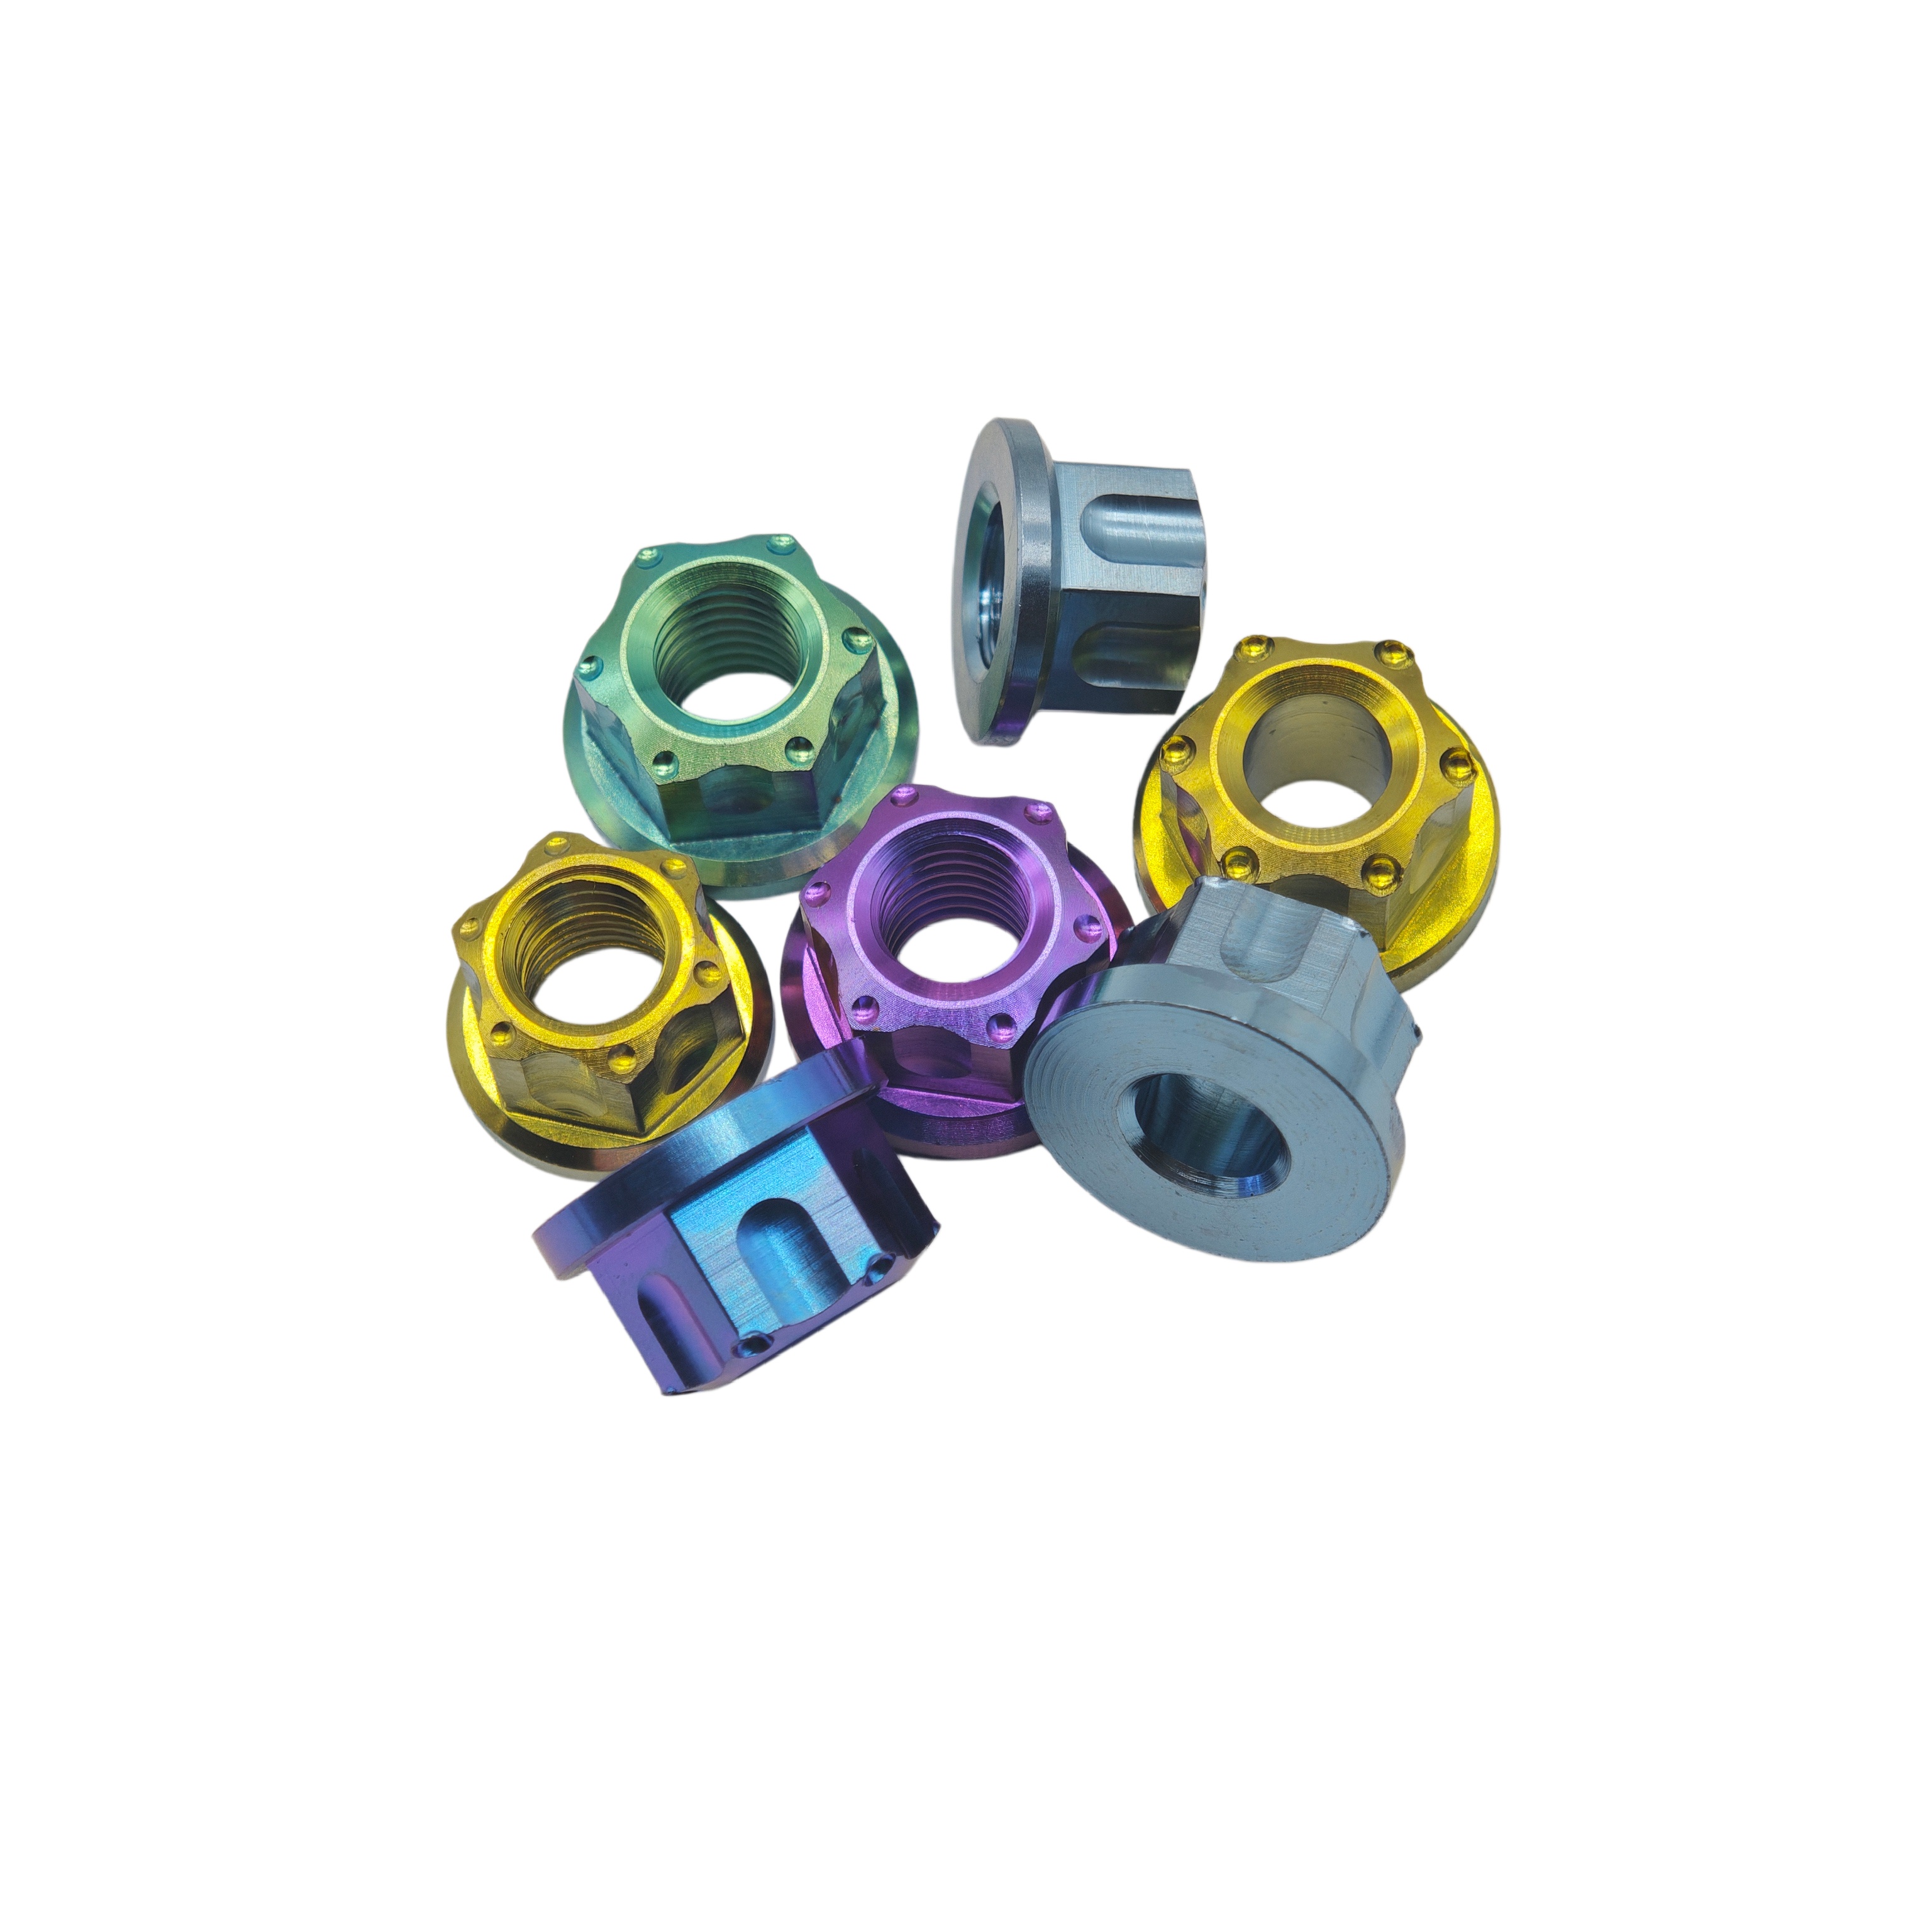
Constructed from certified Ti-6Al-4V aerospace bar stock, cold/hot headed and thread-rolled to deliver superior shear modulus, extreme fatigue cycle thresholds, and total galvanic endurance.
Mechanical Integrity & Metallurgical Superiority of Ti-6Al-4V
In critical aerospace, racing kinematics, and marine chemical assemblies, Grade 5 Titanium (Ti-6Al-4V, UNS R56400, Werkstoff 3.7165) operates as the industrial baseline where steel fasteners fail due to unmanageable reciprocating mass or chloride pitting. Unlike standard cold-headed carbon steel bolts or austenitic A2/A4 stainless fasteners, our CE-certified metric titanium bolts undergo progressive hot-forging heading operations combined with CNC precision turning and cold-rolled thread form generation. Cold-rolling maintains the longitudinal structural grain continuous throughout the thread crests and roots, resulting in a 30% improvement in dynamic fatigue strength and resistance to micro-fissuring under continuous vibrational load.
| Standard Properties | Ti-6Al-4V (Grade 5 Titanium) | A4-80 Stainless Steel | 10.9 Grade Alloy Steel | Al 7075-T6 Alloy |
|---|---|---|---|---|
| Ultimate Tensile Strength | ≥ 895 – 1000 MPa | 800 MPa | 1040 MPa | 570 MPa |
| Yield Strength (0.2% Offset) | ≥ 828 MPa | 600 MPa | 940 MPa | 505 MPa |
| Density & Mass Ratio | 4.43 g/cm³ (44% lighter) | 7.98 g/cm³ | 7.85 g/cm³ | 2.81 g/cm³ |
| Specific Strength (Strength/Density) | 202 kN·m/kg (Class Peak) | 100 kN·m/kg | 132 kN·m/kg | 202 kN·m/kg |
| Corrosion Resistance in Salt Spray | Immune (>3000 hrs ASTM B117) | Moderate / Passivated | Requires Zinc/CAD Coat | Severe Pitting Susceptibility |
| Thermal Operating Window | -196°C to +420°C | -60°C to +300°C | -40°C to +200°C | < 120°C (Softens) |
Future Procurement & Manufacturing Trends in Fastening Systems
How OEMs and Tier-1 procurement offices are recalibrating fastener material bills of materials to achieve carbon reduction, structural optimization, and zero-defect lifecycle targets.
1. E-Mobility & Unsprung Mass Optimization
Global EV OEMs and premium superbike makers are switching rotor bolts, caliper mounts, and subframe anchors to metric Gr5 titanium. Reducing unsprung rotational mass by 44% directly translates to increased battery range, reduced damper inertia, and razor-sharp steering dynamics.
2. PVD Thin-Film Solid-Lubrication Coatings
Traditional titanium anodization is now being supplemented by Physical Vapor Deposition (PVD) Diamond-Like Carbon (DLC) and Titanium Carbo-Nitride (TiCN). This technological migration prevents high-torque galling, lowers friction coefficients (0.10–0.15), and prevents micro-welding in aggressive vibration environments.
3. Traceable Mill Metallurgy (Heat-to-Batch)
Cross-border regulatory mandates in the EU and North America require complete digital material pedigree. Enterprise procurement no longer tolerates generic titanium. Every batch must feature localized EN 10204 Type 3.1 chemical verification to guarantee zero interstitial embrittlement from oxygen or hydrogen pickup.
Factory-Direct Advantages: Baoji Titanium Valley Origin
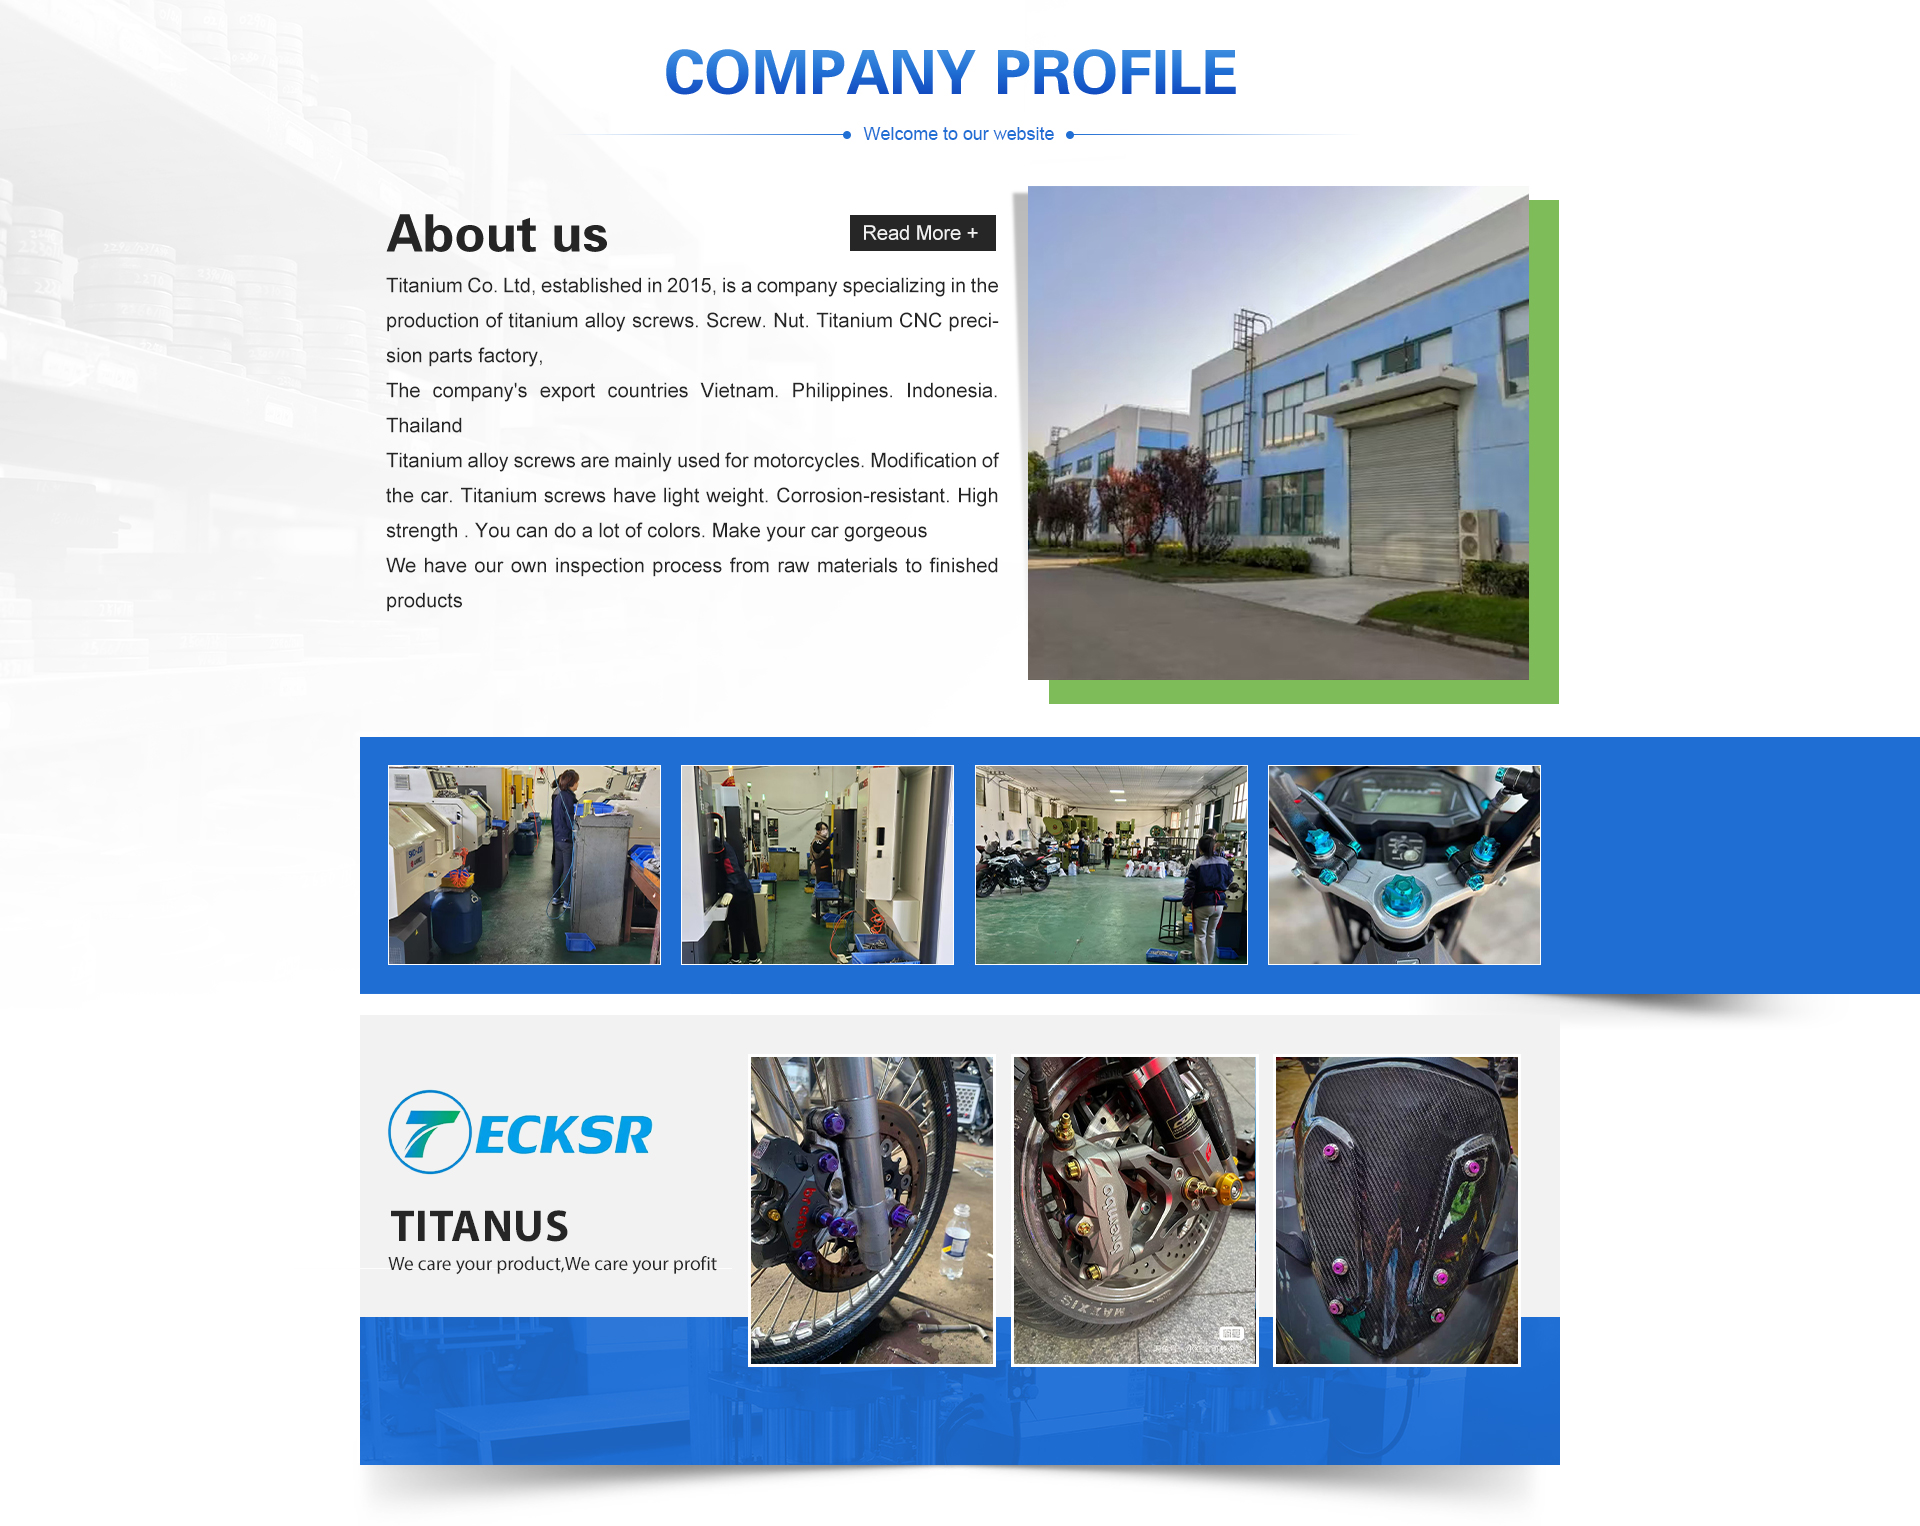
Founded in 2015, Zunvo Titanium operates out of Shiling Road Industrial Park in Baoji—China's undisputed metallurgical capital. Here is how our localized infrastructure safeguards your supply chain.
Primary Smelter Proximity
Direct supply partnerships with adjacent Grade 5 vacuum arc remelting (VAR) ingot mills. We cut raw bar acquisition cycle times by 65% while verifying strict ASTM B348 and AMS 4928 standards.
Multi-Axis CNC Lathes & Thread-Rolling
Equipped with specialized high-torque Swiss turning centers and two-die cylindrical thread rolling machines capable of forming Class 6g/6H threads down to precision tolerances of ±0.005 mm.
Rapid Prototyping in 3 Days
CAD, STEP, and SolidWorks files are verified within 24 hours. Physical custom samples are machined, heat-treated, and color-anodized for express global dispatch in just 72 hours.
100% Comprehensive Quality Control
Every single production batch undergoes Optical Coordinate Measuring (CMM), Rockwell/Vickers hardness validation, Go/No-Go thread pitch testing, and automated optical surface sorting.
Frequently Asked Questions for B2B Fastener Sourcing
Answers to complex metallurgical, logistical, and assembly inquiries faced by technical purchasing managers.
Can Ti-6Al-4V metric bolts safely replace Grade 10.9 and 12.9 high-tensile steel bolts?
Grade 5 Titanium provides a minimum tensile yield of 895–1000 MPa, making it directly equivalent to standard ISO Grade 8.8 and near-grade 10.9 steel. For structural safety-critical locations specified for 12.9 bolts (e.g., severe cyclic shear suspension arms), our engineering team conducts cross-sectional stress recalculations and thread engagement evaluations before certifying the replacement.
How do you mitigate thread galling and cold welding during high-torque assembly?
Titanium self-forms a tenacious passivating oxide film that can cause micro-frictional galling against matching internal threads under high torque. We prevent this by providing precision rolled threads with micro-polished root radii, optional PVD dry-film lubricating coatings (DLC/MoS2), and certified anti-seize copper/nickel assembly compound application procedures.
What is the standard chemical analysis and test documentation supplied per order?
Every delivery includes an EN 10204 3.1 Inspection Certificate declaring exact chemical composition (Titanium balance, 5.5–6.75% Aluminum, 3.5–4.5% Vanadium, max 0.20% Oxygen, max 0.08% Carbon), accompanied by yield strength, elongation percentage, charpy impact values, and dimensional verification reports.
What are your manufacturing minimum order quantities (MOQ) and production lead times?
For off-the-shelf standard DIN 912, DIN 933, and Torx flange bolts, stock is ready for same-day dispatch (100-piece parcels). For custom OEM drawing specifications, tooling and prototypes complete within 3–5 working days, with mass volumes produced within 12–18 days shipped door-to-door globally via DHL, FedEx, UPS, or sea consolidation.
Connect Directly with Our Titanium Fastener Engineering Team
Send your CAD drawing, DIN/ISO specification, or torque requirements. Our metallurgists and pricing analysts review all industrial inquiries within 7 hours with complete volume pricing.
