Featured Titanium Sprocket & Precision Fastener Solutions
Direct factory configurations featuring hot-forged heads, precision CNC machined shank reliefs, rolled M8/M10 threads, and PVD/Anodized surface hardening.
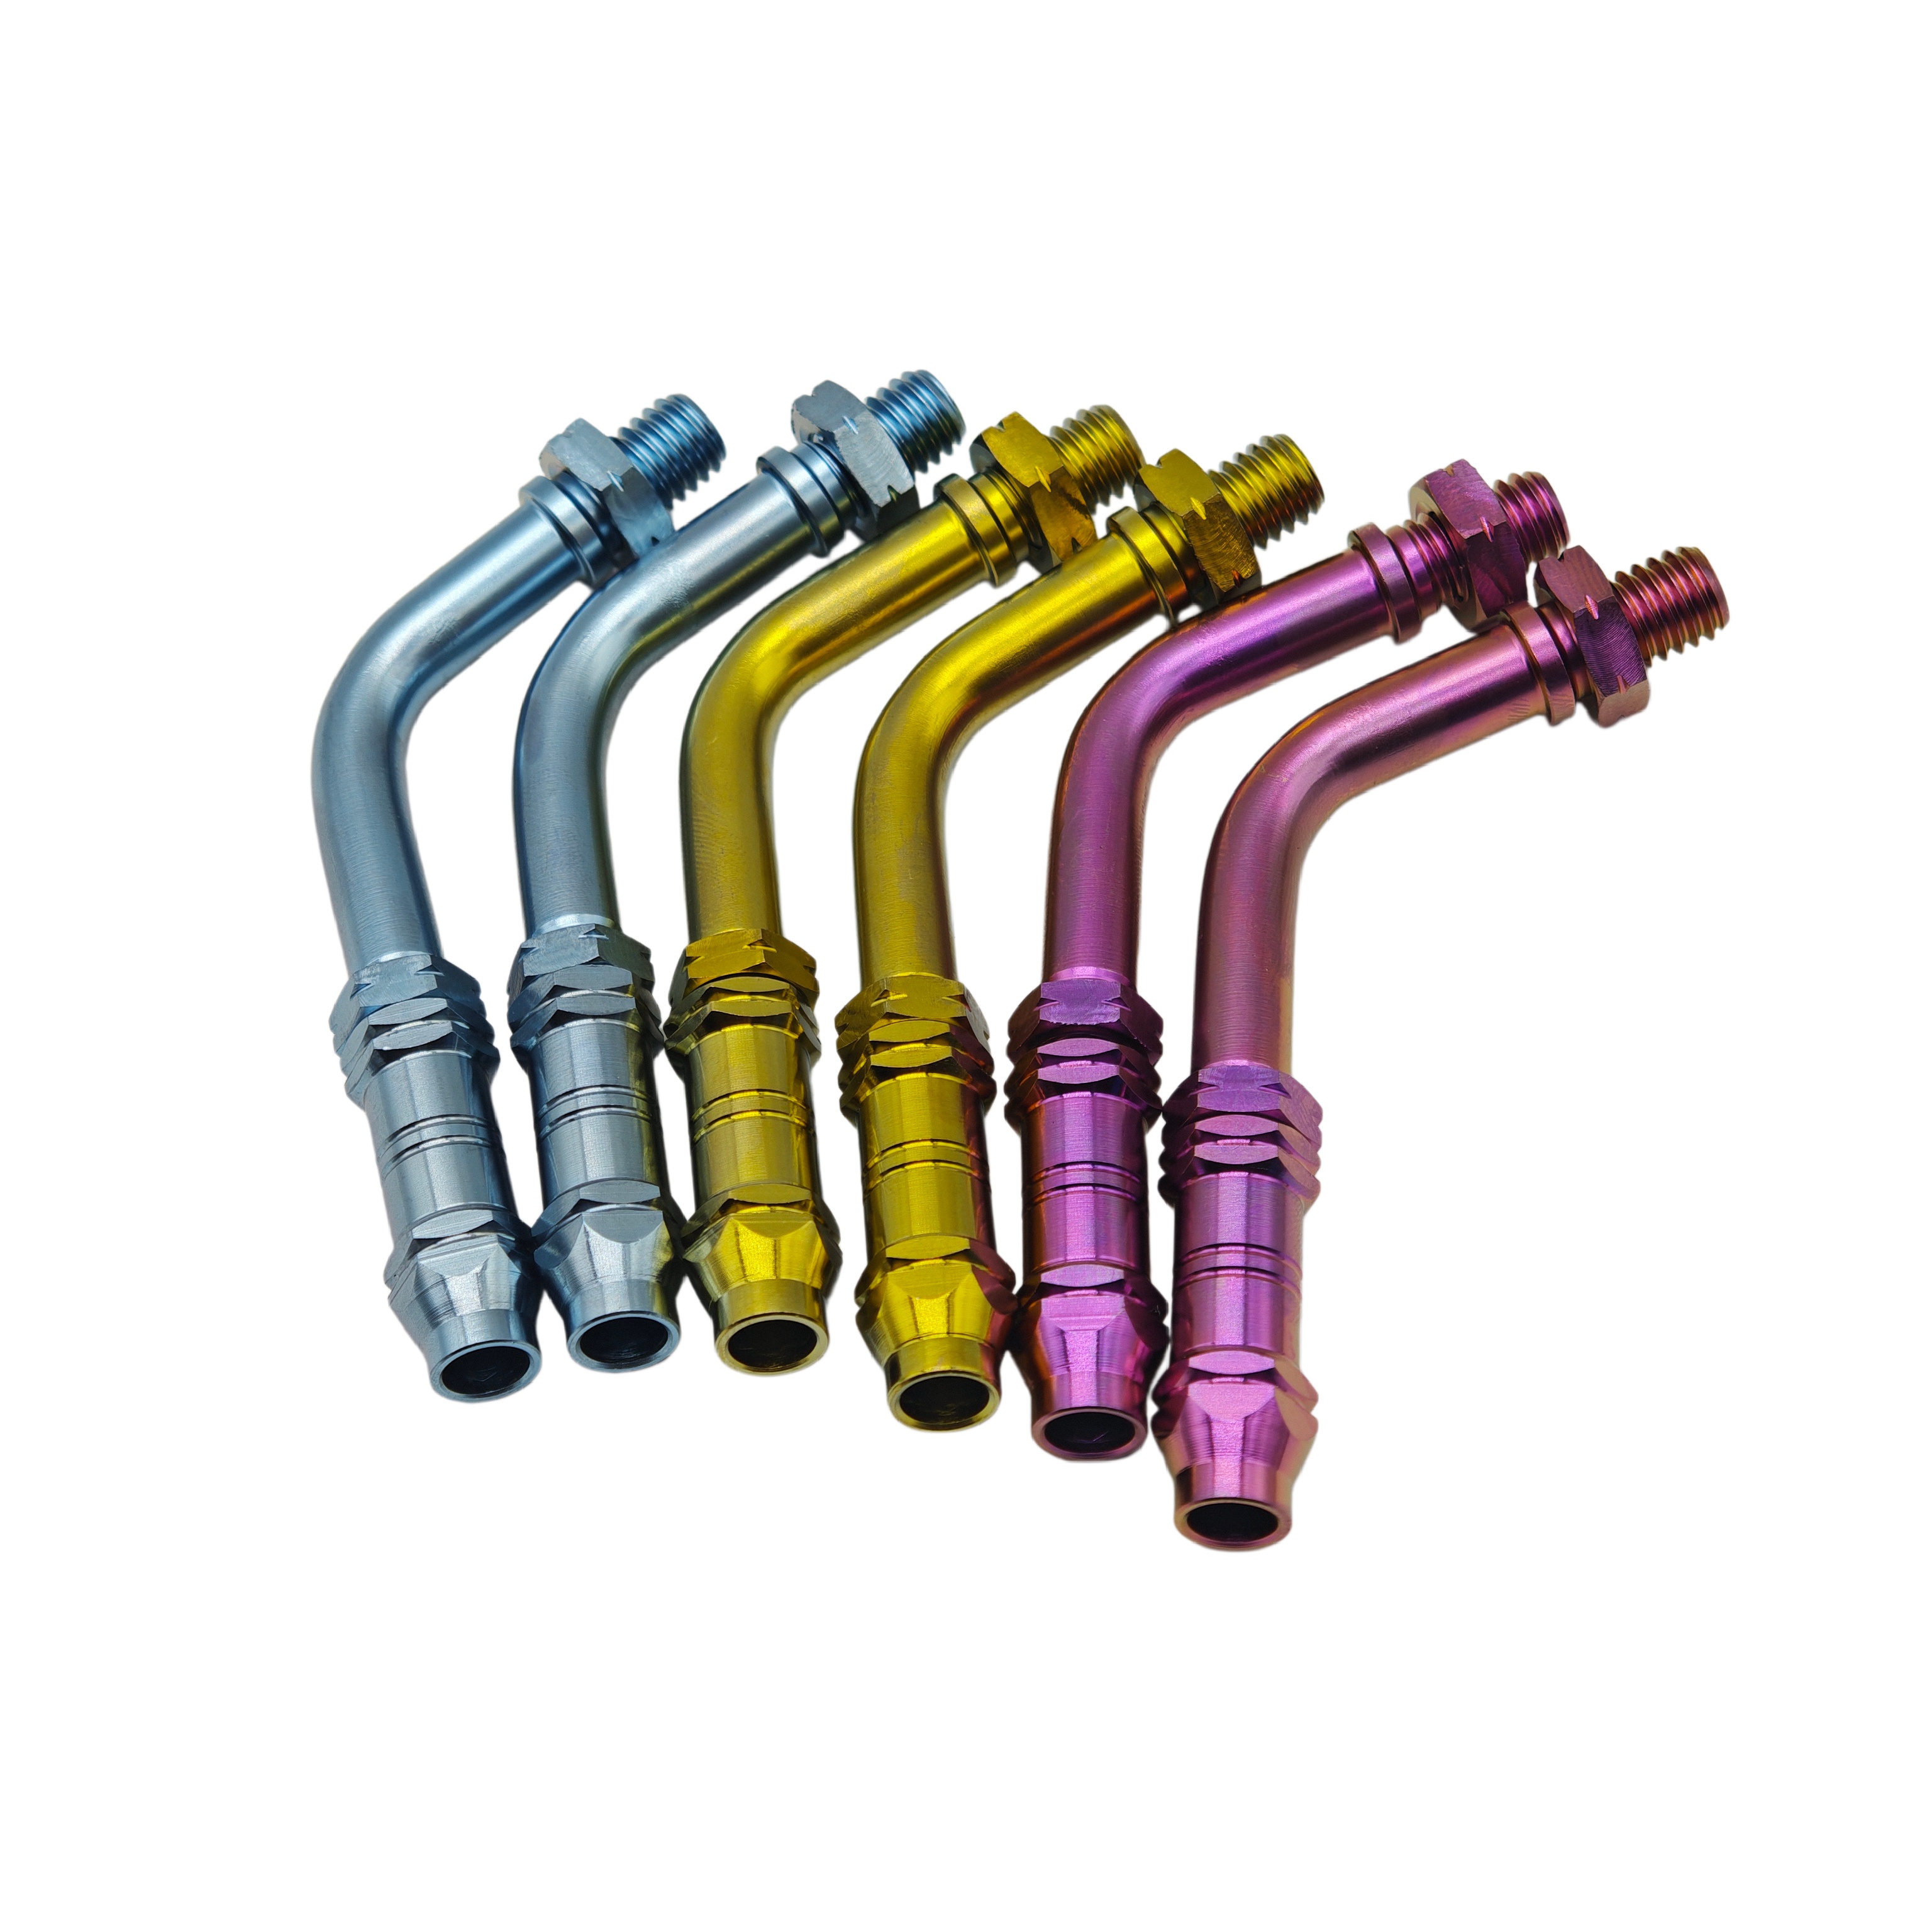
Factory M10 CNC 90-Degree Hex Flange Head GR5 Titanium Plain Wire Cable Adjuster
High-precision 90° throttle and clutch adjuster machined from certified solid Grade 5 titanium billet. Plain finish with clean threads.
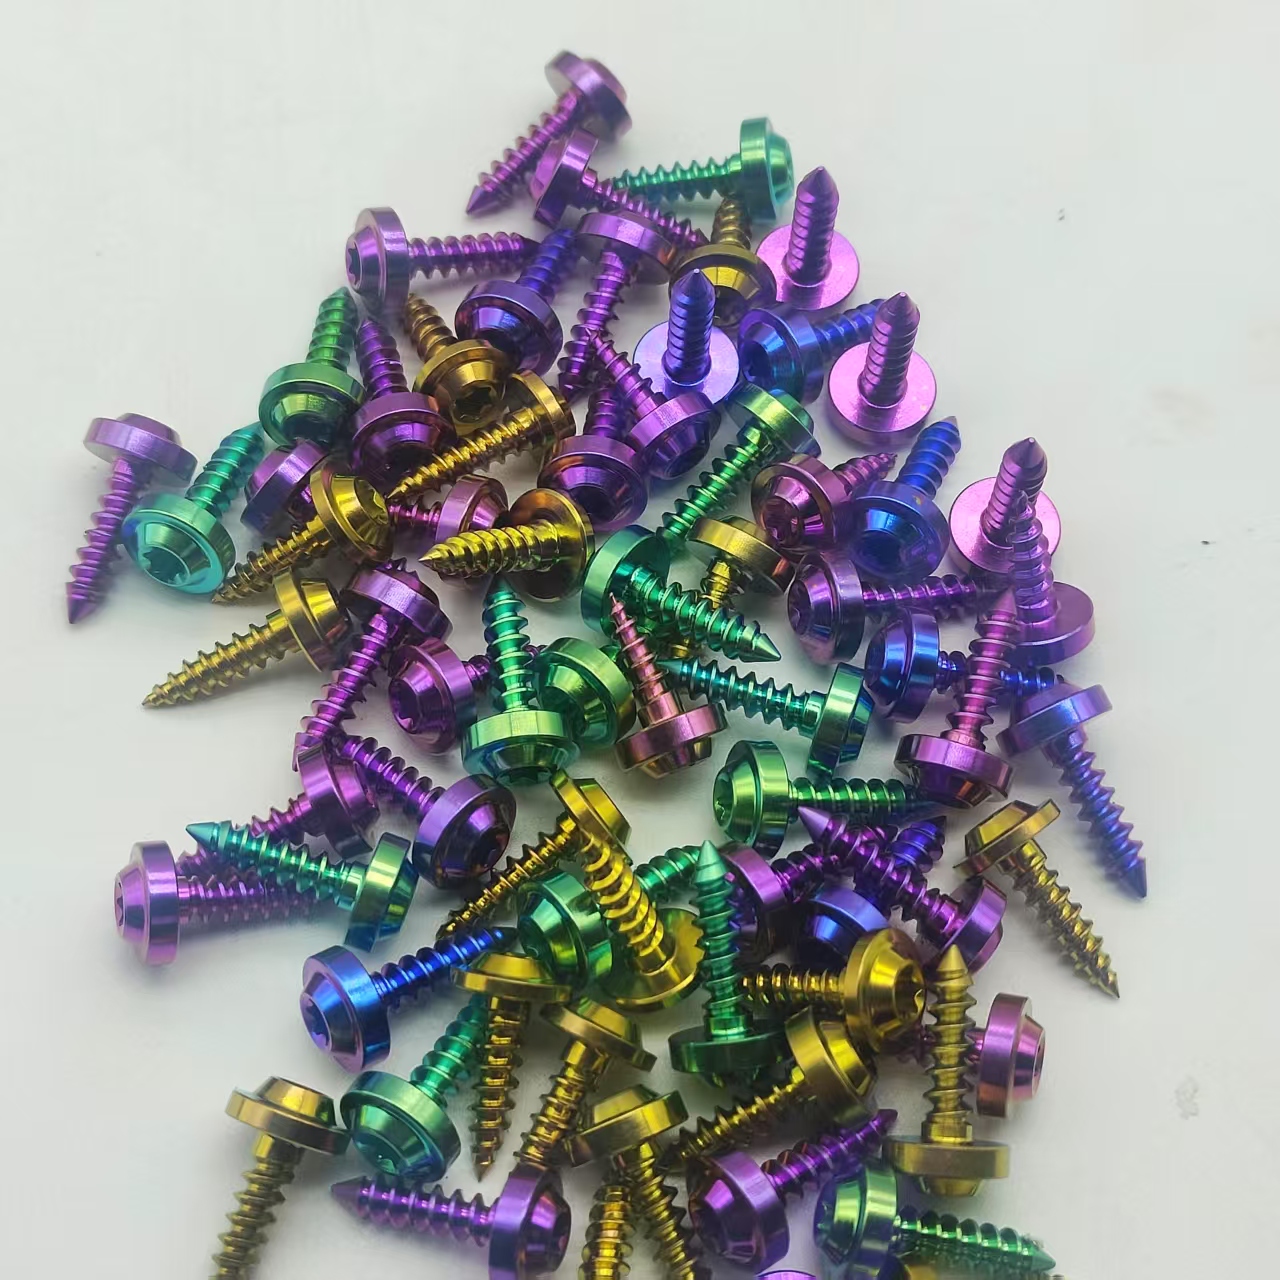
High Strength M4-M5 Titanium Alloy Torx Head Self-Tapping Screws Hex Washer Head
Torx drive with integral flange washer design. Anodized and PVD colored coatings engineered for fairings and auxiliary covers.
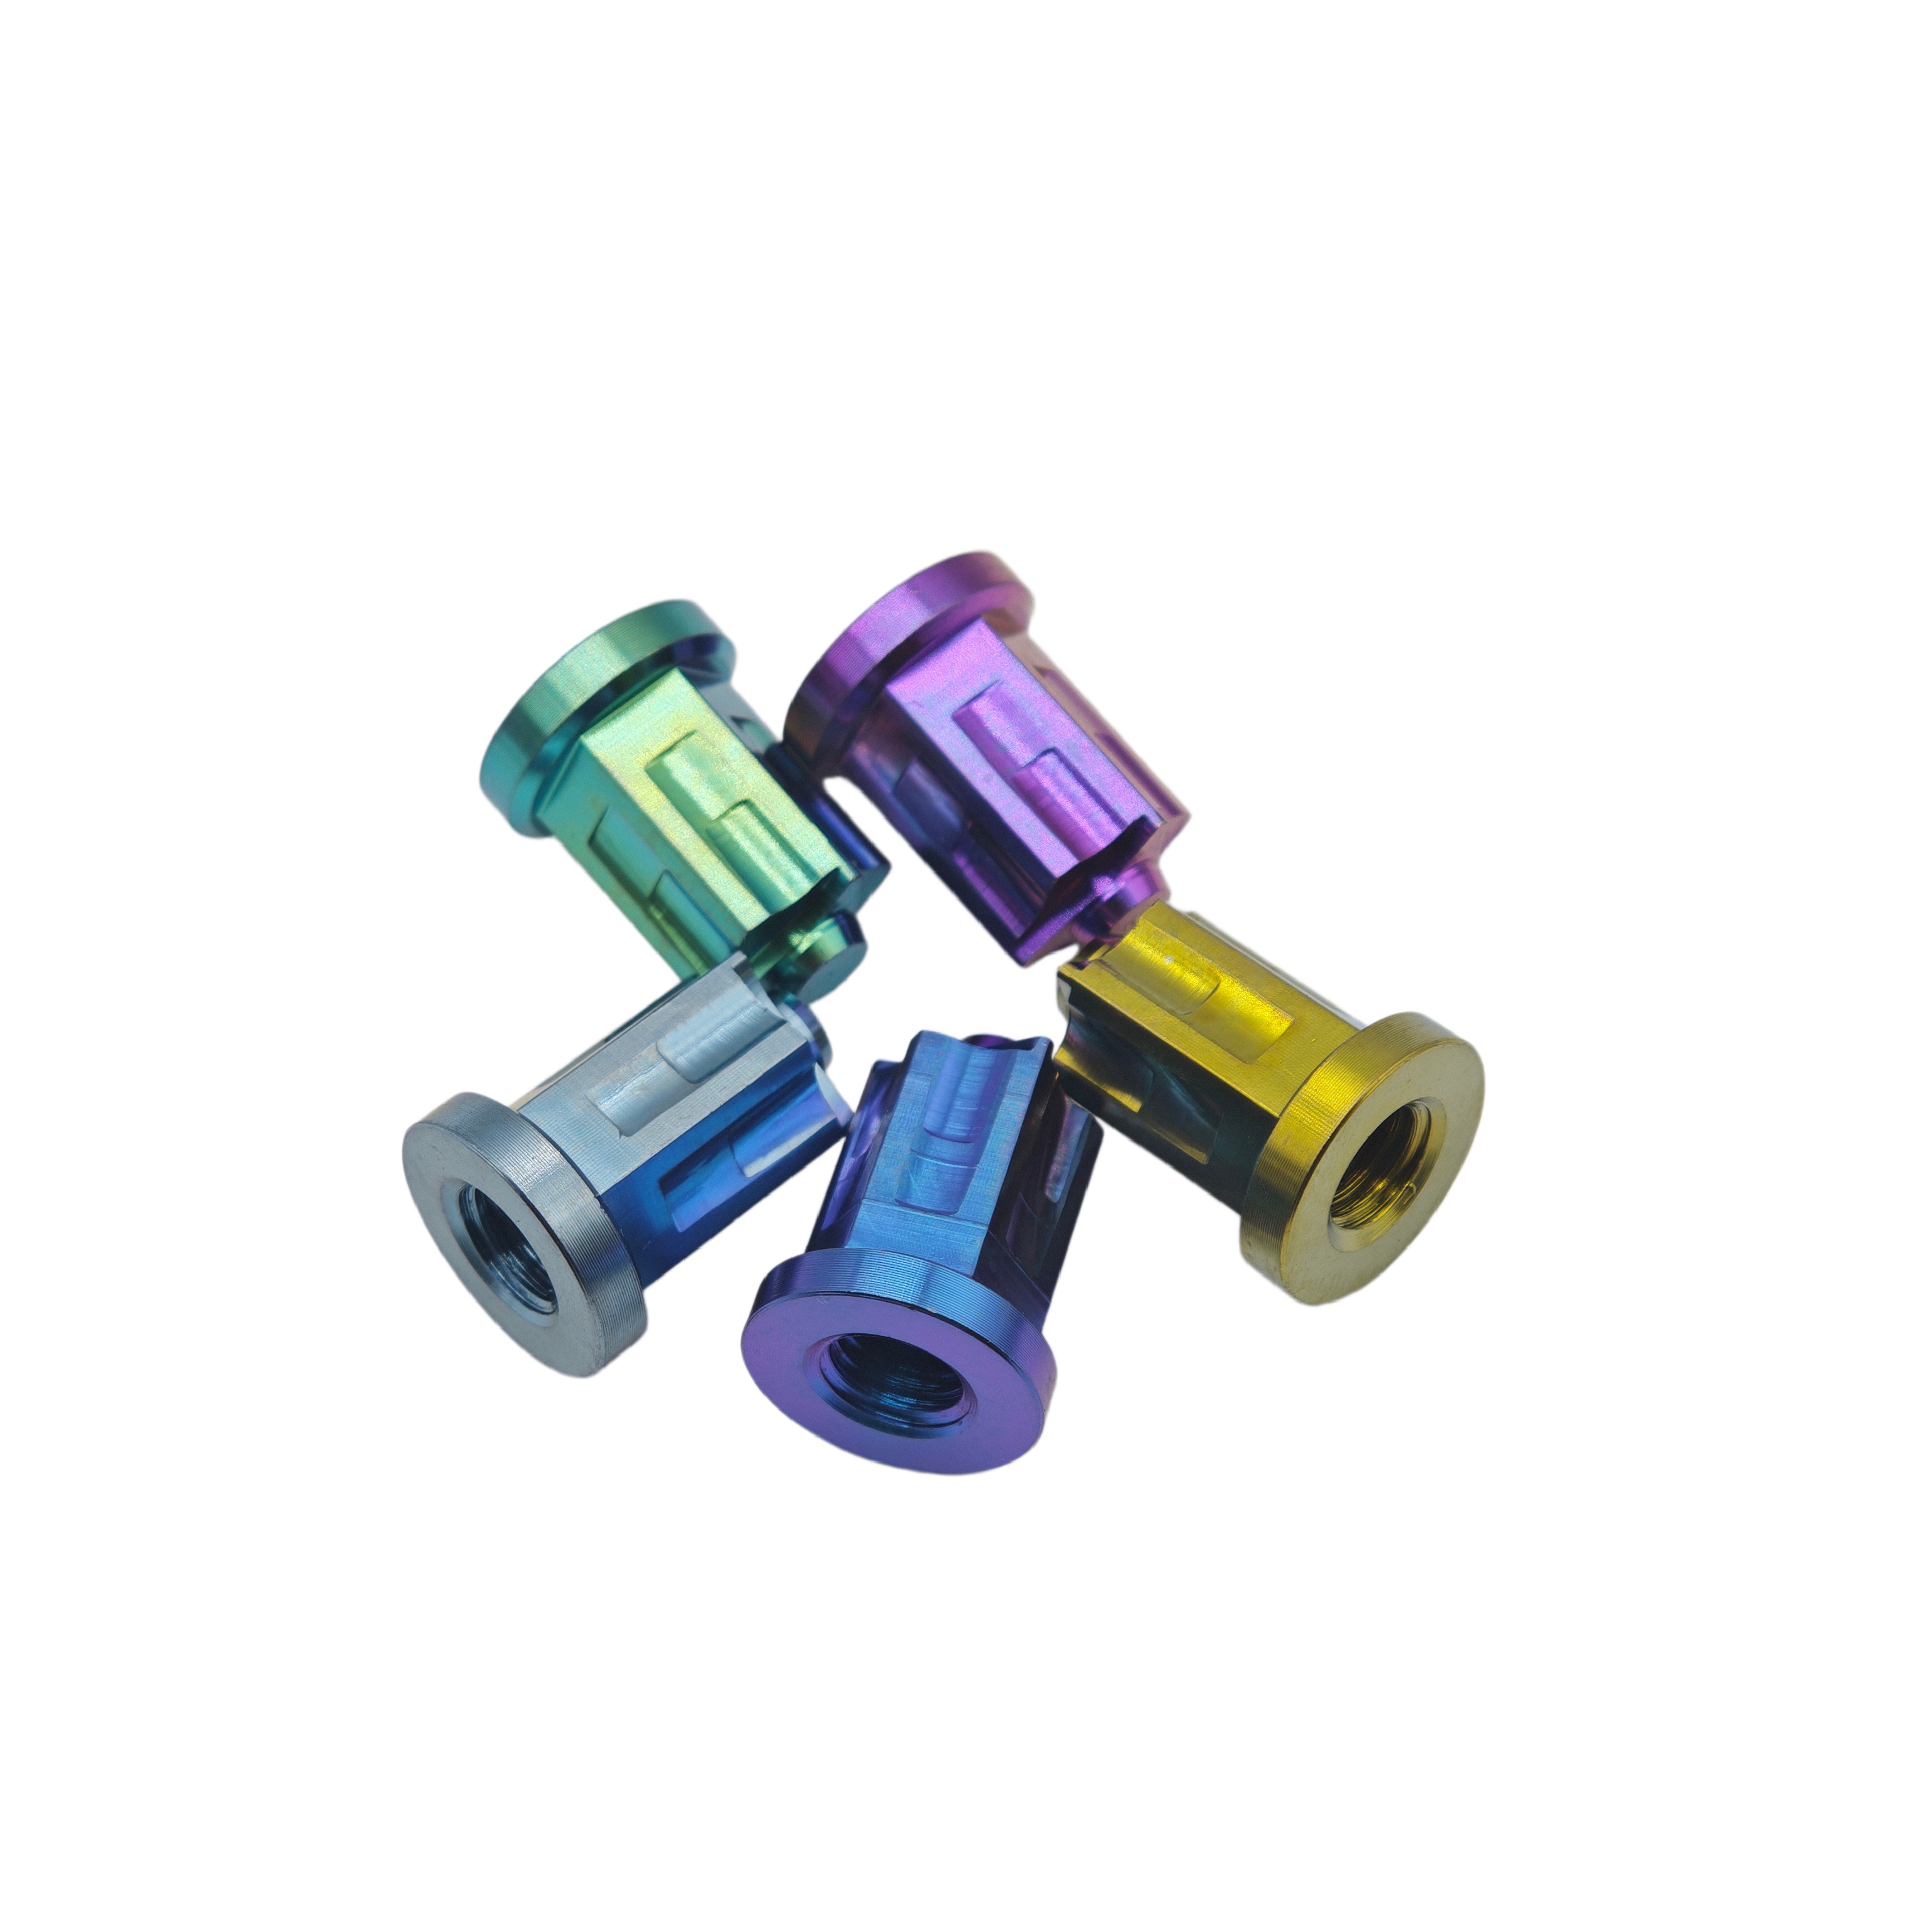
Tecksr Titanium Alloy Hex Head French-style Closed Flower Nuts Class 10 GR5
Closed ornamental flower nut for rear axle blocks and sprocket studs. Class 10 mechanical strength with enclosed thread protection.
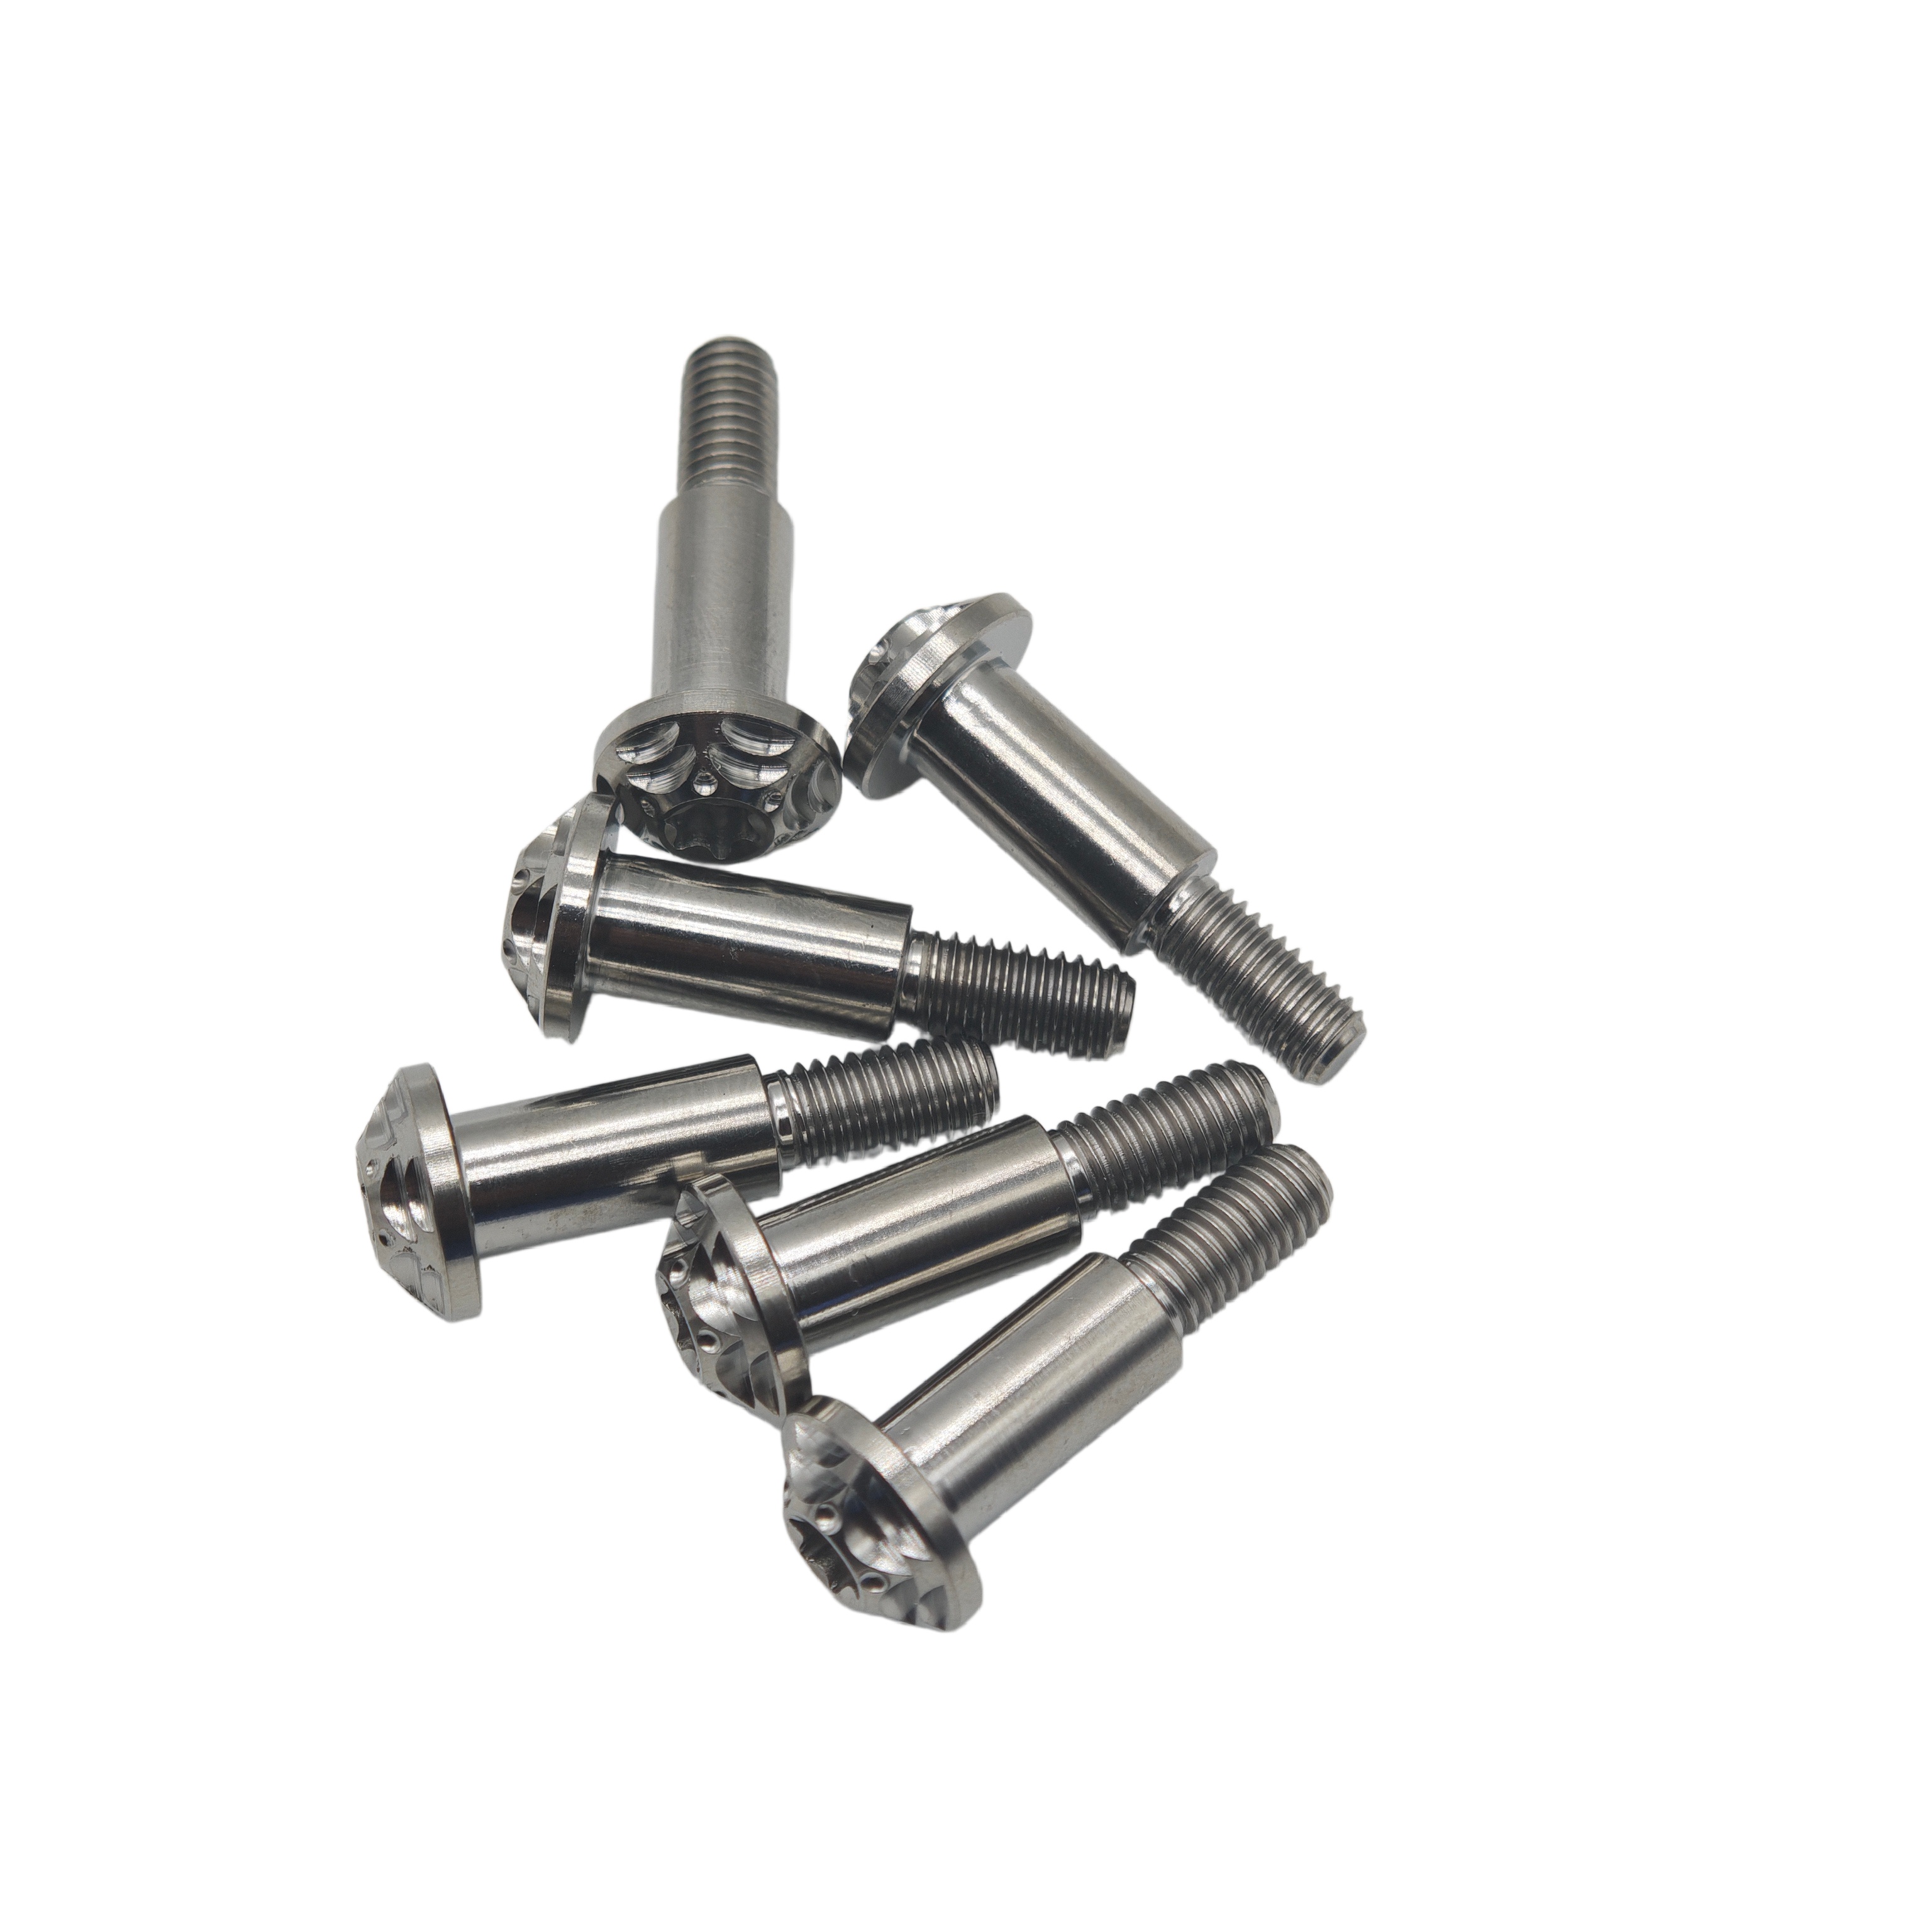
Custom Torx Shoulder Screw CNC Machined GR5 Titanium Socket Head Decorative Bolt
Ground shoulder tolerance (±0.005mm) for linkage pivots and sprocket dust ring spacers. Low cam-out Torx socket interface.
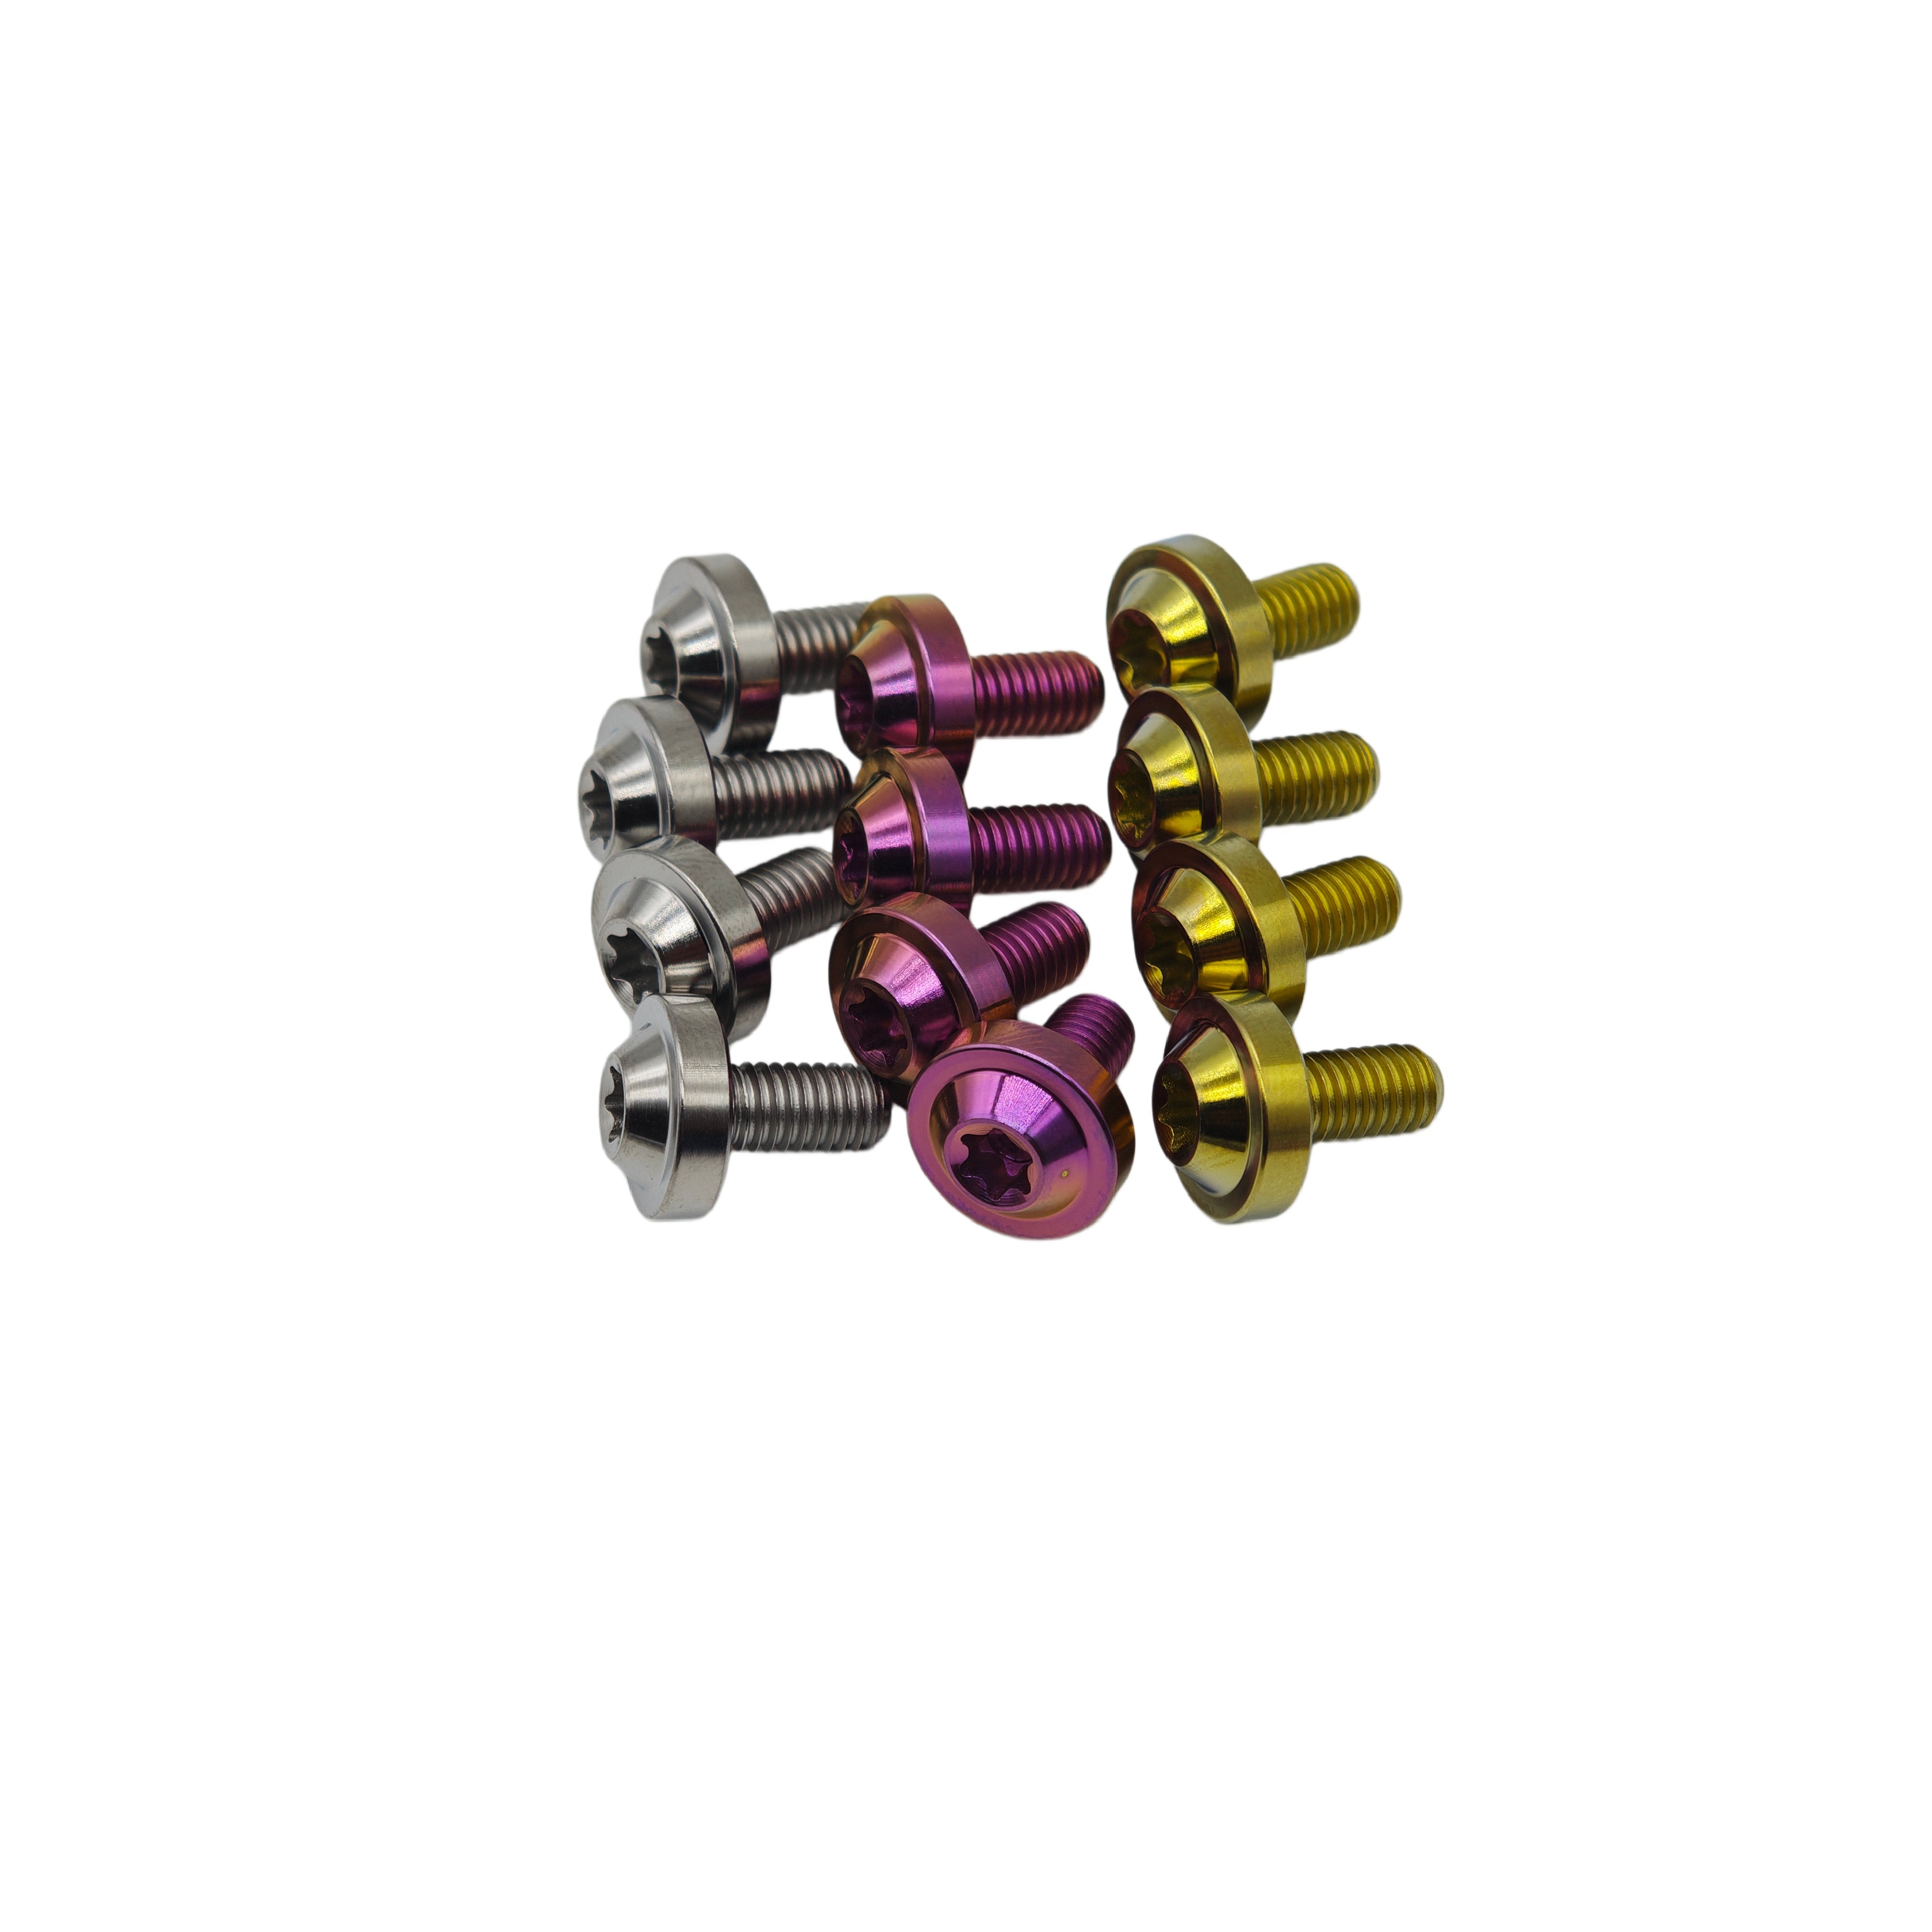
Custom GR5 Titanium M8 Disc Head Bolts with Plain Finish for Bike Motorcycle
Low-profile broad disc head distributing clamping pressure across rear sprockets and brake rotors. High shear tensile stability.
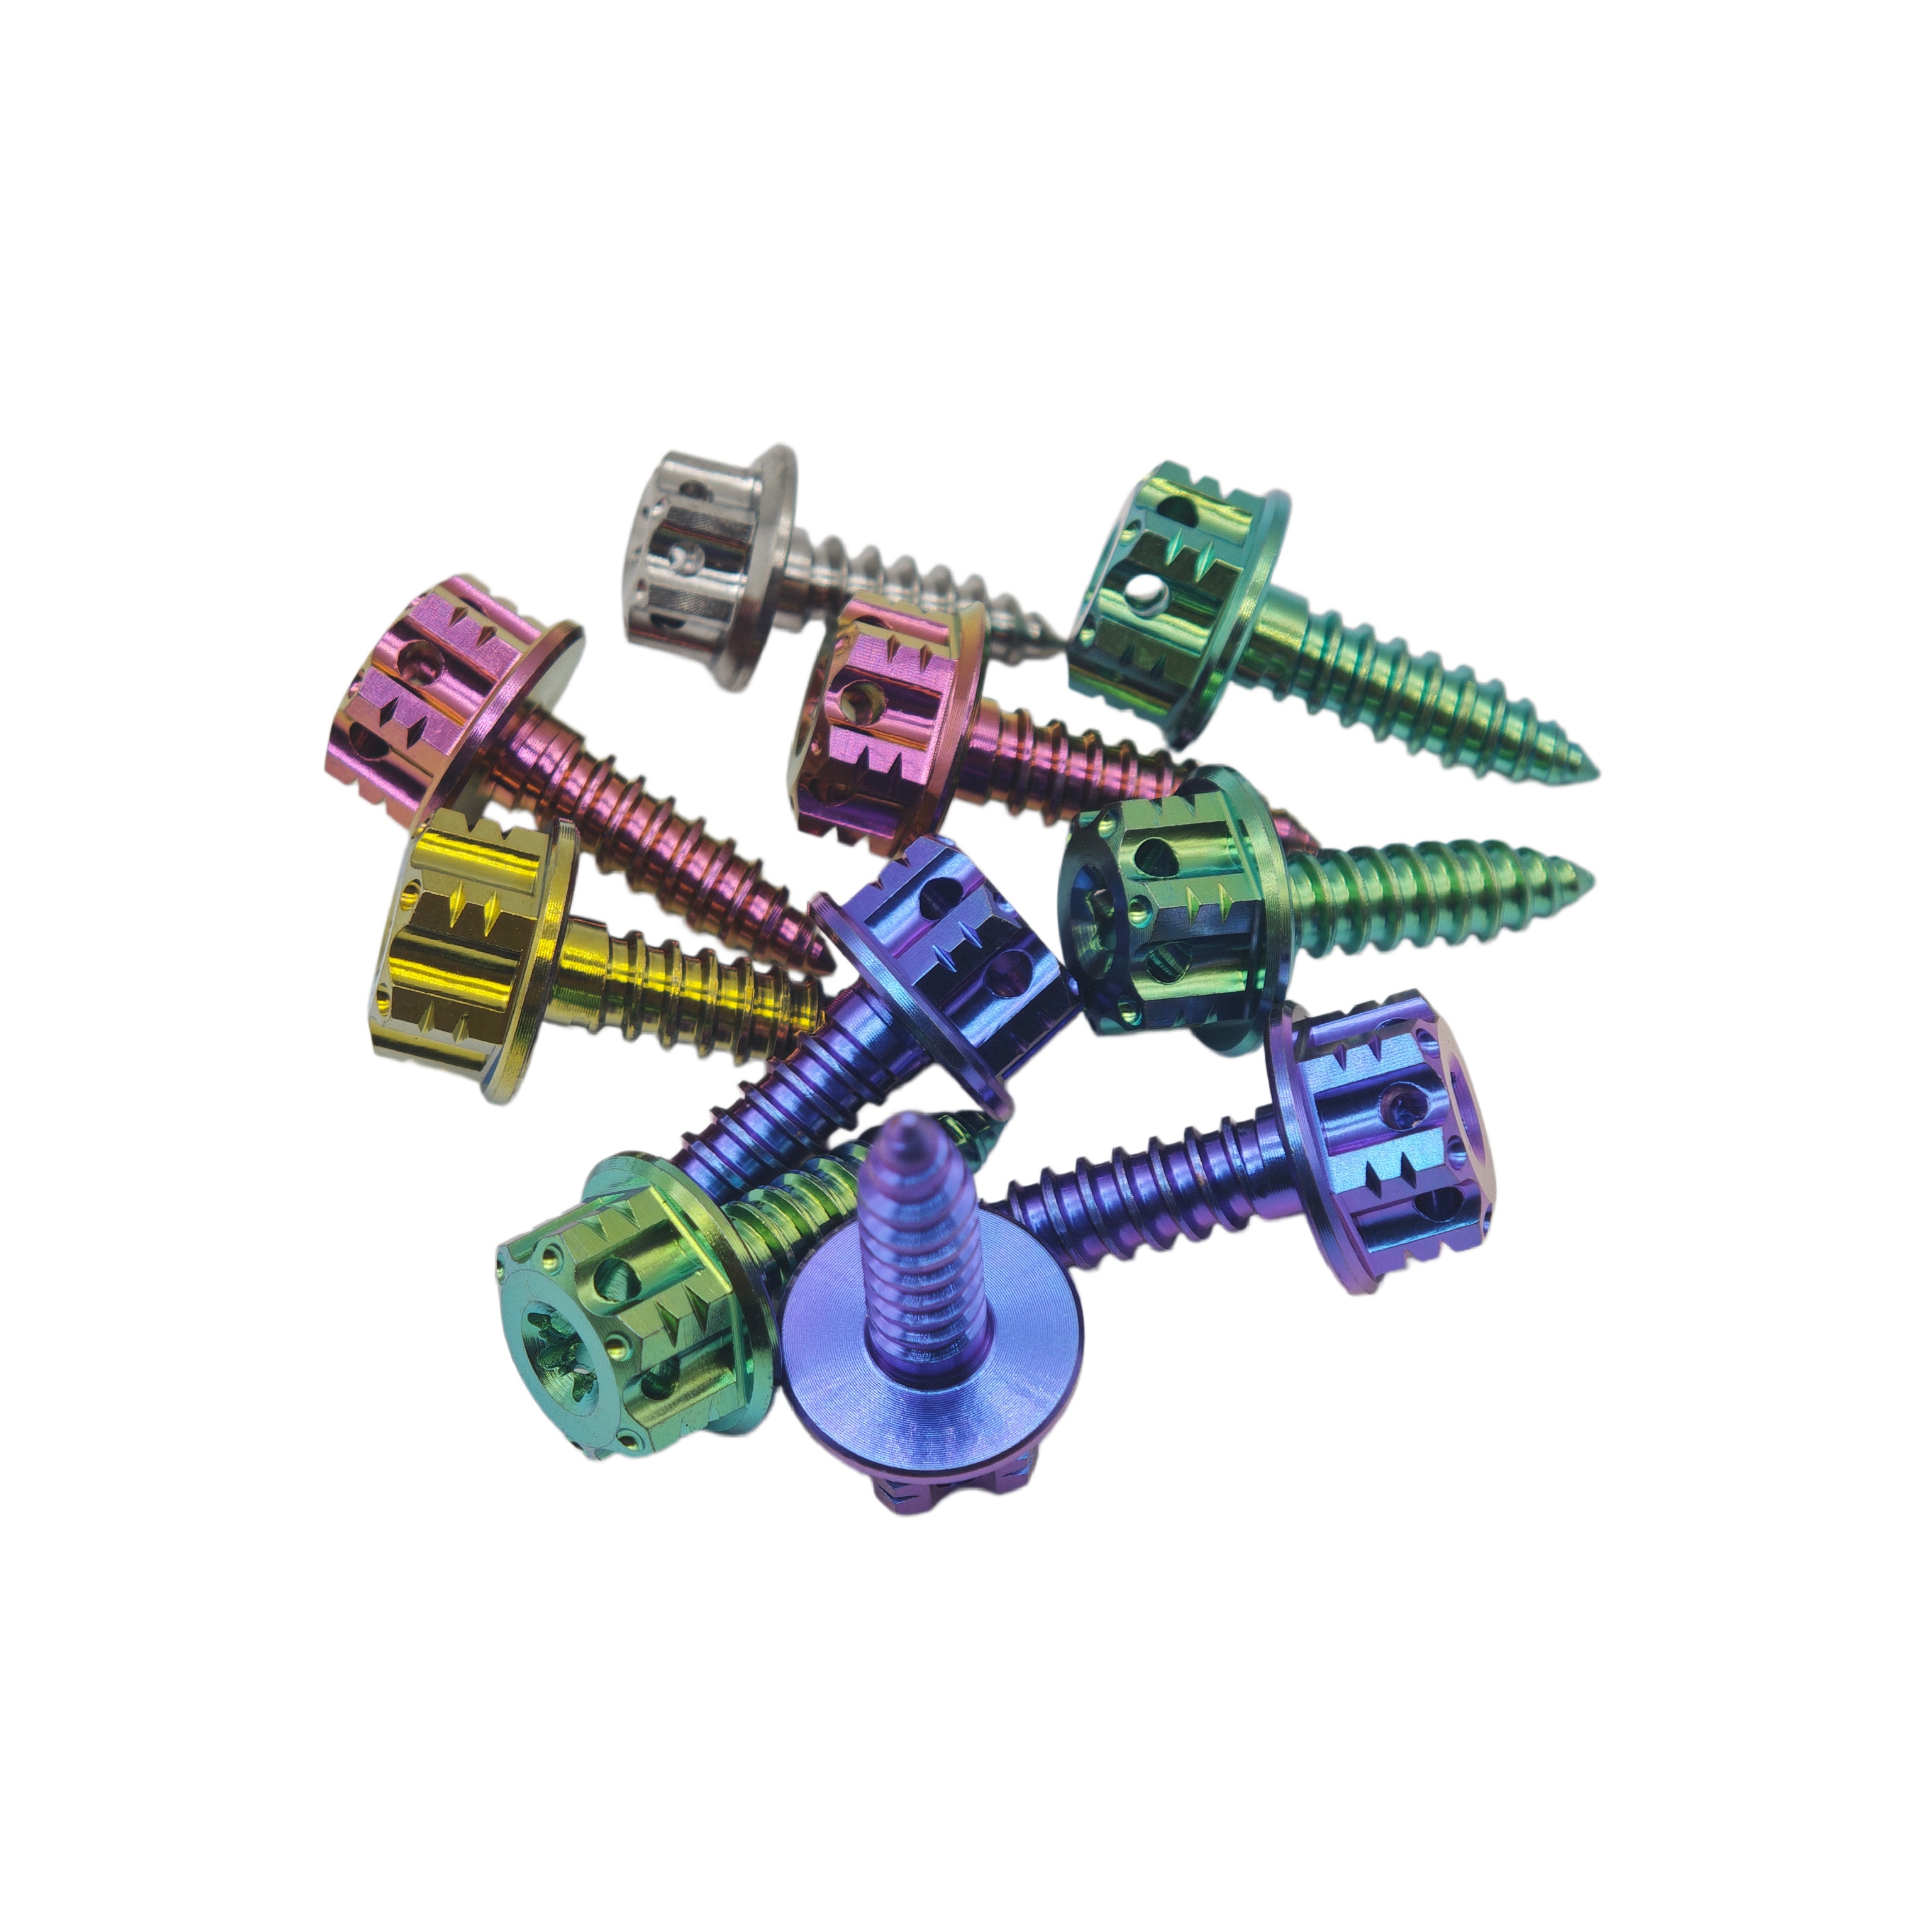
Factory Direct Sales of Metric M5*15 Grade 5 Titanium Alloy Flange Screws
Flanged head bolt with precision rolled metric thread. Multi-industry application from mining sensors to motor casing fixtures.
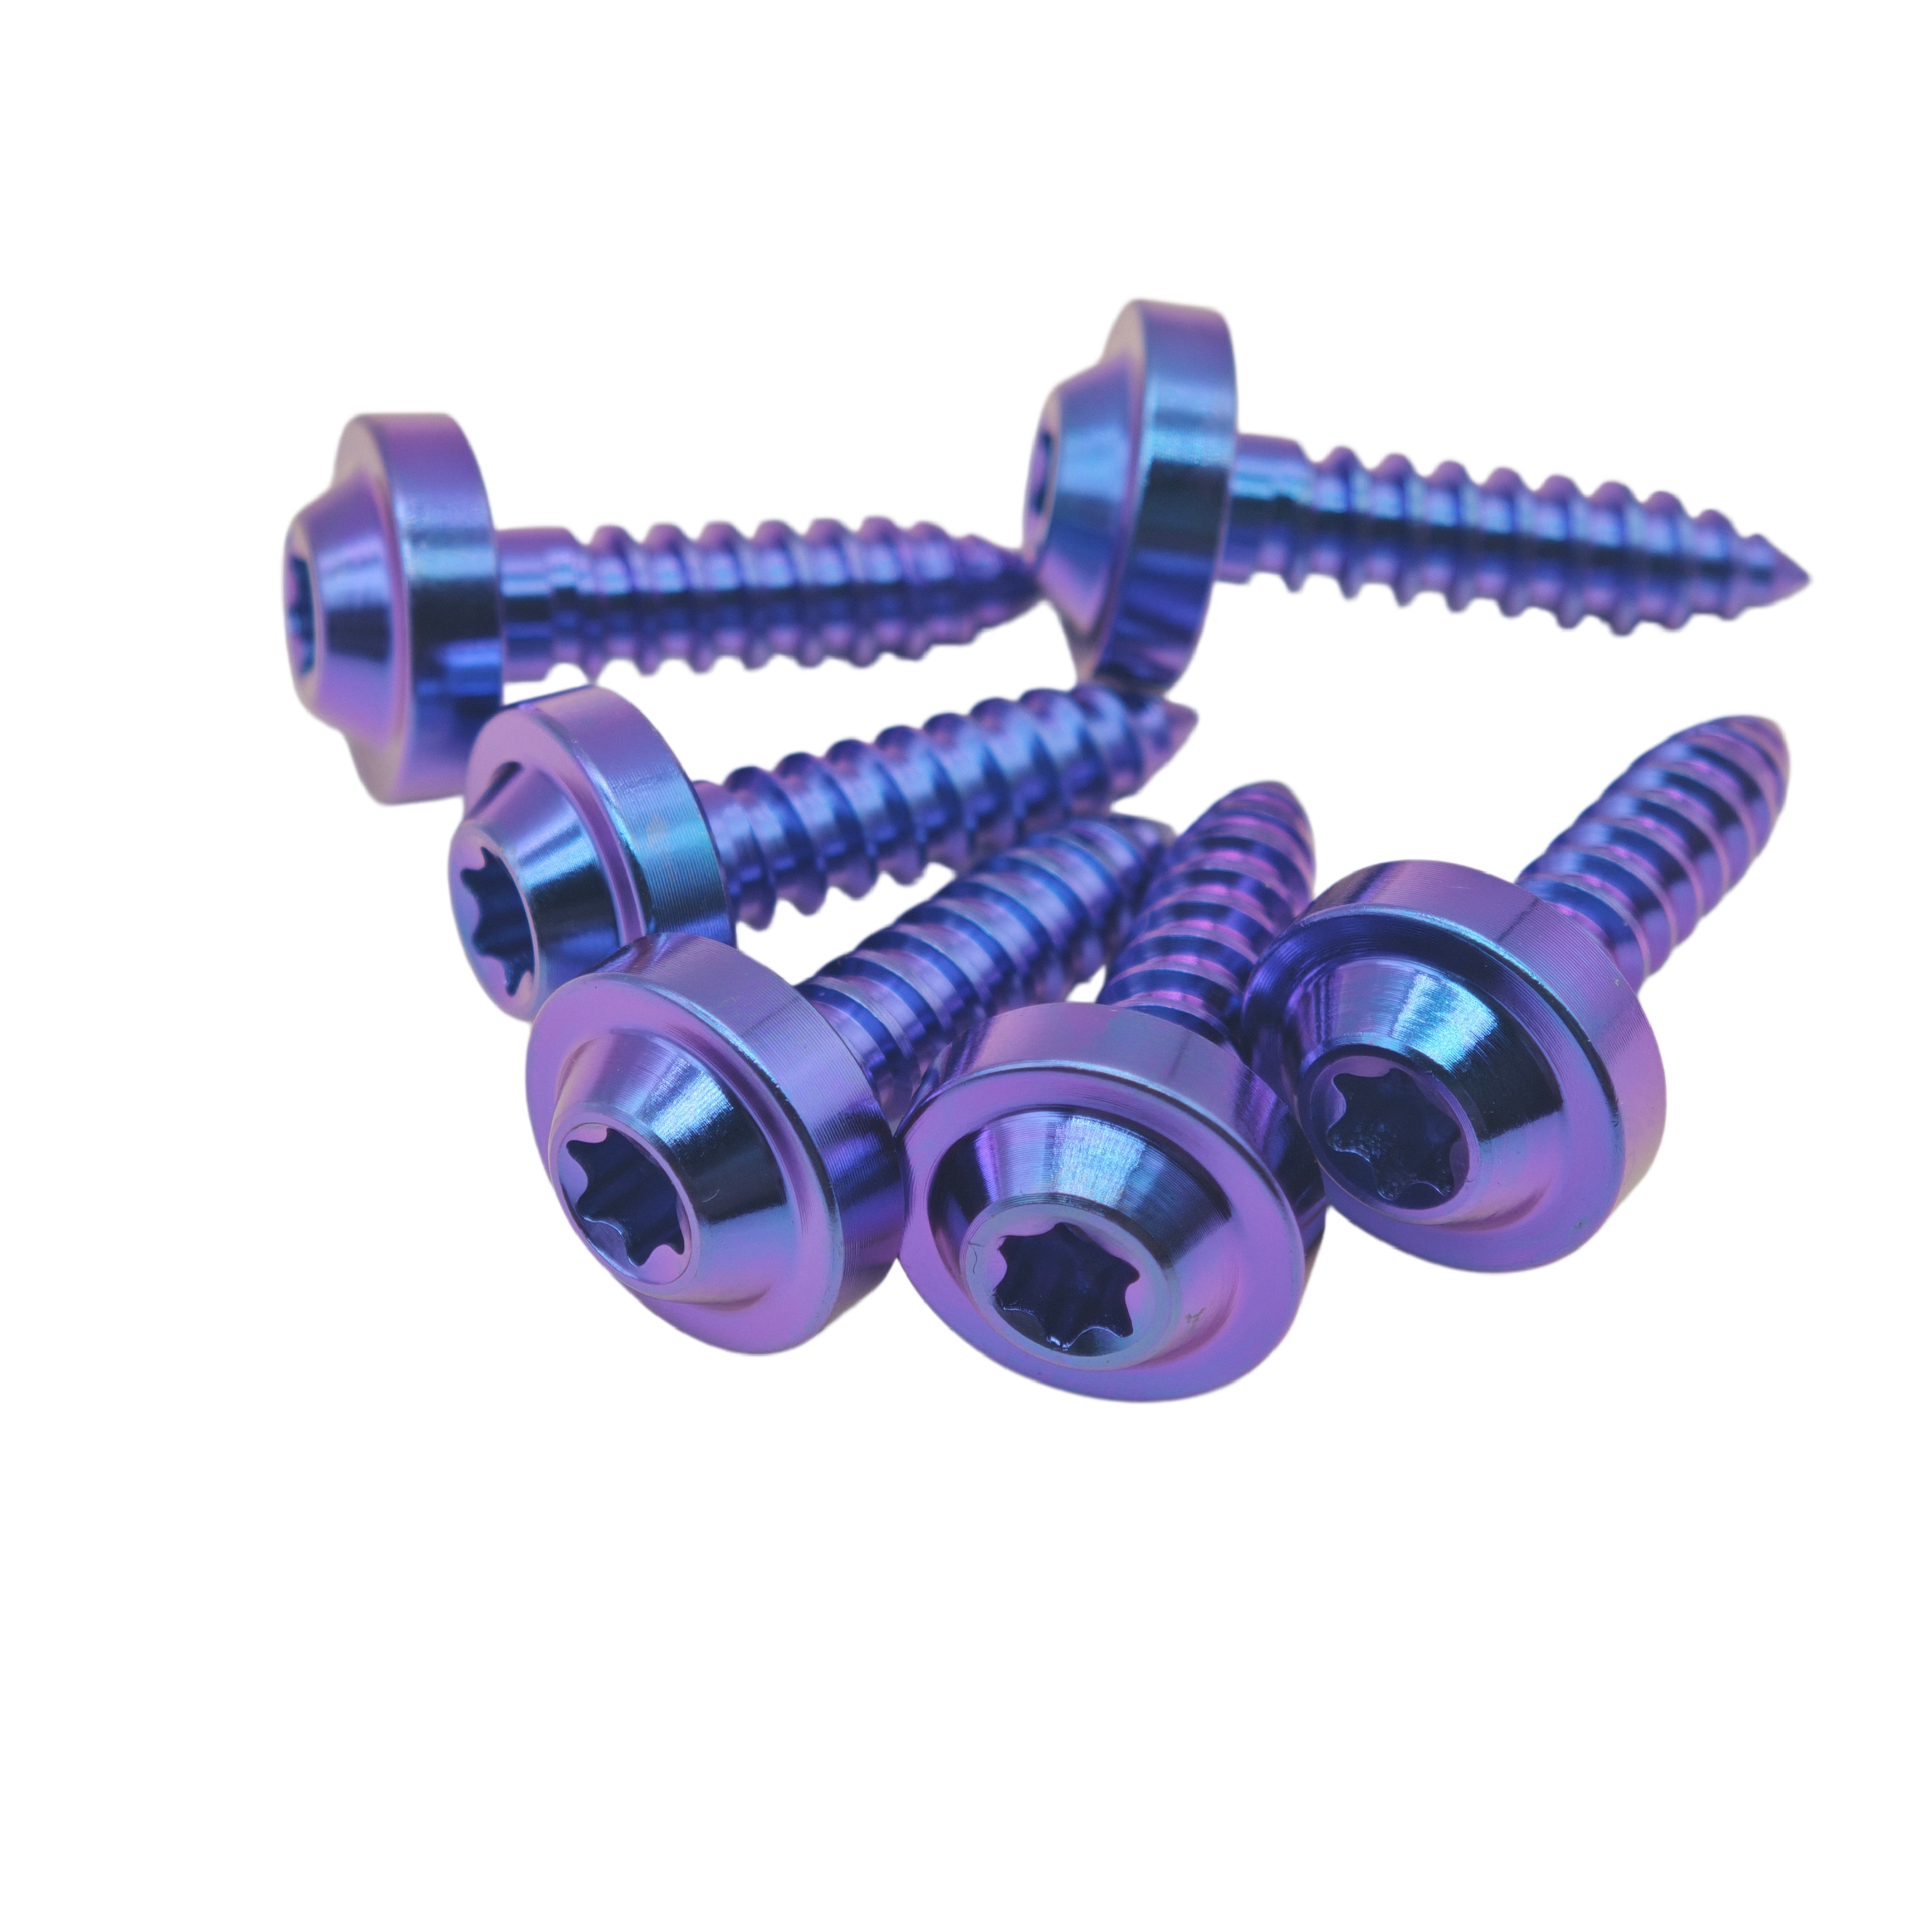
GR5 Anodized Titanium Torx Head Standard Thread Self-Tapping M6 Screw
Electrolytic oxidation coating in metallic blue, gold, and burnt purple. Resists harsh wash chemicals and track corrosion.
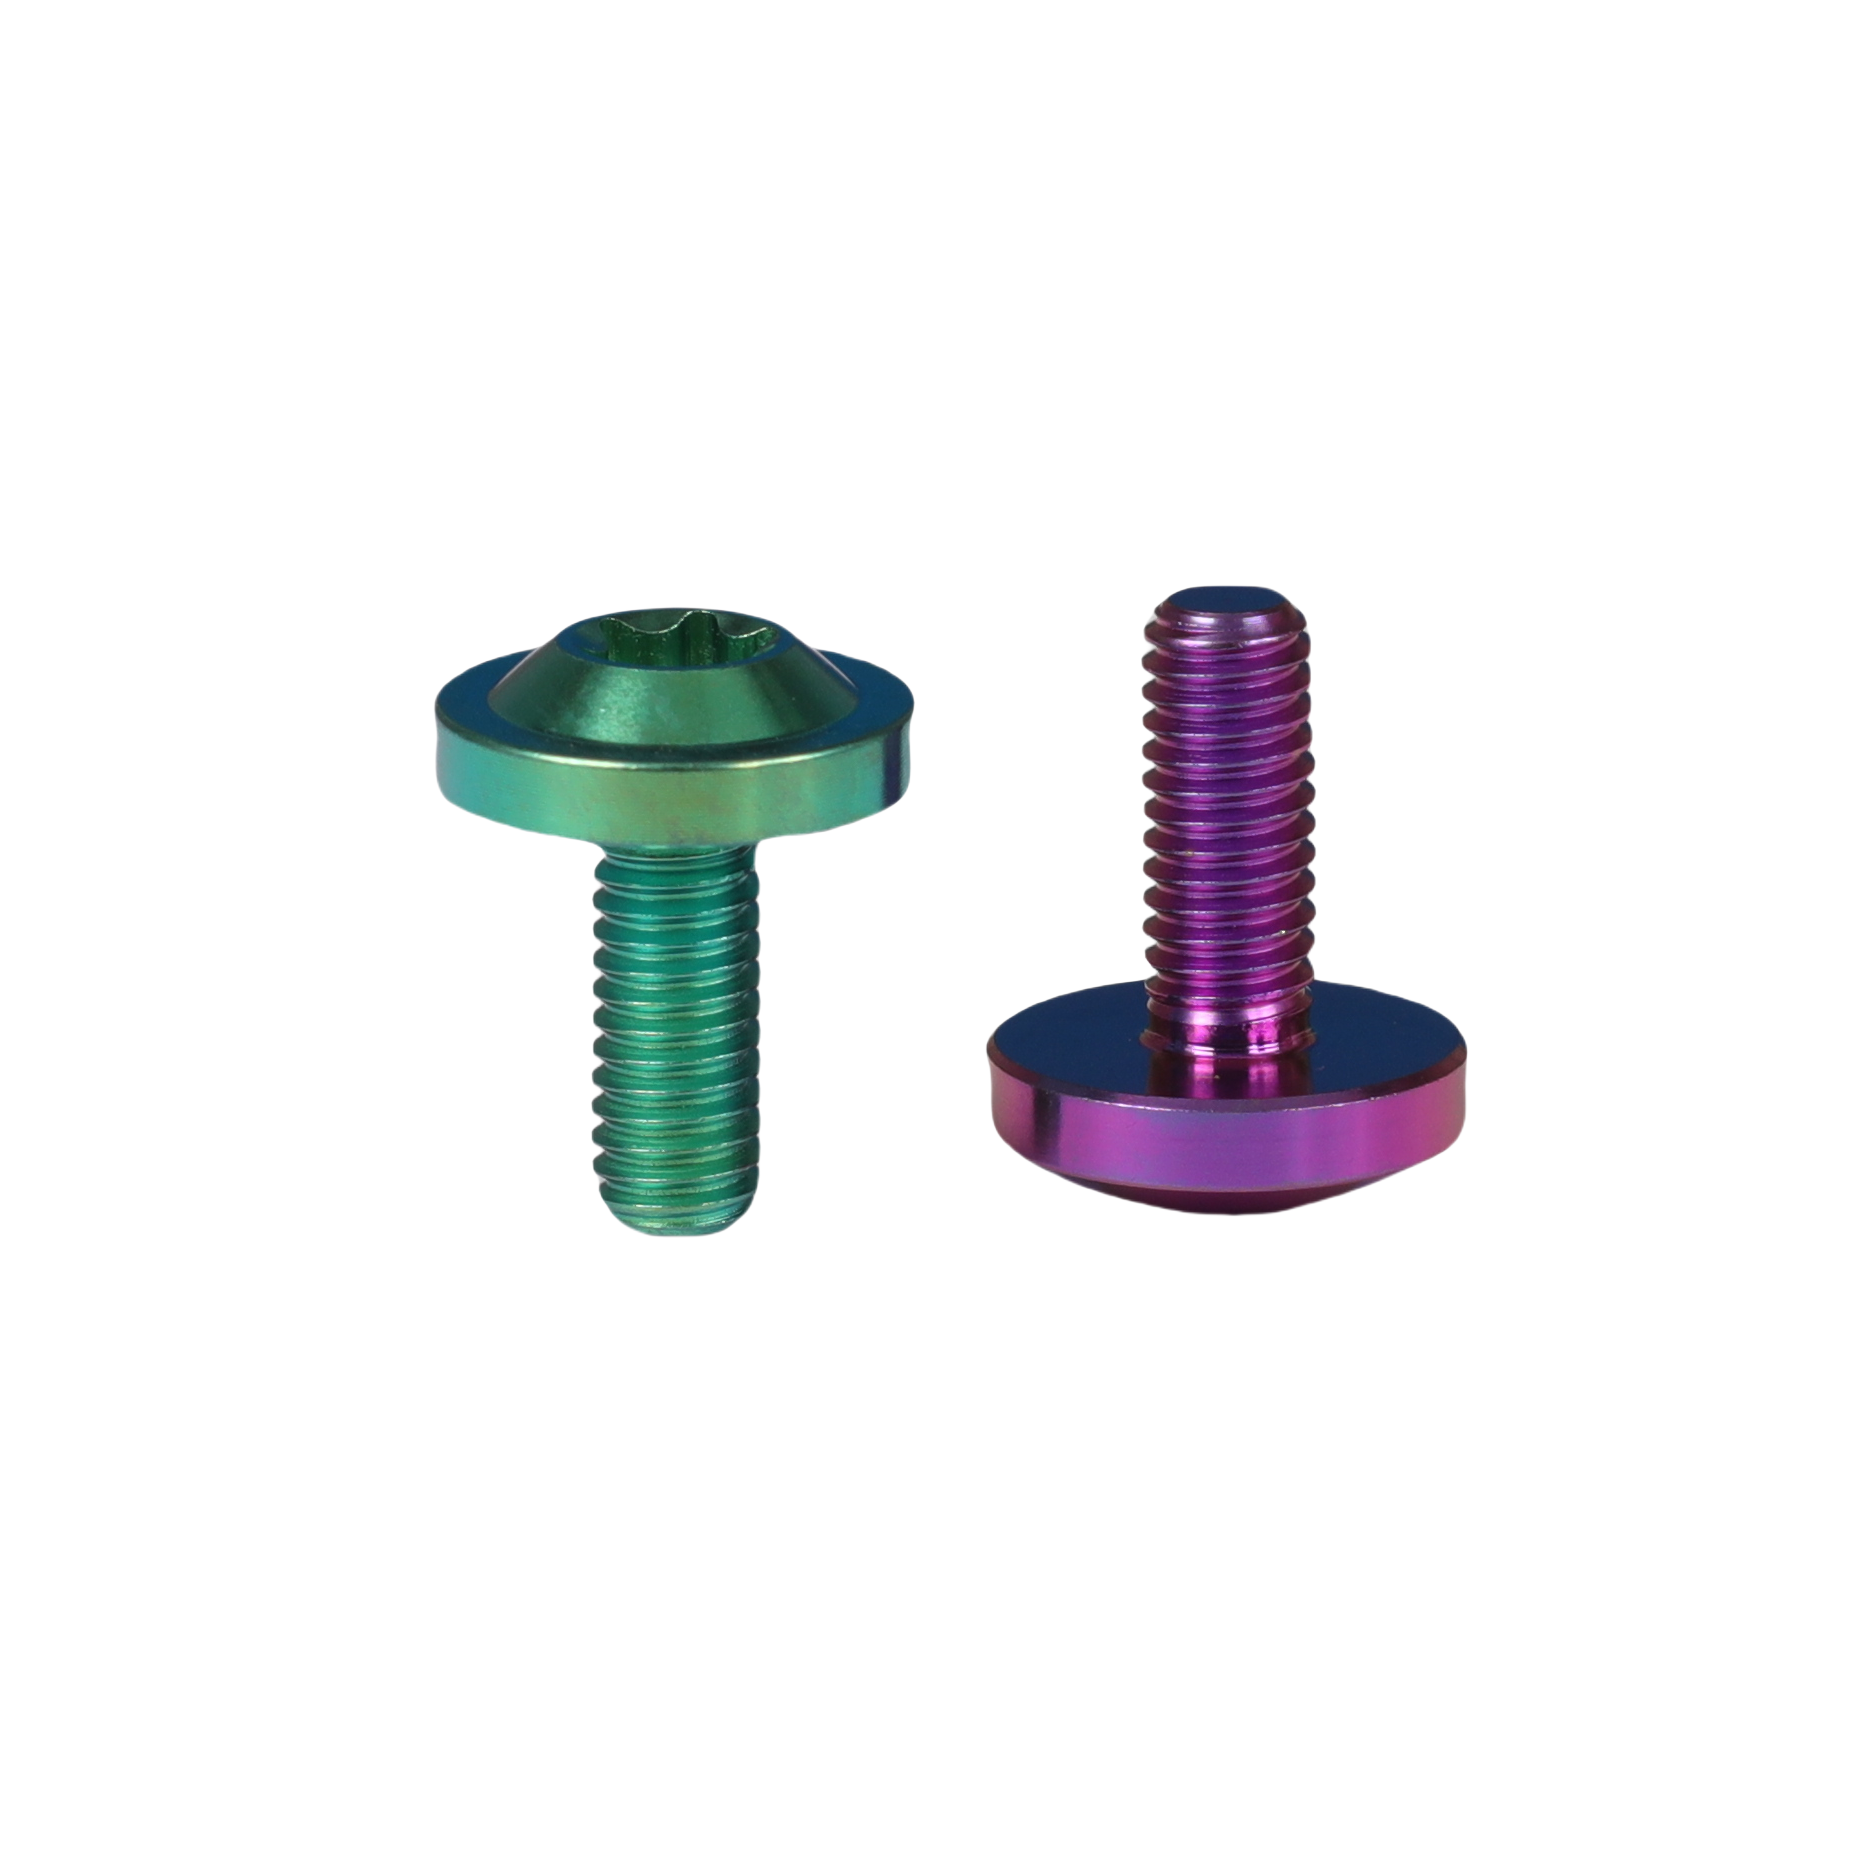
Corrosion-Resistant GR5 M6 Titanium Bolts Fasteners for Engine & Body
High endurance Ti-6Al-4V fasteners providing superior strength-to-weight ratio for critical motorcycle drive train and casing mounts.
Kinematics of Titanium Sprocket Fasteners: Managing Shear & Unsprung Inertia
A comprehensive metallurgical breakdown of rotational dynamics, shear torque tolerance, and thread fatigue life in modern powersports drive hubs.
Rotational Inertia Reduction ($J = \Sigma m r^2$)
Rear drive sprockets represent secondary rotating masses furthest from the wheel axle centerline. Swapping OEM Grade 8.8 or 10.9 steel sprocket bolts for Grade 5 Ti-6Al-4V sheds 44% of parasitic bolt mass at a radius of 60mm–90mm, visibly mitigating angular momentum for faster throttle response and reduced gyroscopic precessional resistance during high-speed corner transition.
Cyclic Shear & Impact Damping Capacity
Under aggressive engine braking and wide-open throttle clutch drops, sprocket hardware experiences immense alternating directional shear loads. Grade 5 titanium possesses a lower modulus of elasticity (~114 GPa) compared to carbon steel (~210 GPa). This metallurgical compliance allows the bolt to absorb peak shock energy elastically without micro-yielding or shearing at the flange-shank interface.
Cold-Rolled Grain Structure Integrity
Zunvo sprocket hardware utilizes fully cold-rolled threads rather than cut or lathe-turned threading. Rolled threading forces the alpha-beta grain crystalline flow lines to contour continuously through the thread root and crest, eliminating stress-riser notches and boosting dynamic mechanical fatigue threshold by over 300% under high-load oscillation.
| Mechanical & Physical Property | Ti-6Al-4V (Grade 5 Titanium) | Class 10.9 Carbon Steel | AISI 304 / A2-70 Stainless | 7075-T6 Billet Aluminum |
|---|---|---|---|---|
| Mass Density (g/cm³) | 4.43 (44% Weight Reduction) | 7.85 | 7.93 | 2.81 |
| Ultimate Tensile Strength (MPa) | 950 – 1050 | 1040 | 700 | 570 |
| Tensile Yield Strength (MPa) | 880 – 920 | 940 | 450 | 505 |
| Modulus of Elasticity (GPa) | 114 (High Shock Absorption) | 210 | 193 | 72 |
| Corrosion Resistance (ASTM B117) | Immune (Spontaneous TiO₂ Layer) | Poor (Requires Zinc/Phosphate) | Moderate (Pitting Risk) | Moderate (Prone to Exfoliation) |
| Fatigue Endurance Limit (10⁷ Cycles) | 510 MPa | 420 MPa | 240 MPa | 160 MPa |
Future Sourcing & Procurement Trends for Titanium Fasteners (2025–2030)
How tier-1 powersports builders, racing syndicates, and aftermarket distributors are pivoting procurement strategies to secure supply chain resilience and cost parity.
Direct Baoji Cluster Integration
International importers are bypassing multi-tier brokerages to contract directly with manufacturers in Baoji (China's Titanium Valley). Sourcing directly within this regional cluster grants verified access to sponge titanium melts, certified vacuum arc remelting (VAR) ingots, and precision centerless-ground bars, slashing procurement markups by 22% to 35%.
Mandatory 100% Heat-Number Traceability
Due to influxes of sub-standard commercial scrap alloy on unregulated exchanges, enterprise procurement protocols now mandate EN 10204 3.1 inspection certification per batch. Buyers demand full chemistry reports (ICP-OES) detailing nitrogen (<0.05%), oxygen (<0.20%), and carbon (<0.08%) limits to prevent interstitial embrittlement in safety-critical drive assemblies.
Demand for Turnkey Packaged Kits
Distributors are moving away from ordering generic bulk loose hardware. Modern procurement contracts require bespoke pre-packaged kits containing exact model-matched rear sprocket bolts (M8x1.25 or M10x1.25), self-locking Fuji-style titanium flange locknuts, and pre-applied anti-galling thread compounds ready for retail shelf display.
Technological & Engineering Evolution of Drive Hardware
Advanced surface treatments, cold-forging hybrid metallurgy, and anti-vibrational geometries elevating modern titanium hardware.
Cathodic PVD Diamond-Like Coatings
While standard anodizing provides dynamic aesthetic coloring, modern motorsport specifications increasingly adopt Physical Vapor Deposition (PVD) Titanium Aluminum Nitride (TiAlN) and DLC coatings. These deposit a 2–3µm ultra-hard ceramic shell (exceeding 2500 HV) that eradicates surface micro-fretting and tool-interface wear.
Hybrid Warm-Heading Manufacturing
Transitioning from pure lathe subtractive machining to induction warm heading (heated between 650°C and 750°C) allows the bolt head to be forged near net-shape without grain disruption. This reduces production lead times by 40% while preserving continuous internal structural fiber lines through the under-head transition radius.
Internal Anti-Loosening Architecture
To counter severe drive harmonics that back off standard nuts, next-generation sprocket bolts feature integrated prevailing-torque locking collared flanges, proprietary spiral thread roots, and precision conical washer seats that mechanically distribute radial clamp forces uniformly across the hub web face.
Low-Friction Solid Film Lubrication
Overcoming the natural galling tendency of untreated titanium threads without requiring messy external paste, modern suppliers apply factory-baked molybdenum disulfide (MoS₂) or fluoropolymer thin-film dry lubricants directly onto threads for stable torque-tension repeatability across repeated wheel removals.
Baoji Factory Infrastructure & Technical Capabilities
Zunvo Titanium Products Co., Ltd. blends geographic raw material proximity with rigorous aerospace inspection regimes.
24-hour engineering turnaround reviewing thread class 6g/6H, head undercuts, and shear plane geometry.
3-day functional sample batches turned on multi-axis CNC lathes for real-world fitment and torque testing.
High-voltage automated spectrum anodizing or vacuum chamber PVD deposition to exact color codes.
Cold hydraulic thread rolling generating hardened roots, followed by tight-tolerance shank machining.
Optical laser sorting for pitch runout, thread gauge go/no-go checks, and optical micro-crack screening.
Why International OEM Brands Partner with Zunvo Titanium:
Founded in 2015 within the Shiling Road Industrial Park of Baoji, Shaanxi, Zunvo operates a dedicated 1,000–3,000 m² modern manufacturing footprint staffed by 101–200 metallurgy specialists. Situated in China's industrial core of titanium production, we access premium virgin bar melts directly from neighboring smelters, certifying every raw lot down to its unique heat number.
Our export operations encompass direct air and ocean consolidation to North America, Europe, Southeast Asia, and the Middle East. With an average quotation response speed under 7 hours and a proven 66% reorder rate across our global buyer catalog, we provide end-to-end packaging, laser etching, custom thread profiles, and verified material certificates (EN 10204 3.1) with every shipment.
Titanium Sprocket Bolt Sourcing FAQ
Practical engineering answers to address installation, galvanic safety, torque calculations, and ordering logistics.
Can Grade 5 titanium safely handle the shear loads of 1000cc+ superbike sprockets?
Yes. Grade 5 Ti-6Al-4V provides an ultimate tensile strength exceeding 950 MPa and a shear yield strength of ~550 MPa, which closely mirrors Class 10.9 heat-treated alloy steel while delivering vastly superior fatigue and impact damping properties. Provided the bolts are torqued to OEM clamping preload, the clamping friction between the sprocket face and wheel carrier hub absorbs the majority of rotational torque, preventing direct shear fatigue.
How do you eliminate galvanic corrosion when pairing titanium bolts with aluminum hubs?
Titanium and aluminum have divergent galvanic potentials. To eliminate galvanic electron transfer, always coat the threads and under-head contact washer with a nickel-based or copper-based anti-seize paste, or specify our dry-film PTFE / MoS₂ coating. For street bikes ridden in salt environments, using our integrated titanium flat washers prevents direct metal-on-metal abrading of the wheel carrier's anodized clear-coat layer.
What is the correct tightening torque for titanium sprocket hardware?
Because titanium has a different friction coefficient than zinc-plated steel, standard dry torque values do not apply. When using anti-seize paste or lubricant, reduce the OEM factory steel bolt torque value by approximately 15% to 20% to prevent over-stretching the fastener while achieving the identical axial clamping load. For M8x1.25 titanium sprocket bolts, torque typically lands between 32–36 Nm; for M10x1.25, between 55–60 Nm.
What are the minimum order quantities (MOQ) and production lead times?
Standard inventory items and catalog sizes (M8/M10 sprocket sets, rotor bolts) carry an MOQ of 100 sets or 100–200 dozen for bulk hardware, with in-stock dispatch within 24 hours. Custom drawing-based specifications require an initial pilot run MOQ of only 100 pieces to validate CAD fitment, with mass production batches scaling within 7–15 working days.
Will anodized color treatments fade under wheel cleaning chemicals or brake heat?
Titanium anodization is an electrochemical growth of the surface titanium dioxide (TiO₂) film that refracts light naturally; it contains zero organic dyes or pigments, meaning it will never chip, flake, or blister from heat. However, harsh industrial acid washes (such as hydrofluoric wheel cleaners) can etch the oxide layer. For maximum chemical and scratch resilience, we recommend our vapor-deposited PVD Black or PVD Gold finishes.
Can you manufacture sprocket bolts to custom OEM drawings with proprietary drive heads?
Yes. Over 60% of our production volume is OEM/ODM custom engineered. We routinely produce countersunk, broad disc, low-profile umbrella, 12-point flange, and internal Torx/hex configurations according to STEP/IGES/DWG files. We can also integrate mechanical lock-wire safety holes across bolt heads for FIM/AMA sanctioned competition compliance.
Request Factory Quotation & Metallurgical Test Report
Partner directly with Baoji’s premier Grade 5 titanium fastener factory. Submit your custom drawings, dimensioned samples, or bulk order quantities for a comprehensive technical review within 7 hours.
