Featured Precision Titanium Fasteners & OEM Components
Engineered from mill-certified Ti-6Al-4V Grade 5 bar stock. Designed for race motorcycles, performance automotive turbo manifolds, and high-stress industrial applications.
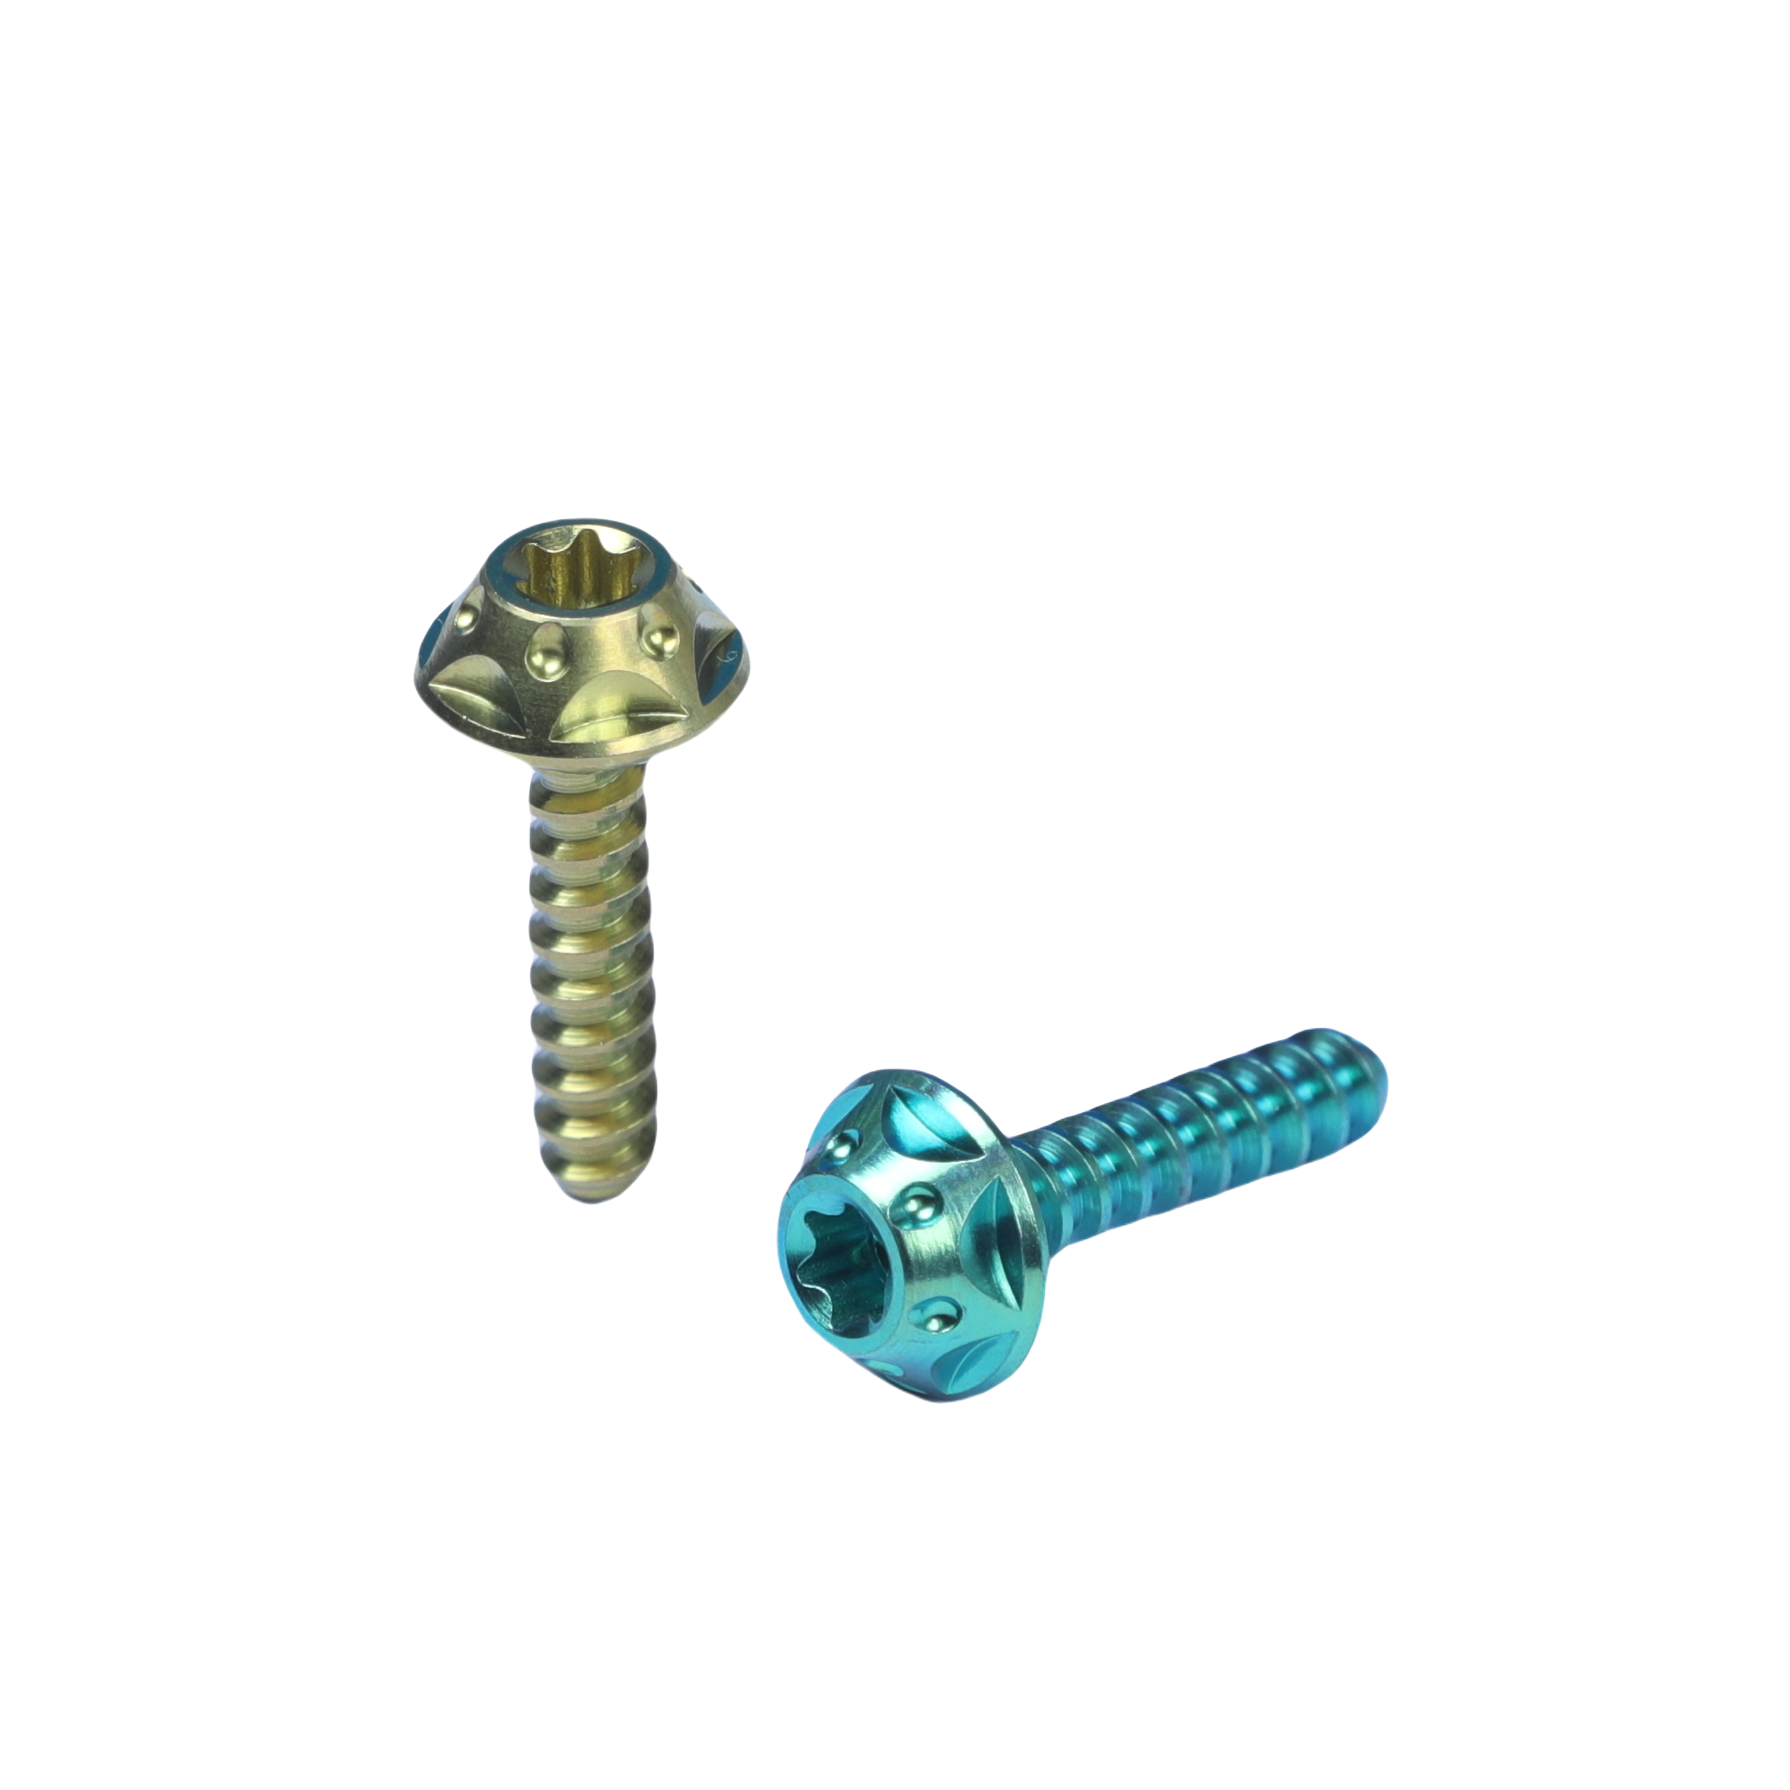
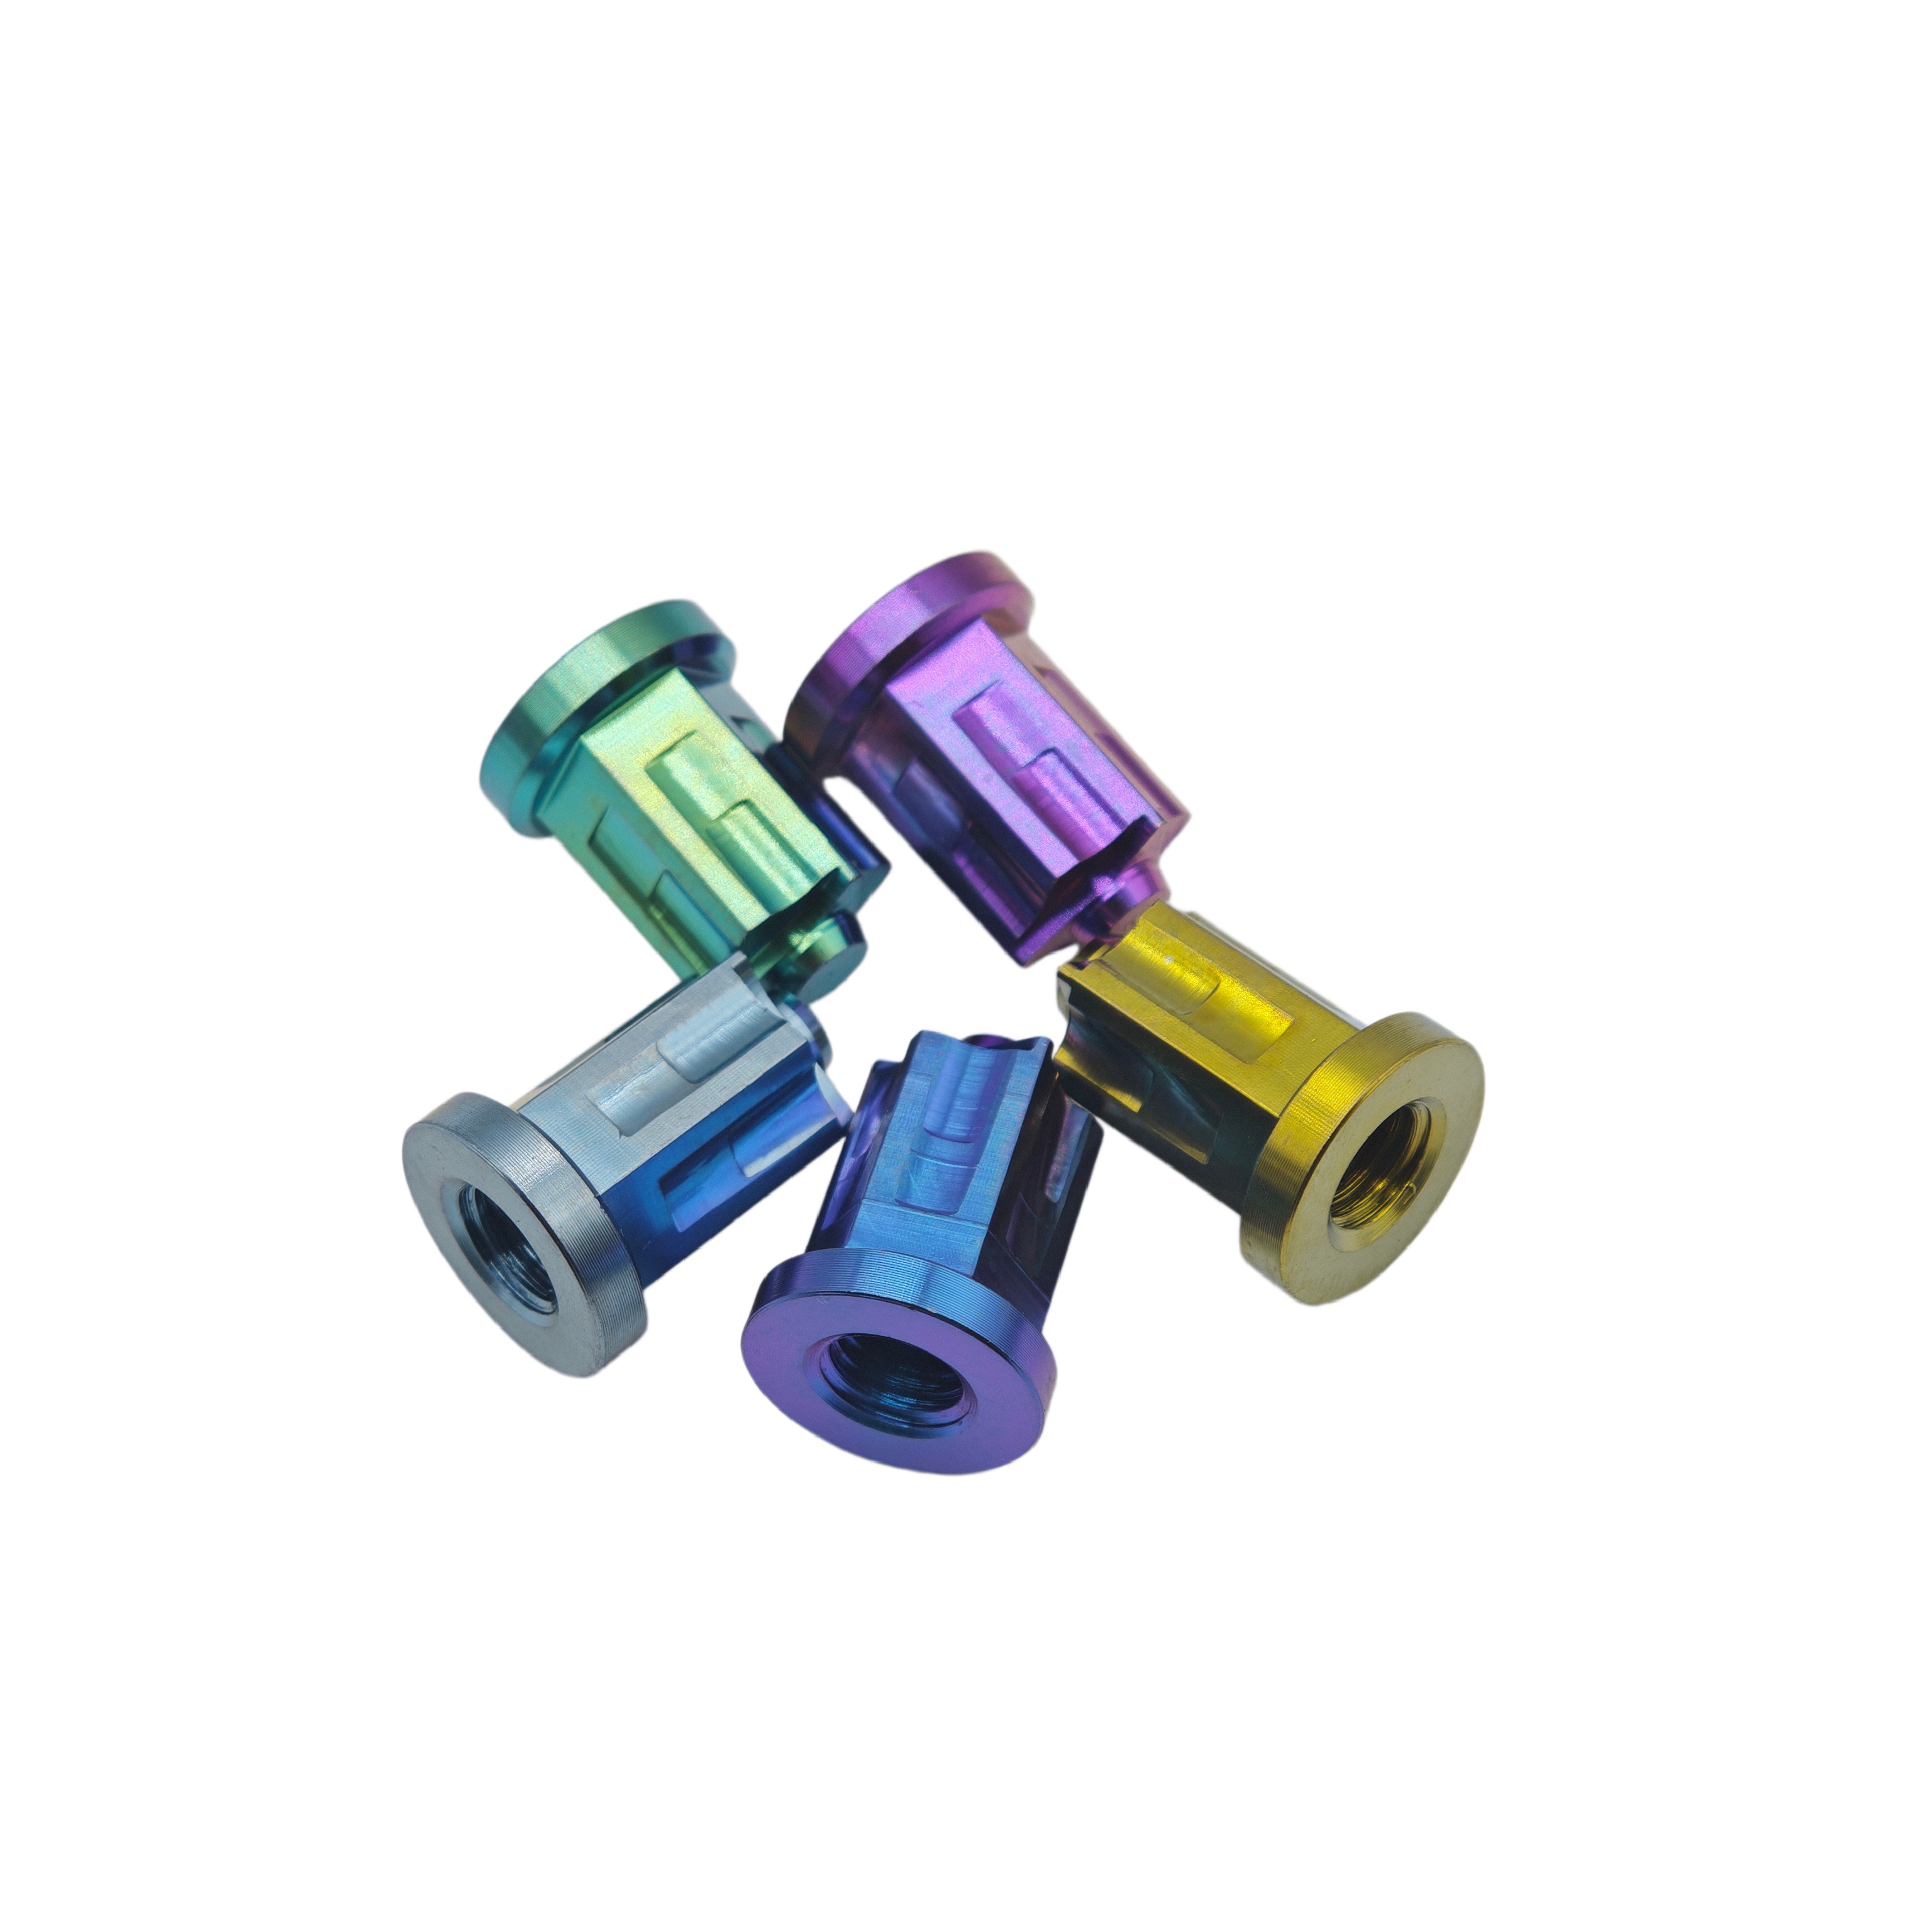
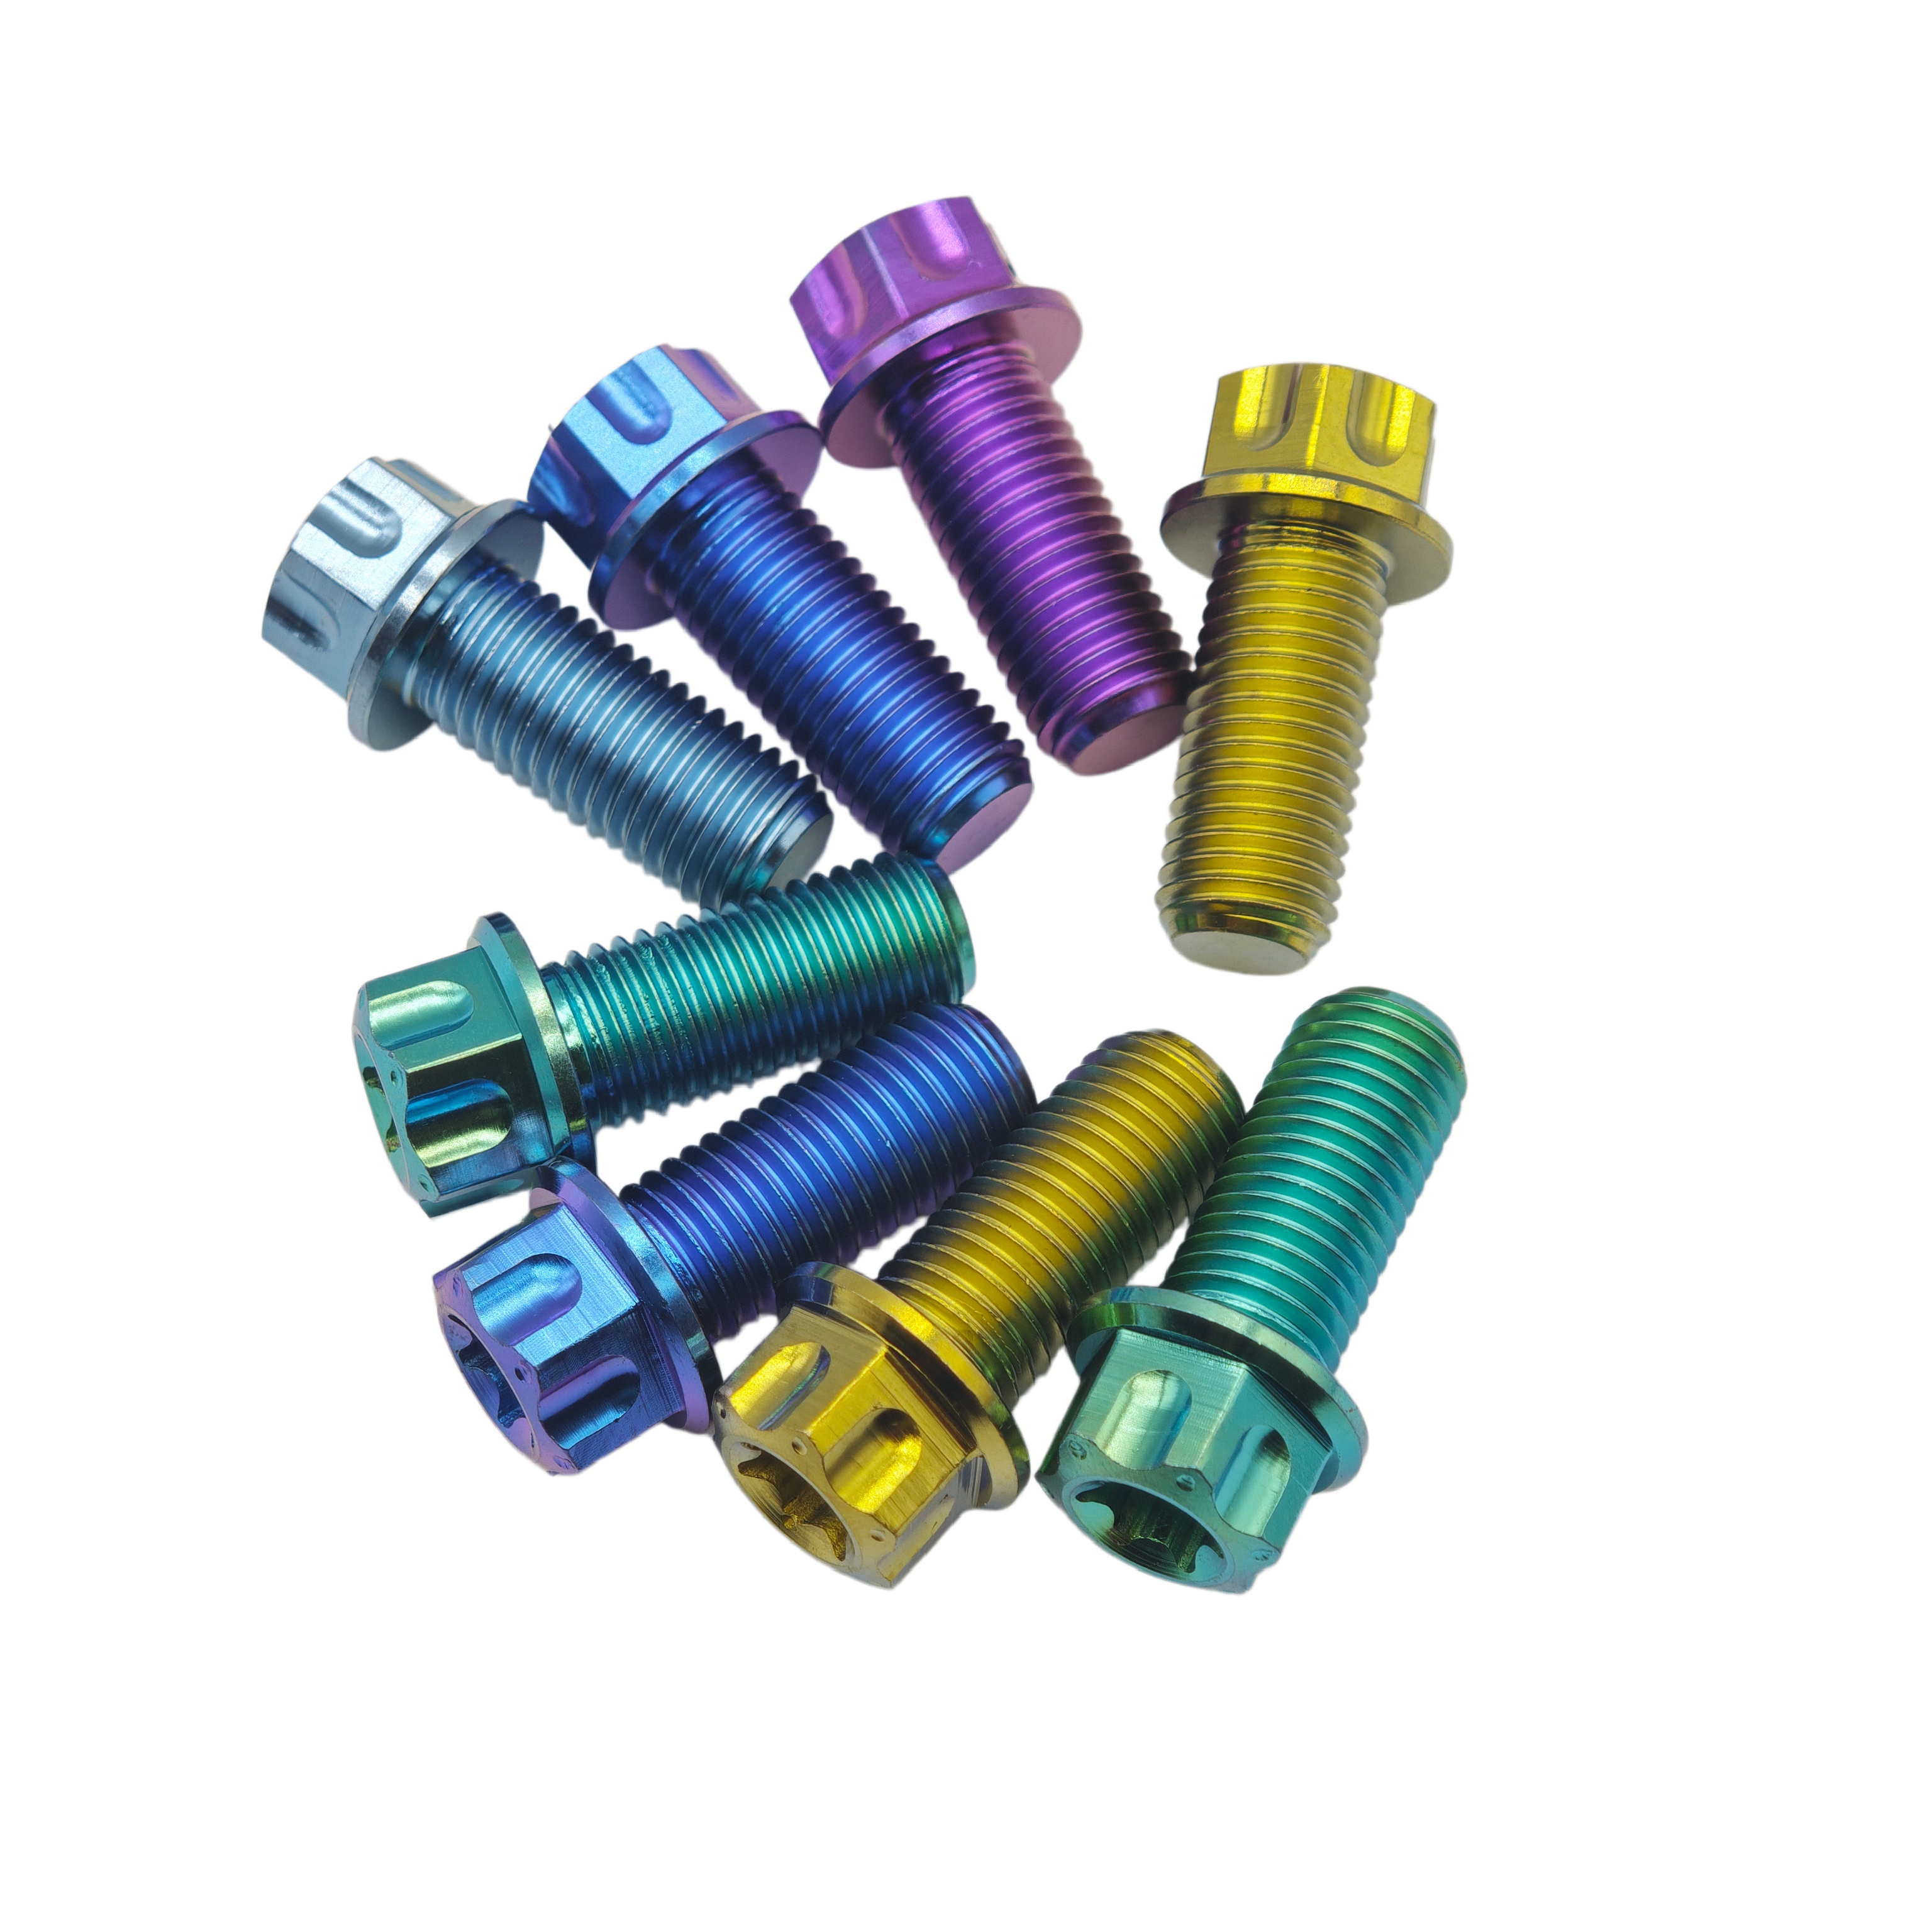
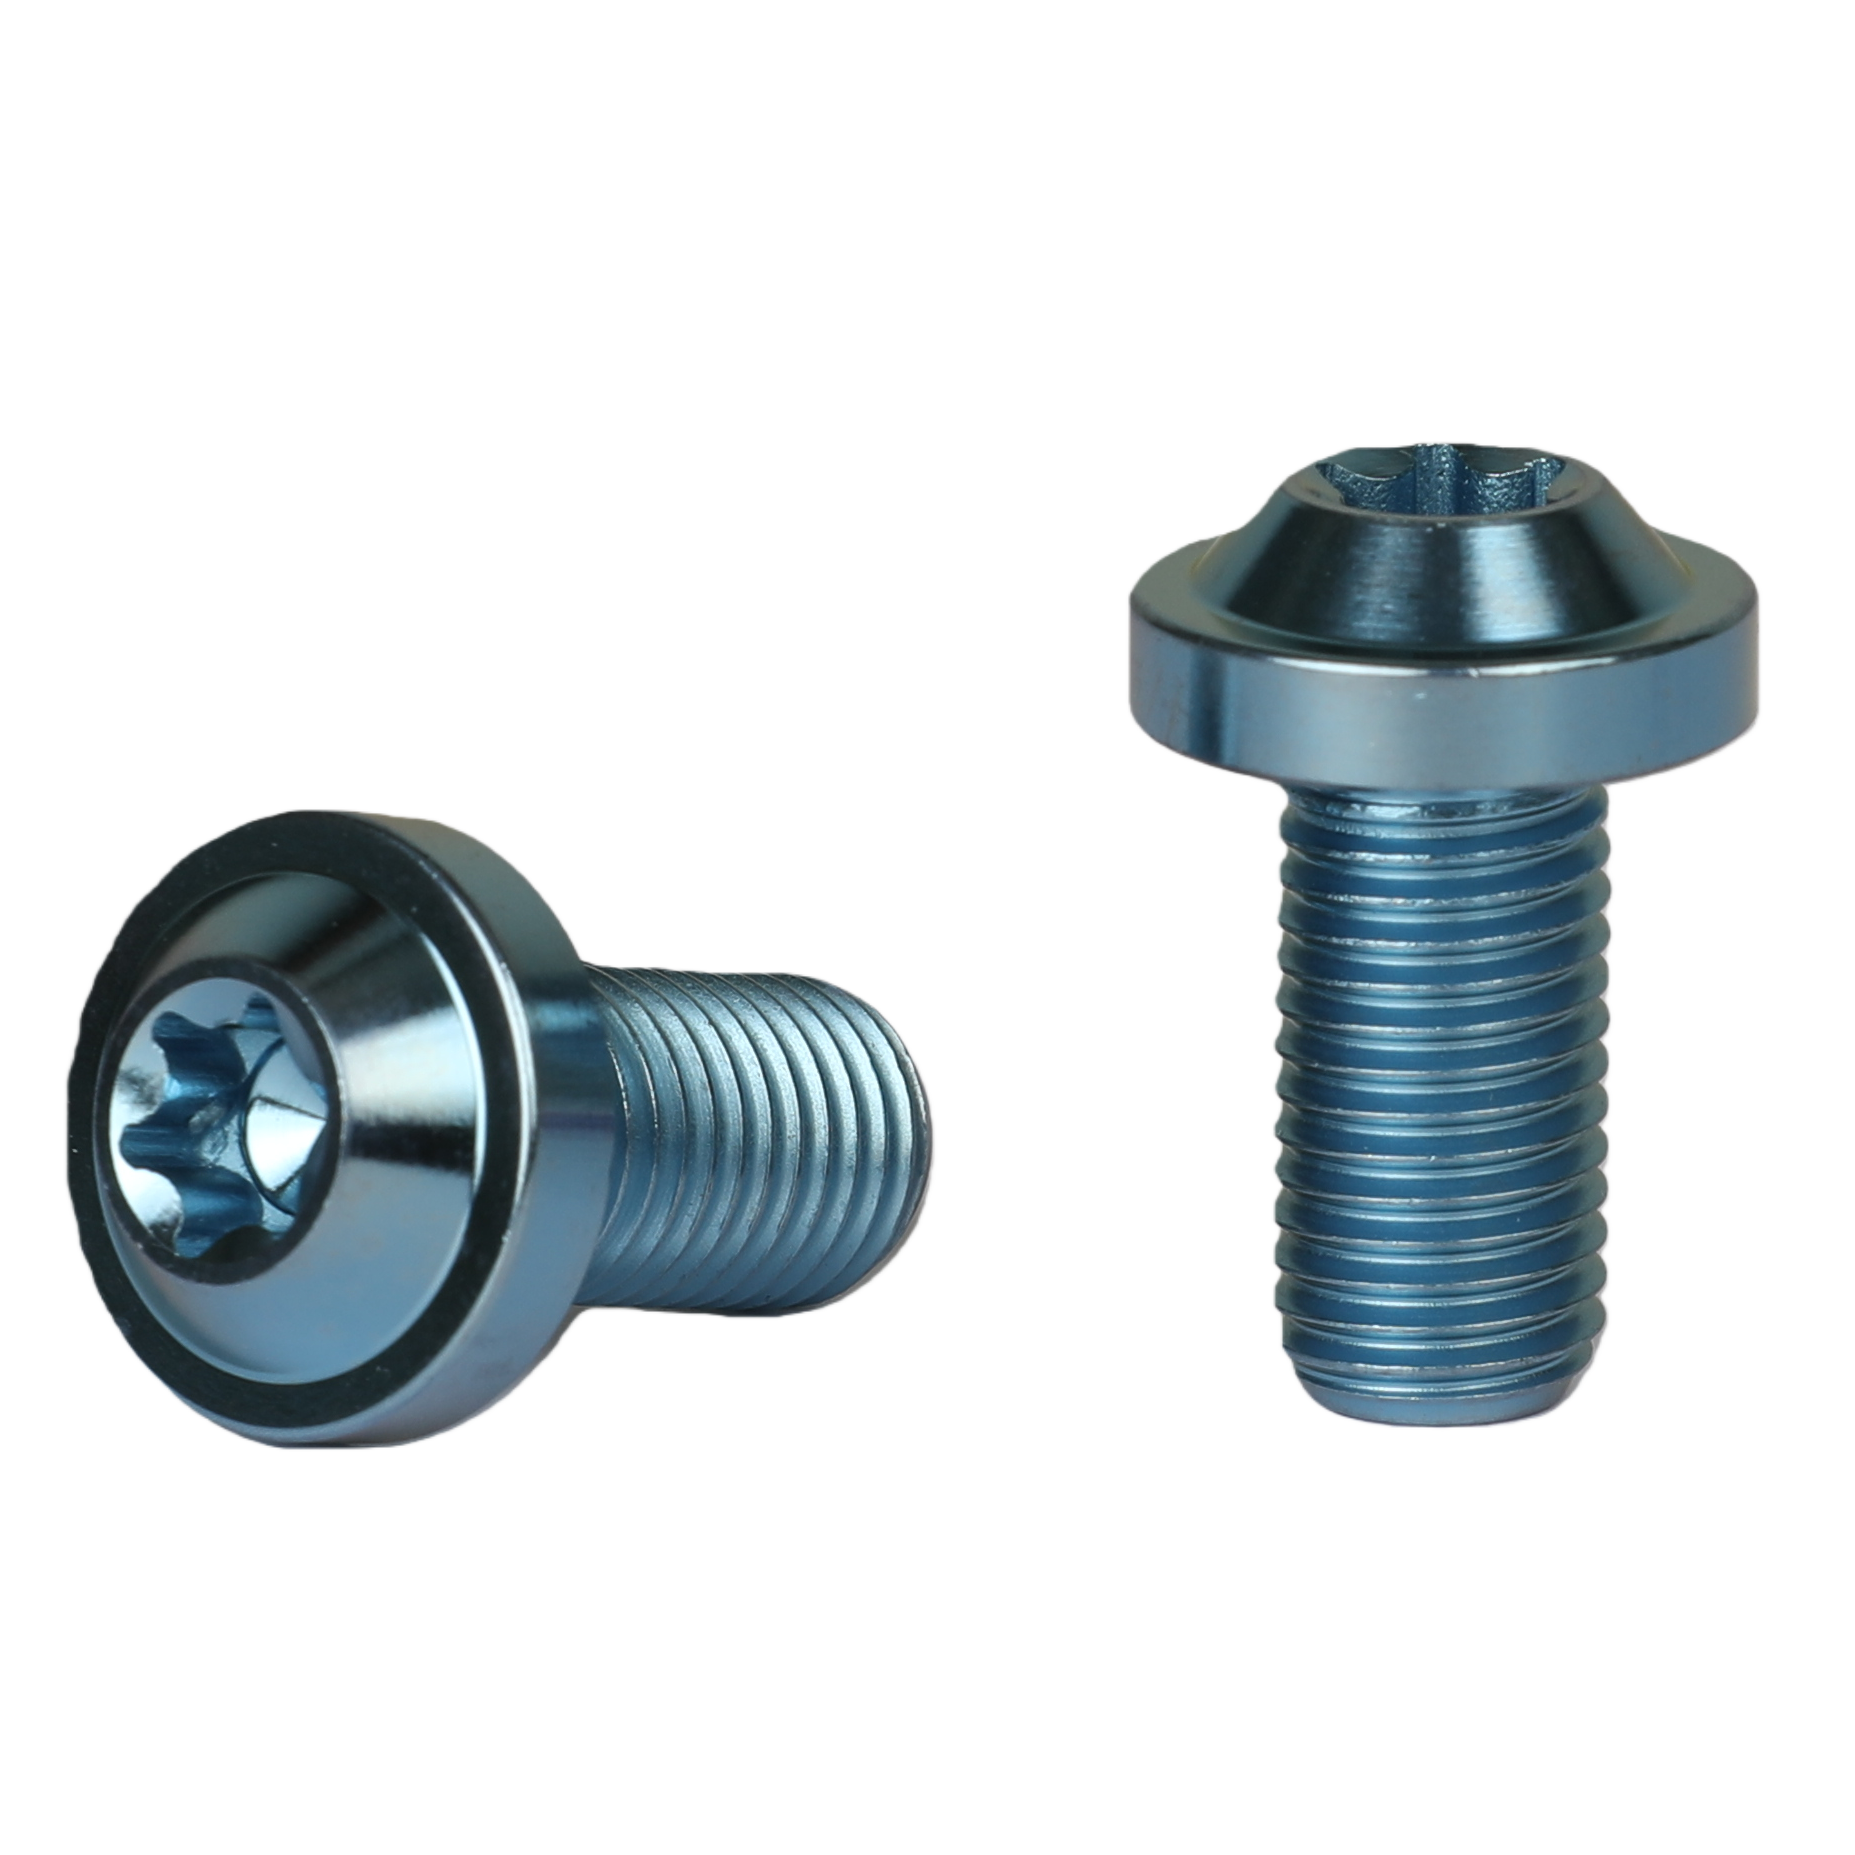
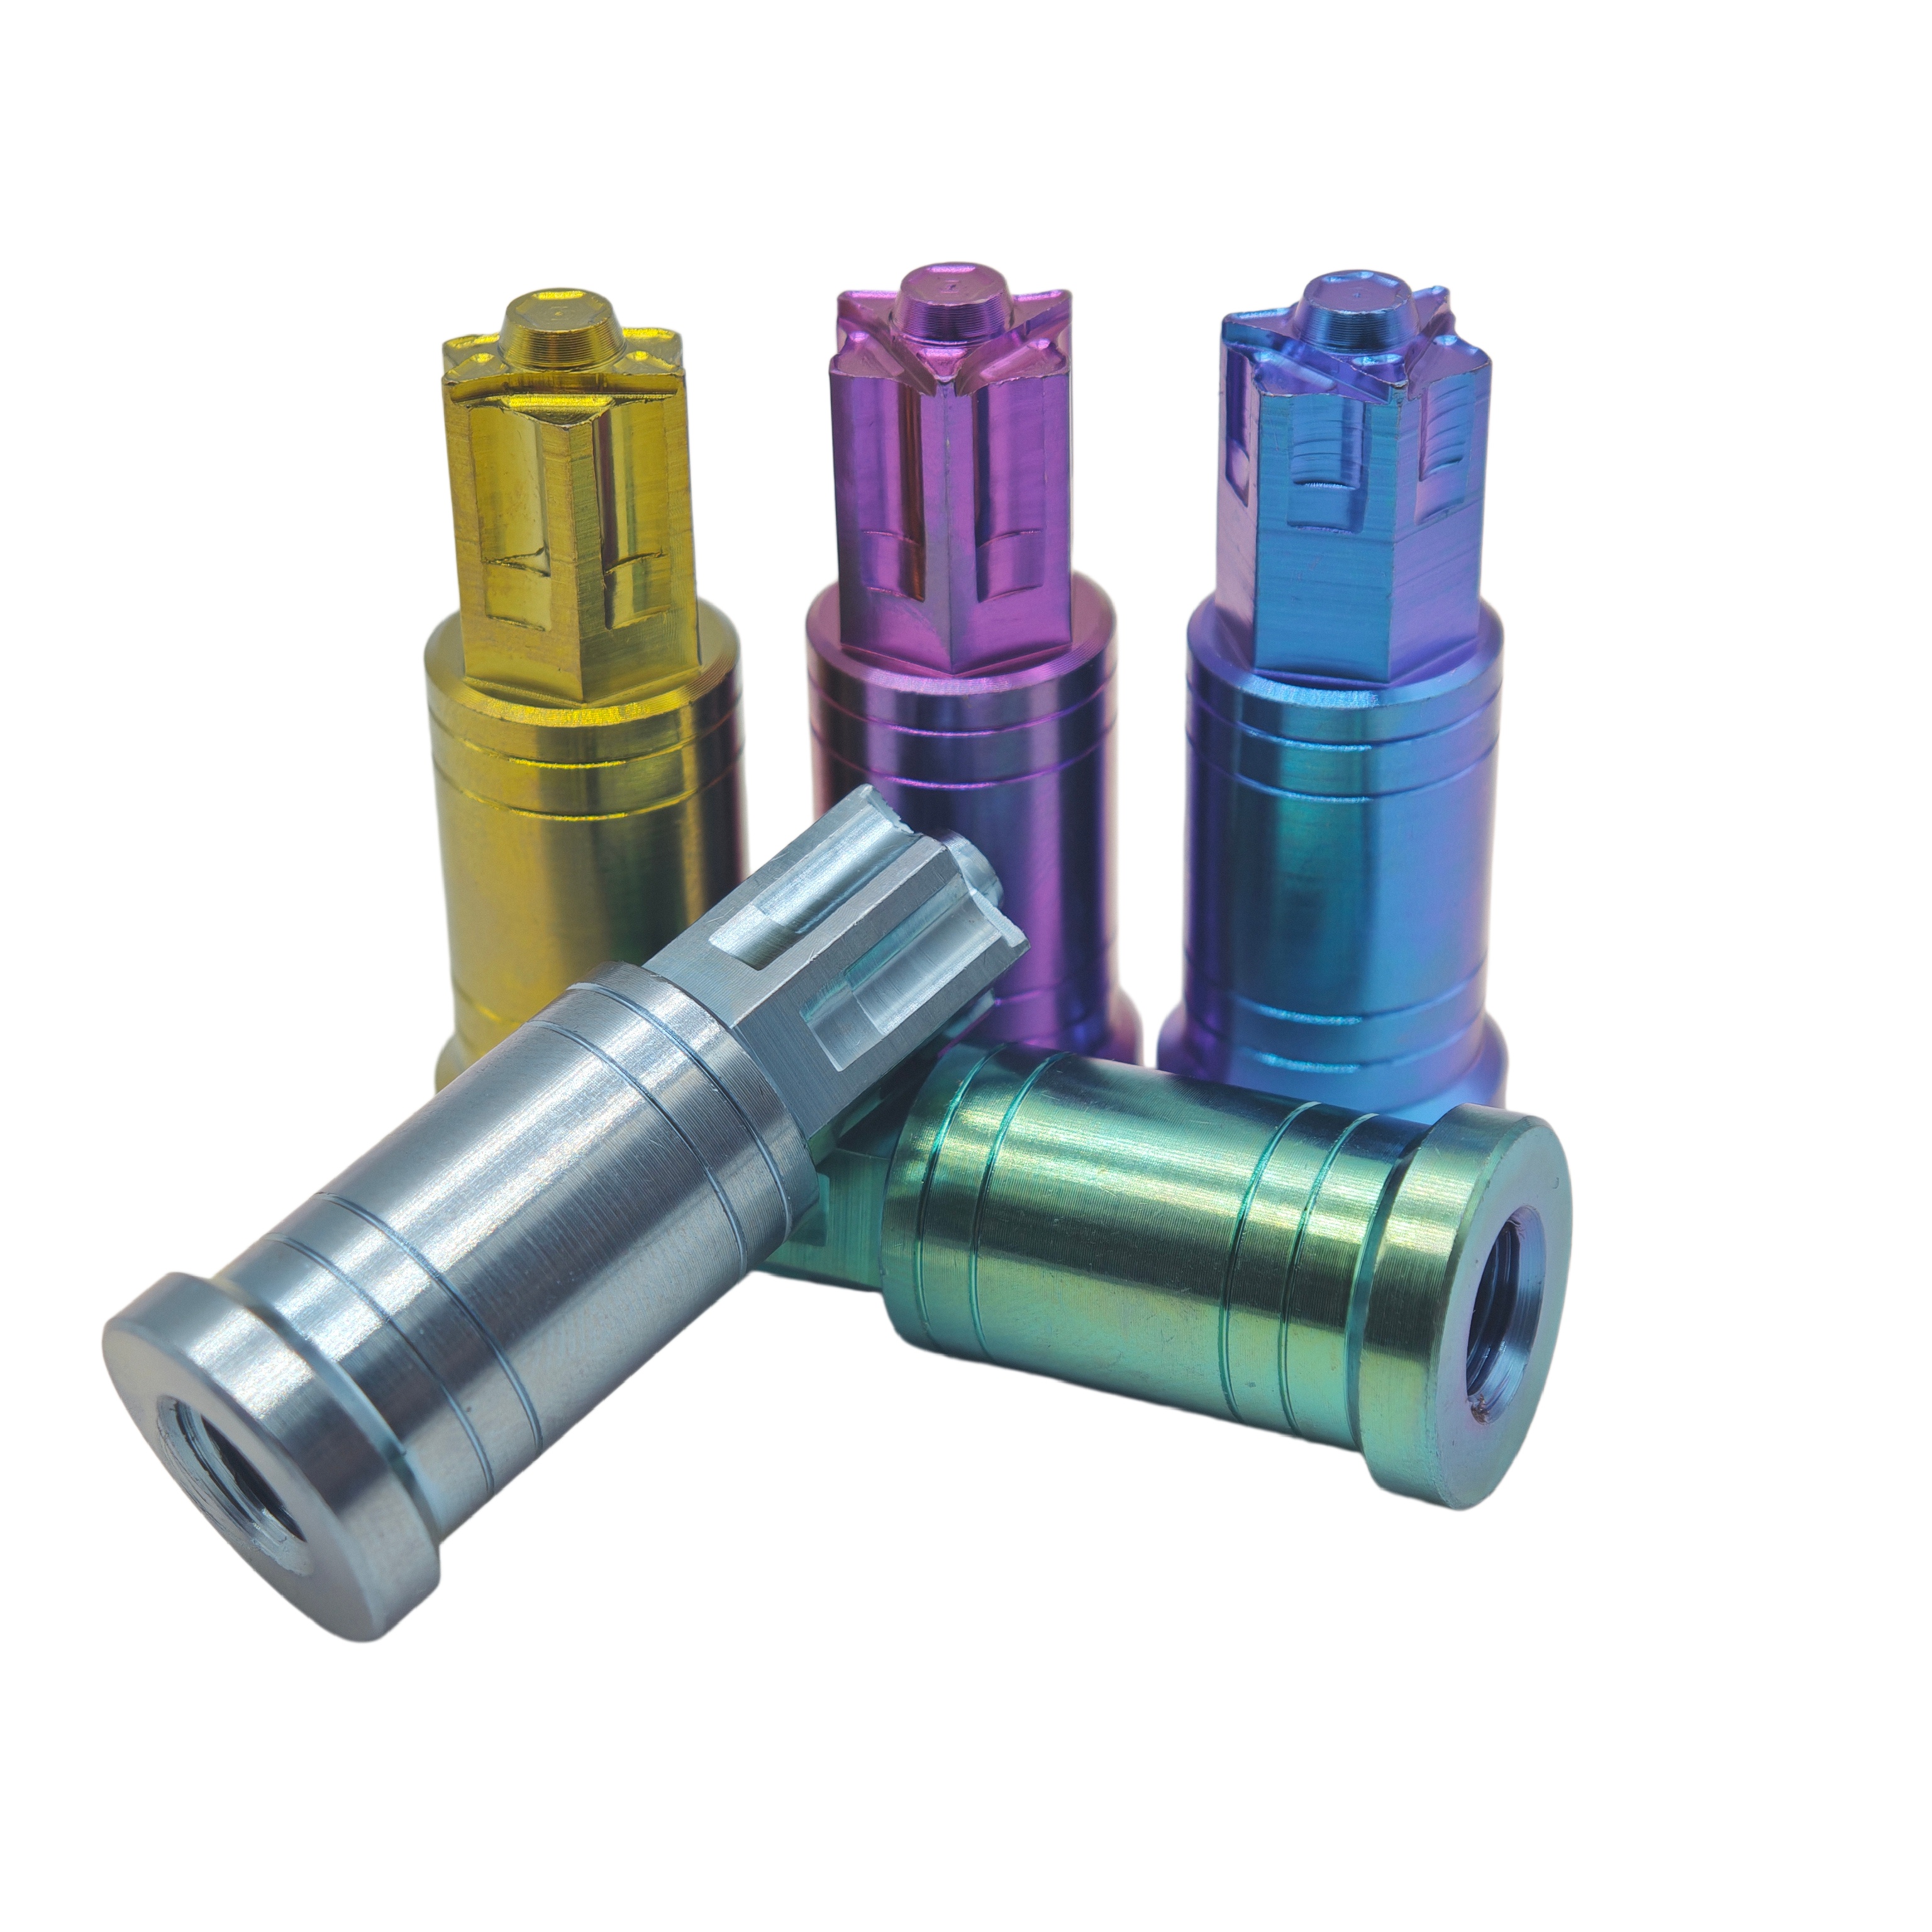
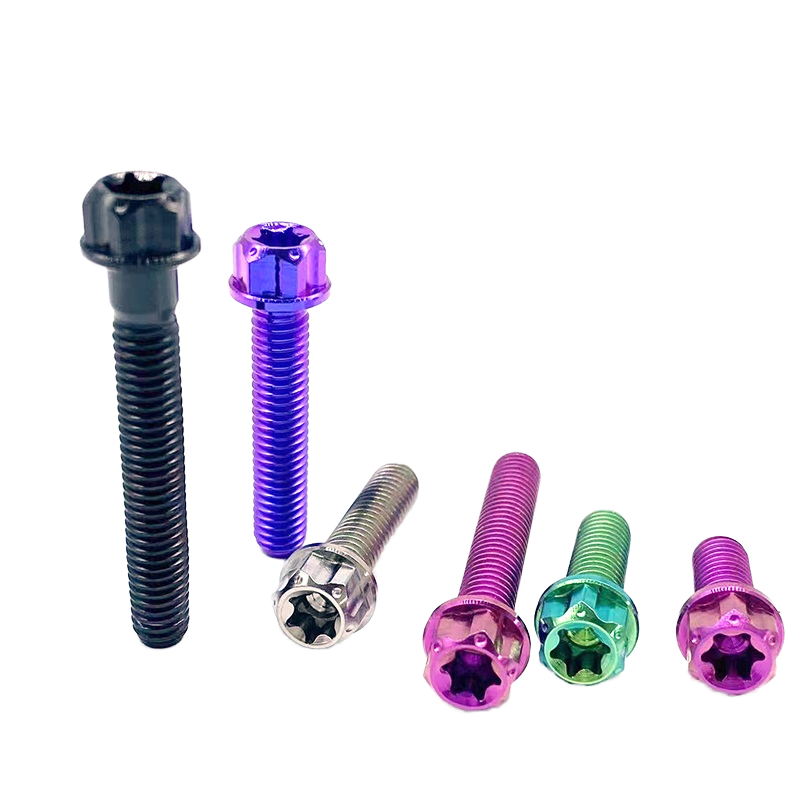
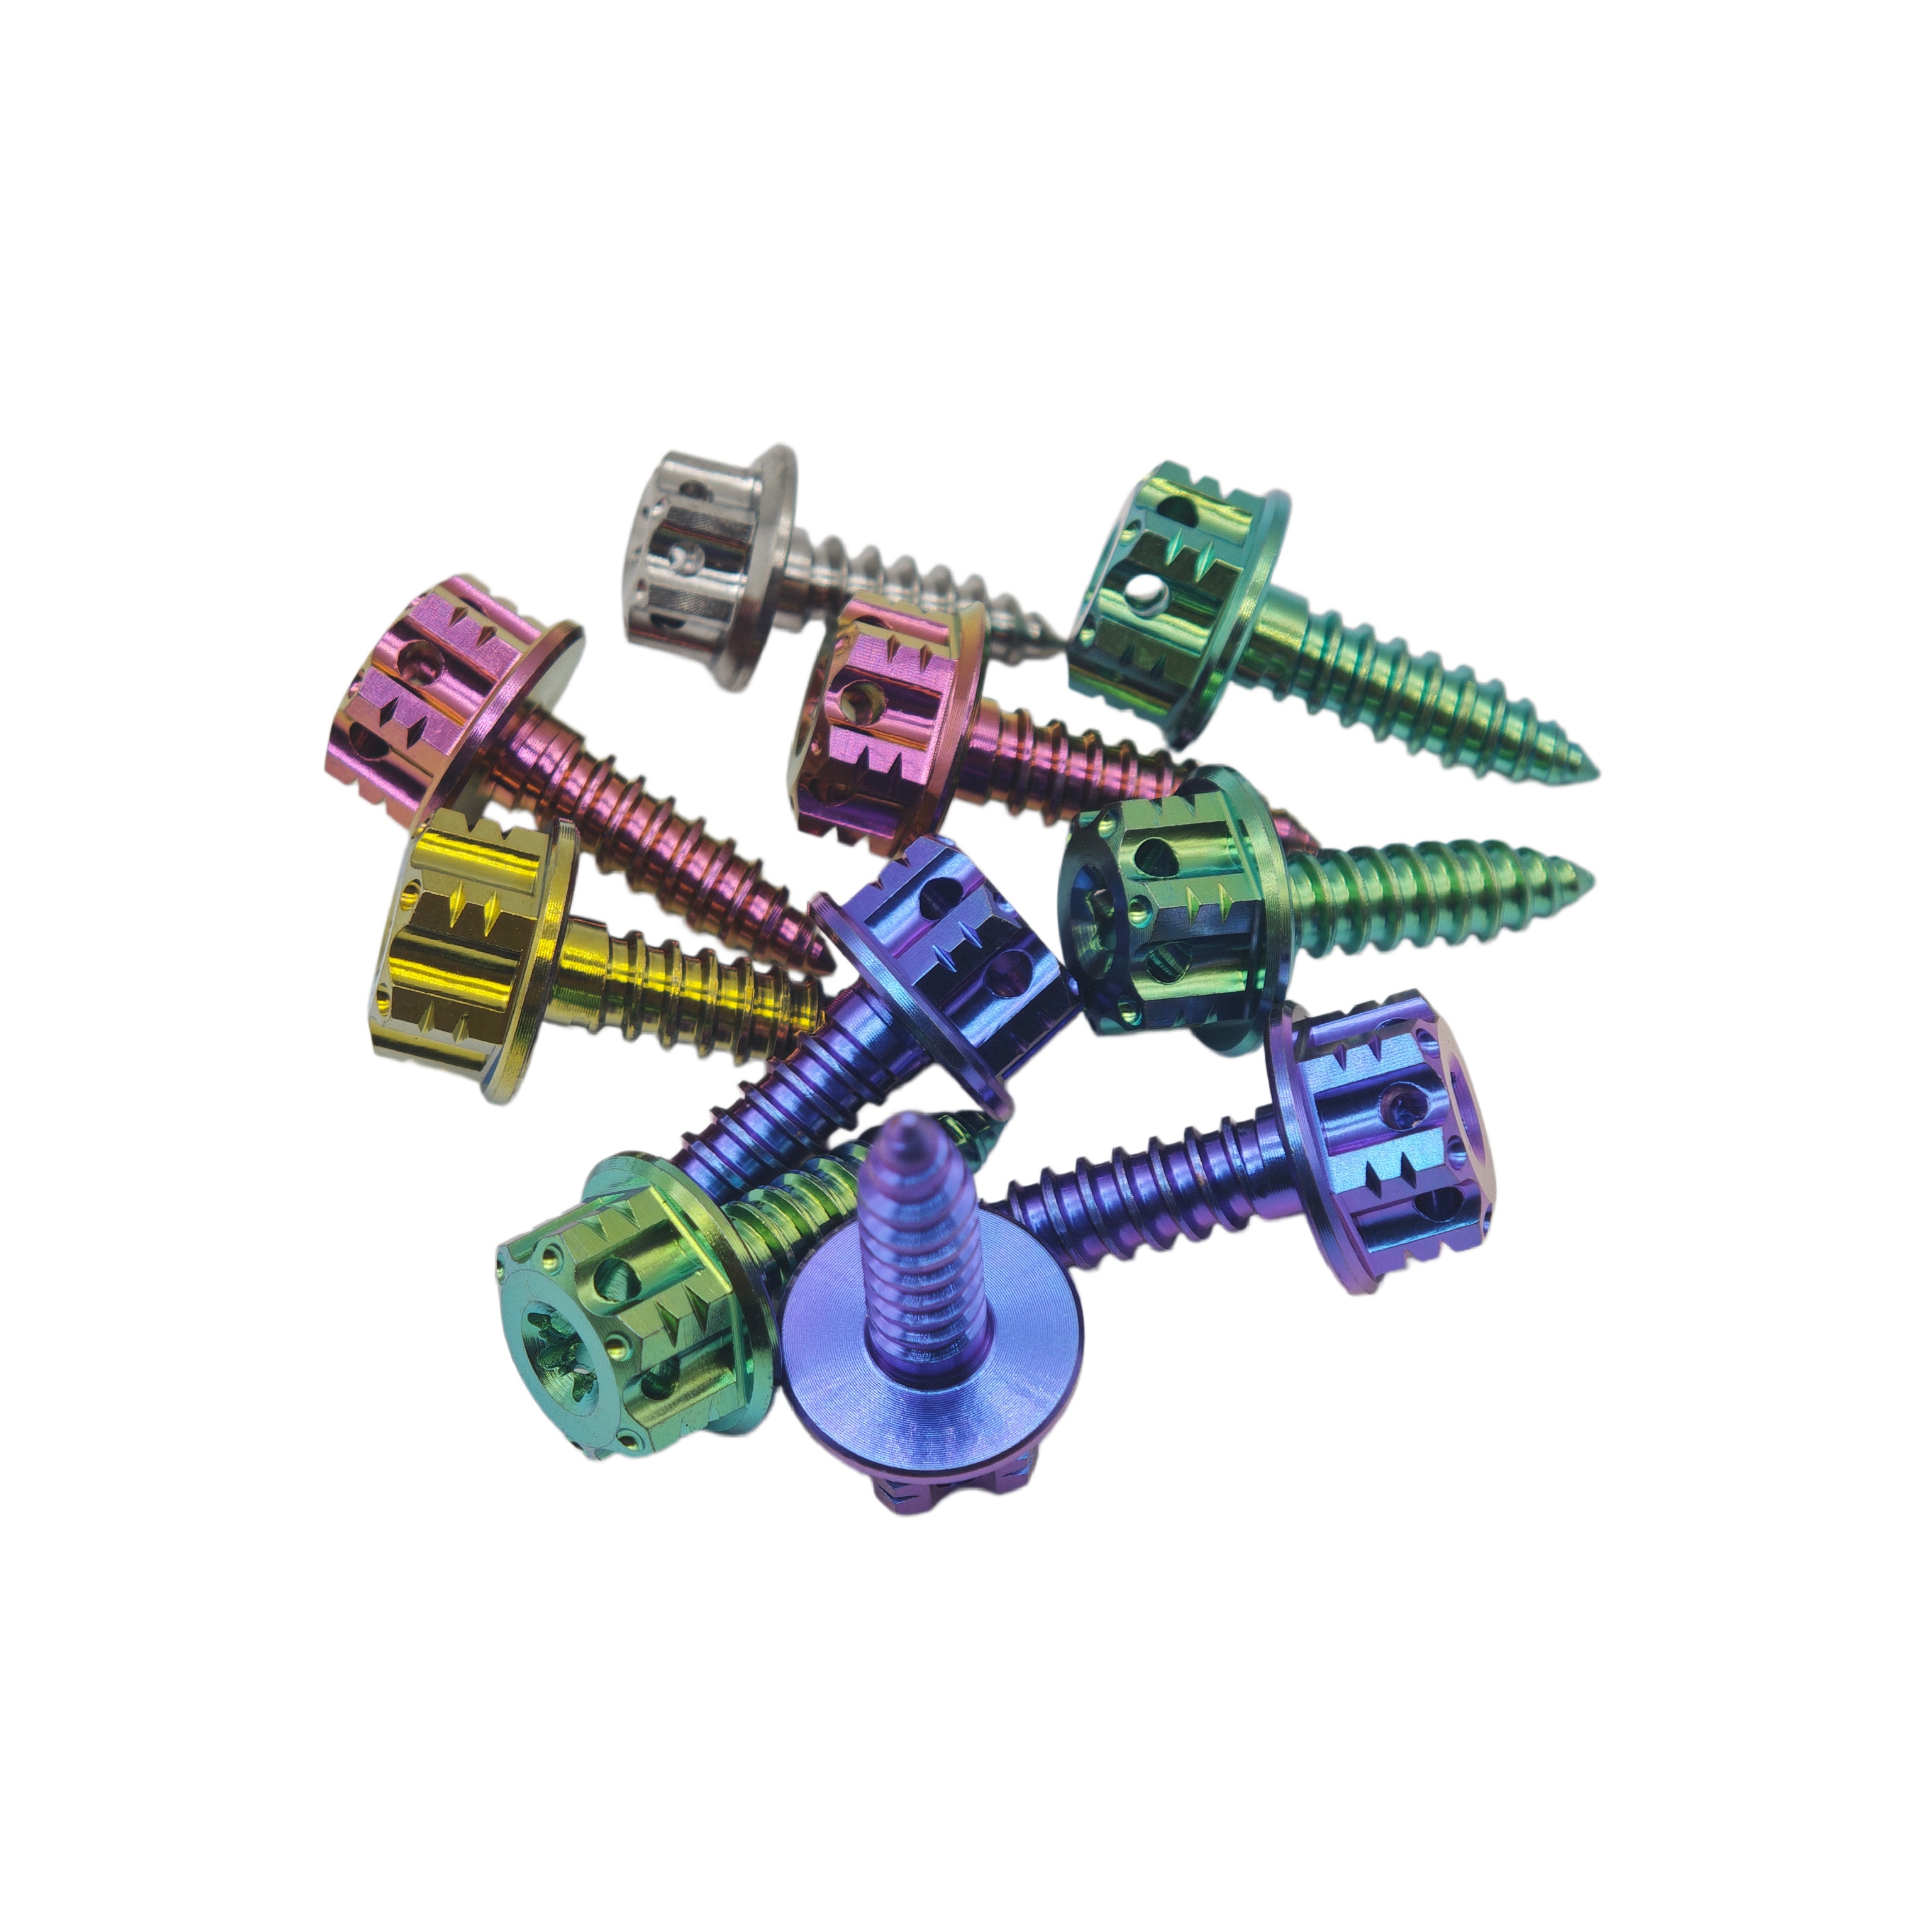
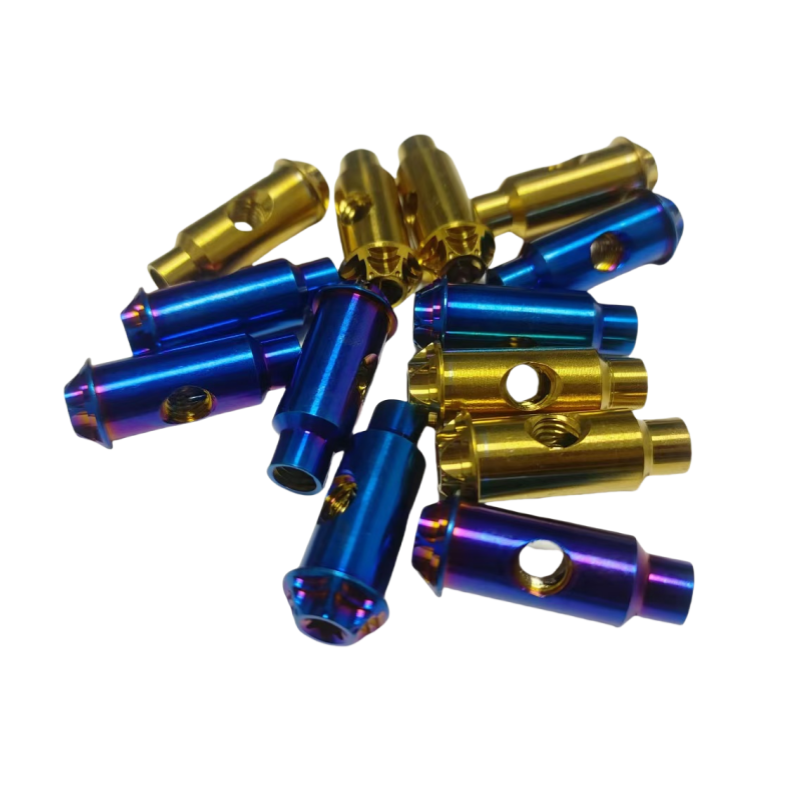
Engineering Benchmark: OEM Titanium Manifold Stud Systems in Extreme Thermal Environments
Why Tier-1 automotive powertrain engineers and race teams are replacing high-strength alloy steel and stainless studs with cold-rolled, hot-headed Ti-6Al-4V titanium manifold studs.
Thermal Creep & Expansion Differential
Exhaust headers experience continuous thermal cycling from ambient temperatures to over 800°C (1472°F). Standard steel studs possess a thermal expansion coefficient ($\approx 12 \times 10^{-6}/\text{K}$) that creates extreme fatigue strain against cast iron or aluminum cylinder heads. Grade 5 Titanium ($\approx 8.6 \times 10^{-6}/\text{K}$) closely matches modern aluminum head expansion rates, dramatically reducing stud necking and exhaust gasket blowout.
Thread Rolling vs. Cut Threads
Cutting threads into titanium bar stock creates localized micro-fractures and stress risers along the root radius. Zunvo Titanium enforces hot heading combined with planetary CNC thread rolling. This process compresses the grain structure along the thread contour, yielding a 30% higher shear strength and preventing fatigue failure under harmonic engine vibration.
Oxidation Resistance & Galling Prevention
At temperatures exceeding 500°C, untreated metals oxidize rapidly, causing exhaust nuts to seize or shear during maintenance. Our custom OEM manifold studs feature specialized physical vapor deposition (PVD) coatings or micro-arc oxidation (MAO) combined with copper-based anti-seize lubrication protocols, guaranteeing clean disassembly even after thousands of heat cycles.
OEM Procurement Insight: Grade 5 Titanium (Ti-6Al-4V) provides a minimum tensile strength of 895 MPa (equivalent to Class 10.9 steel fasteners) while dropping total mass by 44%. In turbocharger and exhaust manifold assemblies, replacing 16 OEM steel studs and hex nuts with titanium reduces unsprung thermal mass on engine mounts and eliminates galvanic corrosion caused by harsh winter road salts.
| Material Specification | Yield Strength (MPa) | Tensile Strength (MPa) | Density (g/cm³) | Thermal Coeff. (10⁻⁶/K) | Exhaust Resistance |
|---|---|---|---|---|---|
| Gr5 Titanium (Ti-6Al-4V) | 828 - 910 | 895 - 1000 | 4.43 | 8.6 | Superior |
| Class 10.9 Alloy Steel | 940 | 1040 | 7.85 | 12.0 | Poor (Corrodes) |
| 304/316 Stainless Steel | 205 - 290 | 515 - 620 | 8.00 | 16.0 - 17.3 | Moderate (Galls) |
| Inconel 718 (High-Temp Nickel) | 1100 | 1375 | 8.19 | 13.0 | Excellent (Heavy) |
Future Sourcing Trends for OEM Titanium Fasteners & Manifold Assemblies
Analyzing shifts in global automotive supply chains, aerospace manufacturing, and motorsport procurement strategies.
1. Transition from Cast Iron to Downsized Hybrid Turbo Powertrains
Modern internal combustion engines (ICE) and hybrid electric vehicles (HEV) use smaller, higher-boost turbocharged engines. Exhaust gas temperatures (EGT) frequently exceed 850°C. OEM procurement departments are mandating custom titanium hardware as standard equipment to handle elevated thermal expansion stresses without structural failure.
2. Demand for Complete Assemblies & Locking Flange Nut Systems
Global buyers are shifting away from purchasing isolated studs or nuts. Future B2B procurement trends favor complete factory kits containing pre-lubricated studs, serrated lock nuts, and double-ended threaded dowels with custom pitch variations (e.g., M10x1.25 to M10x1.5 pitch conversions for aftermarket cylinder heads).
3. Near-Net-Shape Cold Forging & Digital Traceability
Environmental regulations and raw material cost optimization require factories to implement near-net-shape hot heading and precision cold forging. Combined with 100% digital optical sorting and EN 10204 3.1 mill test certification per heat lot, buyers demand total transparency from raw titanium sponge to final shipment.
Why Top Global Brands Partner with Zunvo Titanium Products
Located in Baoji, Shaanxi — China's "Titanium Valley" — Zunvo Titanium Products Co., Ltd. integrates raw titanium processing, CNC multi-axis turning, and custom OEM manufacturing under one verified roof.
Baoji Supply Cluster & Raw Material Traceability
Direct proximity to titanium smelters enables instant sourcing of certified Grade 5 Ti-6Al-4V, Grade 2, and Grade 9 bar stocks. Every production batch includes full material test certificates (MTC) linked directly to the melt heat number.
3-Day Samples & Rapid Production Cycles
Our engineering team evaluates STEP/CAD drawings within 24 hours. Prototype custom manifold studs are machined and dispatched within 3 business days, with full production batch lead times averaging 7 to 15 days.
Advanced CNC Machining & Custom Surface Finishes
Equipped with 5-axis CNC turning centers, automatic thread rollers, and precision anodizing baths. We supply plain polished, PVD burnt blue, rainbow, gold, nitride black, and hard-anodized protective finishes.
100% Quality Assurance & Low MOQs
Every manifold stud, hex nut, and brake disc screw undergoes 100% go/no-go thread gauge verification and visual inspection before packaging. Flexible MOQs start from just 100 pieces for custom drawing projects.
Frequently Asked Questions for OEM Titanium Fastener Sourcing
Answers to common technical questions asked by purchasing directors, motorsport engineers, and industrial distributors.
Why should we choose Grade 5 Ti-6Al-4V instead of stainless steel for exhaust manifold studs?
What torque values should be applied when installing custom titanium manifold studs?
Can your factory produce custom thread pitches and non-standard stud dimensions from CAD files?
How does your factory prevent thread galling on titanium nuts and studs?
What are the minimum order quantities (MOQ) and production lead times for custom orders?
Do you provide material test certificates (MTC) and quality reports?
Ready to Upgrade Your Exhaust Hardware to Grade 5 Titanium?
Submit your technical drawings or request a direct factory quotation today. Our engineering team responds within 7 hours with full manufacturability analysis and volume pricing.
Contact Us