Grade 5
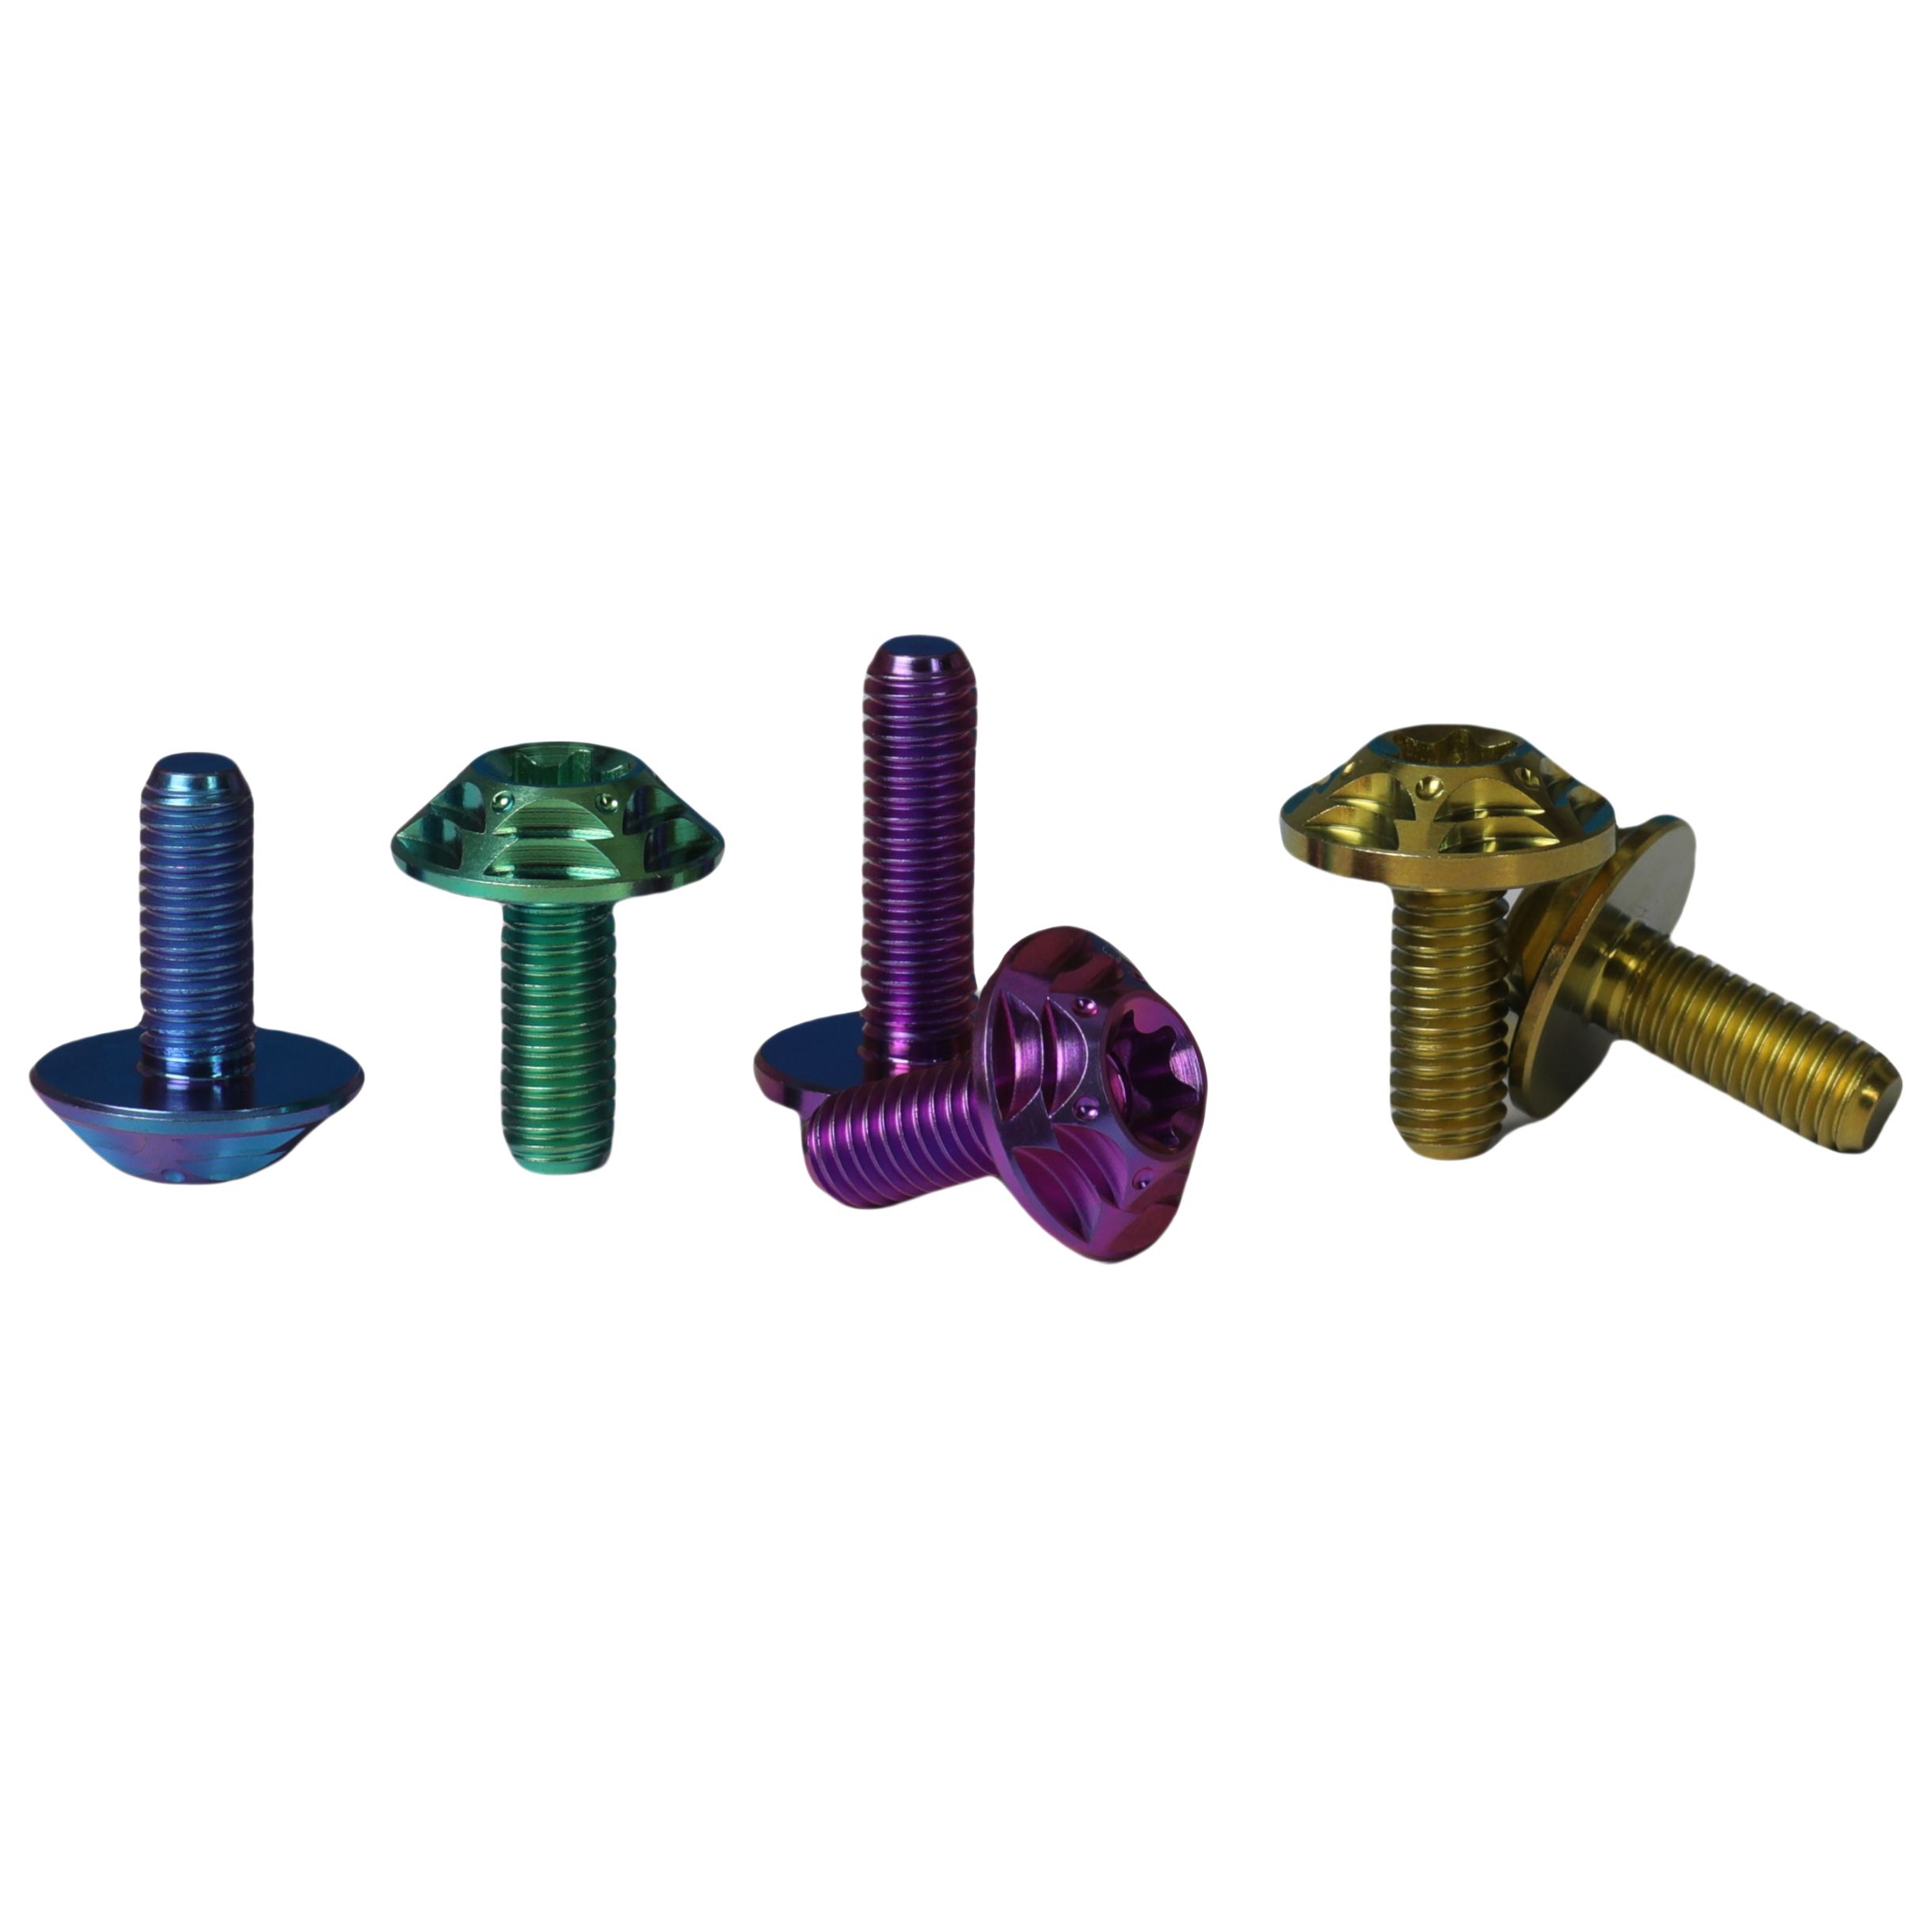
Direct factory supply from Baoji Titanium Valley. Fully customizable thread pitch, slotted geometry, and physical vapor deposition (PVD) finishes.
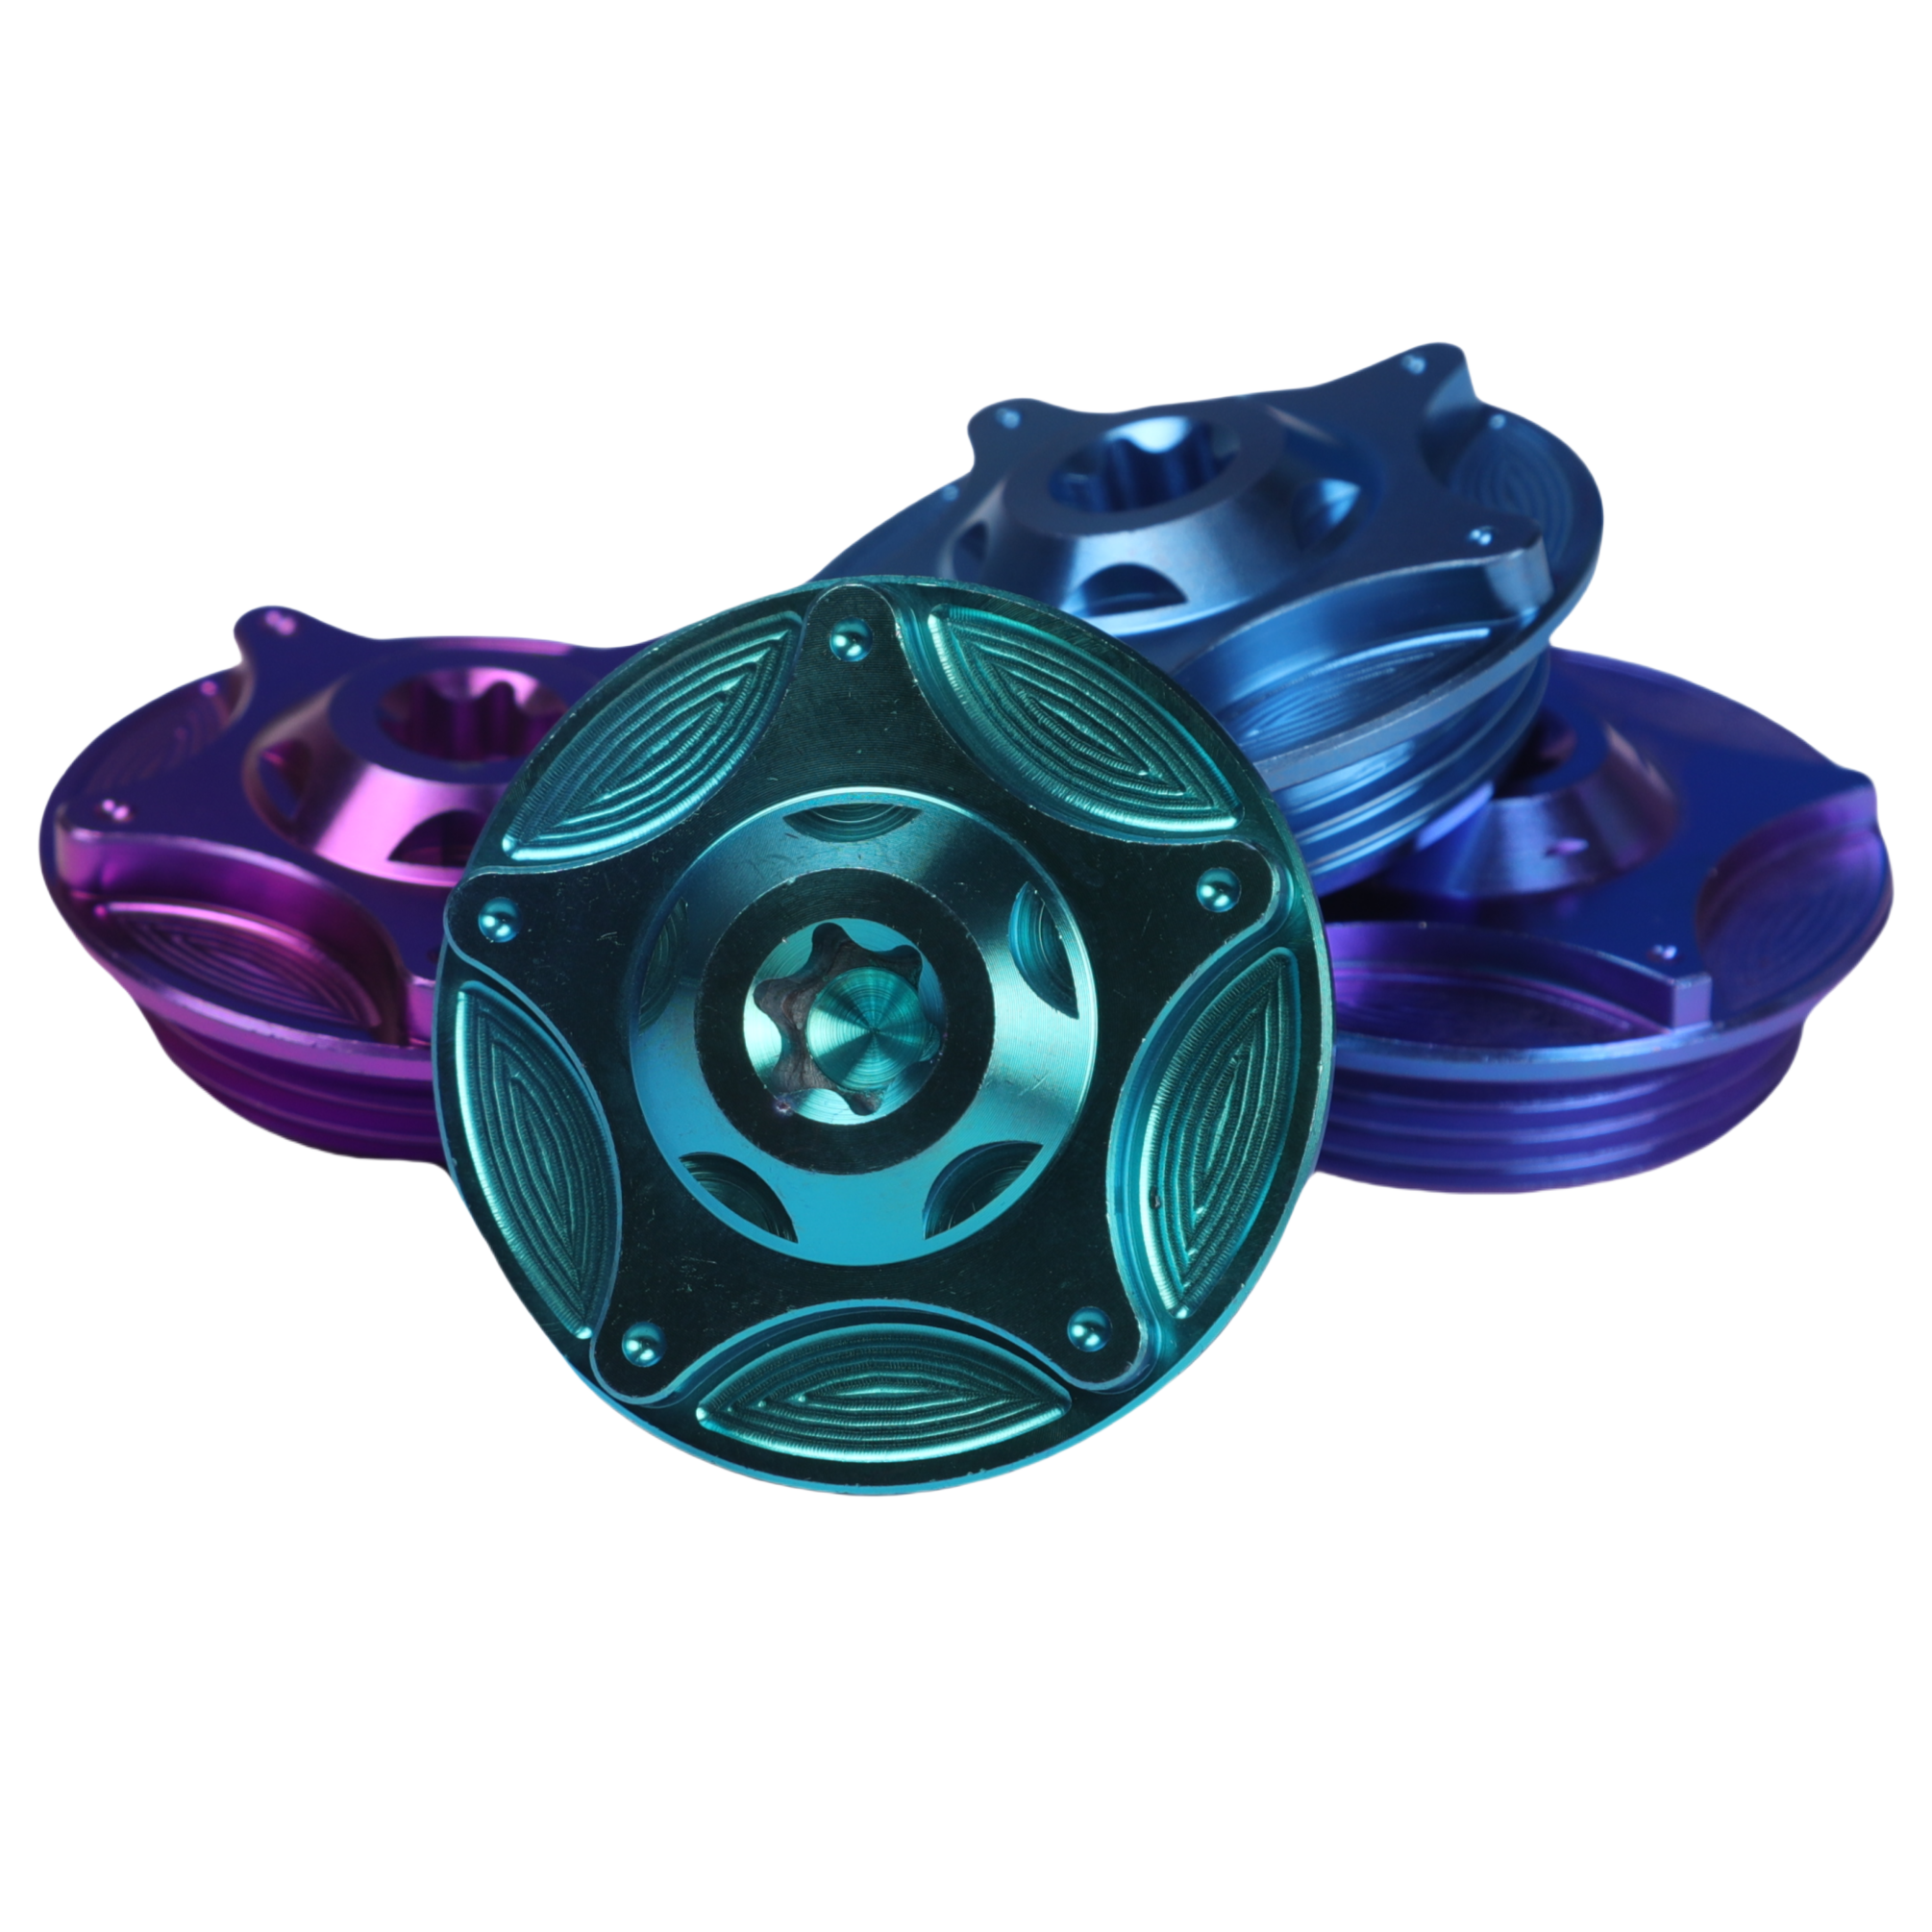
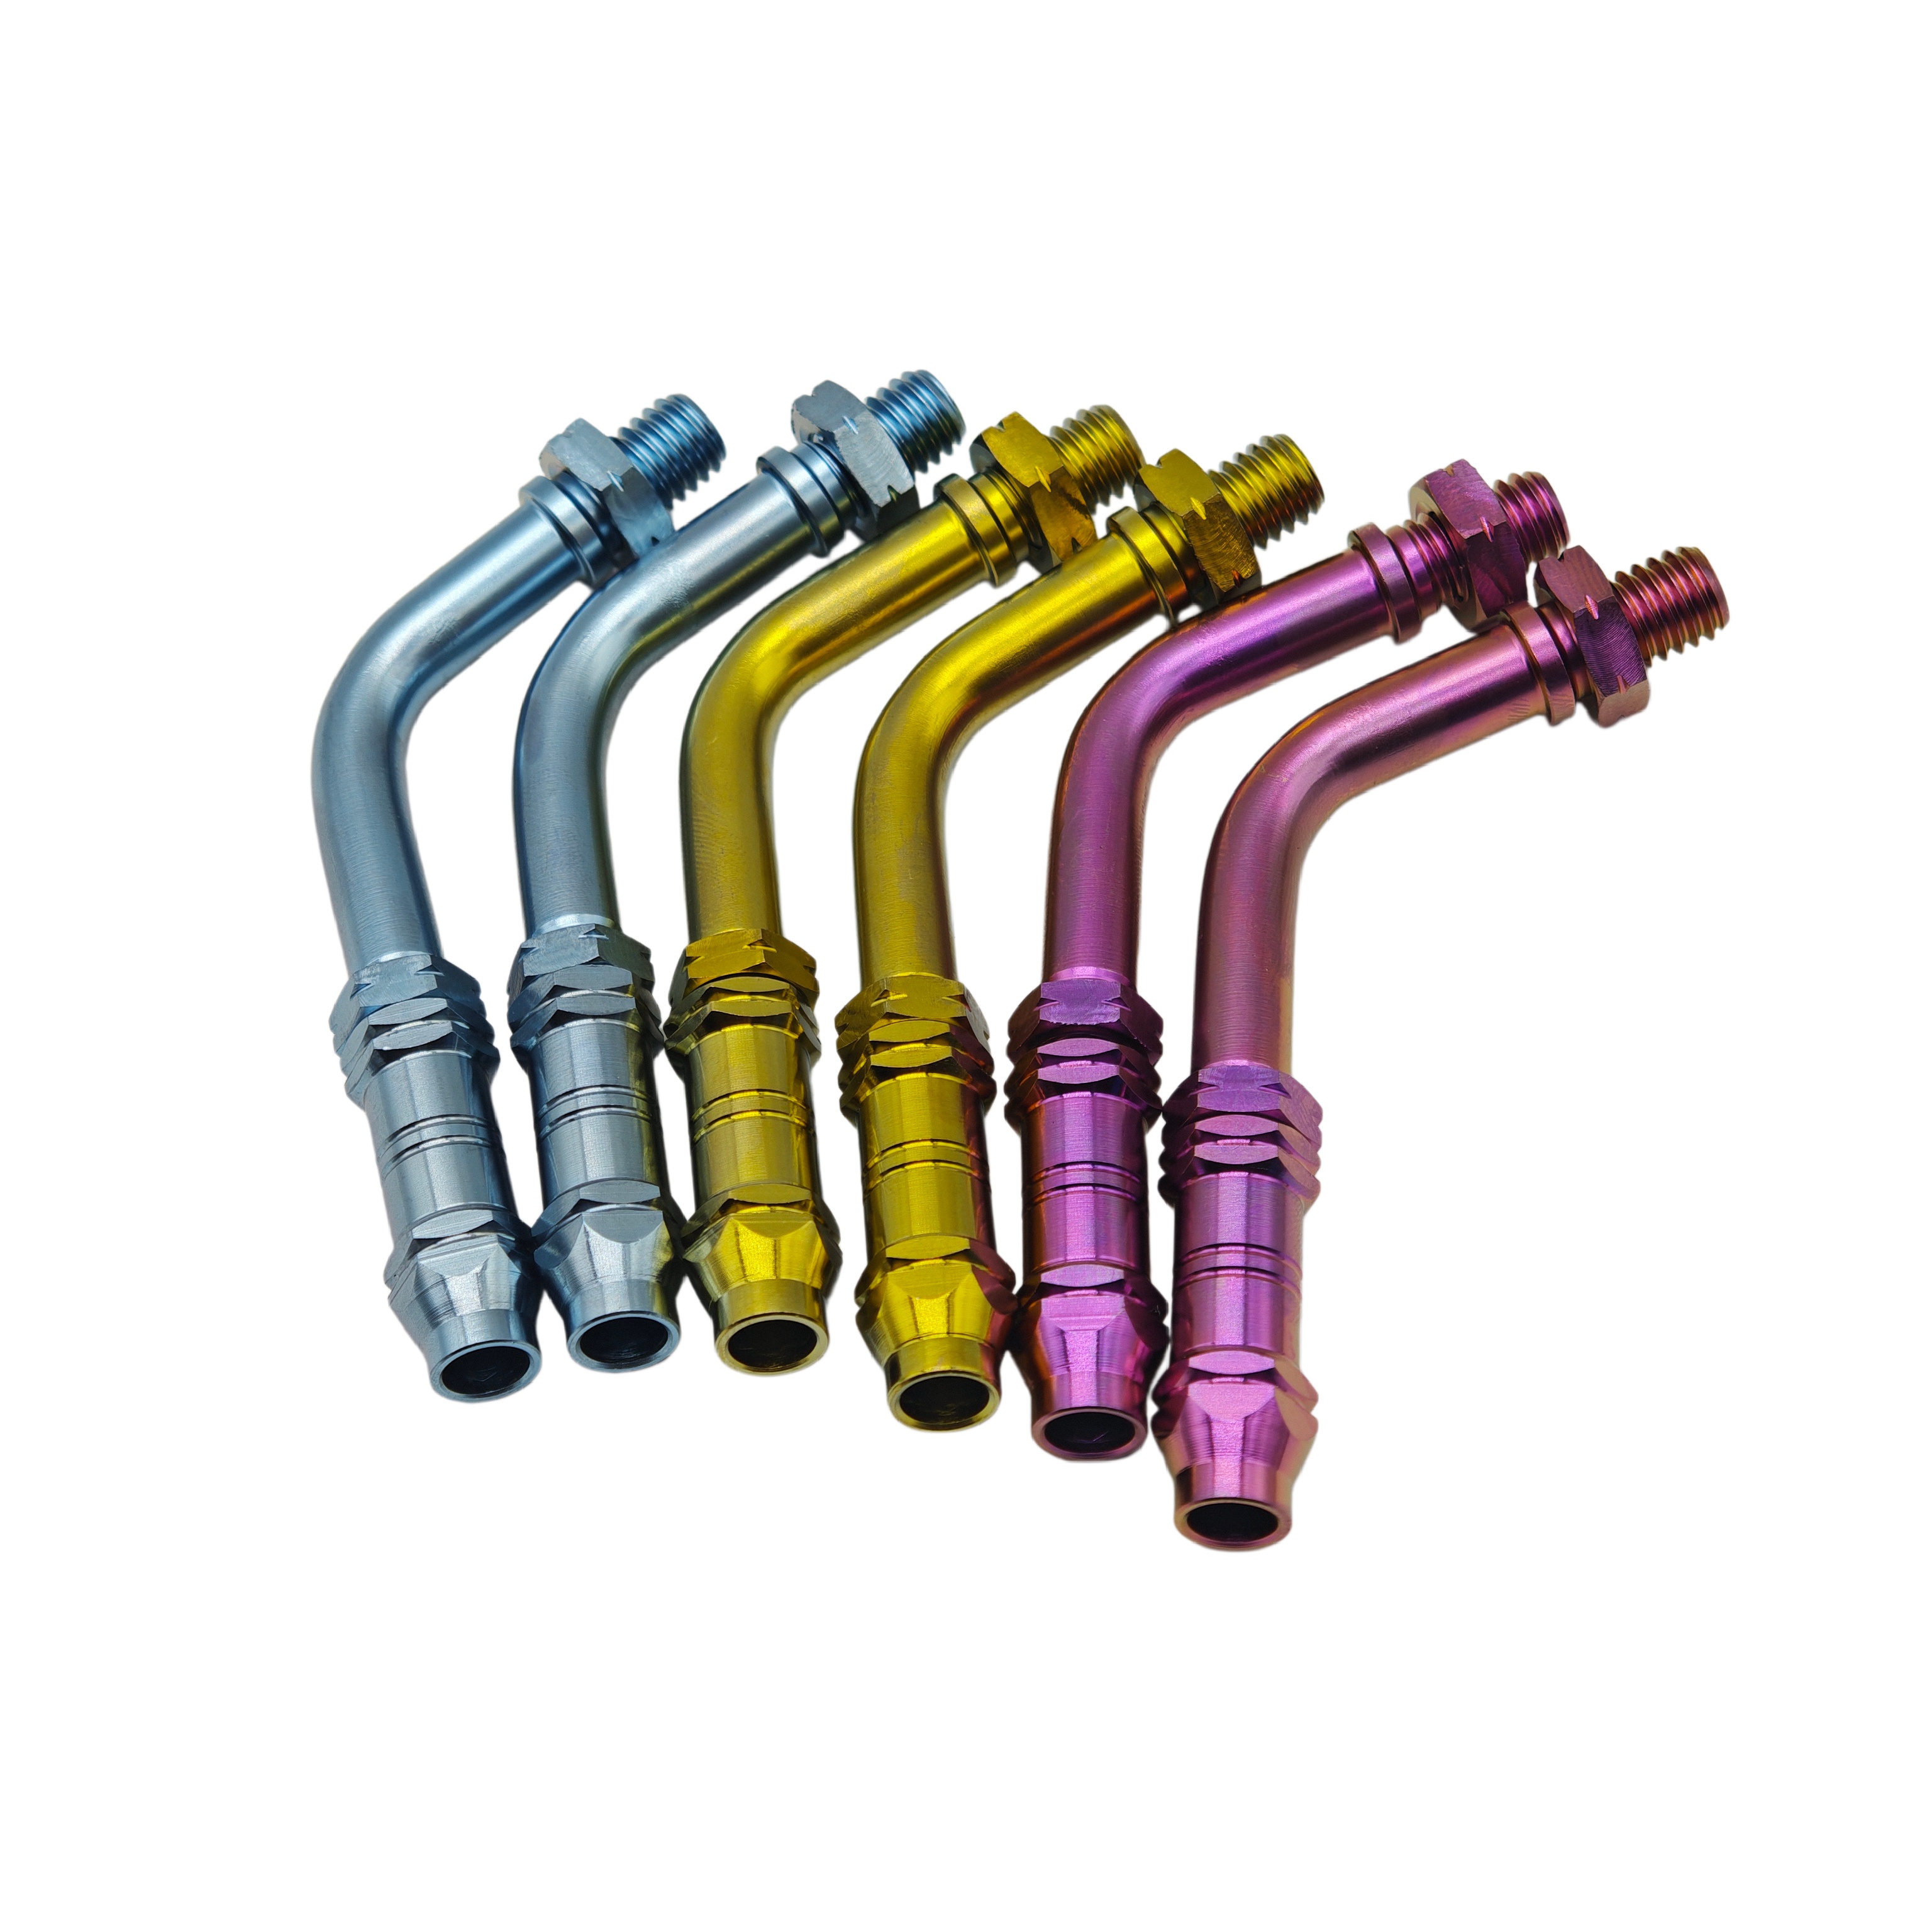
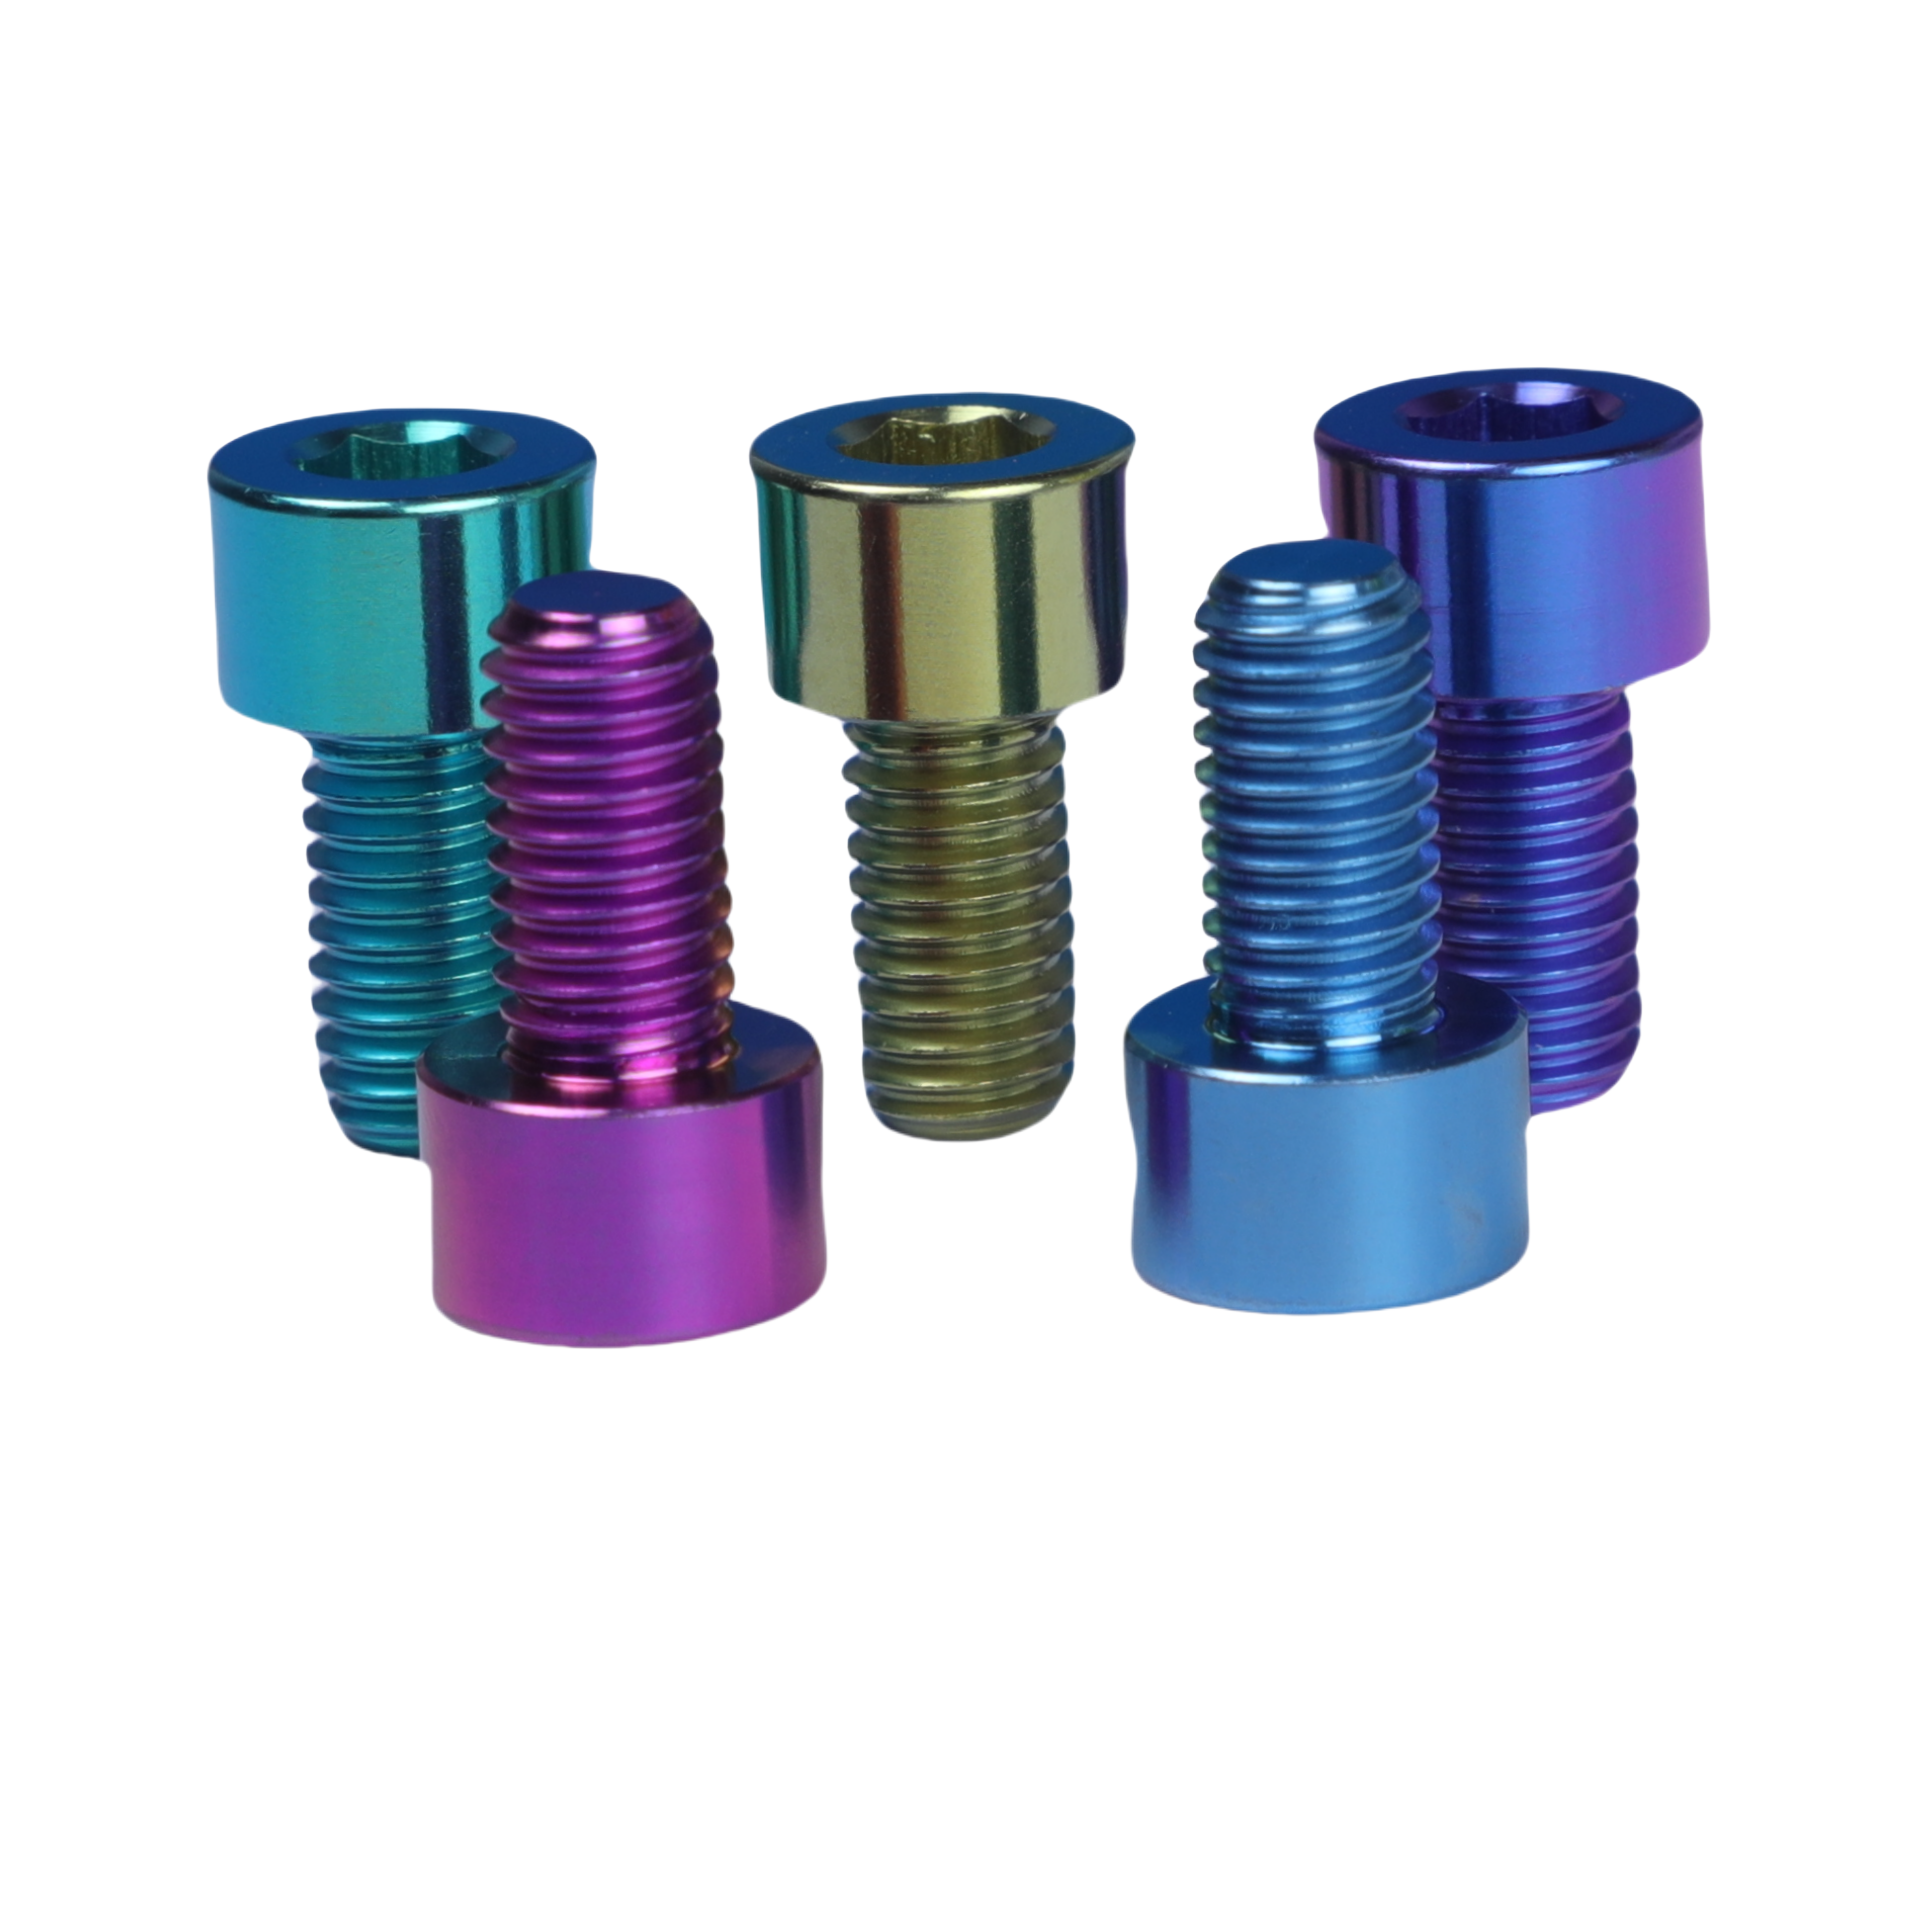
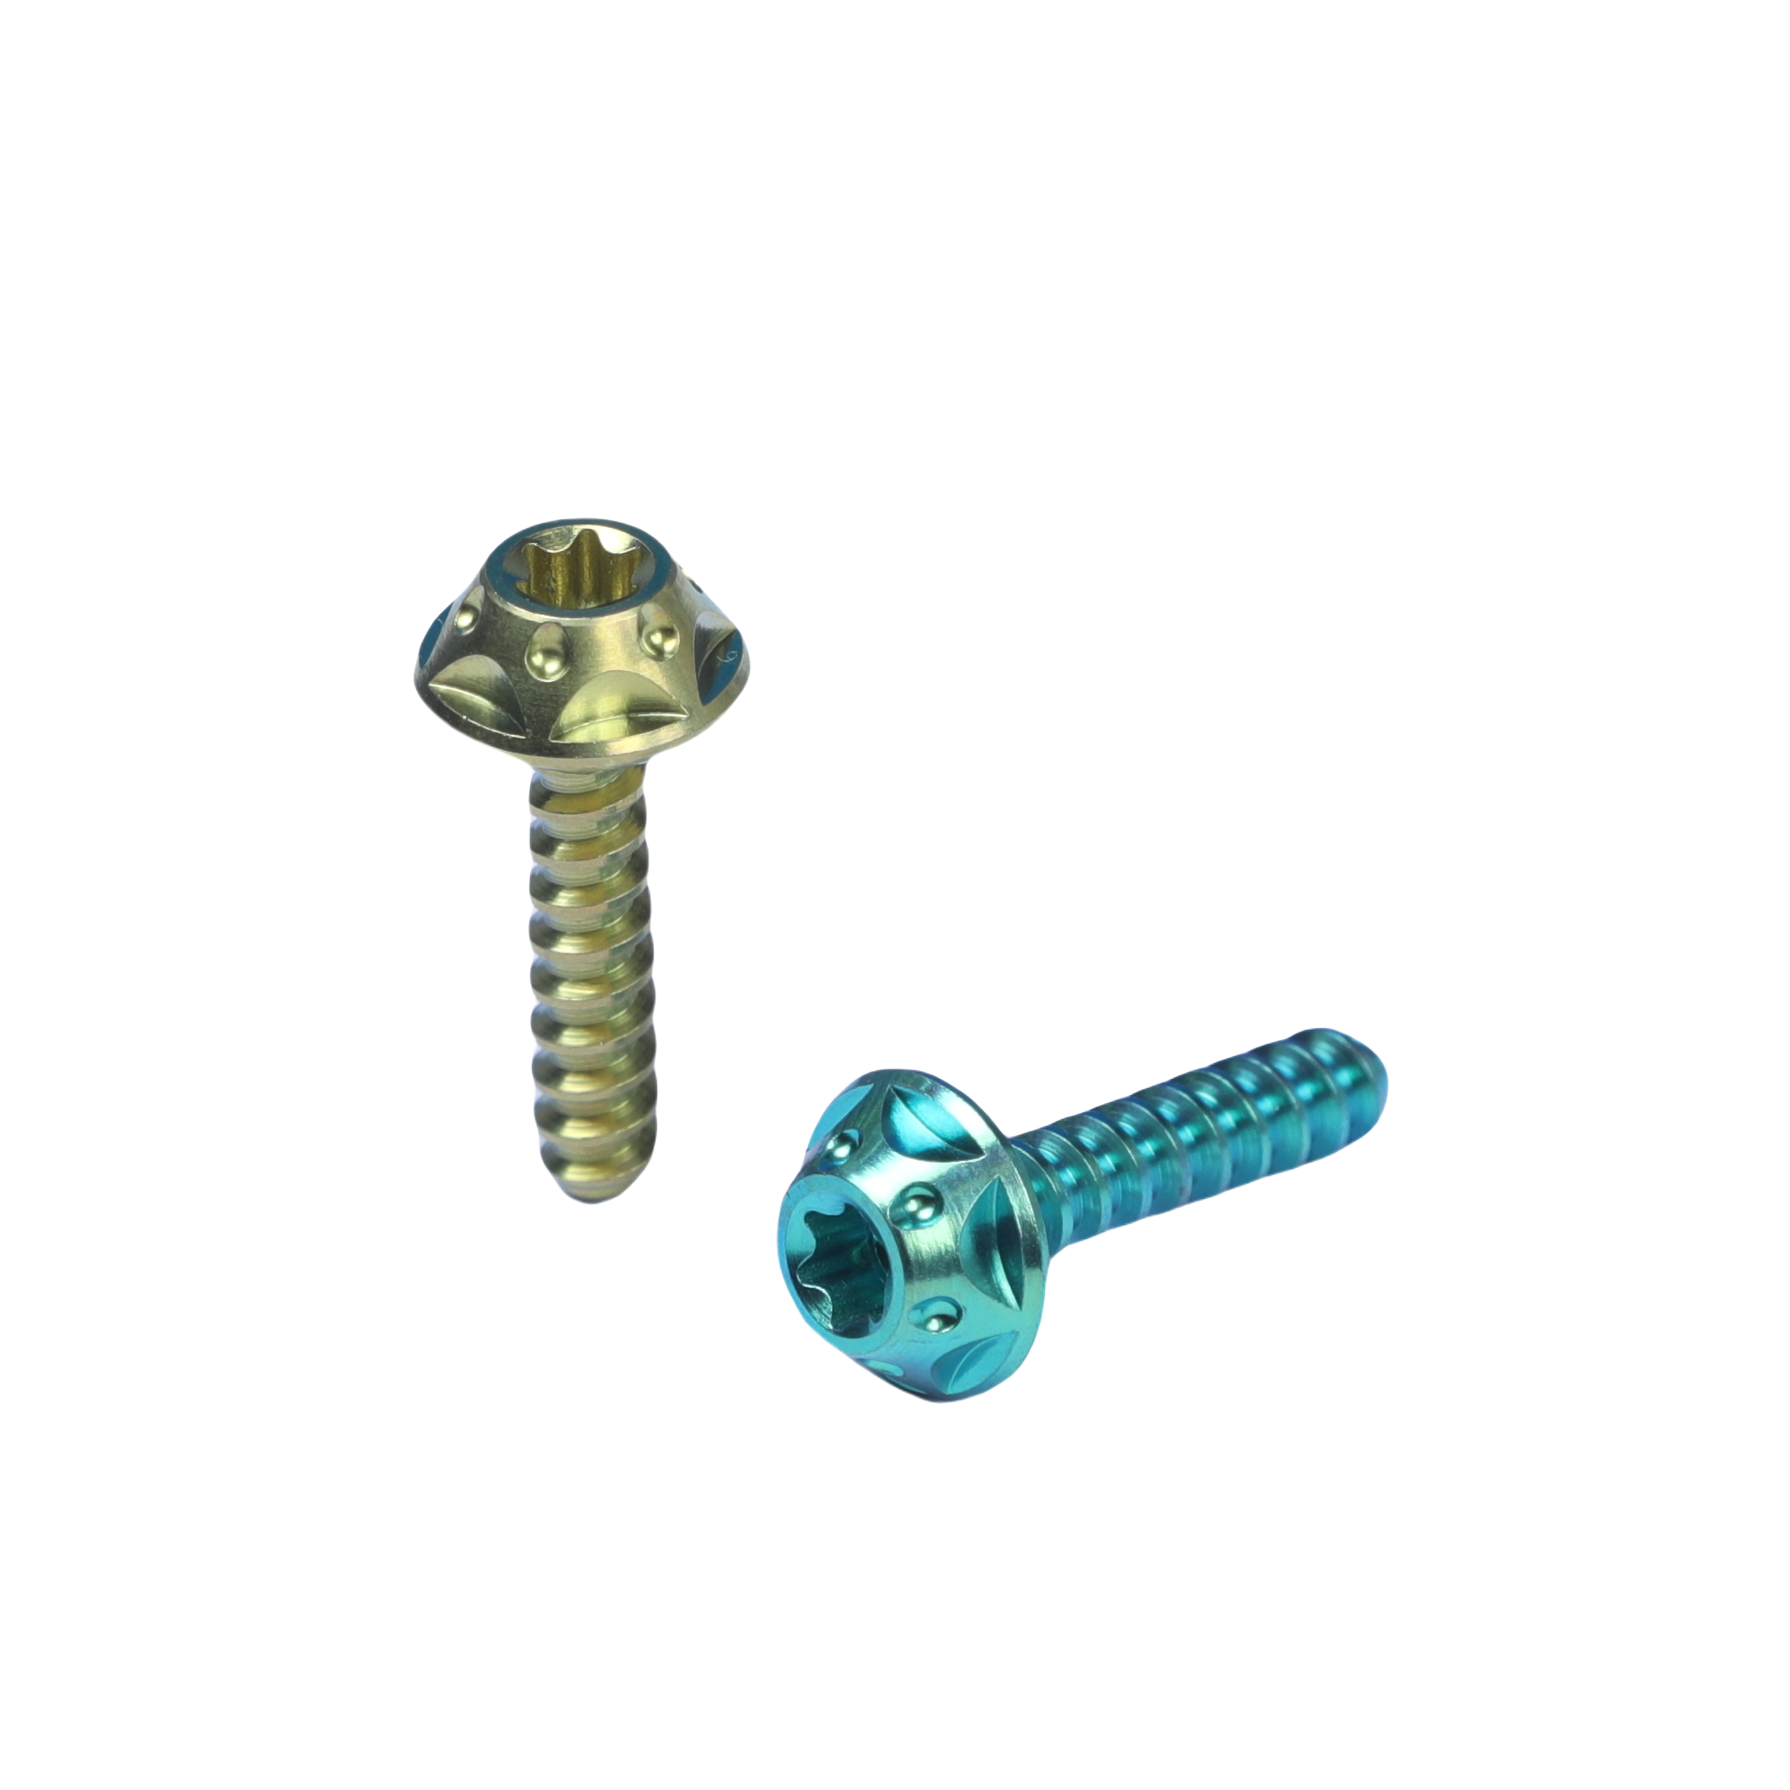
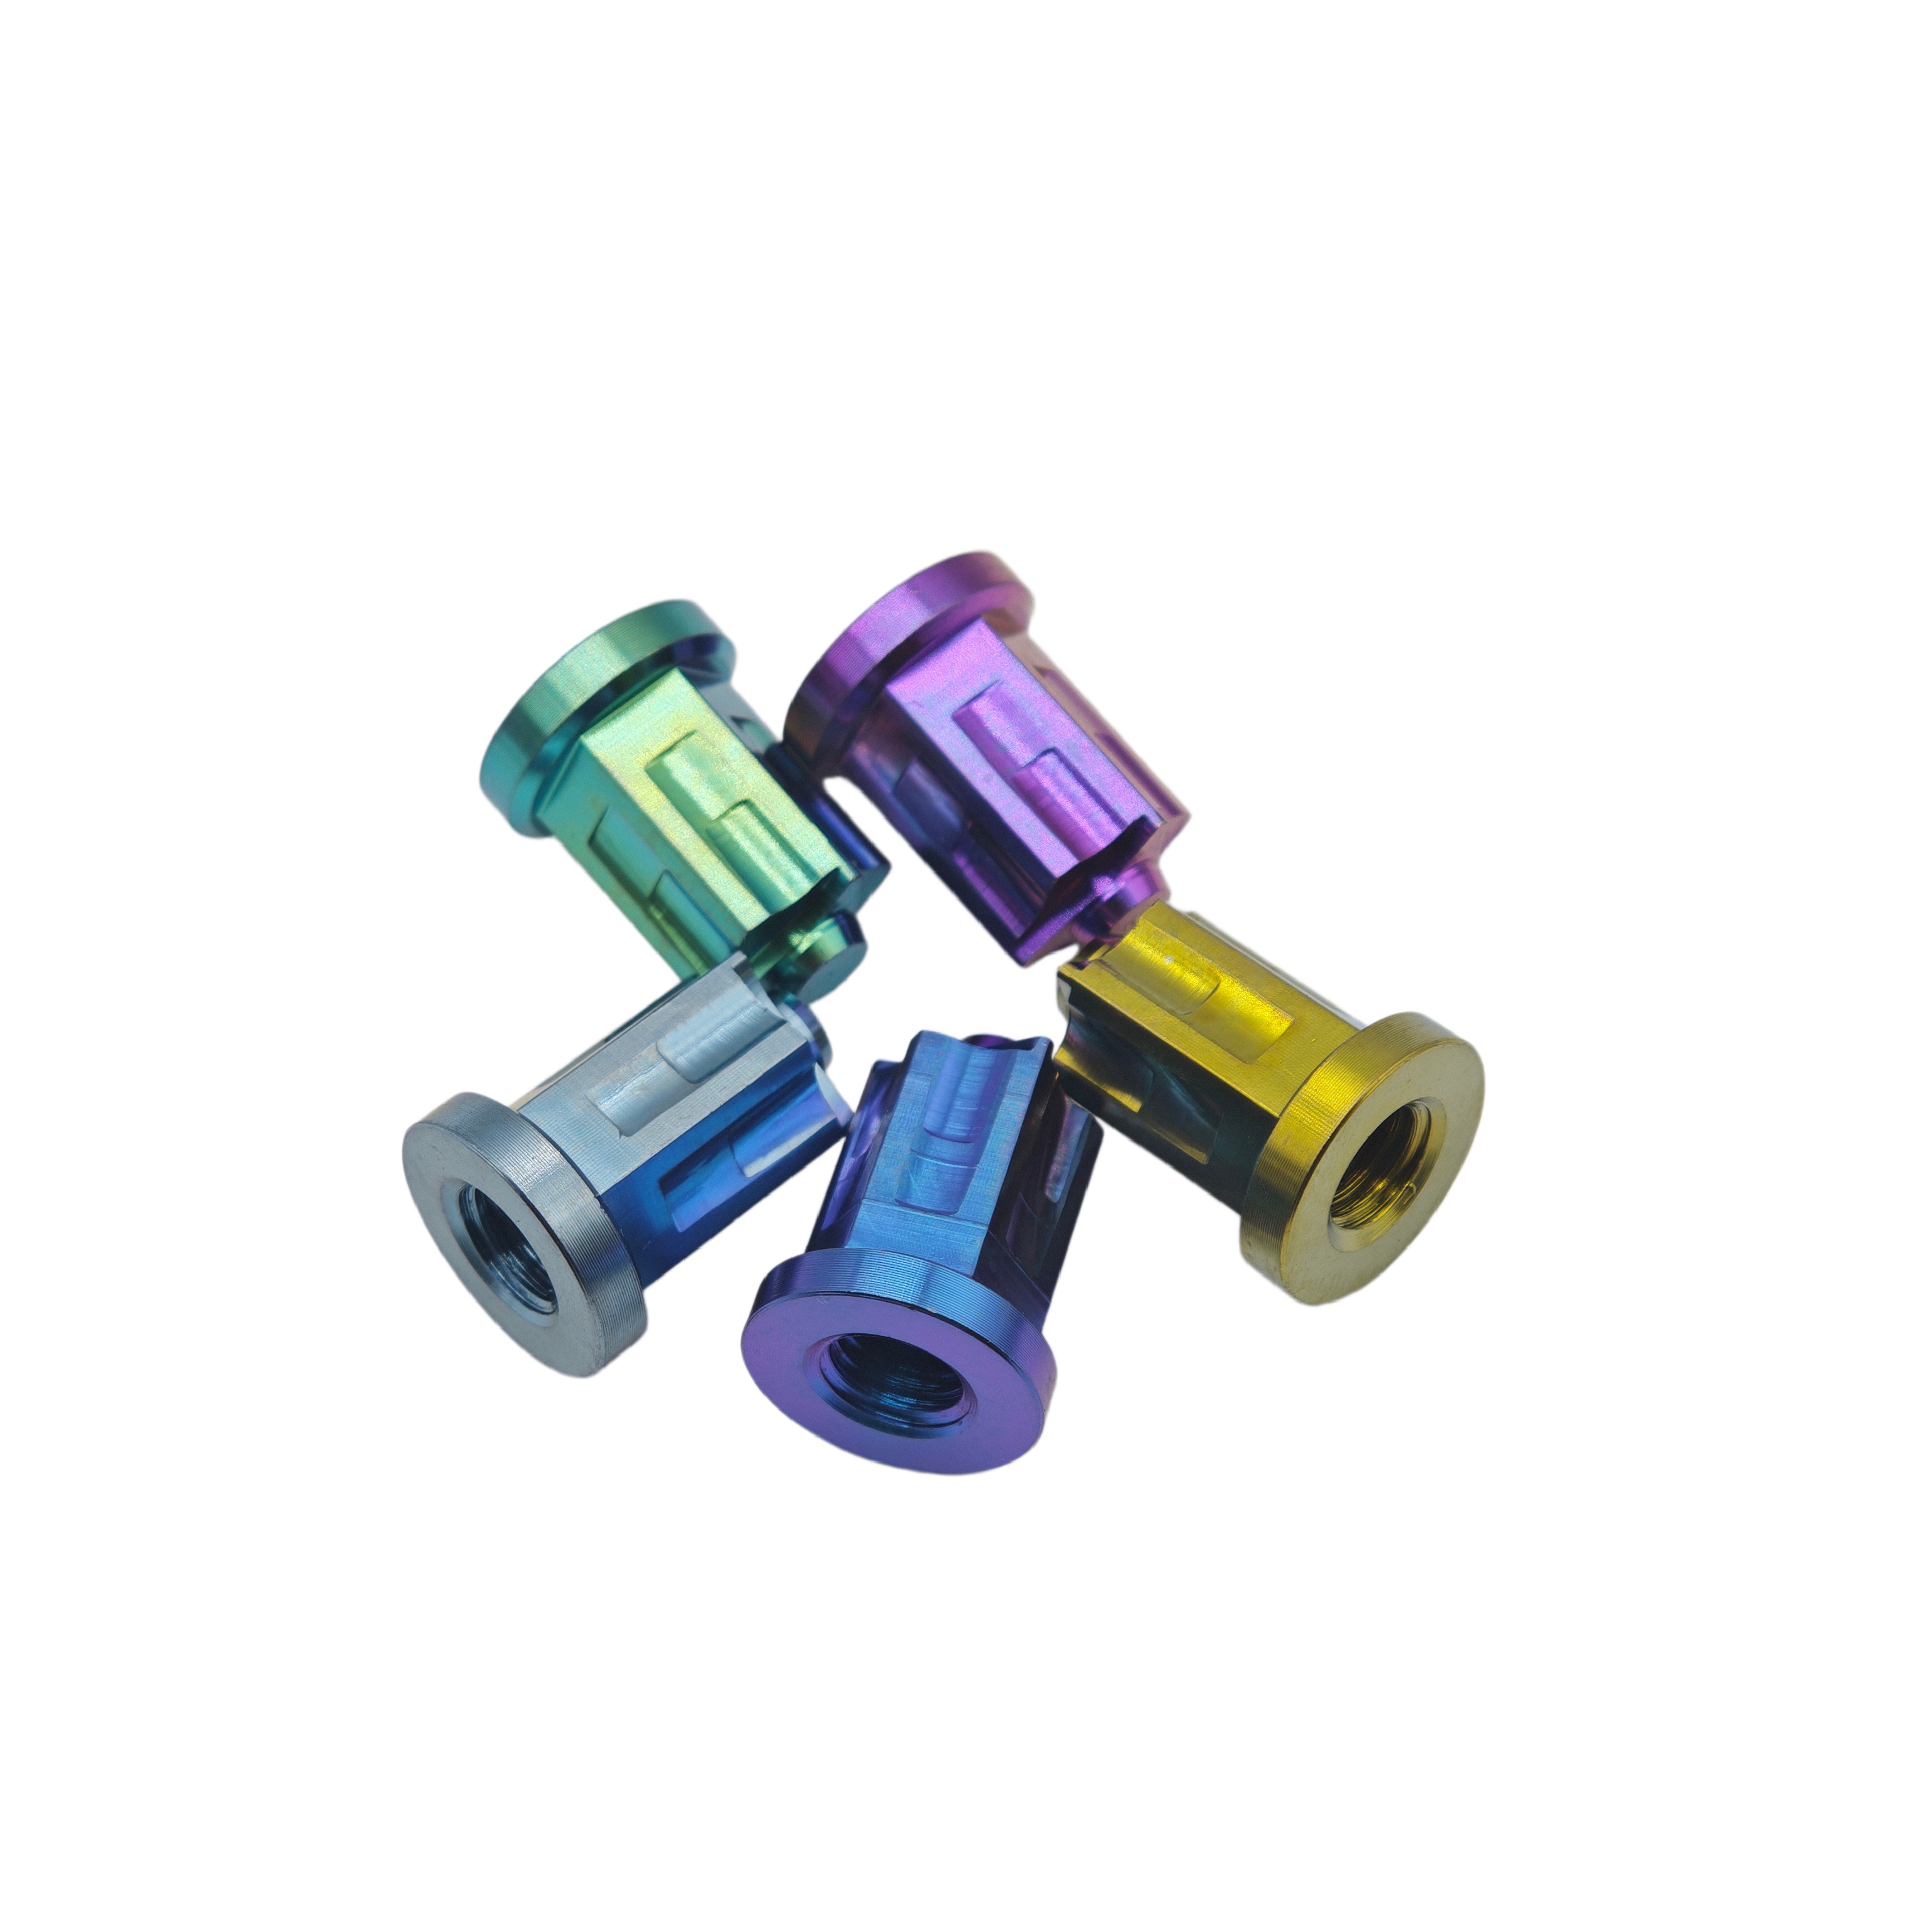
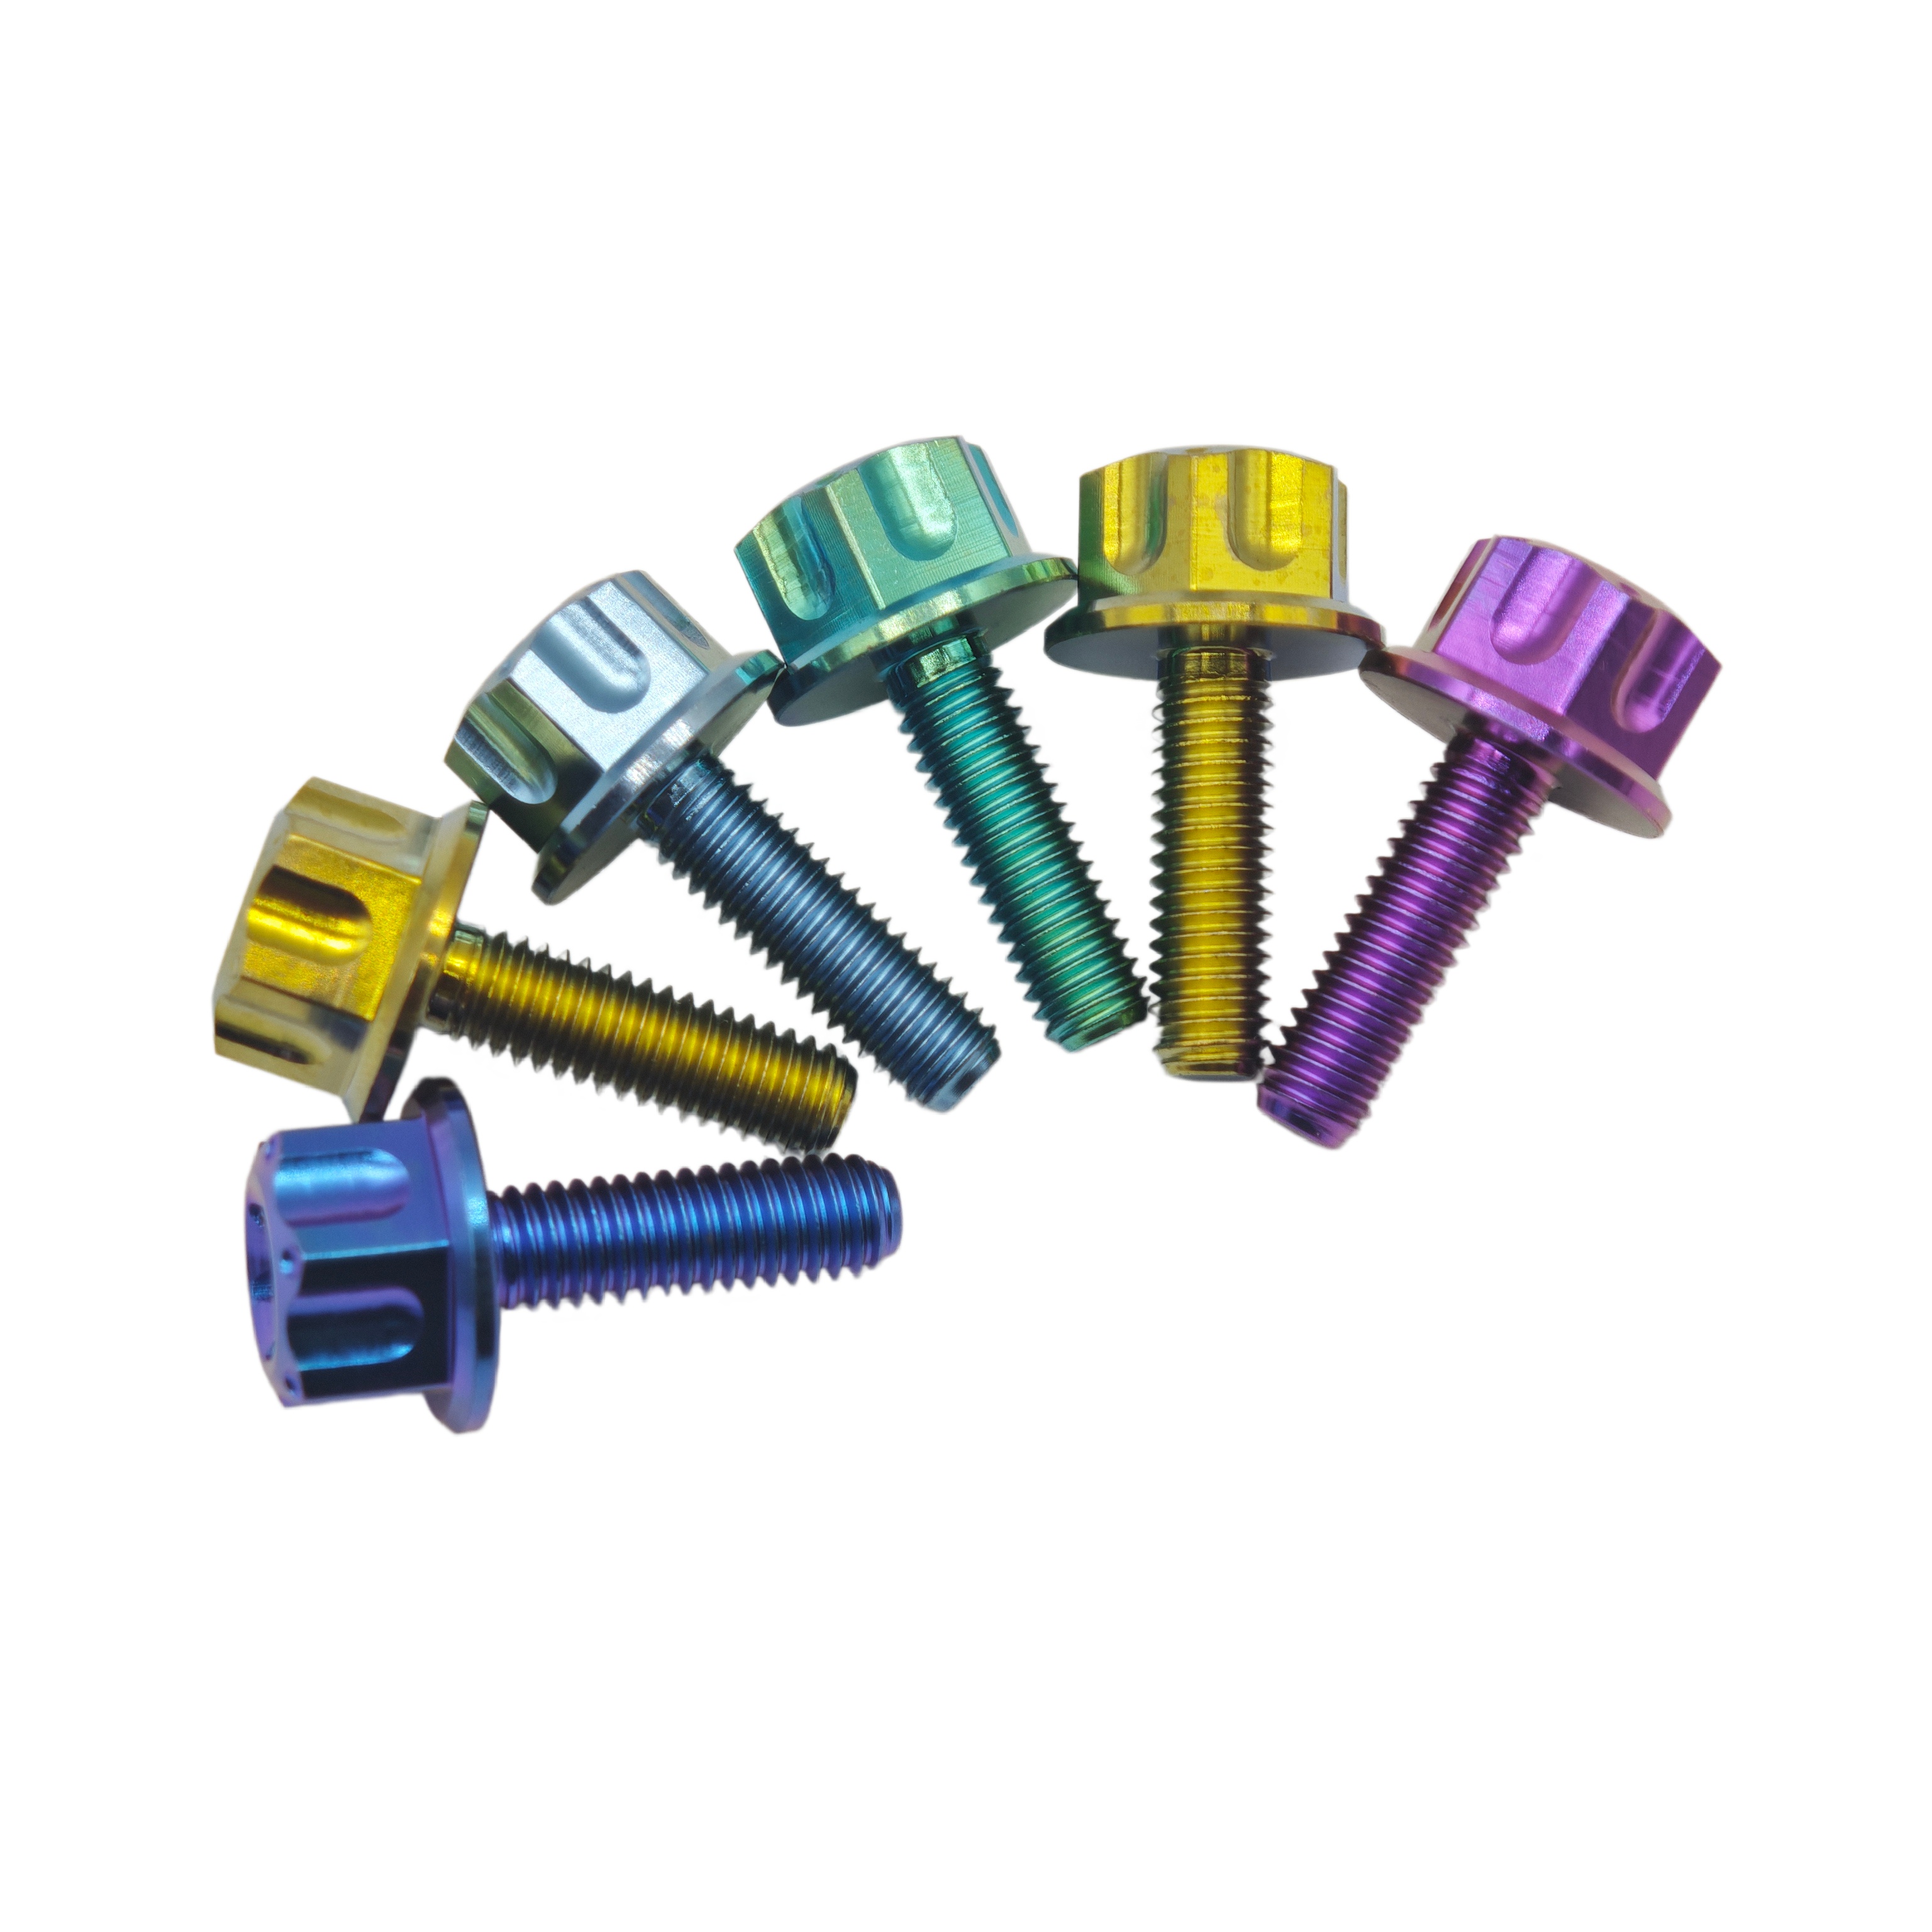
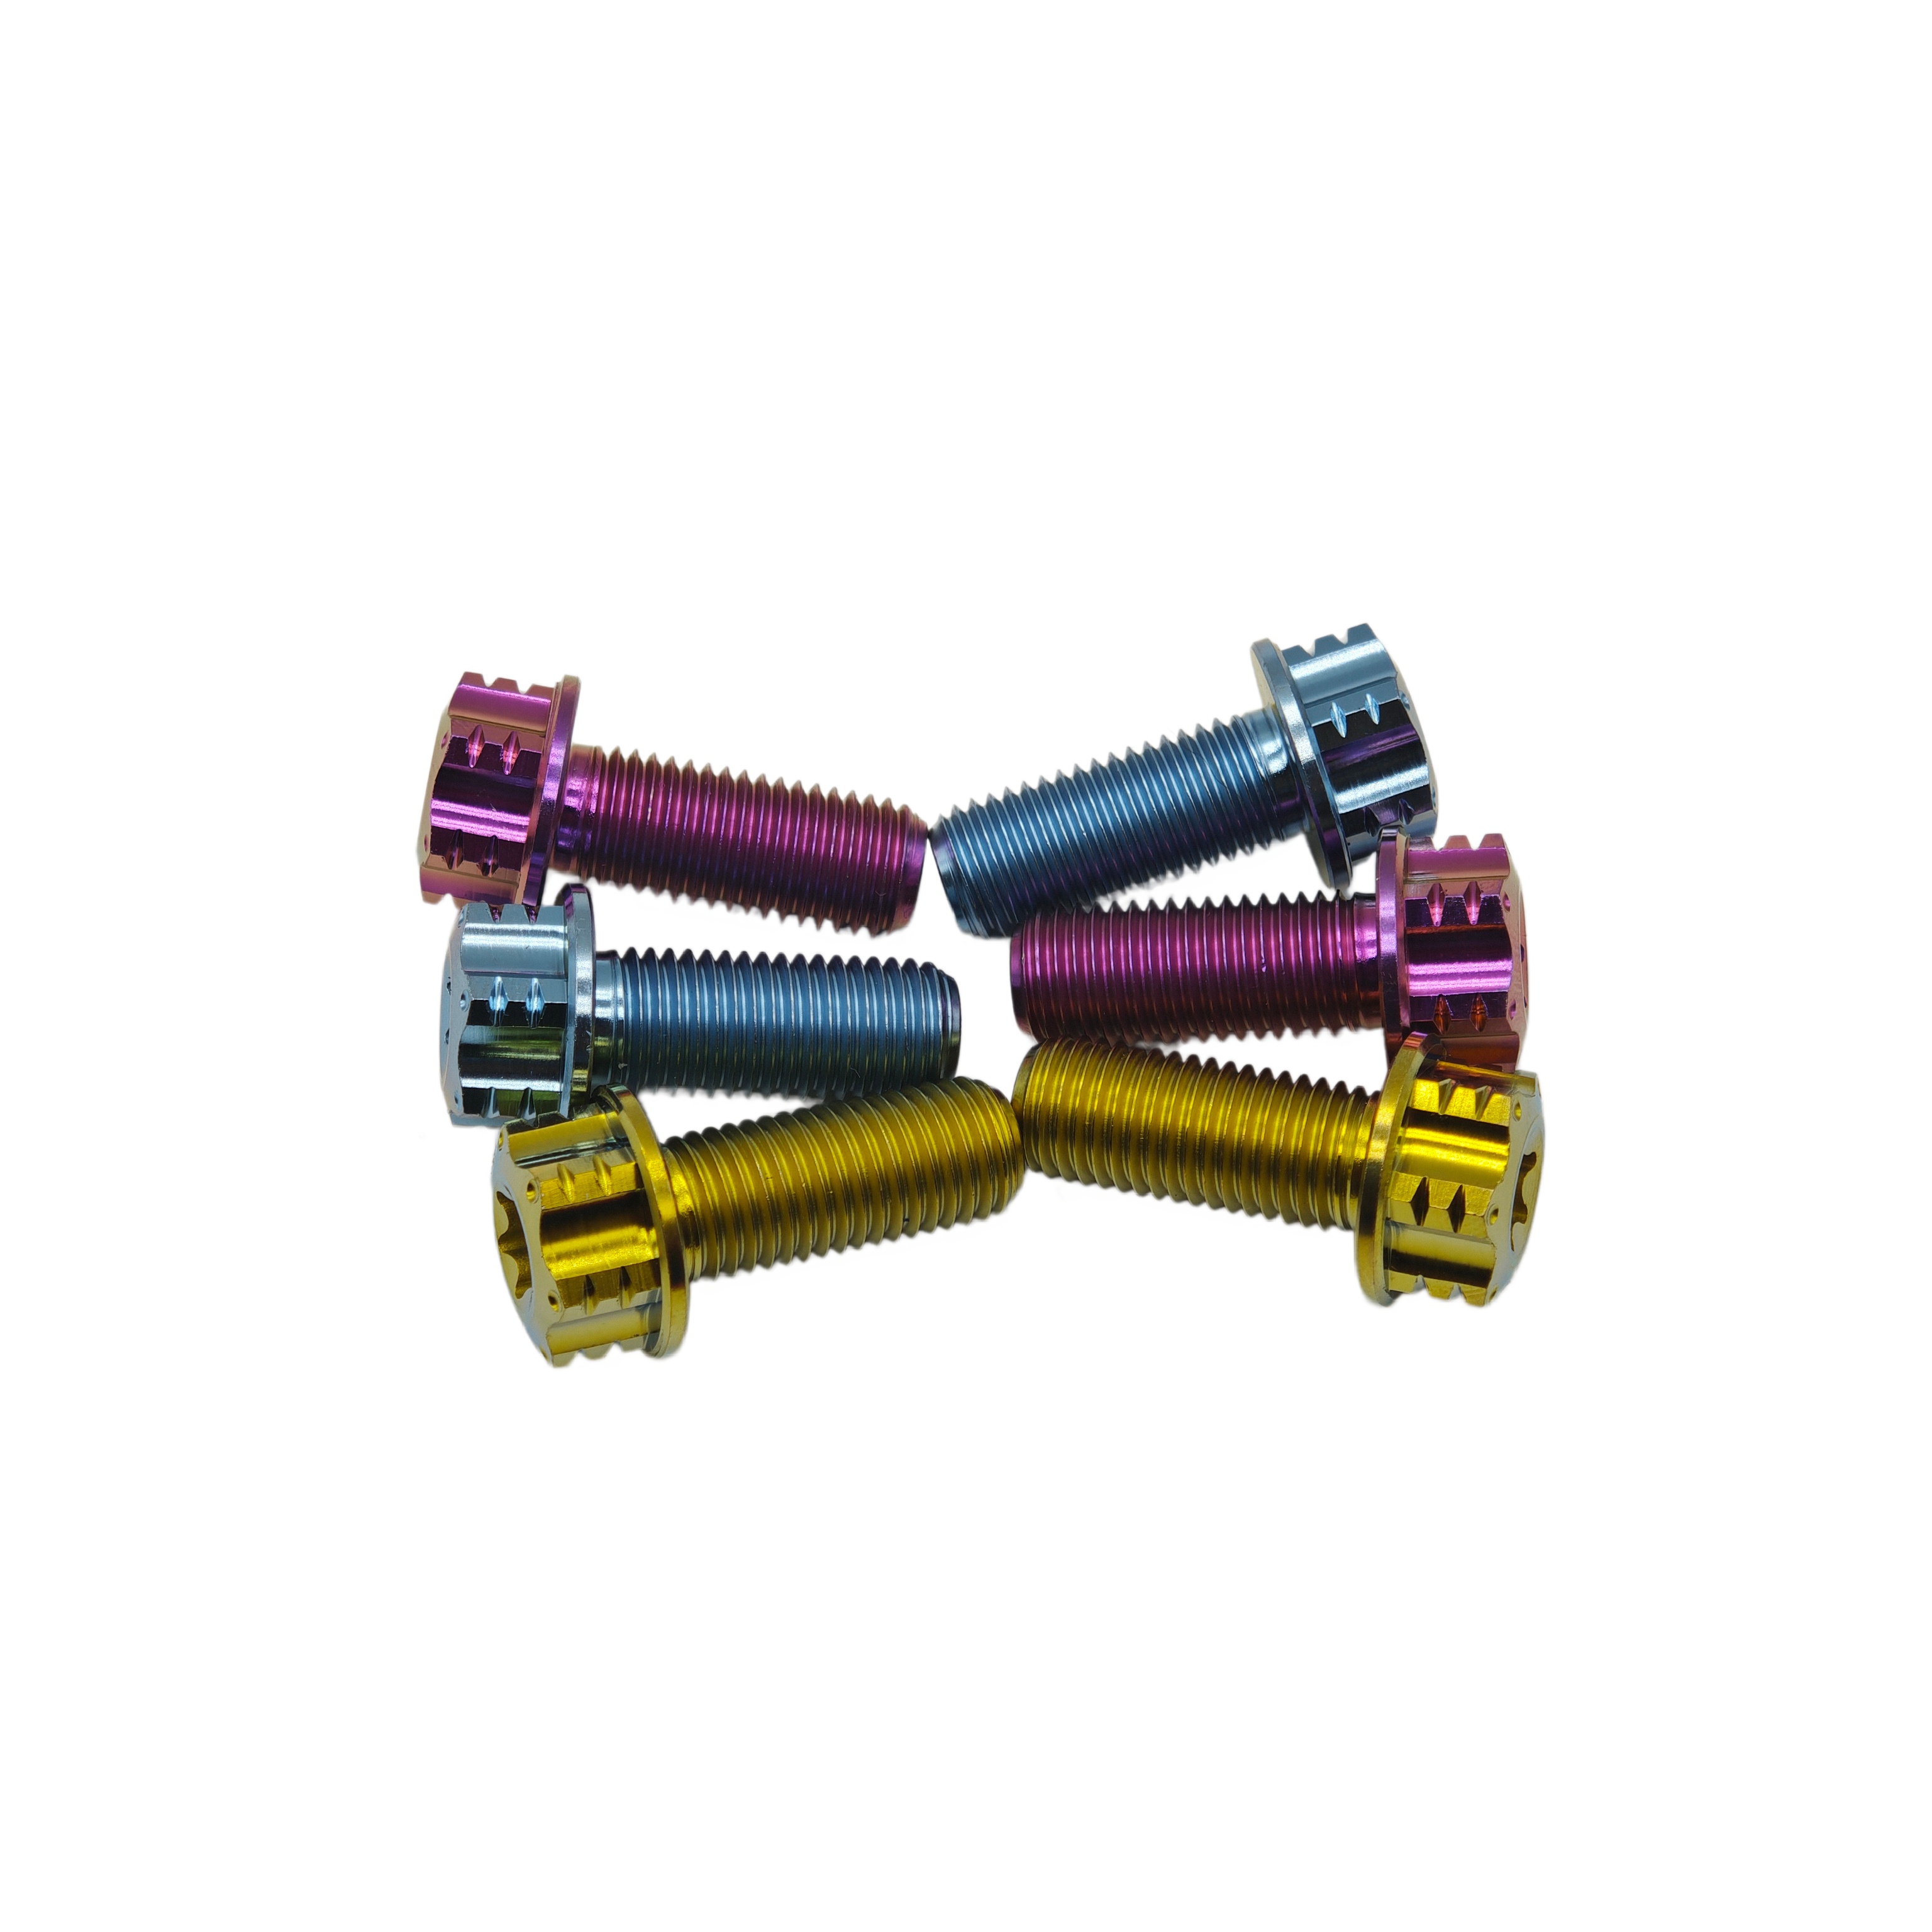
In high-vibration dynamic environments—such as automotive wheel hub spindles, motorcycle rear swingarms, aircraft flight control linkages, and marine propulsion shafts—fastener integrity is non-negotiable. Standard threaded fasteners subjected to transverse harmonic vibration undergo rotational self-loosening due to cyclic micro-slips between mating threads. Titanium Castle Nuts (Slotted Hex/Crown Nuts conforming to DIN 935, ISO 7035, or custom OEM drawings) mitigate catastrophic failure by pairing physical mechanical interlocks (cotter pins, safety wires, or roll pins) with the superior strength-to-weight metrics of Grade 5 Titanium alloy (Ti-6Al-4V).
A castle nut features radial slots (crenellations) machined into a cylindrical crown extending above its hexagonal body. When torqued onto a mating threaded shaft featuring a pre-drilled cross-hole, a stainless steel or titanium cotter pin is inserted through the slots and shaft bore, with its tines bent back. This converts a frictional thread friction lock into a positive displacement shear barrier. Even if pre-load tension drops to zero under extreme thermal cycling or impact loading, the nut cannot rotate beyond the radial clearance of the cotter pin slot ($< 15^\circ$ rotational boundary).
By replacing Grade 8.8 or Grade 10.9 steel spindle axle nuts with CNC-machined Grade 5 Titanium Castle Nuts, automotive and motorsport engineers lower rotational un-sprung mass by over 40%. This directly reduces rotational inertia, improving suspension response frequency, dampening chassis oscillation, and extending wheel bearing service life under high lateral G-force cornering.
To assist procurement directors and structural engineers in material selection, the matrix below highlights the mechanical parameters of Zunvo Titanium's OEM Grade 5 Titanium Castle Nuts against conventional automotive and industrial fasteners:
| Mechanical / Physical Property | Ti-6Al-4V Grade 5 Titanium | Class 10.9 Carbon Steel | A2-70 Stainless Steel | 7075-T6 Aluminum |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 (Super Light) | 7.85 | 7.93 | 2.81 |
| Ultimate Tensile Strength (MPa) | 895 – 1050 | 1040 | 700 | 570 |
| Yield Strength 0.2% (MPa) | 828 – 920 | 940 | 450 | 505 |
| Strength-to-Weight Ratio ($kN\cdot m/kg$) | 202 (Industry Highest) | 132 | 88 | 202 |
| Corrosion Resistance (ISO 9227 Salt Spray) | > 3,000 Hours (Immune to Salt/Acid) | < 96 Hours (Uncoated) | ~ 500 Hours | Pitting Risk in Saline |
| Thermal Expansion Coeff. ($10^{-6}/K$) | 8.6 (Matches Carbon Composites) | 11.7 | 16.0 | 23.4 |
How global OEMs are reshaping their fastener supply chains to meet lightweighting targets, sustainability criteria, and digital quality traceability.
As Electric Vehicle (EV) platforms strive to extend range per kilowatt-hour, reducing chassis and axle mass has become paramount. Titanium castle nuts offer immediate drop-in weight savings on drive axles, steering knuckles, and suspension arms without redesigning casting geometries.
While anodic color oxidation delivers vibrant cosmetic hues, high-load OEM buyers are migrating to Physical Vapor Deposition (PVD) finishes such as Titanium Nitride (TiN), Titanium Aluminum Nitride (TiAlN), and Diamond-Like Carbon (DLC). These coatings double surface micro-hardness (> 2500 HV) and lower galling tendencies during high-torque power tool assembly.
Global quality compliance (ISO 9001 / AS9100) requires full raw material origin verification. Tier-1 buyers now mandate mill test reports (EN 10204 3.1 certification) linking every lot of castle nuts directly to raw titanium ingot smelting chemistry and ultrasonic flaw detection test logs.
From raw titanium bar stock to optical-gauge inspected, custom-packaged safety hardware.
100% vacuum-melted Ti-6Al-4V Grade 5 titanium rod stock sourcing with chemical composition analysis and ultrasonic flaw detection.
Precision multi-axis CNC Swiss lathe turning to shape the hex body, crown flange, and precise slot width tolerances within ±0.005 mm.
Cold thread rolling rather than cut threading preserves grain flow continuity, boosting fatigue endurance limits by up to 300% under cyclic shear loads.
Application of micro-thin ceramic PVD, anodic color oxidation, or dry-film MoS2 lubricant to eliminate galling during high-speed pneumatic installation.
Automated optical sorting system verifies 6g/6H thread pitch consistency, slot alignment symmetry, and crack-free surface morphology.
Situated in Baoji, Shaanxi (China's Titanium Valley), Zunvo Titanium Products Co., Ltd. integrates raw titanium smelting resources with high-precision CNC manufacturing.
Direct proximity to titanium sponge smelters and certified rolling mills guarantees immediate raw material availability, low material overheads, and quick heat batch traceability.
Engineers review custom CAD/3D drawings within 24 hours and deliver CNC-turned functional samples in as few as 3 business days for rapid fit checks.
With a 66% buyer reorder rate, 4.9/5 verified rating, and average response times under 7 hours, Zunvo exports across North America, Europe, Southeast Asia, and the Middle East.
Technical, commercial, and quality assurance answers for fastener engineers and purchasing agents.
Send us your technical drawings, thread specifications, or sample parts. Our engineering team responds within 7 hours with a comprehensive DFM review, price quote, and sample schedule.
