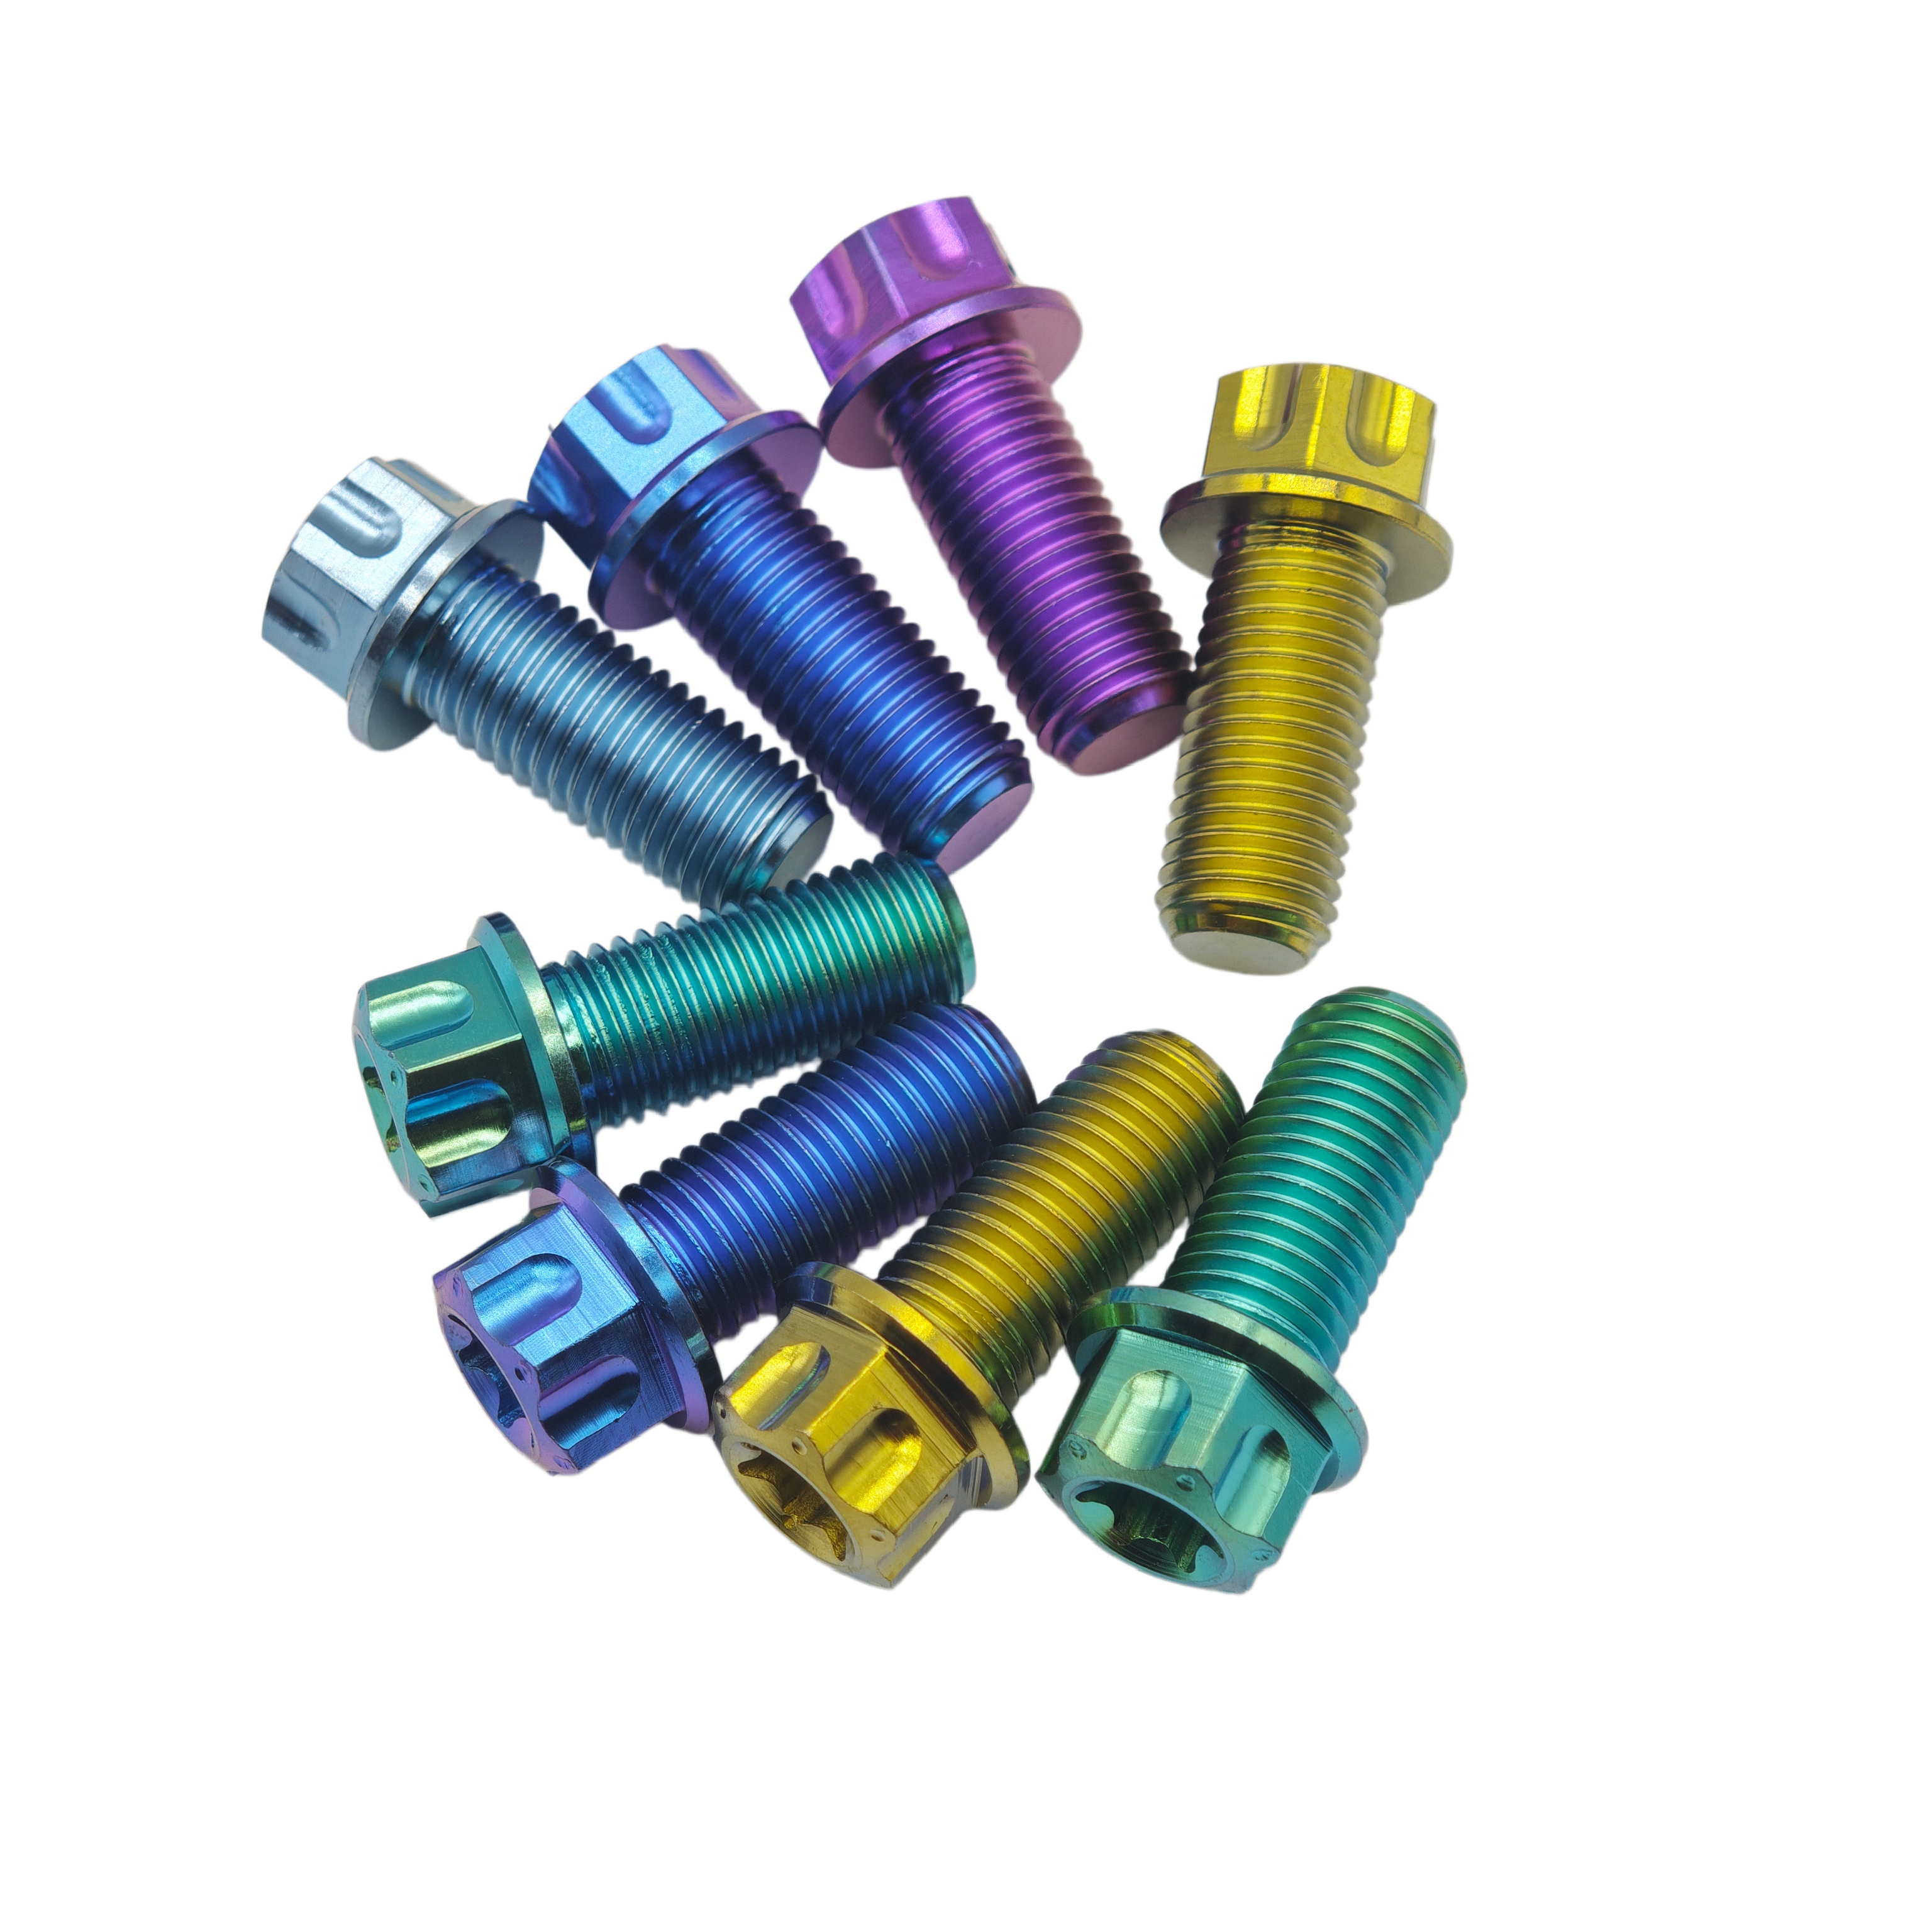
Technical Benchmark: Engineering Gr5 Anodized Fastening Solutions
Precision fastening architecture for cleanrooms, high-vibration mobility, and lightweight advanced robotics.
High Strength-to-Weight Ratio
Ti-6Al-4V (Grade 5) delivers a tensile strength exceeding ≥ 895 MPa while retaining a low density of 4.43 g/cm³. This reduces rotational mass and dynamic inertia by approximately 44% compared to standard Class 8.8 and 10.9 structural steels.
Controlled Oxide Layering
Our micro-arc and electrolytic color anodizing forms an inert TiO&sub2; dielectric barrier. The passive oxide creates structural refraction without introducing heavy pigment coatings, preventing cross-contamination inside ultra-clean high-vacuum assemblies.
Rolled Threads & Micro-Tolerances
Rather than cut threading, cold-rolled external threading guarantees uninterrupted grain flow, increasing high-cycle fatigue resistance. Precision CNC turning maintains critical dimensional tolerances down to ±0.005 mm (6g / 6H thread fit standards).
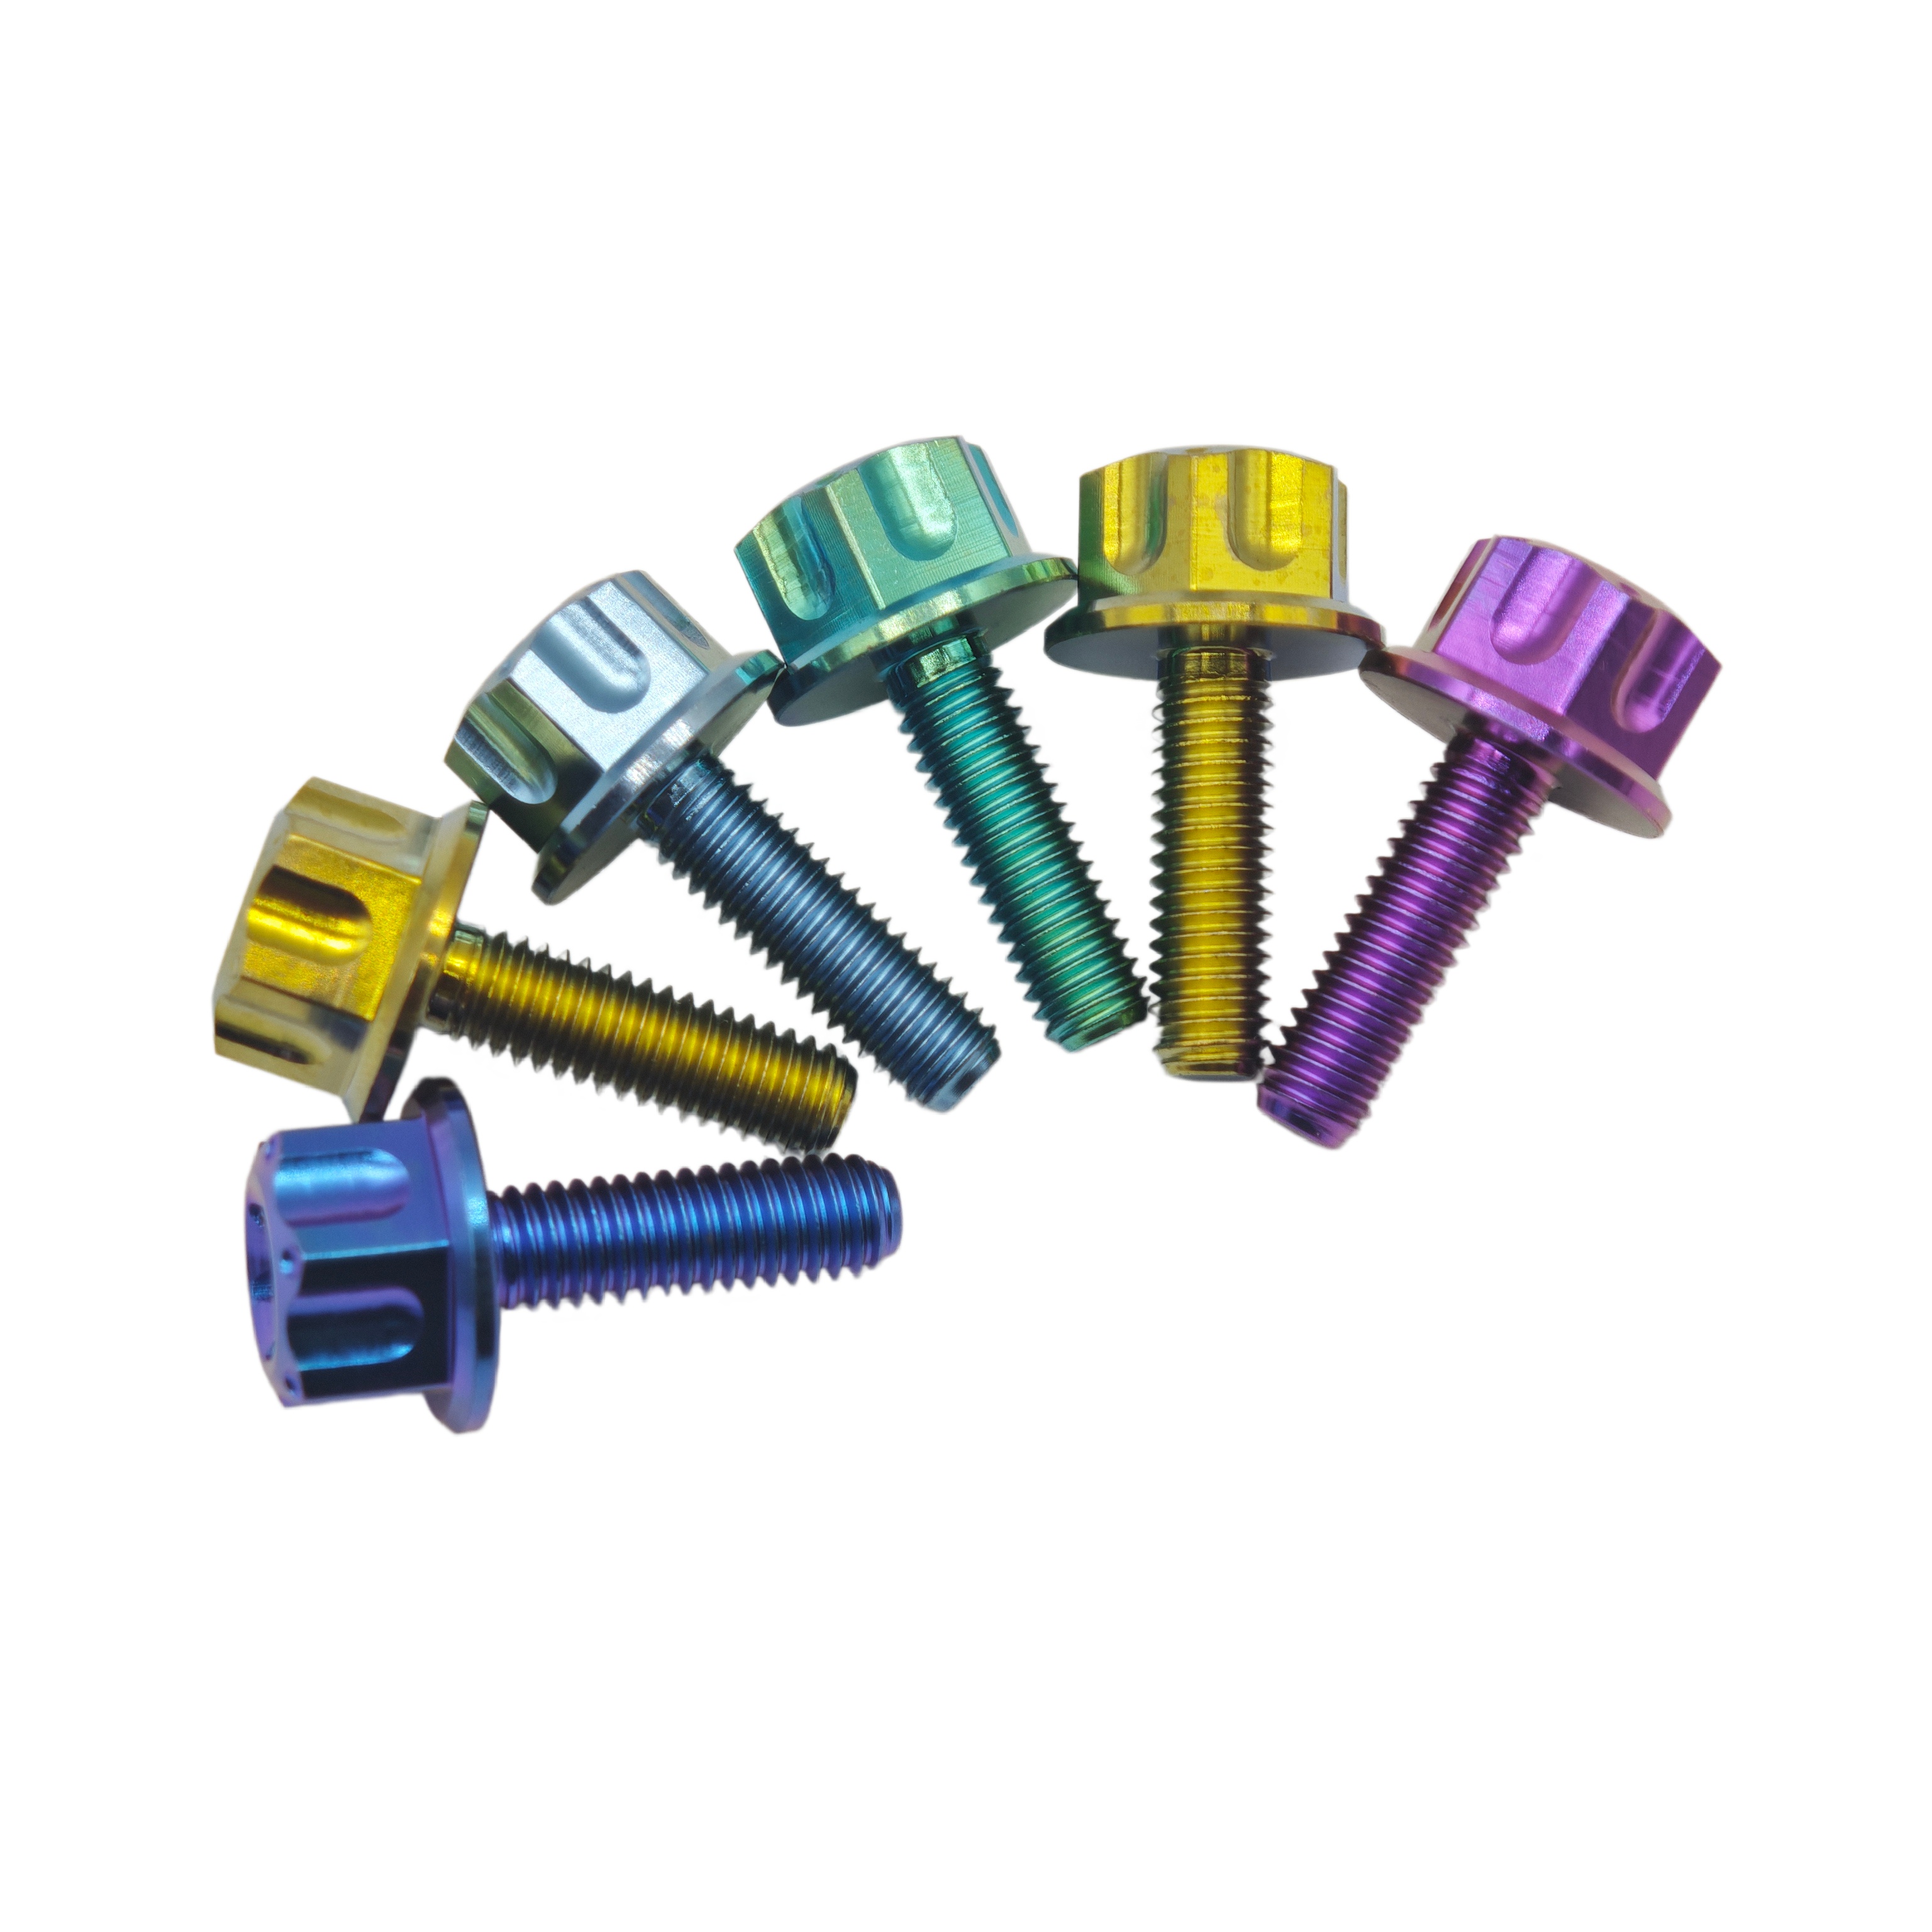
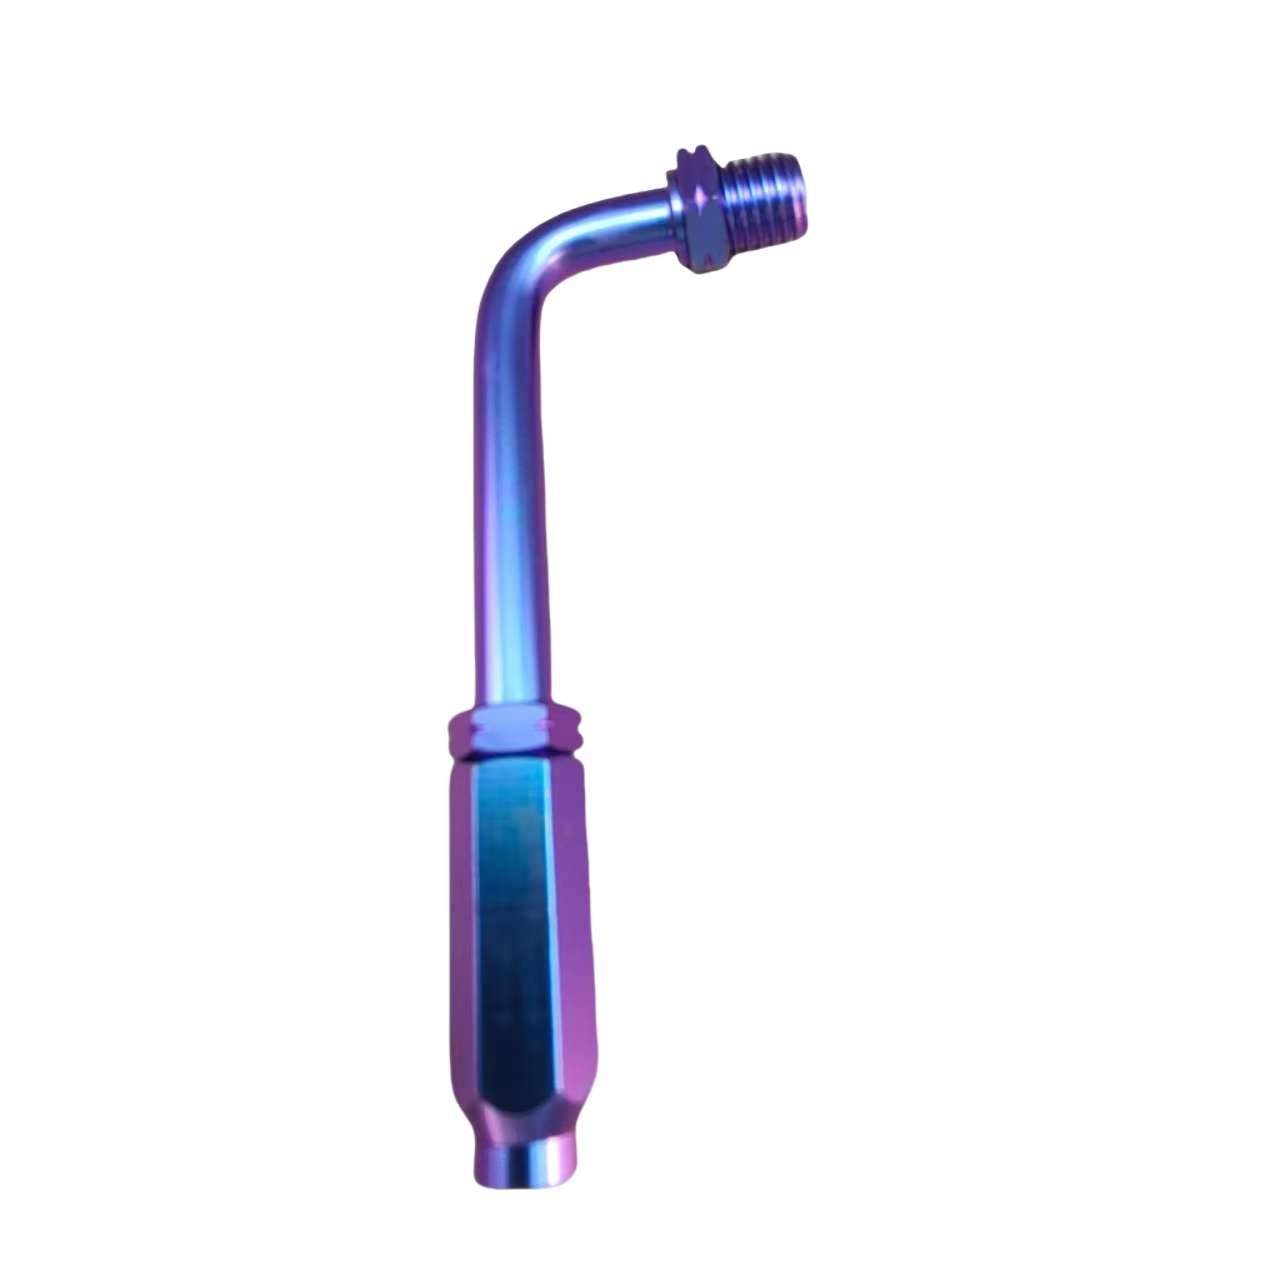
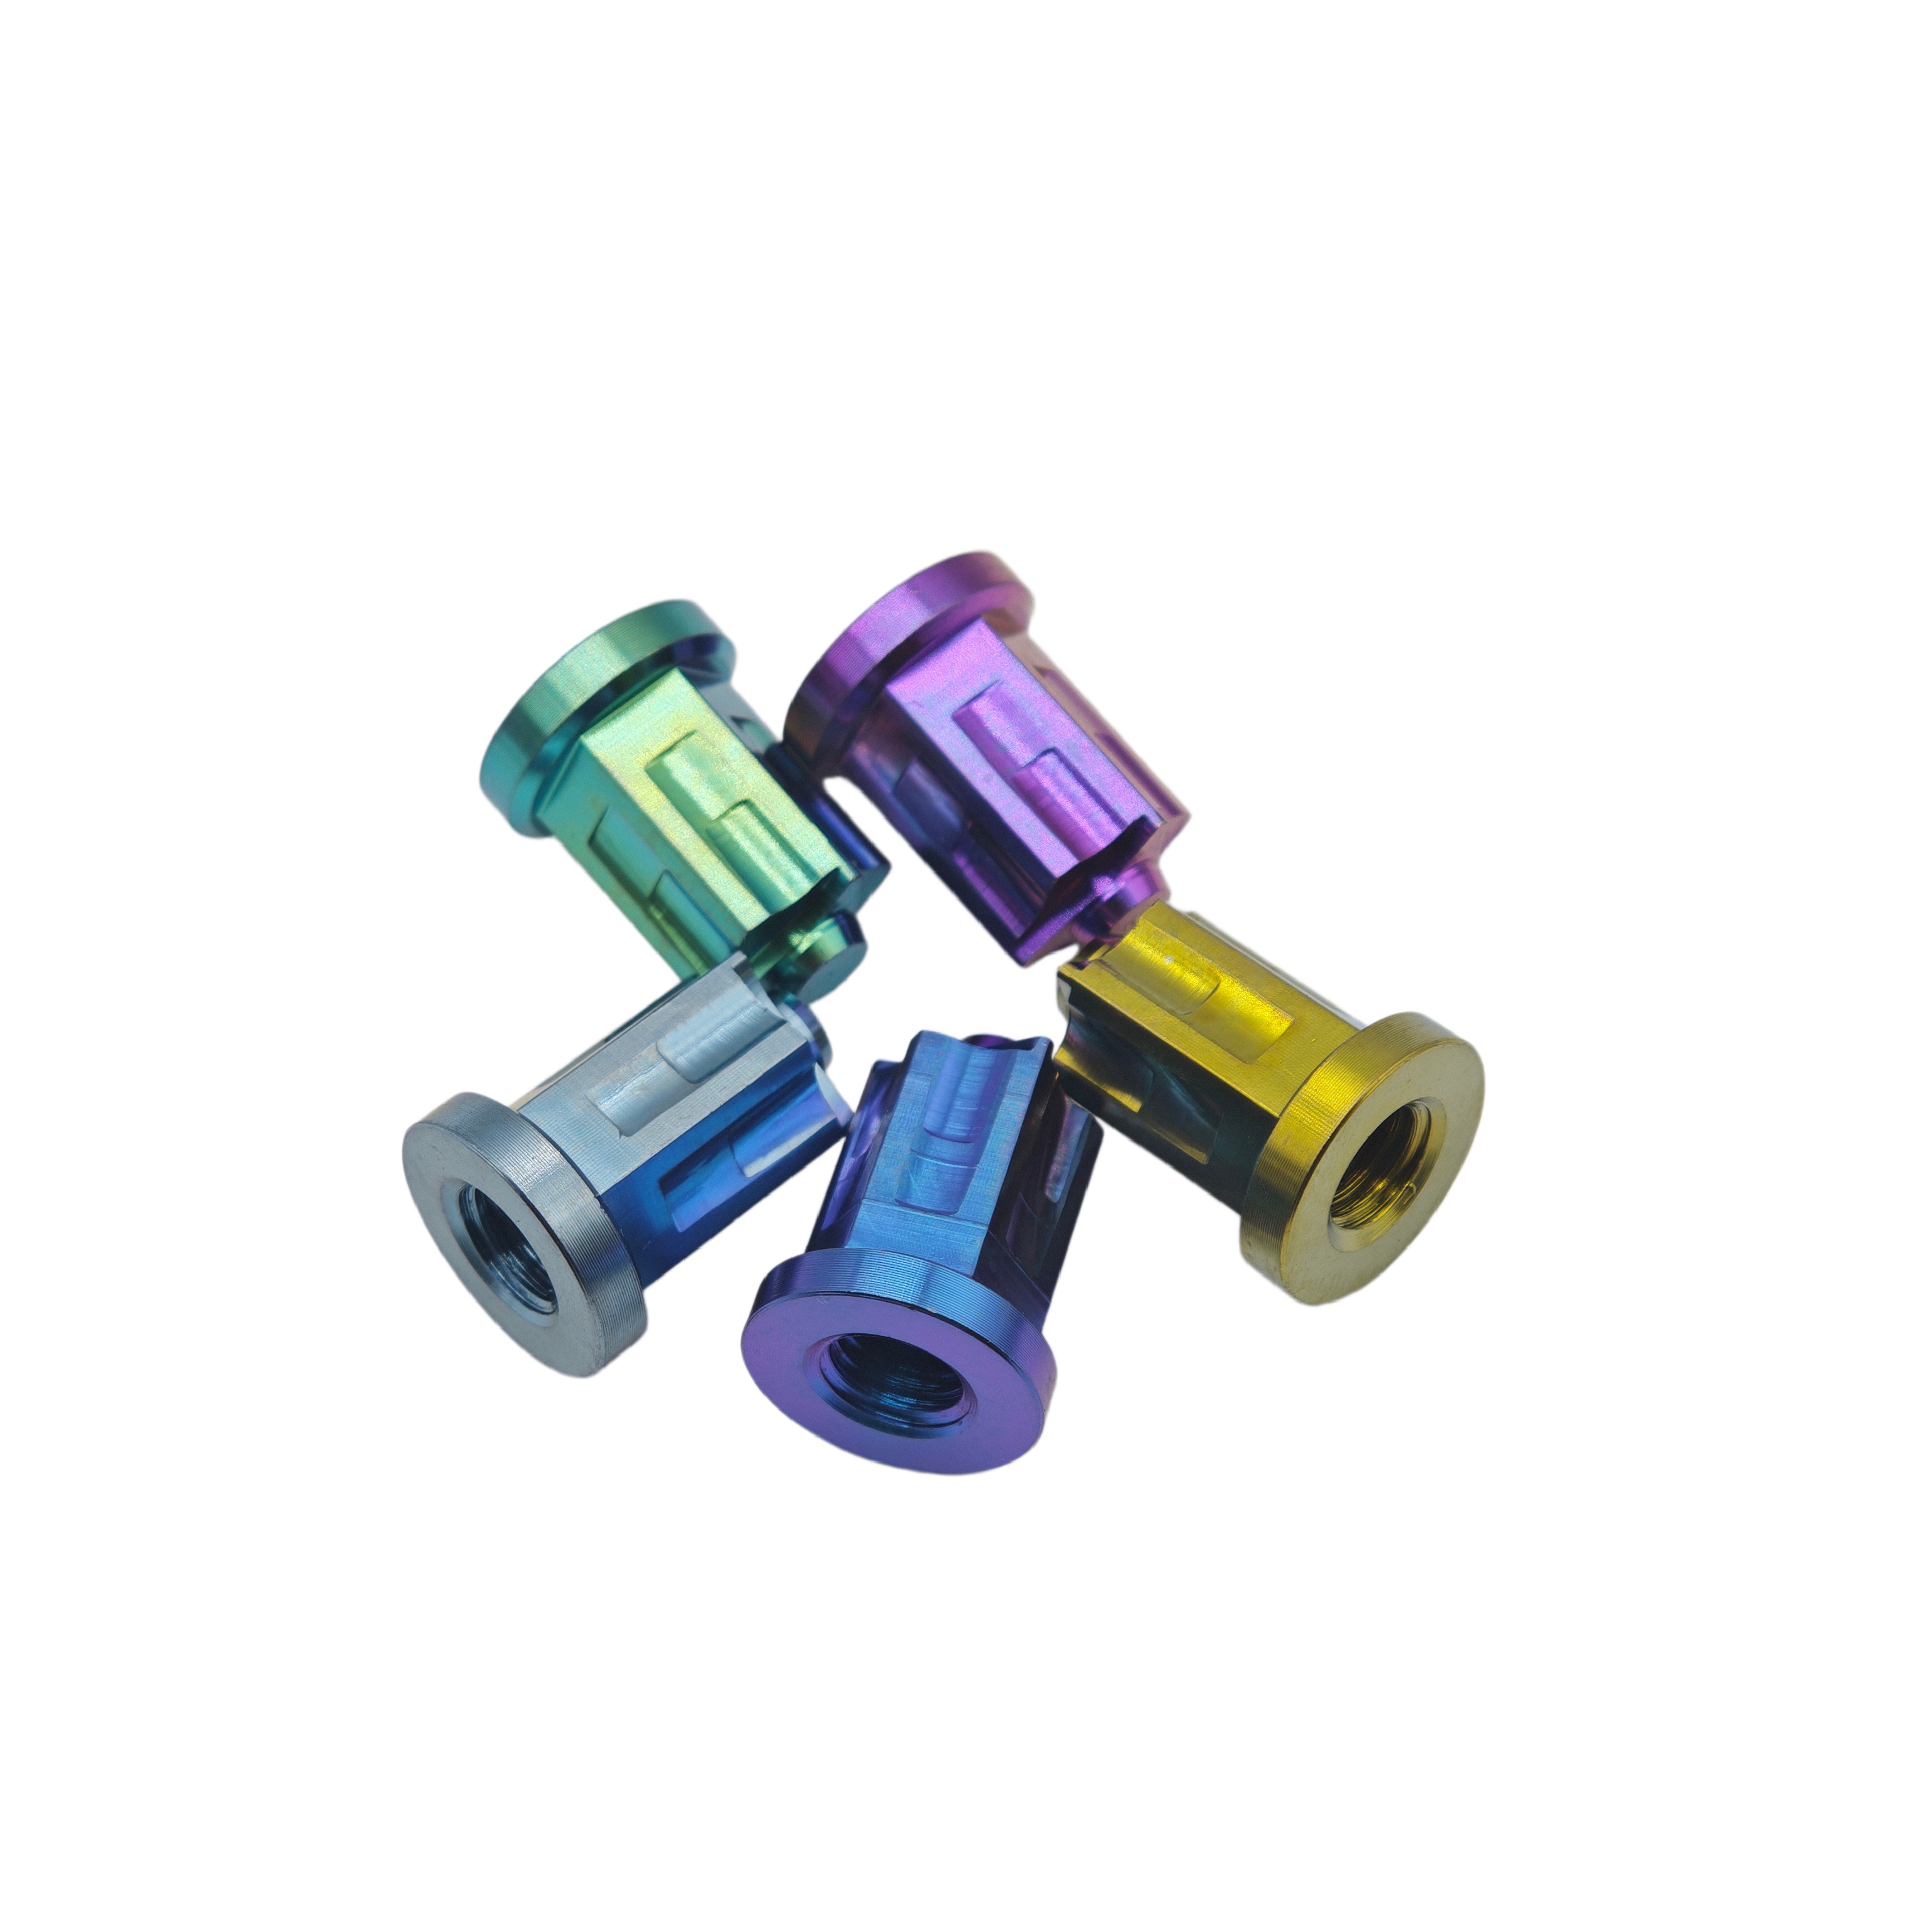
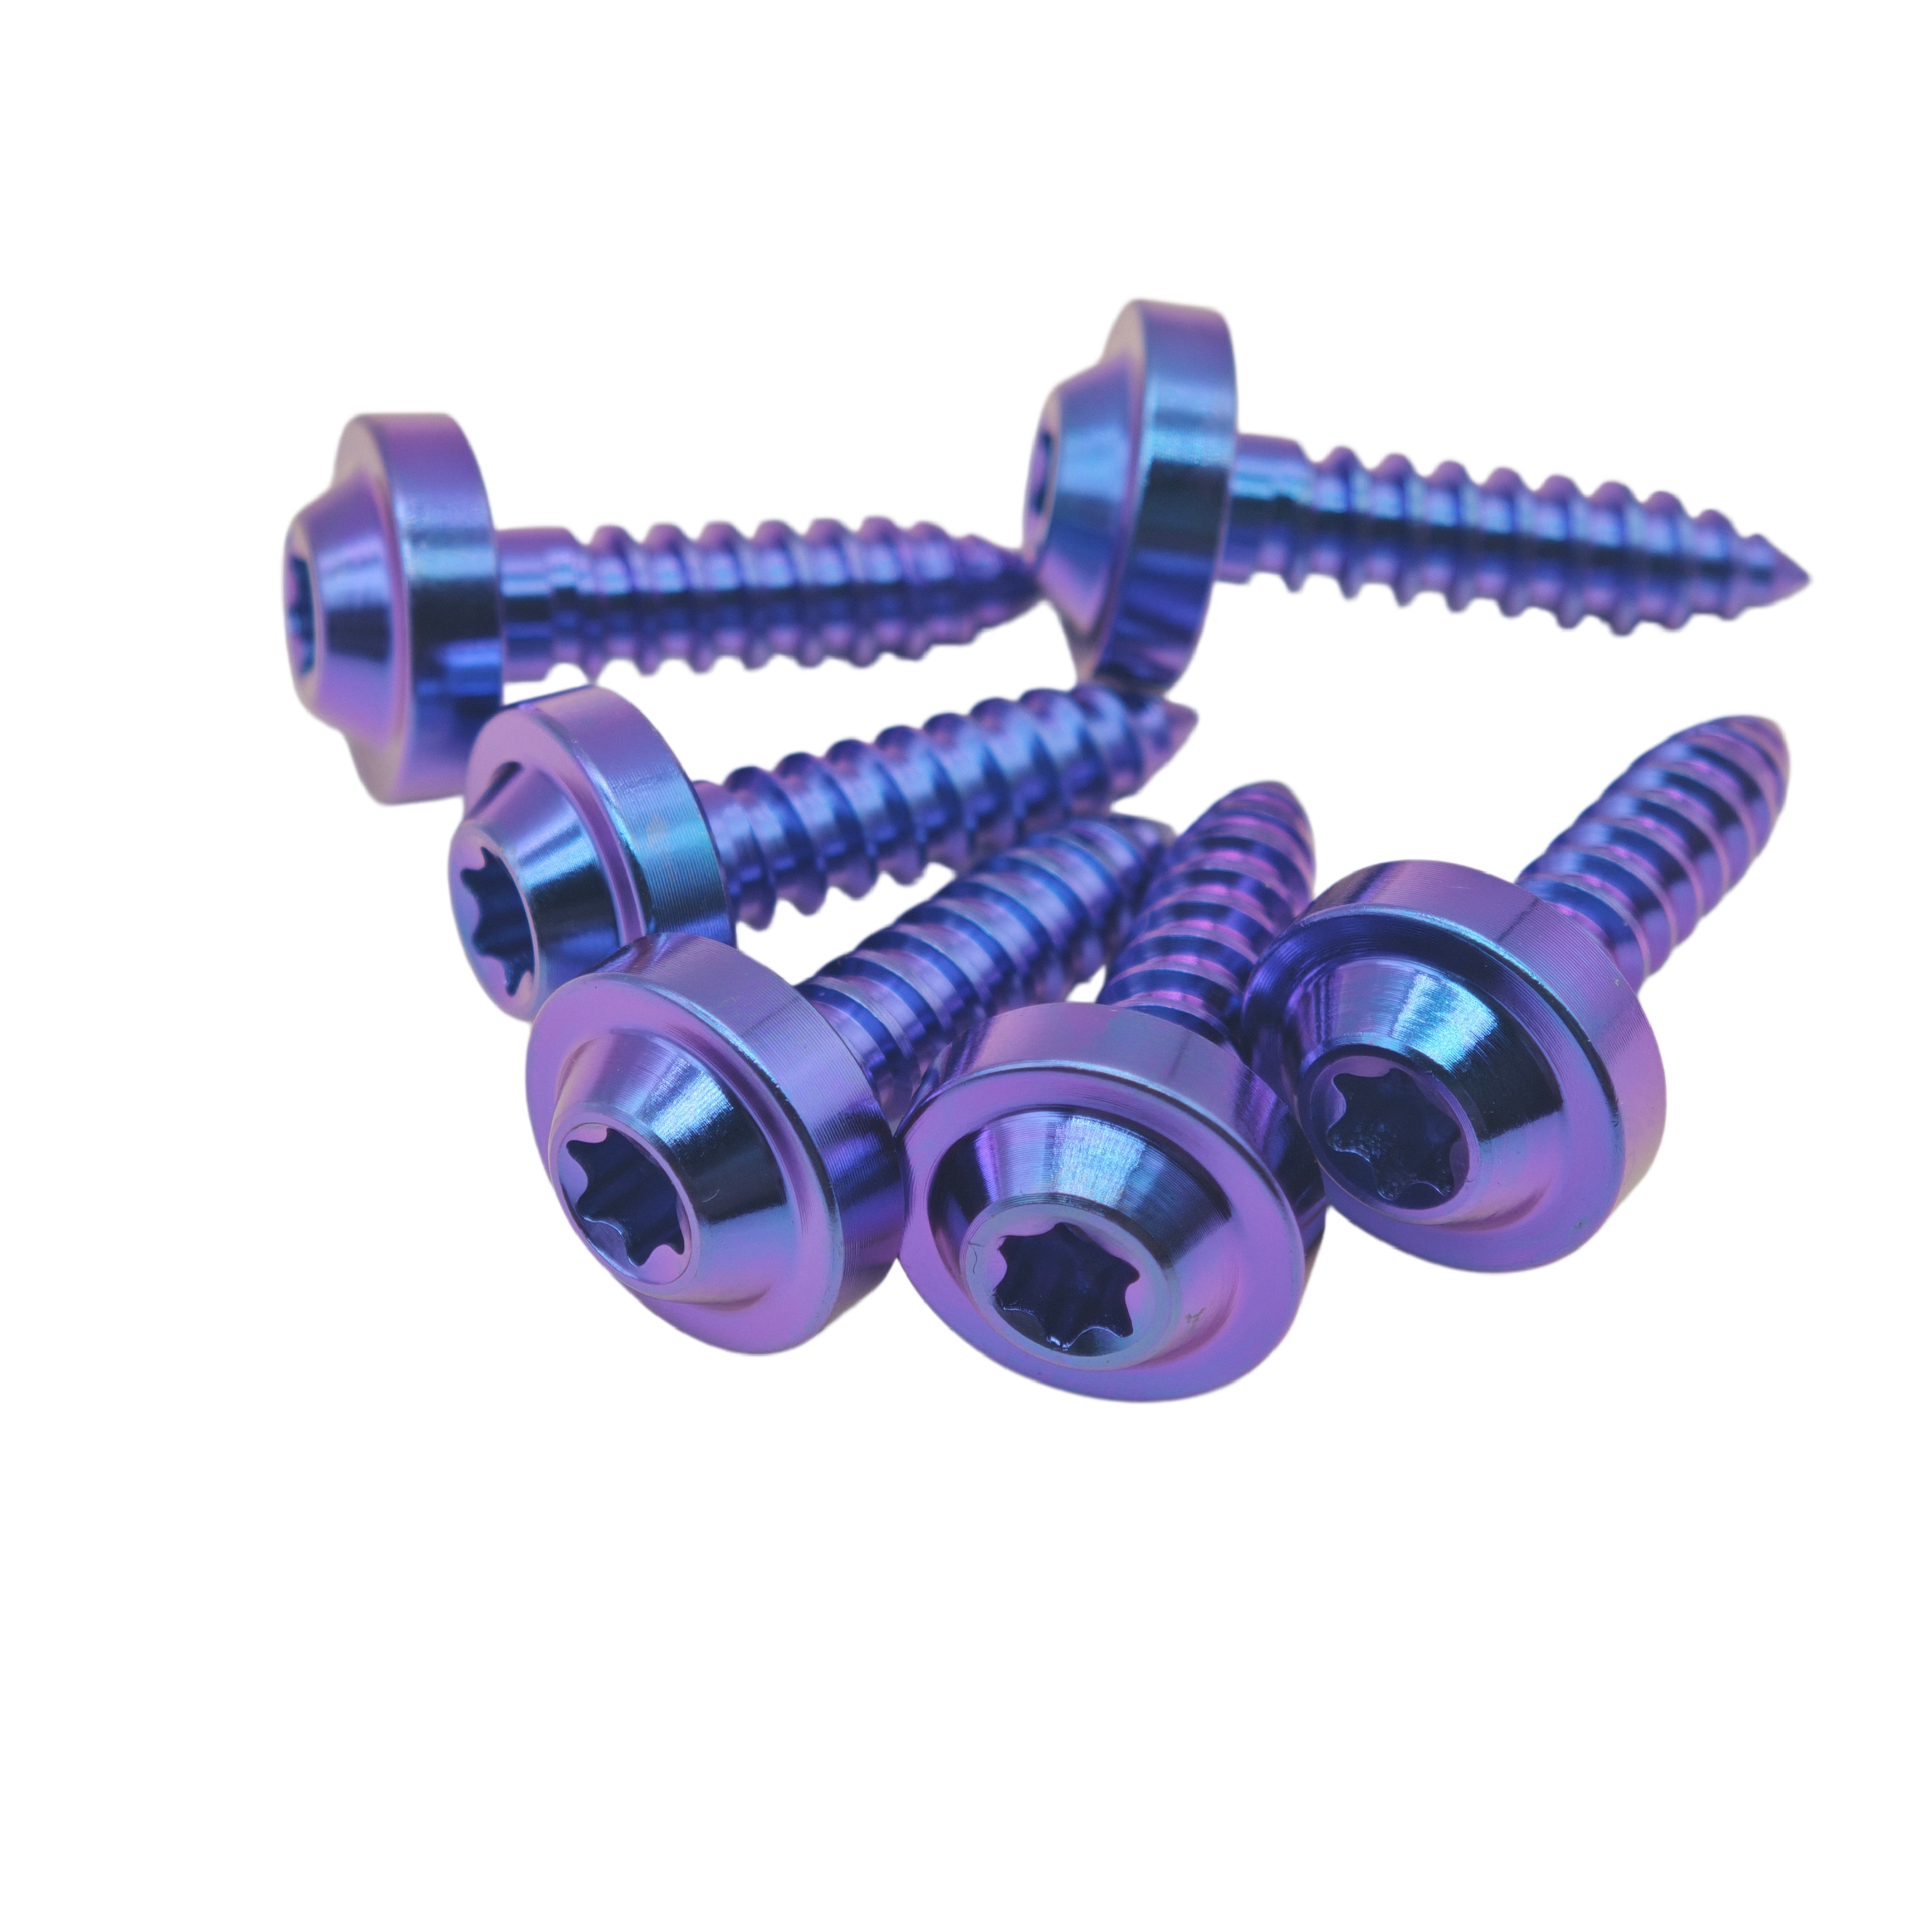
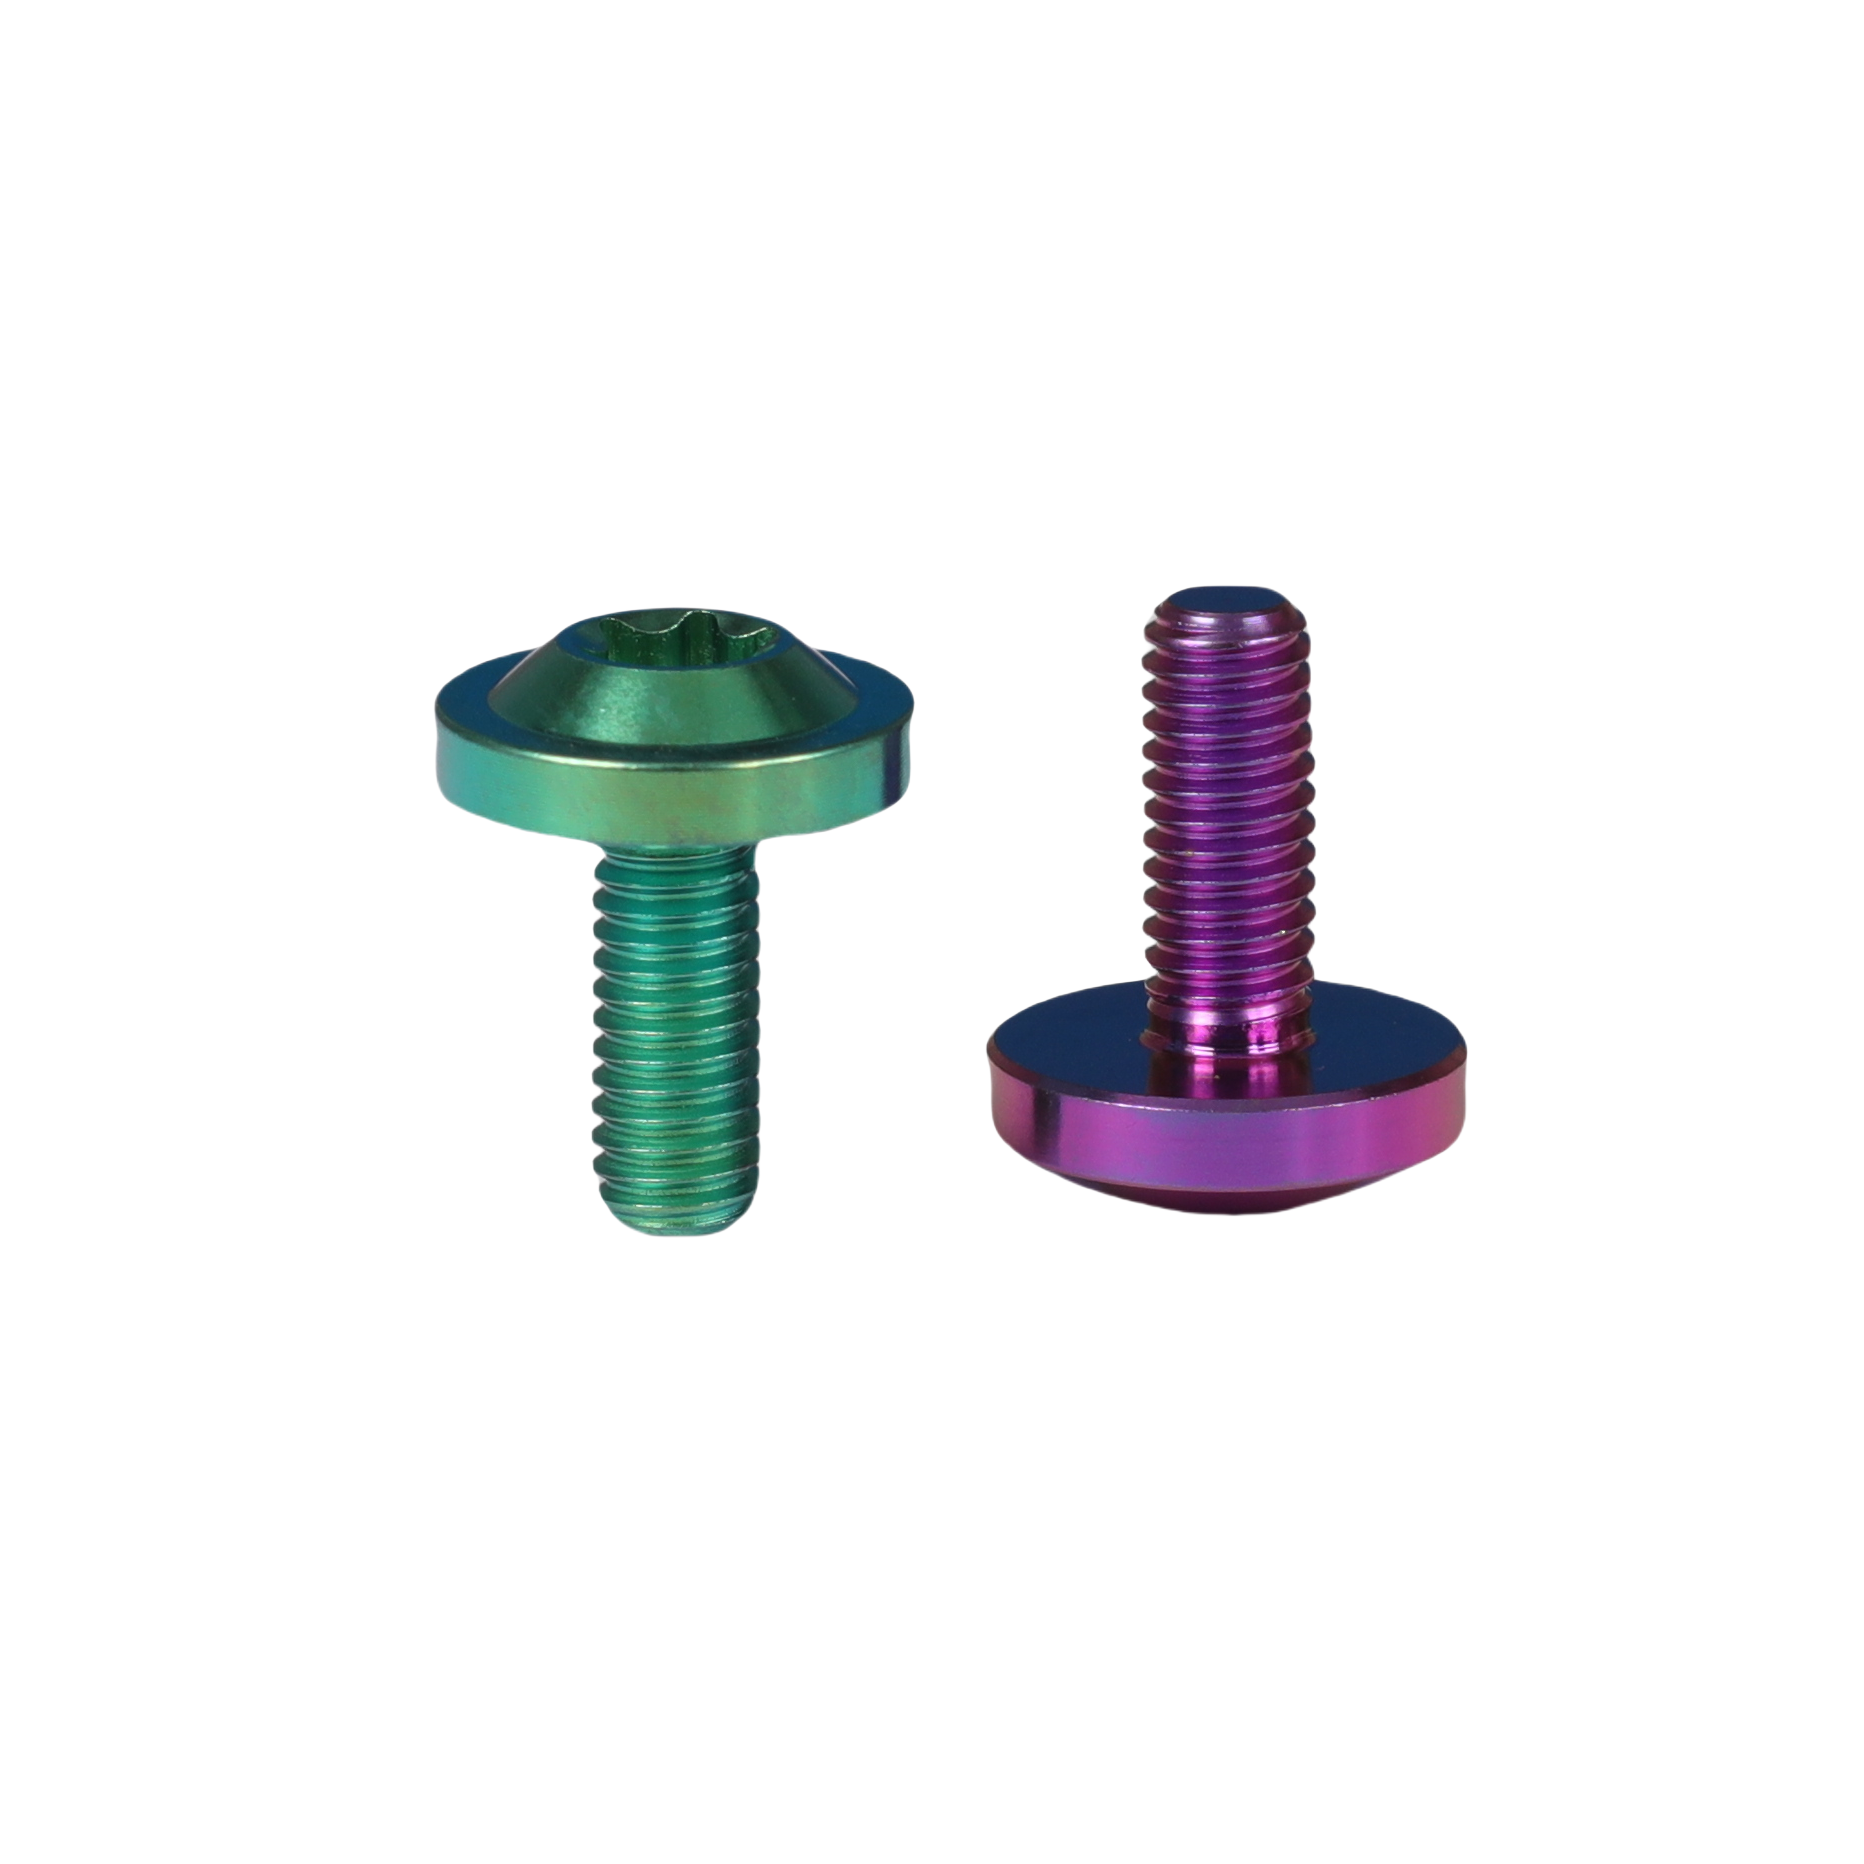
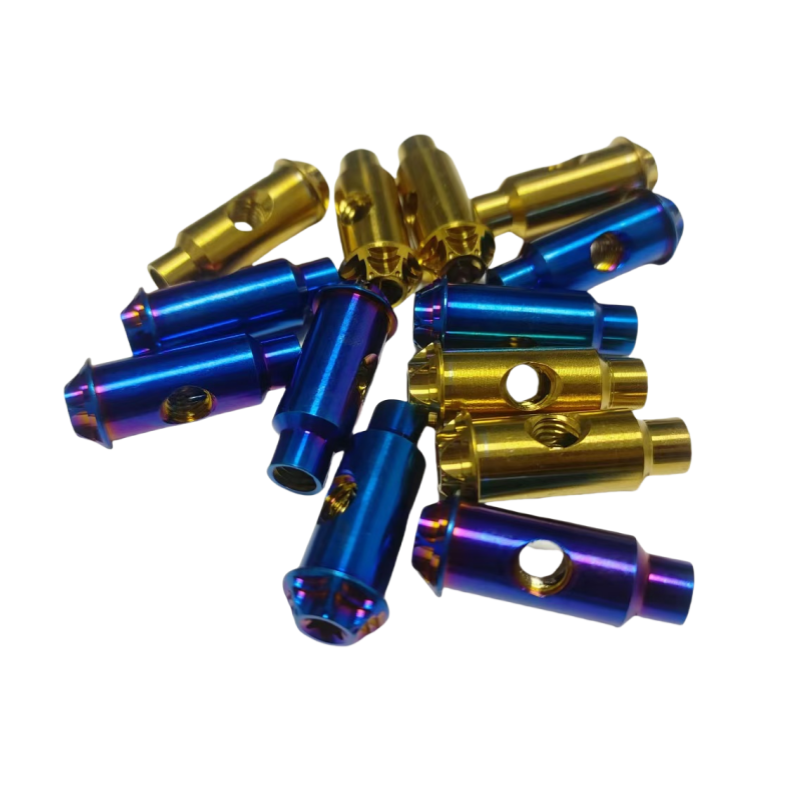
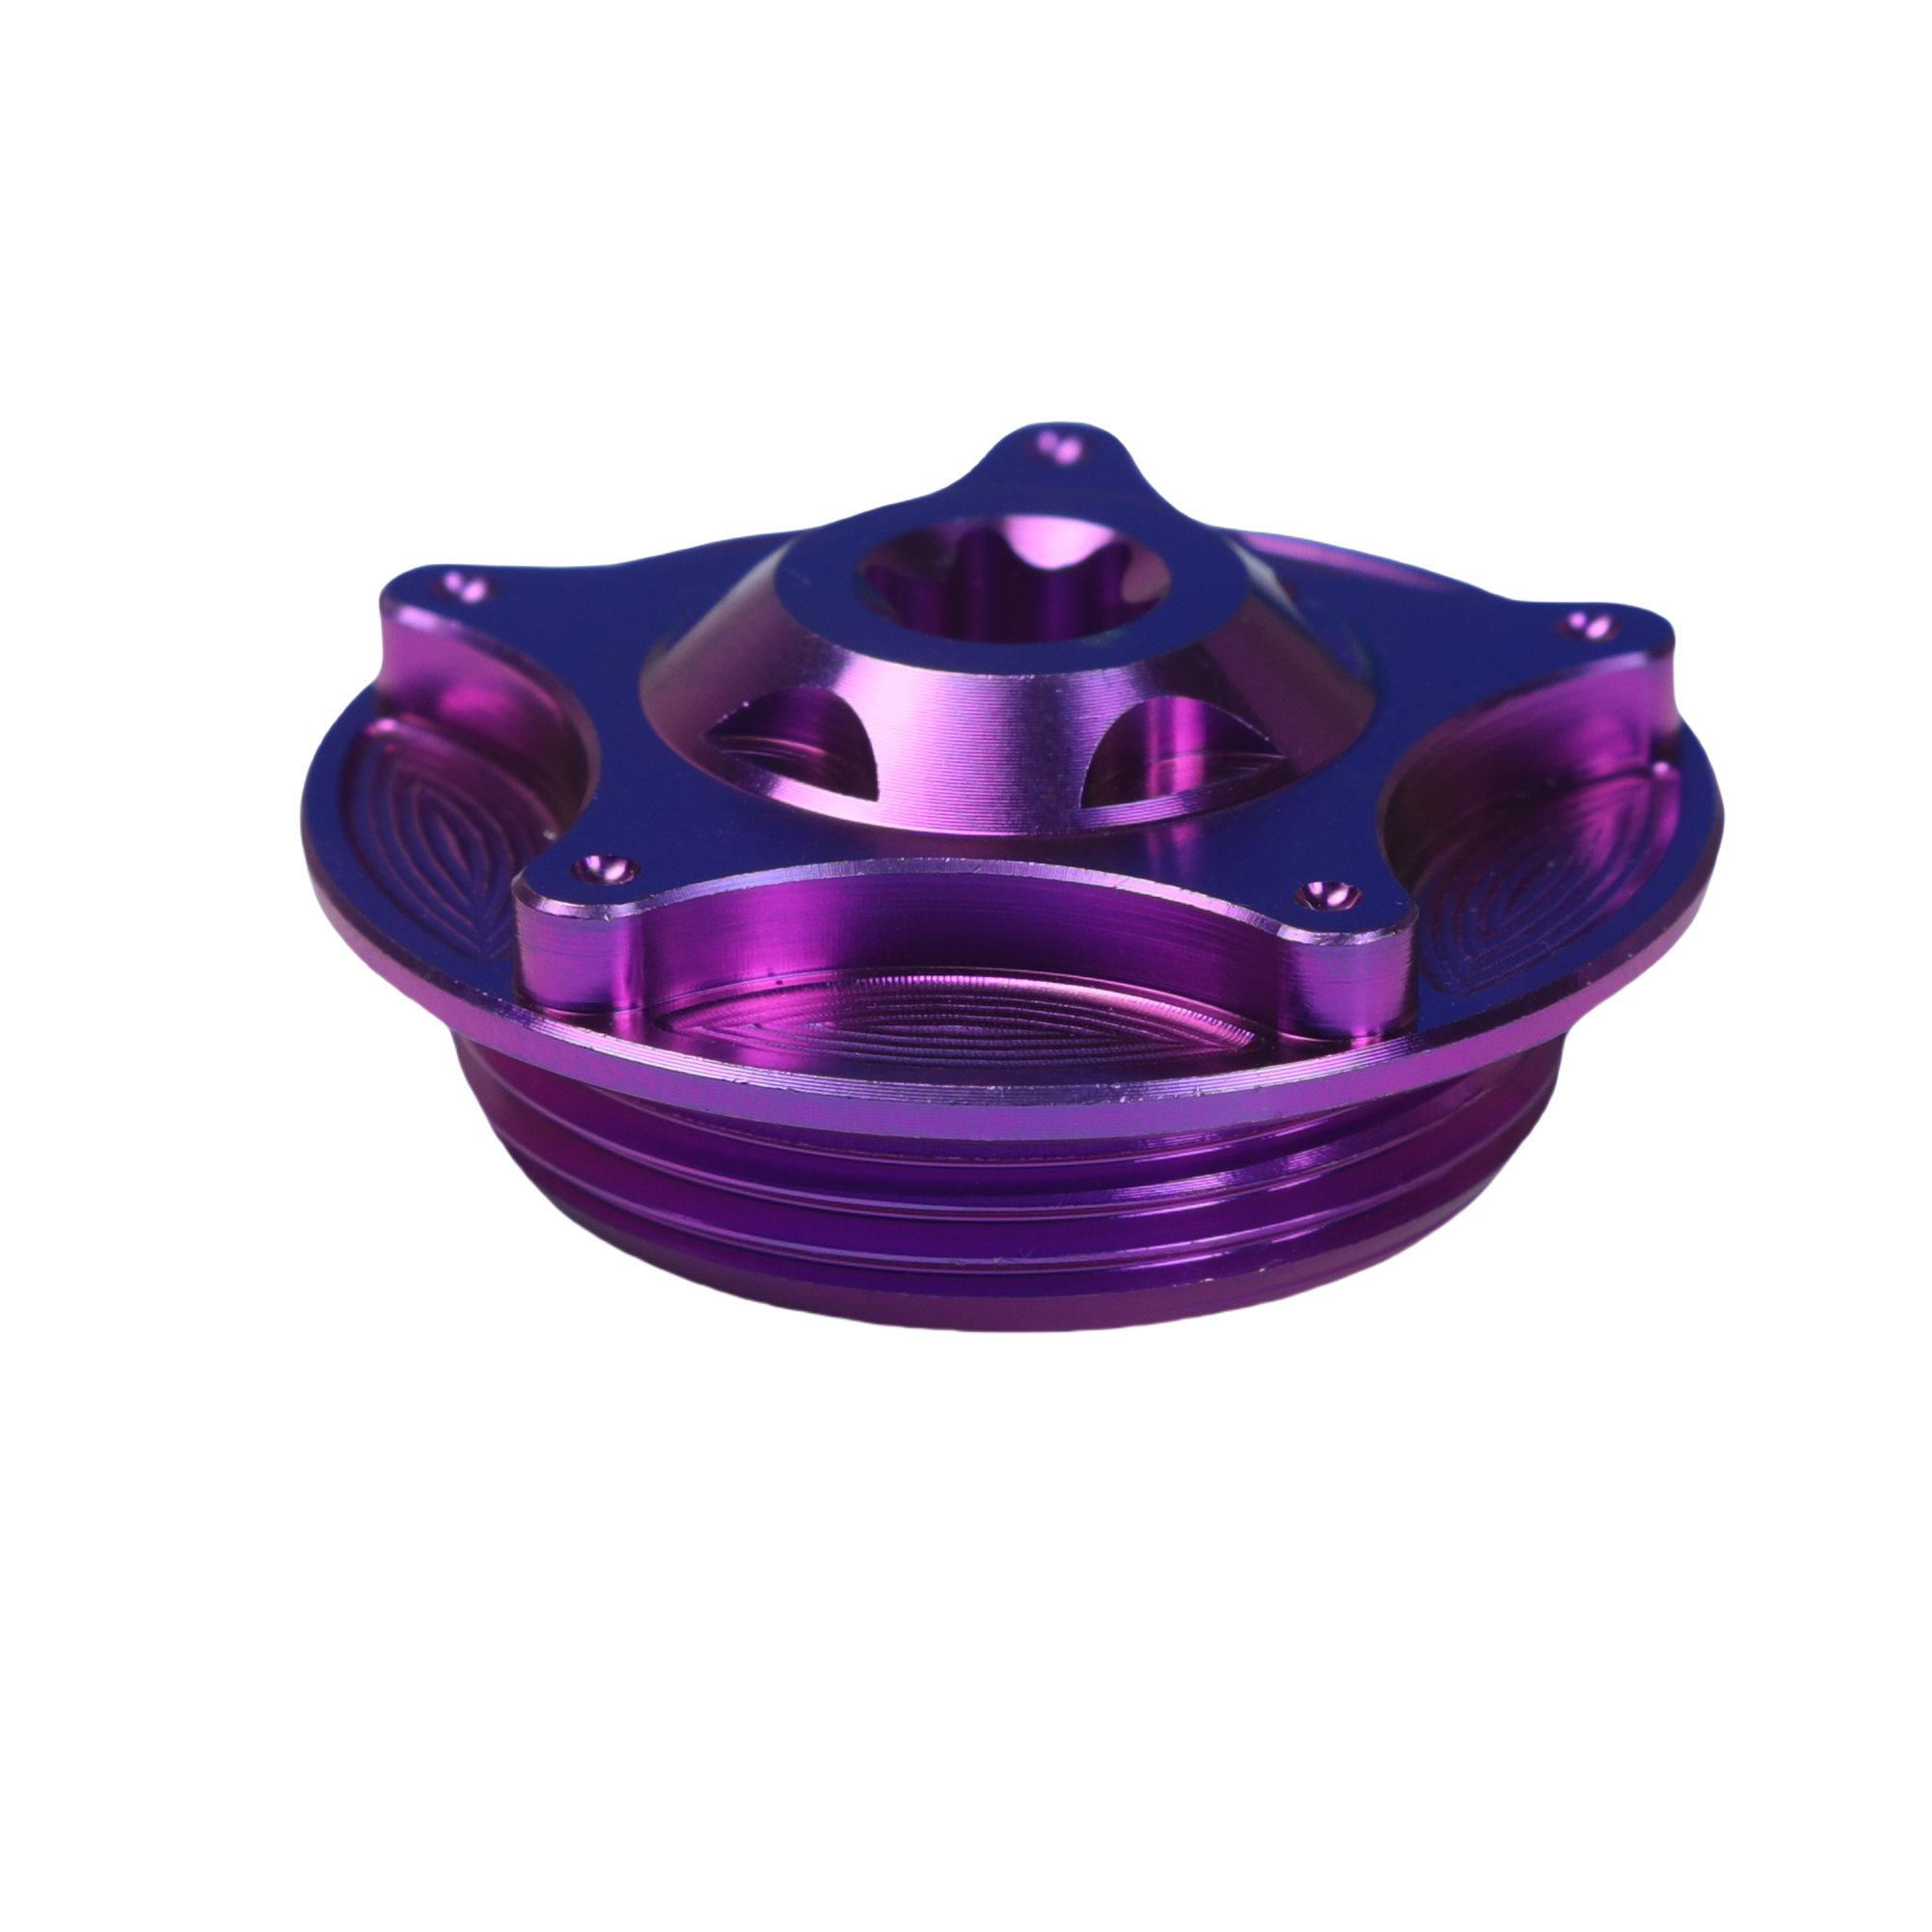
Featured Precision Titanium Fasteners
Standard and custom drawing-machined Ti-6Al-4V components readily exported to Brabant and European supply chains.
Localized Application Scenarios in Eindhoven’s Brainport Hub
Serving precision engineering, mechatronics, and custom performance design across the Greater Eindhoven region.
High-Precision Mechatronics & Cleanroom Robotics
Eindhoven stands as the capital of semiconductor equipment and optical automation. In cleanroom environments where magnetic interference and outgassing must be eliminated, our non-magnetic, acid-etched and ultrasonic-degreased anodized titanium screws eliminate particulate shedding and resist electrochemical contamination.
High-Performance E-Mobility & Custom Motorsport
Eindhoven’s automotive campus develops future-forward racing prototypes and lightweight electric platforms. Replacing high-stress chassis and suspension bolts with our Grade 5 flange screws sheds vital un-sprung weight while maintaining fatigue thresholds capable of handling heavy track vibration and shear stress.
Pro-Cycling Hardware & Harsh Weather Protection
The Netherlands experiences wet, humid, and salt-laden maritime winters. Dutch cycling manufacturers and racing customizers deploy our multi-color anodized M4/M5/M6 stem and disc rotor screws to achieve 100% atmospheric rust prevention, zero chemical degradation, and eye-catching aesthetics.
Procurement & Supply Chain Trends in Eindhoven
Key strategic shifts observed among supply-chain leaders, procurement managers, and R&D labs in North Brabant.
Traceable Full-Spectrum Metallurgy
Procurement teams in Eindhoven reject unverified titanium stock. The market demands direct heat-number traceability back to reputable ingot smelting facilities, coupled with certified EN 10204 3.1 Material Test Reports detailing exact elemental ratios (Al: 5.5–6.75%, V: 3.5–4.5%).
Rapid Prototyping to Low-Volume Scalability
Engineers in Brainport development labs frequently require prototype batches (50–100 pieces) without punitive tooling premiums. Agile Chinese direct-manufacturer relationships offering 3-day rapid-sampling cycles solve the bottleneck between digital CAD models and physical pilot validation.
Functional Anodizing for Visual Identification
Beyond cosmetic appeal, technical engineering units utilize specific electrochemical color-coding (Gold, Burnt Rainbow, Cobalt Blue, Deep Purple) to delineate varying screw pitch sizes, assembly zones, or disassembly access levels during complex line maintenance.
Engineering Data: Grade 5 Titanium vs. Alternative Fasteners
Material properties reference for mechanical, structural, and test engineers.
| Mechanical & Physical Property | Ti-6Al-4V (Grade 5 Anodized) | A2-70 / 304 Stainless Steel | Class 10.9 Structural Steel | 7075-T6 Hard Anodized Aluminum |
|---|---|---|---|---|
| Density (ρ) | 4.43 g/cm³ (44% lighter than steel) | 7.93 g/cm³ | 7.85 g/cm³ | 2.81 g/cm³ |
| Tensile Strength (Ultimate) | ≥ 895 – 1,000 MPa | 700 MPa | 1,040 MPa | 570 MPa |
| Yield Strength (0.2% Offset) | ≥ 828 MPa | 450 MPa | 940 MPa | 505 MPa |
| Elastic Modulus (Young's) | 114 GPa (Superior shock absorption) | 193 GPa | 210 GPa | 72 GPa |
| Corrosion Resistance (Chloride/Acids) | Immune (Forms robust TiO&sub2; shield) | Pitting in marine chlorides | Severe oxidation without zinc/paint | Pitting risk under pH extremes |
| Magnetic Permeability (μ) | 1.00005 (Completely Non-Magnetic) | 1.005 – 1.020 (Slightly magnetic) | Ferromagnetic | 1.00000 (Non-Magnetic) |
Why International Buyers Partner With Zunvo
Direct manufacturing prowess from Baoji, China's "Titanium Valley", built on continuous quality controls.
2015
Established Manufacturing Authority
3,000 m²
Dedicated Production Facility
66%
Annual Client Reorder Rate
≤ 7 Hours
Average Technical Engineering Response
Baoji Ingot Vicinity Advantage
Headquartered at Shiling Road Industrial Park, our plant sits directly adjacent to premier raw titanium sponge smelters. This proximity affords immediate access to prime bar stock, eliminating middlemen delays and lowering overhead costs for our European clients.
Advanced Multi-Axis CNC & Thread Rolling
Equipped with high-precision CNC multi-spindle automatic lathes and cold thread-rolling centers. Rather than machining threads subtractively, thread rolling cold-forms the profile, generating compressive surface stress that suppresses fatigue cracking under cyclic load.
100% Dimensional & Thread Inspection
Every individual production run undergoes comprehensive thread ring-gauge and plug-gauge verification, keyway micro-measurement, optical comparator analysis, and surface uniformity audits to ensure instant, zero-rework insertion into client assembly lines.
Frequently Asked Questions by Eindhoven Procurement Engineers
Direct answers to questions regarding standards, tariff codes, customs clearance, and anti-galling guidelines.
What specific logistics and customs processes apply when importing to Eindhoven?
Shipments to Eindhoven typically enter the Netherlands via Amsterdam Schiphol Airport (AMS) or the Port of Rotterdam (for full container ocean freight) before domestic transit via the A2 corridor directly to industrial parks such as High Tech Campus Eindhoven or De Run in Veldhoven. We generate complete export packages—including Commercial Invoices with correct HS Codes (HS 8108.90 for titanium articles / HS 7318 for threaded screws), Packing Lists, and Certificates of Origin—facilitating seamless VAT declarations through your Dutch freight forwarder or direct DHL/FedEx Express clearance.
How does the anodized layer on titanium behave inside high-vacuum cleanroom settings?
Unlike organic coatings, lacquers, or electroplated zinc finishes, titanium color anodizing does not use dyes or external chemicals. Instead, an electrochemical bath grows a controlled, microscopic titanium dioxide (TiO&sub2;) layer that produces interference colors naturally. Because the film is an integrated transformation of the base metal, it demonstrates exceptional outgassing stability under ultra-high vacuum (UHV) regimes and will not peel, flake, or generate volatile airborne molecular contaminants (AMC).
How can engineers prevent galling (cold welding) when threading titanium bolts into titanium or aluminum blocks?
Titanium exhibits a high coefficient of friction, which creates risk of galling under high torque when metal surfaces contact directly without lubrication. For critical mechanical assemblies, we recommend: 1) Applying an aerospace-grade anti-seize paste (such as molybdenum disulfide or copper-based paste); 2) Opting for our specialized anti-friction micro-coatings or PVD thin films; and 3) Adhering strictly to torque specifications, avoiding pneumatic impact tools that generate rapid frictional heat.
Can Zunvo manufacture non-standard custom thread geometries from CAD models?
Yes. Our in-house engineering team handles STEP, IGES, DXF, and standard PDF mechanical drawings. Whether your project requires custom flange diameters, hollow-drilled lightweight shafts, specialized Torx-Plus driving sockets, fine-pitch UNF/UNC threads, or non-standard metric lengths, our CNC machining workshop produces accurate pre-production evaluation prototypes within 3 working days.
What are the standard order quantities and expected lead times for European deliveries?
Our standard catalog fasteners carry low trial order minimums starting at 100 pieces (or 10–50 dozens depending on specific thread size). In-stock fasteners ship within 24–48 hours. Custom CNC production orders generally require 7 to 15 days of workshop throughput, followed by 3–5 working days via door-to-door air express to Eindhoven and the Benelux region.
Accelerate Your Supply Pipeline with Factory-Direct Gr5 Fasteners
Submit your CAD blueprints, bill of materials, or replacement screw specifications. Receive an itemized quote, mill test certification review, and export schedule within 7 hours.
