High-Performance Titanium Engine & Powertrain Fasteners
Direct factory export specifications: Certified Ti-6Al-4V aerospace grade, hot forged, precision CNC turned, and cold thread-rolled according to metric DIN standards.
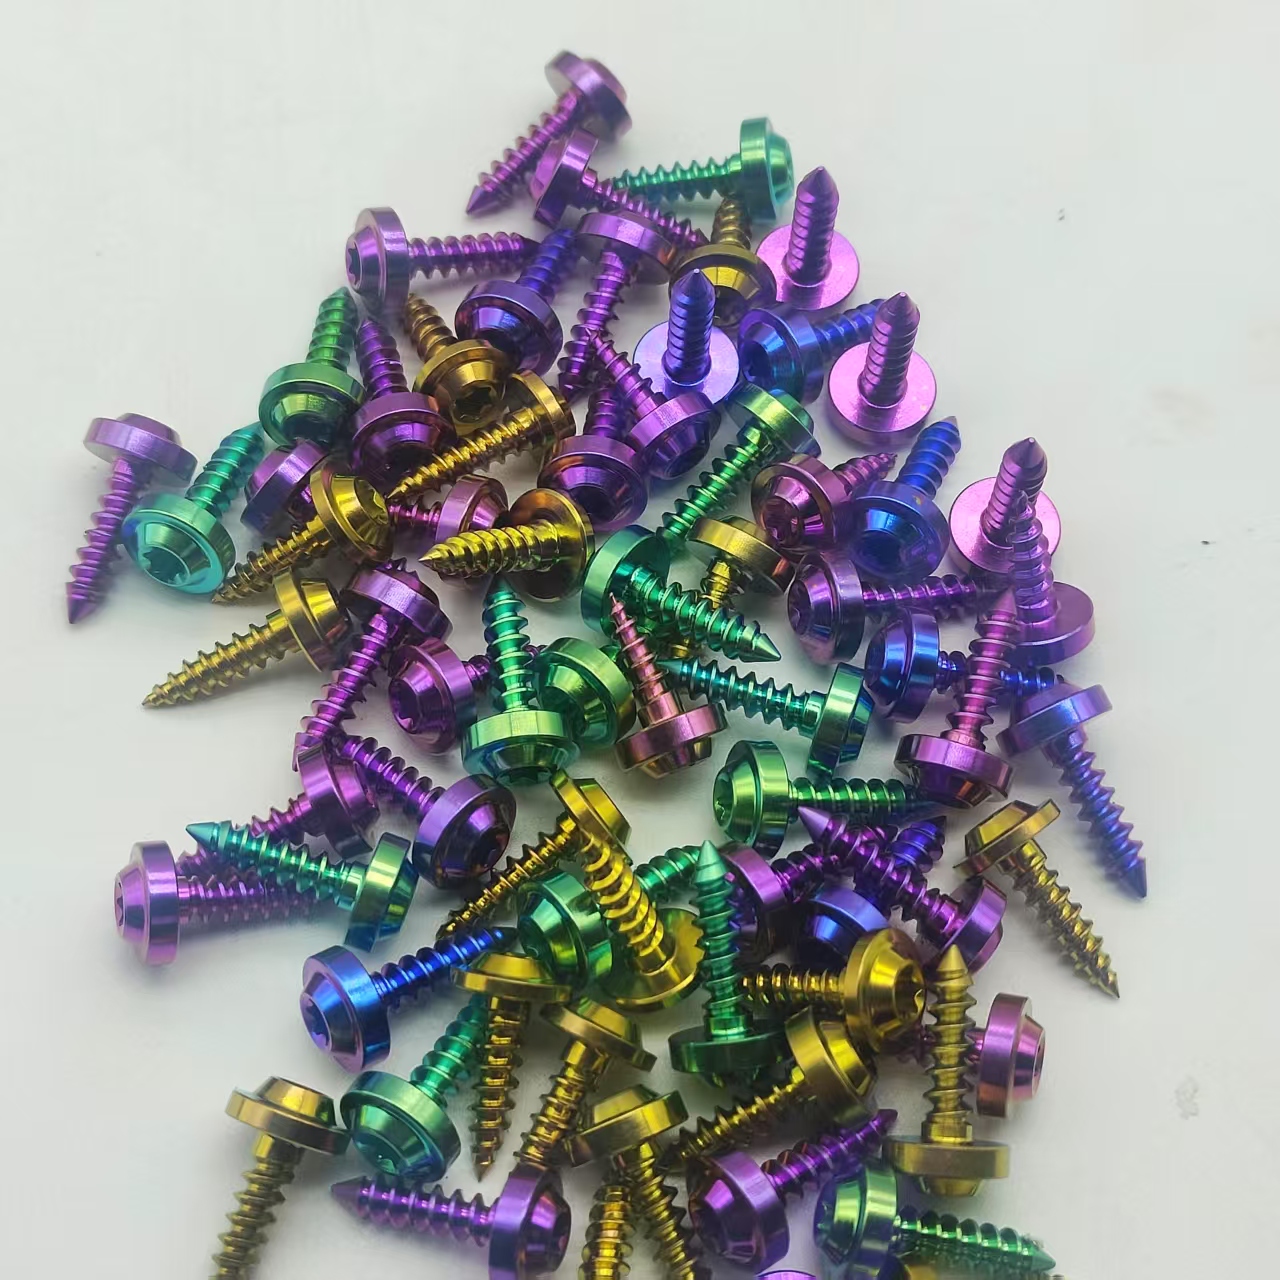
High Strength M4-M5 Titanium Alloy Torx Head Self-Tapping Screws Hex Washer Head
- StandardDIN Metric
- DriveTorx / Hex Washer
- SurfaceAnodizing / PVD
- MaterialGr5 Ti-6Al-4V
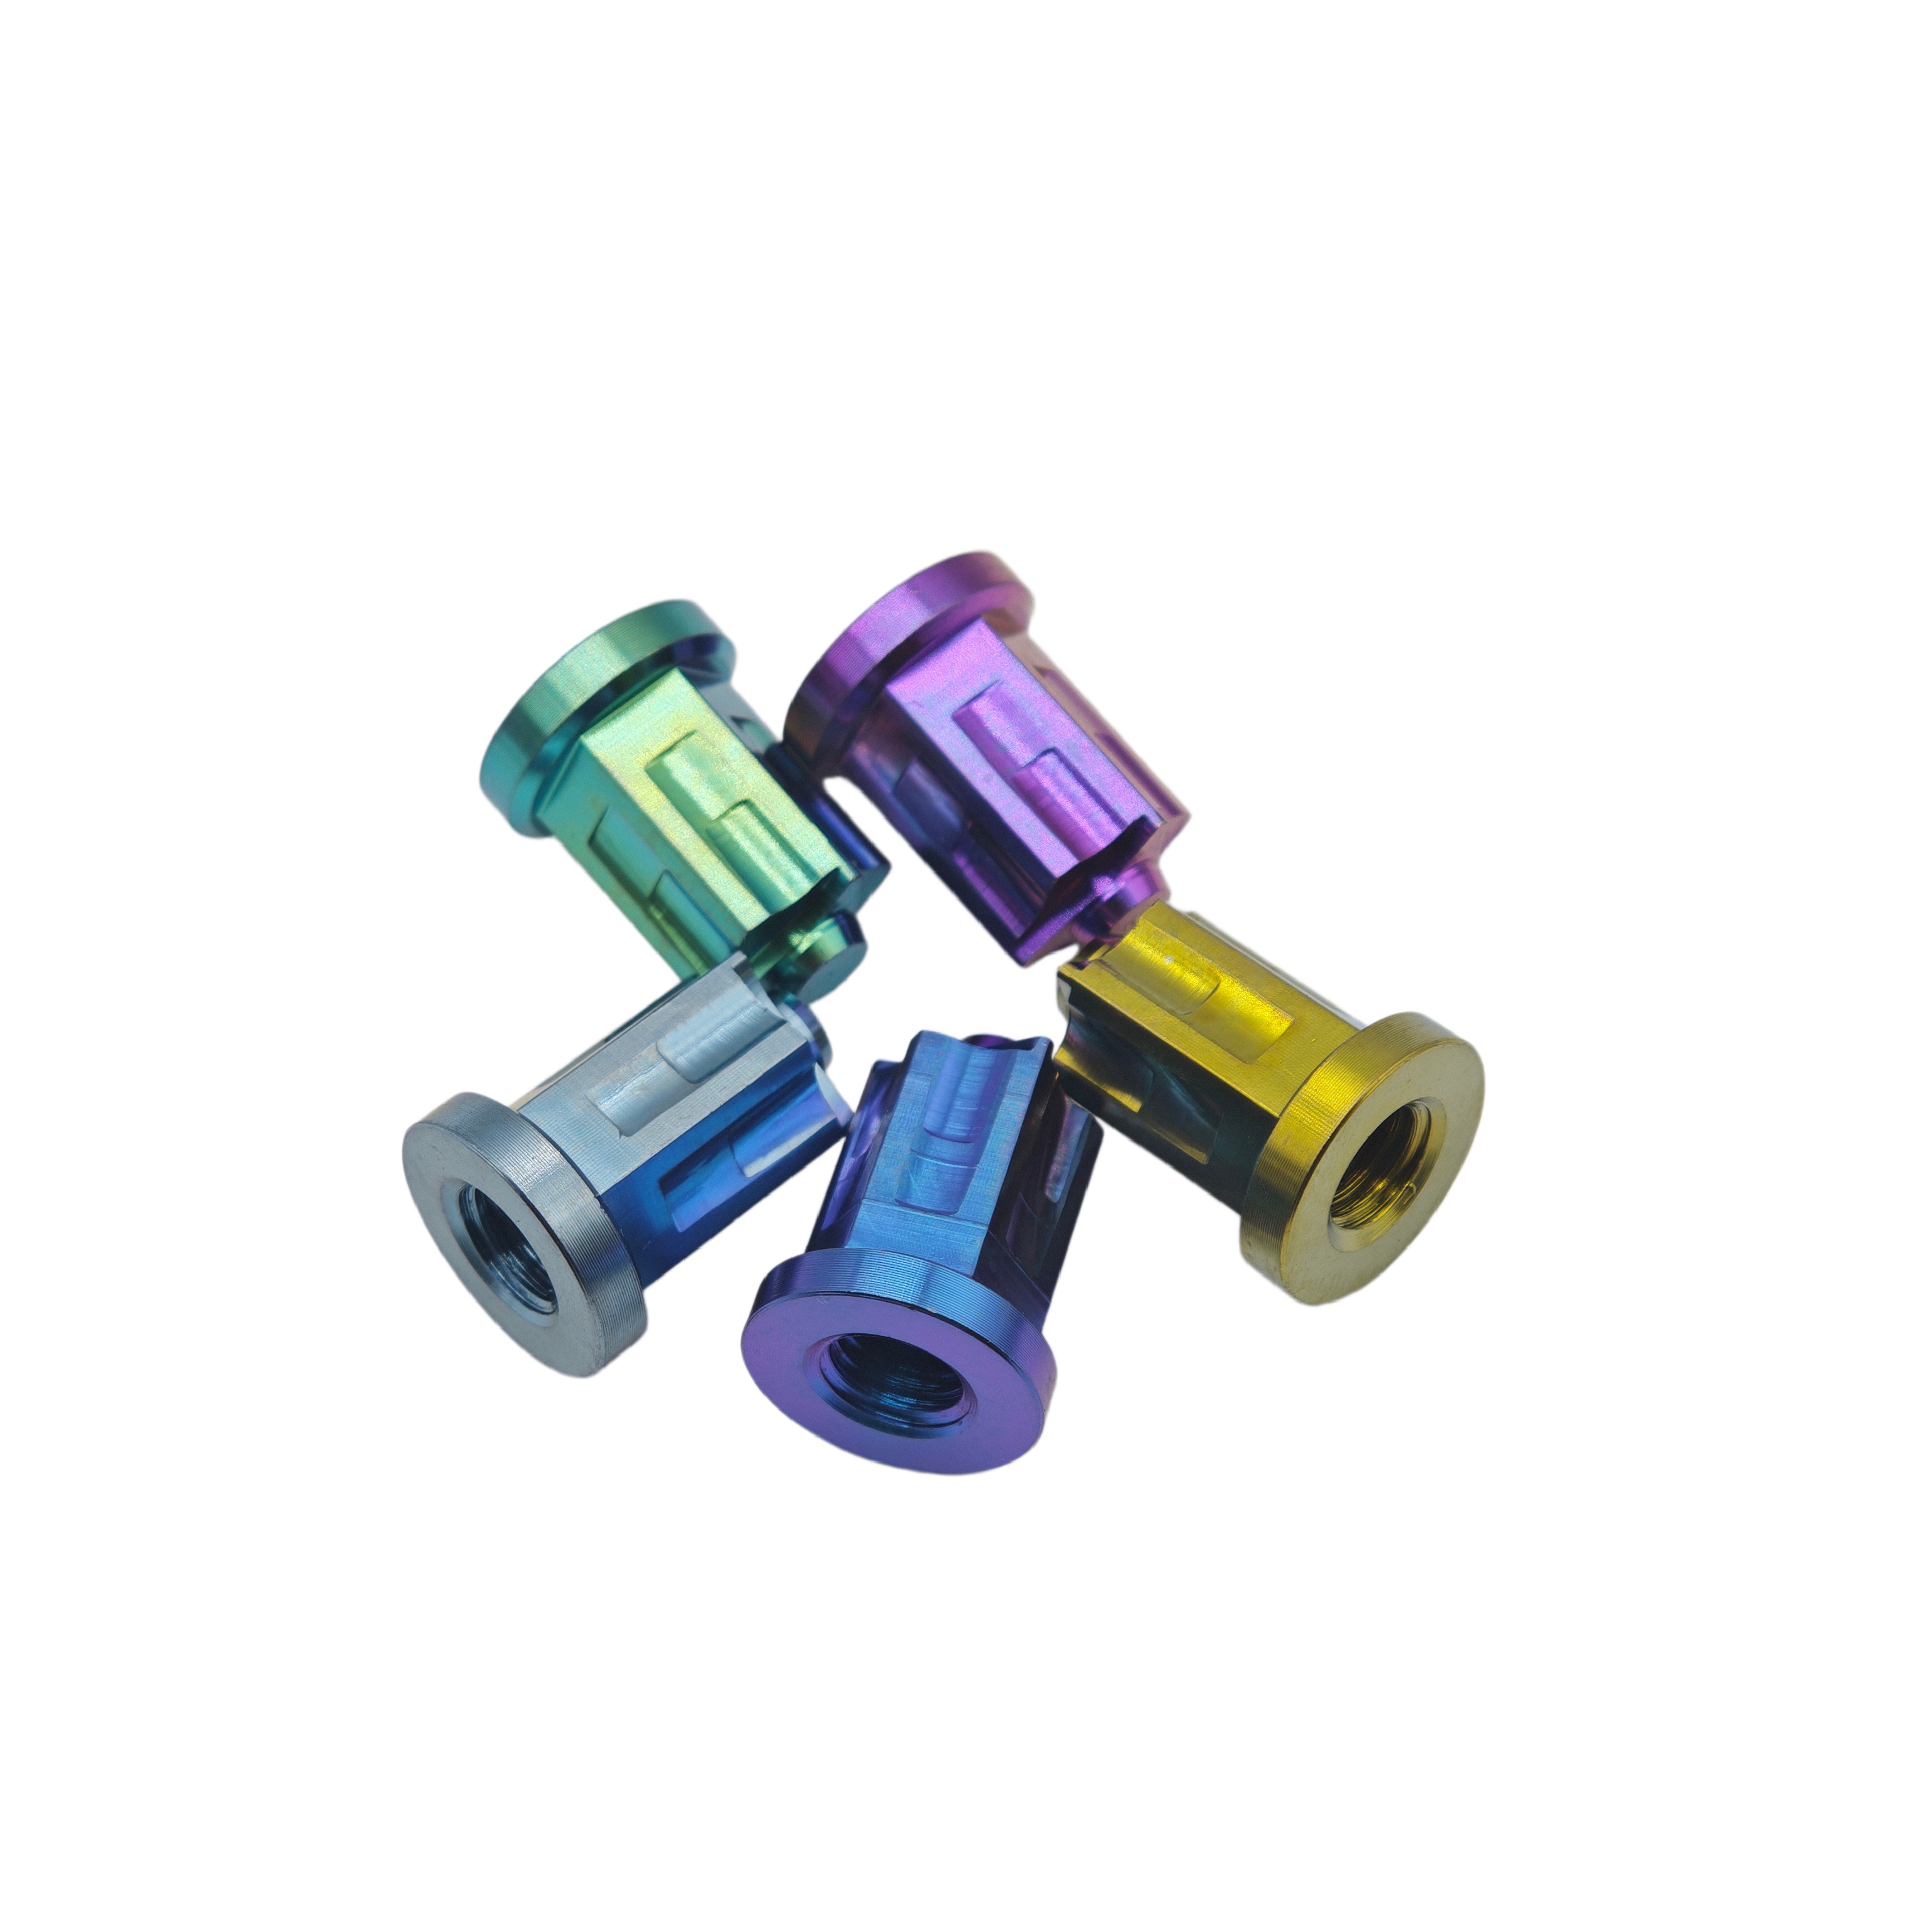
Tecksr Titanium Alloy Hex Head French-style Closed Flower Nuts Class 10 GR5
- ClassClass 10 High Yield
- GeometryClosed Flower / Flange
- ApplicationAxle & Engine Stay
- Tensile≥ 950 MPa
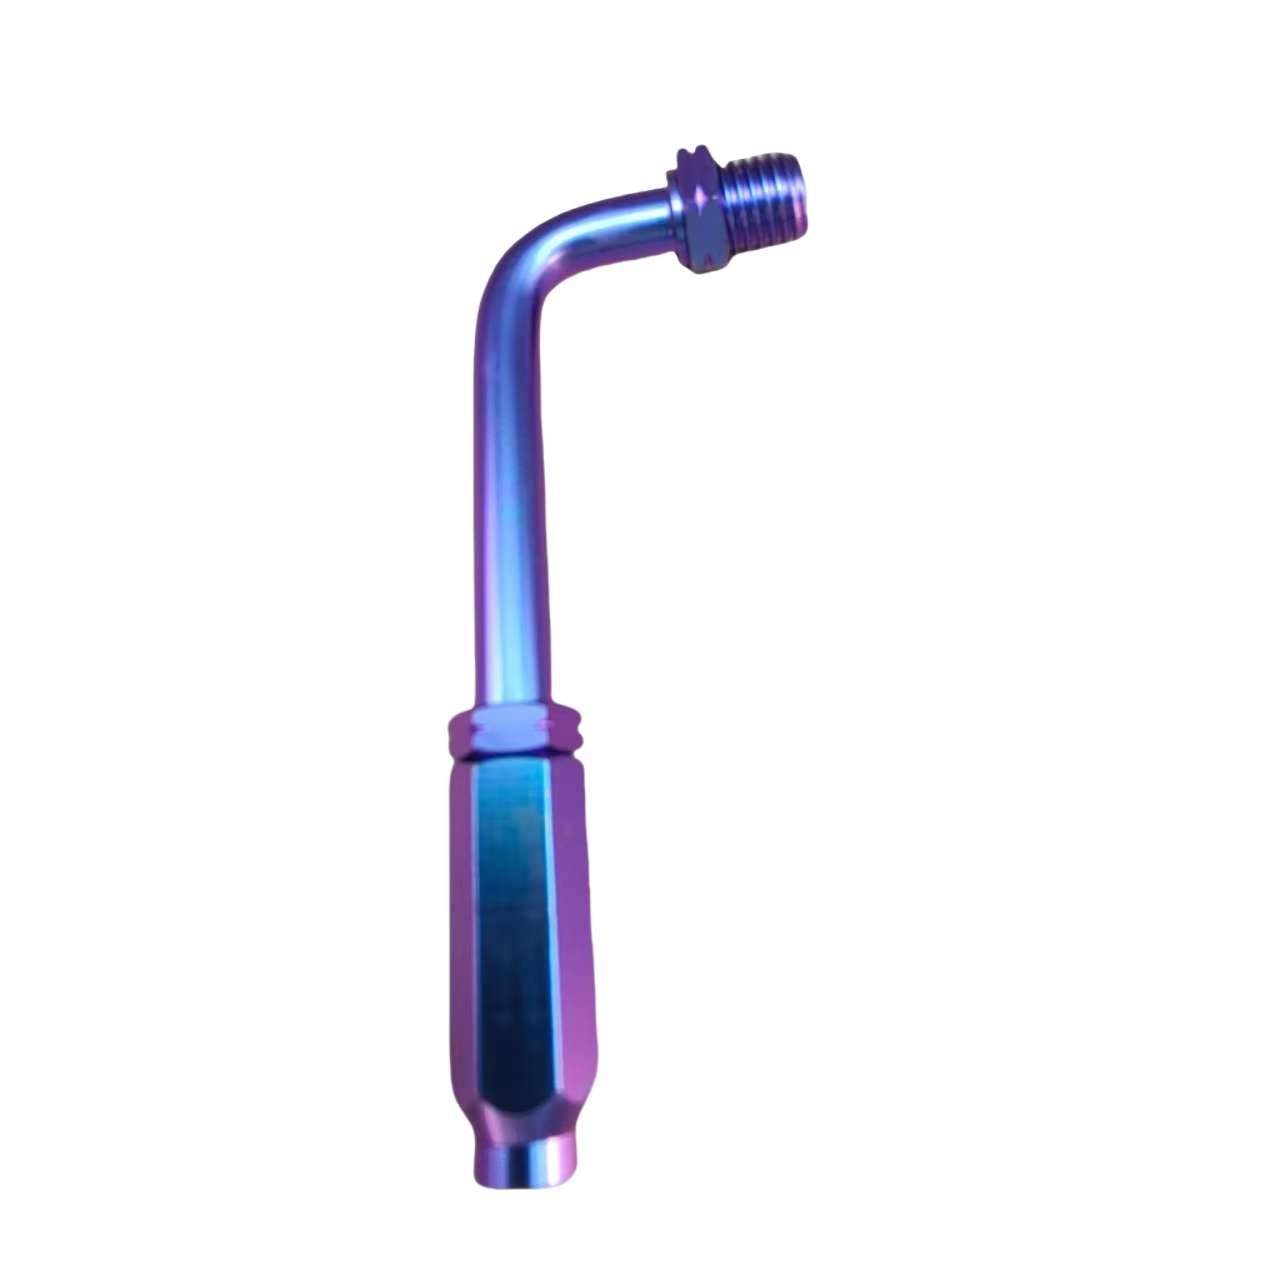
Custom CNC Gr5 Flat Head Titanium Throttle Line Colorful Refueling Cable Fittings
- Process5-Axis CNC Precision
- Tolerance±0.005 mm
- ComponentThrottle / Valve Parts
- TreatmentPVD Vacuum Rainbow
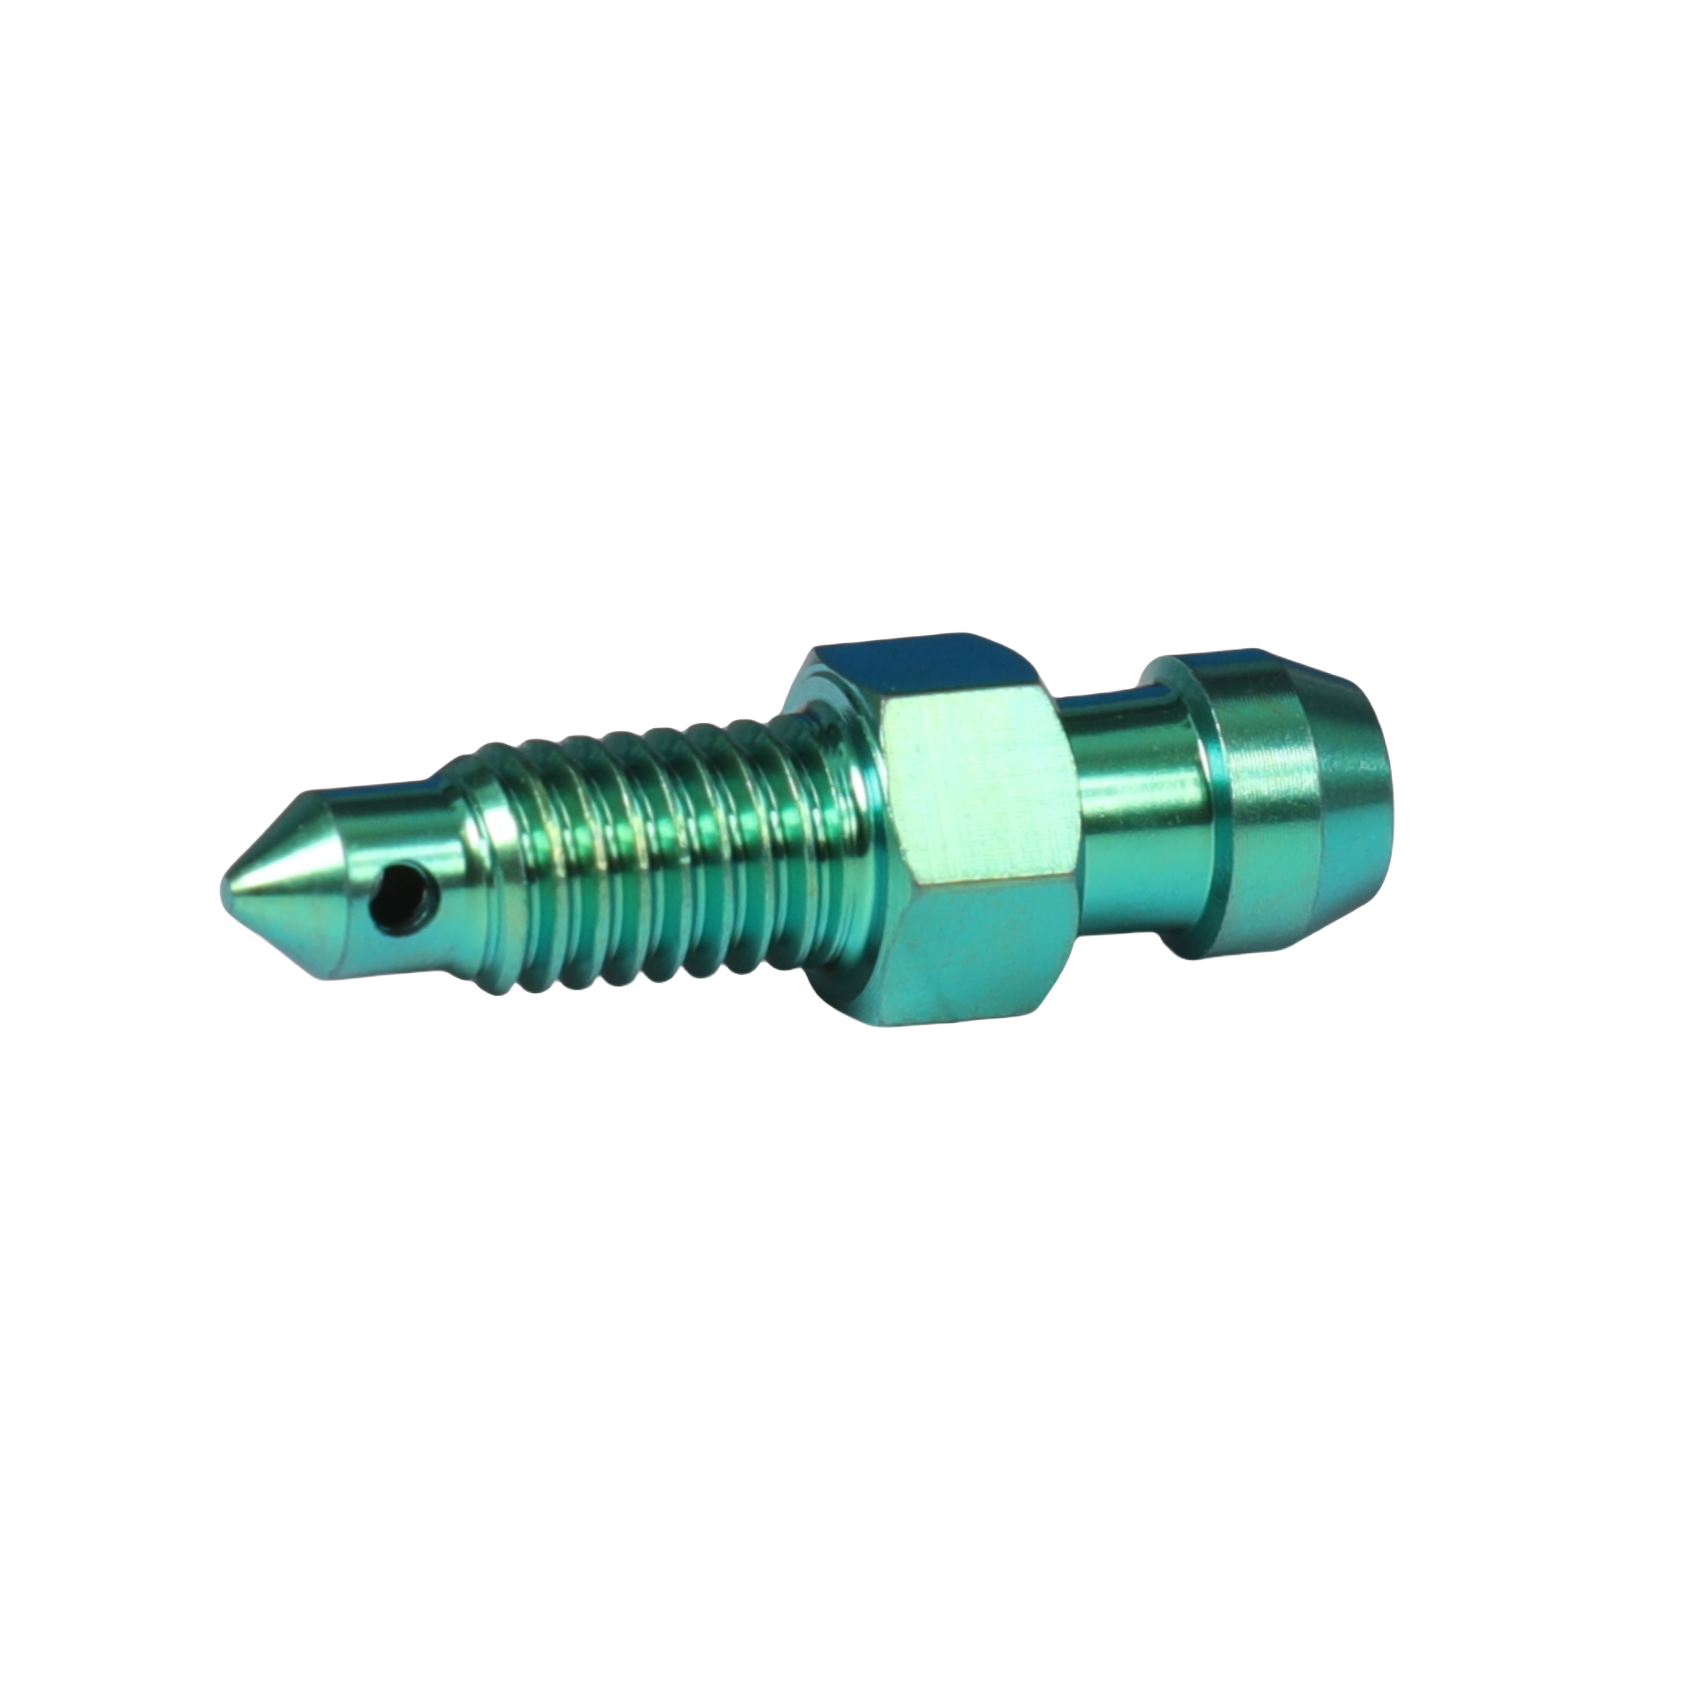
TKS M6 Anodized Gr5 Titanium Hex Motorcycle Caliper Oil Drain Bleed Bolt Screw
- ThreadM6 Metric Fine Pitch
- FluidDOT 4 / 5.1 Compatible
- CorrosionZero Salt Chloride Pit
- SealingCNC Micro-Conical Seat
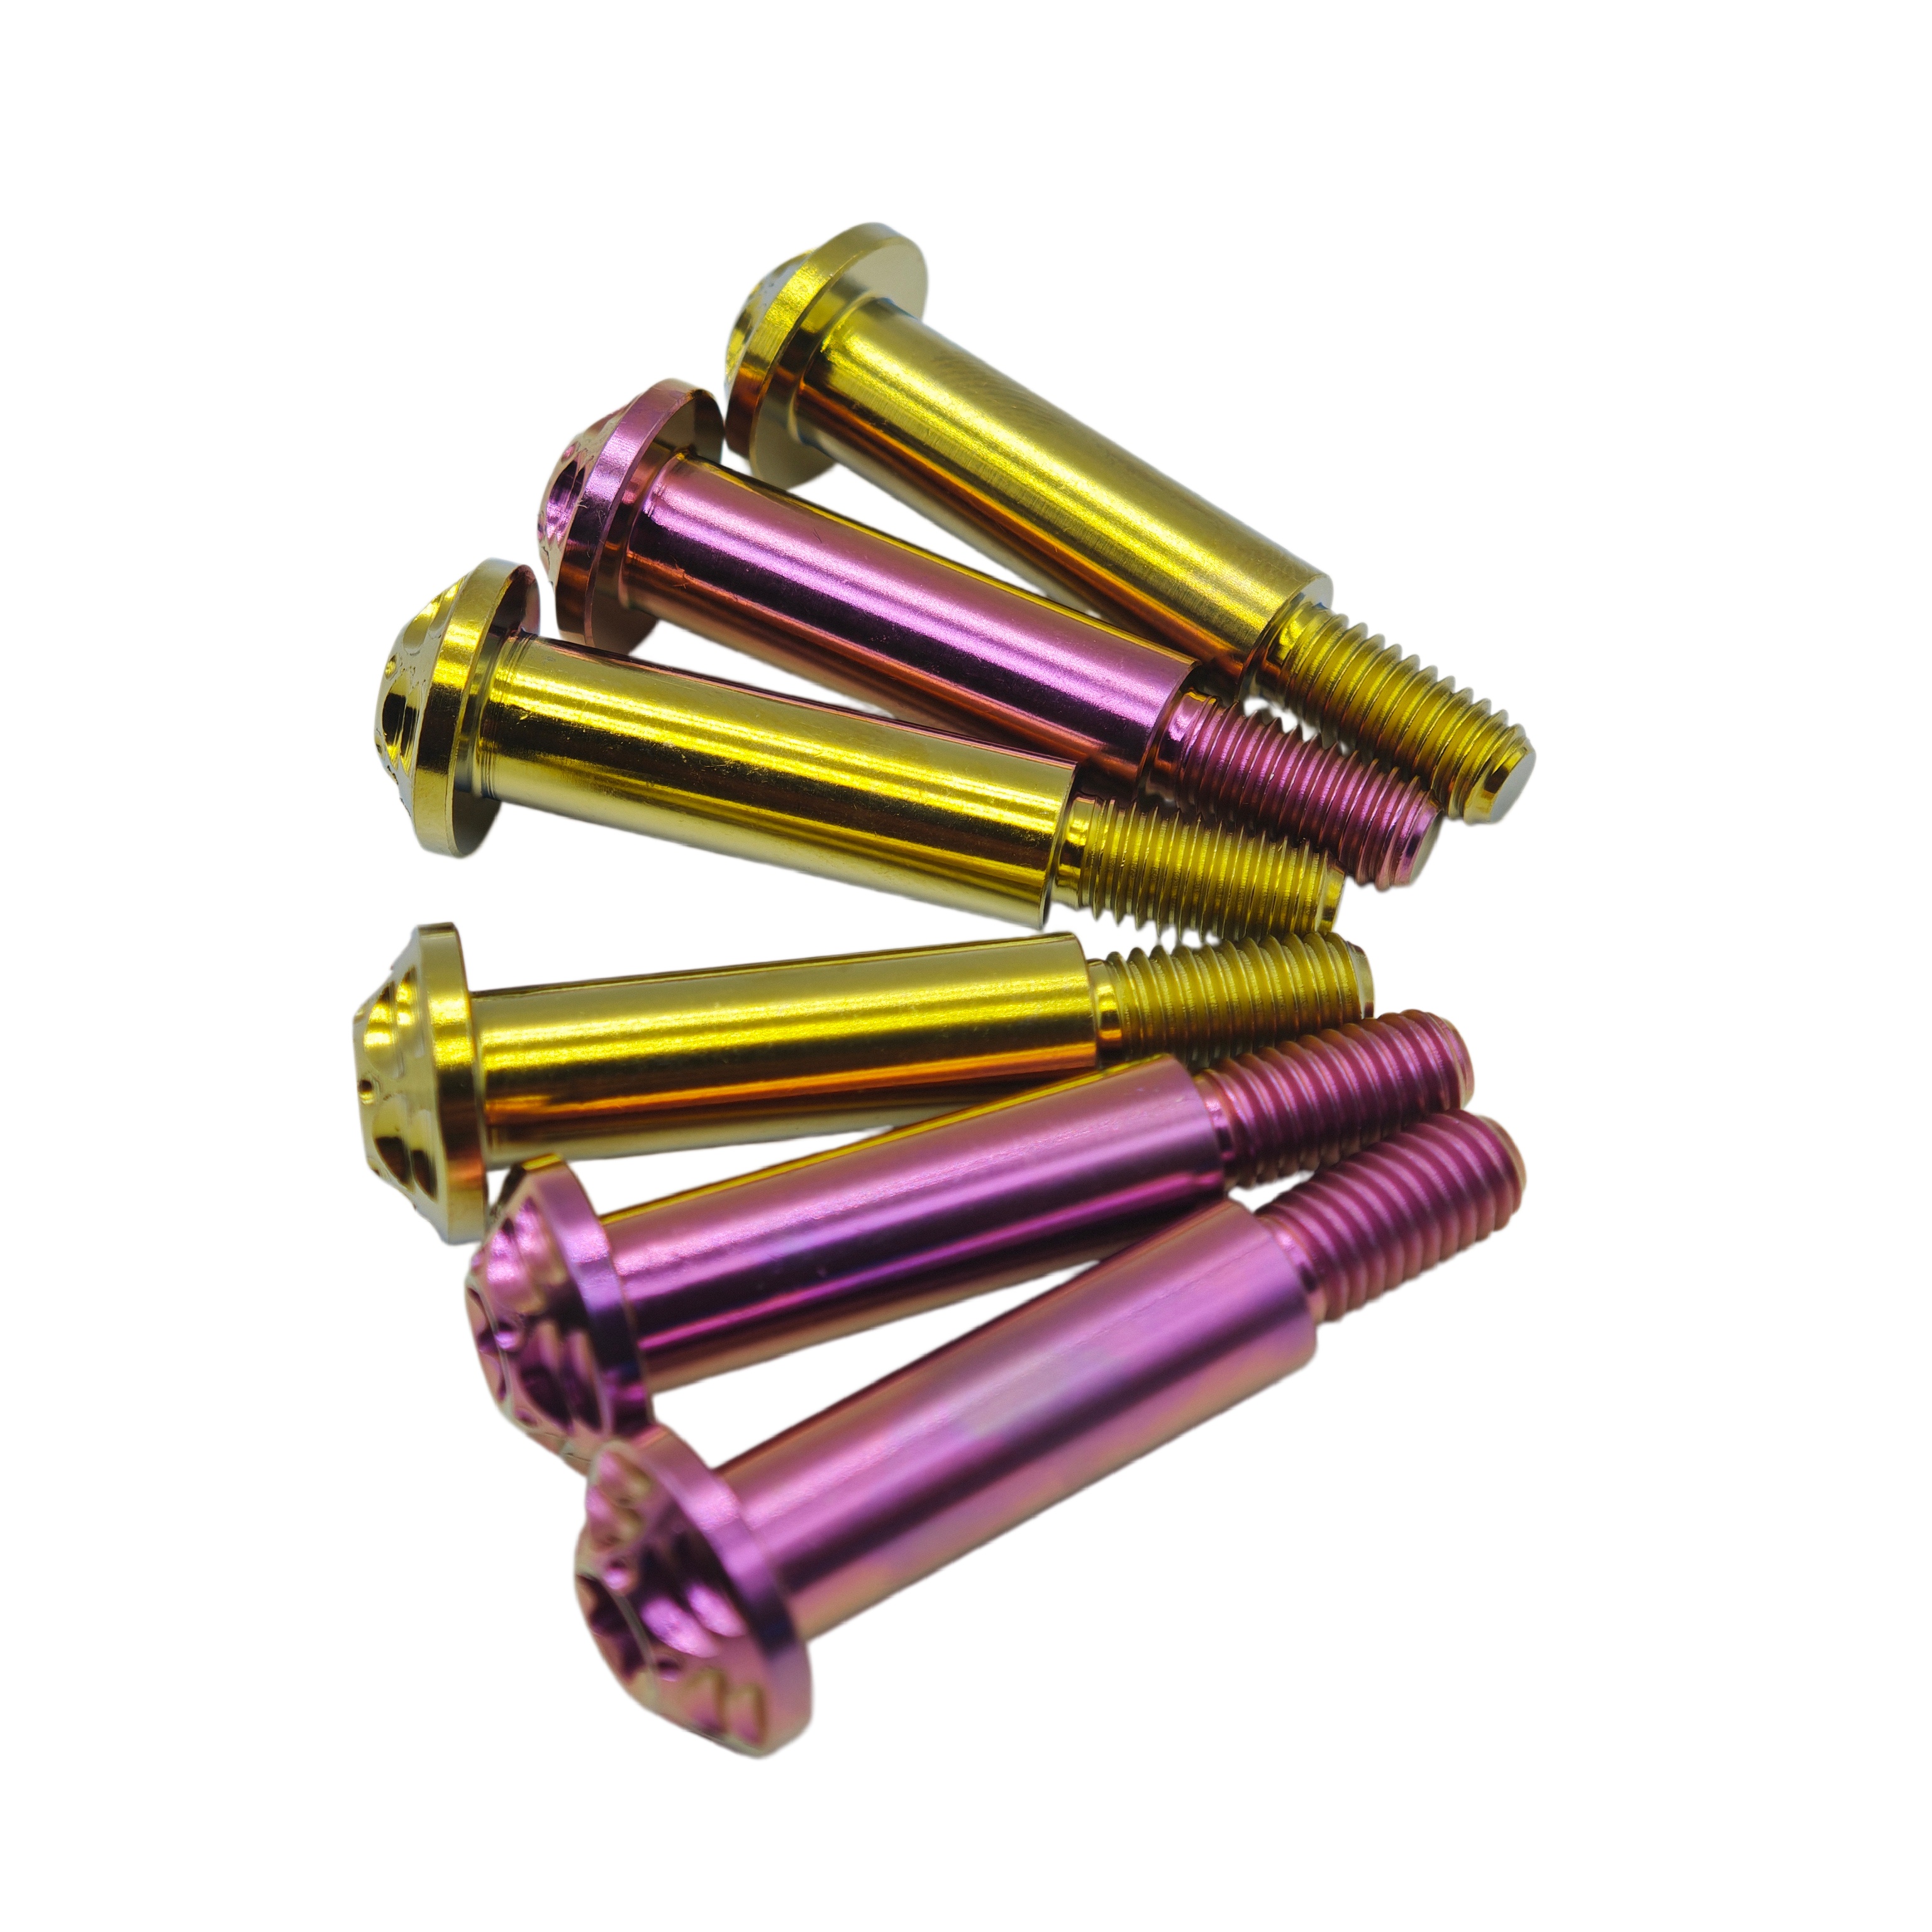
Factory Price GR5 Titanium Alloy Anodized Pan Head M6 Brake Lever Bolt Modification
- ThreadM6 Ground Precision
- HeadLow-Profile Pan Torx
- FinishElectrolytic Anodize
- Weight44% Steel Reduction
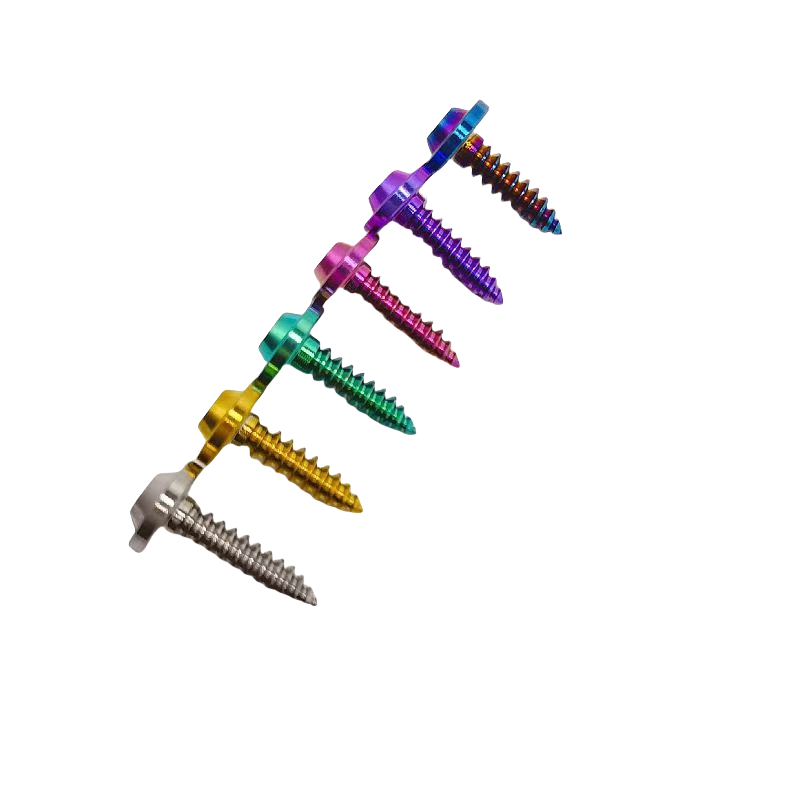
M4/M5 Blue Grey Titanium Pan Head Self-Tapping Screws DIN Standard for Fairing
- SizeM4 / M5 Multi-pitch
- DesignAnti-vibration Flange
- ColorGerman Industrial Grey
- ComplianceRoHS & REACH
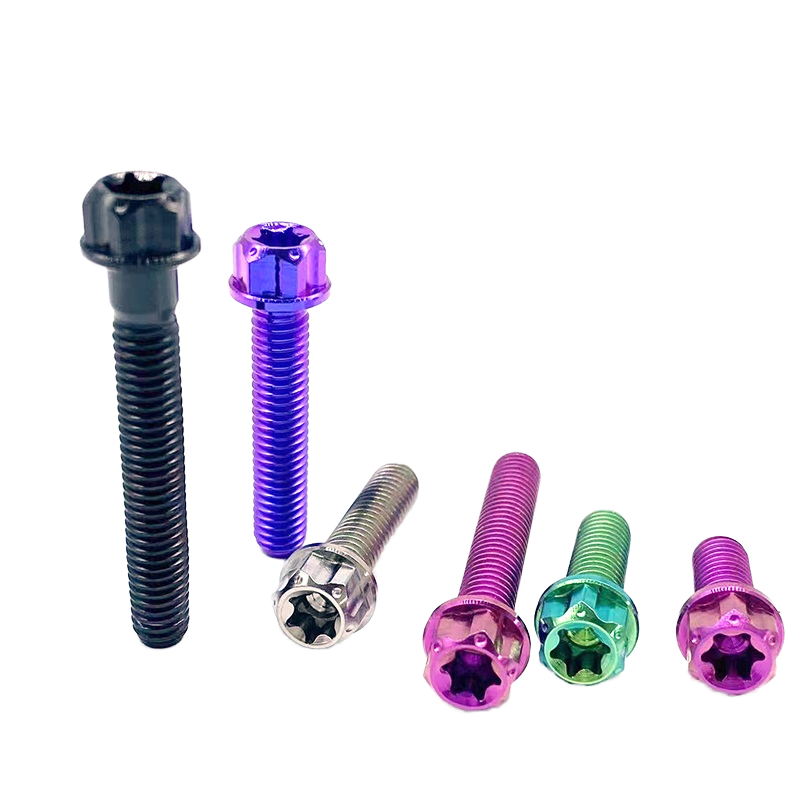
GR5 Titanium Alloy M8 M10 Flange Bolts Hexagon Screws for Powertrain Casing
- DimensionM8 & M10 Casing Lengths
- FlangeIntegrated Load Ring
- ThreadClass 6g Cold-Rolled
- StandardMeets DIN 6921 Metric
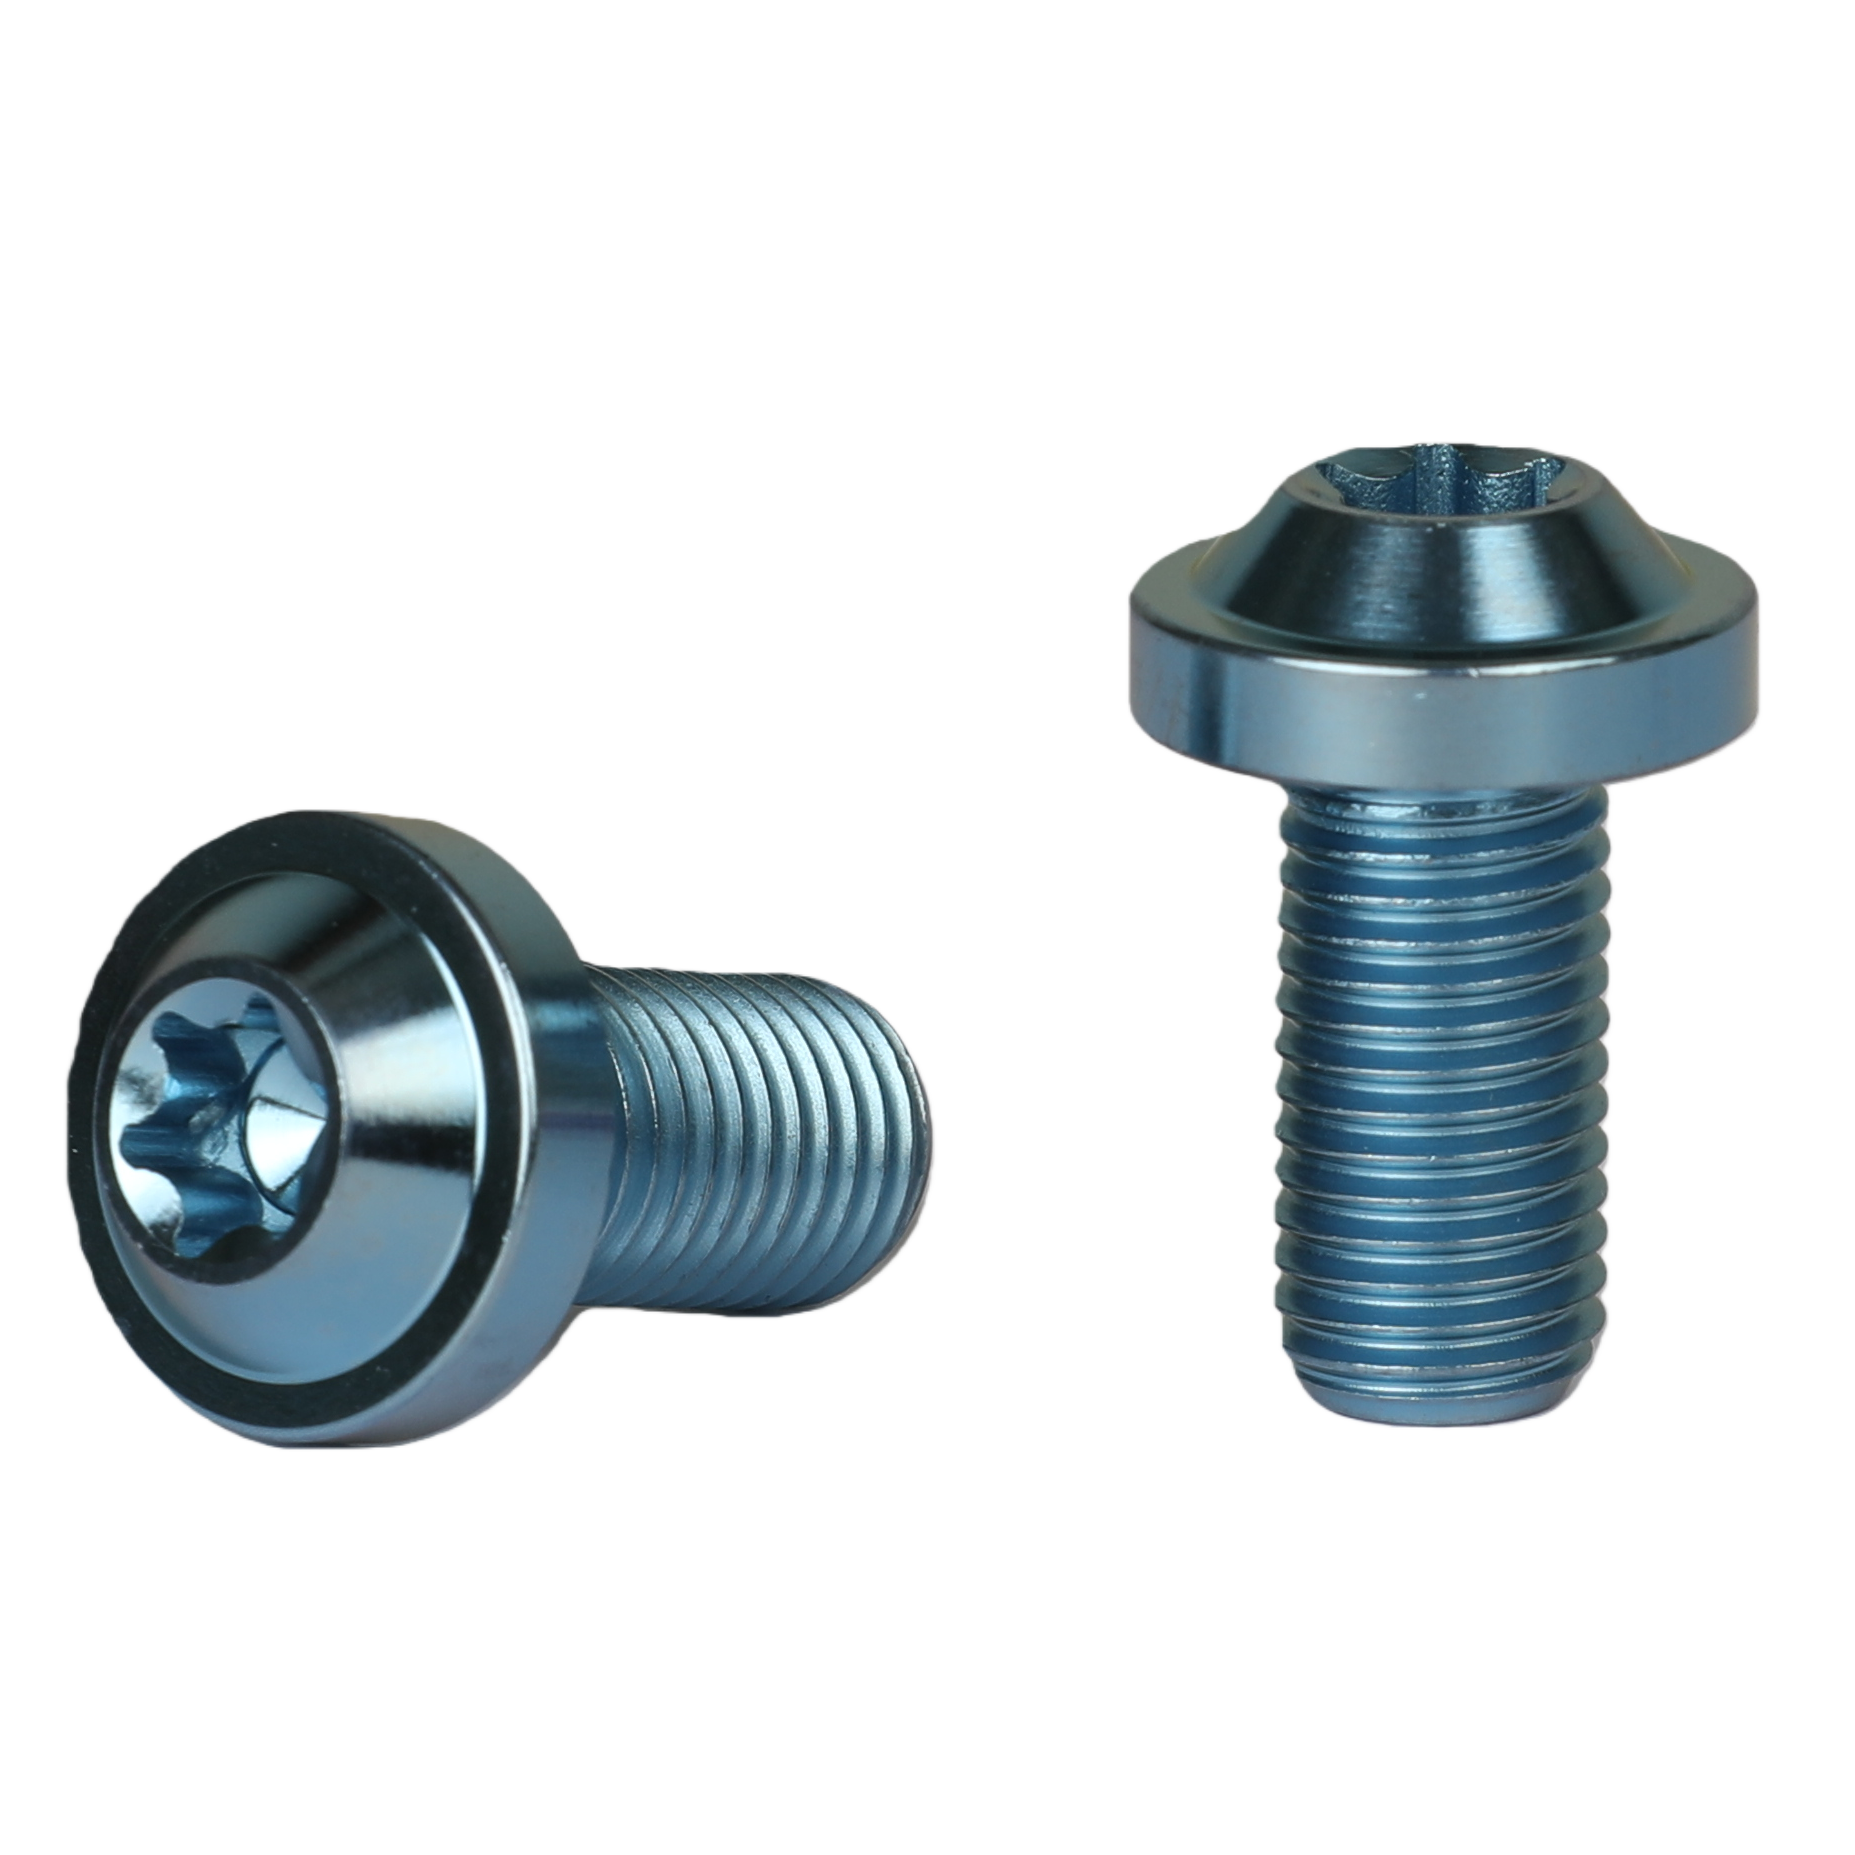
GRX Grade 5 Titanium Pan Head Brake Disc Rotor Screws Race M6/M8/M10 DIN Thread
- Thread ClassISO 965-1 Metric 6g
- DriveTorx T30 / T40 Deep
- Shear ProofHigh Cyclical Fatigue
- RatingTrack & Nordschleife
Metallurgical Superiority in High-RPM German Engine Assemblies
Why Tier-1 performance tuners in North Rhine-Westphalia substitute standard grade 8.8 and 10.9 structural steel with Ti-6Al-4V Grade 5 fasteners.
Mass Reduction & Resonant Frequencies
With a calibrated density of 4.43 g/cm³ compared to carbon steel's 7.85 g/cm³, titanium engine hardware provides an immediate 43.6% reduction in parasitic hardware mass. In valvetrain retainers, crankcase girdle bolts, and cam cover studs, this lower inertia minimizes harmonic vibration amplitudes at high RPMs, directly protecting aluminum block threads from cyclical pull-out stresses.
Thermal Expansion Compatibility
The coefficient of thermal expansion (CTE) of Ti-6Al-4V is 8.6 × 10⁻⁶/K, aligning far closer to cast aluminum engine casings (21-24 × 10⁻⁶/K) than alloy steel (11-12 × 10⁻⁶/K). Under severe thermal cycles encountered on the Autobahn or track environments, titanium engine bolts mitigate differential thermal tension spikes, preserving steady clamp loads across gasket interfaces.
Severe Corrosion & Chemical Resistance
Titanium instantaneously develops an adherent, chemically inert TiO₂ passivating surface film. It remains completely impervious to hot synthetic motor oils, glycol coolants, road salt brines (CaCl₂/NaCl) used across German winters, and extreme combustion blow-by acidity. Unlike plated steel fasteners, our Ti fasteners will never suffer surface micro-pitting or hydrogen embrittlement.
| Mechanical / Physical Property | Gr5 Ti-6Al-4V (Zunvo Engine Spec) | A2-70 Stainless Steel | Class 10.9 Quenched Alloy Steel | Class 12.9 High-Tensile Steel |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 (Lightweight Advantage) | 7.93 | 7.85 | 7.85 |
| Ultimate Tensile Strength (Rm, MPa) | 950 – 1050 | 700 | 1000 – 1040 | 1220 |
| Yield Strength (Rp 0.2, MPa) | ≥ 880 | 450 | 900 | 1100 |
| Strength-to-Weight Ratio (kN·m/kg) | 214 (Industry Benchmark) | 88 | 127 | 155 |
| Modulus of Elasticity (GPa) | 114 (Dampens Harmonics) | 193 | 205 | 210 |
| Hydrogen Embrittlement Vulnerability | Zero Susceptibility | Negligible | Moderate | High Risk (Galvanic Plating) |
| Thread Process Standard | Continuous Cold-Rolled (DIN 965-1) | Cut / Rolled Mixed | Rolled Post-Heat | Rolled Post-Heat |
Serving the Cologne, Eifel & Rhine-Ruhr Motorsport Corridor
Tailored supply chain logistics supporting motorsport manufacturers, tuning ateliers, and Tier-1 engineering hubs across Cologne-Niehl, Cologne-Marsdorf, and nearby testing circuits.
Cologne Powertrain Prototyping
Situated near the historic industrial centers of Cologne-Niehl and high-tech automotive prototyping facilities in Marsdorf, our Grade 5 engine studs, exhaust manifold hardware, and transmission case fasteners provide the dimensional precision required by racing skunkworks and OEM prototype development teams.
Nürburgring Endurance & VLN/NLS Series
Located just 85 kilometers south of Cologne lies the Nürburgring Nordschleife. Endurance GT racing programs running the ADAC 24h race demand absolute fastener reliability under curb strikes, excessive brake rotor radiation, and cyclical shear loads. Our track-proven M8/M10 brake disc screws and wheel hub hardware eliminate thermal warping.
Intermot Cologne & Custom Motorcycle Builders
Cologne is the world stage for motorcycling via INTERMOT. We support boutique motorcycle manufacturers and racing rebuilders throughout North Rhine-Westphalia with complete bespoke CNC bolt kits for engine covers, dry-clutch pressure plates, triple-tree clamps, and suspension linkages with custom PVD anodized aesthetics.
Meeting German Industrial Standards: DIN, ISO & Environmental Norms
Sourcing precision components from China into the German market requires uncompromised conformity to metrological conventions, thread root profiling, and chemical registrations.
Cold-Rolled Grain Structure vs. Cut Threads
Standard European automotive protocols prohibit single-point lathe-cut threads on critical dynamic engine mounts and rotating hardware due to micro-notching stress concentrations. At Zunvo, every metric fastener thread (DIN 912, DIN 6921, ISO 7380) is cold-rolled under high-pressure hydraulic dies after induction heading. This cold work preserves uninterrupted grain-flow lines along the thread flanks and root radii, augmenting fatigue endurance limits by more than 35% under cyclical tensile shock.
Full REACH & RoHS Chemical Conformity
Importing fasteners into Cologne and the wider European Union mandates exhaustive compliance with EU REACH (EC 1907/2006) and RoHS directives. Our Ti-6Al-4V Grade 5 alloys, as well as our PVD color-sputtering finishes (DLC Diamond-Like Carbon, Titanium Nitride, and electro-anodizing baths), are completely free of hexavalent chromium, cadmium, lead, and SVHCs, ensuring streamlined customs processing and environmental certification for German industrial assemblers.
Baoji Manufacturing Excellence: From Raw Ingot to Precision Fastener
Headquartered in China's Titanium Valley, Zunvo integrates melt-source traceability with multi-axis automated heading, CNC contouring, and rigorous quality inspection.
Certified Aerospace Raw Stock
All fasteners originate from premium vacuum arc remelted (VAR) Ti-6Al-4V bar stock. Every mill run is verified with spectrophotometric testing for chemical stoichiometry (Al: 5.5-6.75%, V: 3.5-4.5%, Fe ≤ 0.30%, O ≤ 0.20%), supported by certified EN 10204 3.1 inspection certificates provided with each shipment.
Multi-Station Heading & CNC Milling
Our 1,000–3,000 m² facility features cold/hot multi-station heading machinery and high-speed multi-axis turn-mill machining centers. This hybrid production model provides both rapid cost-effective mass-production volumes and drawing-based customization for complex, lightweighted internal socket designs.
Tribological PVD Surface Coatings
To eliminate galling (Kaltverschweißung) and optimize the friction coefficient (µ = 0.10–0.15), we offer in-house vacuum PVD deposition including DLC (Diamond-Like Carbon), TiN Gold, Burnished Rainbow, and Anodic Oxide blues and purples for distinctive visual branding and high wear resistance.
Frequently Asked Questions by German Engineering & Sourcing Teams
Detailed technical answers addressing mechanical substitutions, tightening torques, anti-galling lubricants, and logistics into Cologne and North Rhine-Westphalia.
