Ti-6Al-4V GR5
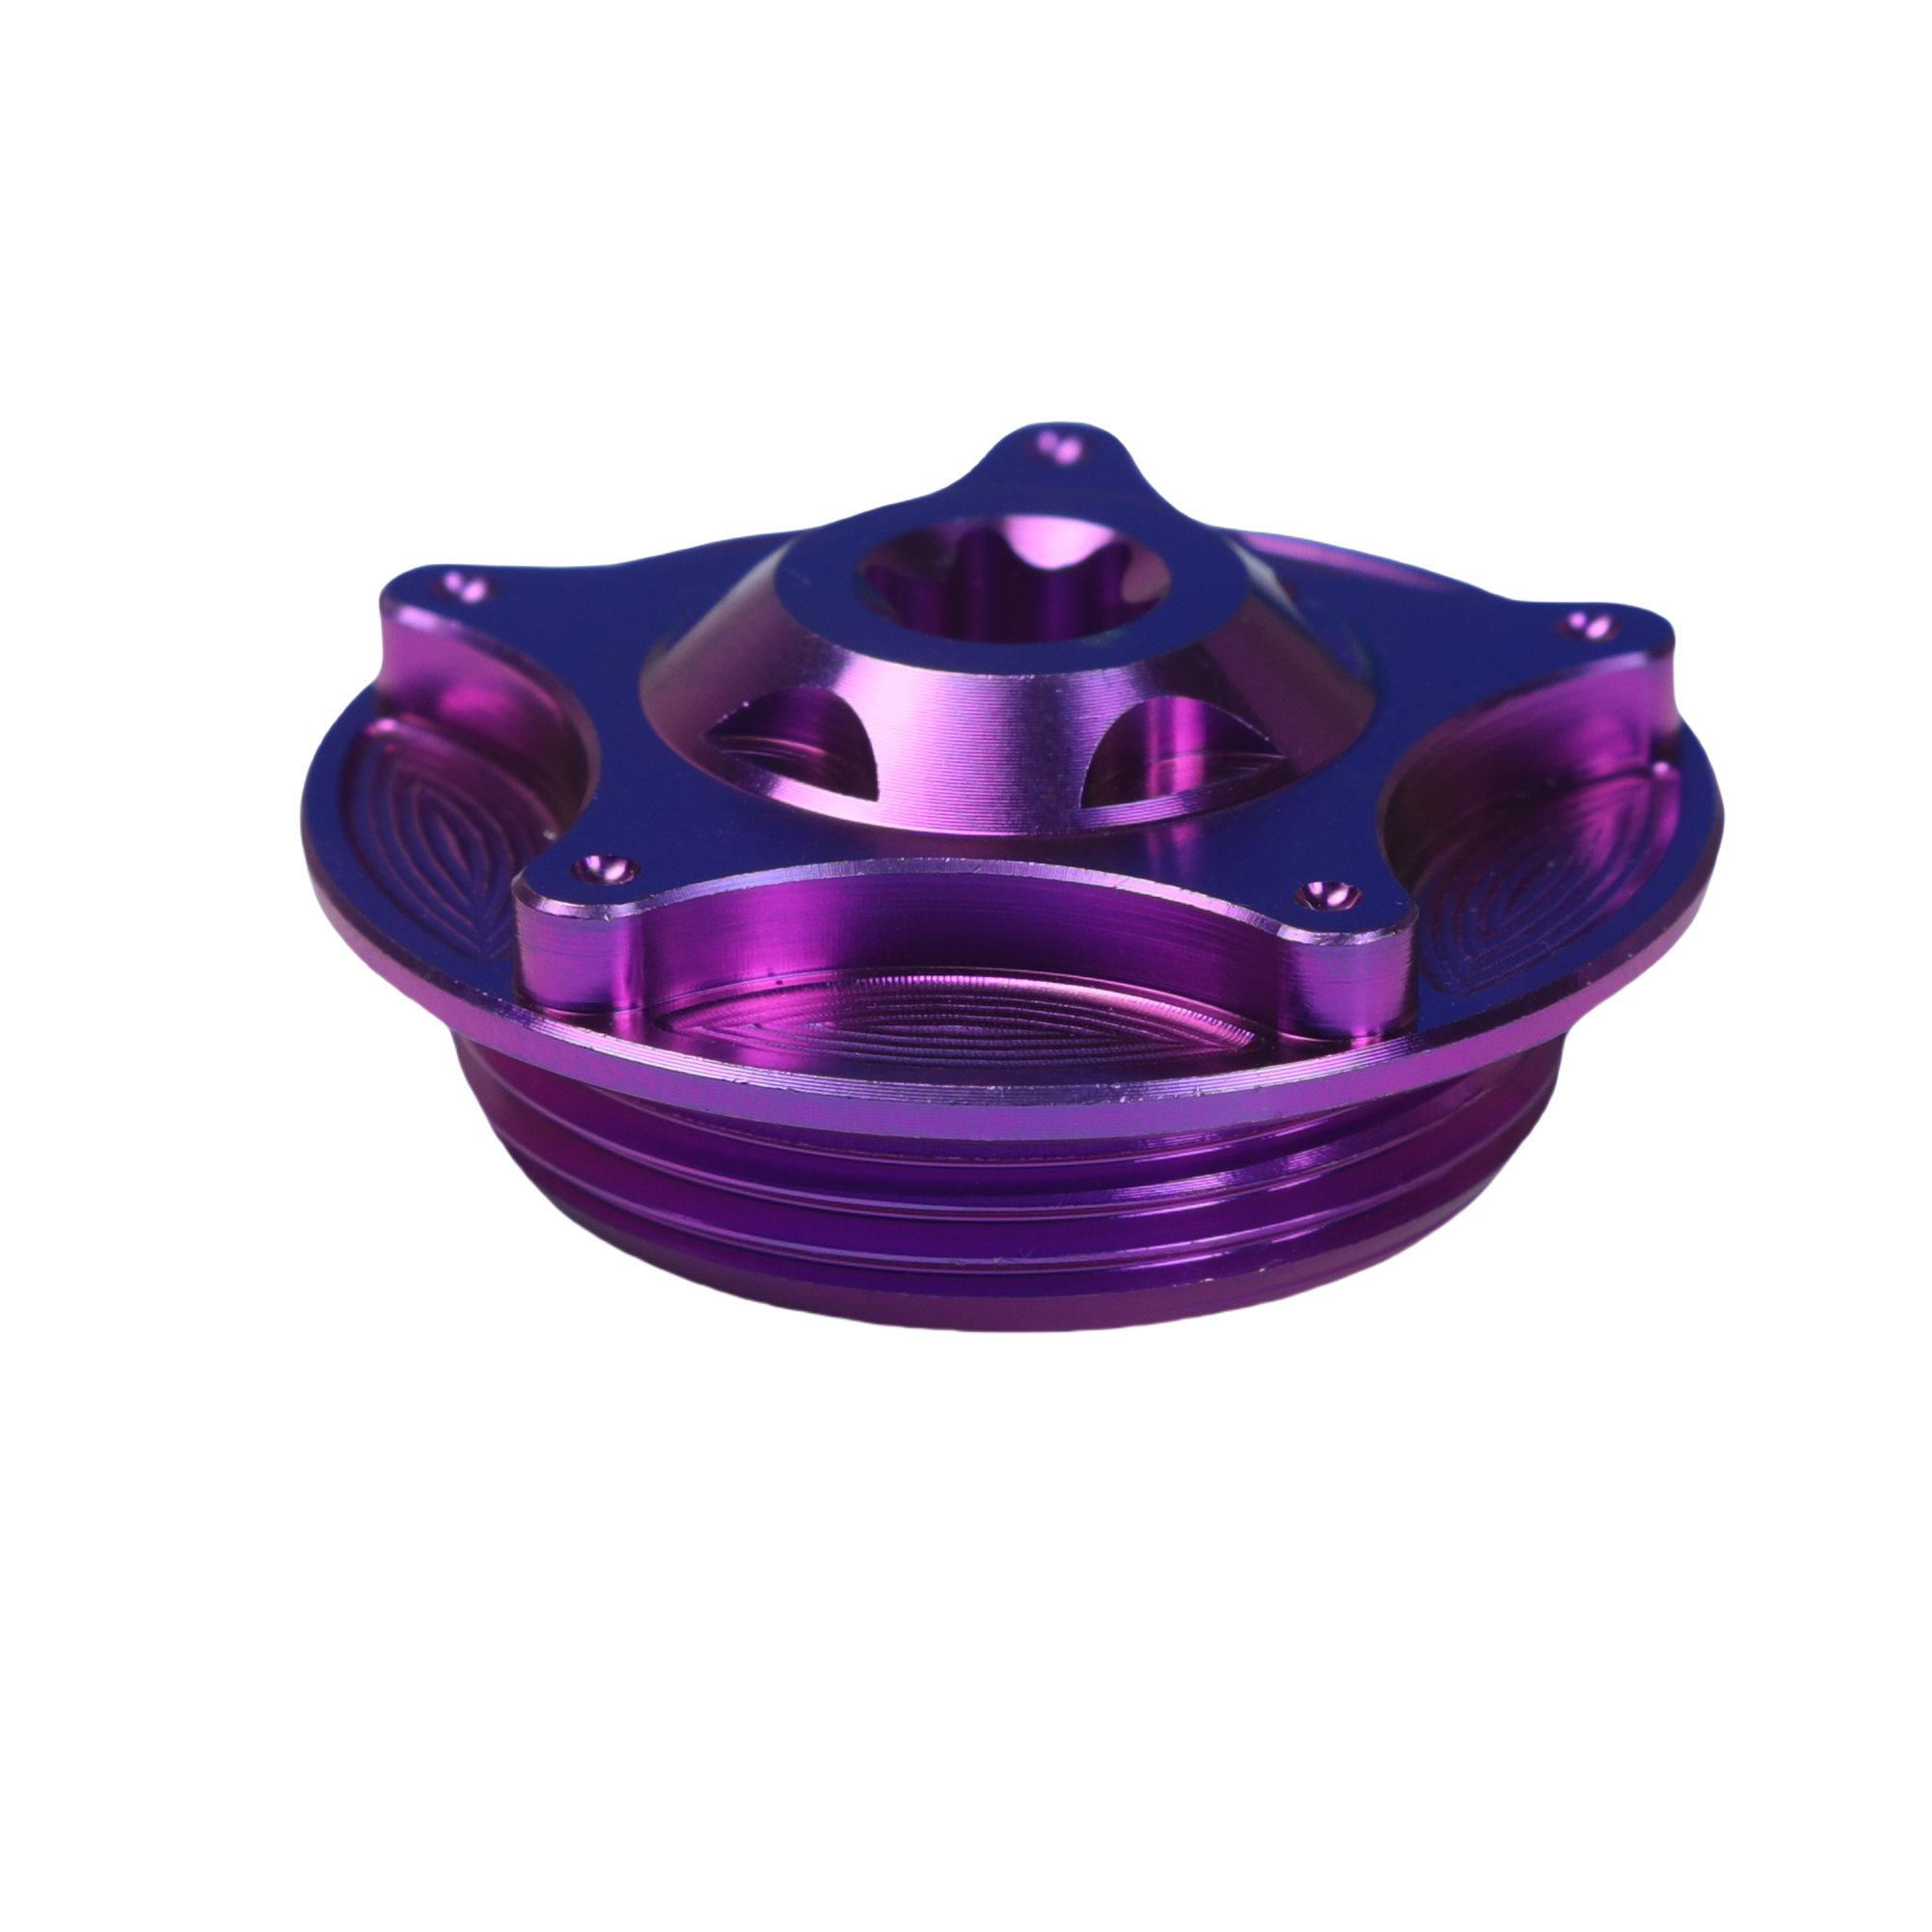
Direct factory supply manufactured to exceed JIS B 1051 Class 10.9 structural load parameters. Precision cold-worked, CNC profile-milled, and multi-stage anodized for extreme operating environments.
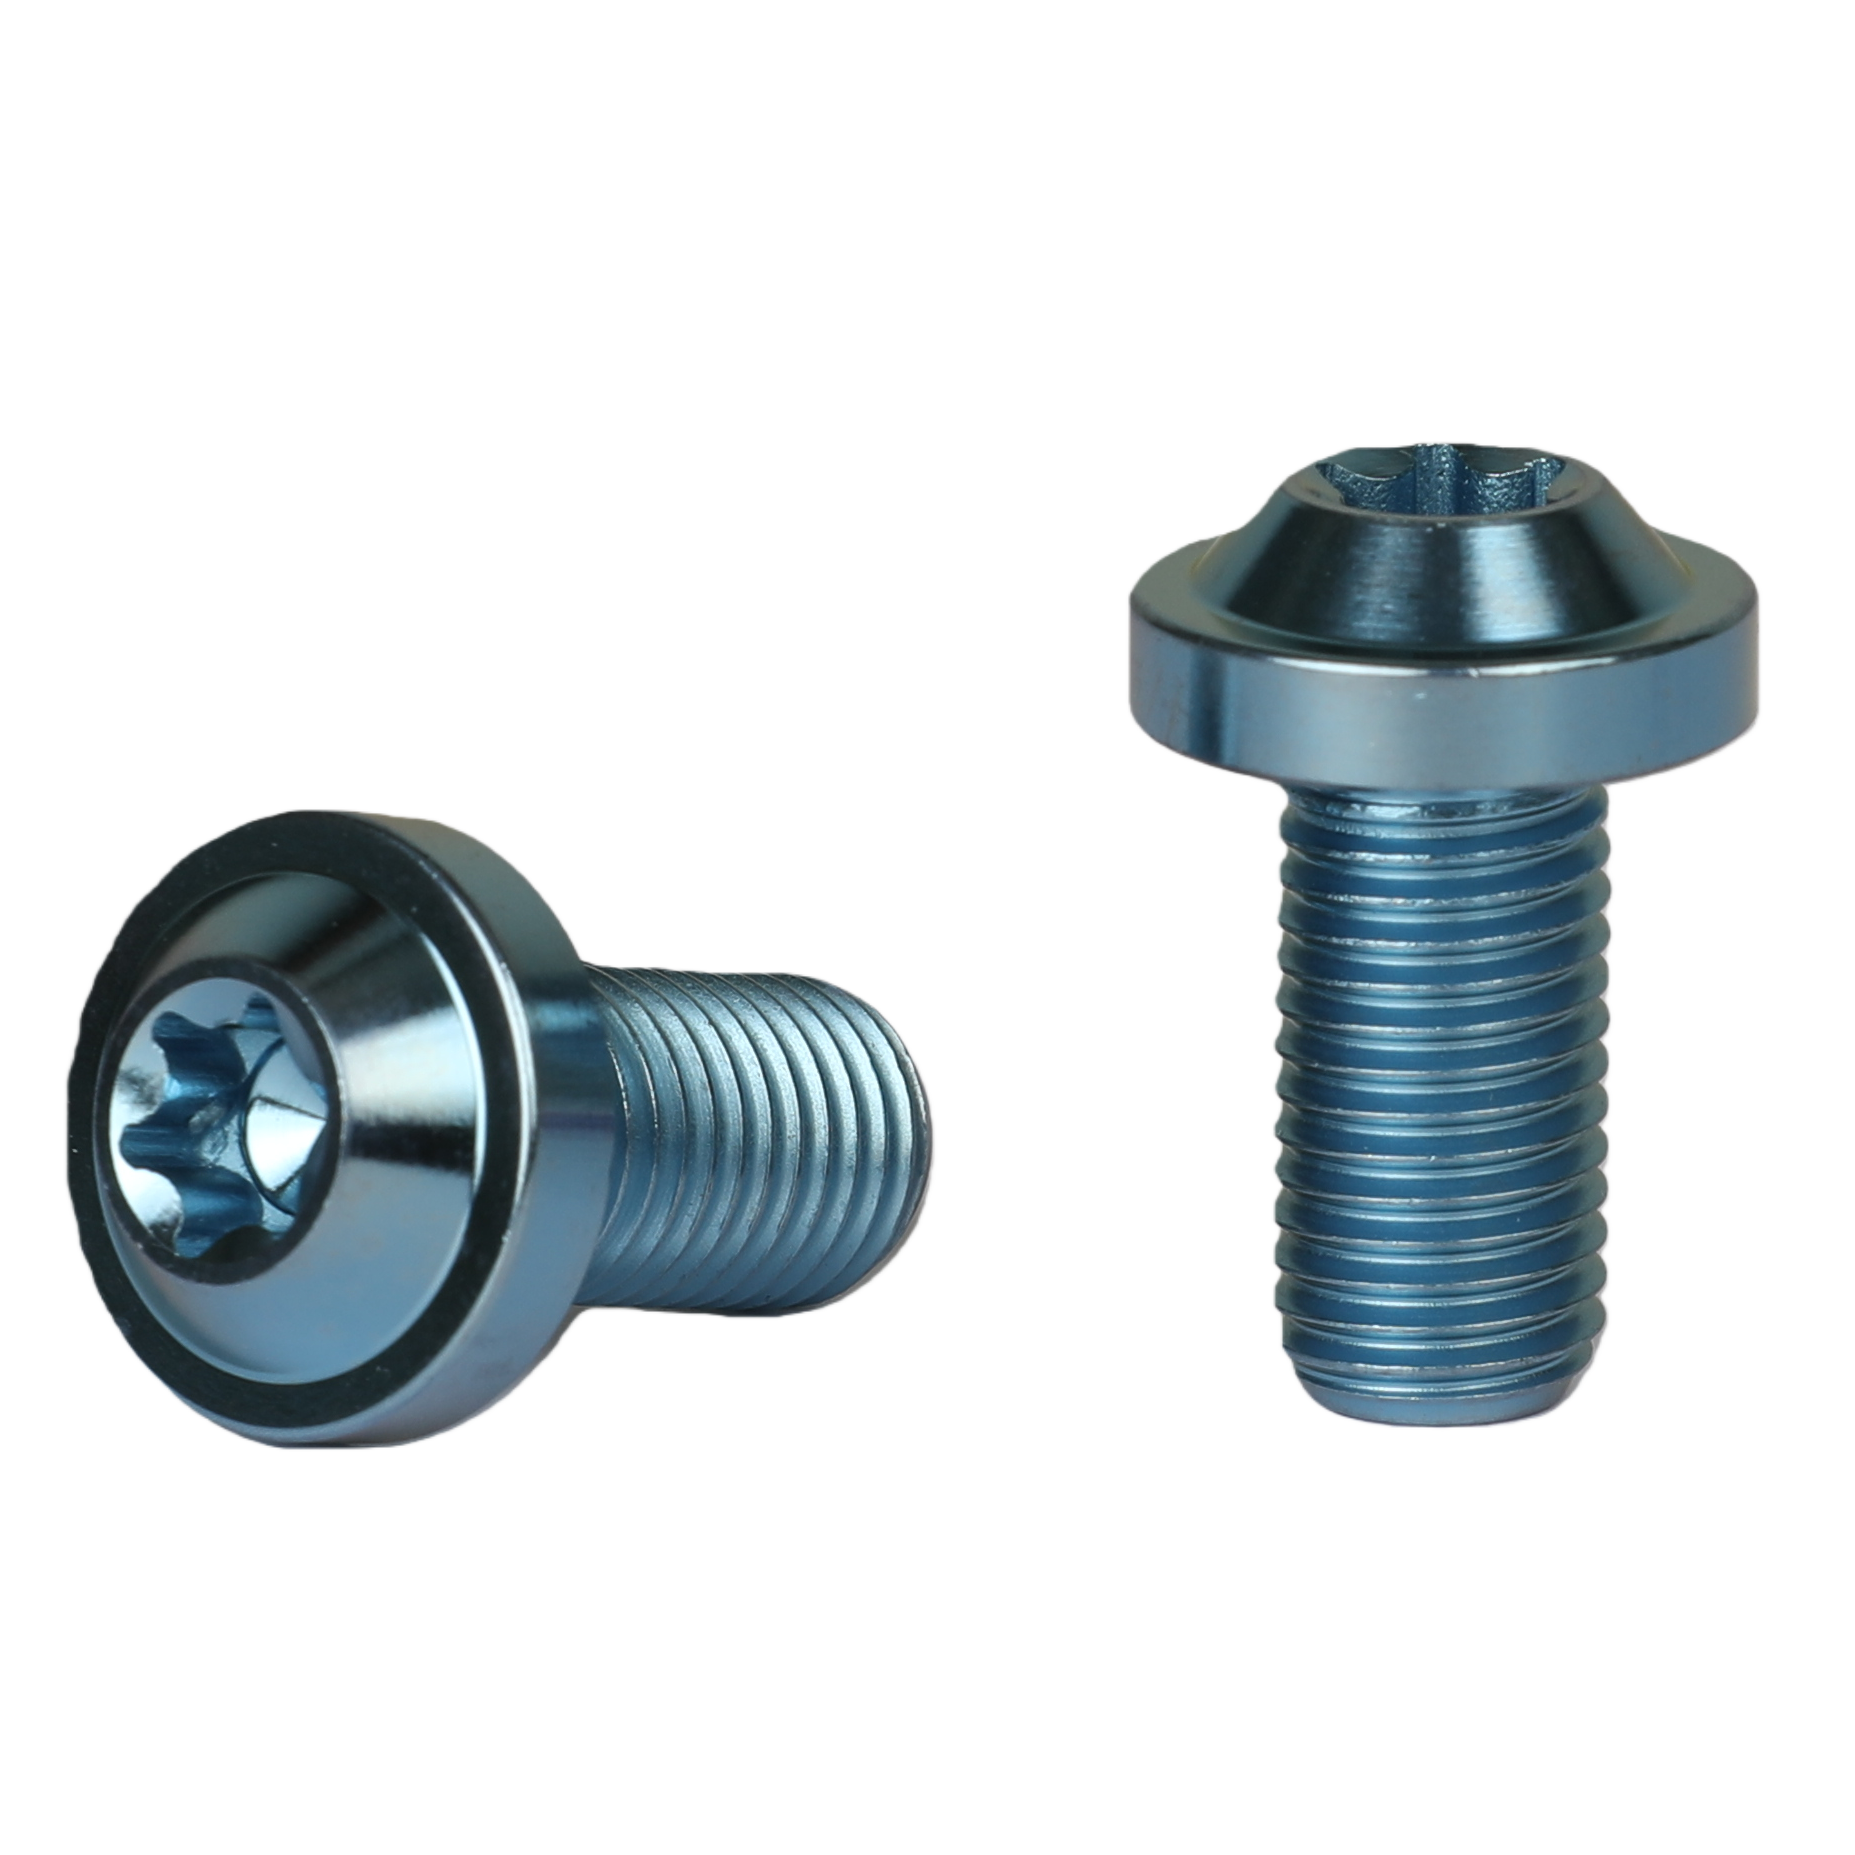
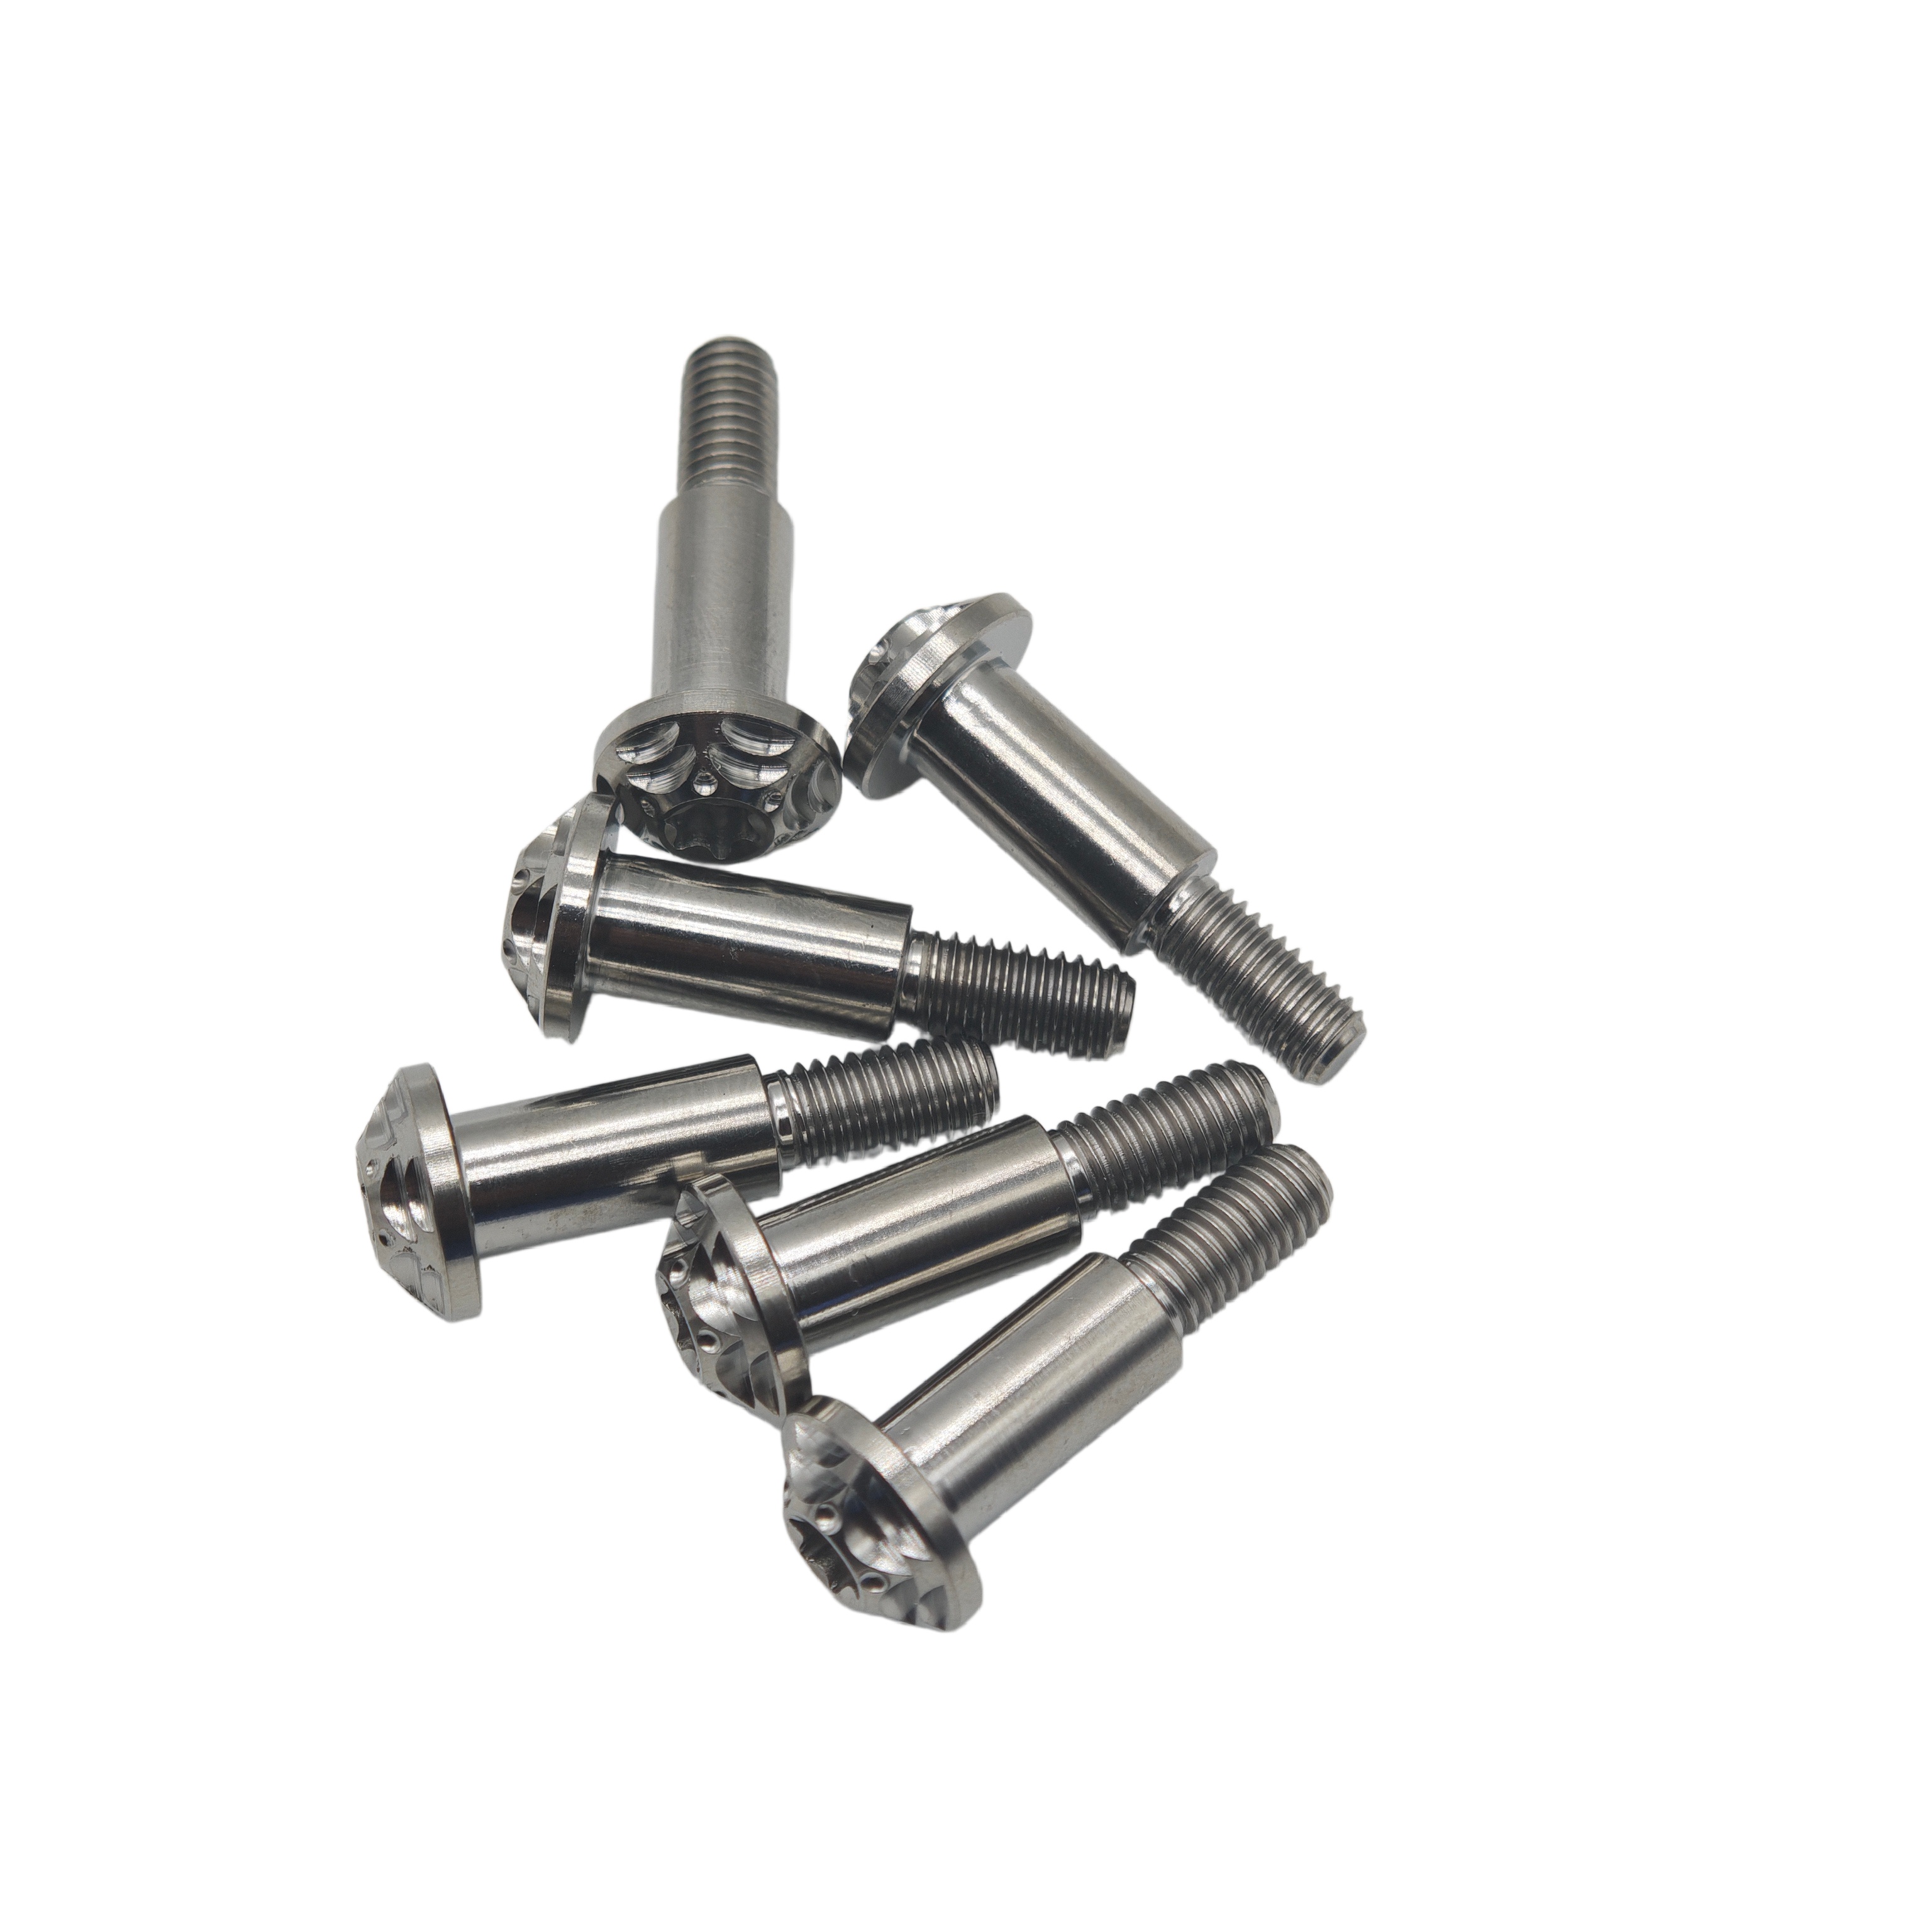
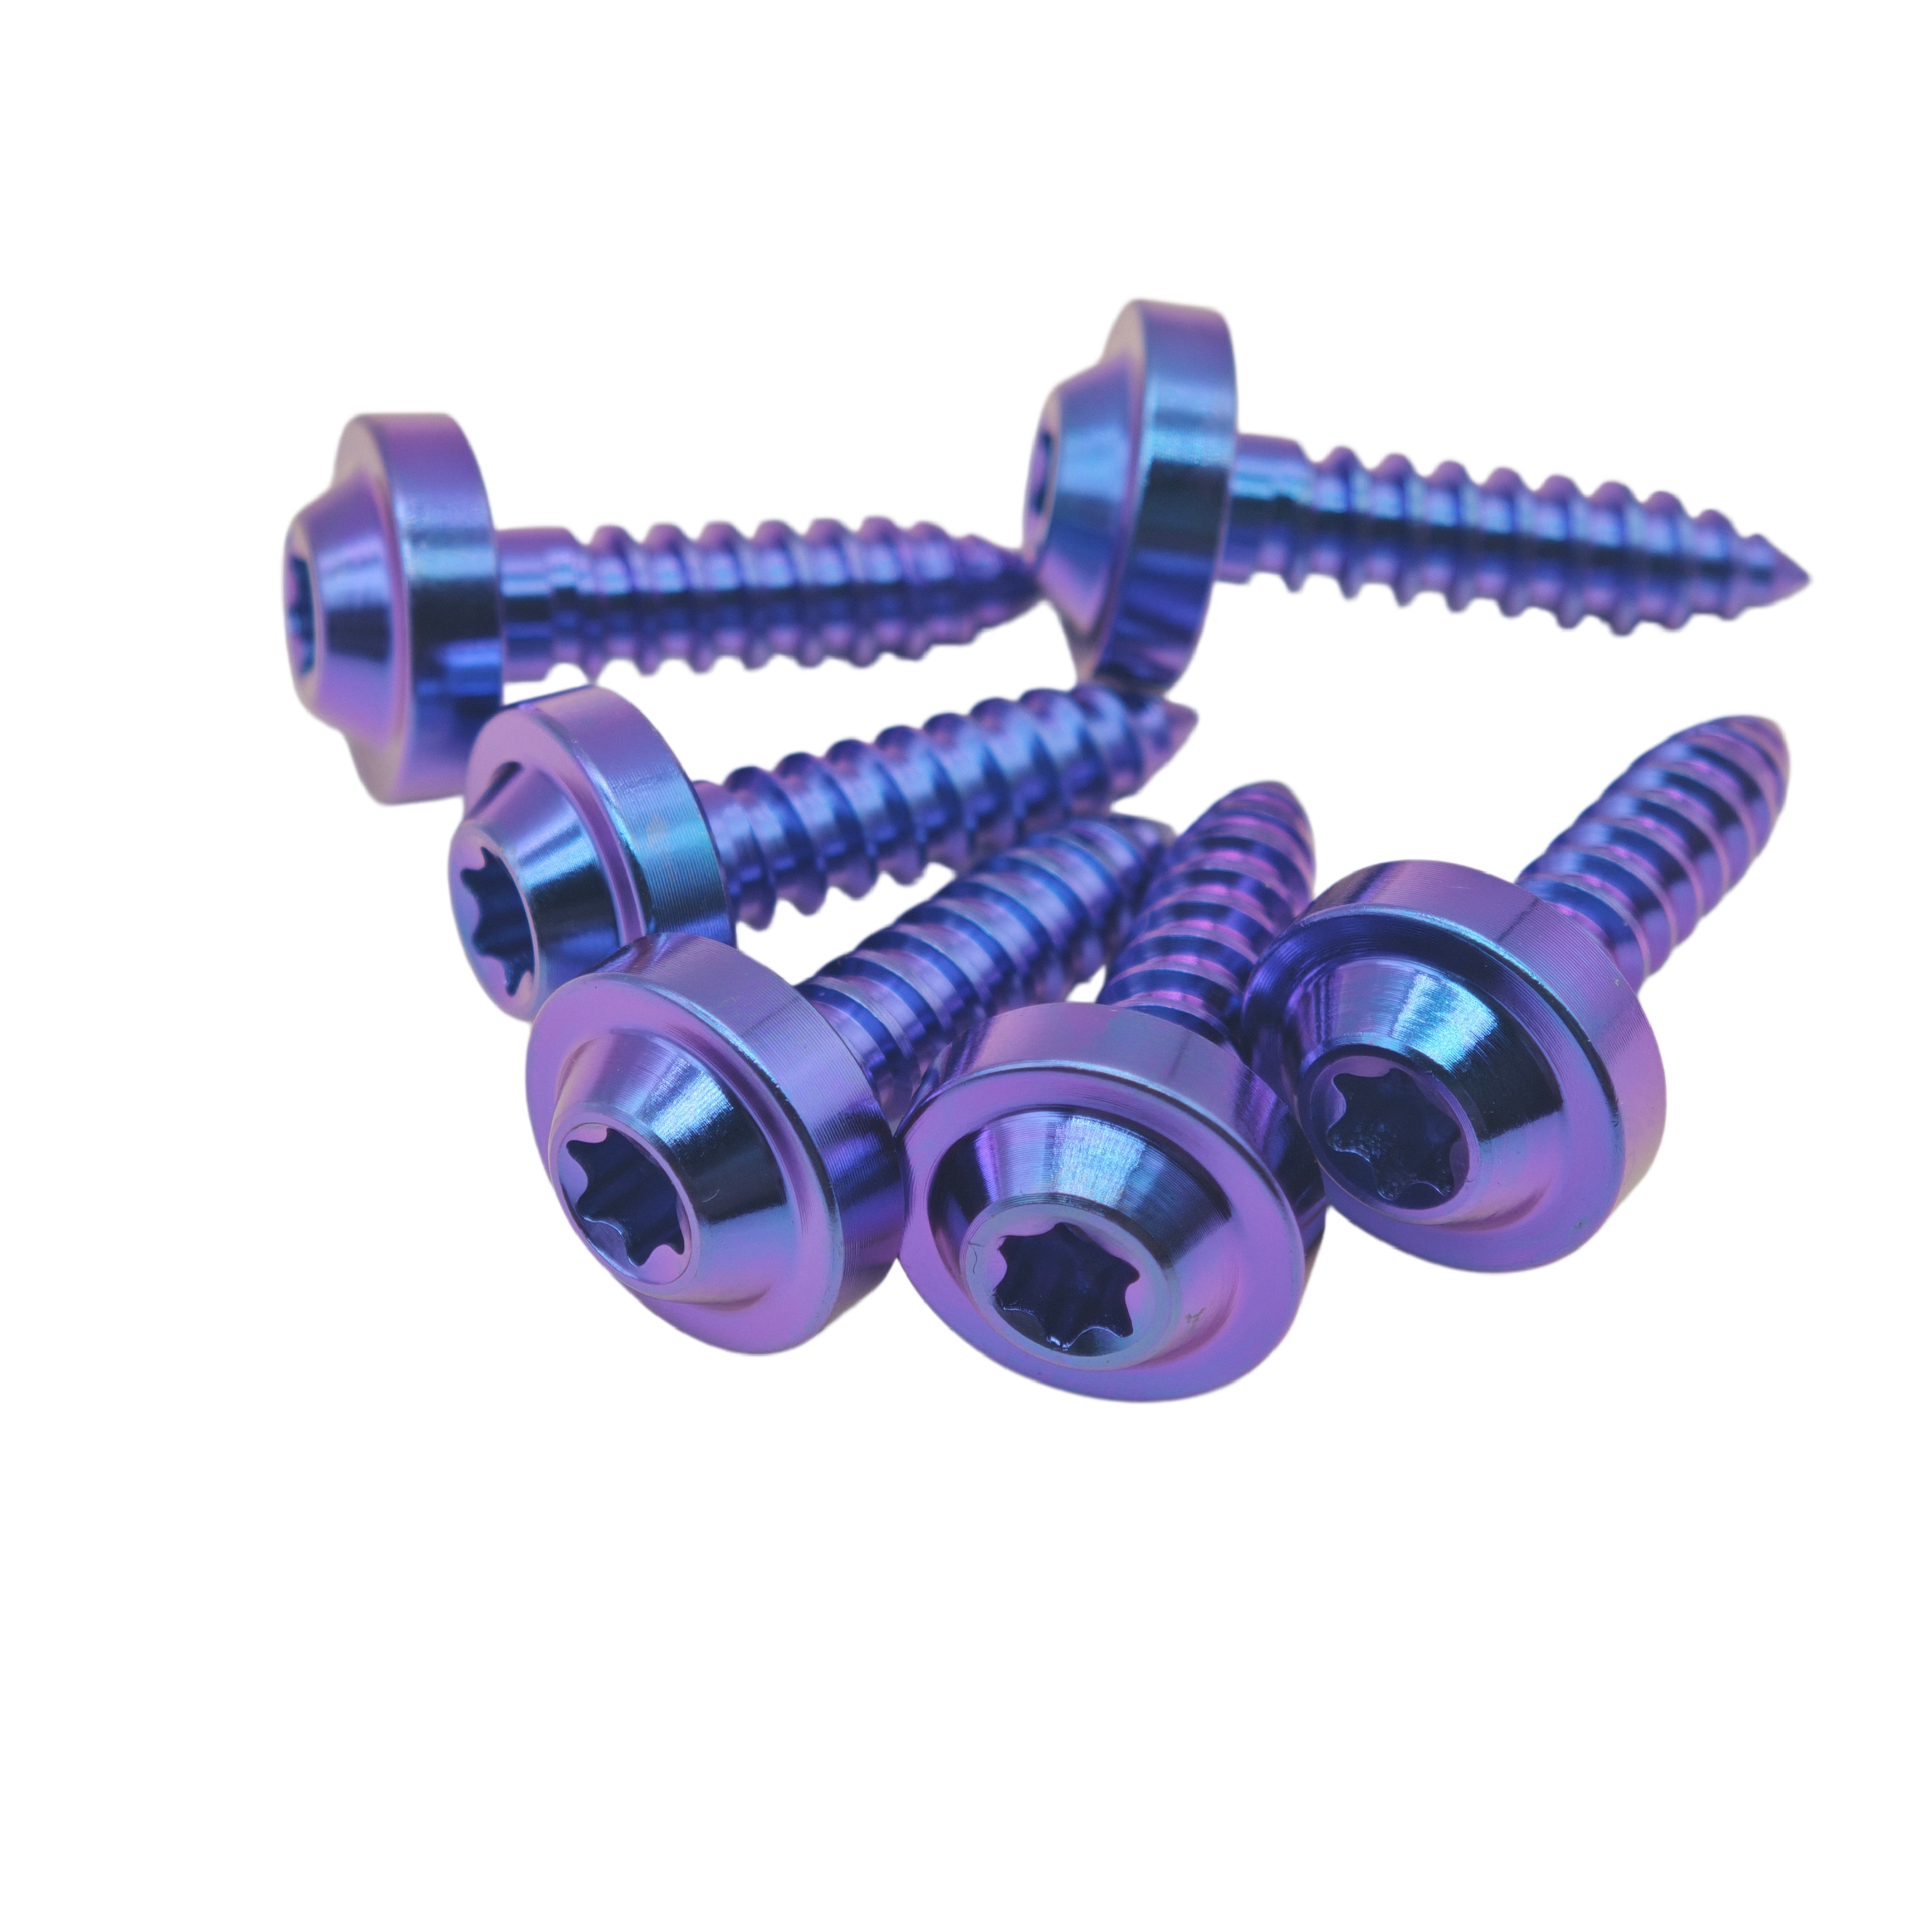
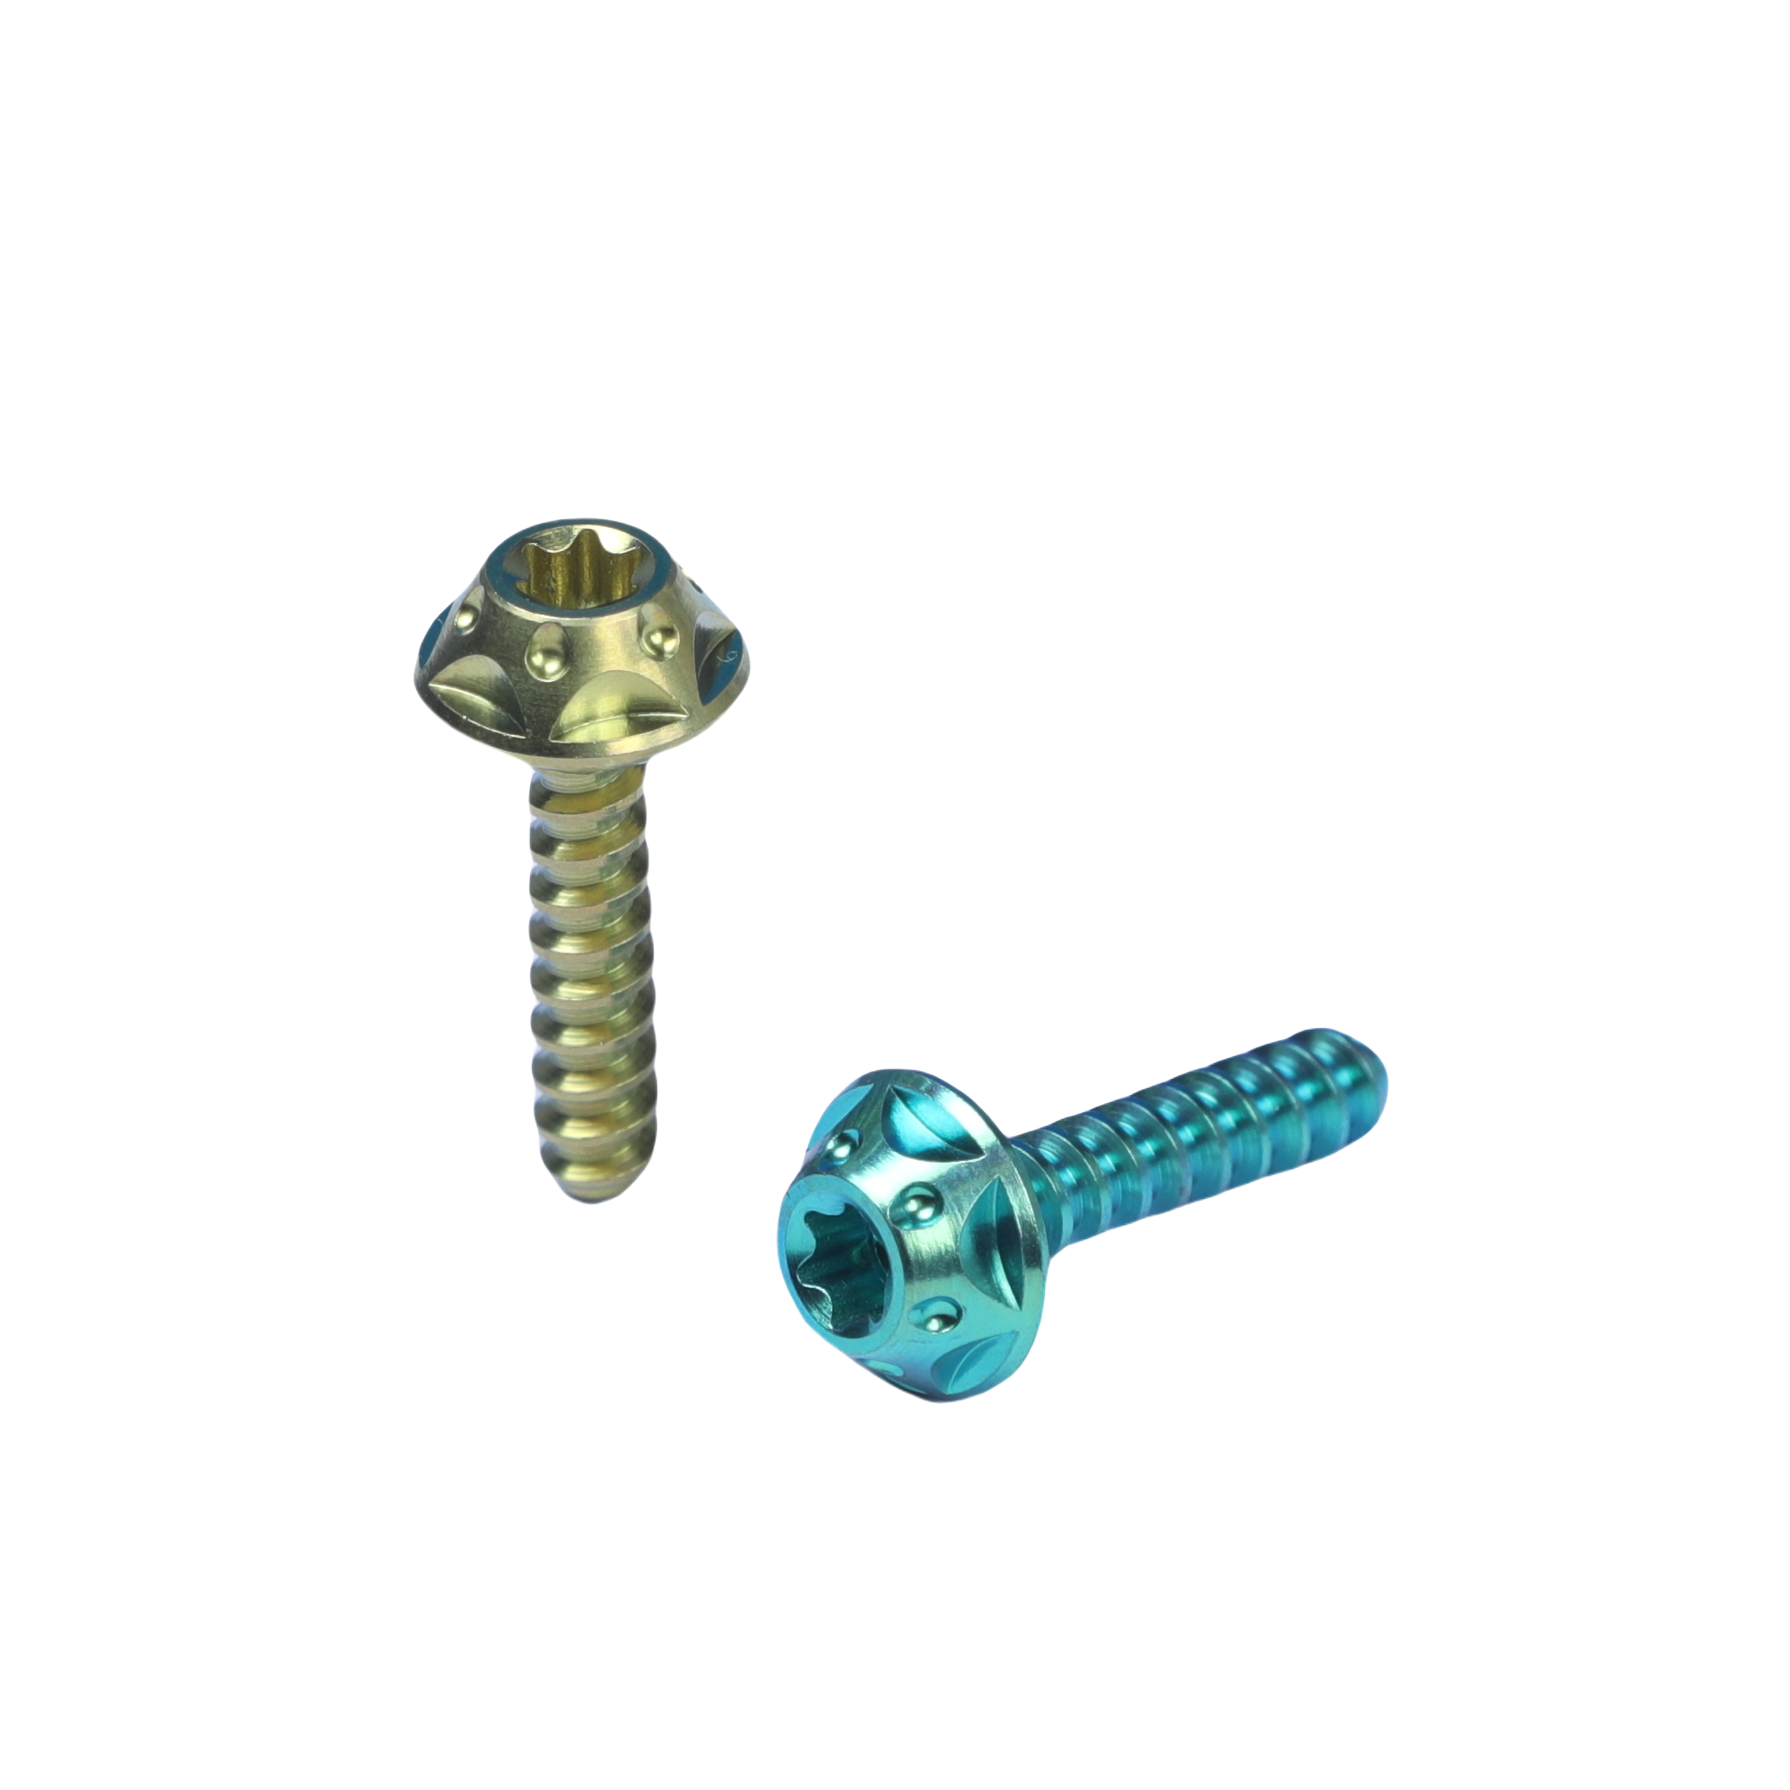
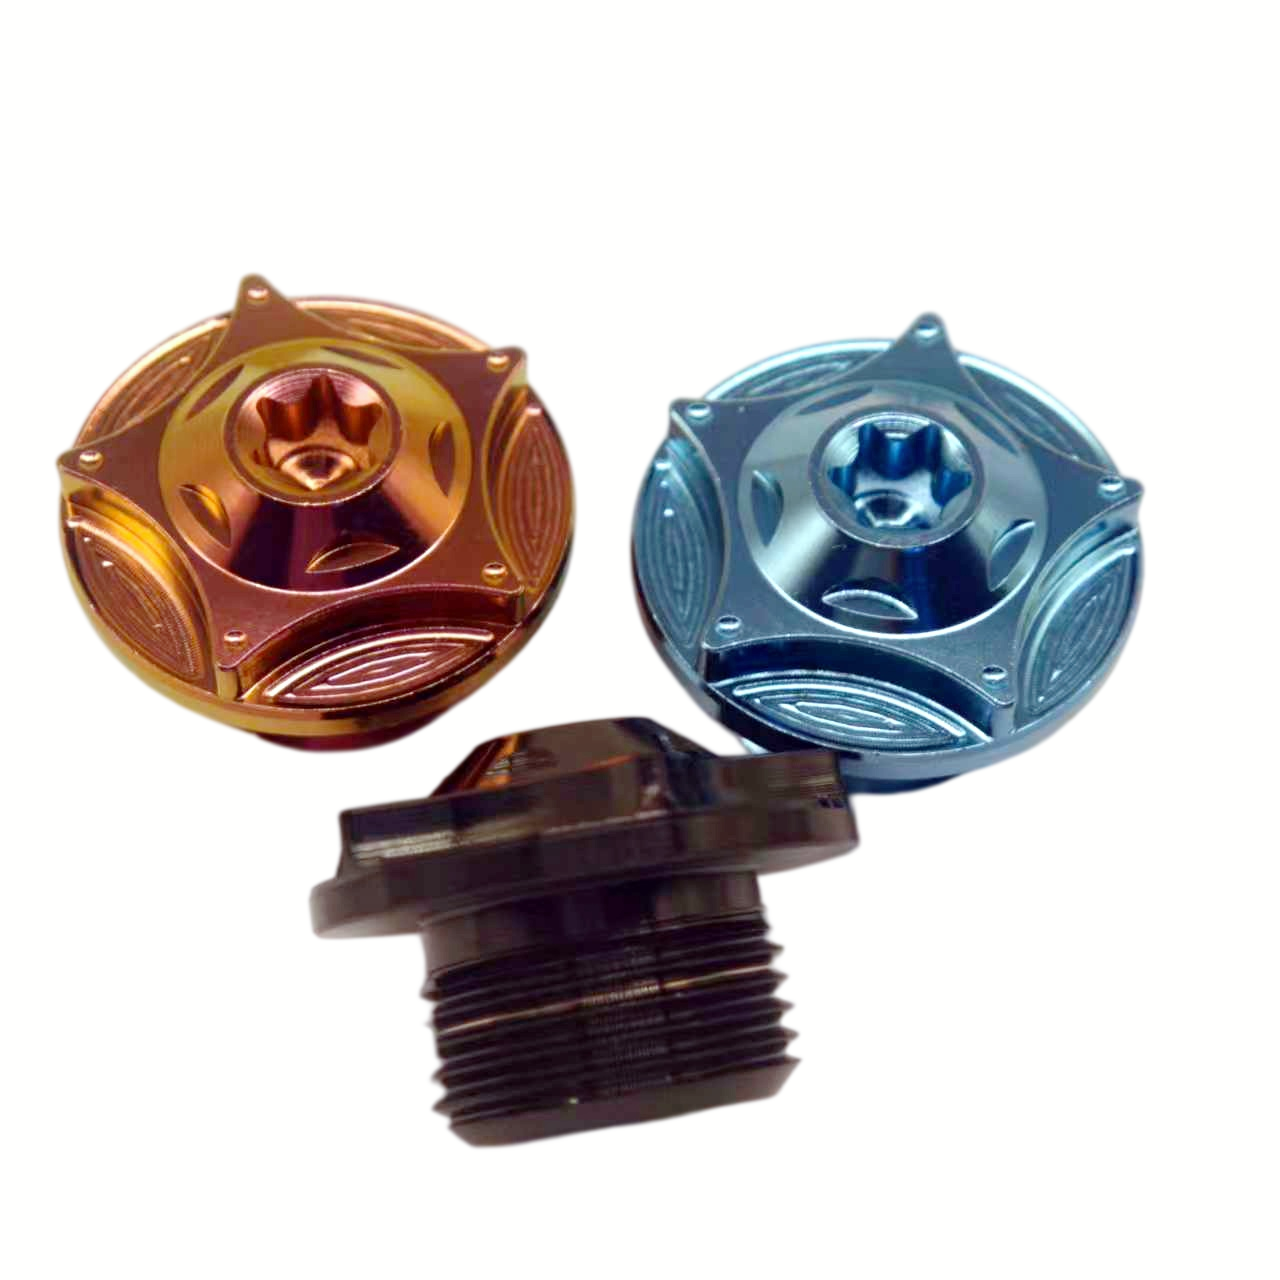
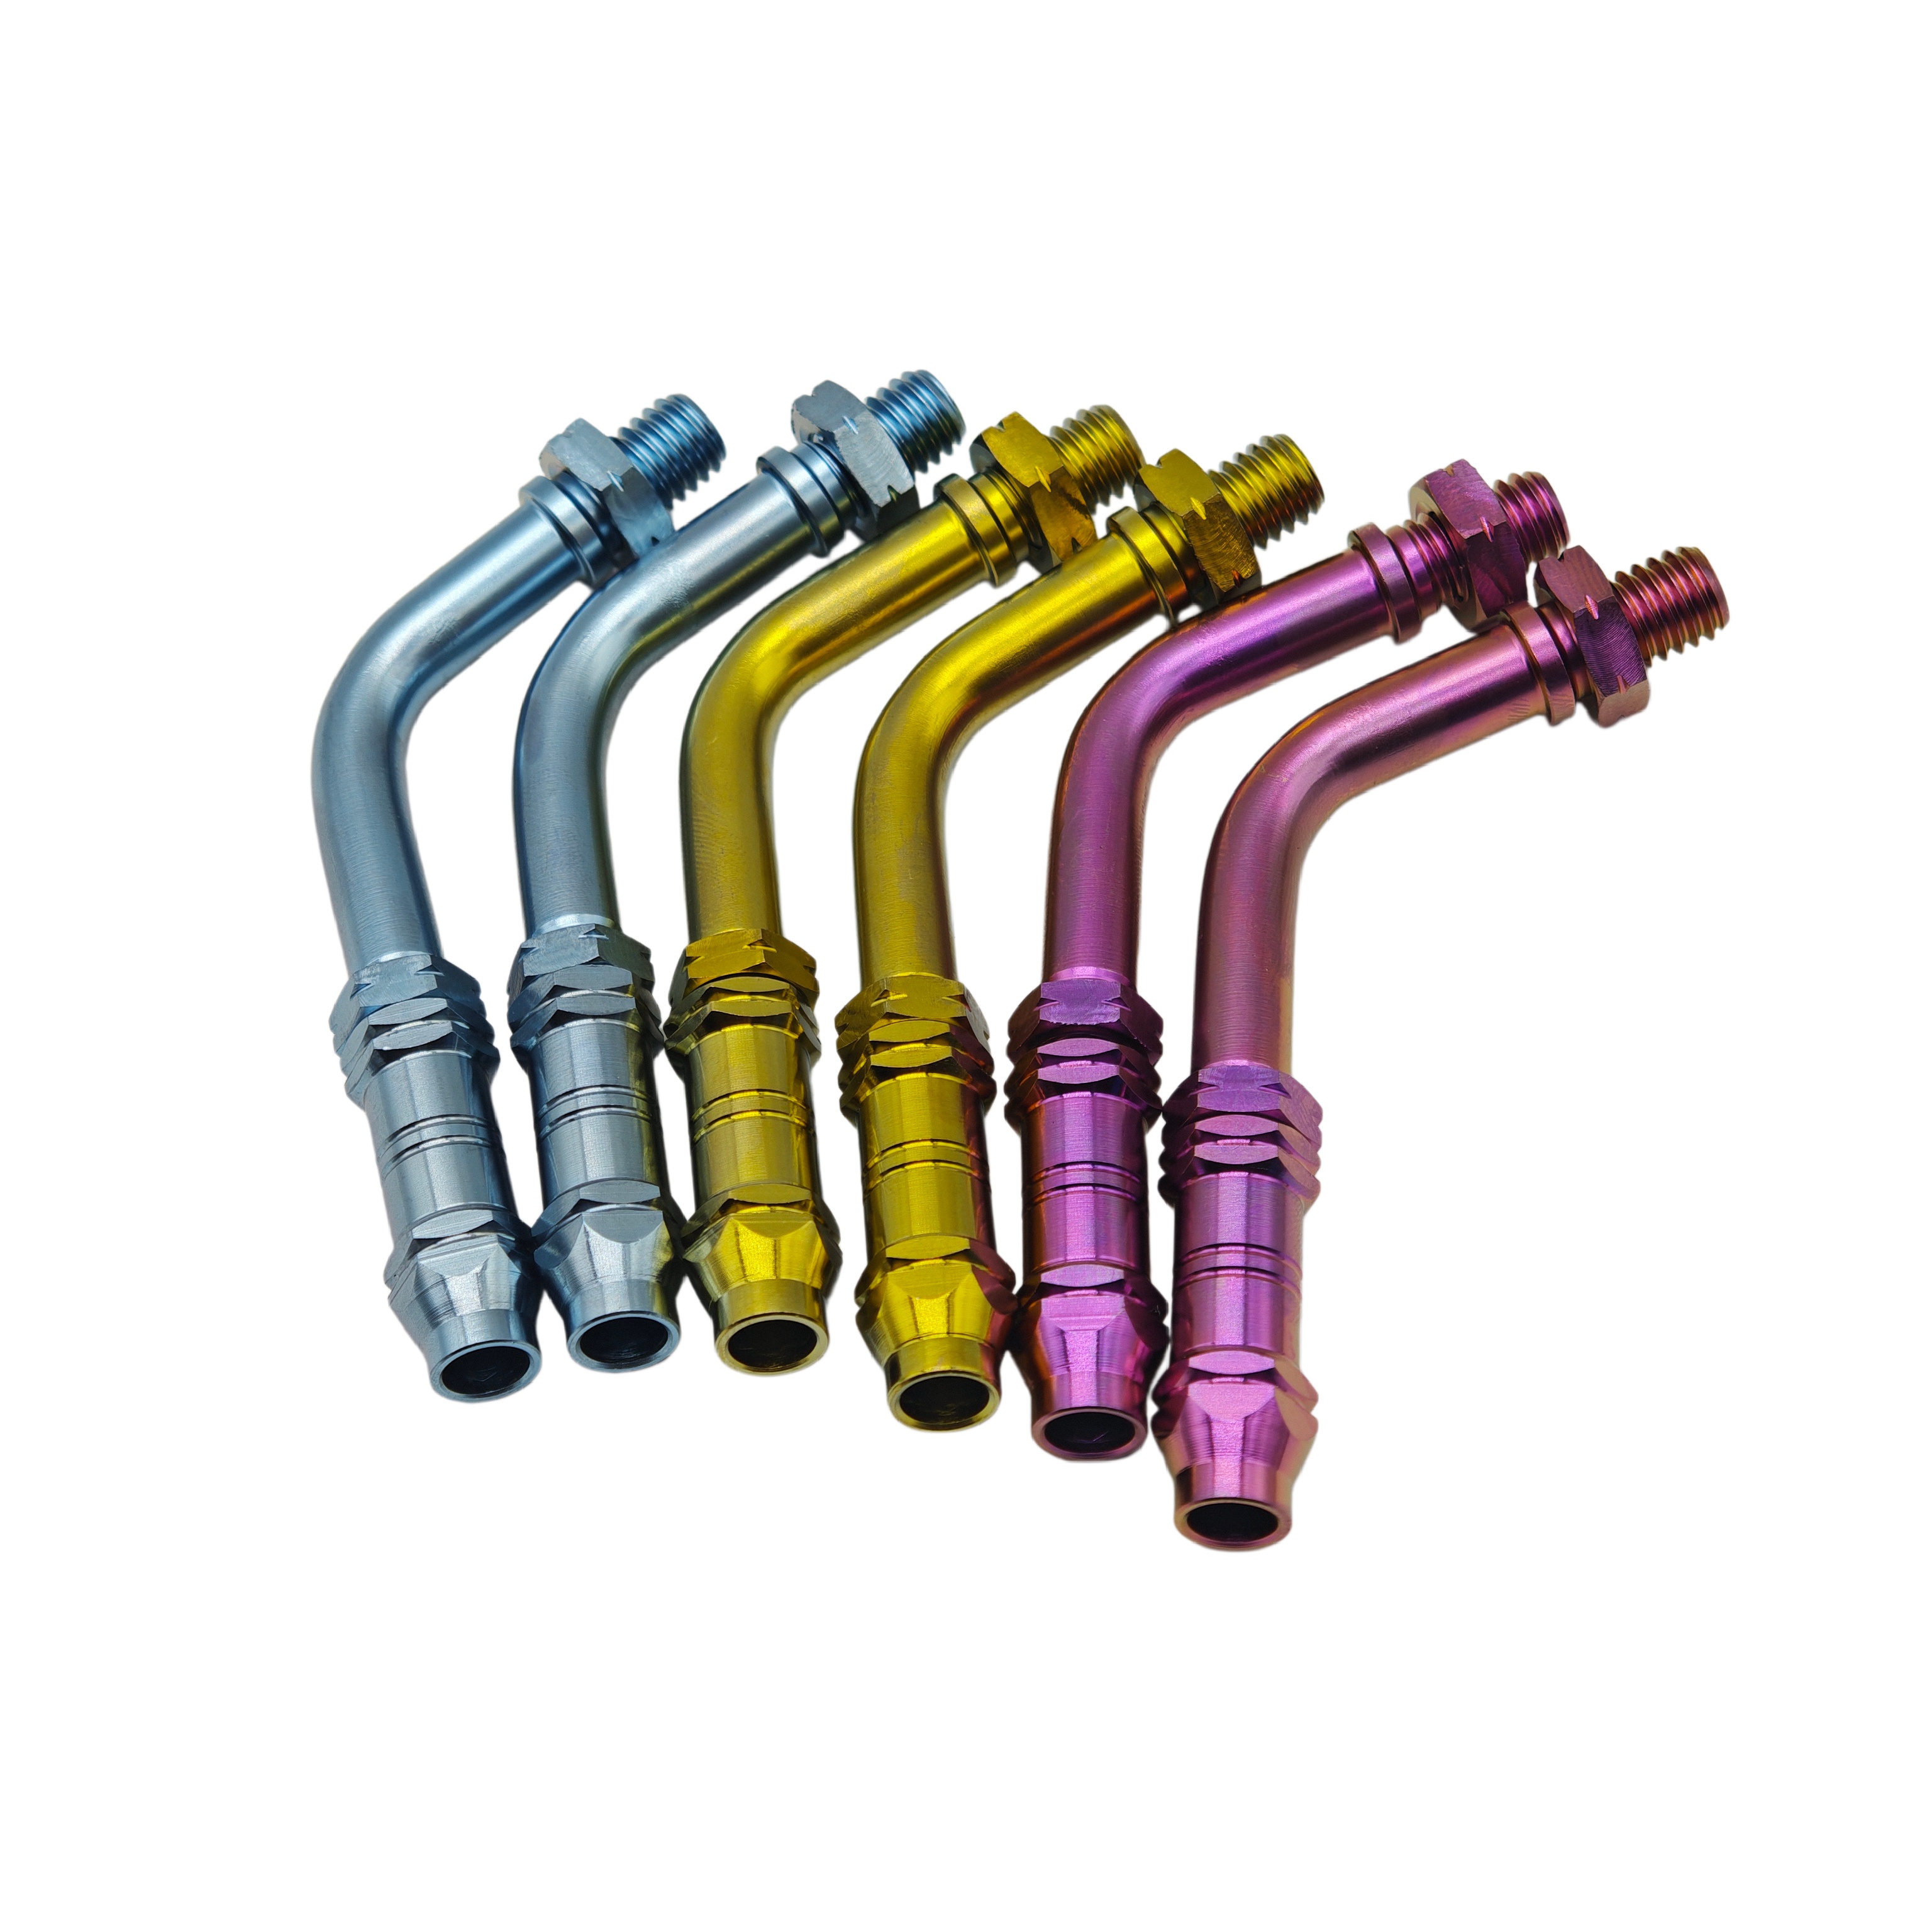
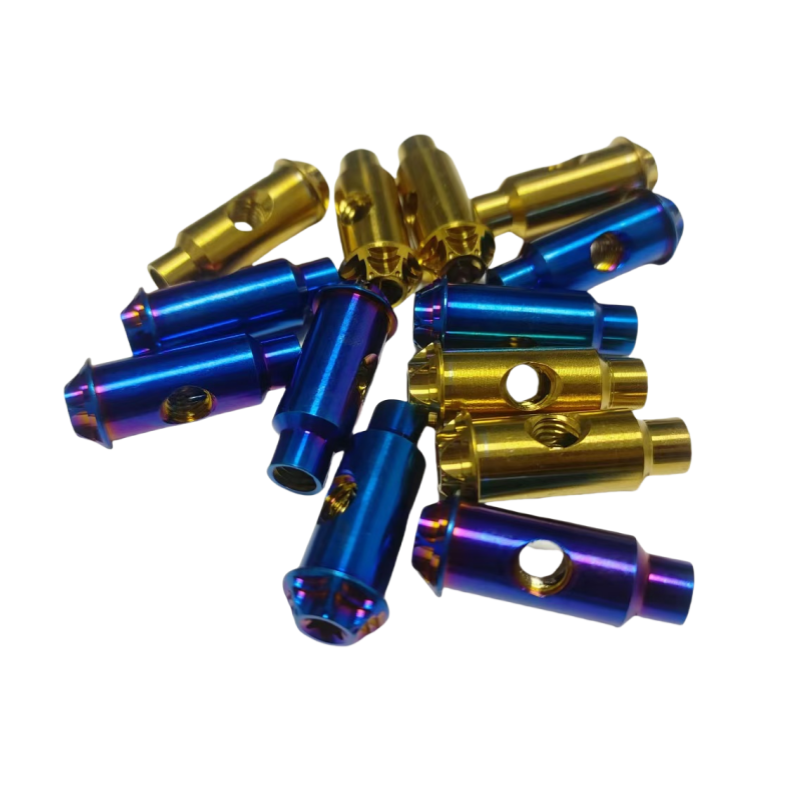
The operational taxonomy of motorcycle performance in the Tokyo metropolitan biome presents extreme metallurgical challenges rarely encountered in conventional transit corridors. Urban density along the Shuto Expressway (首都高速道路), combined with rapid temperature deltas encountered when transiting the mountain switchbacks of Okutama (奥多摩) and Hakone (箱根), demands an uncompromising baseline in structural hardware. For race operations competing at Tsukuba Circuit (筑波サーキット) or staging track-day endurance trials, un-sprung mass minimization is not merely an aesthetic preference—it is a critical determinant of gyro-rotational acceleration, yaw damping rates, and brake thermal management.
As premier CNC motorcycle bolt kit manufacturers serving the Tokyo market, we configure every fastening kit to eliminate parasitic weight without forfeiting pre-load stability. Fastening points across the brake caliper radial mounts, rotor disc carriers, swingarm pivot anchors, and crankcase perimeters bear the brunt of micro-vibrational shear stresses. Conventional chromium-molybdenum steel fasteners carry a substantial weight penalty (density ~7.85 g/cm³), while non-structural 7000-series aluminum alloys lack the cyclical yield endurance necessary for sustained thermal shock resistance. Our aerospace-grade Ti-6Al-4V Grade 5 Titanium bridges this mechanical gulf—delivering a tensile strength ceiling above 895 MPa at an aggregate density of merely 4.43 g/cm³, which yields an immediate 44% un-sprung mass reduction across dynamic suspension assemblies.
Un-sprung mass at the wheel hubs directly inhibits the gyroscope precessional response of supersport machines. Implementing our GRX M8x24 pan-head brake rotor screws and hollow-core axle nuts drops rotating inertia significantly, sharpening turn-in compliance through Tsukuba's technical hairpins.
Motorcycles navigating the Tokyo Bay shorelines, Aqua-Line tunnels, and Yokohama docks encounter high-humidity air laden with marine salts. Titanium forms an instantaneous, passive titanium dioxide (TiO2) oxide film that resists pitting, stress cracking, and atmospheric galvanic erosion completely.
In hotbeds of bespoke bike building like Sumida and Ota wards, builder communities re-engineering classic Japanese multi-cylinder powerhouses (CB750, Z1) require exact replica dimensions mated to modern mechanical tolerances with custom non-cam-out Torx and socket heads.
A quantifiable operational benchmark verifying why Grade 5 Titanium serves as the preferred structural baseline over legacy alloy steel and lightweight aluminum alternatives.
| Evaluation Parameter | Zunvo Gr5 Ti-6Al-4V | Class 10.9 Carbon Steel | SUS304 Stainless | 7075-T6 Billet Aluminum |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 (Optimized) | 7.85 | 7.93 | 2.81 |
| Tensile Yield Strength (MPa) | ≥ 895 - 950 | 940 - 1040 | 205 - 240 | 460 - 505 |
| Strength-to-Weight Ratio (kN·m/kg) | 202 (Industry Leader) | 120 | 63 | 180 |
| Thermal Expansion Coeff. (10⁻⁶/K) | 8.6 (Low Expansion) | 11.7 | 17.3 | 23.4 |
| Marine Salt Spray Resistance | >1000h (Zero Pitting) | <48h (Corrosion Failure) | 120h (Surface Pitting) | 96h (Anodize Blistering) |
| Torque Relaxation / Galling Risk | Zero (with Anti-Seize) | Low | Extremely High | Severe Shear Risk |
The specialized components trade across the Kanto plain is experiencing a transformative structural shift. As observed across Tokyo's specialist engineering sectors in Koto, Adachi, and Kanagawa's Ota-adjacent manufacturing belts, professional maintenance facilities and tuning divisions are transitioning away from fragmented distribution middle-tiers. Several macroeconomic drivers define this evolution:
1. Shifting Toward Complete Vehicle-Specific Bolt Kits: Individual screw sourcing is increasingly considered operationally inefficient. Tuners servicing machines like the Yamaha YZF-R1M, Kawasaki Ninja H2, Honda CBR1000RR-R, and Suzuki Hayabusa require complete engine casing kits, subframe packages, or full caliper assemblies packaged with precise torque mapping sheets. Unified packaging mitigates assembly floor delays and eliminates pitch-mismatch hazards.
2. Tightened Verification of Raw Material Chemistry: The proliferation of low-purity Grade 2 commercially pure titanium masquerading as structural Grade 5 fasteners has caused critical joint failures in high-shear environments. Tokyo mechanical engineers now enforce strict verification mandates requiring optical emission spectrometry (OES) certifications, mill test certificates (MTC) tied to raw billet heat numbers, and independent eddy-current crack detection.
3. Advanced Functional Surface Finishing over Pure Optics: While multi-spectrum anodization (Burnt Rainbow, Electric Blue, Gold) continues to serve a robust aftermarket aesthetic role, track teams and engineering developers increasingly specify physical vapor deposition (PVD) titanium carbo-nitride (TiCN) or diamond-like carbon (DLC) finishes. These atomic coatings deliver ultra-high surface hardness (HV >2500) and an exceptionally low friction coefficient, preventing thread galling during rapid wheel changes in endurance pit-lanes.
Founded in 2015 within Baoji—the recognized "Titanium Valley" producing the vast majority of China's structural refractory metals—Zunvo sources directly from adjacent primary smelting operations, securing guaranteed titanium purity with fully traceable heat lot numbers.
Equipped with high-precision multi-axis sliding-head automatic lathes, thread-rolling machines, and optical profile sorting projectors. We execute intricate geometries—from 90-degree internal cable passes to weight-reducing hollow-flange profiles—within ±0.005mm tolerances.
Every production lot undergoes rigorous multi-point verification: thread go/no-go ring testing, Rockwell/Vickers hardness validation, optical comparator checking for root radius fatigue conformity, and coordinate measuring machine (CMM) dimensional verification before dispatch.
Clear, unvarnished metallurgical and logistics guidance for workshop directors, procurement leads, and performance specialists.
Our Grade 5 (Ti-6Al-4V) titanium fasteners deliver an ultimate tensile strength exceeding 895-950 MPa with a yield strength baseline of 825 MPa. This places them on par with ISO/JIS Class 8.8 to 10.9 automotive steel fasteners under dynamic vibration loads, but with a 44% mass reduction. For critical rotational and braking mountings, our threads are formed via high-pressure hydraulic thread-rolling dies rather than single-point cutting. This creates continuous grain-flow along the thread root, substantially boosting shear resistance and cyclical fatigue limits beyond cut threads.
Titanium possesses a notable affinity for friction welding against stainless steel or bare aluminum under extreme torque pressures—a phenomenon known as cold galling. We mitigate this through micro-finished thread surfaces and precision Class 6g/6H pitch cut tolerances. For installation, we mandate the application of a high-load anti-seize paste (such as copper, molybdenum disulfide, or nickel-based assembly paste) to the threads. Furthermore, because titanium exhibits a modulus of elasticity approximately half that of carbon steel (~114 GPa vs ~210 GPa), torque ratings should generally be adjusted by 10% to 15% below standard dry steel torque tables unless a specific wet torque rating is established.
Catalog items and standard model bolt kits maintained in inventory dispatch within 24 to 48 hours of order confirmation. For custom CNC prototype runs configured from CAD drawings (STEP, IGES, DXF) or OEM samples provided by Tokyo workshops, physical evaluation samples are completed within 3 to 5 business days. Mass CNC production batches typically require 7 to 15 working days depending on surface treatments (PVD vs. micro-arc oxidation). Express air-freight logistics via DHL, FedEx, or SF Express ensures direct delivery to Tokyo locations (Haneda/Narita clearing channels) within 2 to 4 transit days.
Yes. Beyond standard multi-color voltage-controlled anodization (Purple, Blue, Gold, Rose, Burnt Rainbow), we specialize in high-adhesion Physical Vapor Deposition (PVD). PVD coatings yield hard ceramic surfaces such as Titanium Nitride (TiN, brilliant gold), Titanium Carbo-Nitride (TiCN, slate grey/bronze), and Diamond-Like Carbon (DLC, rich tactical black). These coatings resist thermal decay up to 600°C and are completely unaffected by calcium chloride winter road de-icers, industrial detergents, and abrasive brake particulate.
We operate full OEM/ODM private-label packaging programs for motorcycle shops, distribution chains, and performance teams across Japan. Our multi-axis fiber-laser engraving suites can apply custom brand logos, batch tracking codes, and torque specifications directly onto bolt heads or washer collars. Packaging configurations range from bulk workshop-pack bags to custom blister packs, compartmentalized blister trays, and branded cardboard boxes customized to your operational branding guidelines.
Whether you require a complete CNC motorcycle bolt kit replacement program for Japanese superbikes, bespoke prototypes based on 3D CAD models, or containerized wholesale supply directly to Tokyo, our engineers provide complete manufacturability feedback and transparent factory-direct pricing within 7 hours.
