≥895 MPa
Tensile Yield Strength (Gr5)
±0.005 mm
Precision CNC Tolerance Control
44%
Mass Reduction vs Steel SCM435
100%
Heat-Lot Mill Cert & Thread Testing
Certified Gr5 Fasteners Tailored for Kyushu & Fukuoka Procurement
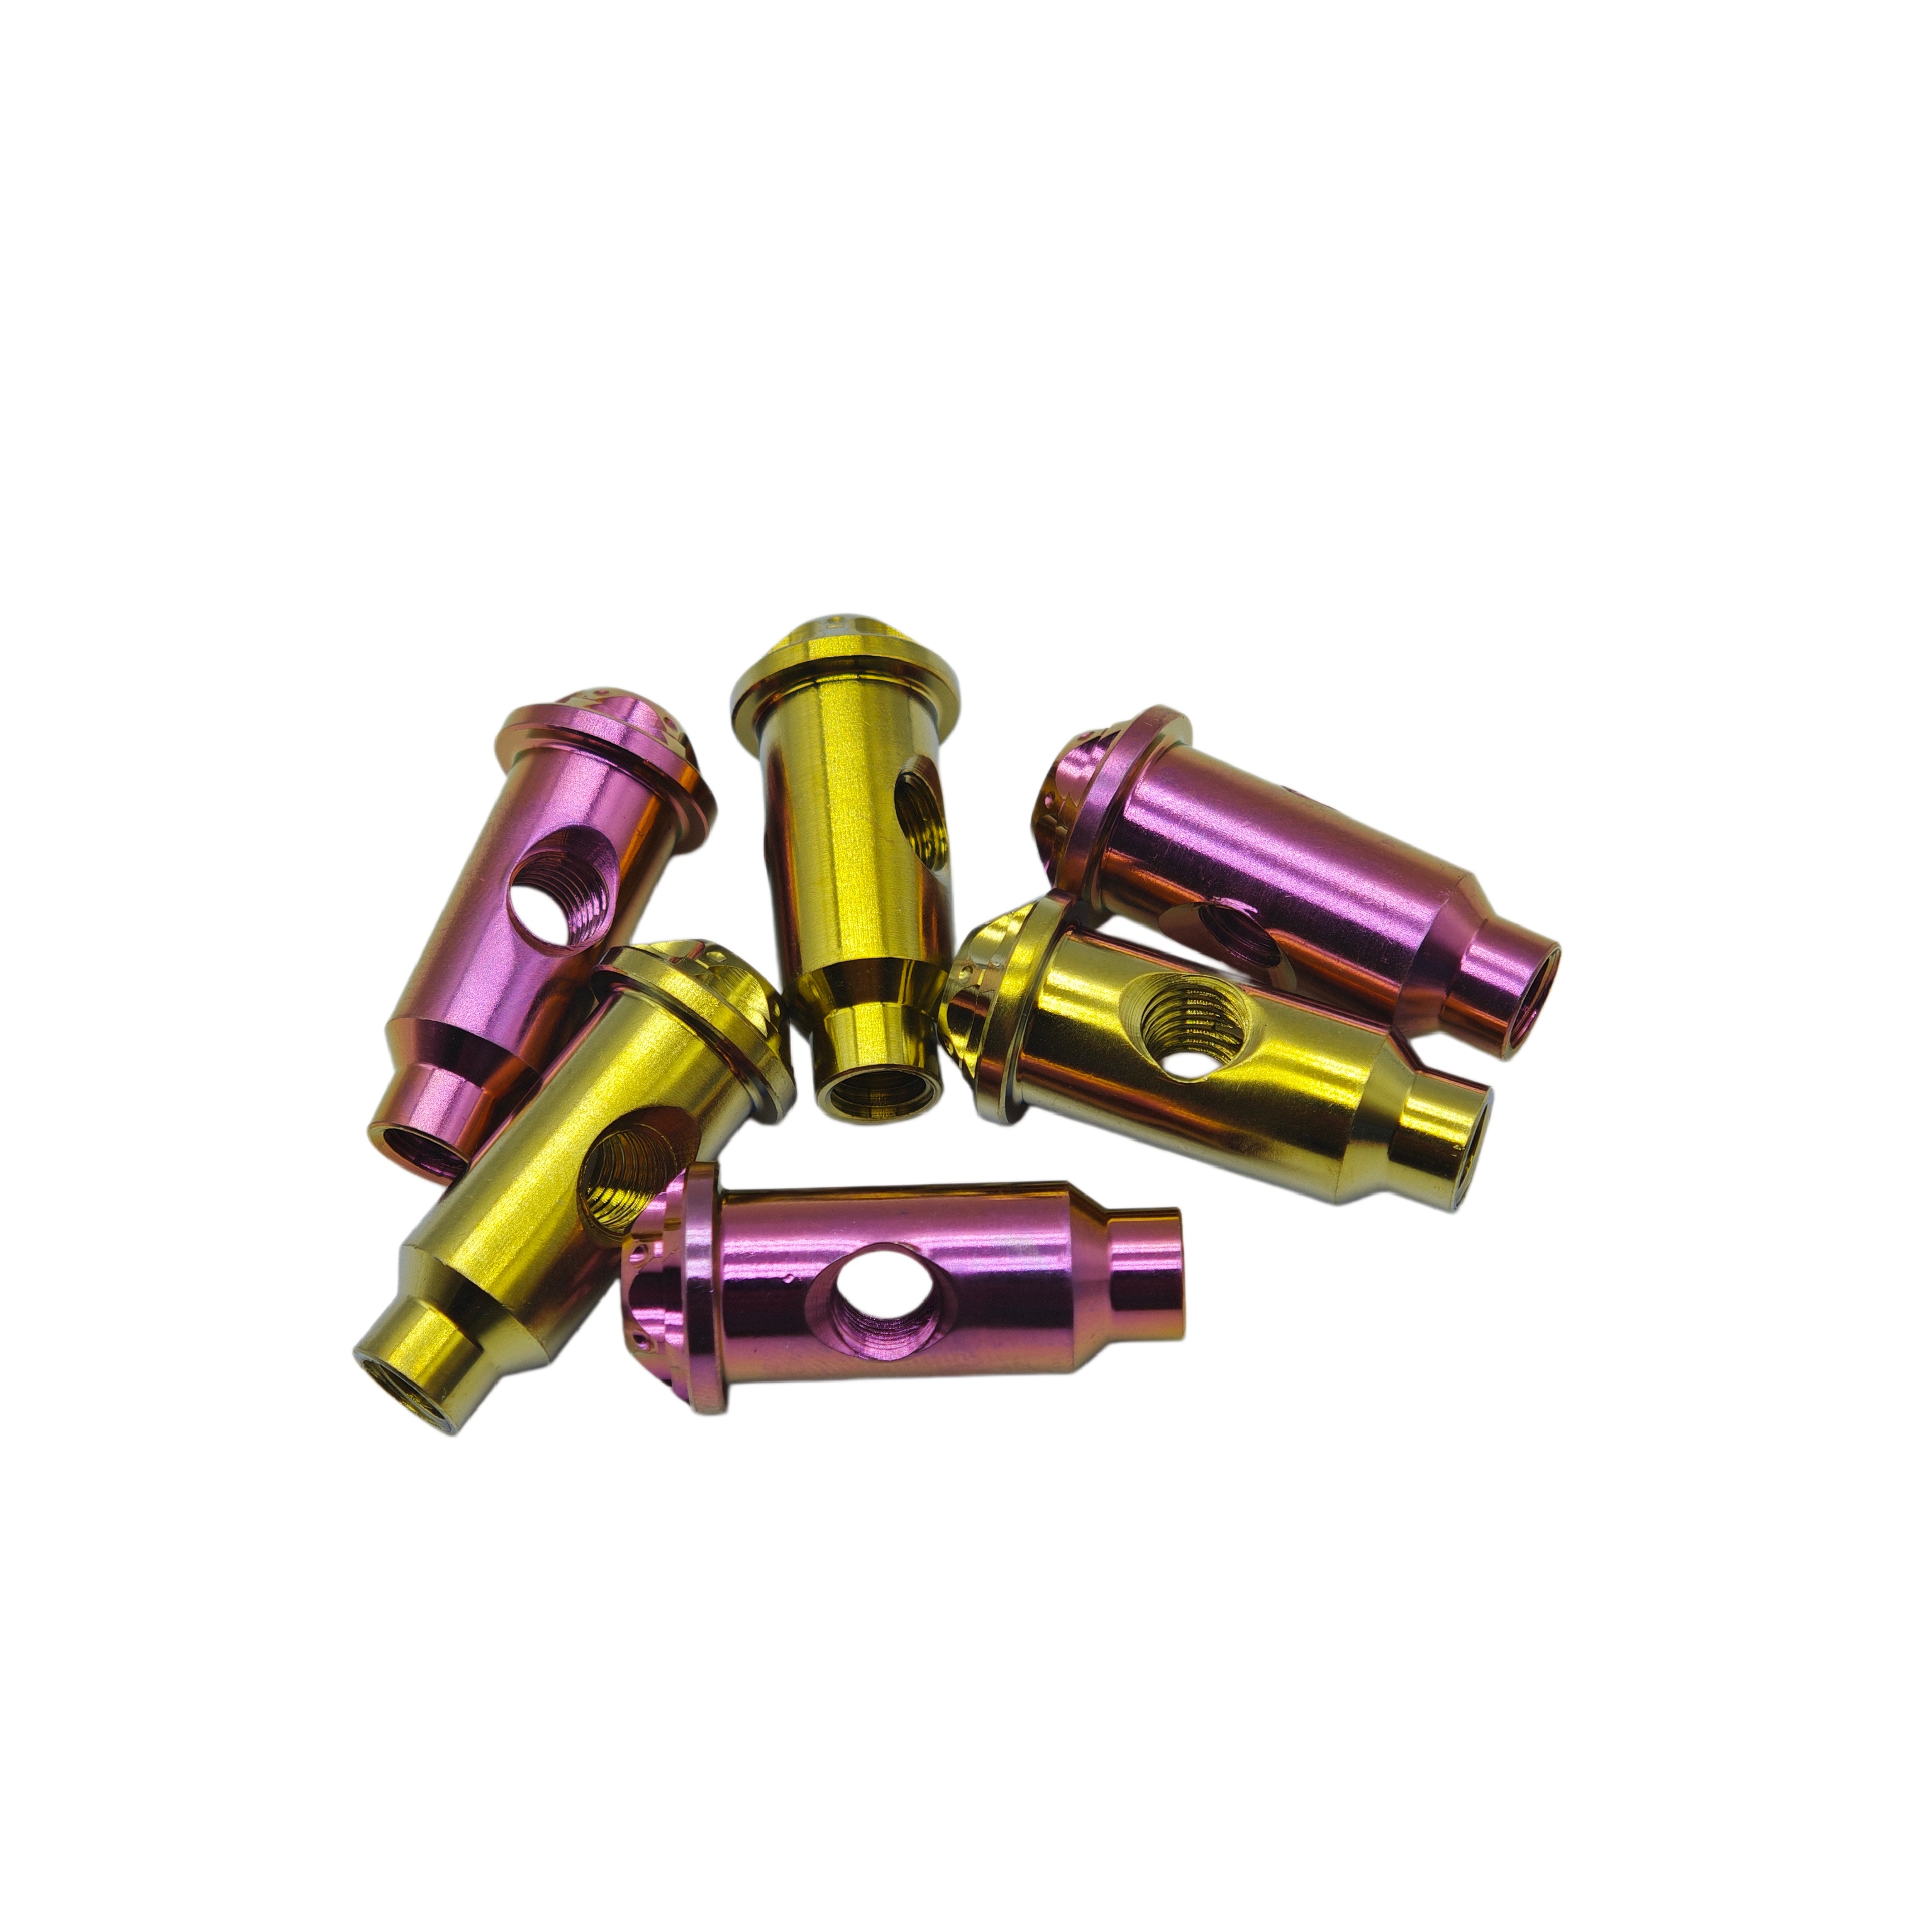
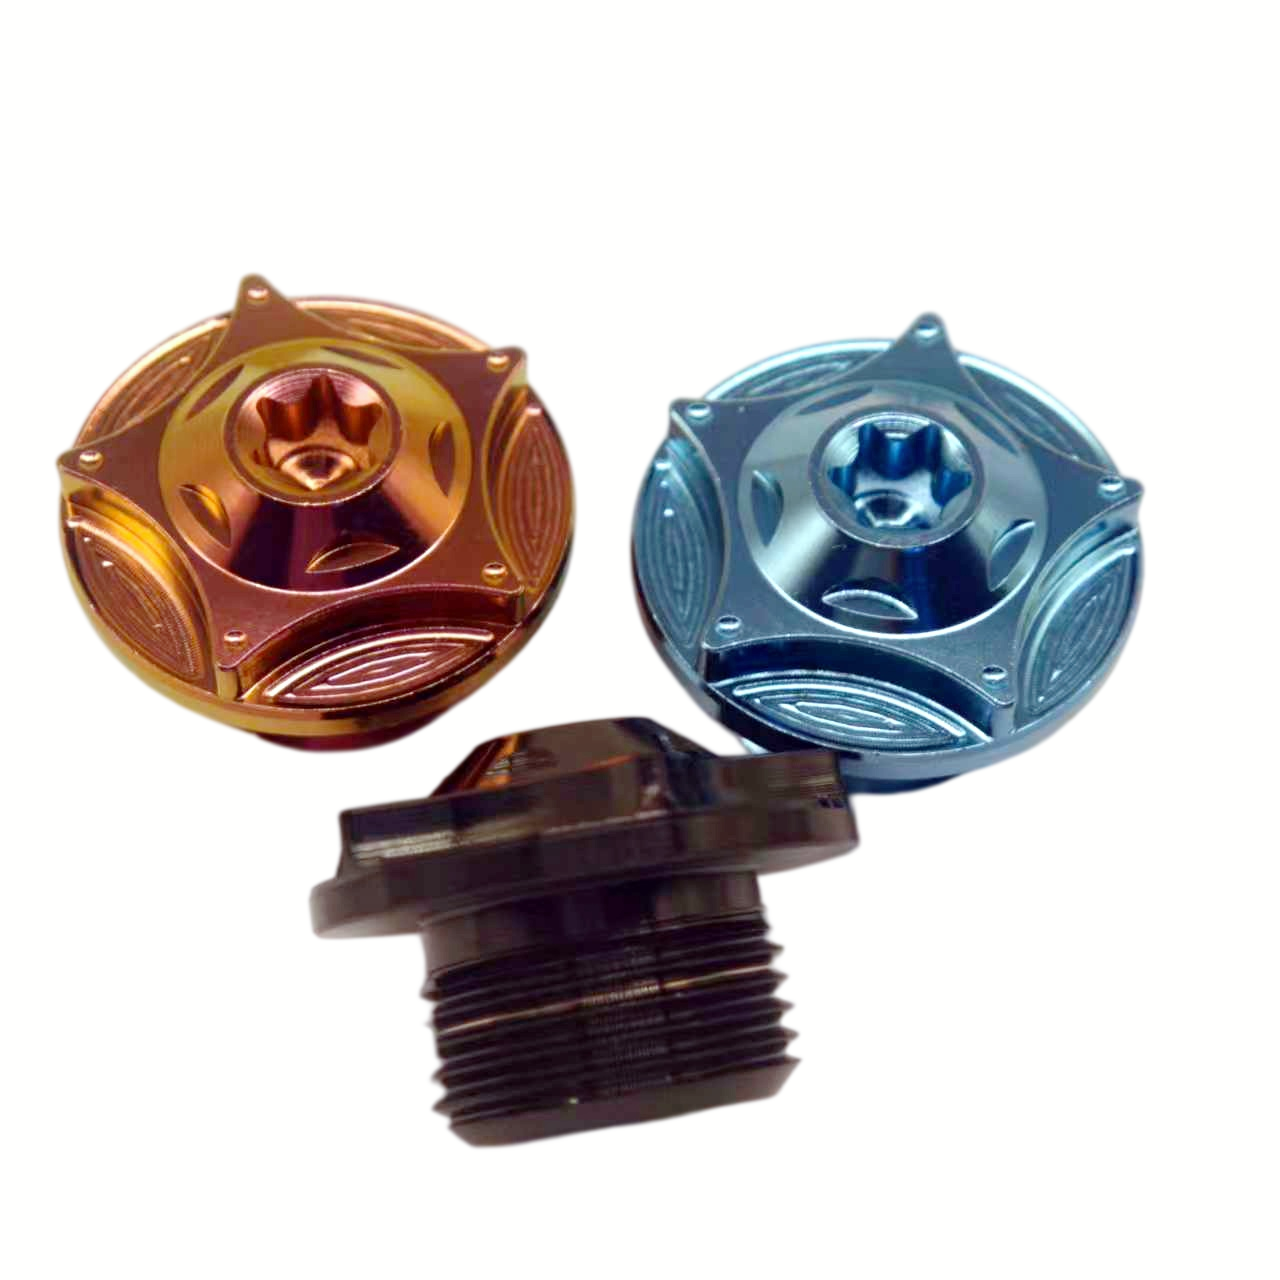
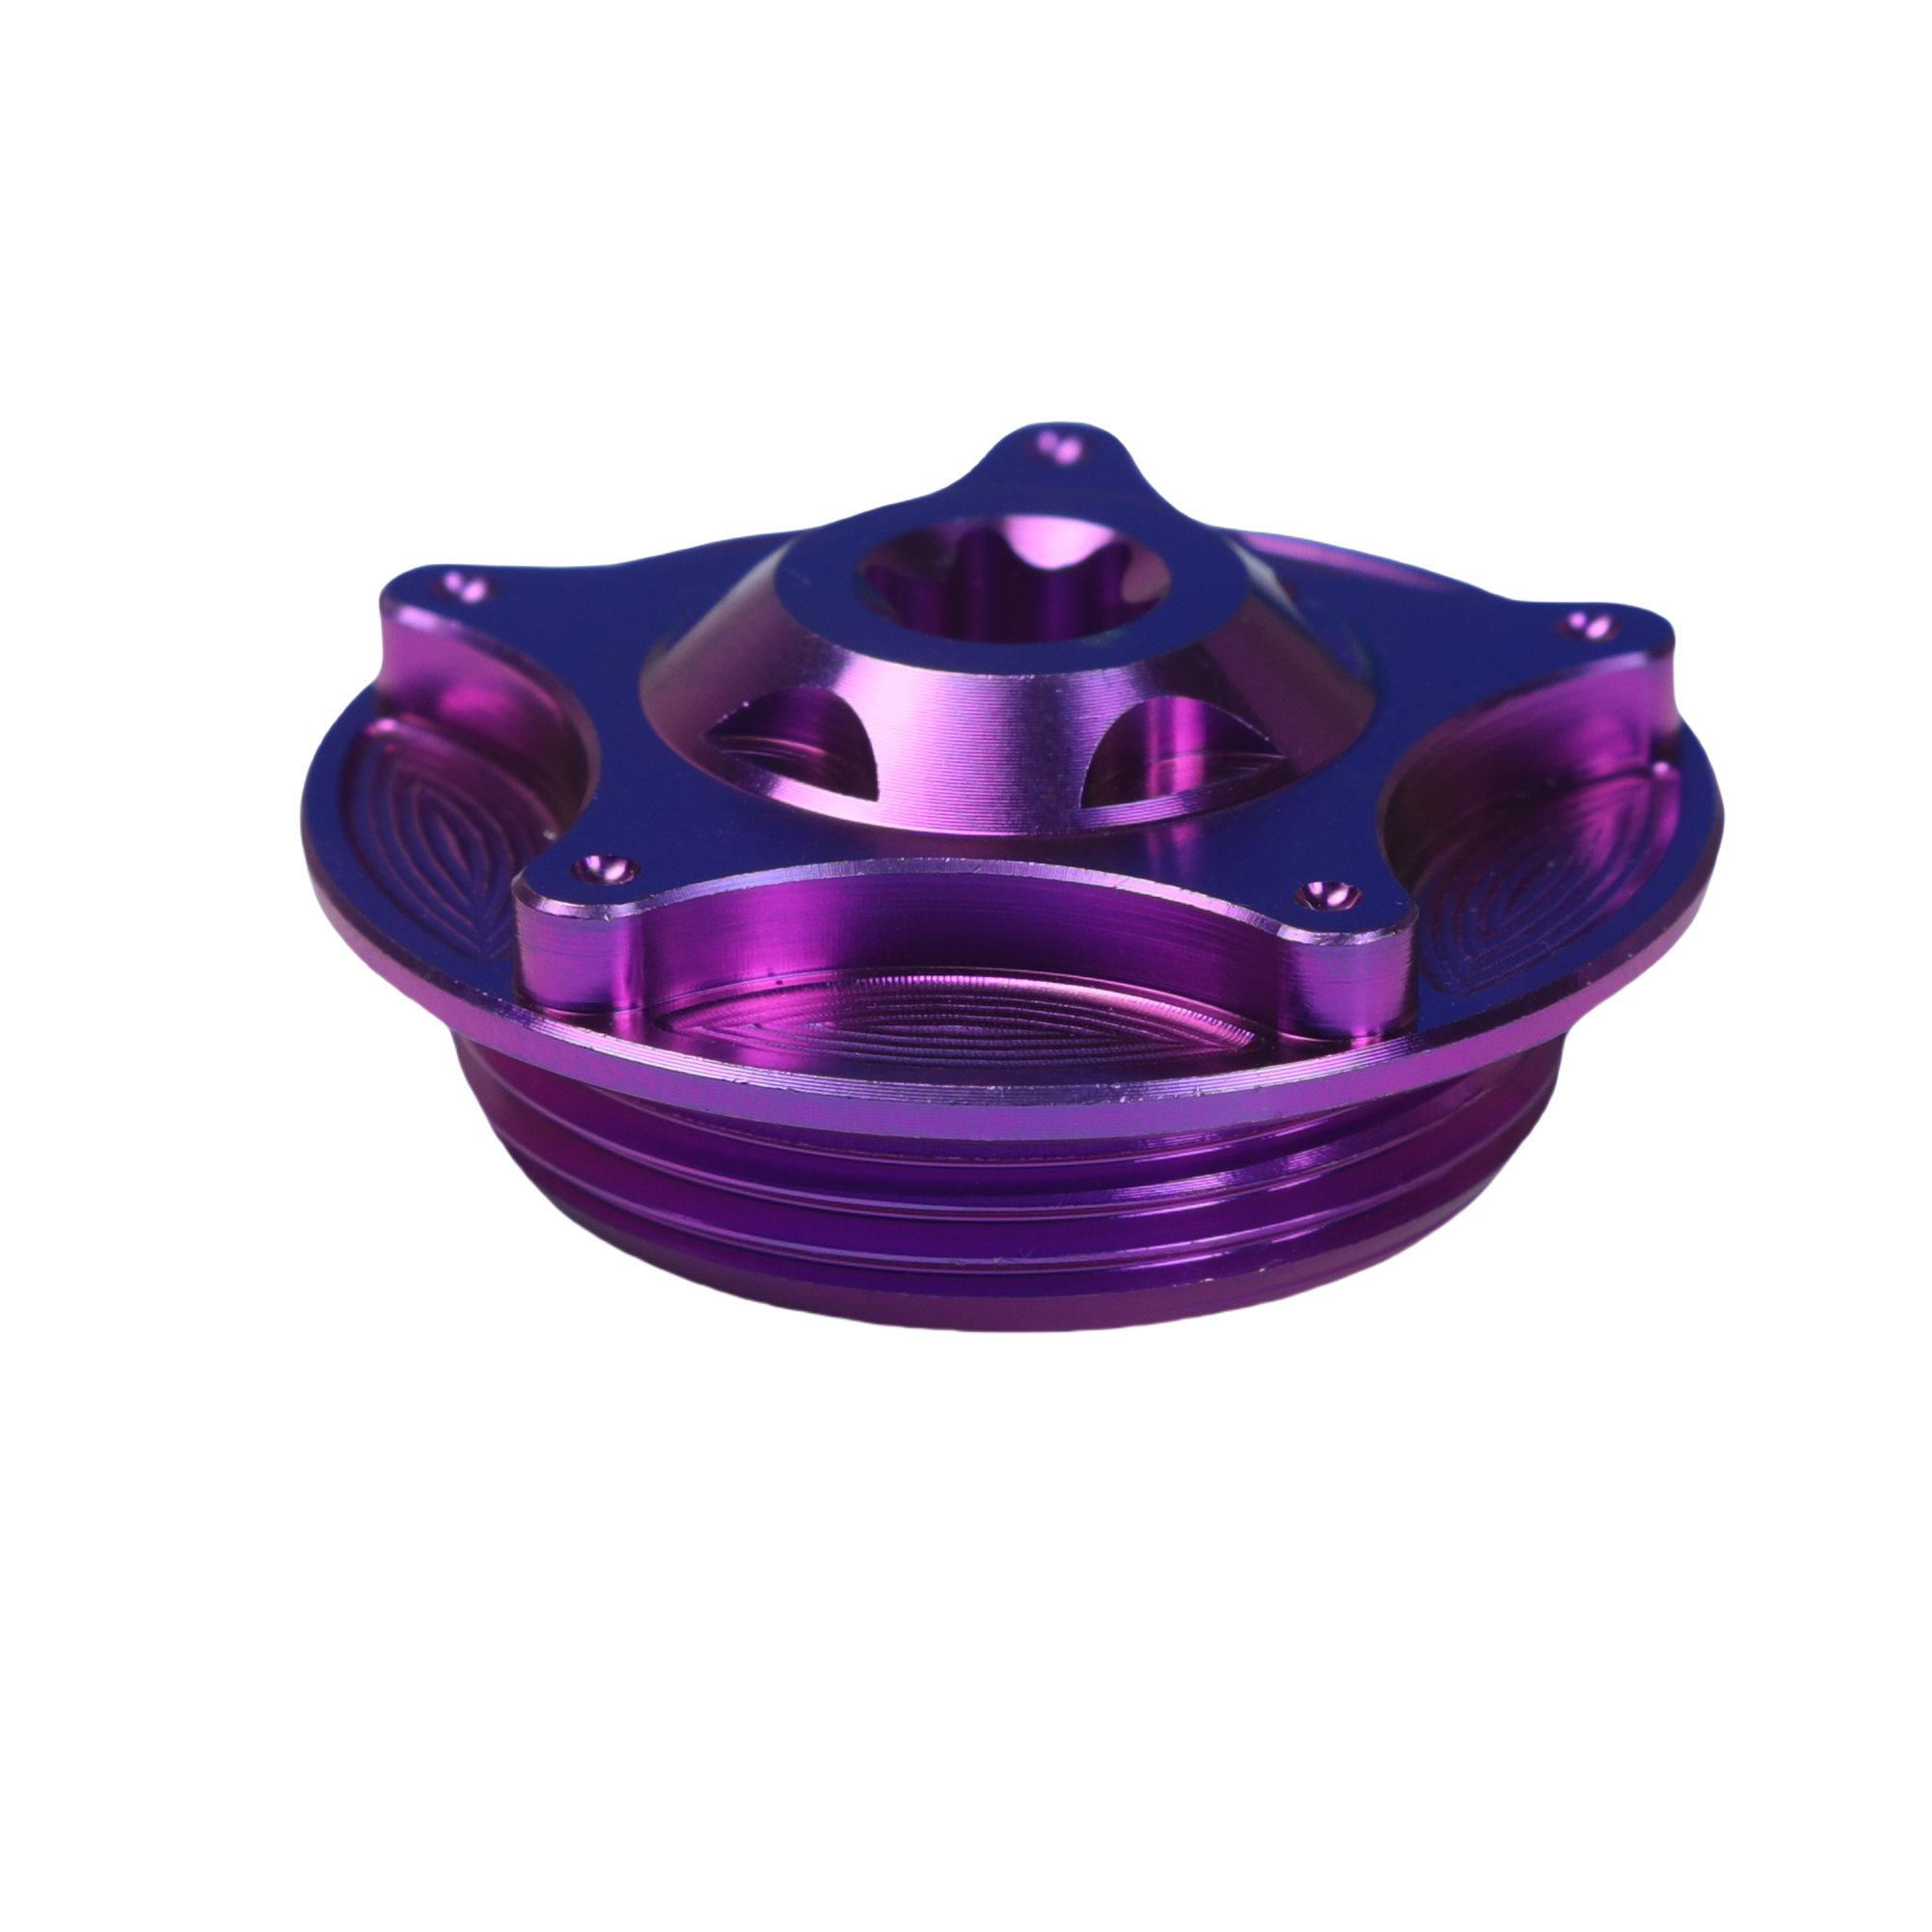
Exclusively crafted using aerospace-tier Ti-6Al-4V Grade 5 cold-headed and precision CNC-machined bar stock. Optimized to eliminate galvanic corrosion in salt-fog marine atmospheres while significantly dropping un-sprung rotating mass.
Fukuoka & Northern Kyushu: Regional Engineering Use Cases
Fukuoka acts as the vital maritime trade gateway and technological manufacturing hub of Western Japan. From deep-water installations across Hakata Bay to Kitakyushu's advanced industrial corridor, operating environments demand hardware that exceeds ordinary stainless steel capabilities.
Marine & Port Infrastructure (Hakata Port)
Exposure to chloride-dense marine spray around Fukuoka Bay causes rapid pitting and stress corrosion cracking (SCC) in austenitic 304 and 316 stainless steels. Ti-6Al-4V Grade 5 spontaneously generates a continuous, regenerative titanium dioxide (TiO2) ceramic passivation film, rendering fasteners virtually impervious to marine crevice corrosion, saltwater immersion, and industrial sulfur washouts.
Motorsport & Dynamic Weight Optimization
Northern Kyushu is home to premier automotive manufacturing and racing teams competing at circuits like Autopolis. Utilizing Gr5 titanium for brake caliper mounting bolts, brake rotor bobbins, and axle pinch hardware strips 44% of un-sprung rotating mass compared to grade 10.9 steel. This drastically improves suspension response, mitigates gyroscopic inertia, and maintains high-temperature shear strength above 350°C.
Semiconductor & Cleanroom Automation
As Kyushu expands its role as "Silicon Island," cleanroom robotic end-effectors and wafer processing units demand totally non-magnetic materials with minimal outgassing profiles. Our vacuum-degassed Gr5 titanium fasteners exhibit magnetic permeability μr ≈ 1.00005, preventing electronic beam interference and eliminating particulate contamination caused by degrading plating materials.
Ti-6Al-4V Grade 5 vs Conventional Fastening Alloys
A direct metallurgical comparison highlighting why engineering firms throughout Fukuoka Prefecture are transitioning critical joints from structural steels and aluminum alloys to high-yield Grade 5 titanium.
| Mechanical / Physical Property | Ti-6Al-4V (Grade 5 Titanium) | SCM435 (Class 10.9 Steel) | SUS304 / A2-70 Stainless | 7075-T6 Duralumin |
|---|---|---|---|---|
| Density (ρ) | 4.43 g/cm³ (Ultra-lightweight) | 7.85 g/cm³ | 7.93 g/cm³ | 2.81 g/cm³ |
| Tensile Yield Strength (Rp0.2) | 895 – 1000 MPa | 900 – 940 MPa | 450 – 500 MPa | 460 – 500 MPa |
| Strength-to-Weight Ratio | 214 kN·m/kg (Unmatched) | 120 kN·m/kg | 88 kN·m/kg | 180 kN·m/kg |
| Marine Atmospheric Pitting Resistance | Immune (PREN > 40 eq.) | Severely Vulnerable | Pitting in < 6 months | Severe intergranular attack |
| Thread Forming Execution | Precision CNC + Cold Rolled | Hot Formed / Rolled | Cold Rolled / Cut | Machined / Weak Shear |
| Thermal Operation Ceiling | -250°C to +400°C | Up to +200°C | Up to +300°C | Degrades rapidly > +100°C |
Industrial Evolution & Fastener Trends in Kyushu
Insights into regional manufacturing developments shaping fastener procurement across Fukuoka's coastal, robotics, and transportation ecosystems.
Offshore Hydrogen & Wind Energy
With Hibikinada Port in Kitakyushu developing into a national offshore wind base, fasteners must survive 25+ years in harsh sea spray without electrolytic degradation. Titanium fasteners eradicate recurring subsea maintenance costs.
Electrification of Vehicle Fleets
Kyushu's vehicle assembly sectors are prioritizing light-weighting to offset dense battery architectures. Replacing standard fasteners with rolled-thread Gr5 titanium recovers crucial payload margins across performance EVs.
Precision Drone & Robotics Hubs
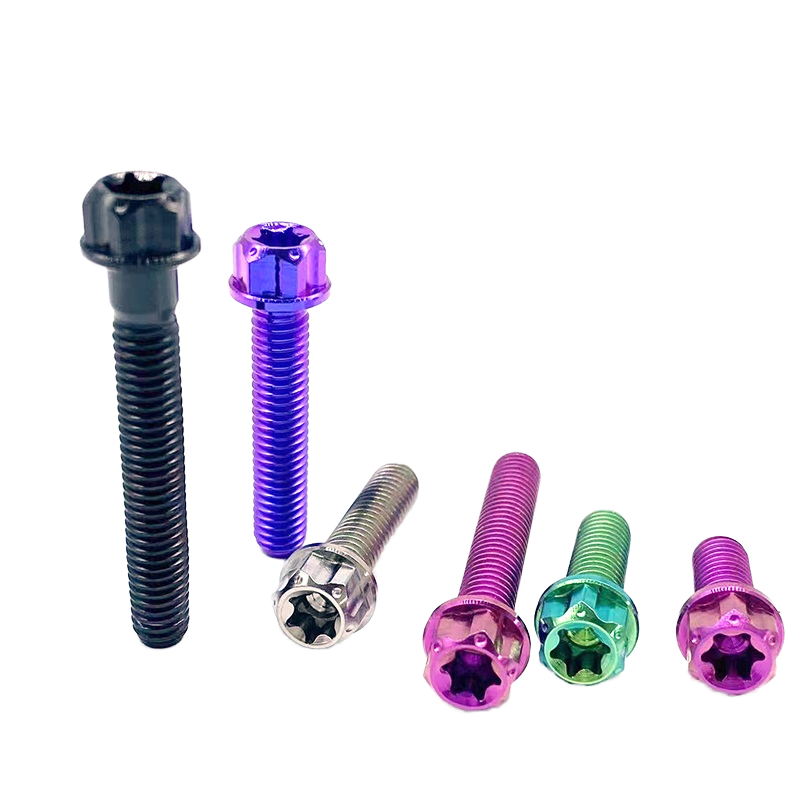
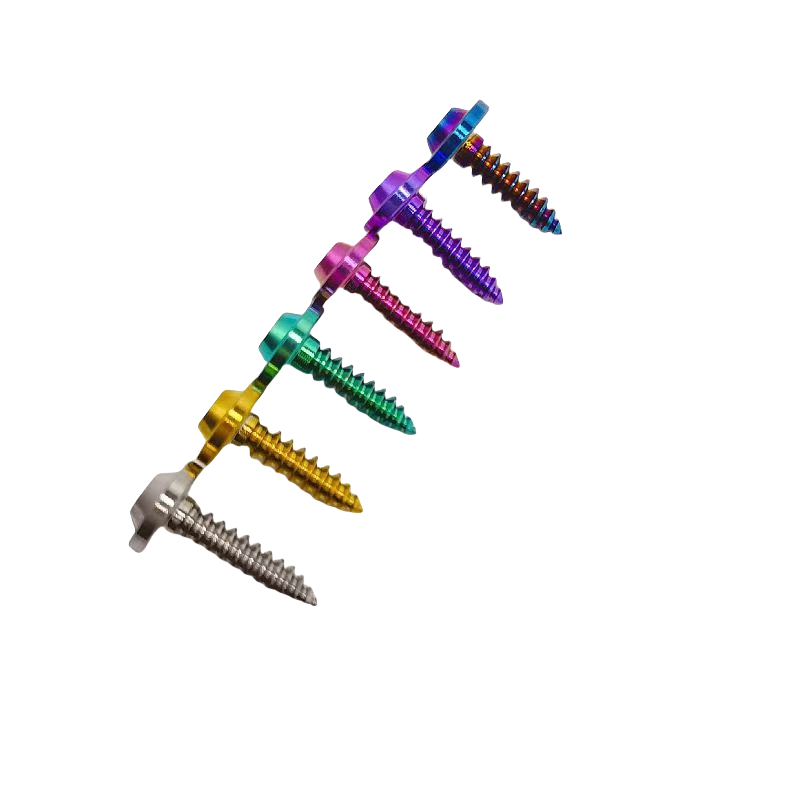
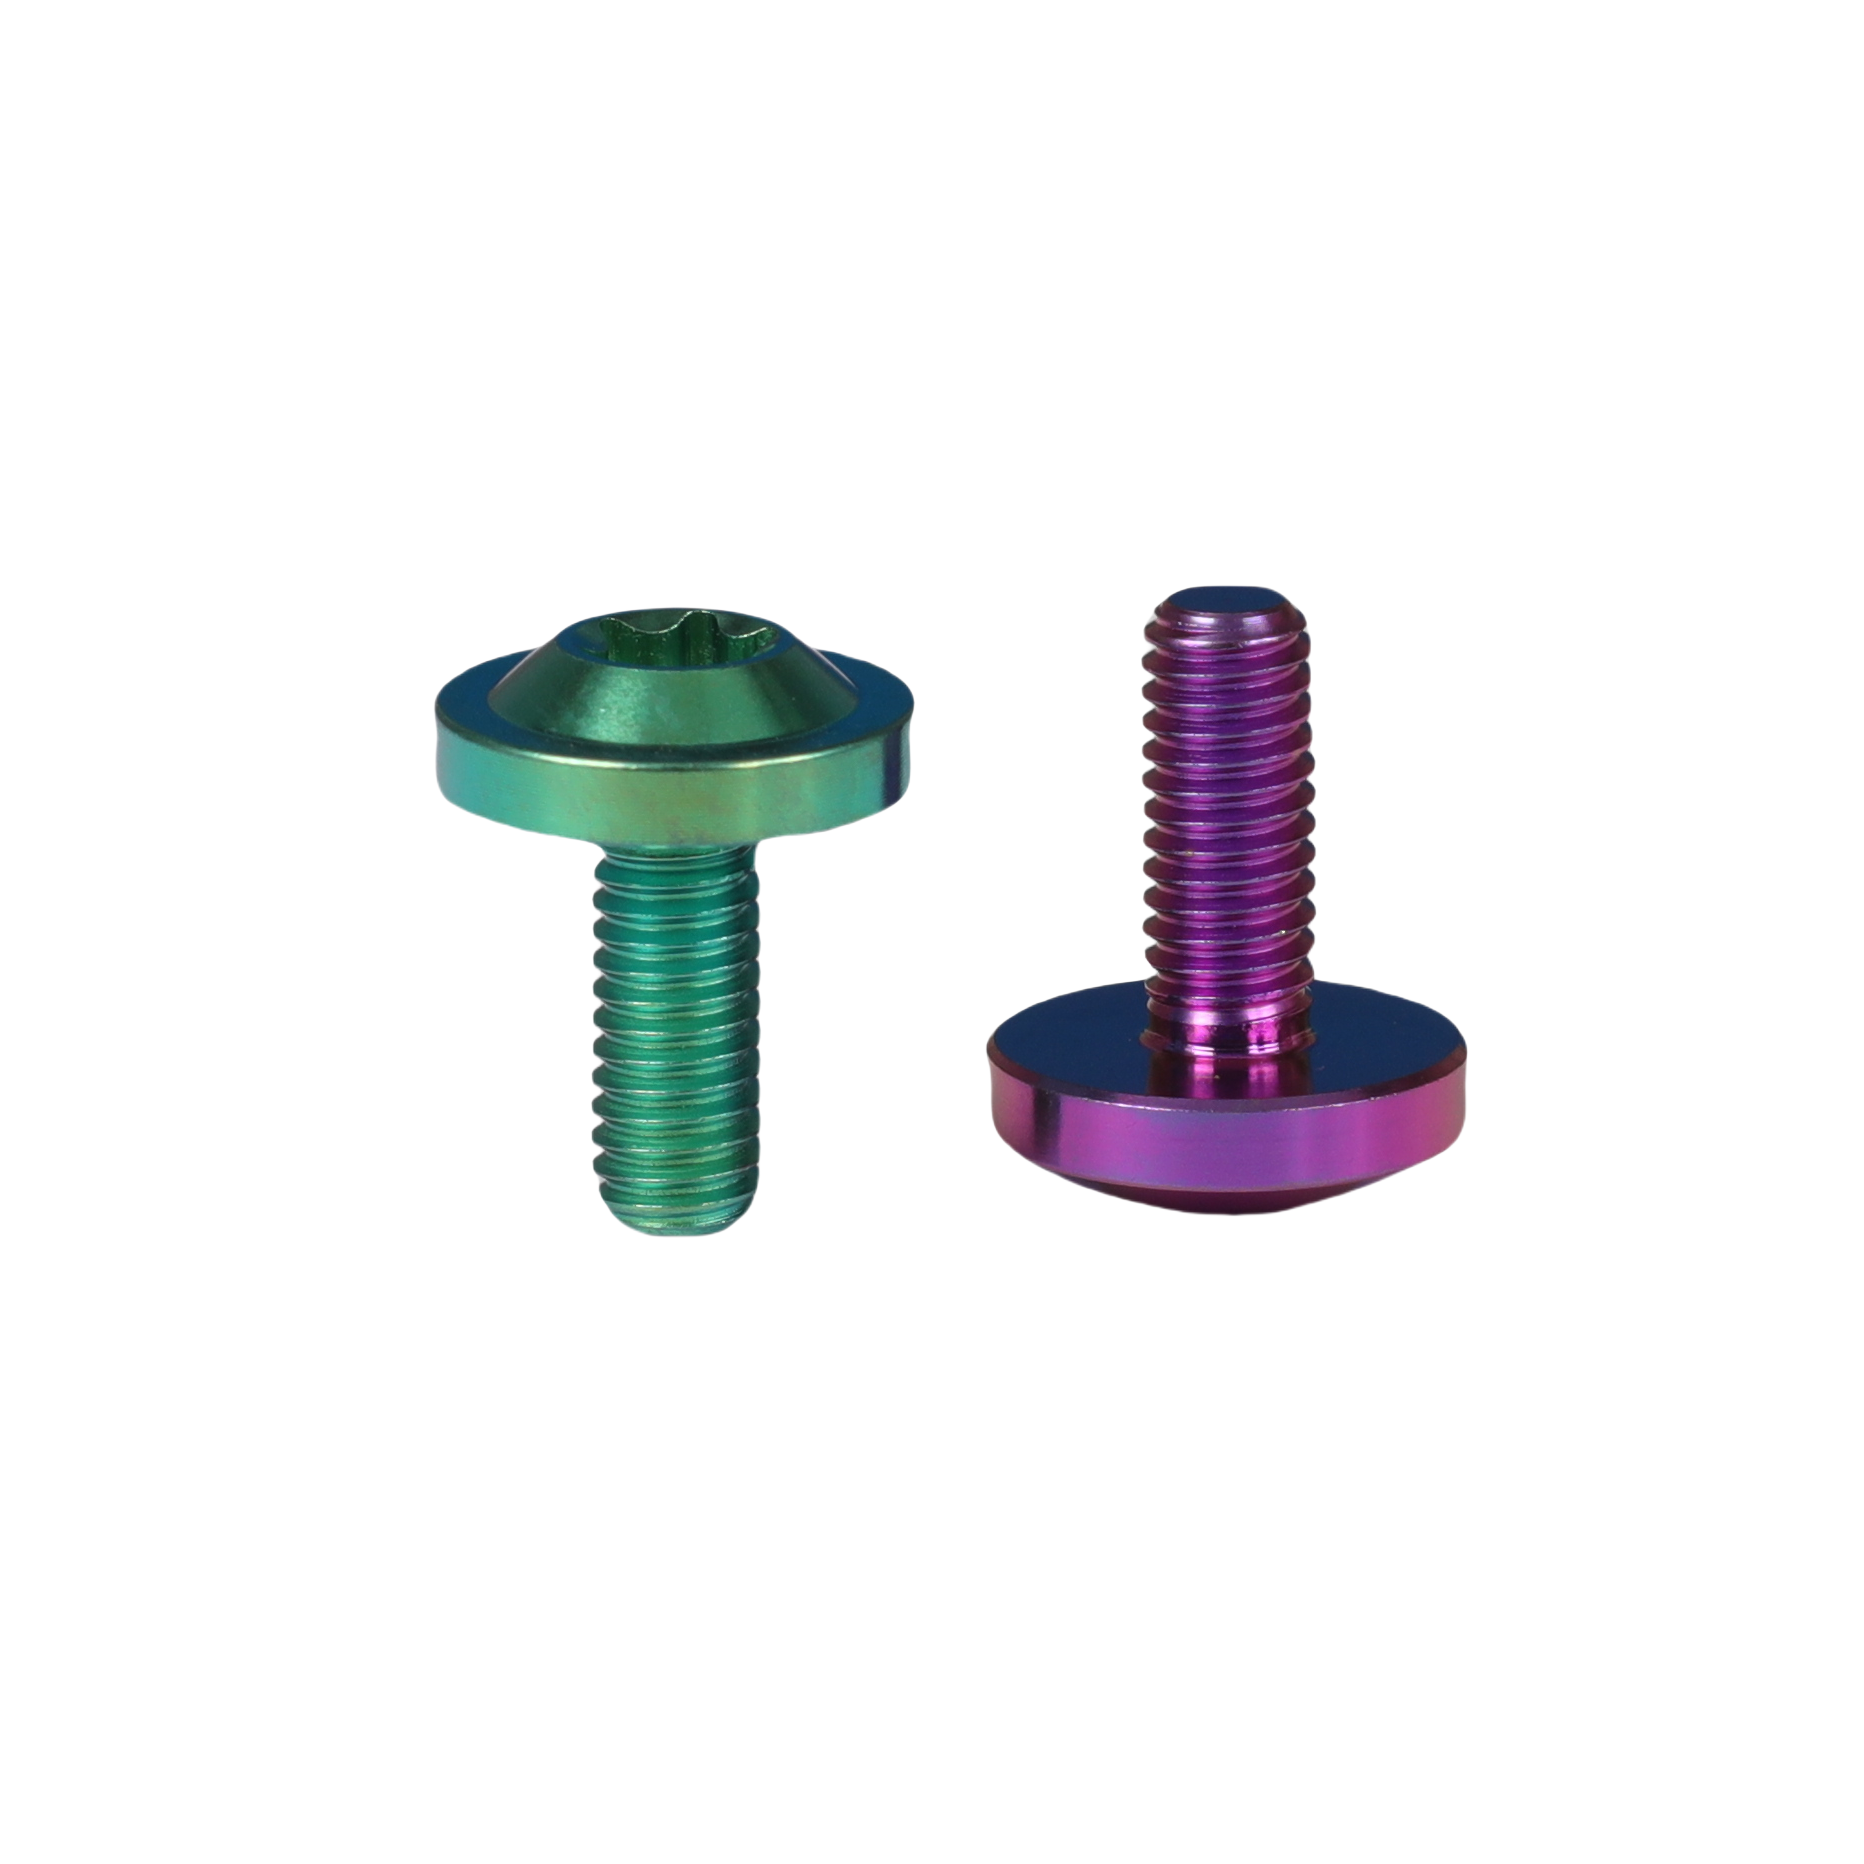
Fukuoka's vibrant tech start-up community focuses on autonomous inspection drones and robotic logistics. Miniature Grade 5 Torx screws provide maximum axial tension without weight penalties, preserving payload flight times.
Ultra-High Vacuum Environments
Advanced optics, cleanrooms, and testing facilities in Fukuoka require non-magnetic components with high fatigue life. Titanium alloy guarantees absolute joint integrity without flaking electroplate residue.
Enterprise Strengths & Certified Quality Assurance
Directly originating from Baoji—the recognized Titanium Valley producing the majority of high-purity titanium stock—our facility integrates end-to-end metallurgical verification with high-speed multi-axis CNC manufacturing.
Full Heat-Number Traceability
We source only certified Ti-6Al-4V ingot stock. Every production run is issued alongside an EN 10204 Type 3.1 Mill Test Certificate (MTC) detailing complete chemical composition (Fe ≤ 0.30%, O ≤ 0.20%, N ≤ 0.05%) and mechanical tensile verification.
Rolled Thread Grain Flow
Unlike common cut threads that shear through grain boundaries, our fastener threads are cold-rolled using carbide dies under precision lubrication. This work-hardens the root radii, doubling cyclical fatigue resistance and practically eliminating shear notch failure.
Multi-Axis Turn-Mill Centers
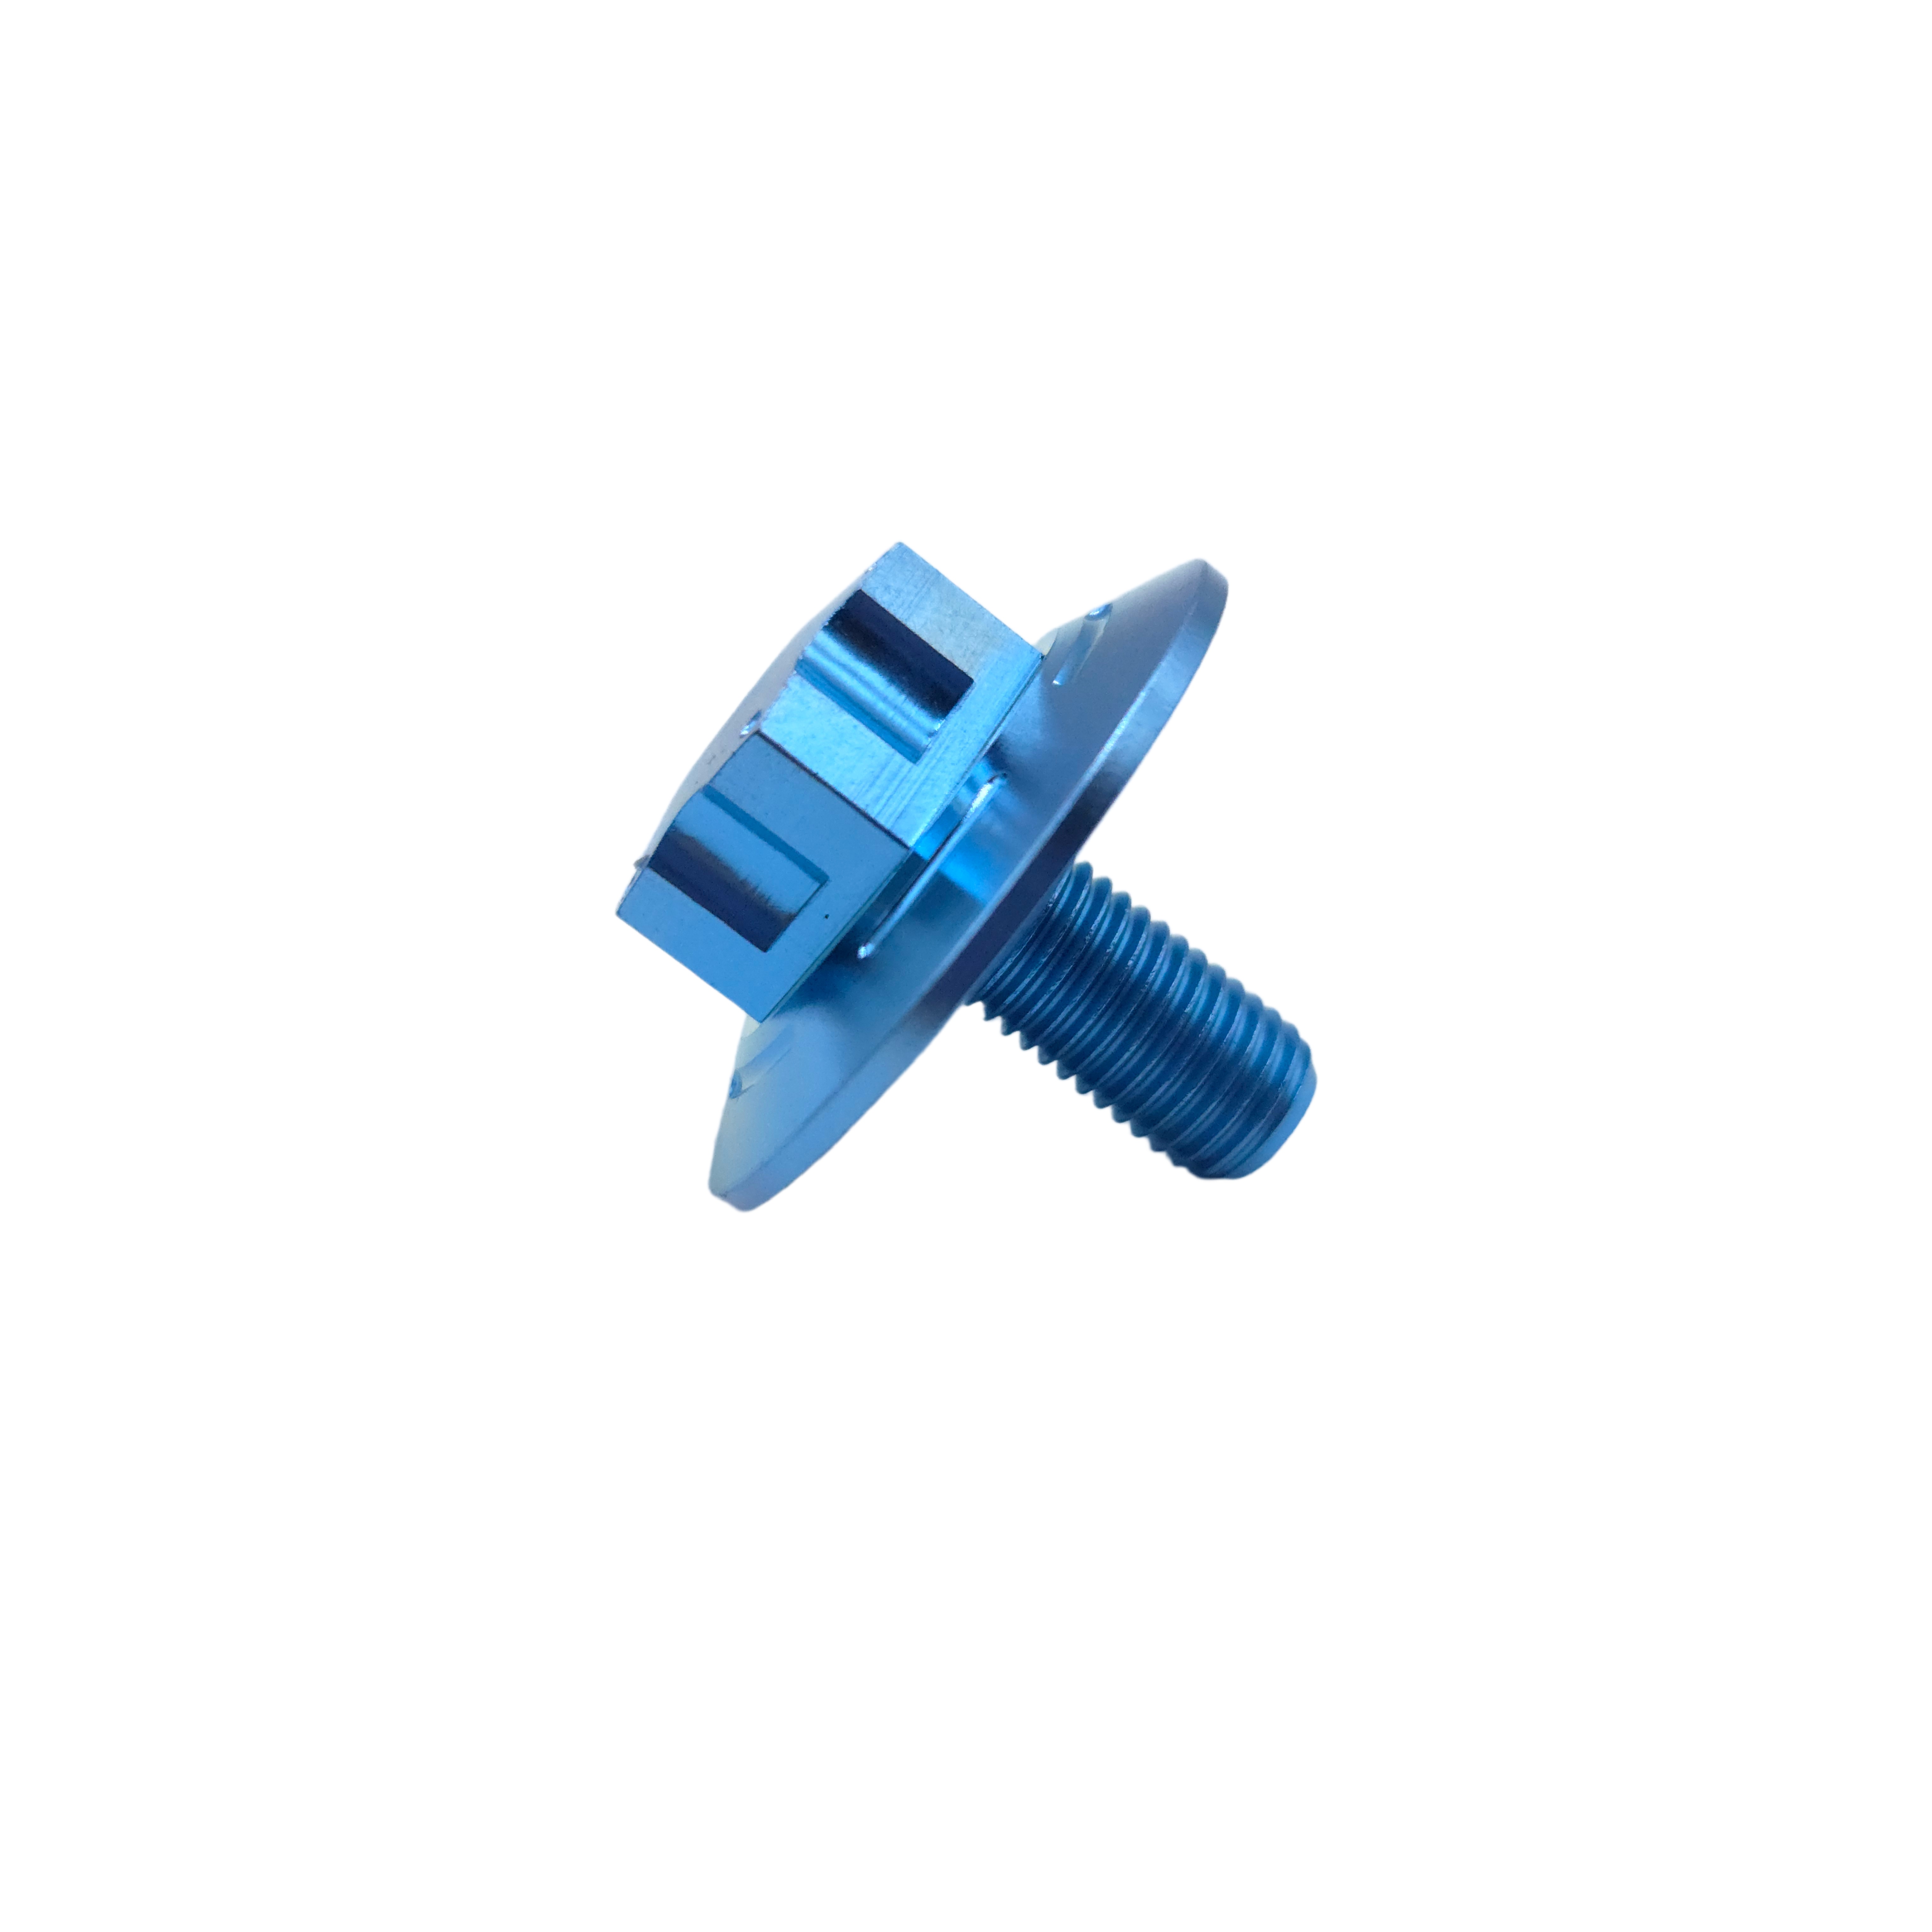
Equipped with automated multi-axis Swiss-lathes and 5-axis CNC machining complexes capable of maintaining tight tolerances down to ±0.005 mm. Flange head runouts, custom sockets (Torx, Hex, Star), and cross-drilled safety lock features are finished in single setups.
Frequently Asked Questions by Japanese Engineers
Critical technical considerations addressing galling prevention, international compliance, customs transport to Fukuoka, and exact torque engineering calculations.
How does your factory prevent galling (thread seizing) when threading titanium into aluminum or stainless joints?
Titanium forms an adhesive oxide film under dry friction, which can induce galling when paired against softer metals. To counter this, we apply two engineering solutions: precision rolling that yields ultra-smooth surface root finishes (Ra ≤ 0.4 μm), and physical vapor deposition (PVD) / specialized micro-arc anodizing that creates a high-hardness barrier. For field assembly, we provide torque-coefficient documentation and recommend high-grade molybdenum disulfide or nickel-based anti-seize lubricants.
What shipping corridors and delivery timeframes apply for orders arriving in Fukuoka or Kitakyushu?
Due to Fukuoka’s close geographical proximity to China's export hubs, standard air express shipments via DHL, FedEx, or SF Express reach Fukuoka Airport (FUK) within 2 to 4 working days after dispatch. For large-tonnage OEM production batches, direct ocean freight services to the Port of Hakata deliver transit within 5 to 7 days, complete with automated customs packing declarations, Japanese-compliant commercial invoices, and bilingual packing lists.
Can custom components be machined directly to JIS (Japanese Industrial Standards) or proprietary CAD files?
Yes. Our engineering department routinely works with JIS standards (such as JIS B 1176, JIS B 1180, and JIS B 1189) as well as DIN, ISO, and ASTM/ASME specifications. Clients can submit STEP, IGES, or DWG drawings. We conduct pre-production DFM (Design for Manufacturability) audits within 24 hours, guaranteeing that lead-in chamfers, head fillets, and thread tolerances strictly match your assembly requirements before machining begins.
How does Gr5 Ti-6Al-4V compare in fatigue life against high-tensile 12.9 class alloy steel?
While class 12.9 alloy steel provides higher nominal ultimate tensile strength (1220 MPa), it is prone to hydrogen embrittlement, stress corrosion, and notch sensitivity in coastal environments like Fukuoka. Ti-6Al-4V features a fatigue limit-to-tensile ratio of roughly 0.5 to 0.6, which is substantially superior to most structural alloys. When threads are cold-rolled, the residual compressive stresses at the thread root deliver continuous cyclical reliability without sudden catastrophic fatigue fracture.
What quality certification and chemical assay reports accompany our order?
Every production consignment is tracked to its original vacuum-arc remelted ingot. We supply complete EN 10204 3.1 inspection certificates verifying spectrometry chemical analysis, tensile testing, elongation percentages, and hardness (HRC 32-38). Additionally, our quality assurance laboratory can provide optical CMM dimensional reports, thread pitch gauge verification records, and salt spray exposure data upon request.
Connect Directly with Our Titanium Fastener Engineers
Send your CAD models, JIS/DIN part numbers, or volume requirements for a comprehensive technical quote and DFM report delivered within 7 hours.
