Featured Industrial Titanium Cap Screws & Fasteners
Precision-machined from certified aerospace Grade 5 titanium (Ti-6Al-4V) bar stock. Thread-rolled under calibrated cold-heading dies to maximize structural fatigue resistance, offering a 44% mass reduction against 8.8/10.9 structural steels with complete corrosion immunity.
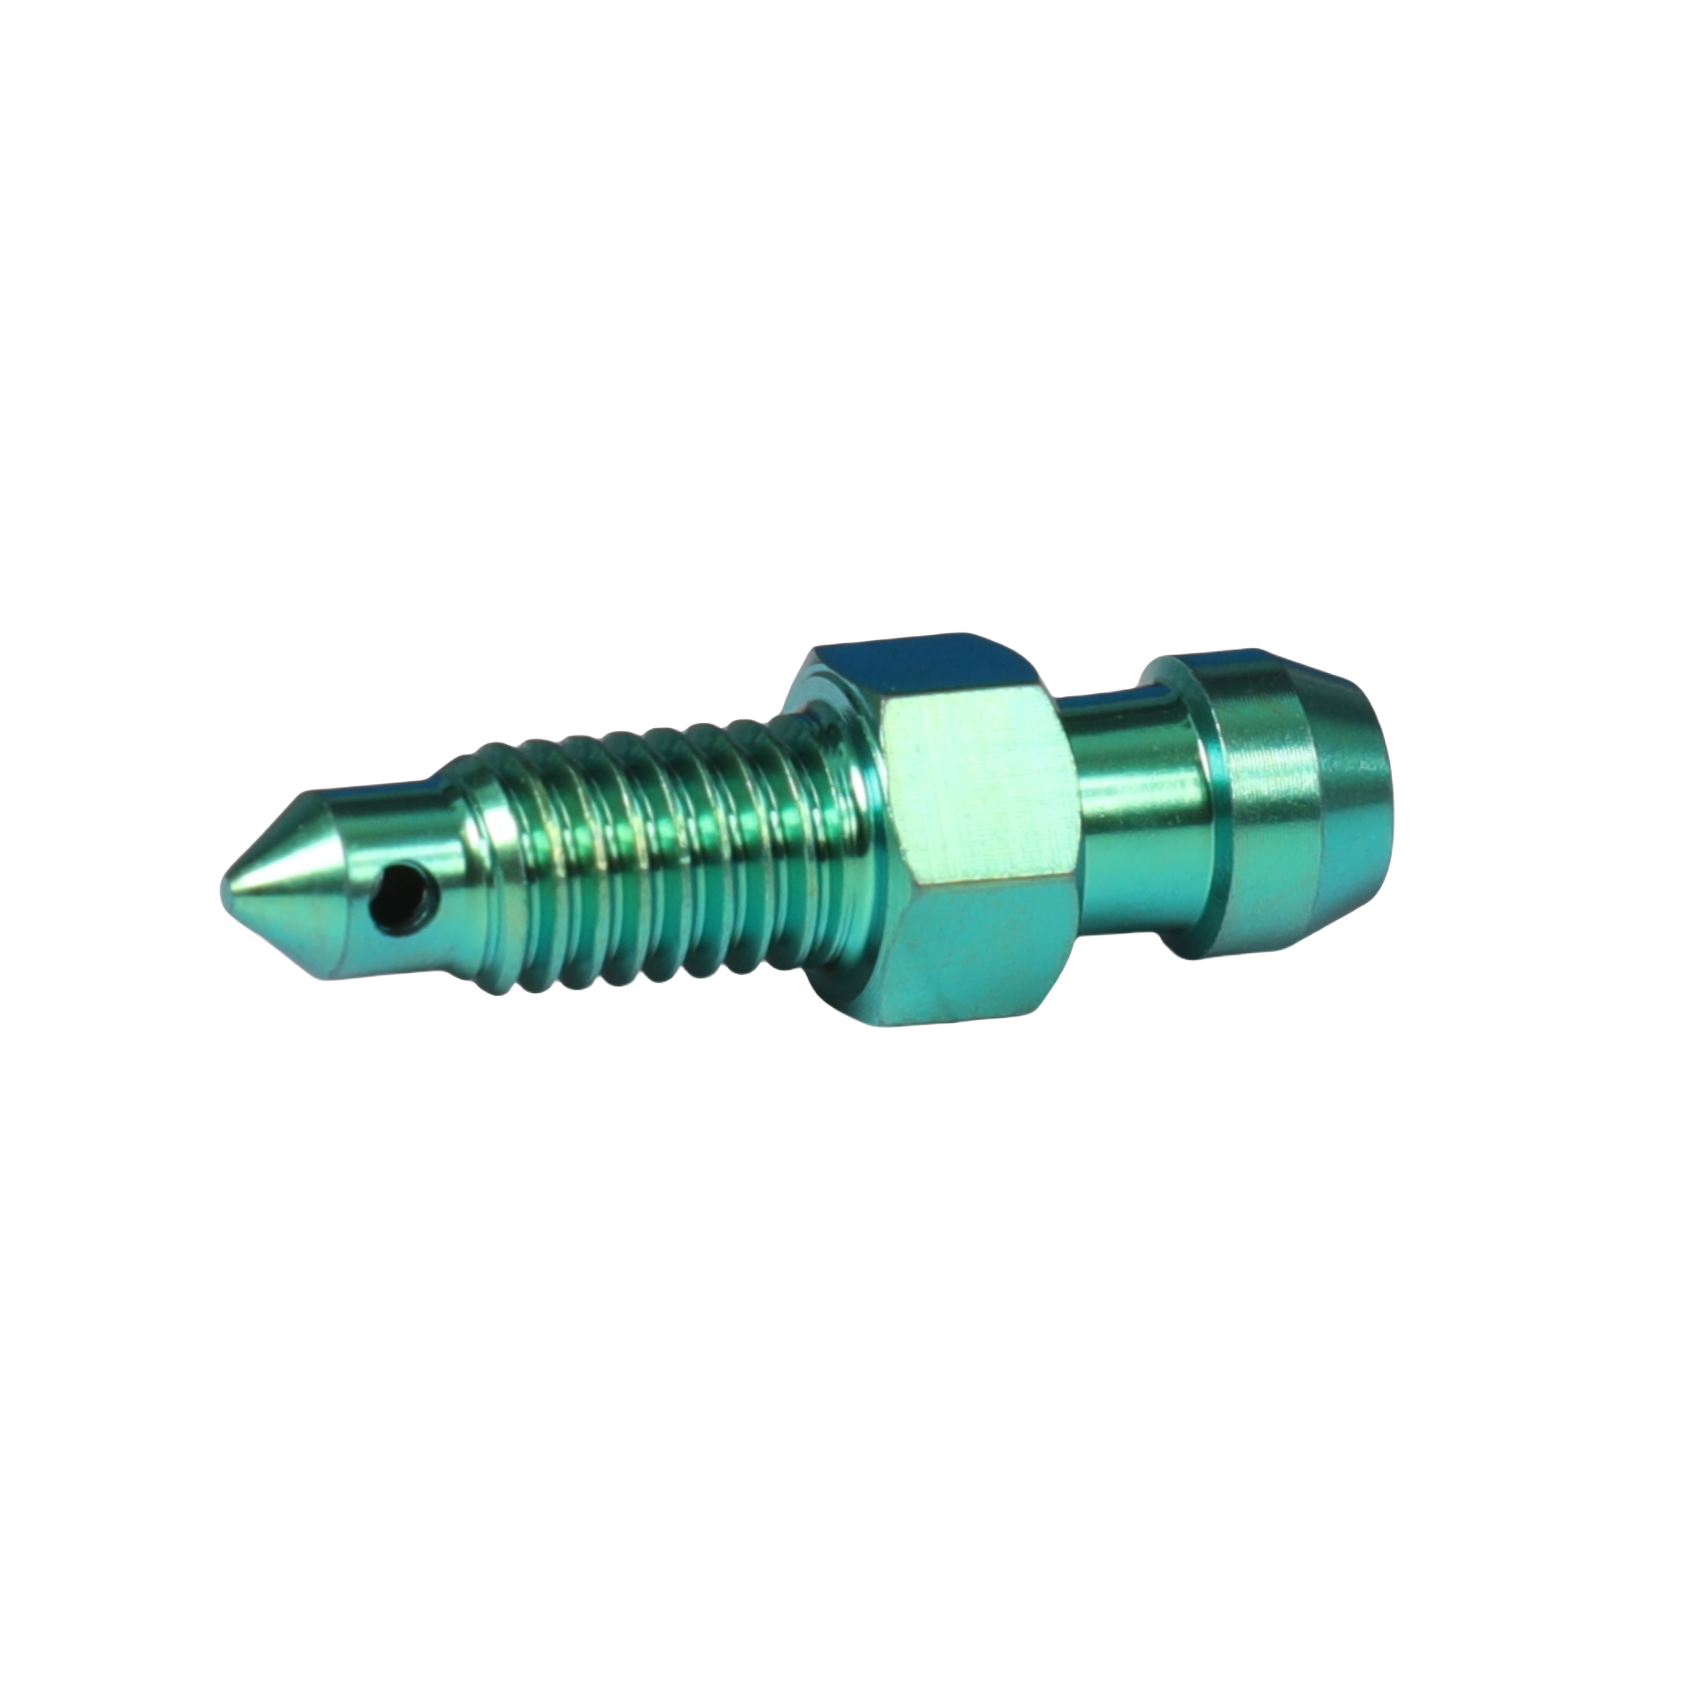
TKS M6 Anodized Gr5 Titanium Hex Caliper Oil Drain Bolt
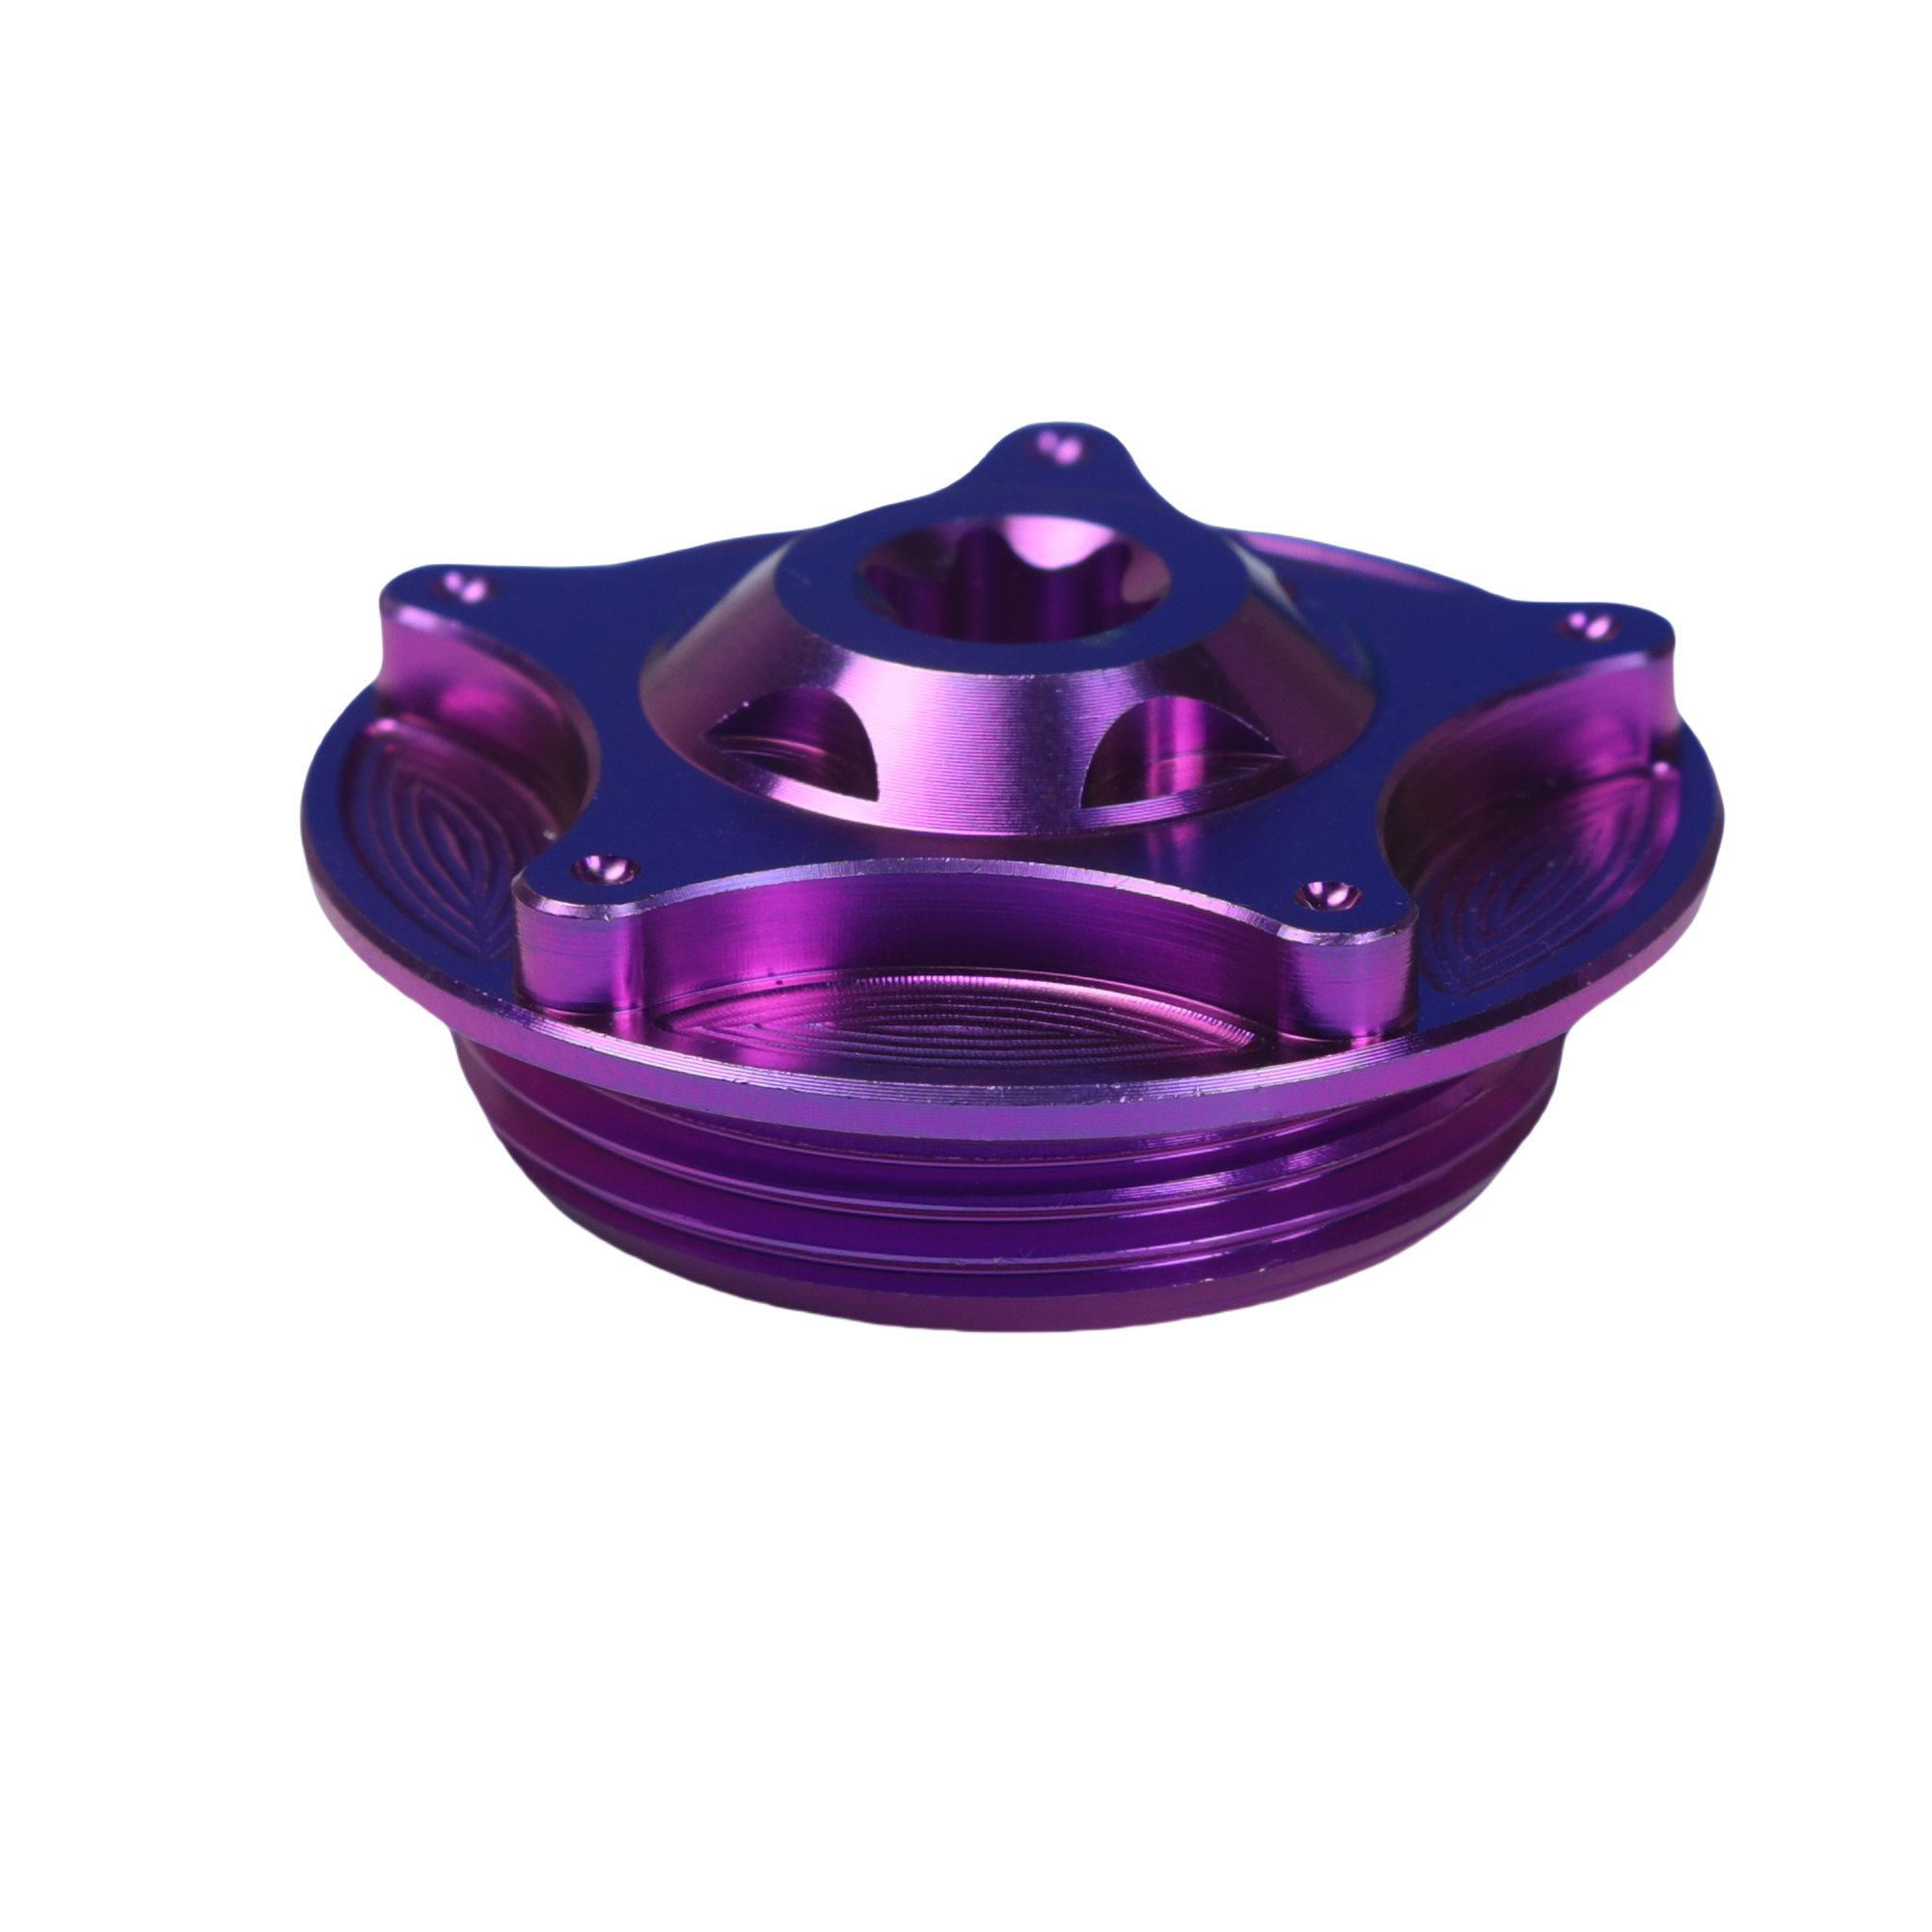
Factory Wholesale Titanium Alloy Oil Cap Nut & Fasteners
Custom GR5 Titanium M8 Low-Profile Disc Head Bolts
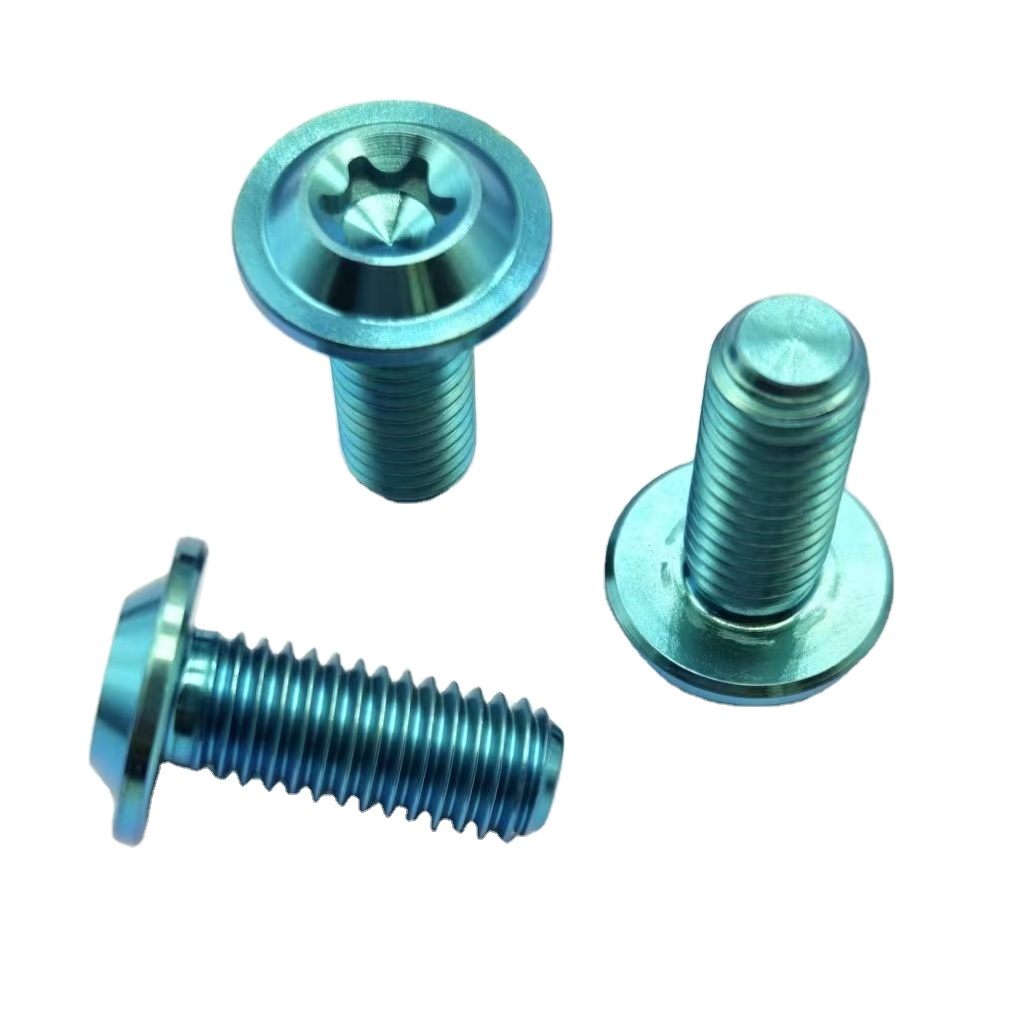
Customized M8 Gr5 Titanium Alloy Pan Head Socket Screws
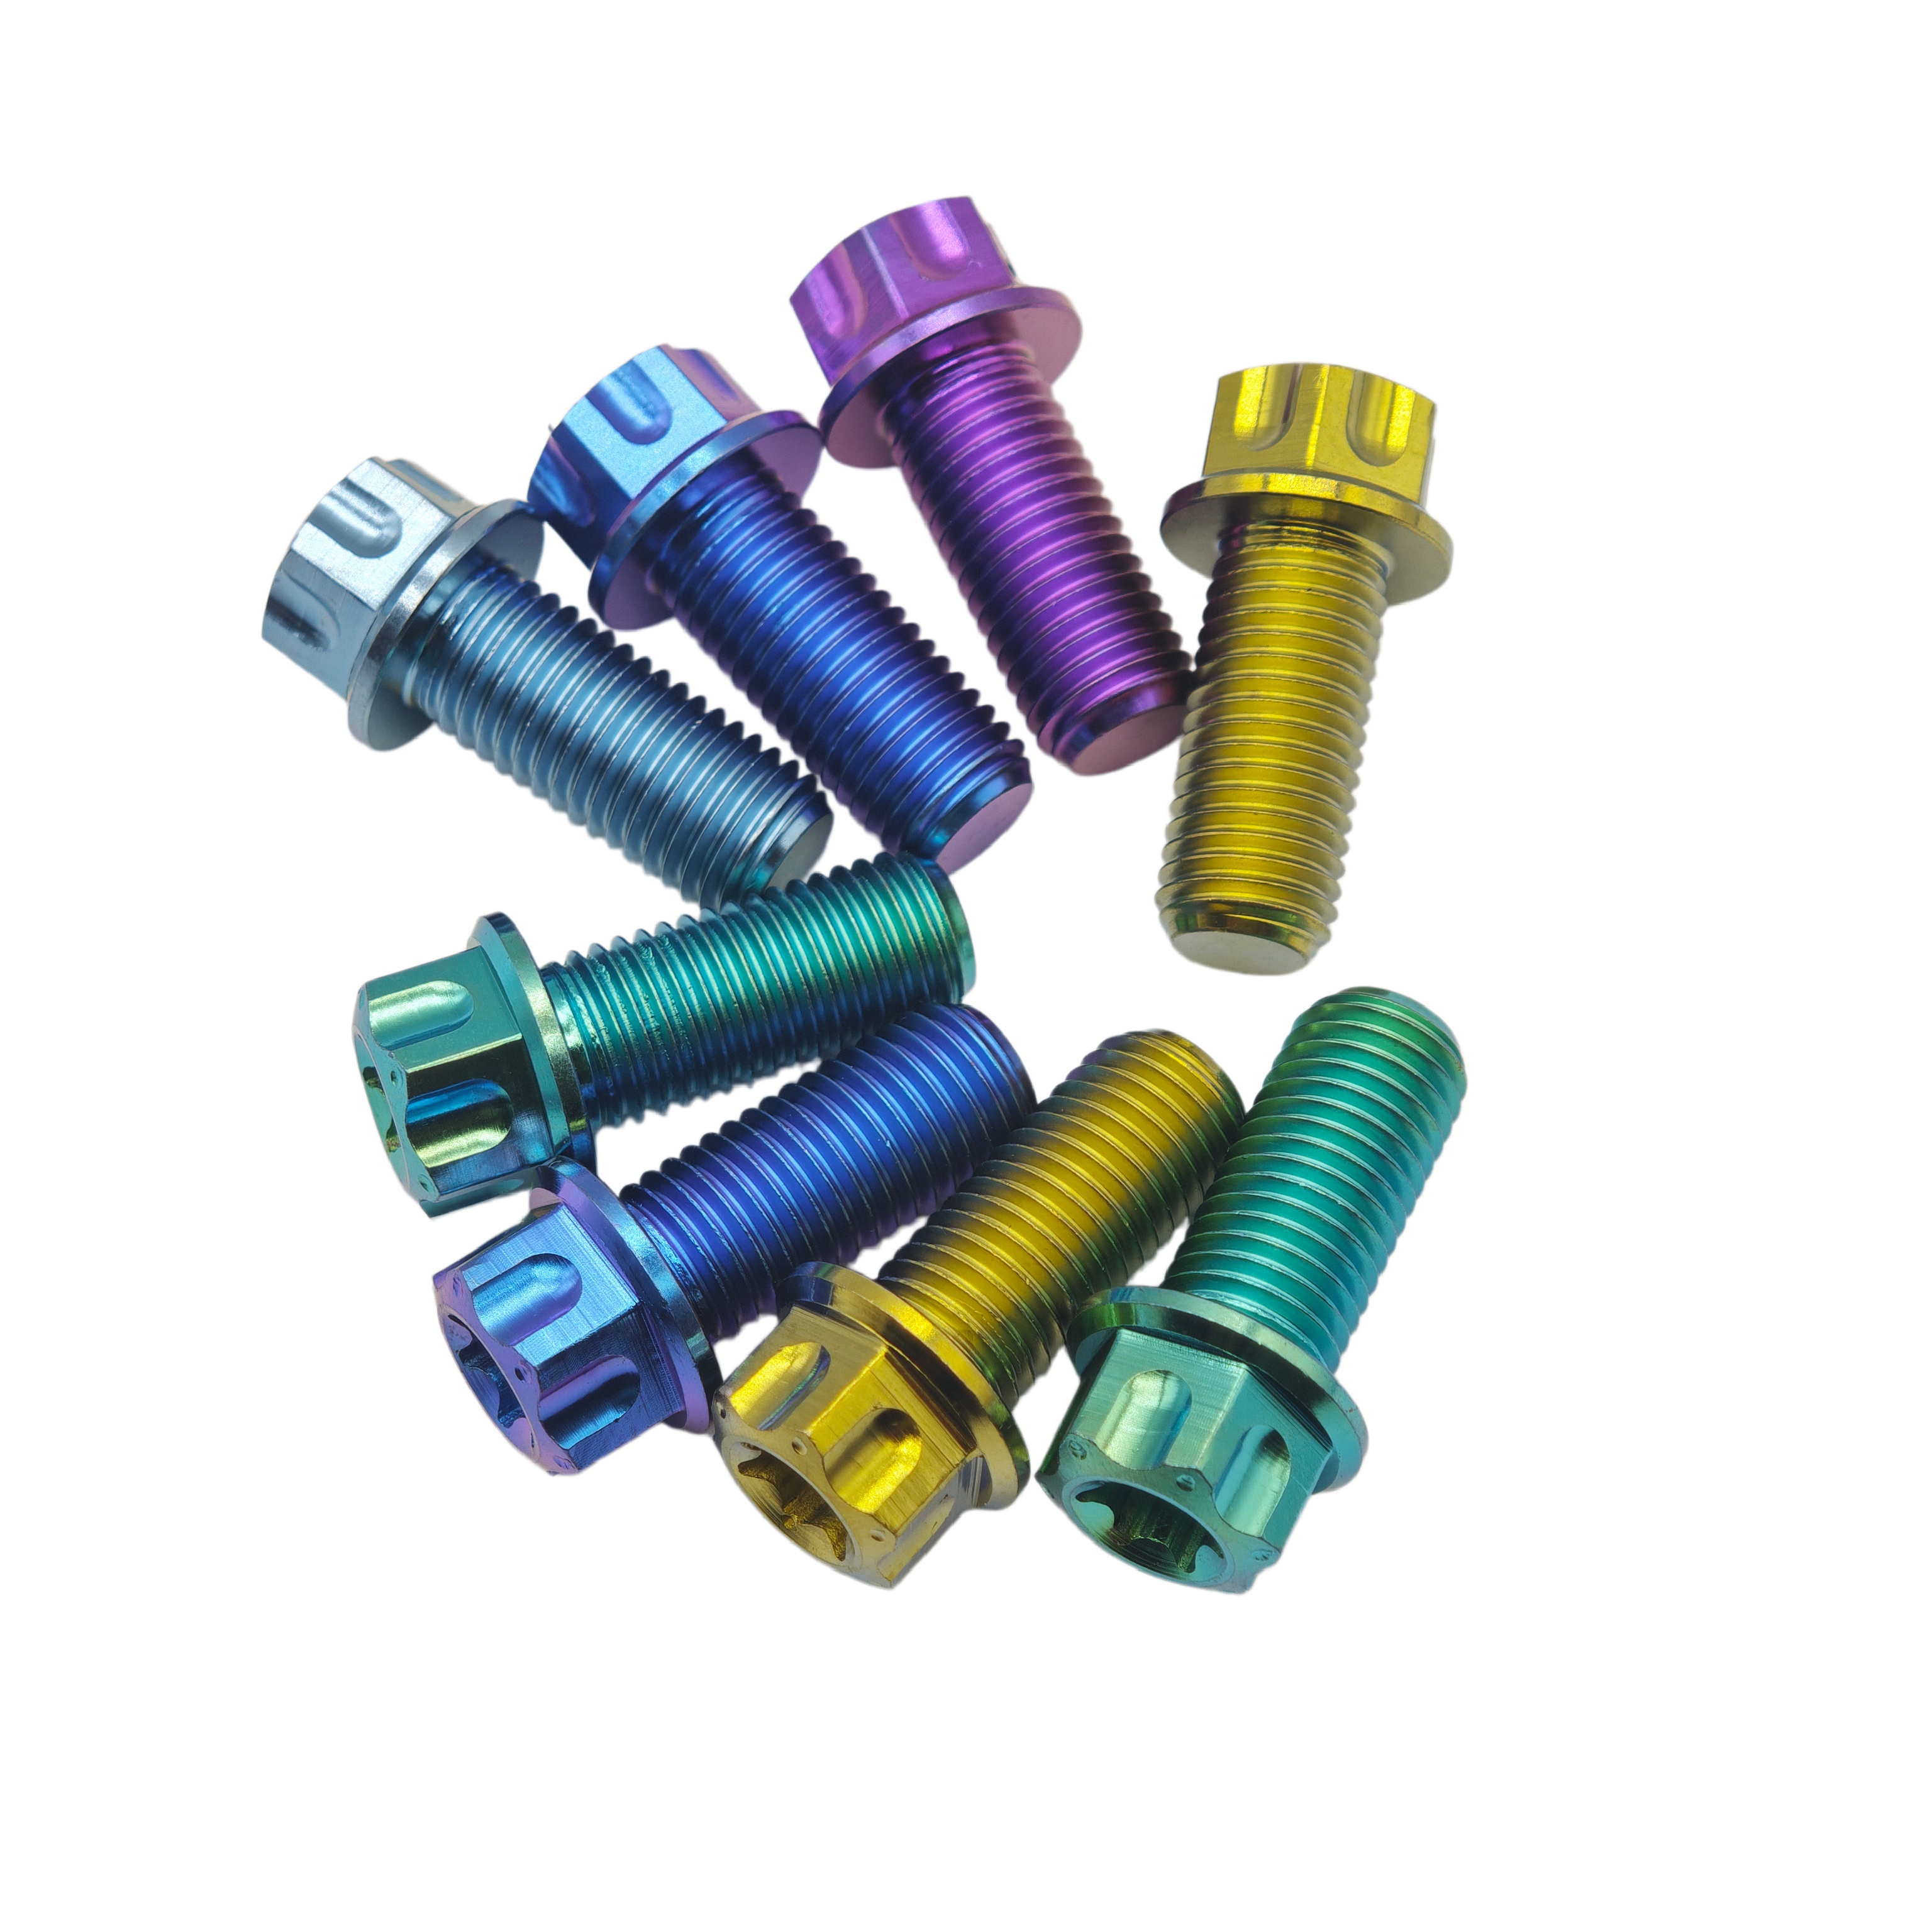
Factory Wholesale Anodized GR5 Titanium Hex Flange Bolts
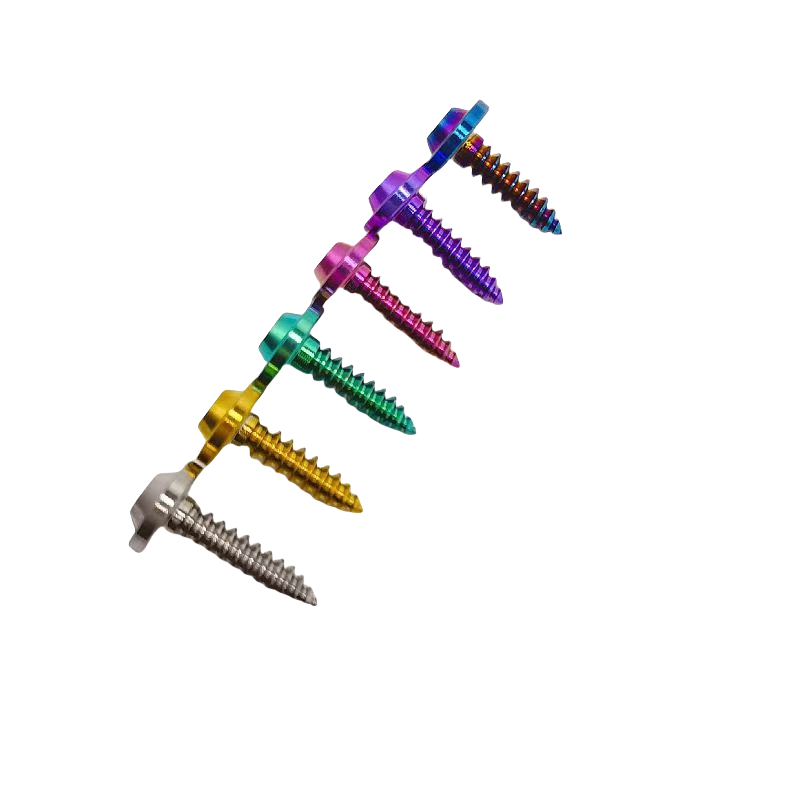
M4/M5 Blue-Grey Titanium Pan Head Self-Tapping Screws
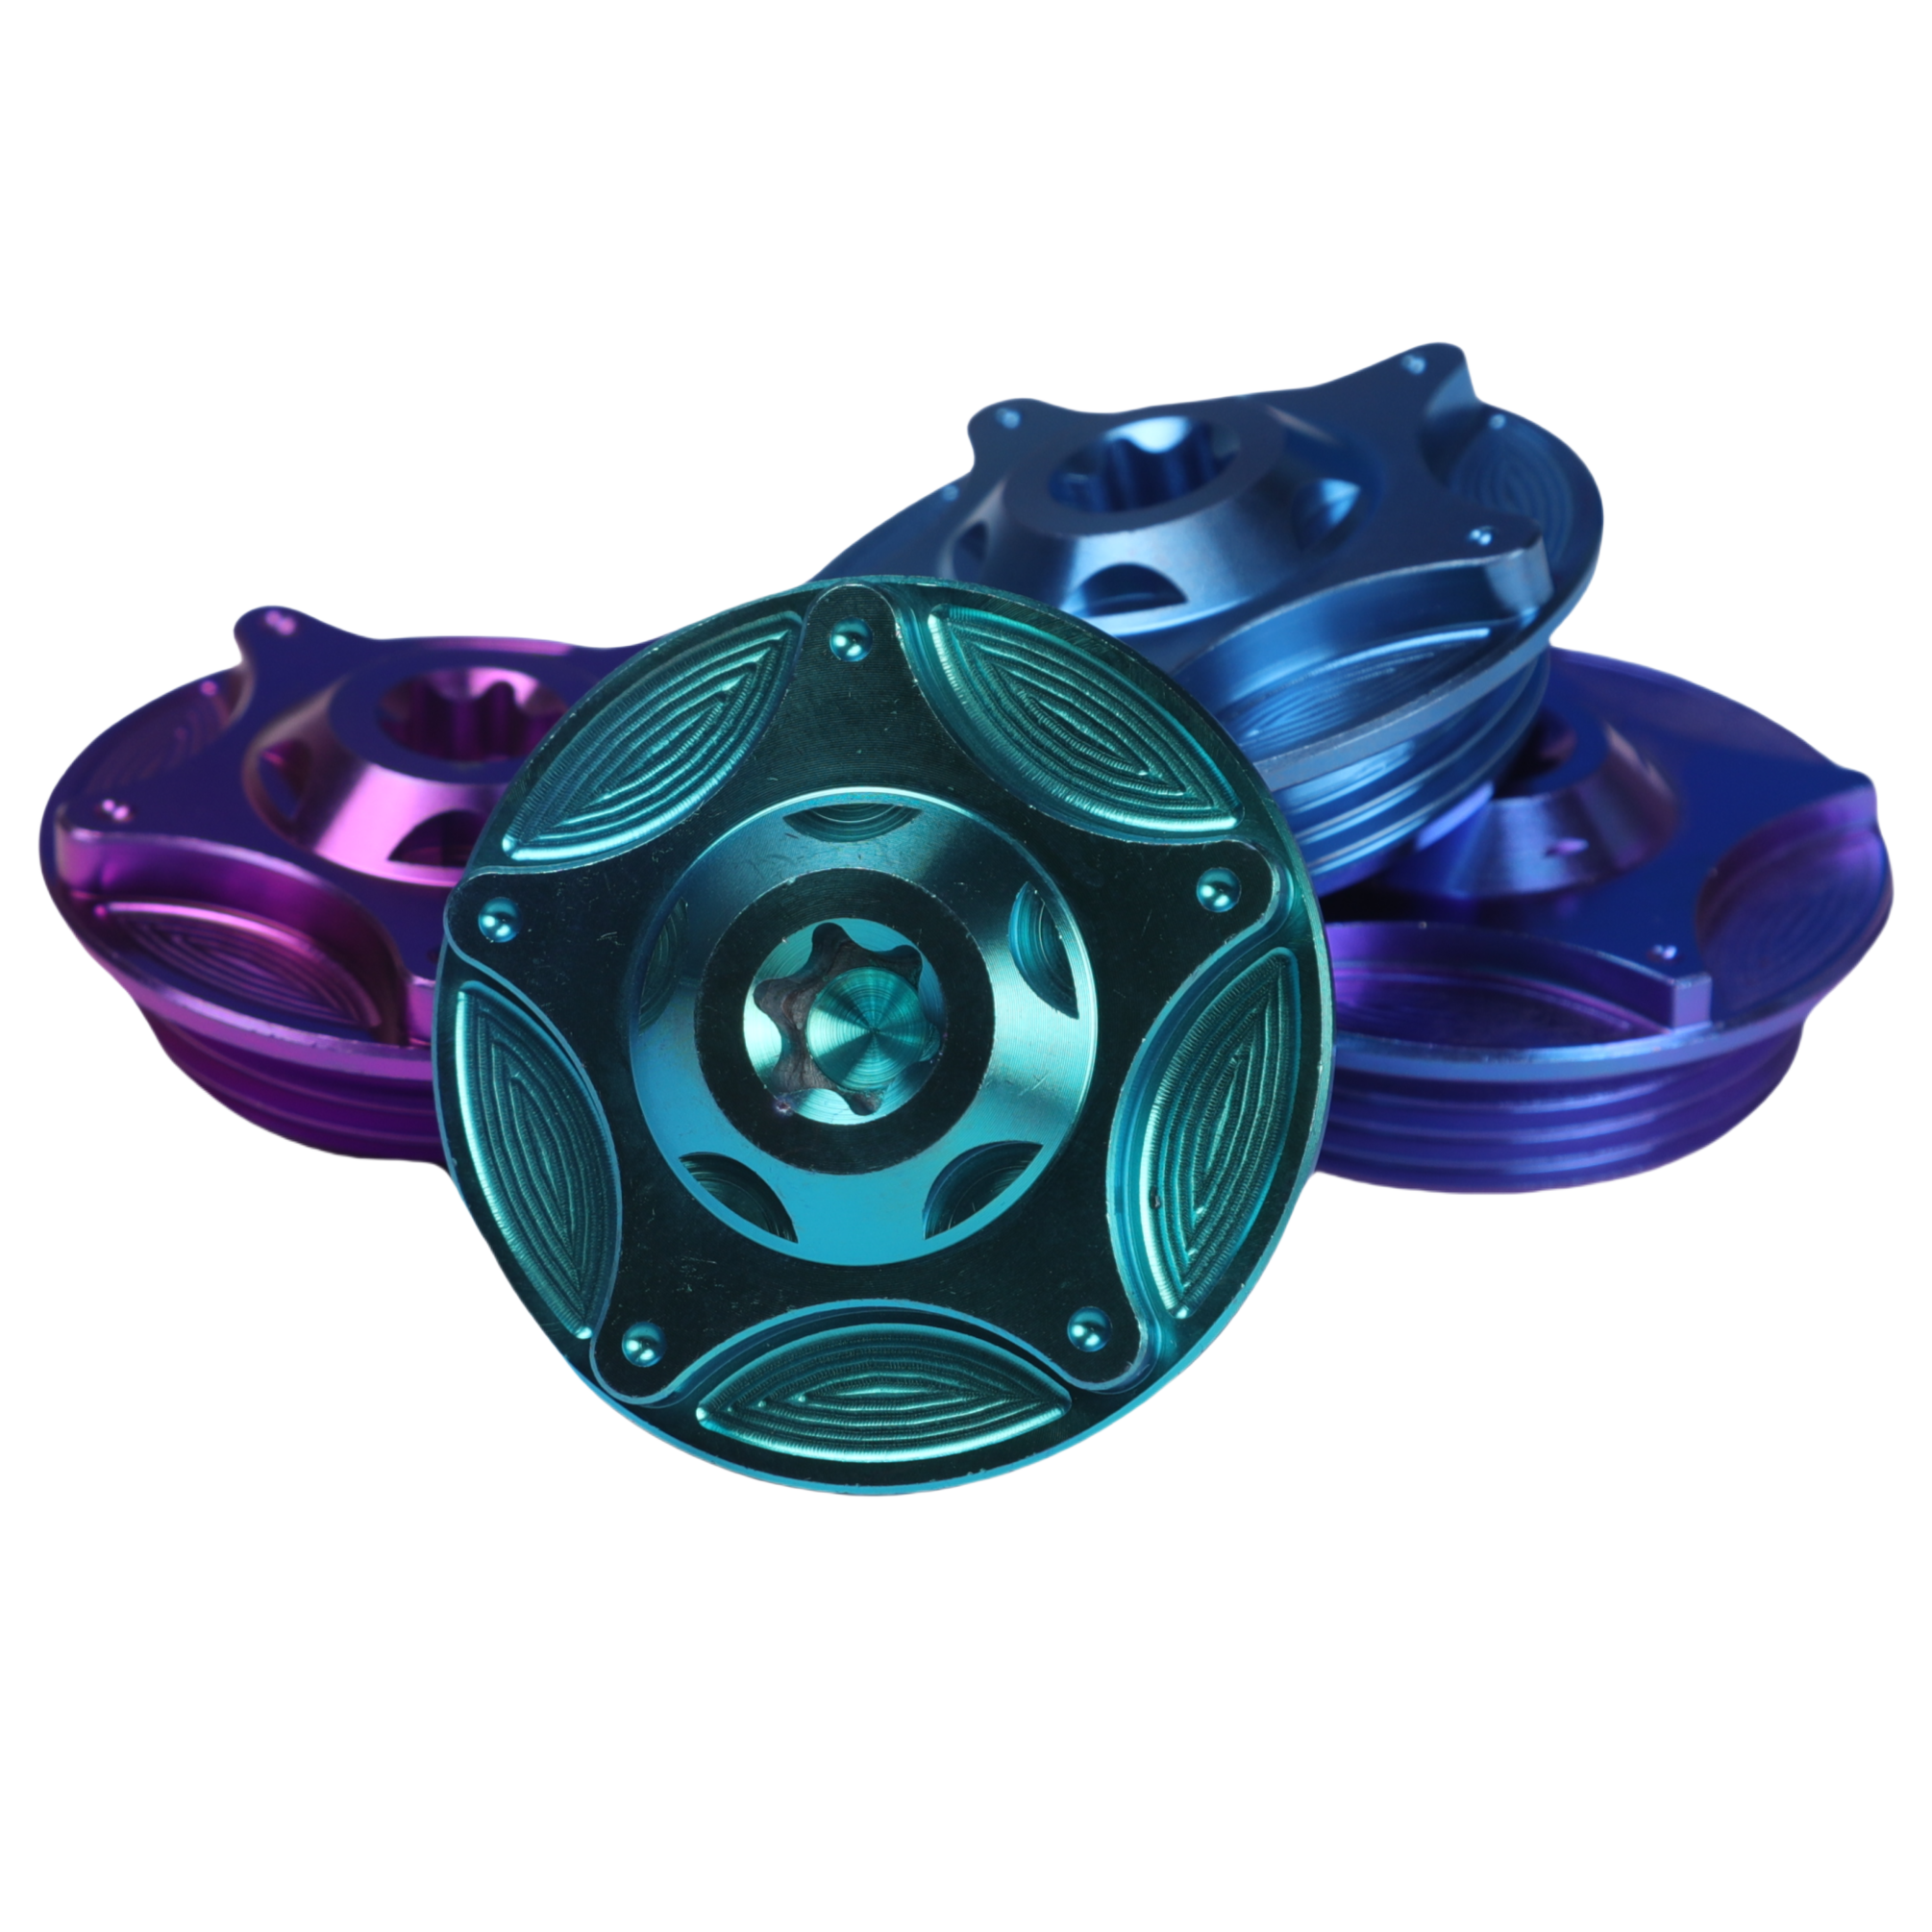
High-Strength Customized M31 Super-Light Anti-Skid Cap
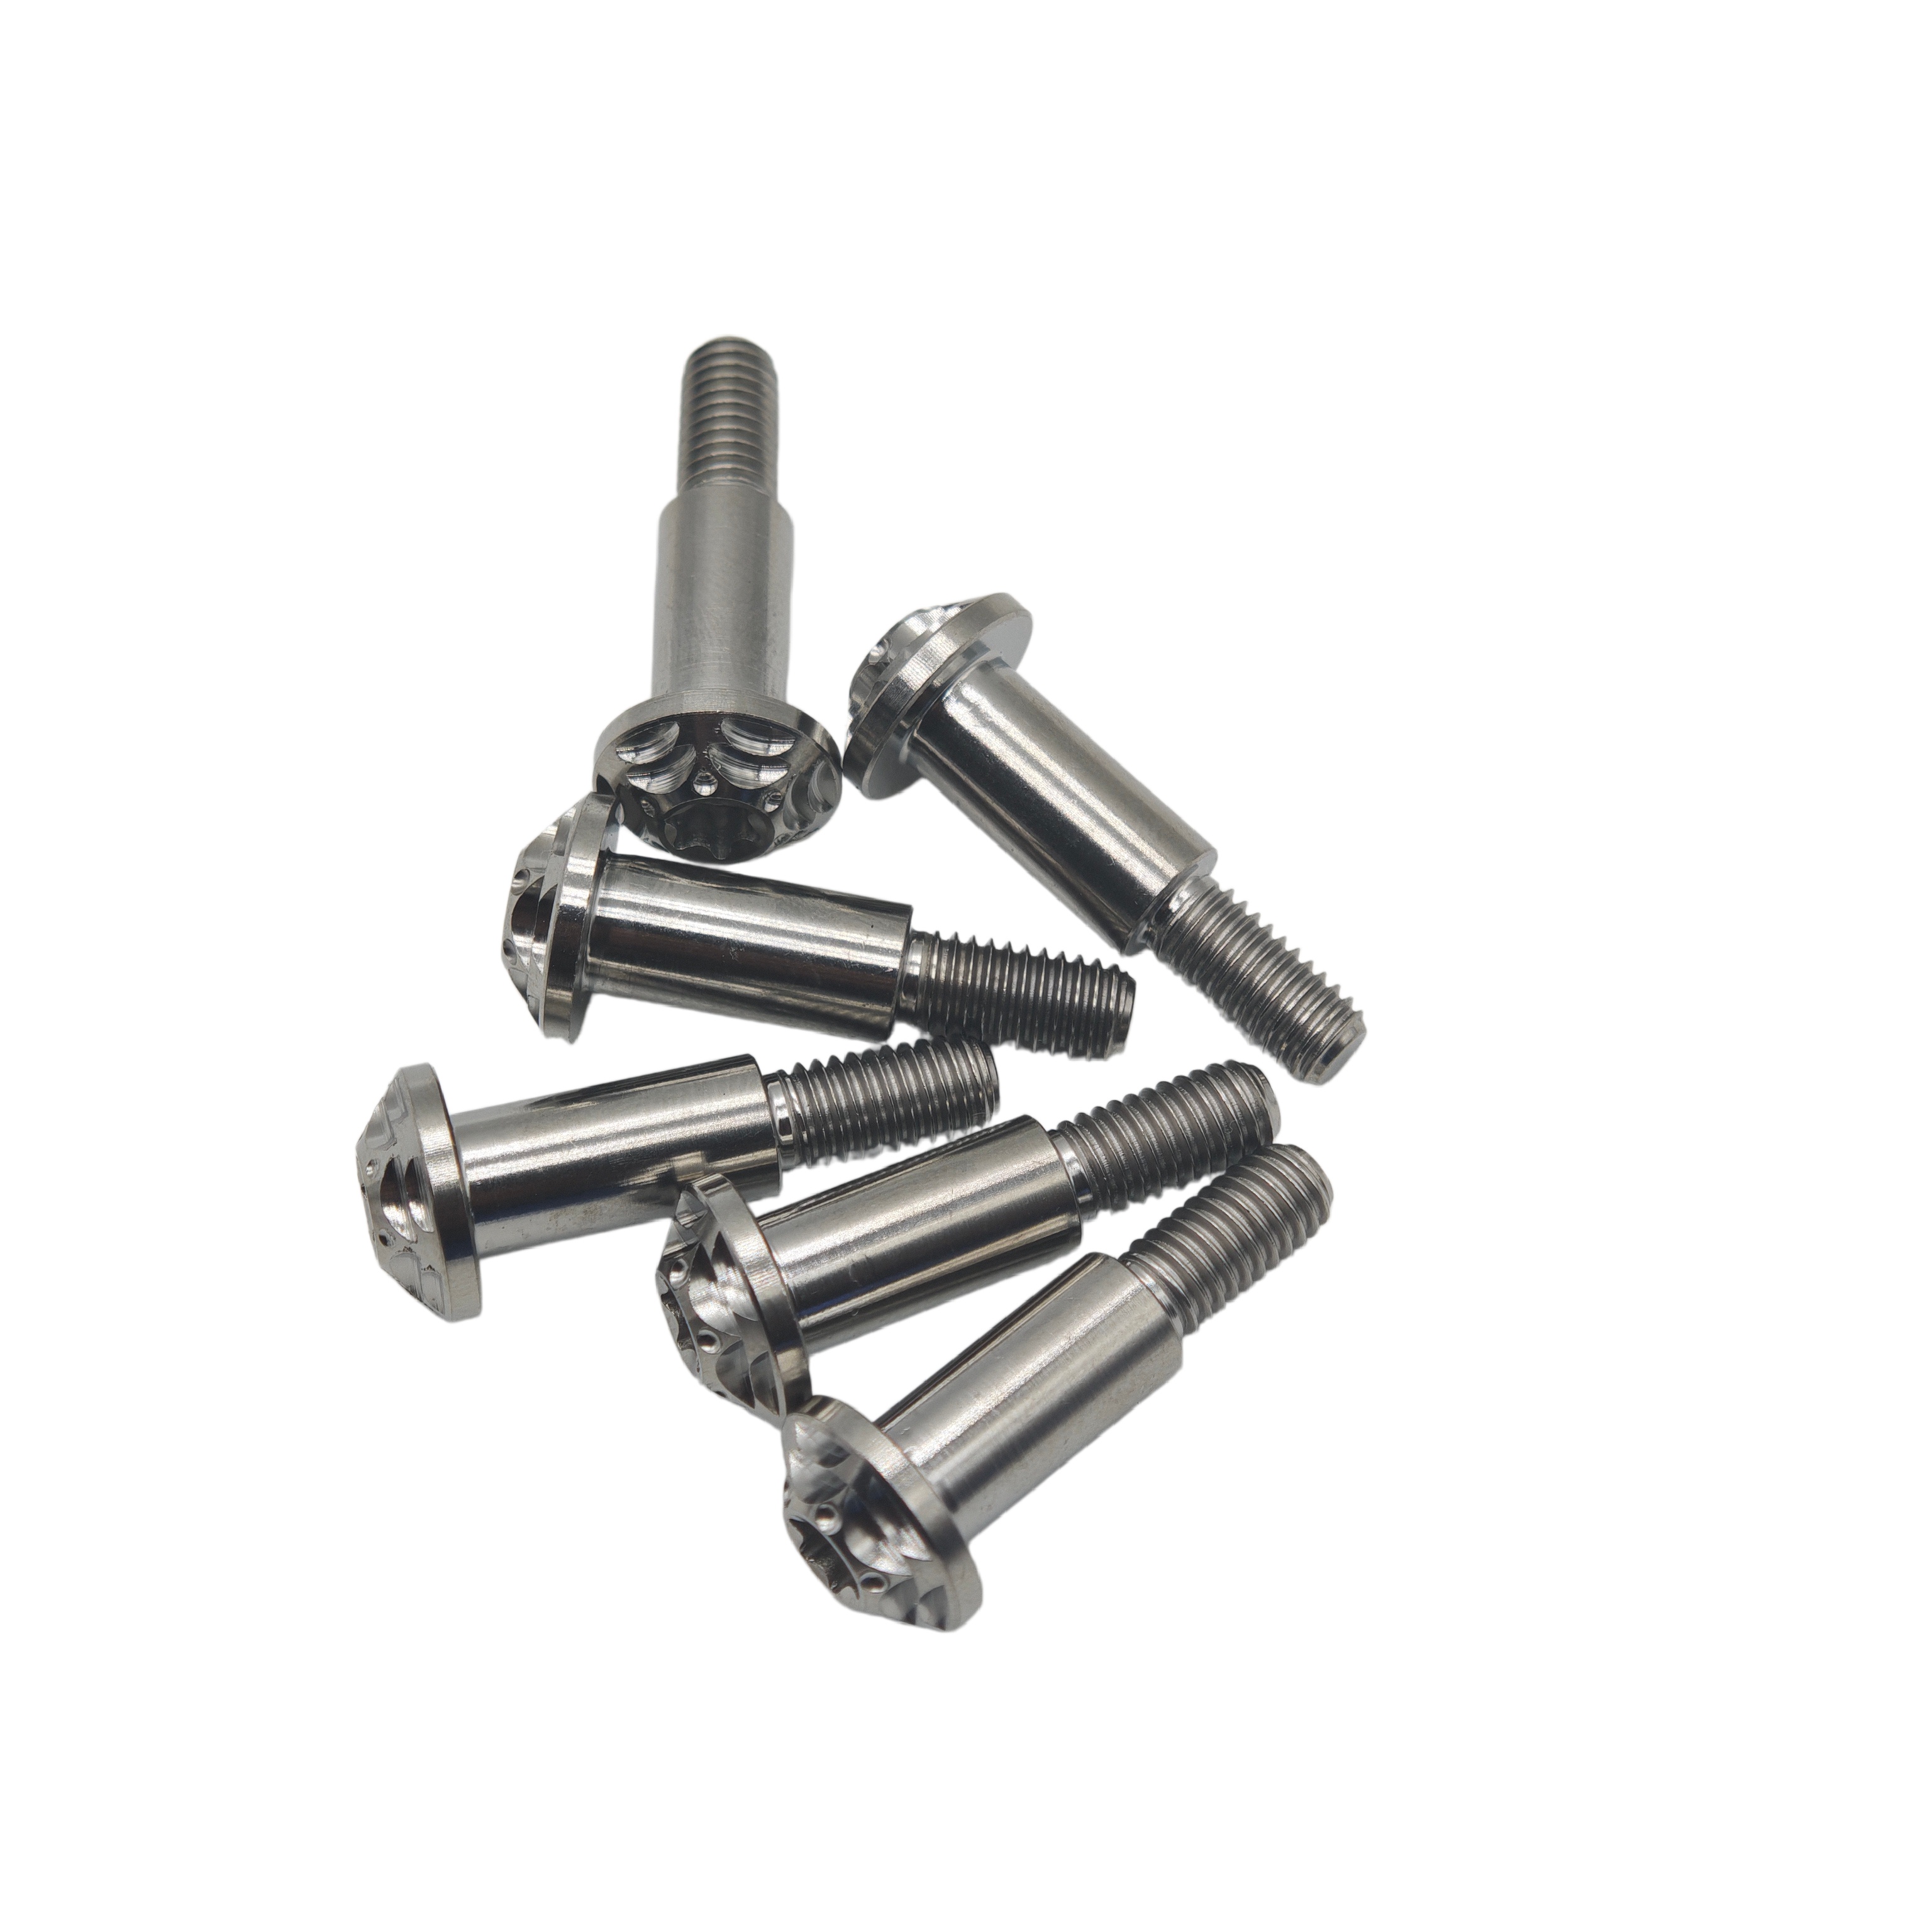
Custom Torx Shoulder Screw CNC Machined GR5 Socket Bolt
Industrial Mechanics: Why Berlin Engineering Demands Ti-6Al-4V Grade 5 Cap Screws
An authoritative technical review on replacing standard DIN 912 Class 8.8, 10.9, and A2/A4 stainless steel screws with vacuum-melted alpha-beta alloy titanium in high-stress dynamic assemblies.
In mechanical systems operating within the Berlin metropolitan industrial and research corridors, component design constraints have shifted permanently toward high-efficiency payload optimization, electrochemical compatibility with Carbon-Fiber Reinforced Polymers (CFRP), and total resistance against de-icing salts and harsh urban atmospheric conditions. Hexagon socket head cap screws (DIN 912 / ISO 4762) form the structural backbone of mechanical assemblies. When produced from certified Grade 5 Titanium (Ti-6Al-4V, Werkstoff 3.7165, UNS R56400), these fasteners achieve an extraordinary strength-to-density ratio exceeding 200 kN·m/kg—vastly surpassing austenitic stainless steels (A2-70, A4-80) and outperforming quench-and-tempered alloy structural steels under cyclic fatigue loading.
Mechanical Properties: Grade 5 Titanium vs. Standard Fastener Alloys
Verified laboratory test metrics based on ASTM B348, ASTM F467/F468, and DIN EN ISO 898-1 specifications.
| Material Designation | Ti-6Al-4V Grade 5 (Zunvo) | A4-80 Stainless (1.4404) | Alloy Steel 10.9 (34CrMo4) | Aluminum 7075-T6 |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 | 8.00 | 7.85 | 2.81 |
| Ultimate Tensile Strength (Rm, MPa) | ≥ 950 - 1050 | ≥ 800 | ≥ 1040 | ≥ 540 |
| Yield Strength (Rp 0.2, MPa) | ≥ 880 - 920 | ≥ 600 | ≥ 940 | ≥ 480 |
| Modulus of Elasticity (GPa) | 114 | 193 | 210 | 72 |
| Specific Strength (kN·m/kg) | 214.4 | 100.0 | 132.5 | 192.1 |
| CFRP Galvanic Corrosion Potential | Immune (Close Potential) | Acceptable in dry conditions | Severe Galvanic Attack | Catastrophic Pitting |
| Operational Temperature Range | -250°C to +420°C | -196°C to +350°C | -50°C to +200°C | -50°C to +120°C |
Thread Integrity via Cold Rolling vs. Cut Threads: Zunvo Titanium exclusively employs thread rolling for all socket cap screws destined for critical German industrial applications. Unlike traditional lathe-turned or chip-cut threads which interrupt the alloy's crystalline grain structure, cold thread rolling plastically deforms the Grade 5 grain boundaries, orienting them along the root contours of the thread. This inducing of beneficial compressive residual stress across the thread roots enhances cyclic fatigue life by more than 300%, eliminating stress riser micro-cracks under dynamic vibrations commonly experienced in Berlin rail transit and e-mobility drive shafts.
Localized Application Scenarios Across Berlin & Brandenburg
From academic spin-offs in Berlin-Adlershof to high-throughput electric vehicle manufacturing corridors in the surrounding Brandenburg region, titanium cap screws serve mission-critical roles.
WISTA Adlershof: Aerospace & Optical Instrumentation
Berlin-Adlershof hosts Germany's preeminent technology park where microsatellite manufacturers, synchrotrons, and quantum optical sensor developers require non-magnetic fasteners with negligible thermal expansion coefficient (8.6 × 10⁻⁶ /K) to maintain optical alignment in ultra-high vacuum (UHV) chambers.
- Non-magnetic permeability (µr < 1.00005)
- Zero outgassing under orbital vacuum conditions
E-Mobility & Automotive Prototyping (Berlin-Brandenburg)
The rapid industrialization of the Berlin-Brandenburg corridor has established an epicenter for electric powertrain development. Our DIN 912 titanium cap screws are deployed directly in lightweight structural battery enclosures, inverter heat-sink clamp assemblies, and high-performance electric superbike suspension pivots.
- High vibration dampening capacity (Q⁻¹)
- Galvanic isolation when threaded into carbon tubs
HealthCapital Berlin-Buch: Surgical Robotics & Cleanroom Automation
Berlin's medical technology sector relies on biocompatible, autoclavable fasteners that withstand repeated cycle sterilization with superheated steam, hydrogen peroxide plasma, and caustic disinfectants without surface pitting or chemical degradation.
- Inert titanium oxide passivation layer (TiO₂)
- ISO Class 5 cleanroom ultrasonic pre-degreasing
Procurement Trends & European Supply Chain Resilience
How German engineering standards (DIN), the EU Green Deal, and supply-chain due diligence laws (LkSG) are transforming fastener sourcing for Berlin OEMs.
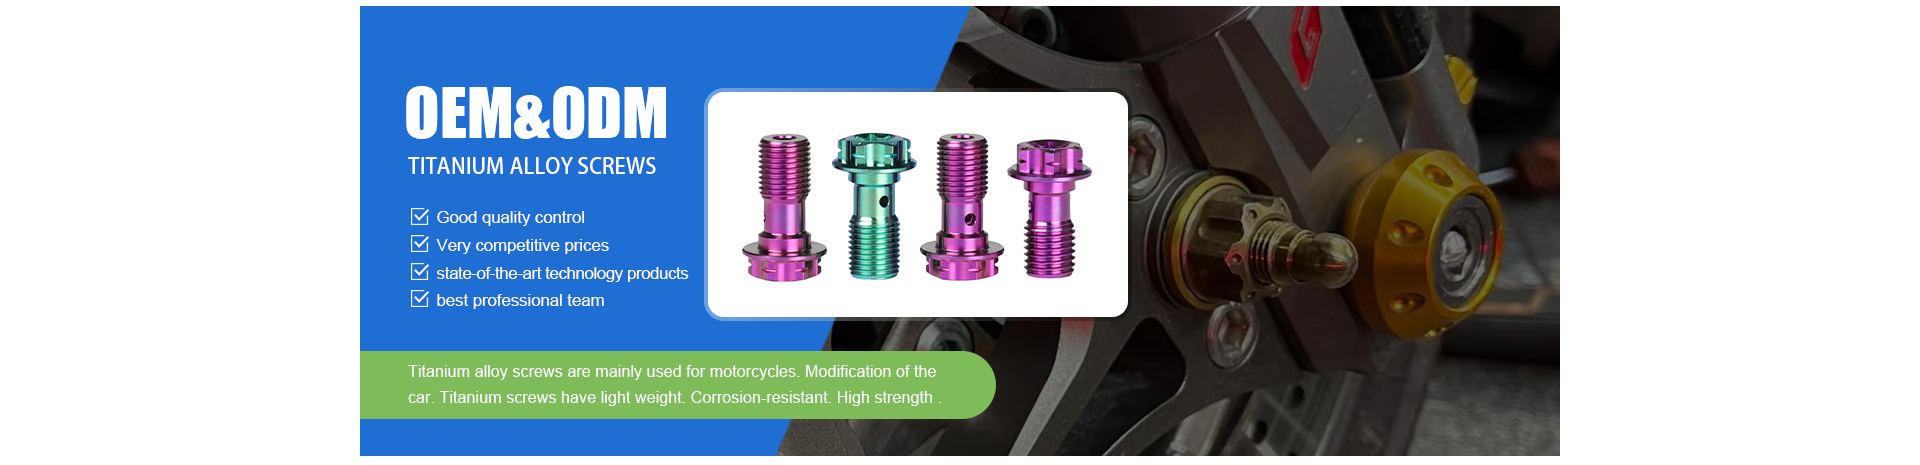
Strict DIN 912 / ISO 4762 Geometric Tolerancing
Berlin engineering teams adhere strictly to Deutsches Institut für Normung (DIN) tolerances. Our automated multi-axis Swiss CNC equipment yields pitch diameters within 6g external thread tolerances, ensuring friction-free engagement in tapped blind holes without binding.
Full EU REACH & RoHS Environmental Compliance
Every fastener shipped into Germany complies fully with Regulation (EC) No 1907/2006 (REACH) and Directive 2011/65/EU (RoHS). Free of lead, cadmium, and hexavalent chromium (CrVI), accompanied by certified lab analysis documentation.
Direct Air Logistics to Berlin Brandenburg Airport (BER)
Through dedicated express freight agreements with DHL Express and FedEx, customs-cleared consignments land directly at BER within 3 to 5 business days from final production sign-off, bypassing congested sea freight bottlenecks.
Why Berlin Enterprises Partner With Zunvo Titanium Co., Ltd.
Headquartered in Baoji, China's internationally renowned "Titanium Valley", Zunvo Titanium delivers full vertically integrated production from certified sponge melting to finished high-tensile hardware.
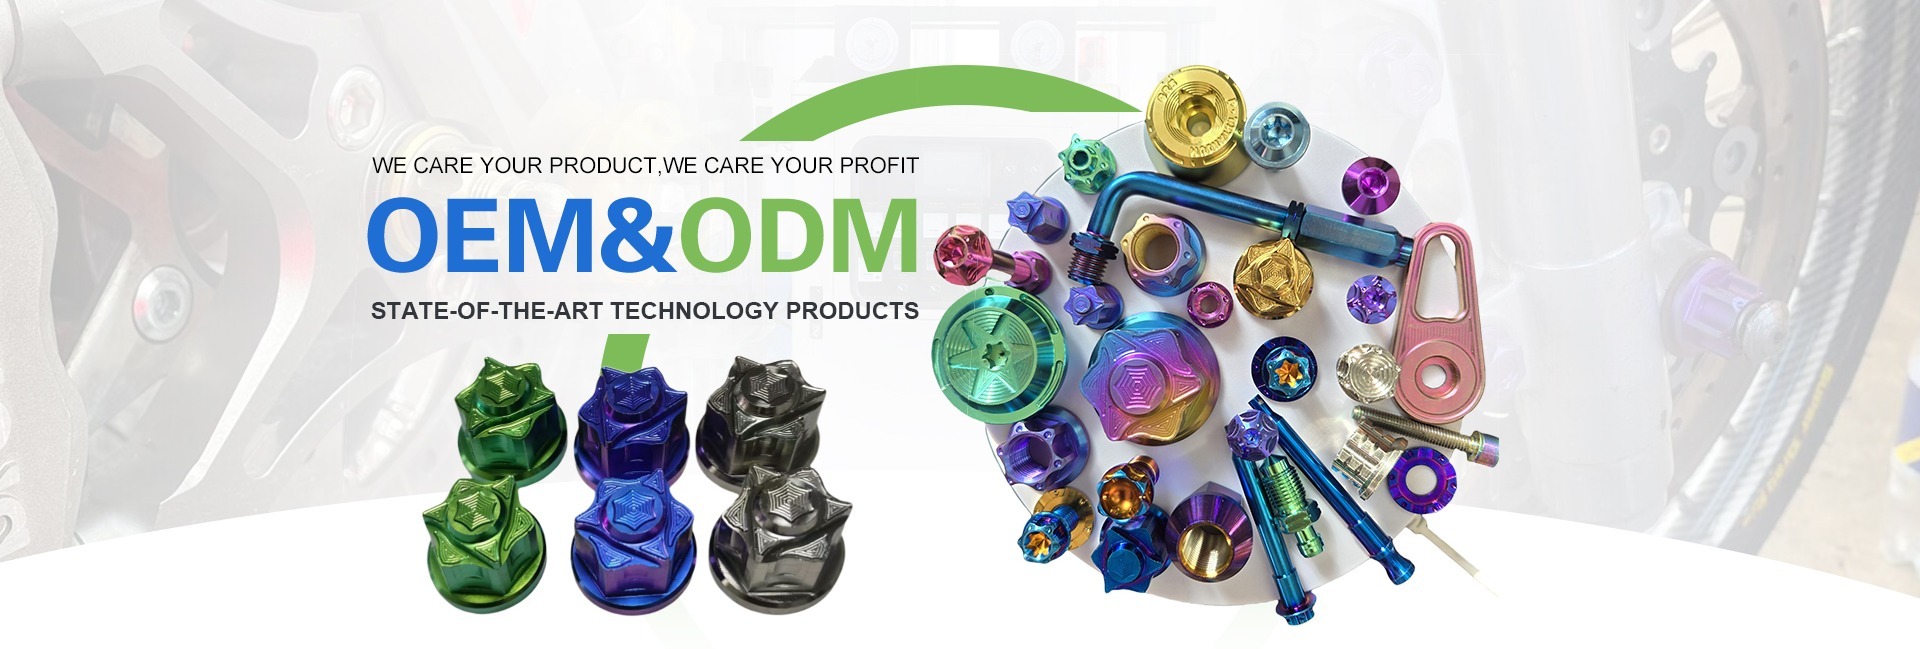
Complete Heat Number Traceability & EN 10204 3.1 MTR
We source raw Ti-6Al-4V exclusively from Tier-1 certified titanium smelters. Each production lot is coded by heat number, backed by mill test certificates (MTR) specifying exact chemical composition (O, Fe, C, N, H gas limits) and physical mechanical yields.
Rapid 3-Day Prototyping for R&D Centers
Understanding the agile design cycles of Berlin startups, our rapid-response tooling bay delivers custom CAD/STEP prototype screws in as few as 72 hours, with volume production ramp-up executed in 7 to 15 business days.
Advanced Surface Finishing: PVD & Type II Anodizing
In addition to raw mechanical polishing, we operate in-house automated micro-arc anodizing and physical vapor deposition (PVD) chambers to apply Titanium Nitride (Gold TiN), DLC (Diamond-Like Carbon), and rainbow interference coatings with micro-hardness reaching HV 2200.
Frequently Asked Questions by Berlin Engineers & Buyers
Detailed answers covering customs clearance into Germany, installation torque specifications, galling prevention, and certified test documentation.
How do you handle German customs clearance (Zollabfertigung) and import VAT (EUST)?
We routinely supply German industrial clients under DDP (Delivered Duty Paid) terms via our international freight partners (DHL Express / DB Schenker). In this scenario, all export customs, air transit, German customs clearance via the Hauptzollamt, and standard EU import tariffs are settled upfront, delivering goods directly to your facility in Berlin or Brandenburg without administrative delay. Alternatively, for corporate buyers with an existing EORI number seeking FOB or DAP terms, we provide accurate HS codes (typically 8108.90 for titanium structural articles or 7318 for threaded hardware) along with commercial invoices and packing lists.
Can Grade 5 titanium cap screws directly replace 10.9 or 12.9 grade steel bolts?
Grade 5 (Ti-6Al-4V) provides a minimum tensile yield of 895–950 MPa, making it a direct replacement for Class 8.8 and Class 10.9 structural steel fasteners while cutting weight by ~44%. However, for extreme applications specified for Class 12.9 (tensile strength ≥ 1220 MPa), direct 1:1 replacement is only permissible if our engineering review confirms that the joint's shear and clamping loads fall within Grade 5 parameters. If required, we can also machine fasteners from Grade 23 (Ti-6Al-4V ELI) or specialized beta-alloys (such as Ti-10V-2Fe-3Al) designed for ultra-high-strength aerospace service.
How do we prevent thread galling (Kaltverschweißung) when installing titanium cap screws?
Titanium possesses an oxide film (TiO₂) that can gall under dry high-pressure friction, especially when mating with titanium female threads or stainless steel inserts. To eliminate galling and achieve uniform bolt preload, we recommend applying an anti-seize lubricant (molybdenum disulfide MoS₂, copper paste, or synthetic PTFE-based ceramic assembly grease). Lubrication stabilizes the friction coefficient between µ = 0.10 and 0.15. For extreme cleanroom or aerospace applications where wet lubricants are forbidden, we provide dry-film MoS2 coating or DLC (Diamond-Like Carbon) surface modifications.
Do you provide EN 10204 3.1 Inspection Certificates with production batches?
Yes. Every batch dispatched to European customers is accompanied by a comprehensive EN 10204 Type 3.1 Material Test Report (MTR) directly linked to the melt heat number. This includes optical emission spectrometry (OES) chemical breakdowns, tensile testing data, yield points, elongation percentages, and hardness test figures (HRC / HV). Third-party inspections via TÜV Rheinland or SGS are also supported on project-specific demand.
What is the standard lead time for customized drawings sent from Berlin?
For custom components manufactured from STEP/DWG drawings: our engineering team completes feasibility reviews and provides quotation within 7 hours. Physical prototypes are typically completed and measured via optical coordinate measuring machines (CMM) within 3 business days. Following sample sign-off, volume manufacturing runs (from 500 to 50,000 pieces) require 7 to 15 working days, followed by 3-day express air freight to Berlin.
Ready to Optimize Your Structural Fasteners in Berlin?
Send your CAD files, DIN specifications, or required dimensions to our engineering team. Benefit from certified Grade 5 titanium, rapid CNC prototyping, and guaranteed German-standard compliance.
