Precision Titanium Motorcycle Axle Nuts & Fastener Components
Manufactured strictly from certified Grade 5 Ti-6Al-4V bar stock with rolled metric threads, tight dimensional tolerances (down to ±0.005 mm), and vacuum-deposited PVD or anodized surface finishes.
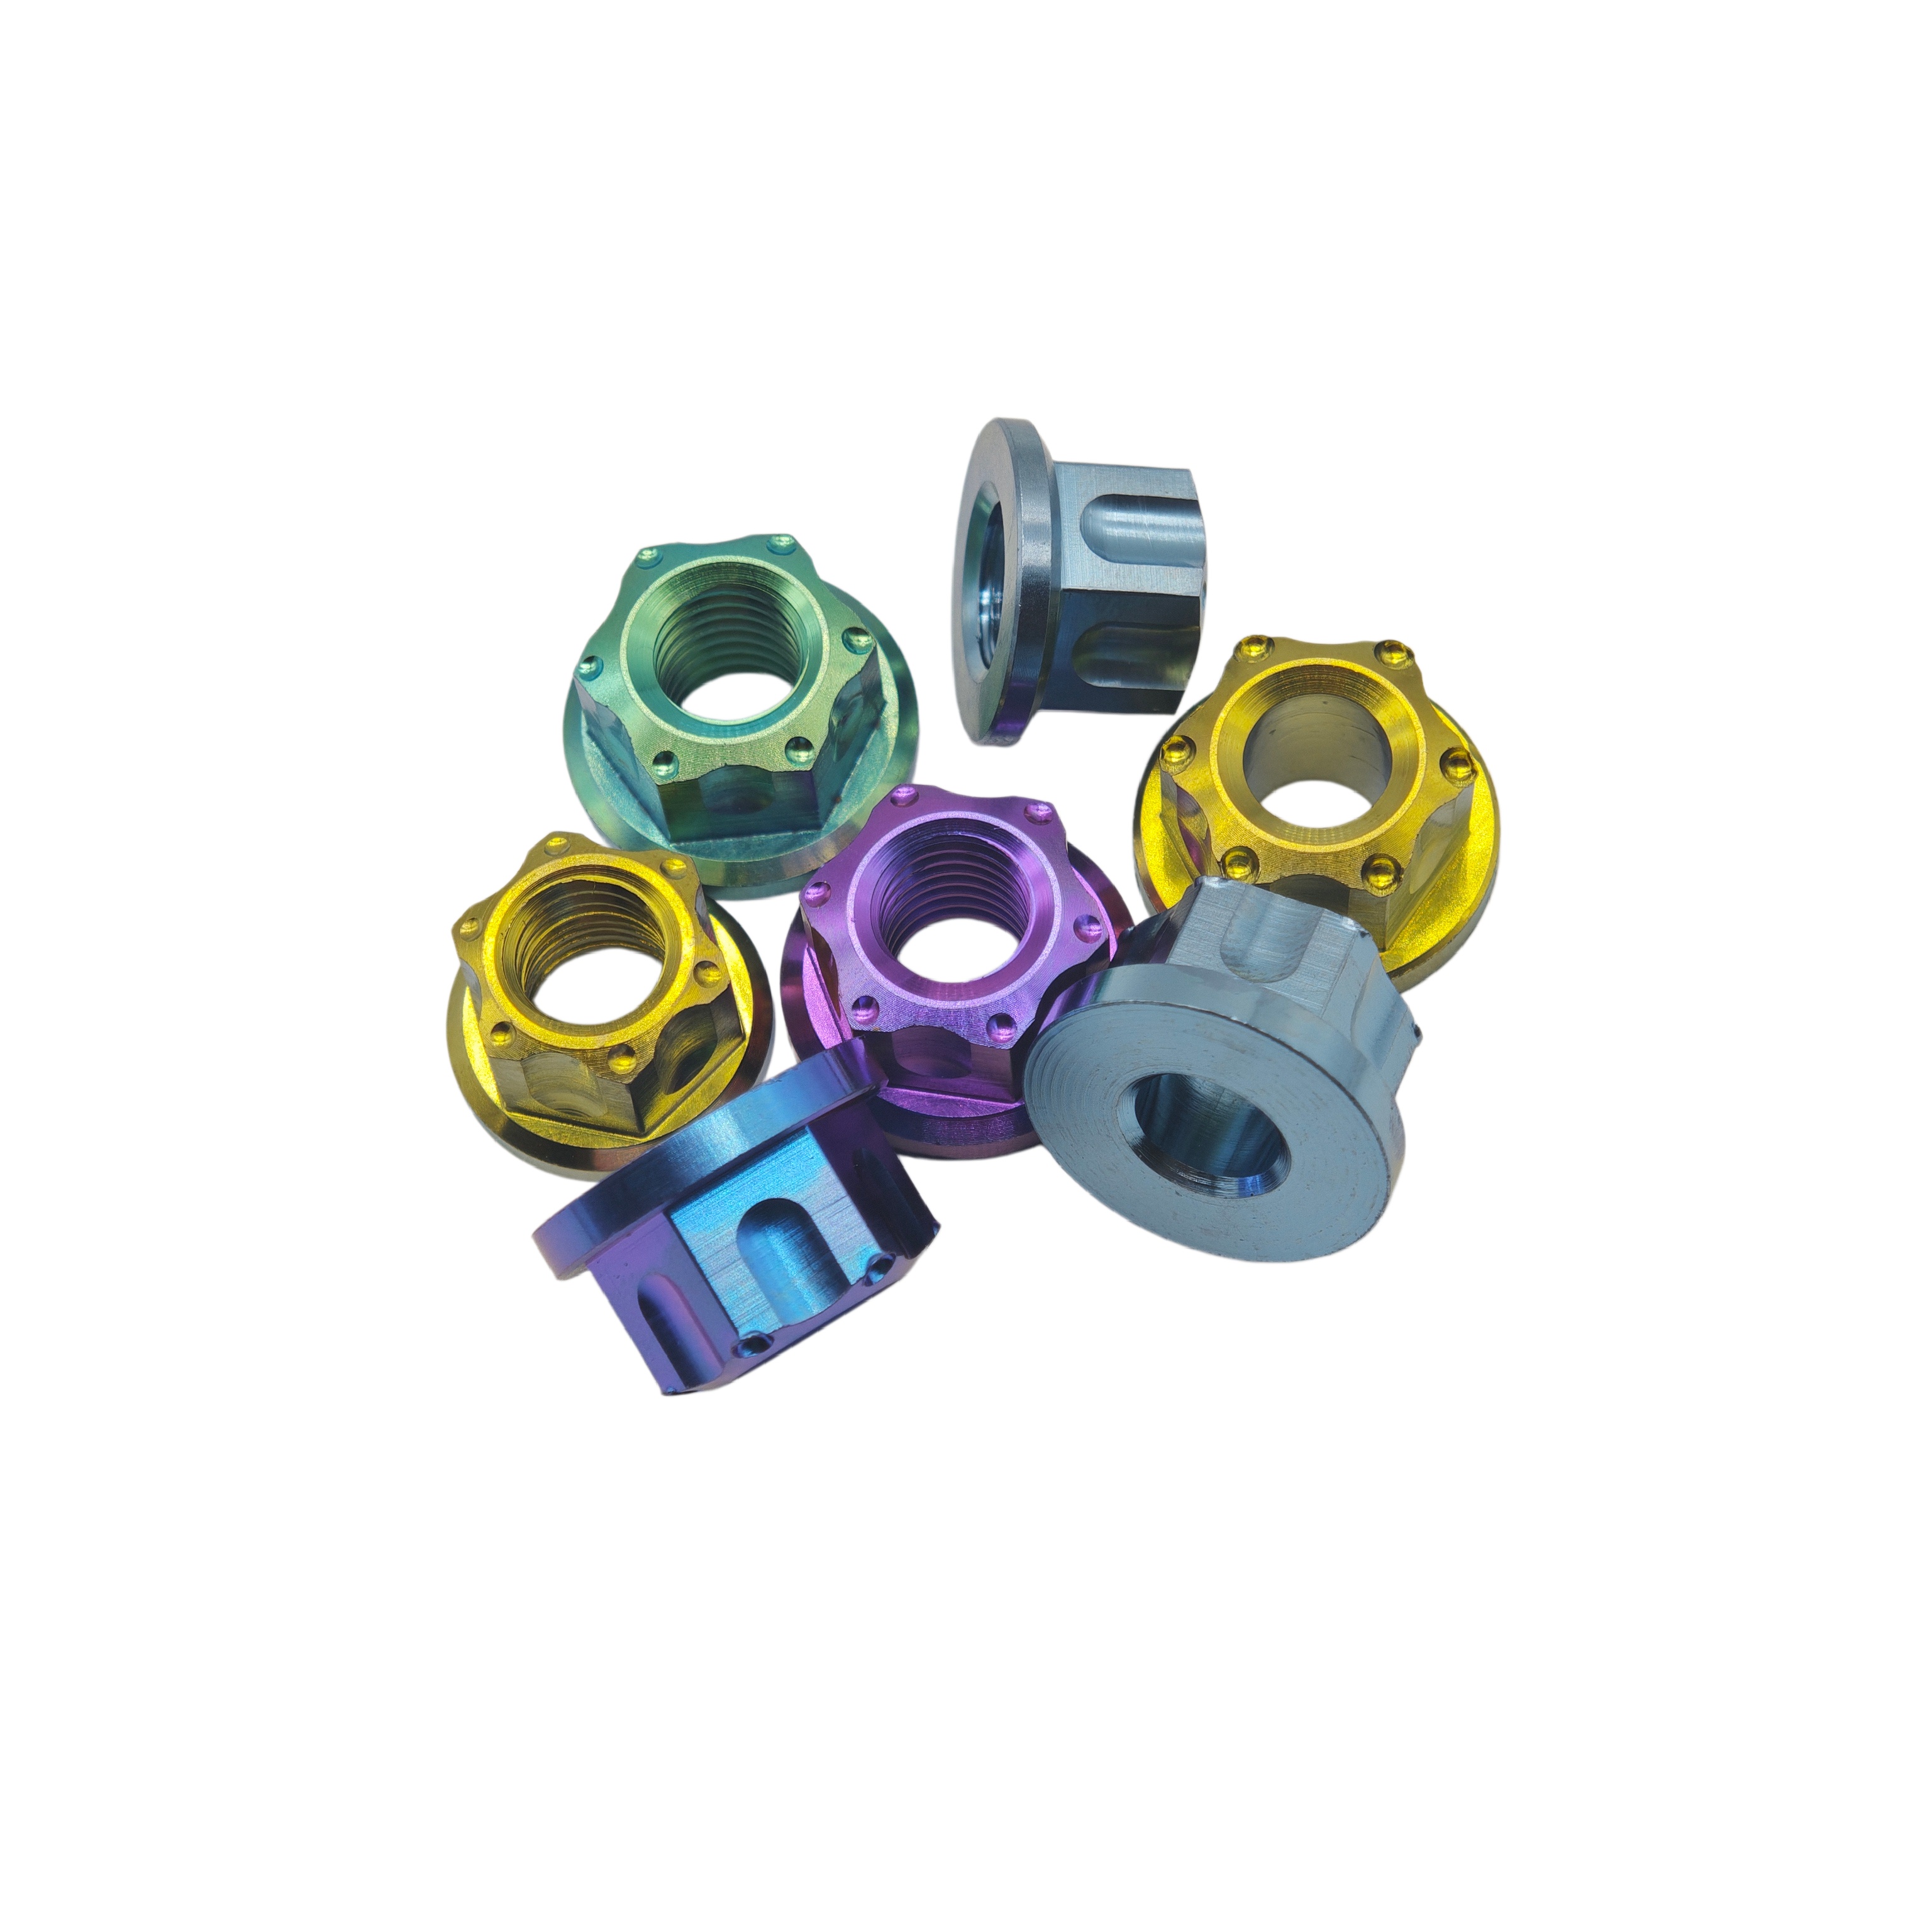
Factory Direct Sales Anodized/Plain Finish Right Hand Thread Gr5 Hexagon Flange Titanium Open Nut M10/M8
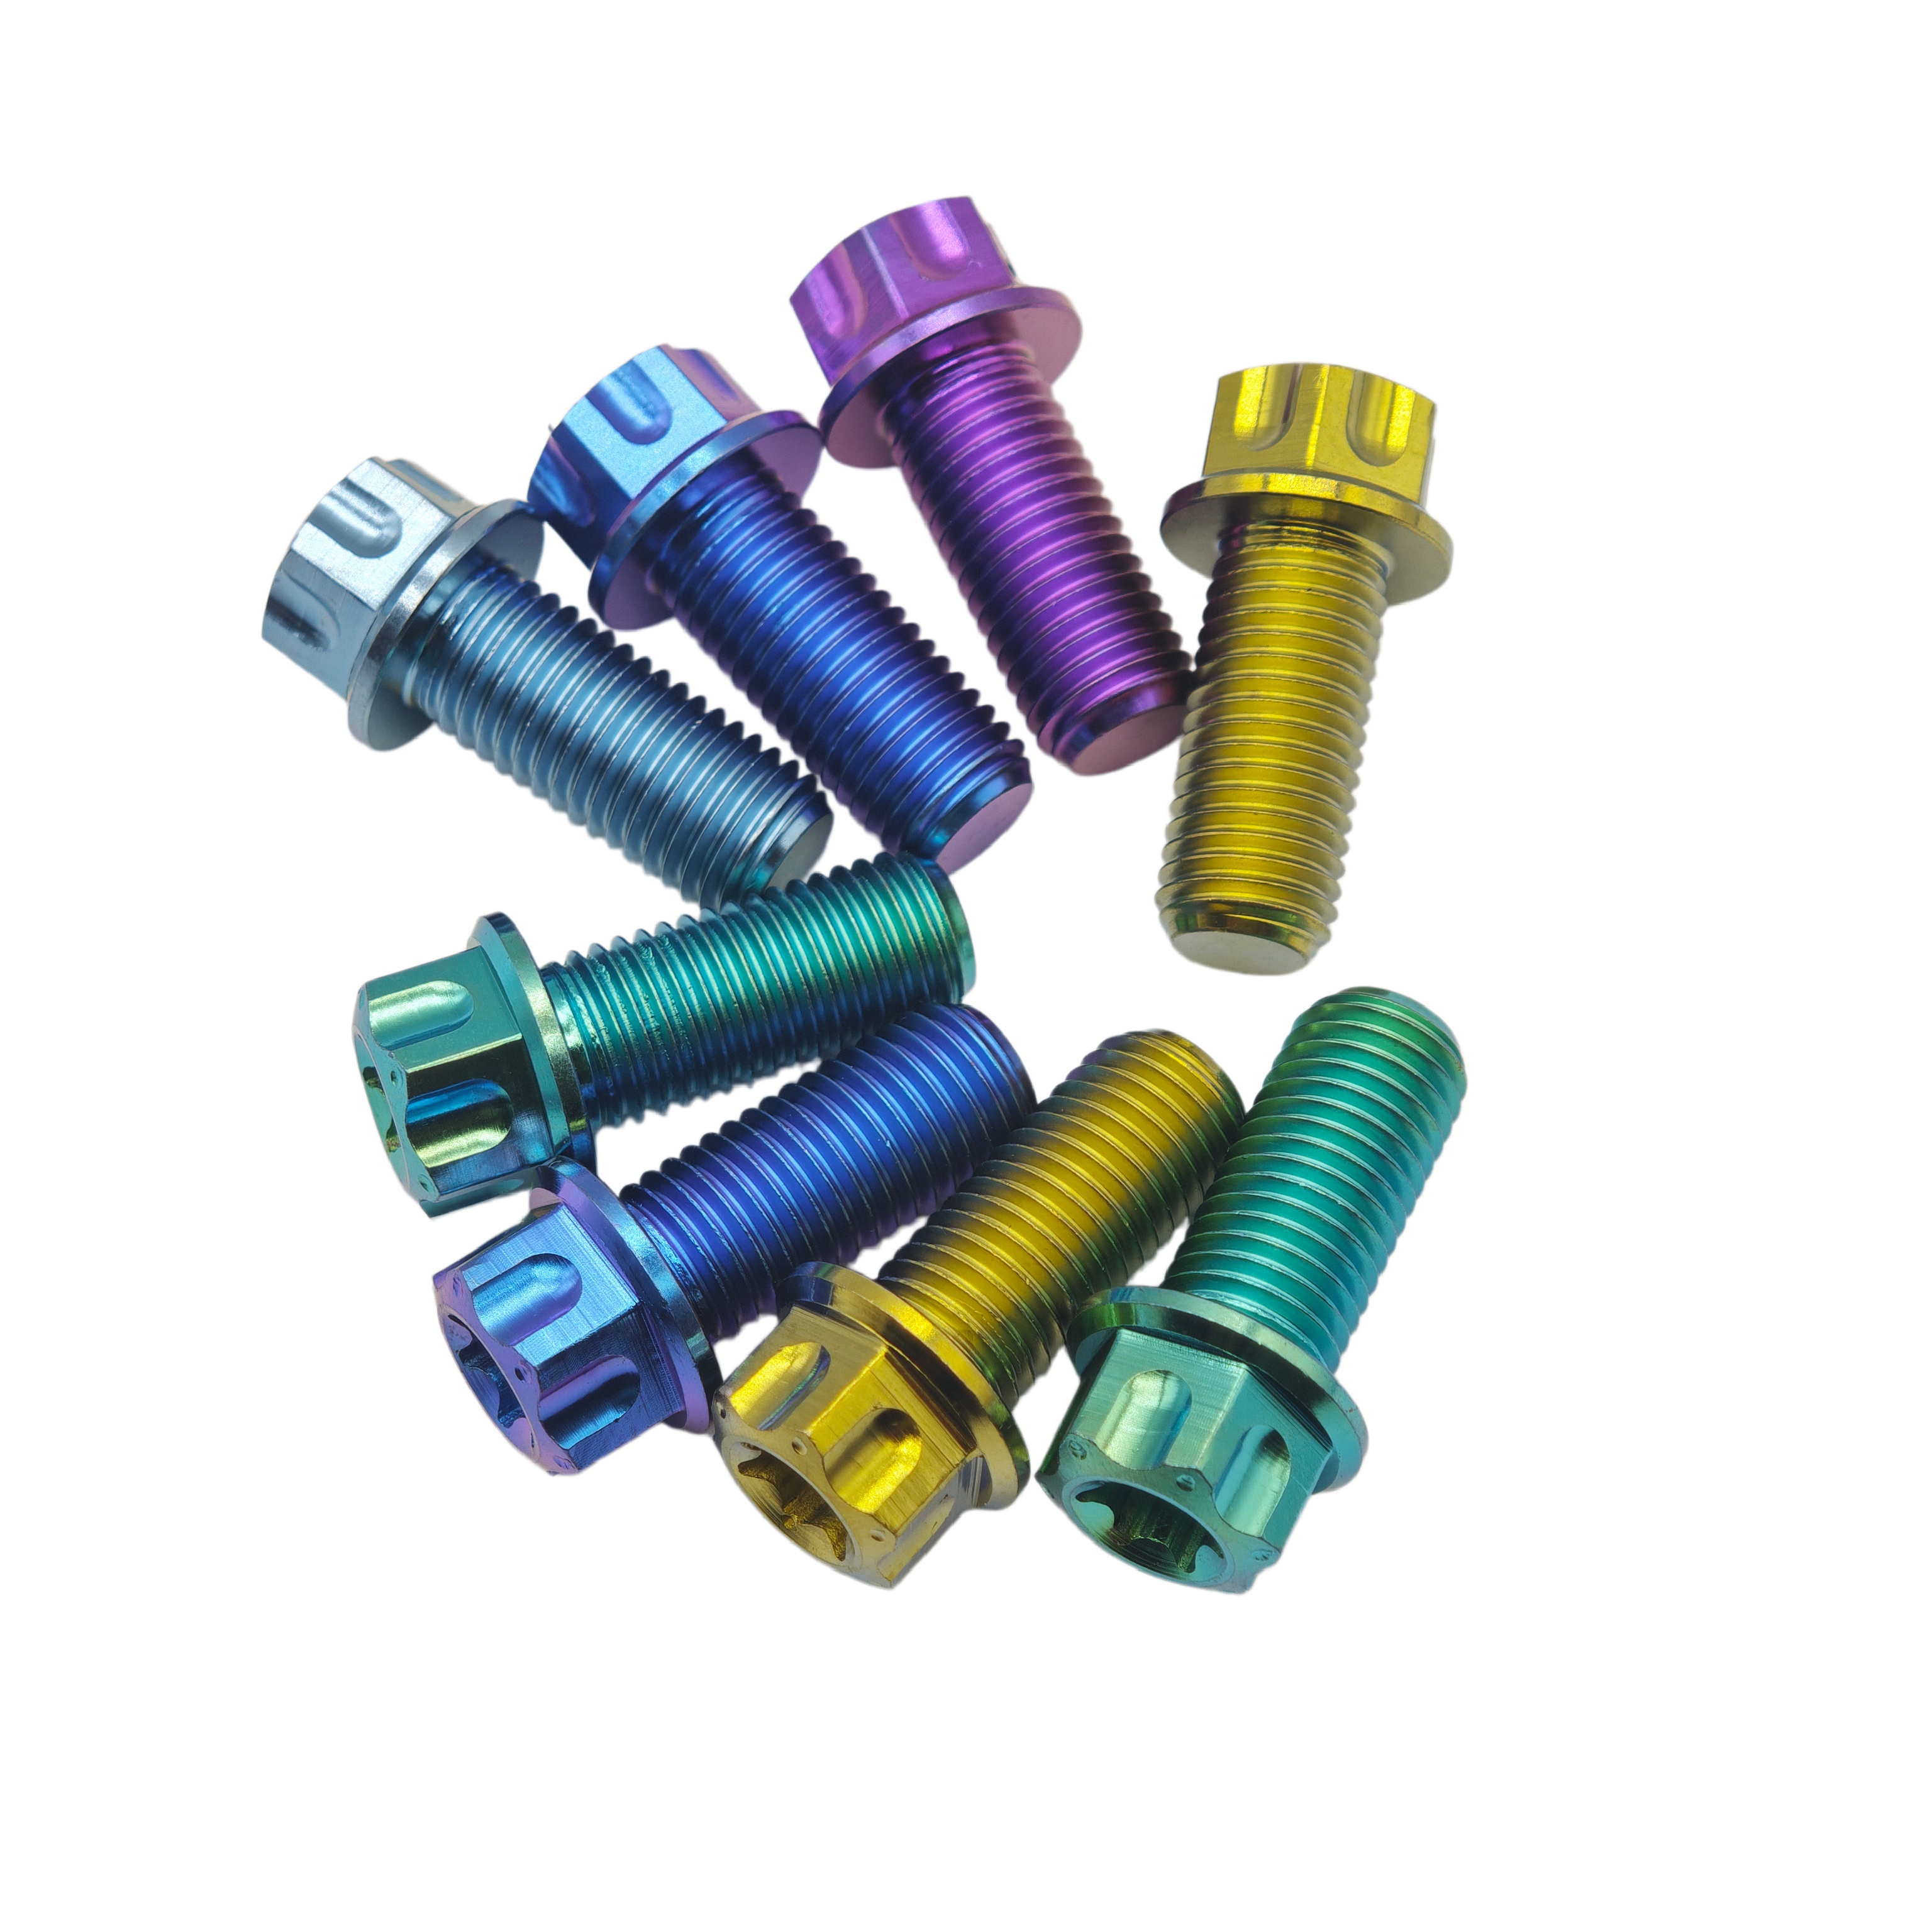
Factory Wholesale Anodized GR5 Titanium Hex Flange Head Bolts M8/M10 UNF Thread Motorcycle Bolts
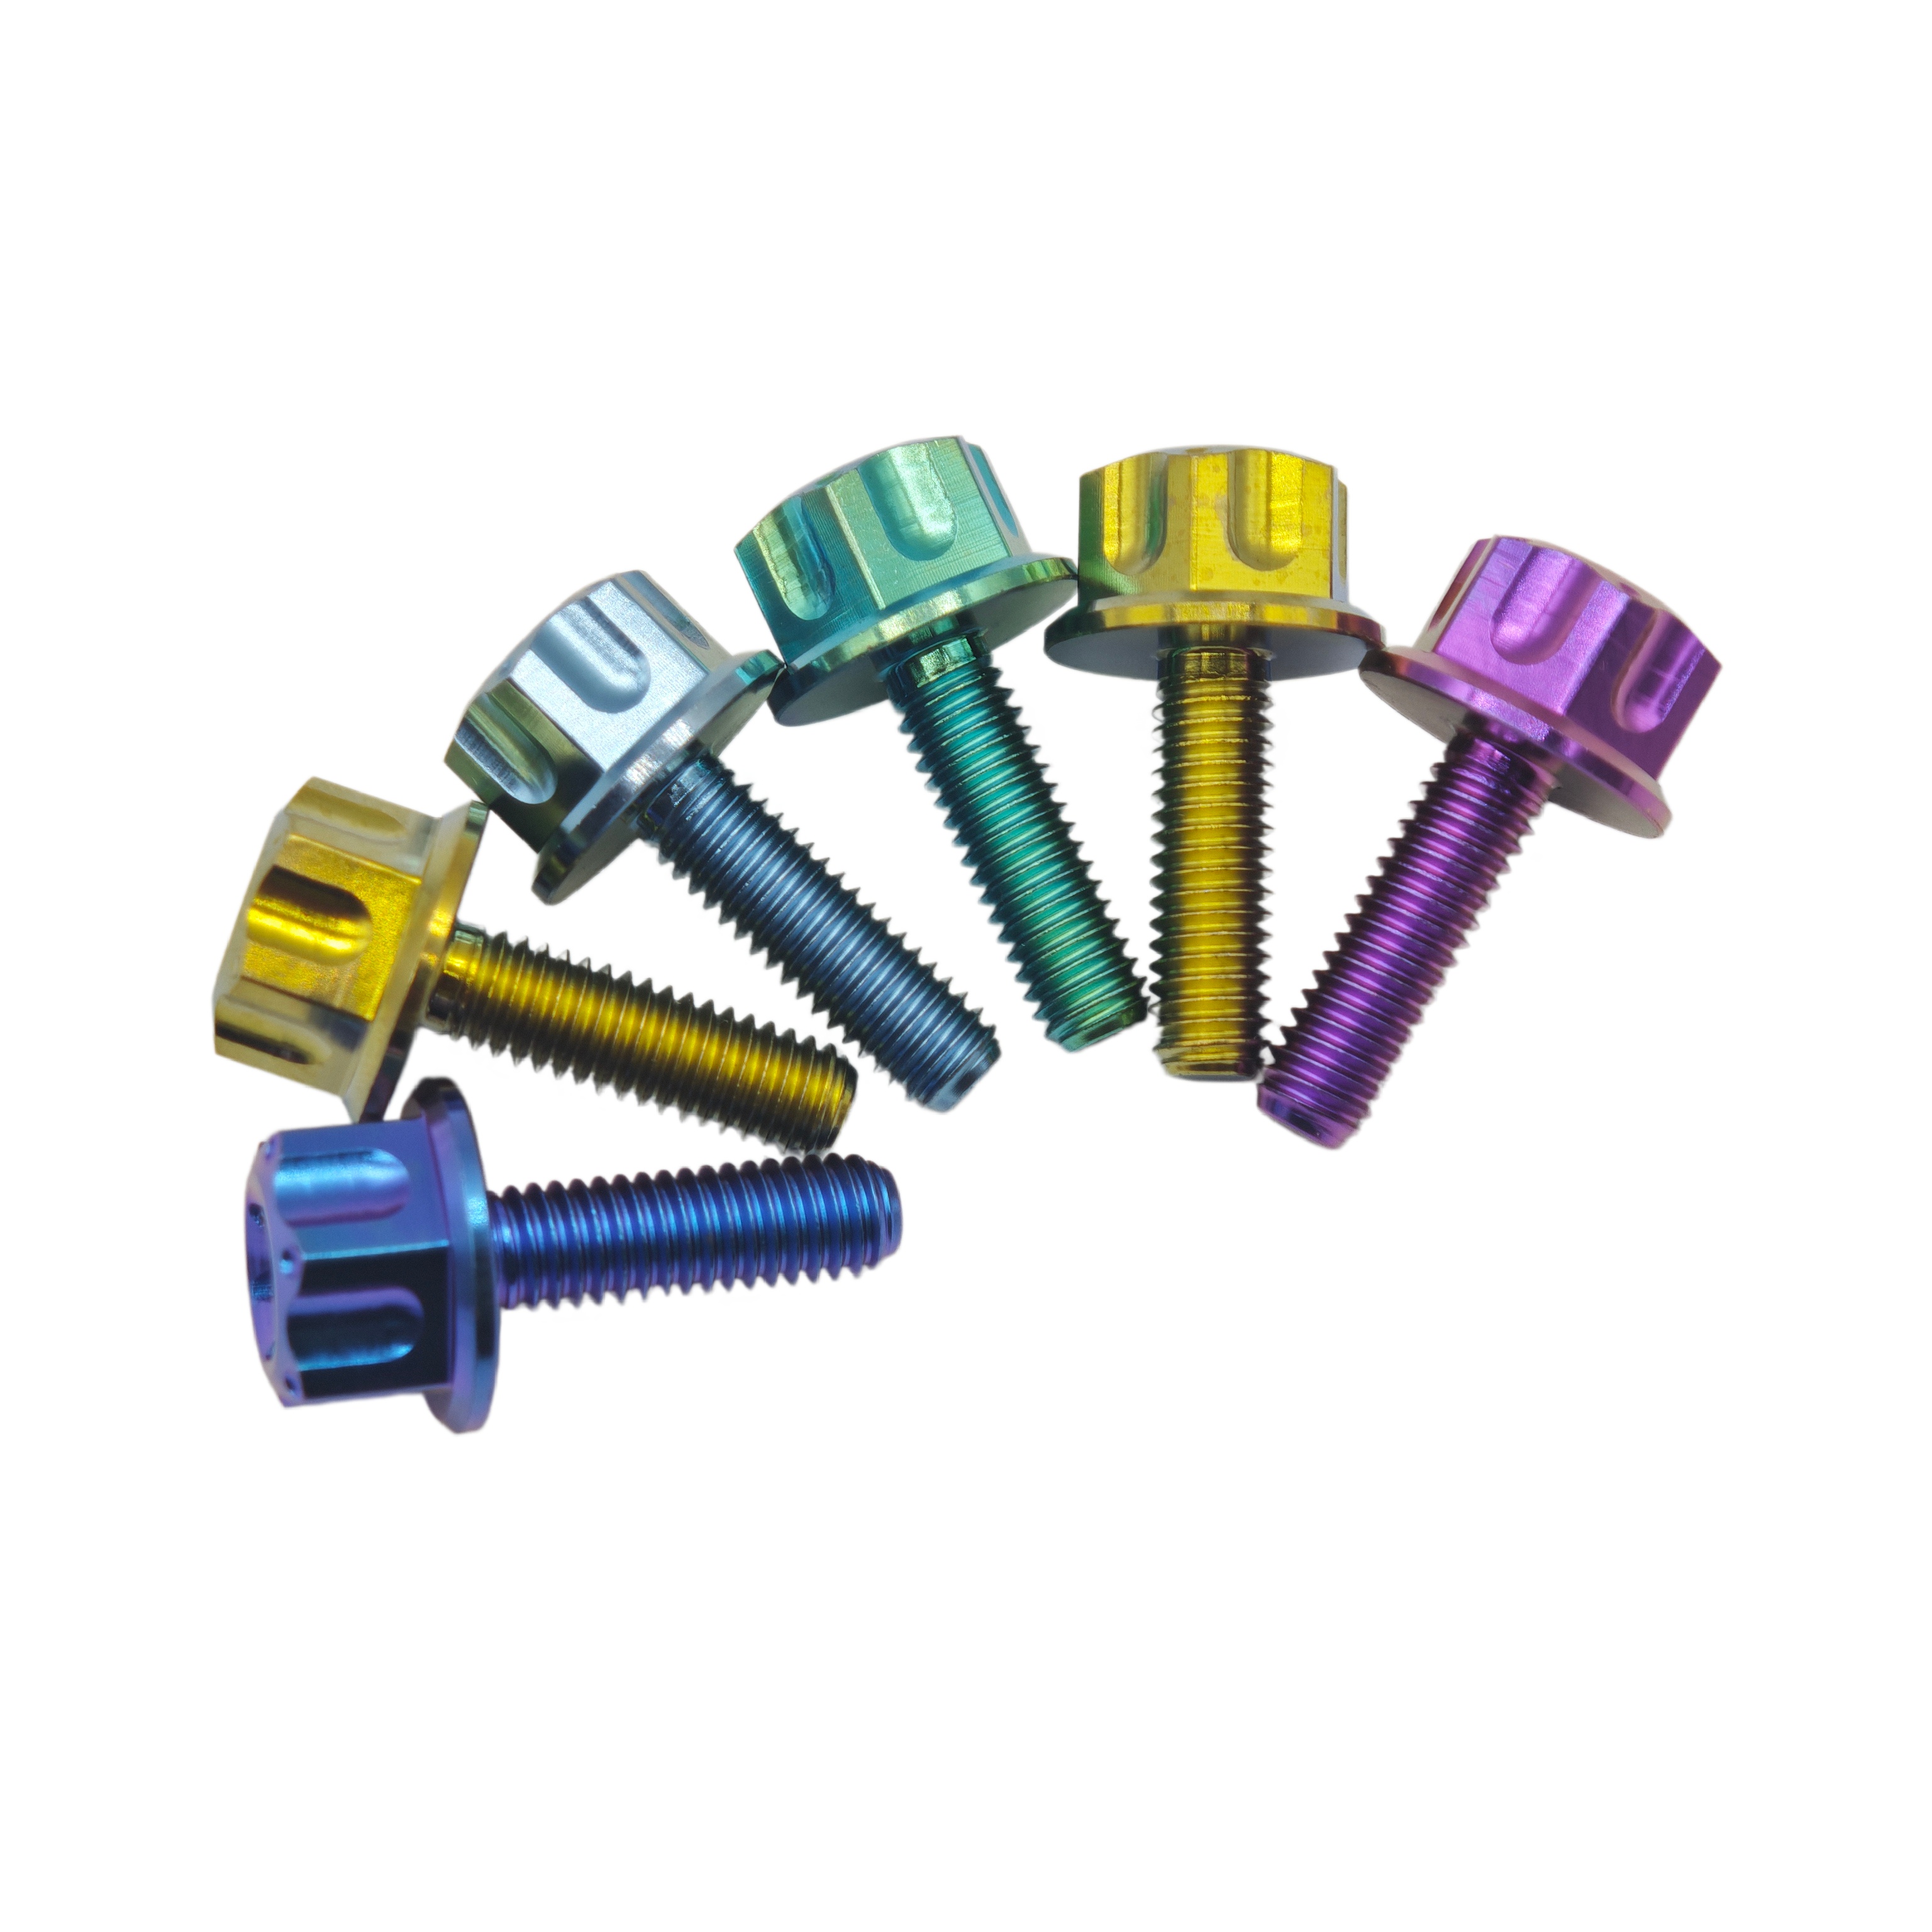
TECKSR Factory Price M4 Anodized GR5 Titanium Hex Flange Head Torx UNF Thread Class 5 Motorcycle Bolts
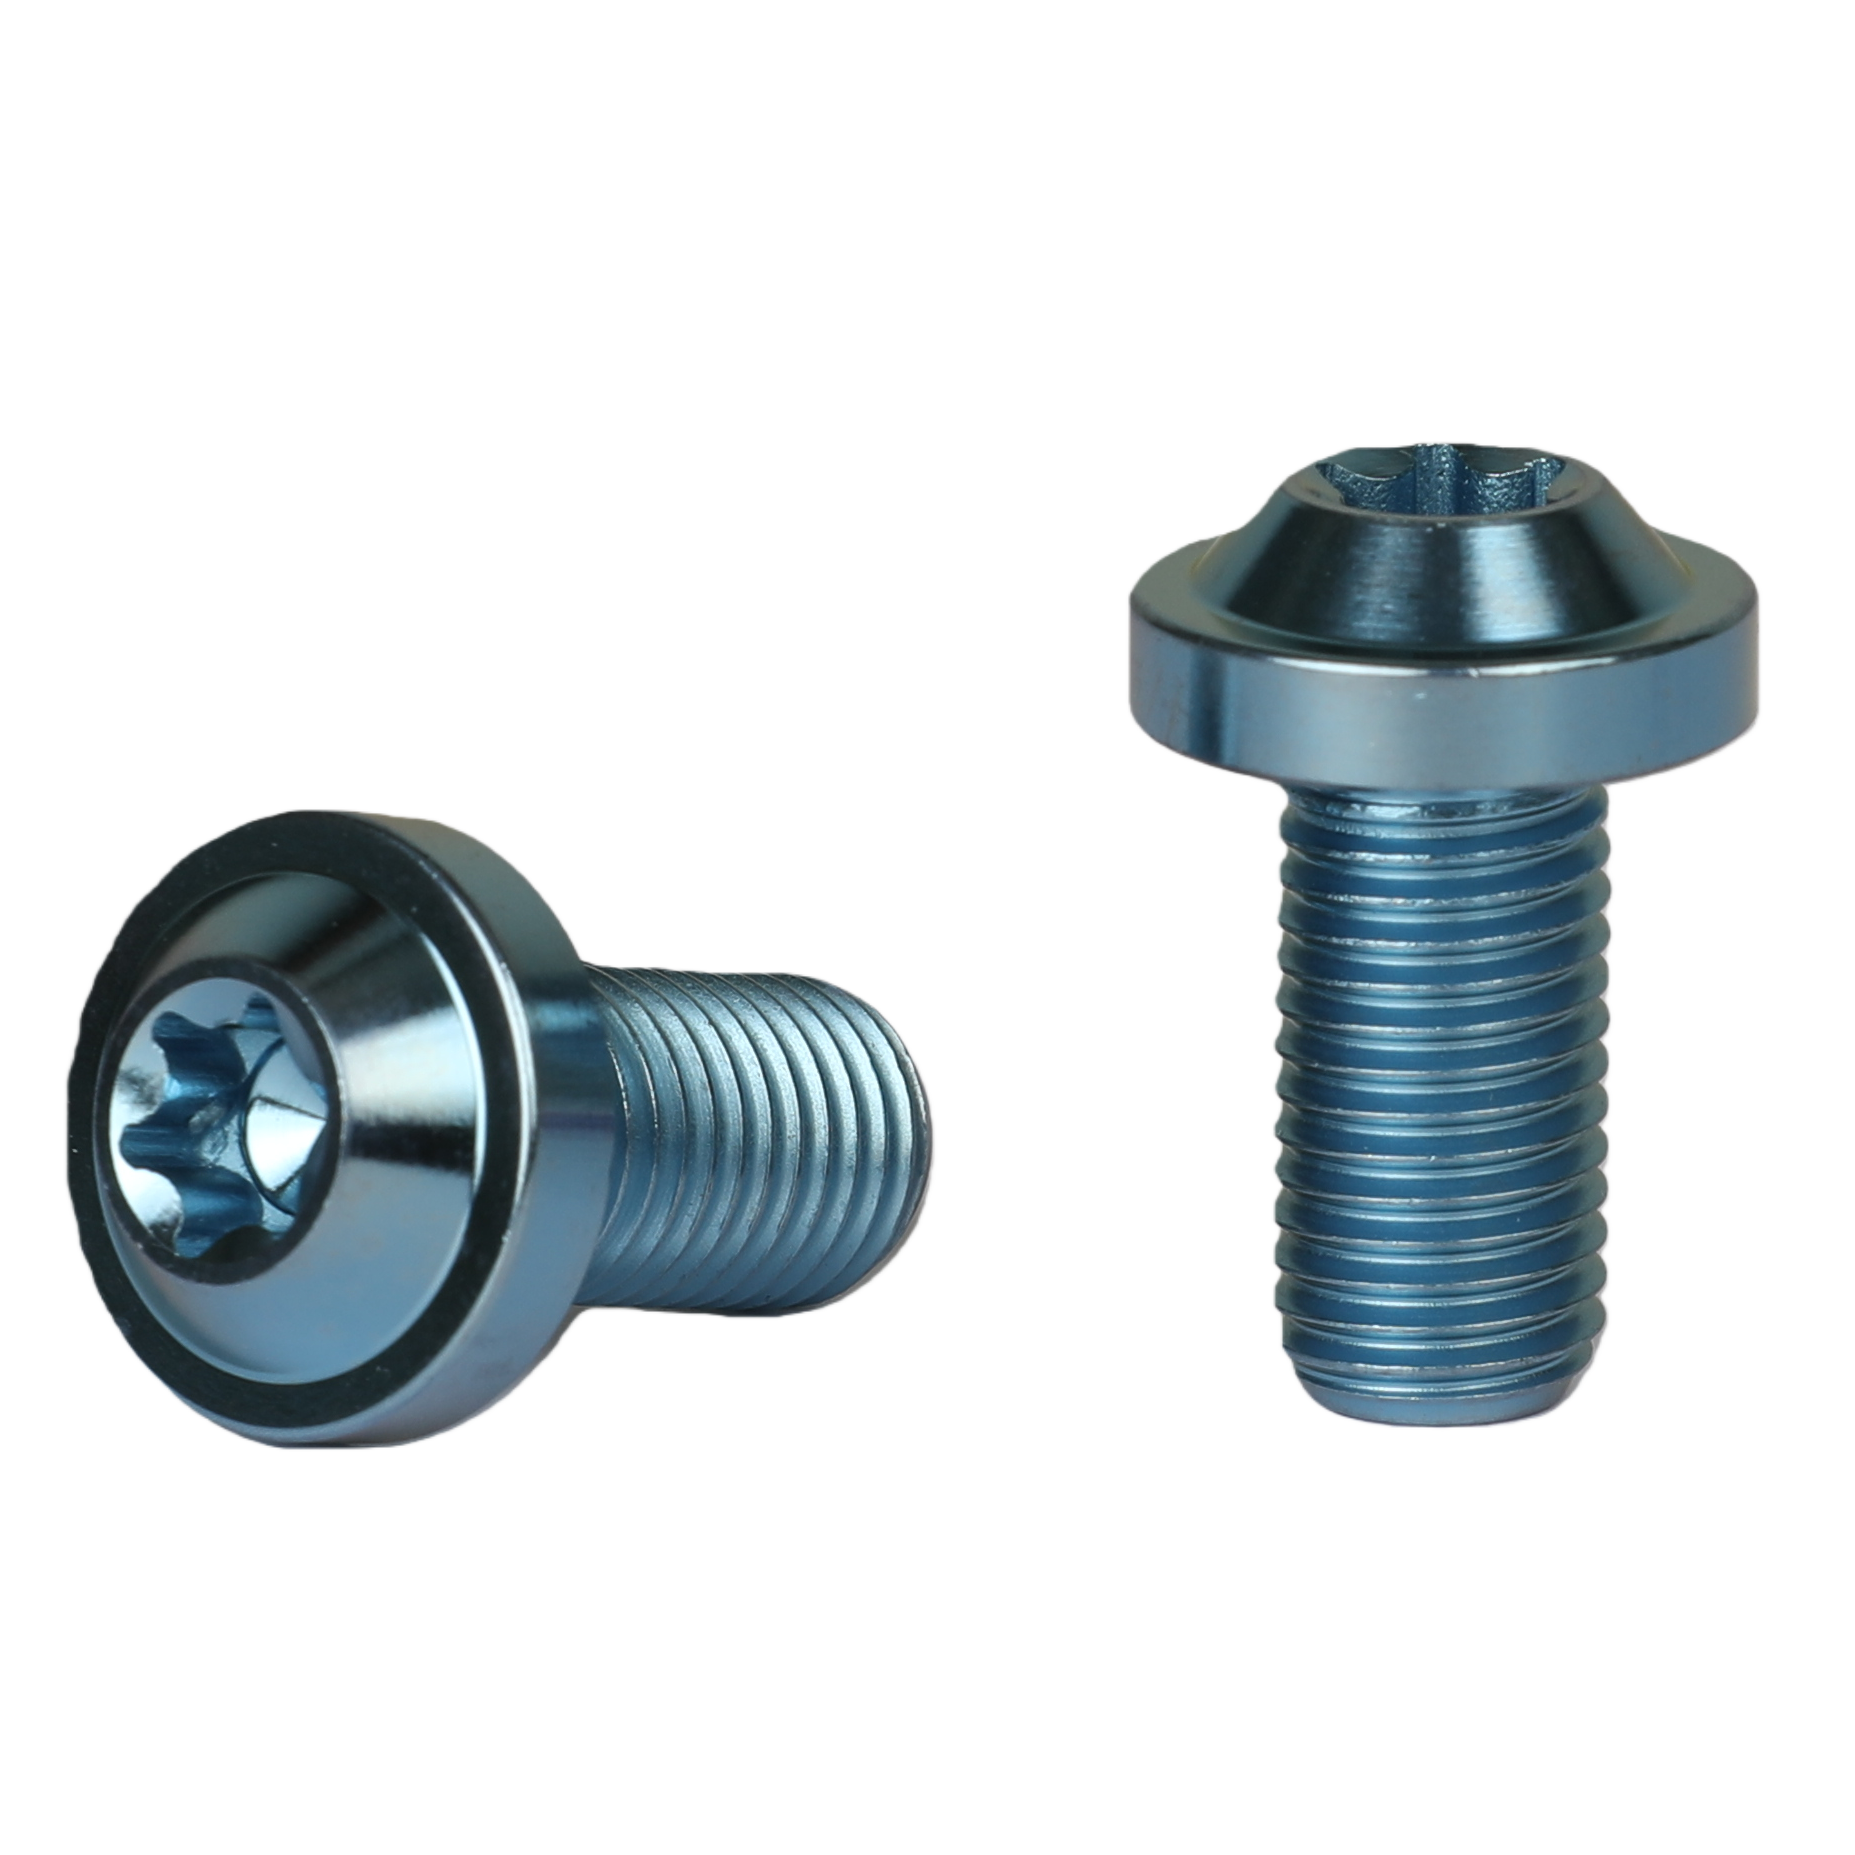
GRX Grade 5 Titanium Pan Head Brake Disc Screws for Race Motorcycle M6/M8/M10 DIN Thread
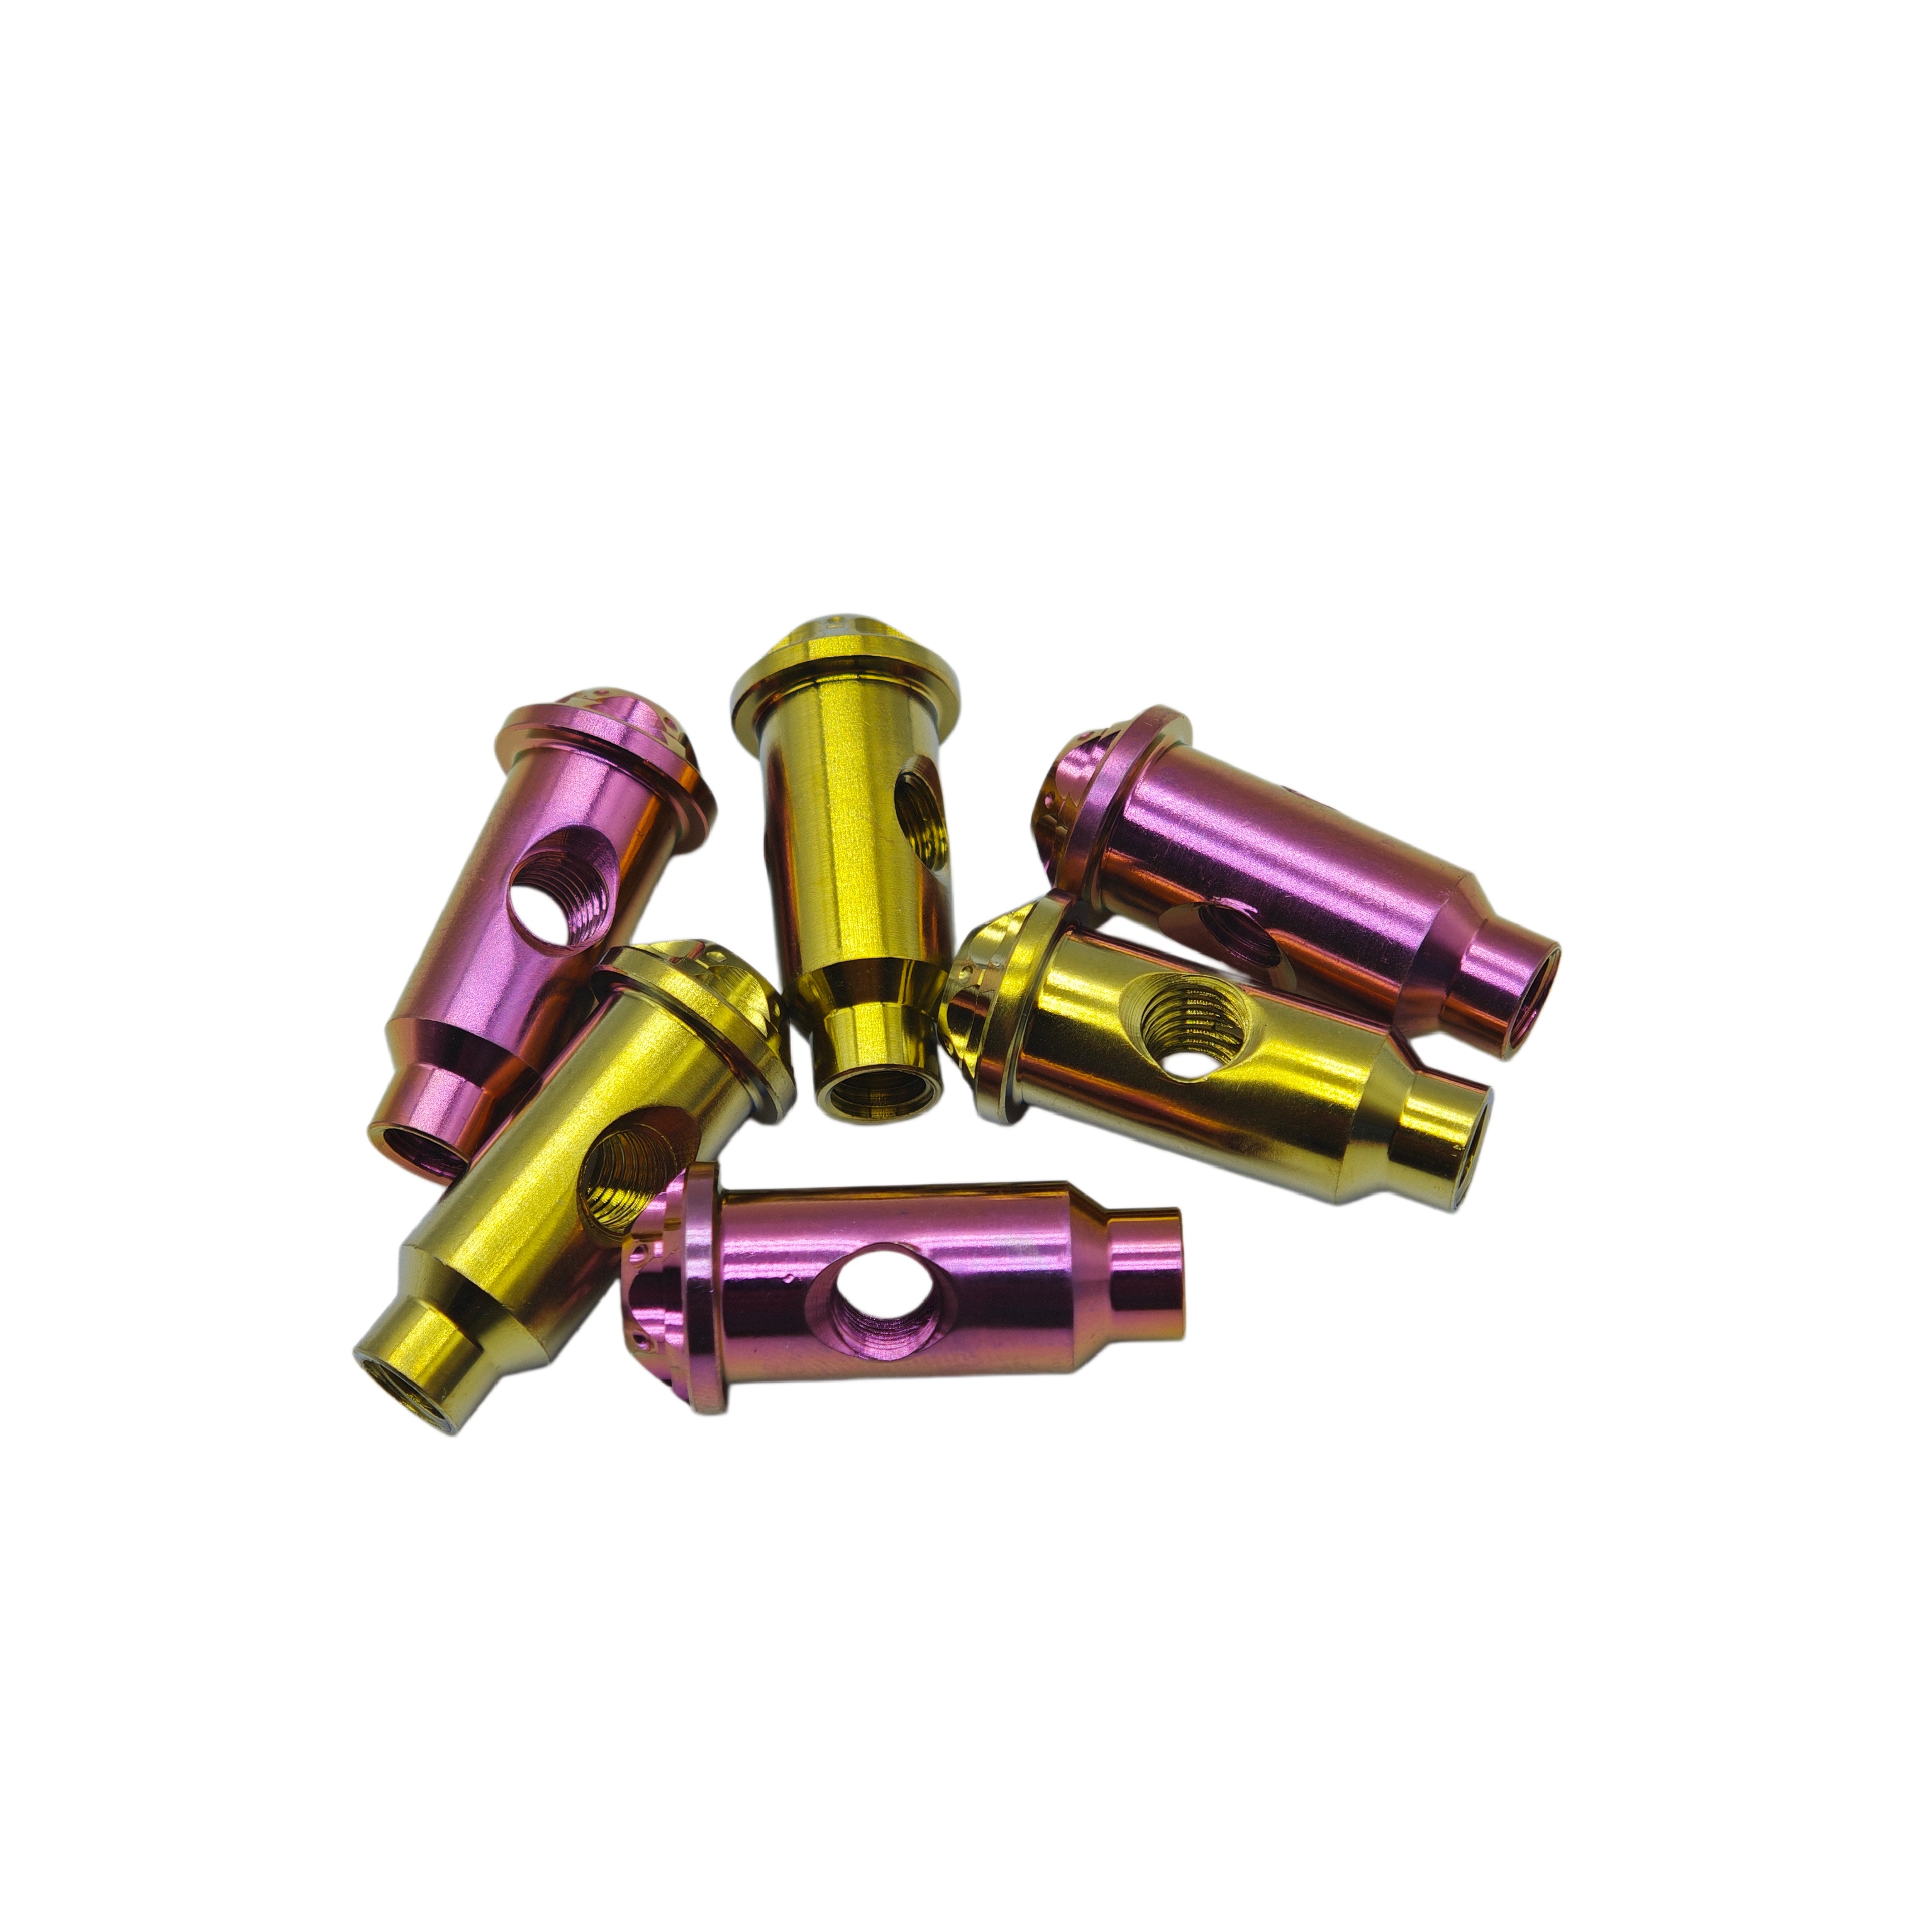
High Quality Gr5 Titanium Cross Dowel Nuts Titanium Adjusters' Knobs Bolt
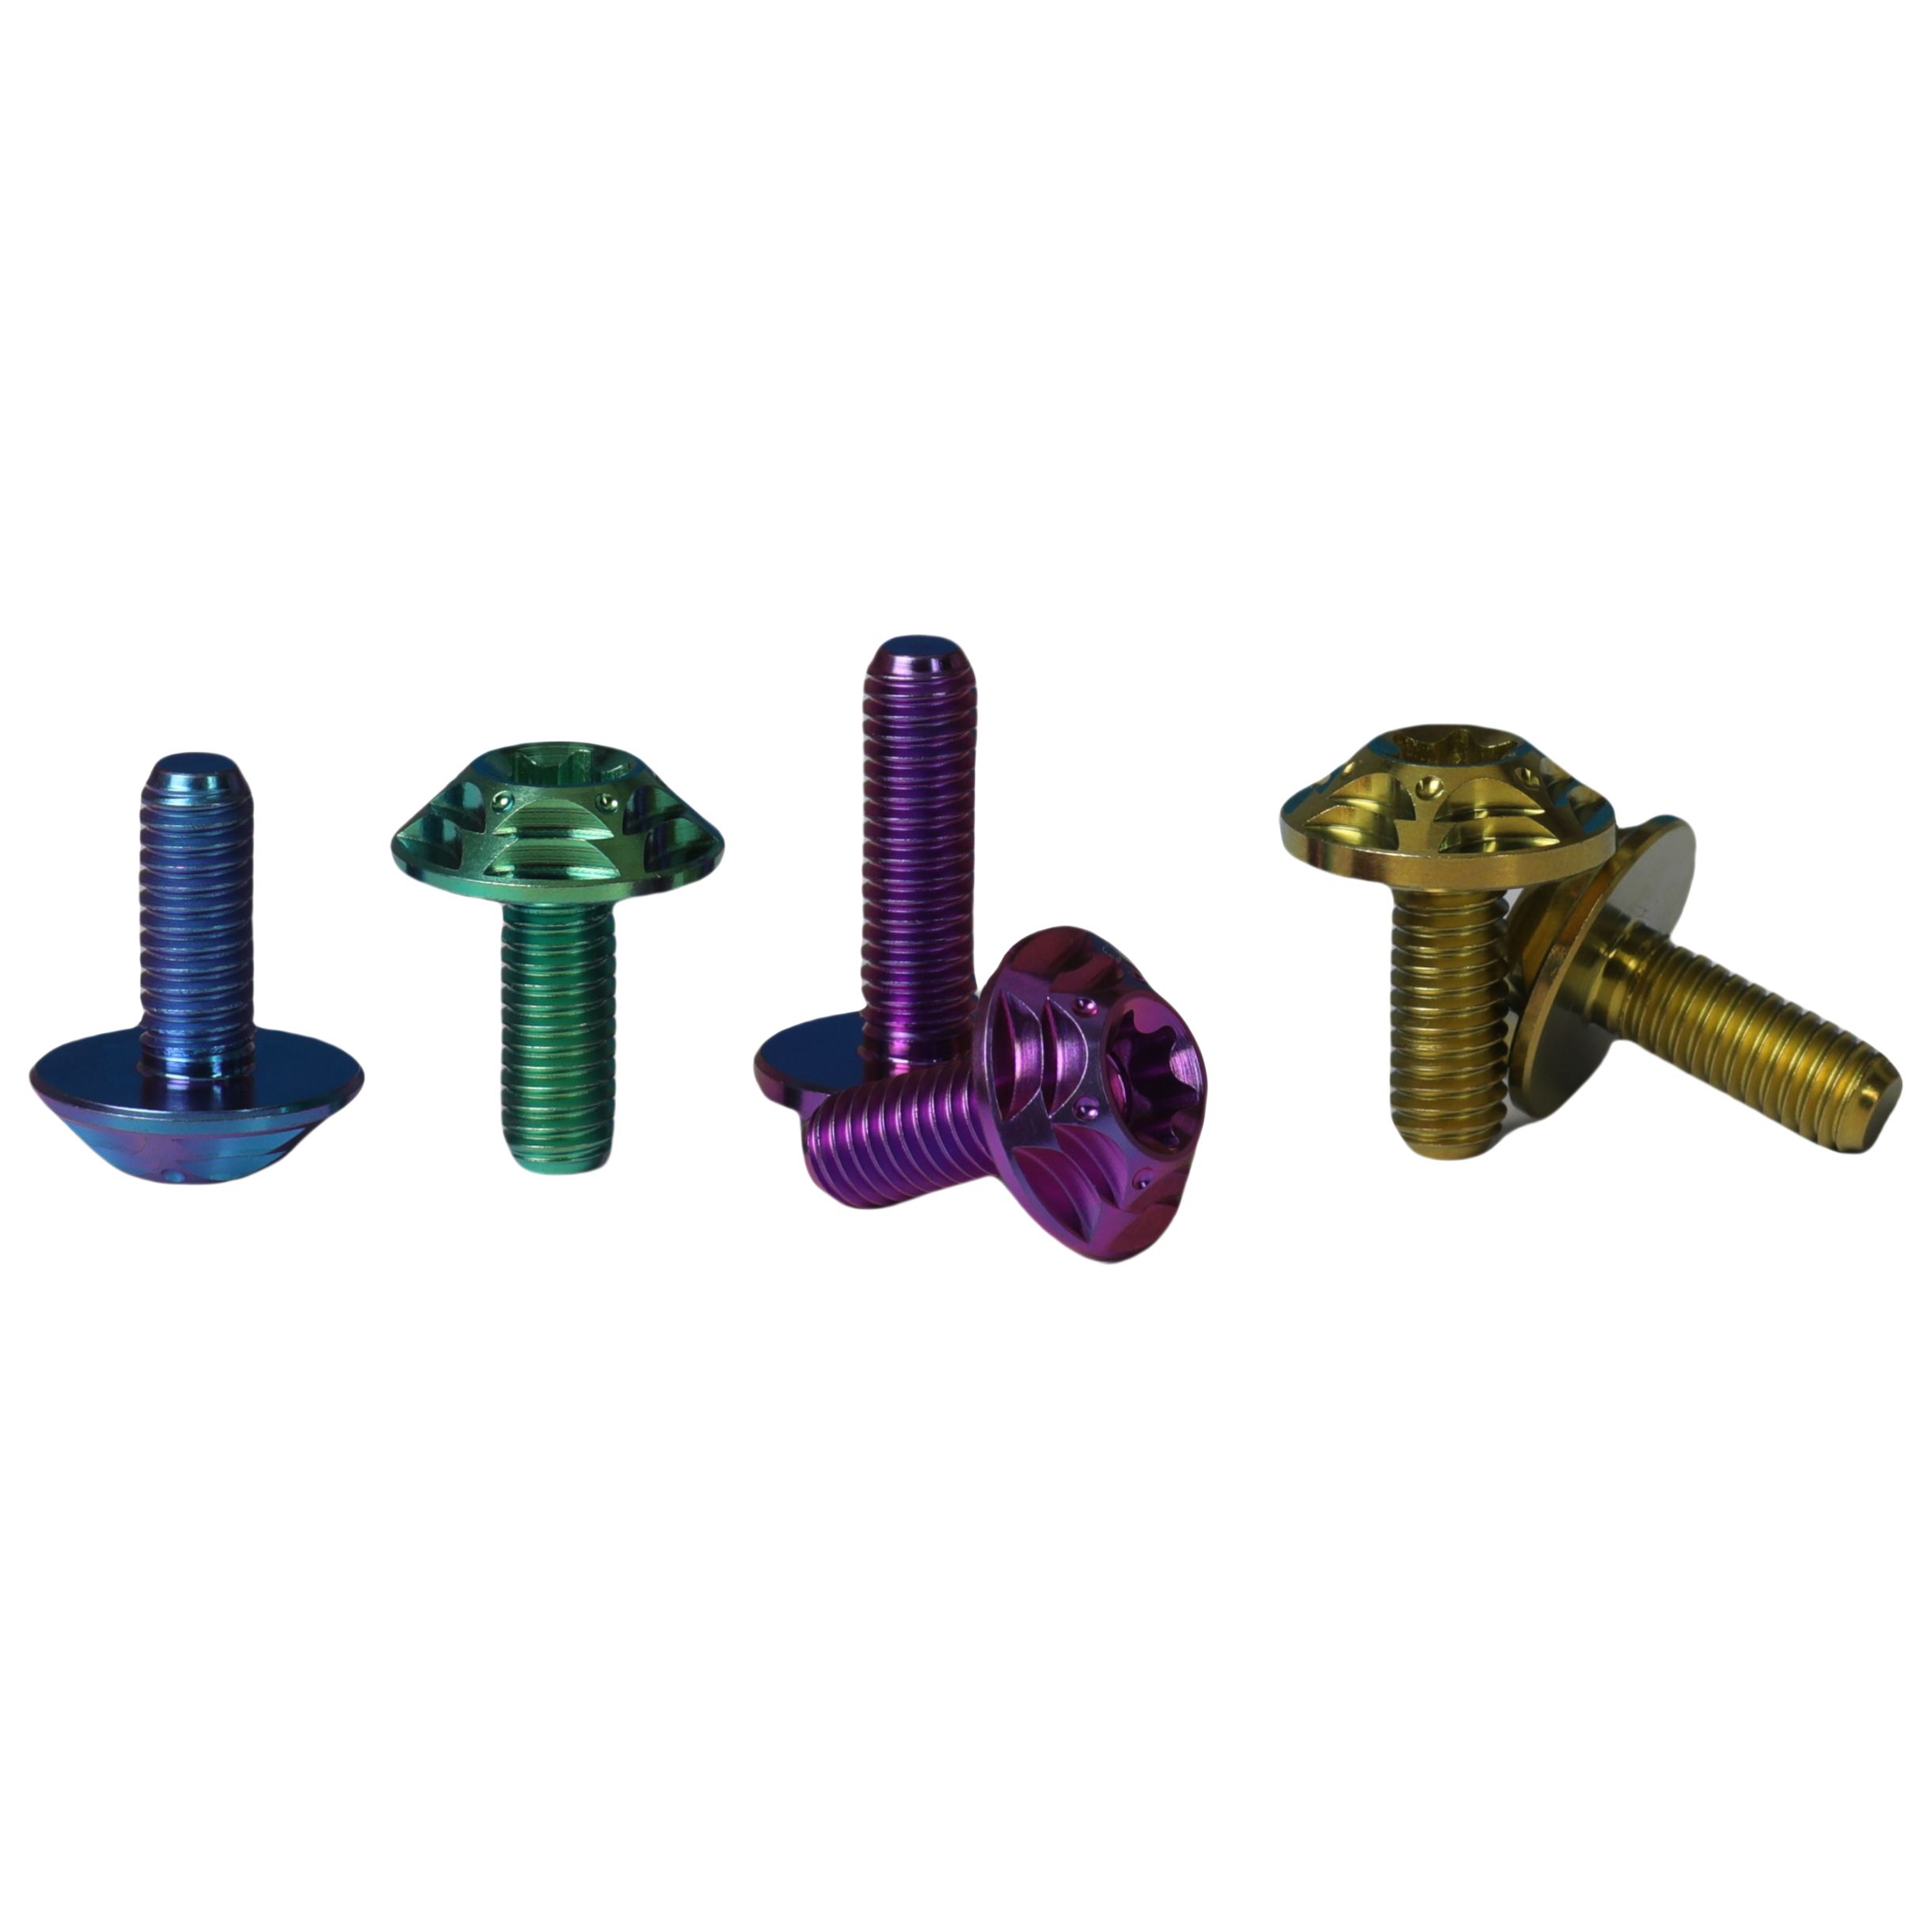
Titanium Alloy CNC Disc Brake Disc Head Bolts Torx Head DIN Thread Anodized/PVD Finish Class 10.9/12.9 Grade
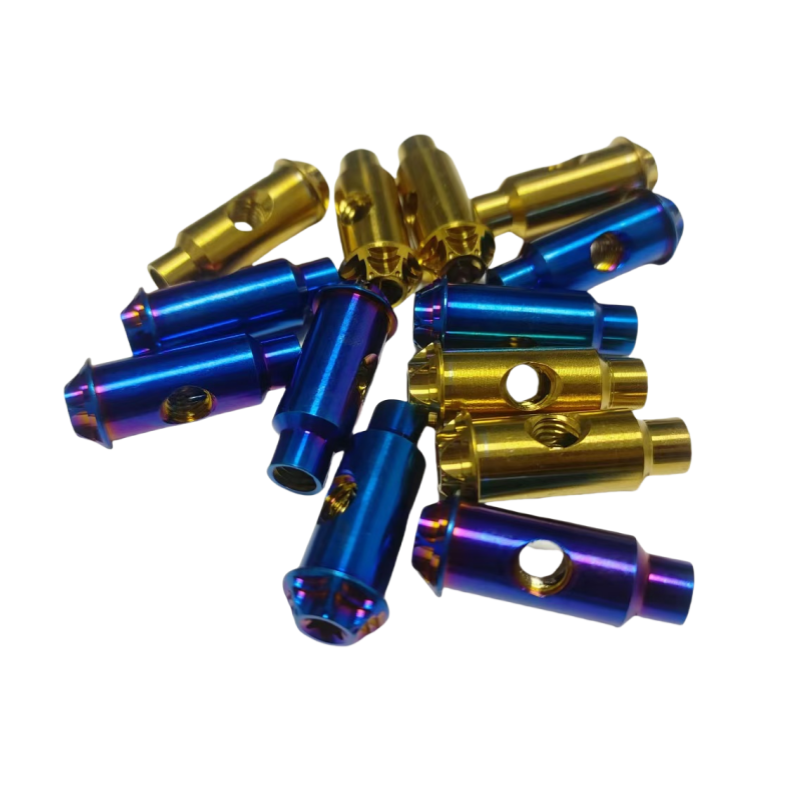
High Performance Gr5 Titanium Cross Dowel Nuts Titanium Adjusters' Knobs Bolt
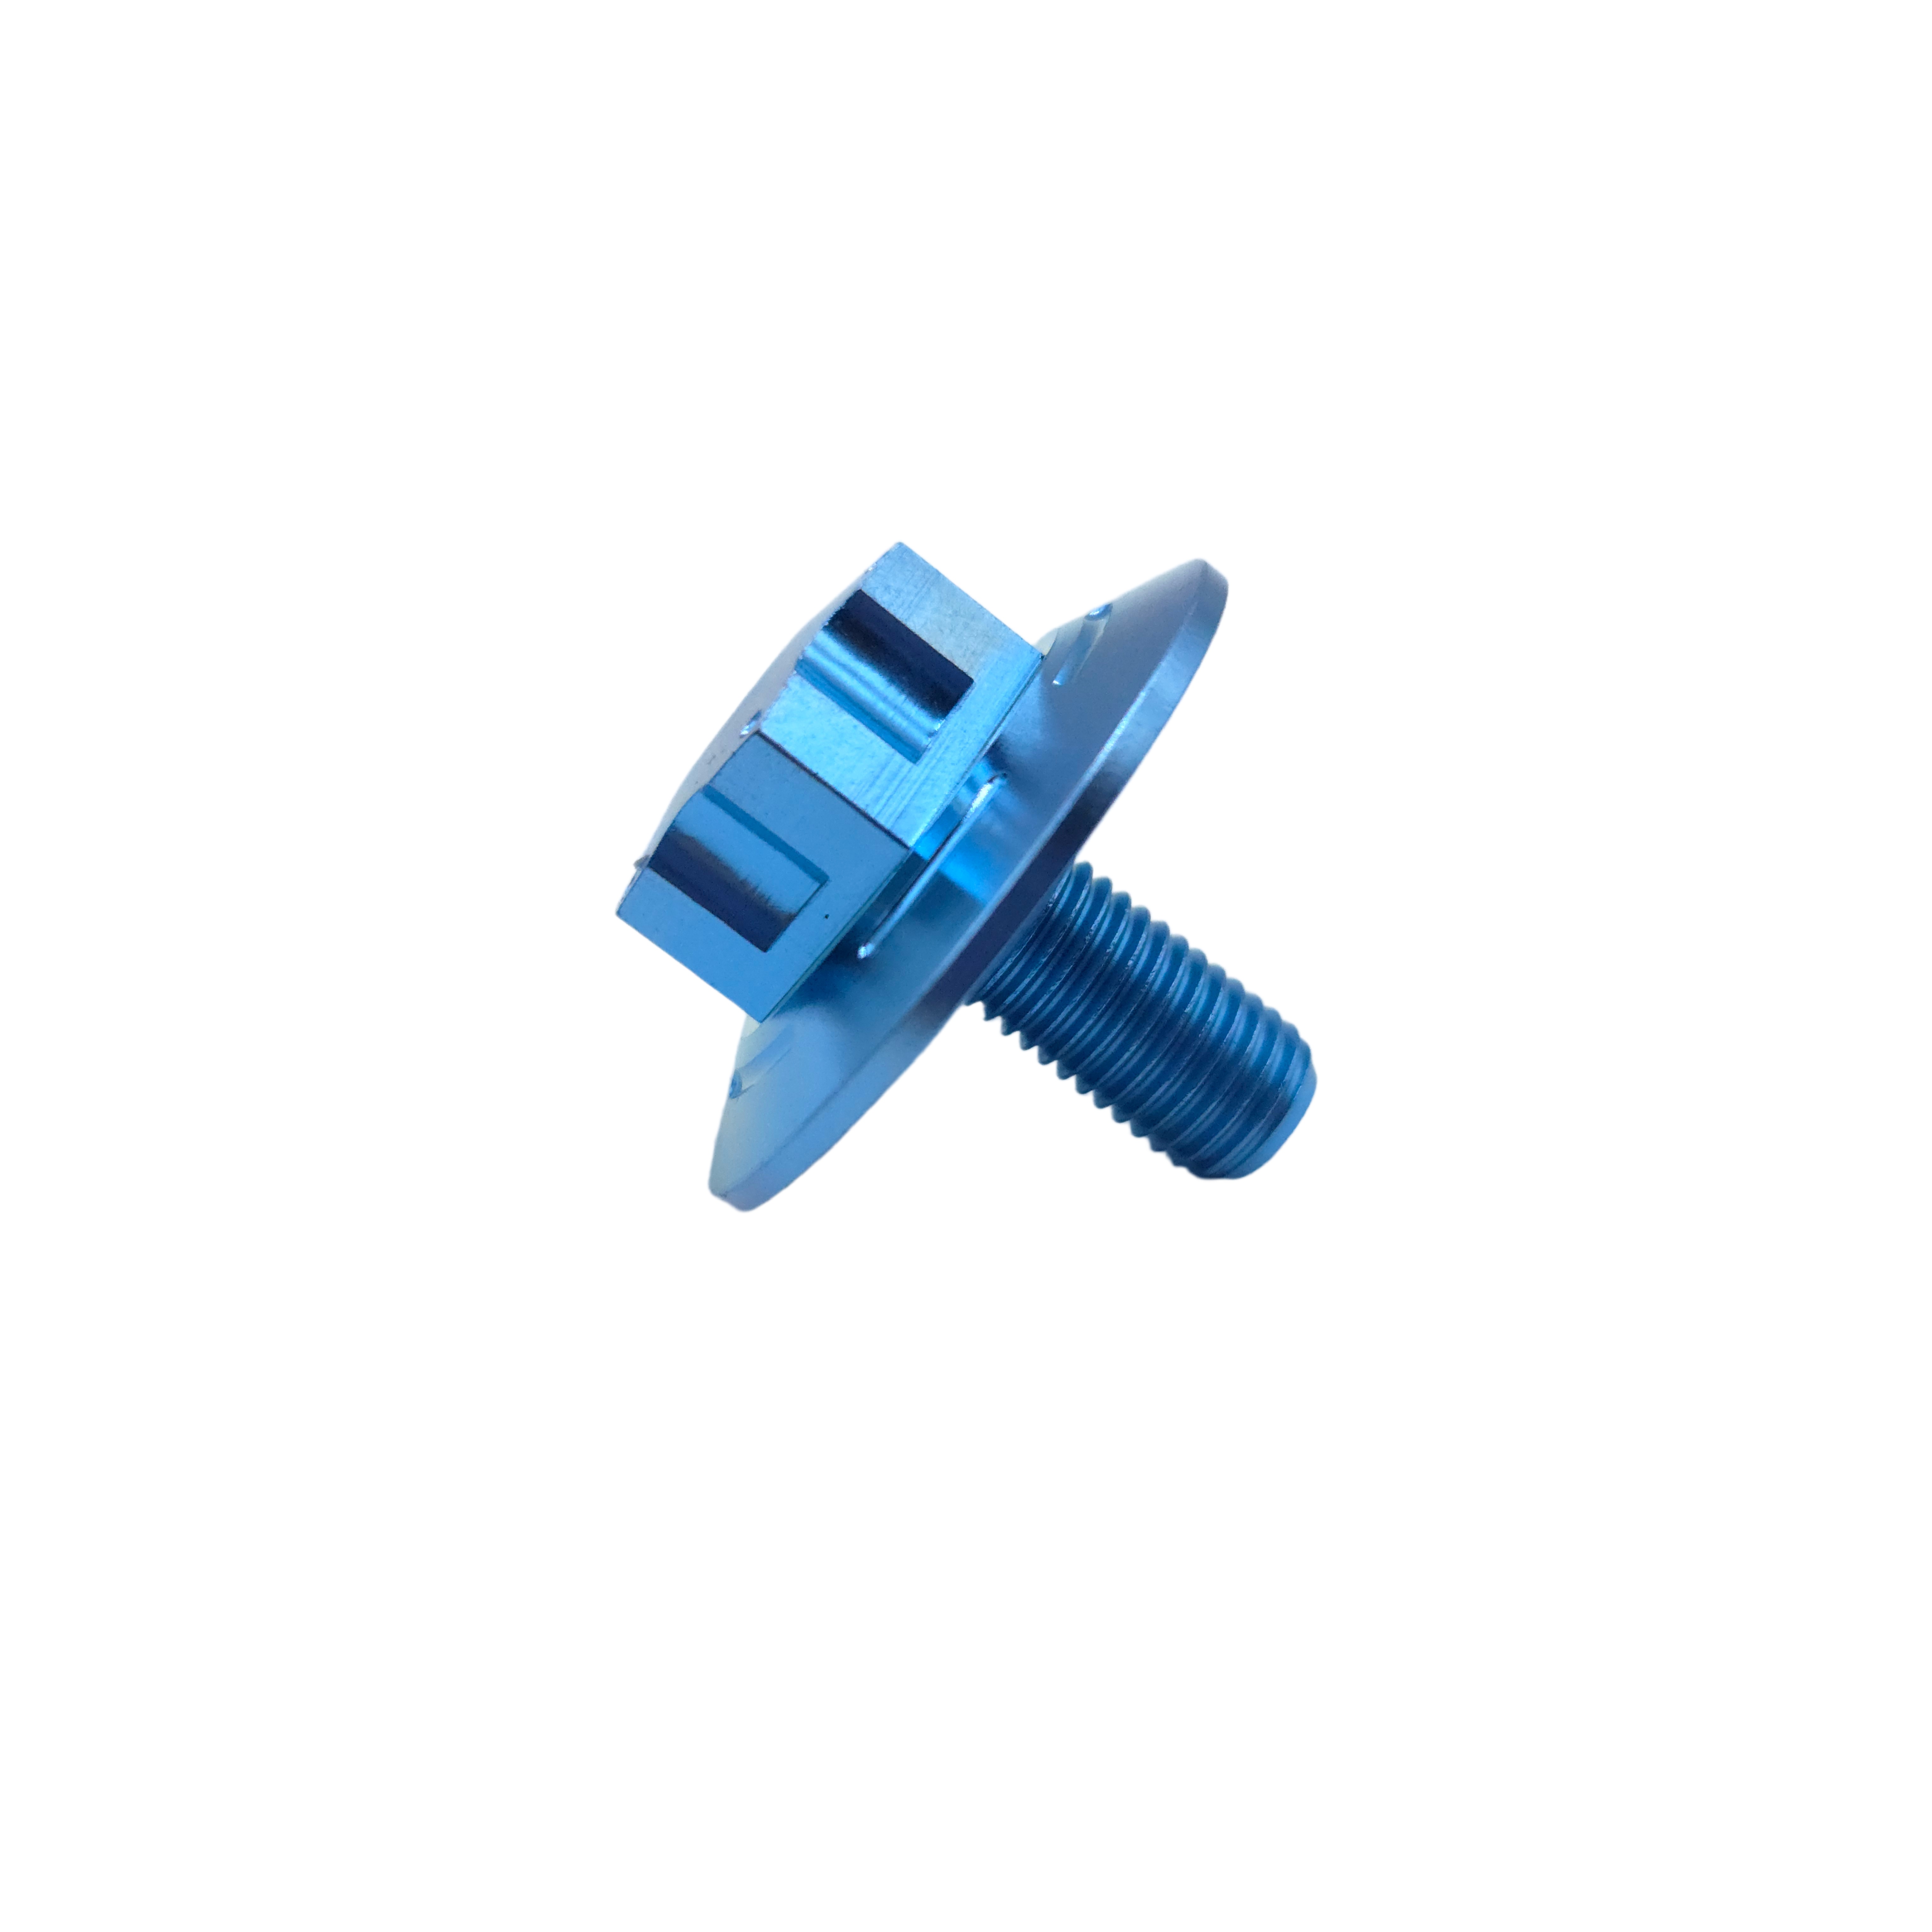
Factory Supply GR5 Titanium Hex Flange Head Bolt M10X20 DIN Thread Anodized Polish Finish
Whitepaper: Metallurgical Dynamics of Ti-6Al-4V Axle Nuts in High-Stress Motorcycle Kinematics
The rear spindle assembly is arguably the most safety-critical threaded junction on a motorcycle chassis. Subjected to simultaneous asymmetric chain tension, torsional braking reaction torques, and high-frequency unsprung shock impacts, axle fasteners require superior dynamic yield properties. For motorcycle engineering enterprises and performance workshops across the Lyon metropolitan zone and the wider Auvergne-Rhône-Alpes basin, transitioning from zinc-electroplated class 8.8 or 10.9 carbon steel to precision-turned Grade 5 titanium (Ti-6Al-4V) represents a substantial engineering leap in unsprung weight optimization and structural integrity.
1. Unsprung Rotational Mass & Suspension Dynamics
In performance dynamics, unsprung mass (masse non suspendue) directly dictates wheel-to-ground compliance over irregular asphalt. Because the rear wheel spindle, swingarm chain adjuster dowels, and outer axle retaining nuts reside on the outer perimeter of the suspension linkage, any mass reduction here exponentially lowers wheel inertia. Grade 5 titanium possesses a specific density of 4.43 g/cm³ compared to 7.85 g/cm³ for chrome-moly steel. Swapping an OEM M22×1.5 steel castle nut and washer setup for a lightened, CNC-machined Grade 5 titanium flanged axle nut yields a weight decrease of approximately 44% to 47%. This enables racing suspensions—such as those tuned by suspension workshops around Lyon for circuits like Bresse and Laquais—to respond rapidly to high-frequency chatter without inducing mid-corner tire scrub.
2. Rolled Threads vs. Cut Threads in Fatigue Endurance
A frequent failure mechanism of low-tier aftermarket motorcycle hardware is thread shear under cyclic vibrational loading. At our Baoji manufacturing plant, all external and internal threads on motorcycle axle nuts and spindle studs are formed via cold thread-rolling processes rather than subtractive lathe cutting. Cut threads sever the continuous metallurgical grain flow of the titanium alloy, creating microscopic notch stresses at the root of the pitch. Conversely, cold rolling compresses the crystalline lattice, inducing compressive residual surface stresses and burnishing the thread flank. This increases cyclic fatigue life by more than 30%, providing an essential safety threshold when an axle nut is tightened to factory torque specs (frequently 90 to 110 N·m on superbikes) and exposed to severe lateral chain pull.
| Mechanical & Physical Parameter | Grade 5 Titanium (Ti-6Al-4V) | Class 10.9 High-Tensile Steel | 7075-T6 Billet Aluminum | A2-70 Austenitic Stainless |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 | 7.85 | 2.81 | 7.93 |
| Ultimate Tensile Strength (MPa) | ≥ 895 – 1000 | 1040 – 1220 | 540 – 570 | 700 |
| Yield Strength 0.2% (MPa) | ≥ 828 | 940 | 480 | 450 |
| Strength-to-Weight Ratio (kN·m/kg) | 214 (Extreme) | 142 (Moderate) | 196 (High) | 88 (Low) |
| Corrosion Resistance (De-Icing Salt / Rain) | Immune (Stable TiO₂ Passive Layer) | Poor (Requires Galvanic Zinc) | Moderate (Prone to Pitting) | High (Risk of Crevice Attack) |
| Modulus of Elasticity (GPa) | 110 – 114 | 205 – 210 | 71.7 | 193 |
| Resistance to Cyclic Galling | High (with MoS₂ / Ti Anti-Seize) | Moderate | Poor | High Risk (Severe Galling) |
3. Tribological Behavior & Galling Prevention Protocol
Titanium alloys exhibit a high friction coefficient against dissimilar metals if torqued dry (μ ≈ 0.35–0.45), which can precipitate micro-welding or galling (grippage) between the axle nut and the steel rear spindle shaft. In accordance with professional engineering protocols supplied to our Lyon distributor network, every titanium axle nut must be installed using a specialized lubricating medium containing molybdenum disulfide (MoS₂) or ceramic-based anti-seize paste. This reduces the torque friction coefficient to μ ≈ 0.10–0.12, ensuring that wrench torque converts smoothly into axial clamping preload rather than torsional thread friction.
Specialized Application Scenarios across Greater Lyon & Auvergne-Rhône-Alpes
From the switchbacks of the French Alps to regional circuit racing and year-round urban transit, discover how our Grade 5 titanium hardware meets the exact operating conditions of the Rhône Valley.
Alpine Passes & High Thermal Cycles
Riders departing Lyon towards the Col du Galibier, Mont Ventoux, or the Vercors Massif push motorcycle chassis through rapid altitude shifts and violent gradient braking. Grade 5 titanium retains its tensile modulus across thermal swings from -20°C in high mountain air to over +350°C of radiated heat near rear brake rotors, avoiding the thermal relaxation common in alloy studs.
Track Day & Superbike Competition
Teams racing at nearby Circuit de Bresse, Circuit du Laquais, or the Magny-Cours club events require quick wheel changes during endurance sessions. Our custom flange axle nuts are designed with broad bearing shoulders and integrated locking pins or castle slots, allowing rapid impact-socket engagement without rounding off wrench flats under pressure.
Rhône Corridor Chemical Resistance
The winter road maintenance along the Rhône valley (autoroutes A6, A7, and A43) relies heavily on liquid magnesium chloride and abrasive de-icing salts. While standard OEM cad-plated or zinc fasteners bubble and corrode within two winters, our Ti-6Al-4V fasteners form an instantaneous, self-healing titanium oxide film that is entirely impervious to chloride-induced pitting.
Market Shifts Transforming the French Motorcycle Hardware Sector
Key economic, regulatory, and technological trends influencing fastener procurement for motorcycle distributors, OEM modifiers, and speed shops throughout France.
Contrôle Technique Moto (CT2R) Compliance
With the implementation of compulsory vehicle inspections (Contrôle Technique deux-roues) in France, certified dimensional accuracy and structural fastener integrity are under direct scrutiny. Riders and workshops in Lyon avoid sub-par decorative fasteners and demand certified DIN/ISO equivalent Grade 5 titanium with documented tensile strength to pass chassis safety audits.
Surge in Electric Superbike Conversions
The Auvergne-Rhône-Alpes green mobility initiative has stimulated a wave of electric motorcycle prototype development across Lyon’s tech clusters (such as Vaulx-en-Velin and Villeurbanne). Due to heavy onboard lithium-ion battery modules, EV motorcycle developers aggressively optimize every gram of chassis hardware, prioritizing titanium rear axle assemblies and motor mount studs.
Custom Atelier Aesthetic Differentiation
Lyon's thriving boutique motorcycle builders (specializing in bespoke BMW R-series, Ducati Scramblers, and Triumph retros) require distinct aesthetic finishes. Our facility supports voltage-controlled electrochemical anodizing (burnt blue, gold, violet) and vacuum Physical Vapor Deposition (PVD black, DLC), providing ultra-hard surface coloring that will not chip or strip under heavy impact wrenching.
Direct Factory Manufacturing from Baoji, China's "Titanium Valley"
Partnering with Zunvo Titanium Products Co., Ltd. gives Lyon buyers direct access to certified raw materials, high-precision multiaxis CNC machinery, and end-to-end quality assurance.
Certified Raw Material Traceability
Established in 2015 within Baoji's Shiling Road Industrial Park, we are located directly adjacent to prime national titanium sponge smelters. Every batch of Ti-6Al-4V Grade 5 wire and bar stock is tracked via individual melt heat numbers. We furnish complete EN 10204 Type 3.1 chemical inspection certificates and physical test reports with every European export shipment.
High-Precision CNC Machining & Heading
Our manufacturing floor spans 1,000–3,000 m² operated by 101–200 skilled specialists. Equipped with automated multi-axis Swiss-type CNC lathes and hot heading presses, we maintain strict dimensional tolerances down to ±0.005 mm. Standard M14, M16, M18, M20, M22, and M24 rear axle nuts feature flawless 6H internal thread fits, ensuring smooth hand threading and precise engagement.
Rapid Prototyping & OEM/ODM Support
We offer 3-day rapid turnaround on custom prototype axle nuts from customer CAD drawings or physical reference parts. Standard catalog configurations ship within 24 hours from stock, while customized bulk production runs are fulfilled in 7 to 15 days. We provide white-label laser marking (custom logos, torque indicators) and eco-friendly custom blister packaging for French retail distribution.
Looking for Custom Titanium Axle Nuts for Your Lyon Workshop or Brand?
Send us your dimensional drawings (STP, CAD, PDF) or OEM part numbers. Our technical engineering desk delivers DDP pricing and feasibility evaluations within 7 hours.
Frequently Asked Questions: Sourcing Titanium Fasteners in Lyon
Clear, direct answers regarding European trade regulations, customs clearance, shipping logistics to Lyon Saint-Exupéry, material authenticity, and engineering fitment.
What thread pitches and sizes are available for European and Japanese motorcycles in Lyon?
We manufacture motorcycle axle nuts across the complete spectrum of OEM and race specifications: M14×1.5, M16×1.5, M18×1.5, M20×1.5, M22×1.5, M24×1.5, and M25×1.25. These cover dominant motorcycle platforms in France, including Yamaha MT/YZF series, BMW S1000RR/GS, Ducati Panigale/Multistrada, Triumph Speed Triple, and KTM RC/Duke ranges. We also produce custom pitch variations and self-locking bi-hexagonal or castellated designs based on CAD drawings.
How are customs clearance, French VAT (TVA), and import duties handled when shipping to Lyon?
We accommodate both DAP (Delivered at Place) and DDP (Delivered Duty Paid) Incoterms 2020. Under DDP terms, our logistics division manages all customs declarations, French import duties, and 20% TVA through our forwarding partners, delivering shipments directly to your door in Lyon, Villeurbanne, Saint-Priest, or anywhere in the Auvergne-Rhône-Alpes region without administrative friction or unexpected border fees.
What is the standard shipping lead time to Lyon Saint-Exupéry Airport (LYS)?
For urgent workshop requirements and prototype evaluations, sample orders and stock items ship via DHL, FedEx, or UPS Priority Air Freight, landing at Lyon-Saint Exupéry (LYS) in 3 to 5 business days. Bulk production shipments (500 to 10,000+ pieces) can be dispatched via air freight consolidation (5–7 days) or dedicated rail/sea container freight to European logistics hubs for maximum freight cost efficiency.
What material certifications are provided to verify genuine Ti-6Al-4V Grade 5 titanium?
Every shipment is accompanied upon request by an authentic EN 10204 Type 3.1 Mill Test Certificate (MTC) traceable to the furnace heat number. This document validates the exact chemical breakdown (Titanium balance, 5.5–6.75% Aluminum, 3.5–4.5% Vanadium, Iron ≤0.40%, Oxygen ≤0.20%) and confirms mechanical performance, including tensile strength (≥ 895 MPa), yield strength (≥ 828 MPa), and elongation percentages.
What torque values should be applied to titanium axle nuts compared to stock steel fasteners?
Because Grade 5 titanium shares similar yield strength to high-tensile steel, stock OEM torque figures can generally be maintained, provided anti-seize paste is applied. The anti-seize lubricant lowers the friction coefficient; consequently, we advise setting your torque wrench to 85% to 90% of the OEM dry torque spec to achieve equivalent spindle clamping force without over-stretching the threads. Never install titanium axle hardware dry.
What is the Minimum Order Quantity (MOQ) for custom-machined or private-label axle nuts?
Standard catalog items (plain, natural polished, or common anodized colors) require an MOQ of just 100 dozens (or 100 units for large diameter spindle nuts). For fully custom, drawing-based OEM projects involving unique flange widths, wire-lock drillings, or bespoke thread pitches, our prototype MOQ starts at only 100 pieces, allowing French speed shops and racing ateliers to validate fitment before full-scale volume production.
Connect Directly with Our Titanium Technical Engineering Team
Get factory-direct quotation sheets, 3D CAD reviews, and material test documentation for your next motorcycle hardware order in Lyon.
