High-Torque Titanium Wheel Bolts & Specialty Fasteners
Manufactured from certified Ti-6Al-4V Grade 5 bar stock with rolled threads exceeding DIN/ISO standards. Designed specifically for track-day stability at Circuit of The Americas (COTA), Texas Hill Country endurance racing, and high-spec aftermarket tuners in Austin.
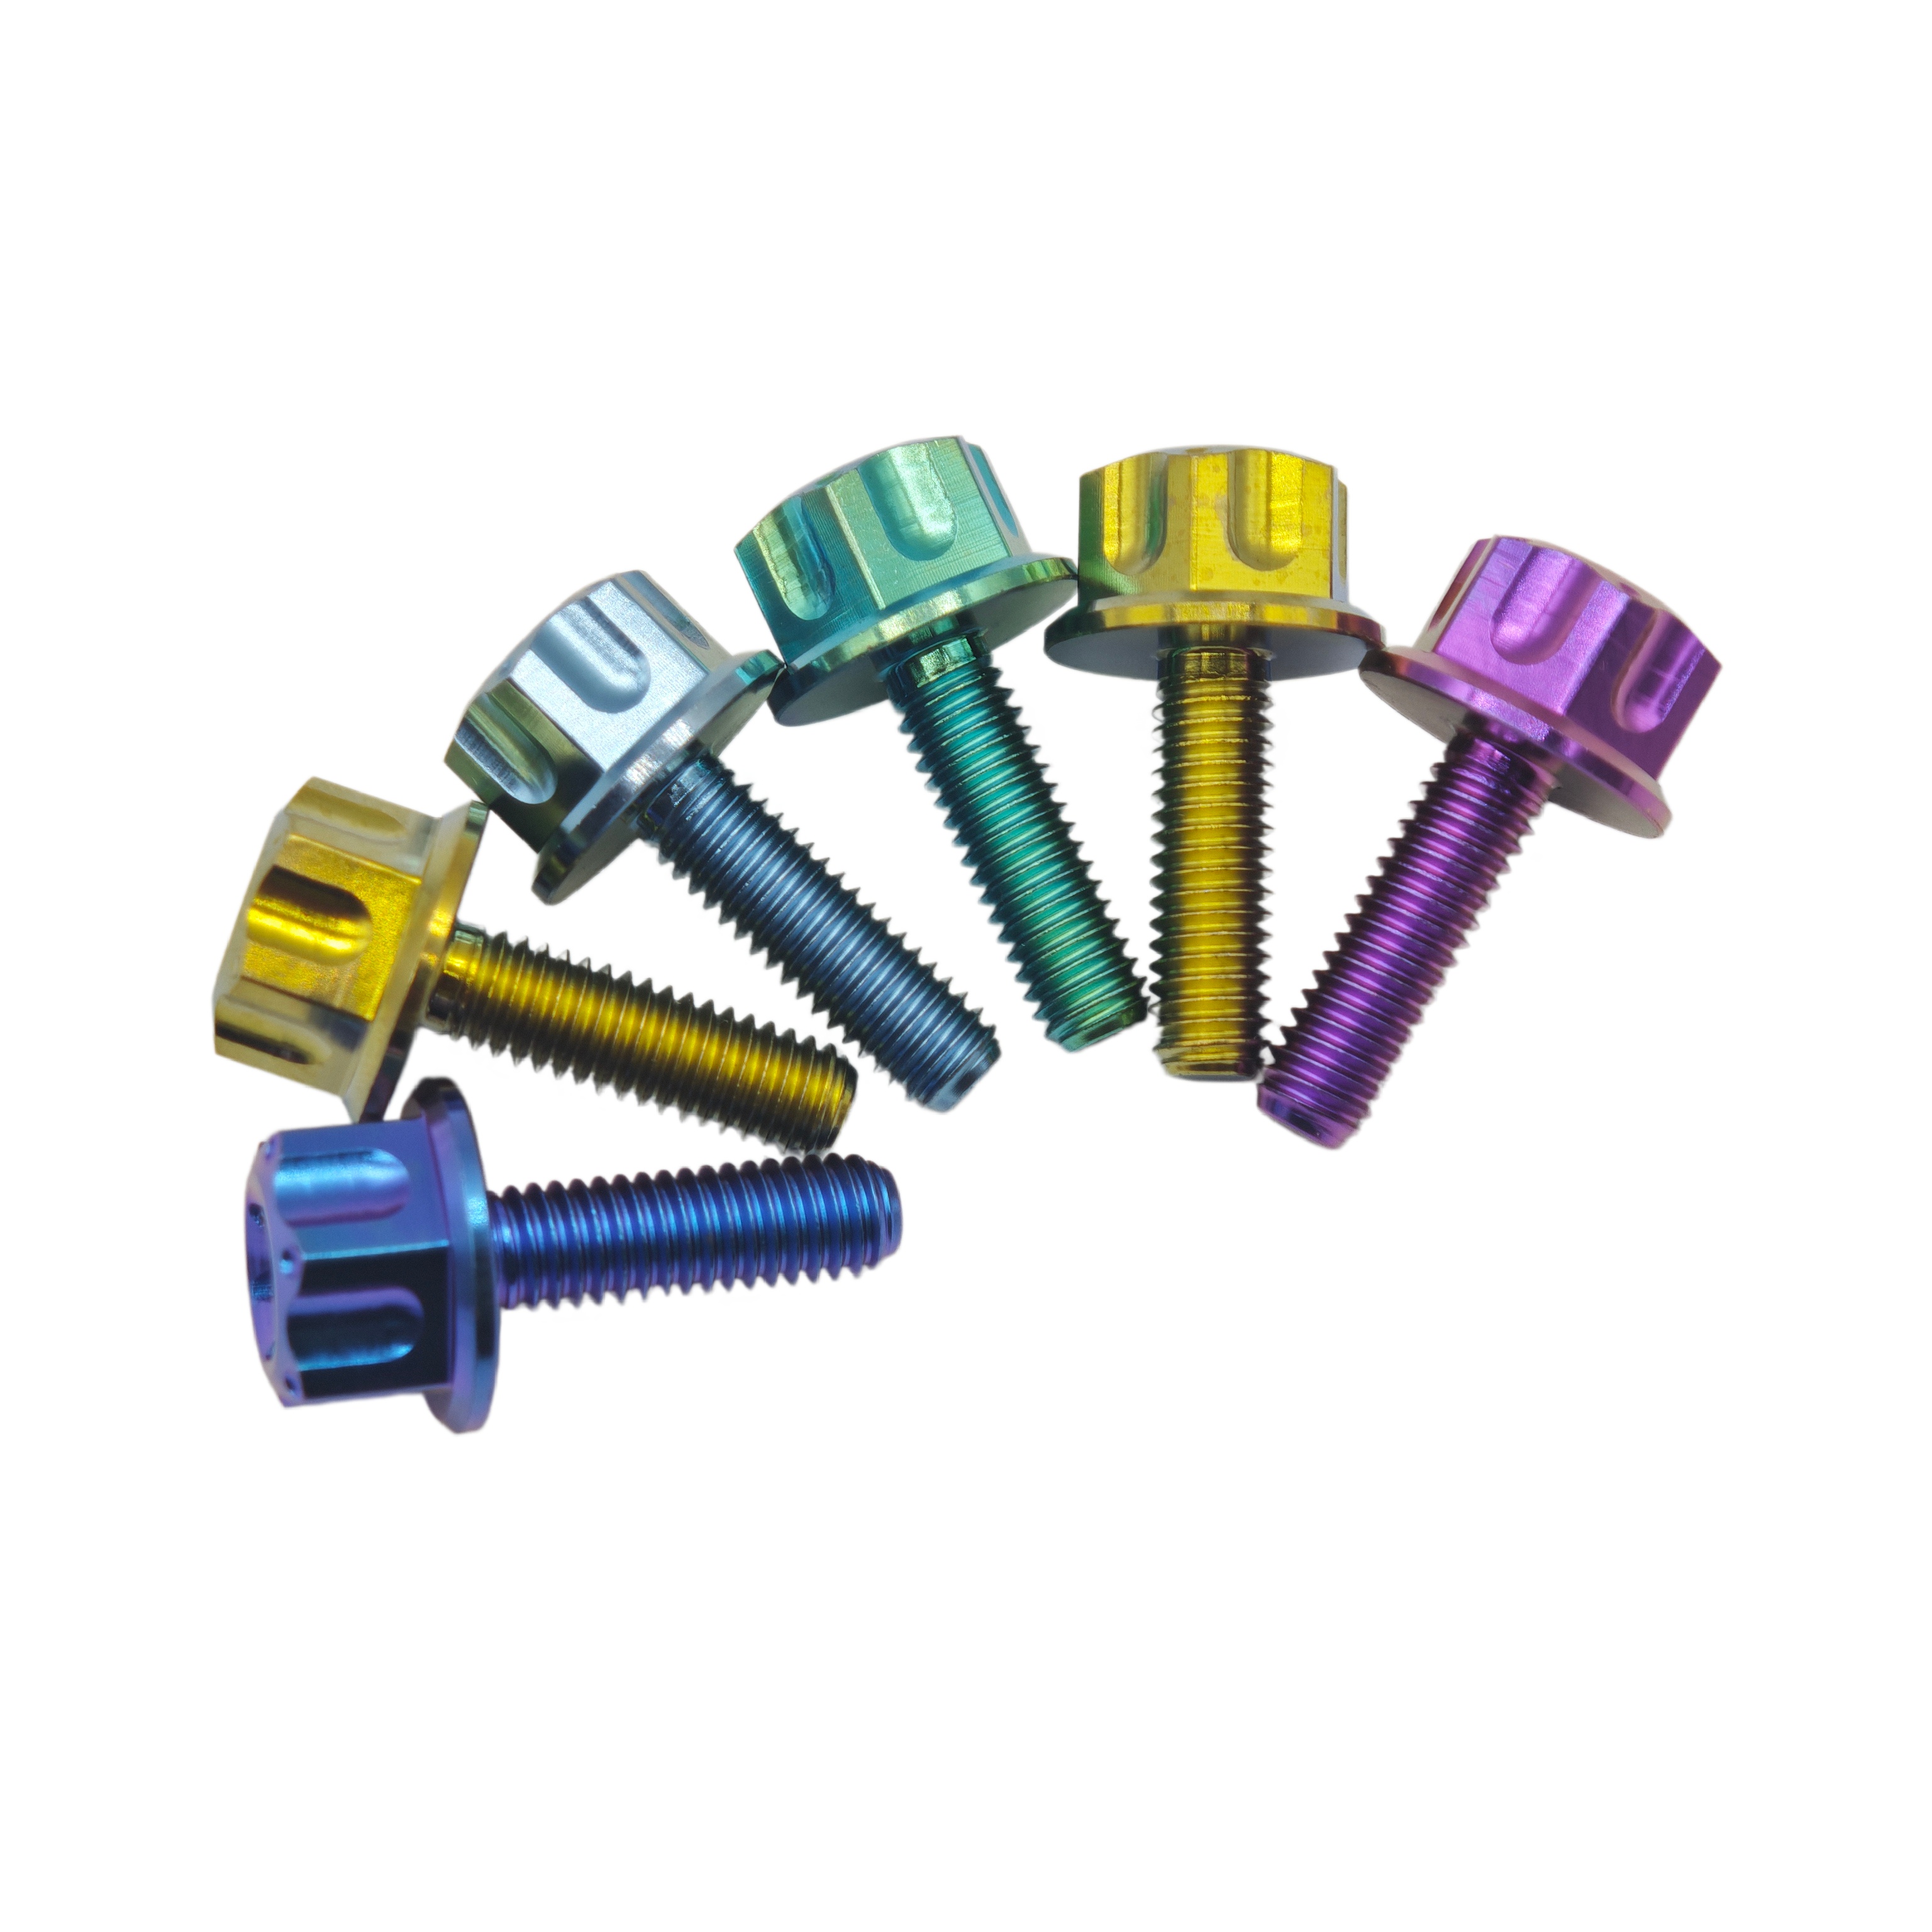
TECKSR M4 Anodized GR5 Titanium Hex Flange Head Torx UNF Bolts
Precision-machined hex flange Torx bolts with anti-cam-out engagement. Ideal for motorcycle fairings, perimeter rotor accents, and telemetry sensor mounting.
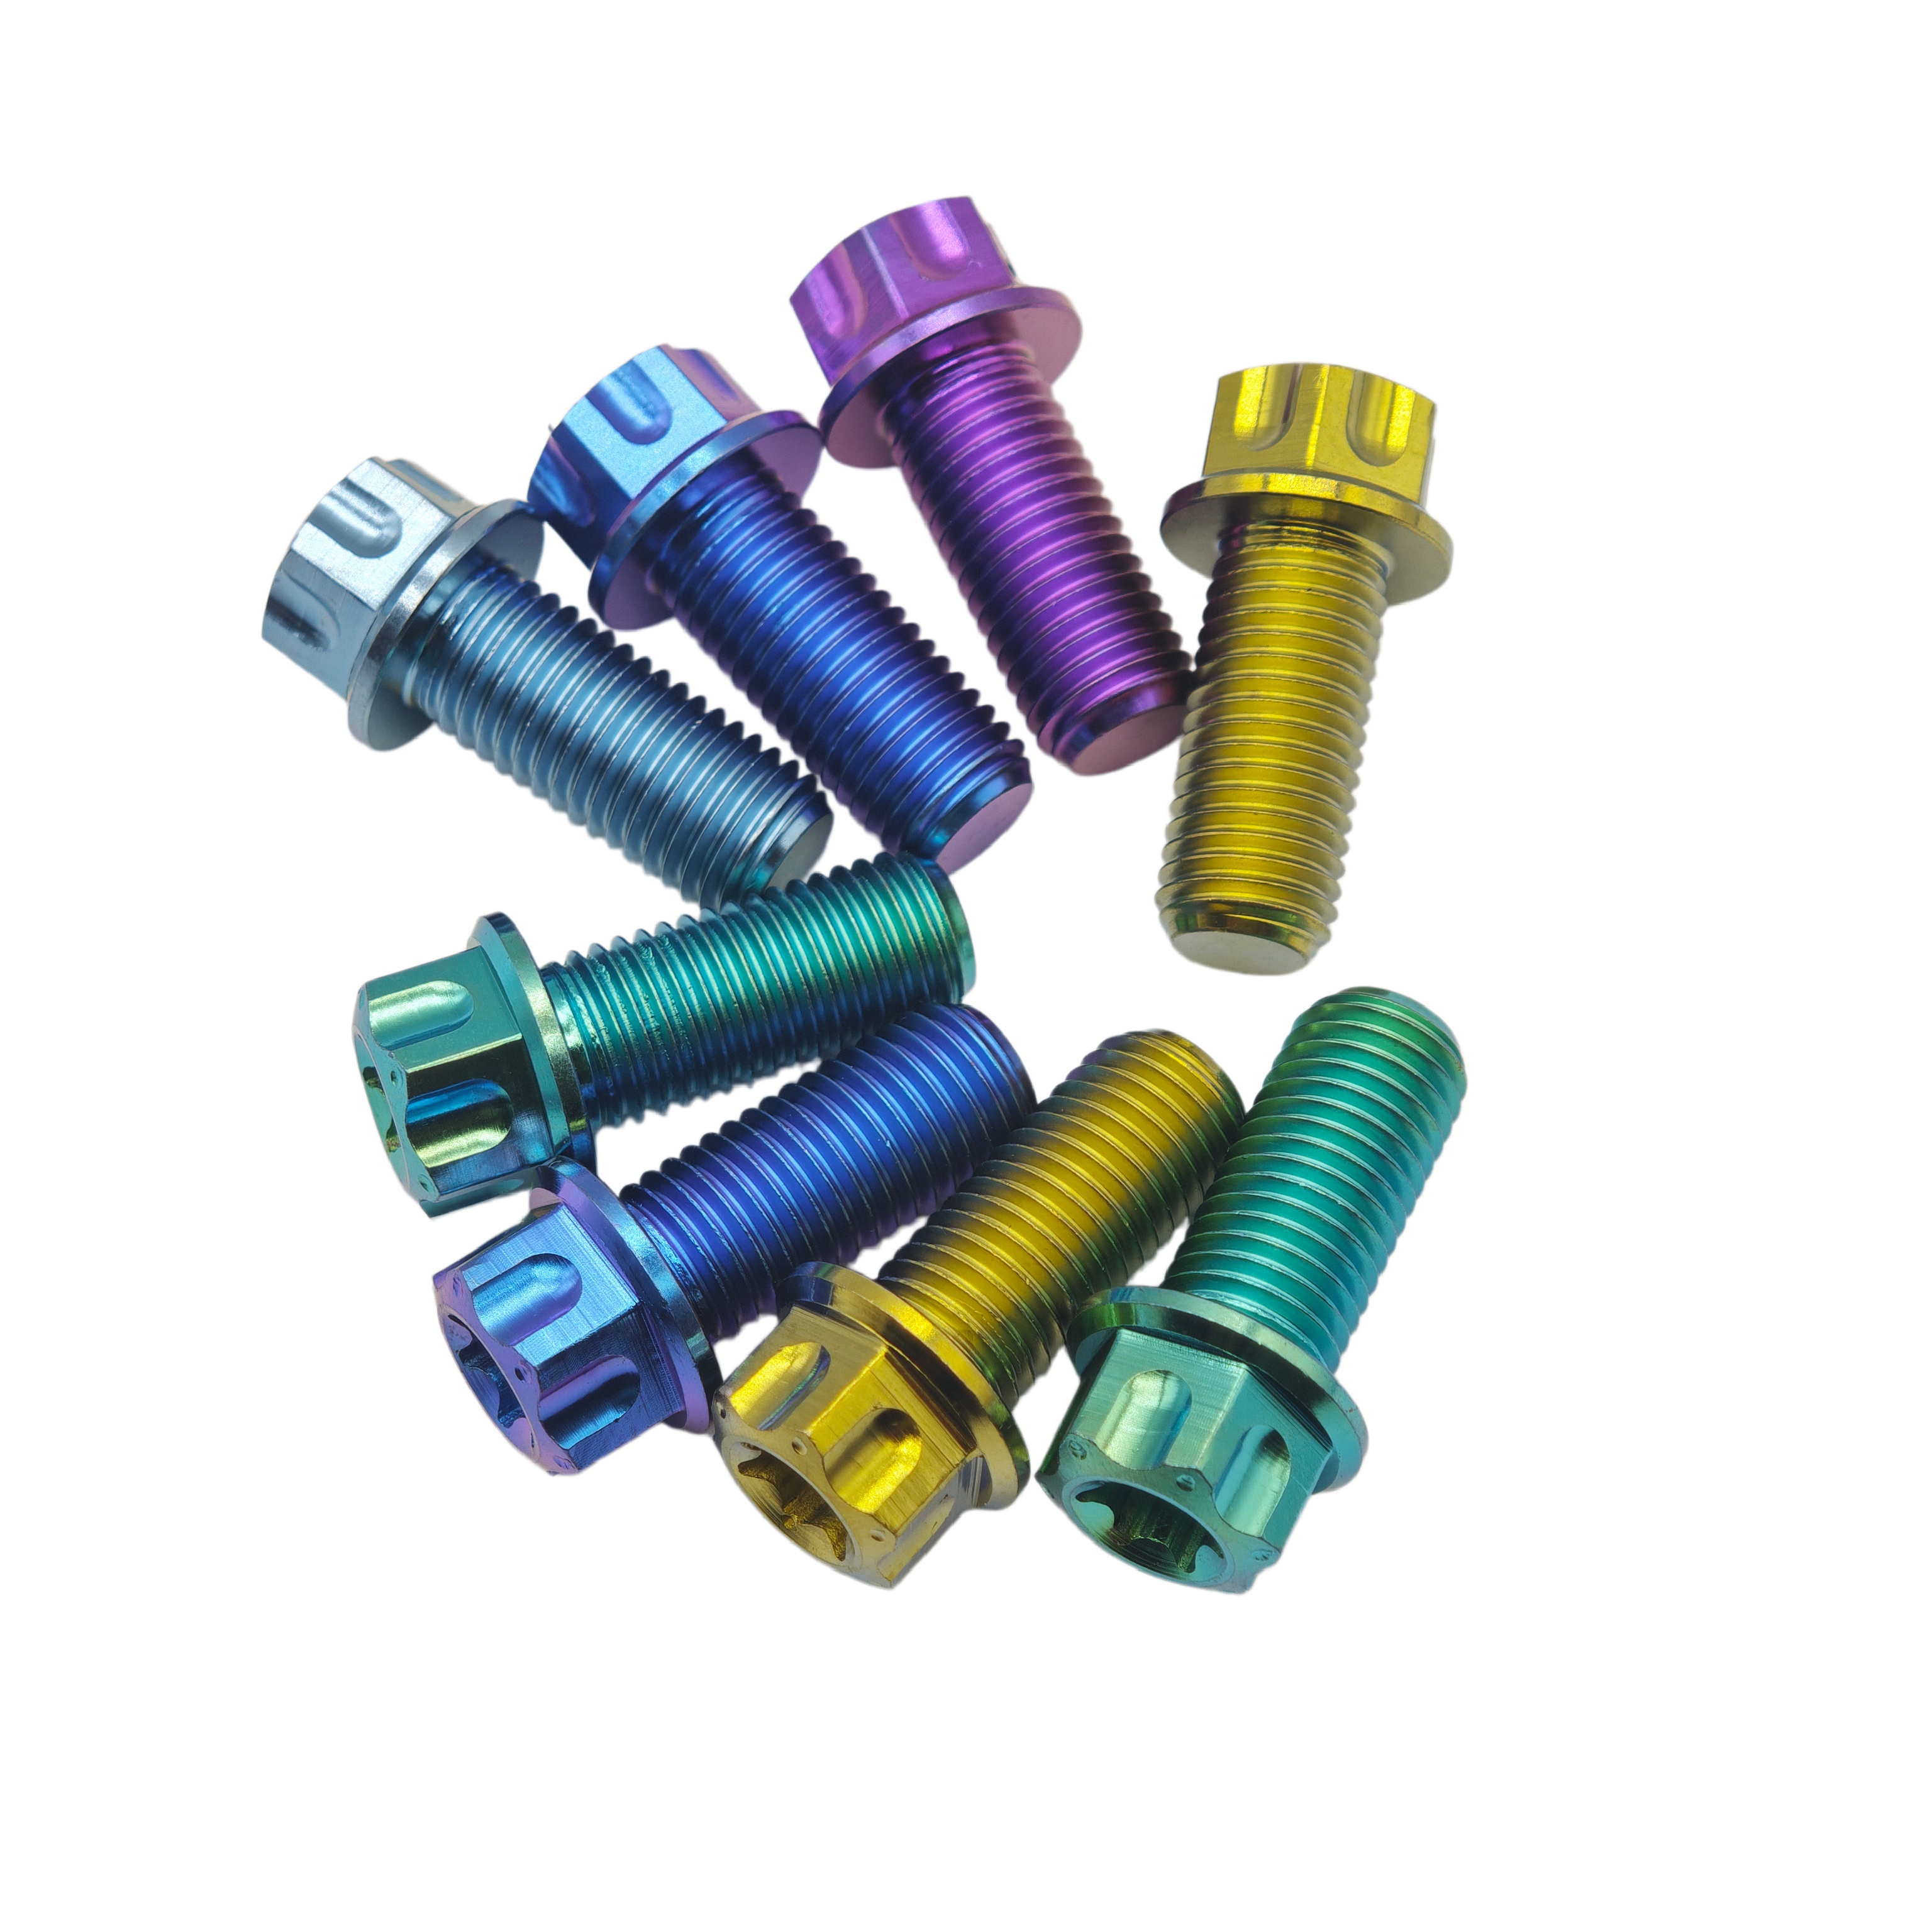
Factory Wholesale Anodized GR5 Titanium Hex Flange Bolts M8/M10
Engineered for high-shear brake caliper mounts, suspension links, and wheel hubs. Features rolled threads with 950 MPa minimum tensile yield strength.
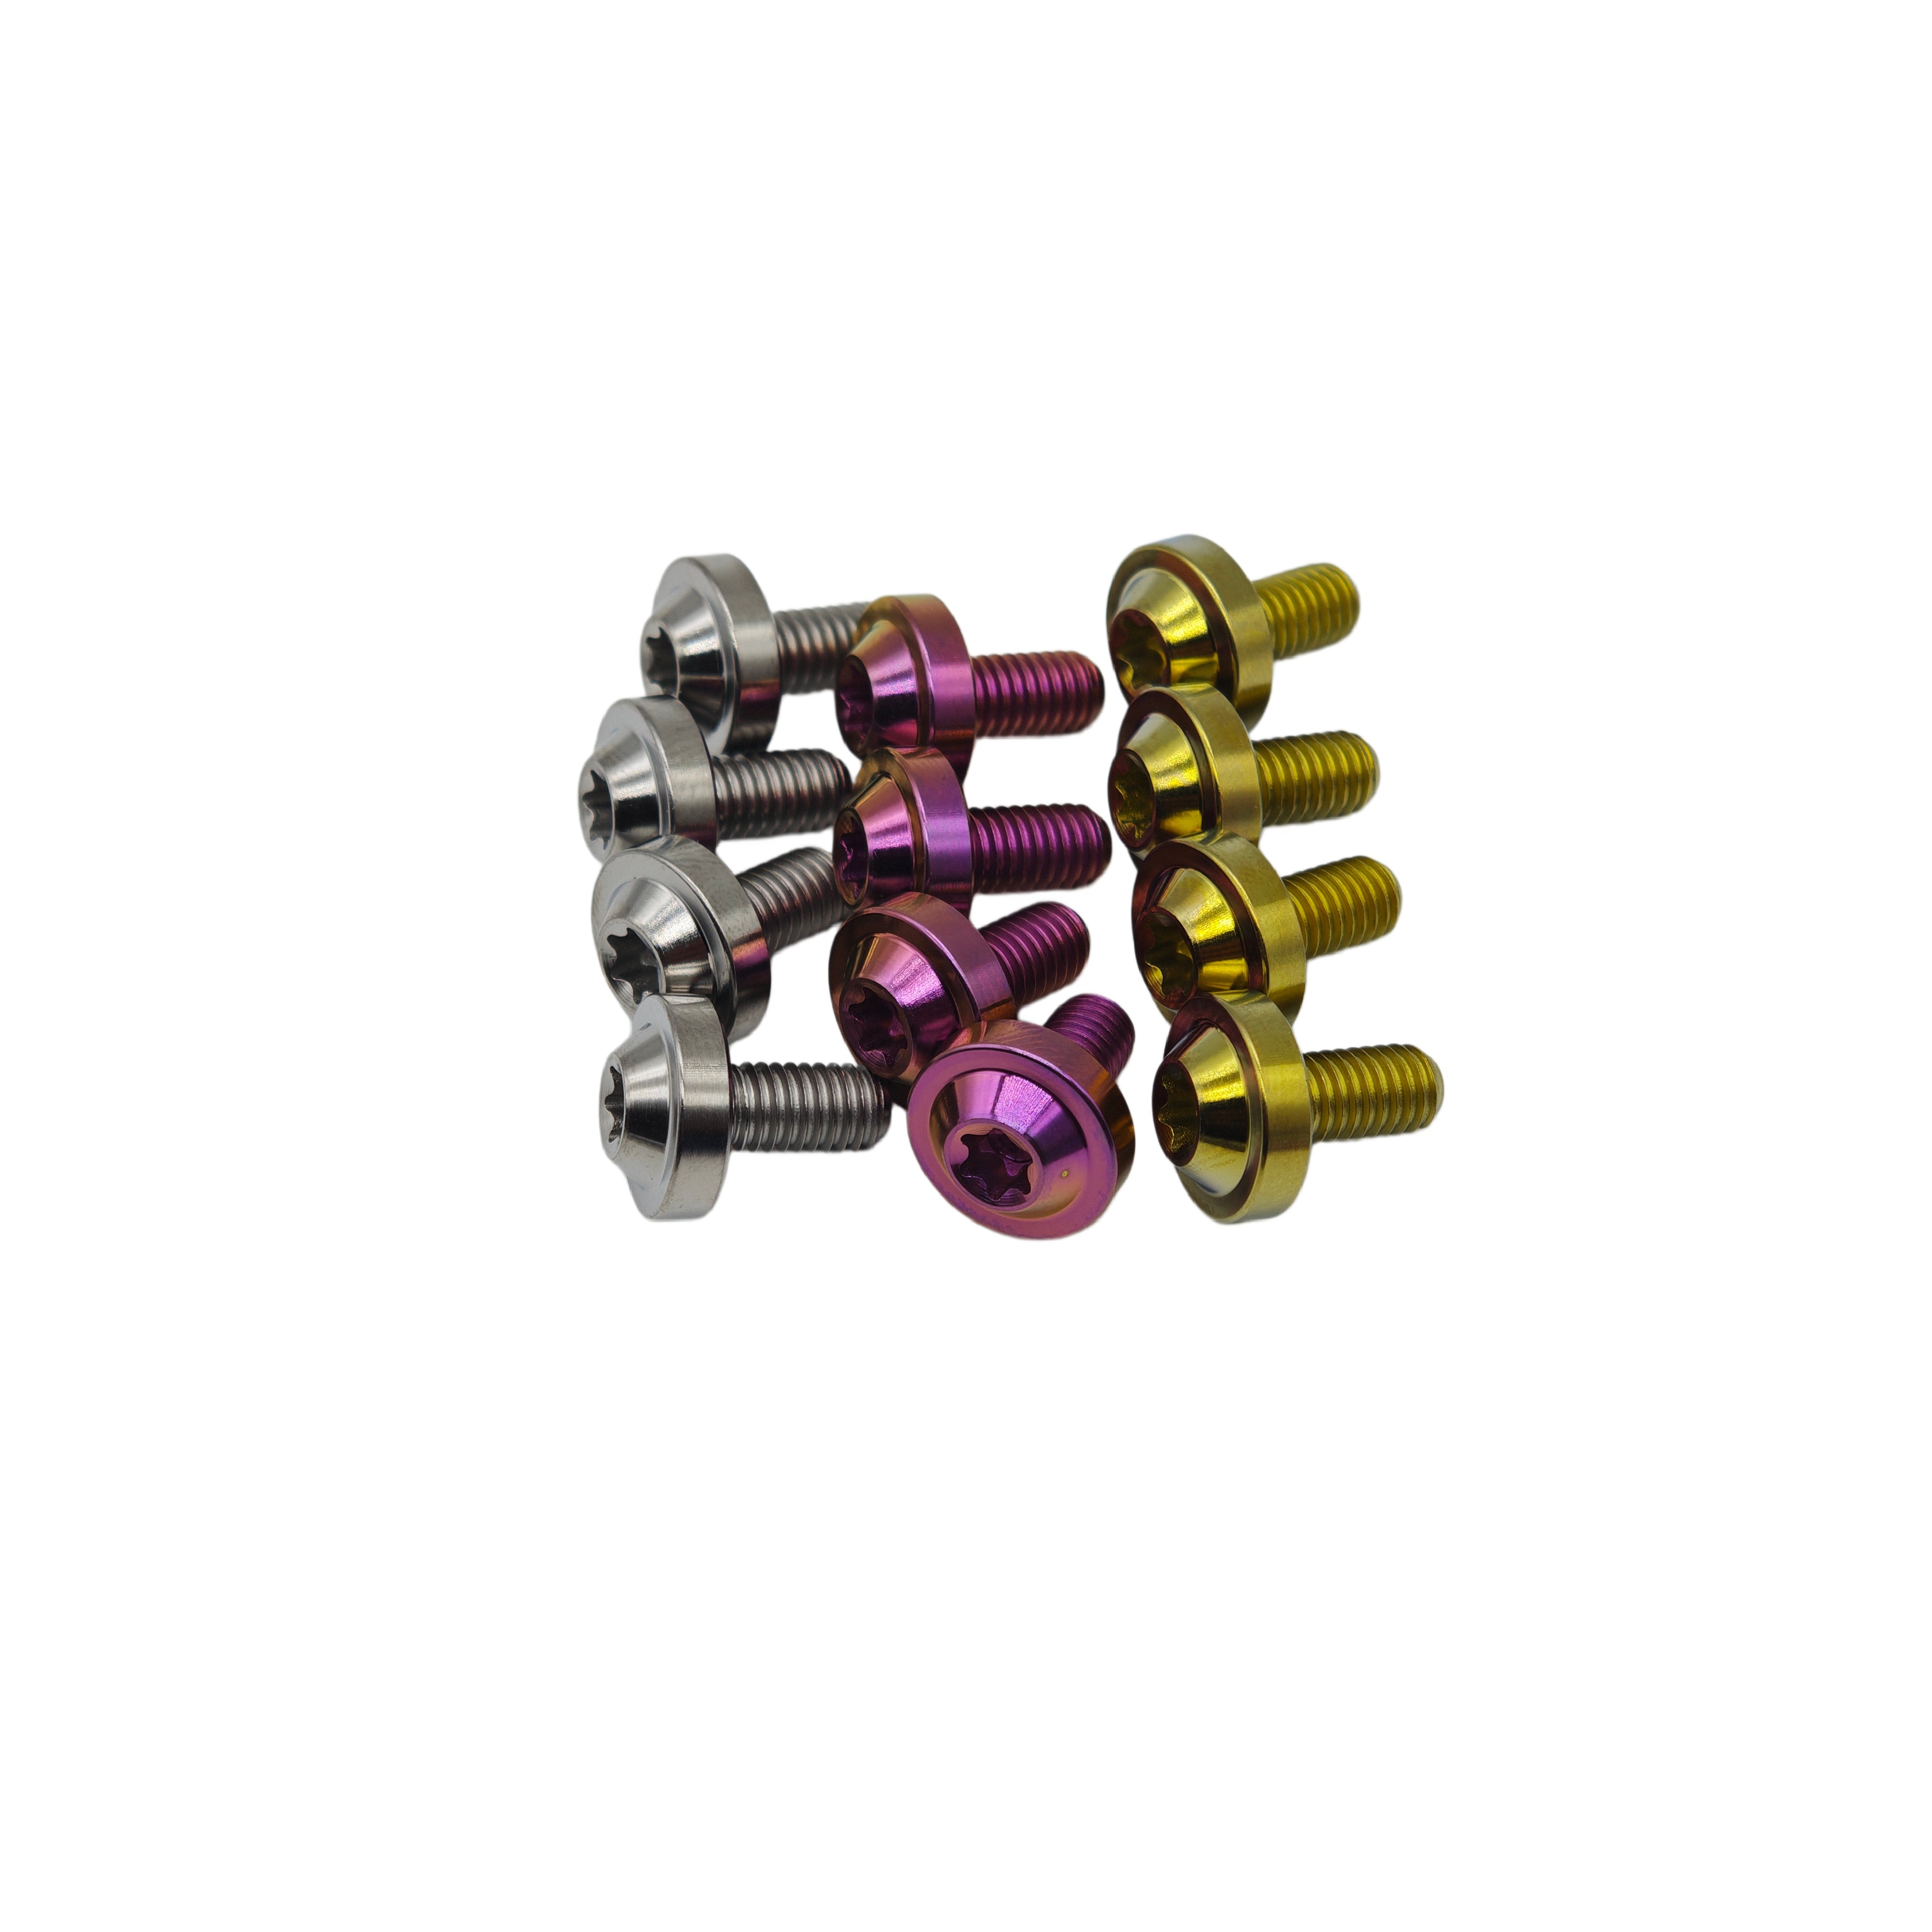
Custom GR5 Titanium M8 Disc Head Bolts with Plain Finish
Ultra-low profile head design prevents clearance friction with caliper bodies. CNC turned from annealed Gr5 bar stock for extreme thermal resistance.
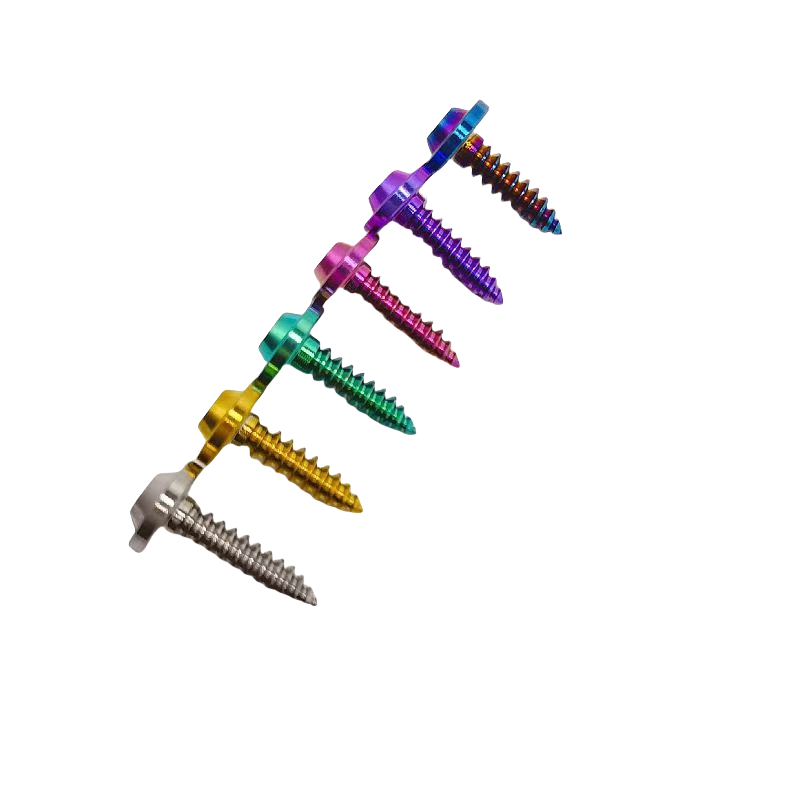
M4/M5 Blue-Grey Titanium Pan Head Self-Tapping Screws DIN Spec
High-hardness PVD titanium nitride coating prevents thread galling in carbon composite panels, composite wheel fairings, and motorsport aerodynamic strakes.
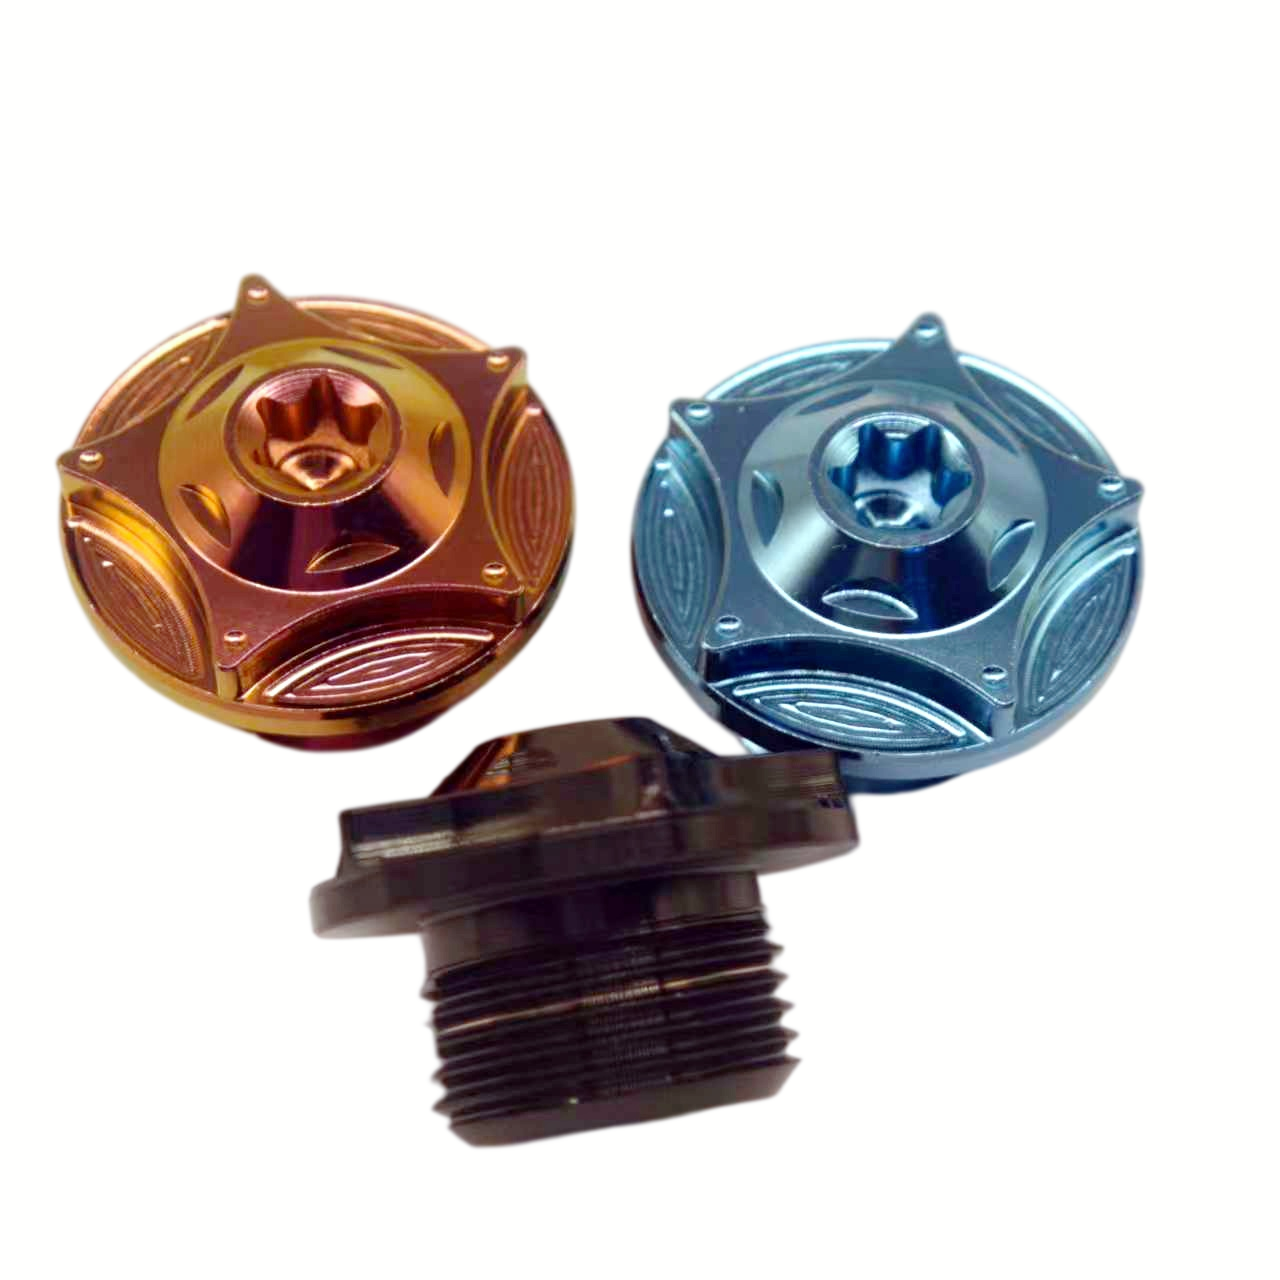
Engine Parts M14 Titanium Gr5 Nuts & Magnetic Sump Drain Plugs
Engineered for extreme heat cycles up to 400°C without thread elongation. Features pre-drilled safety wire lock ports for track regulation compliance.
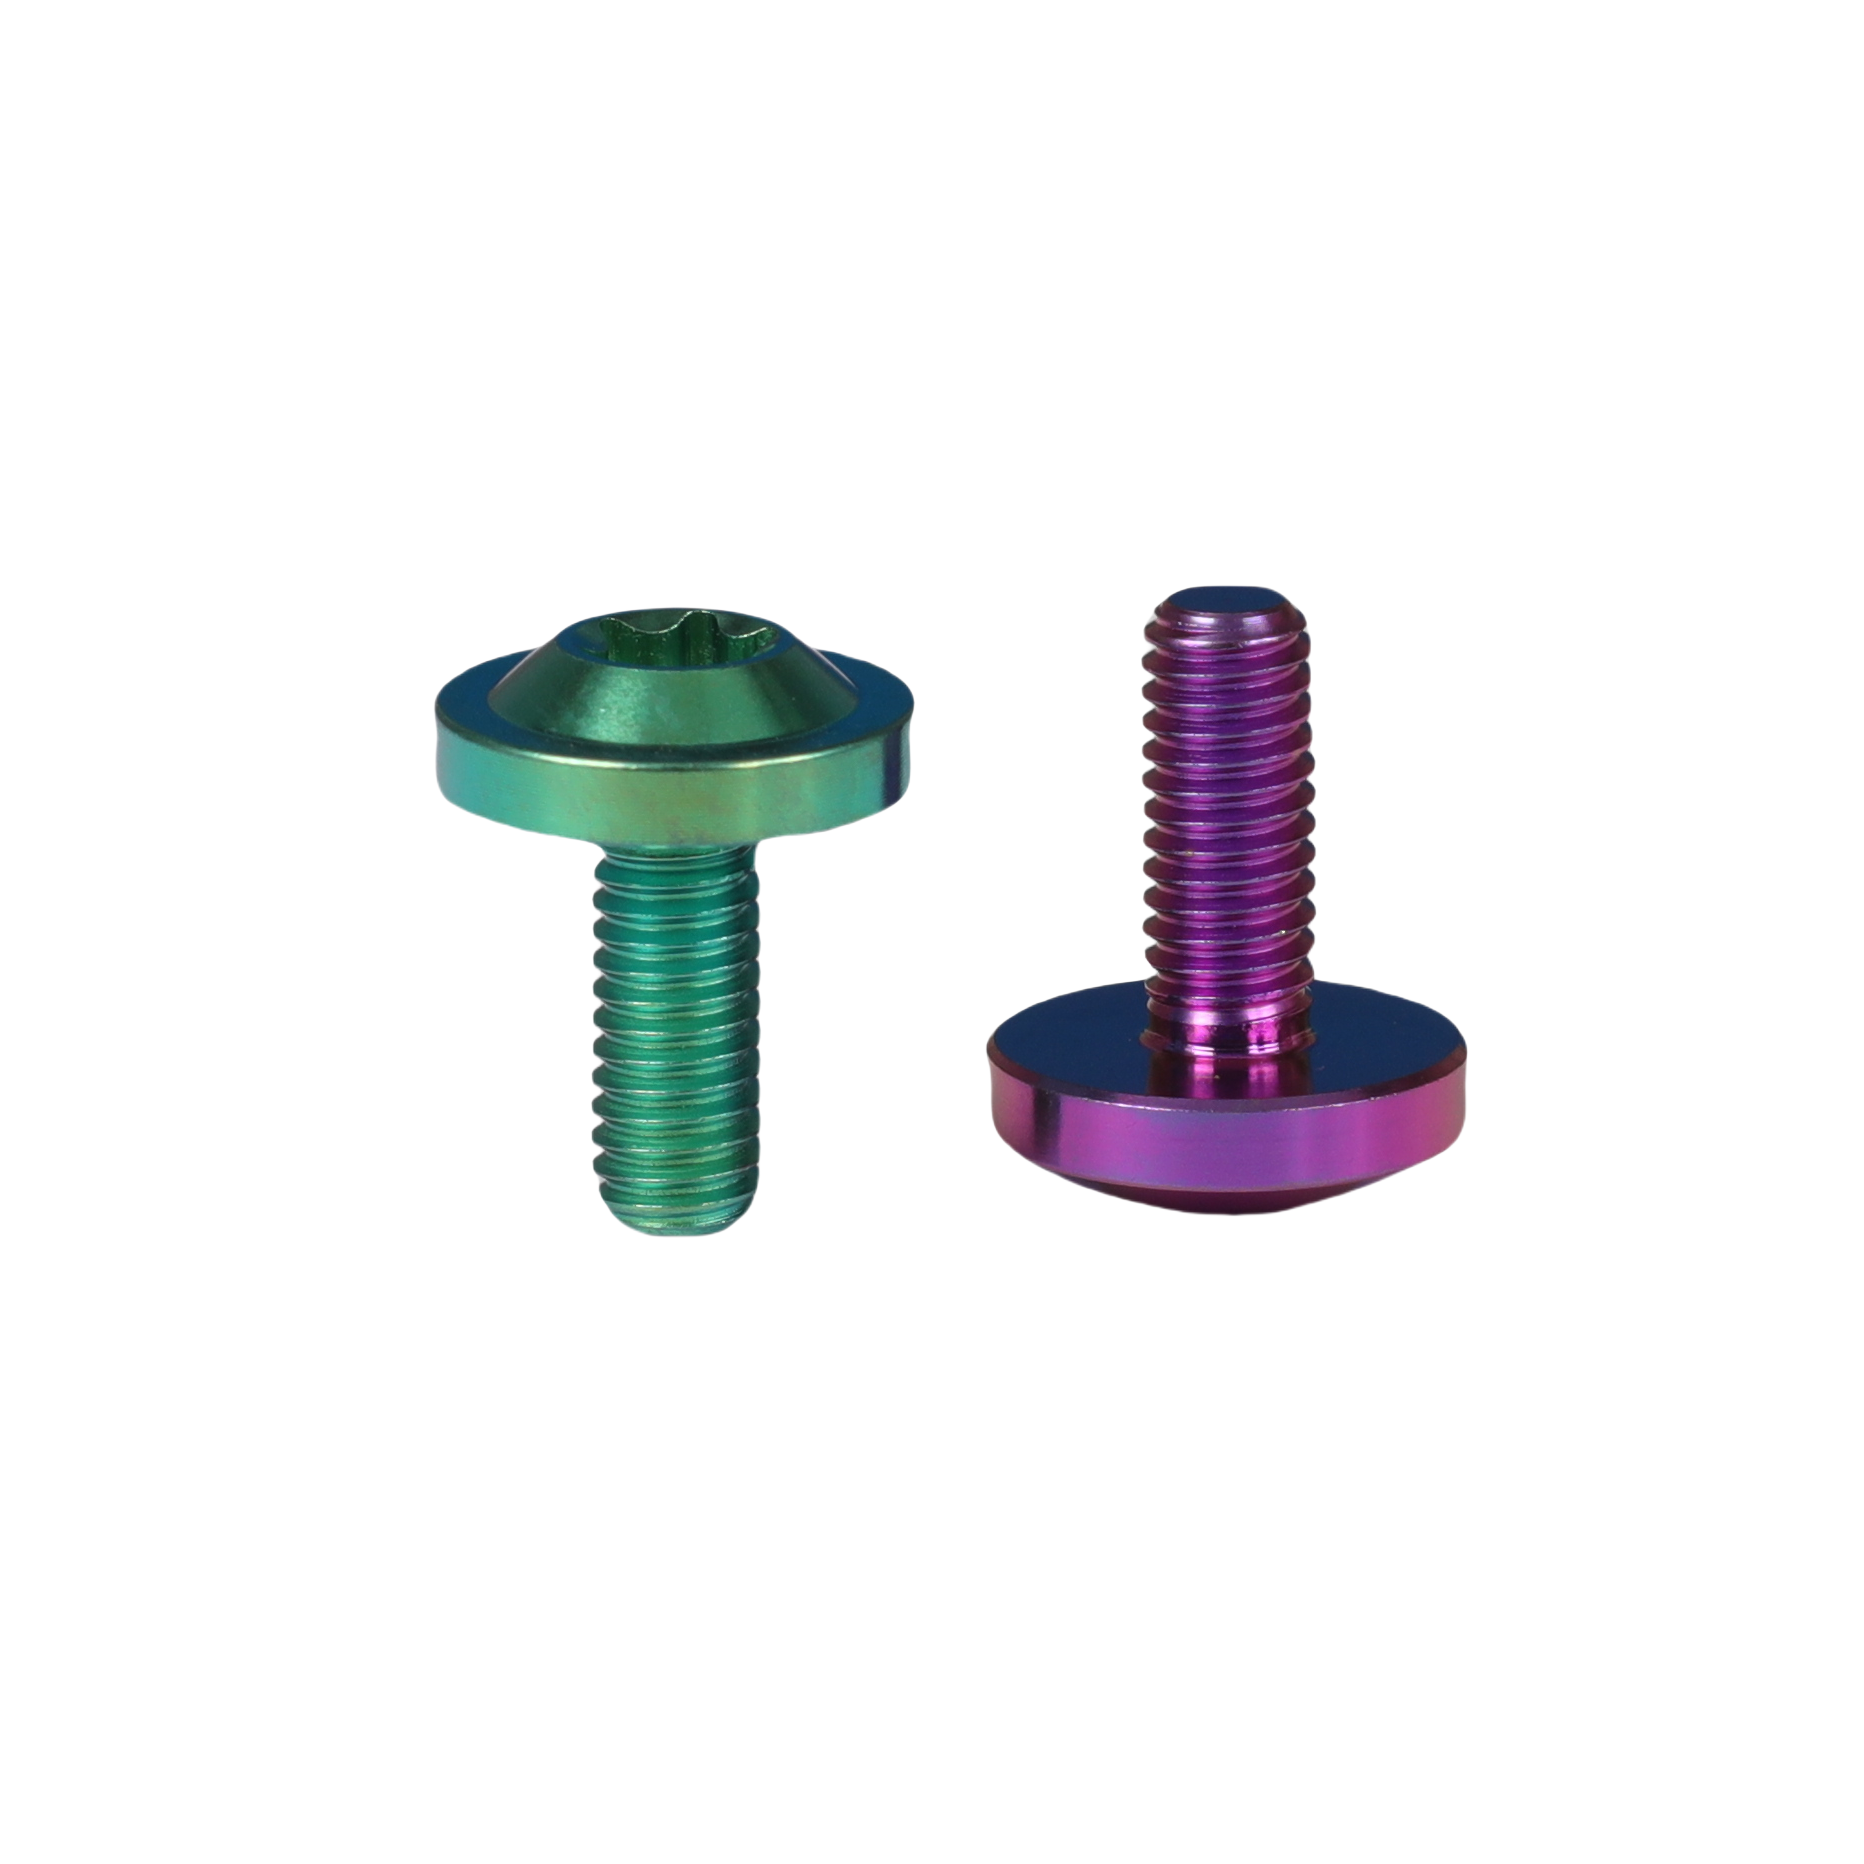
Factory Supply Class 6 M6×15 GR5 Titanium Pan Head Anodized Screw
Class 6g precision thread pitch ensuring zero play in high-vibration automotive chassis setups. 44% lighter than standard grade 8.8 and 10.9 steel fasteners.
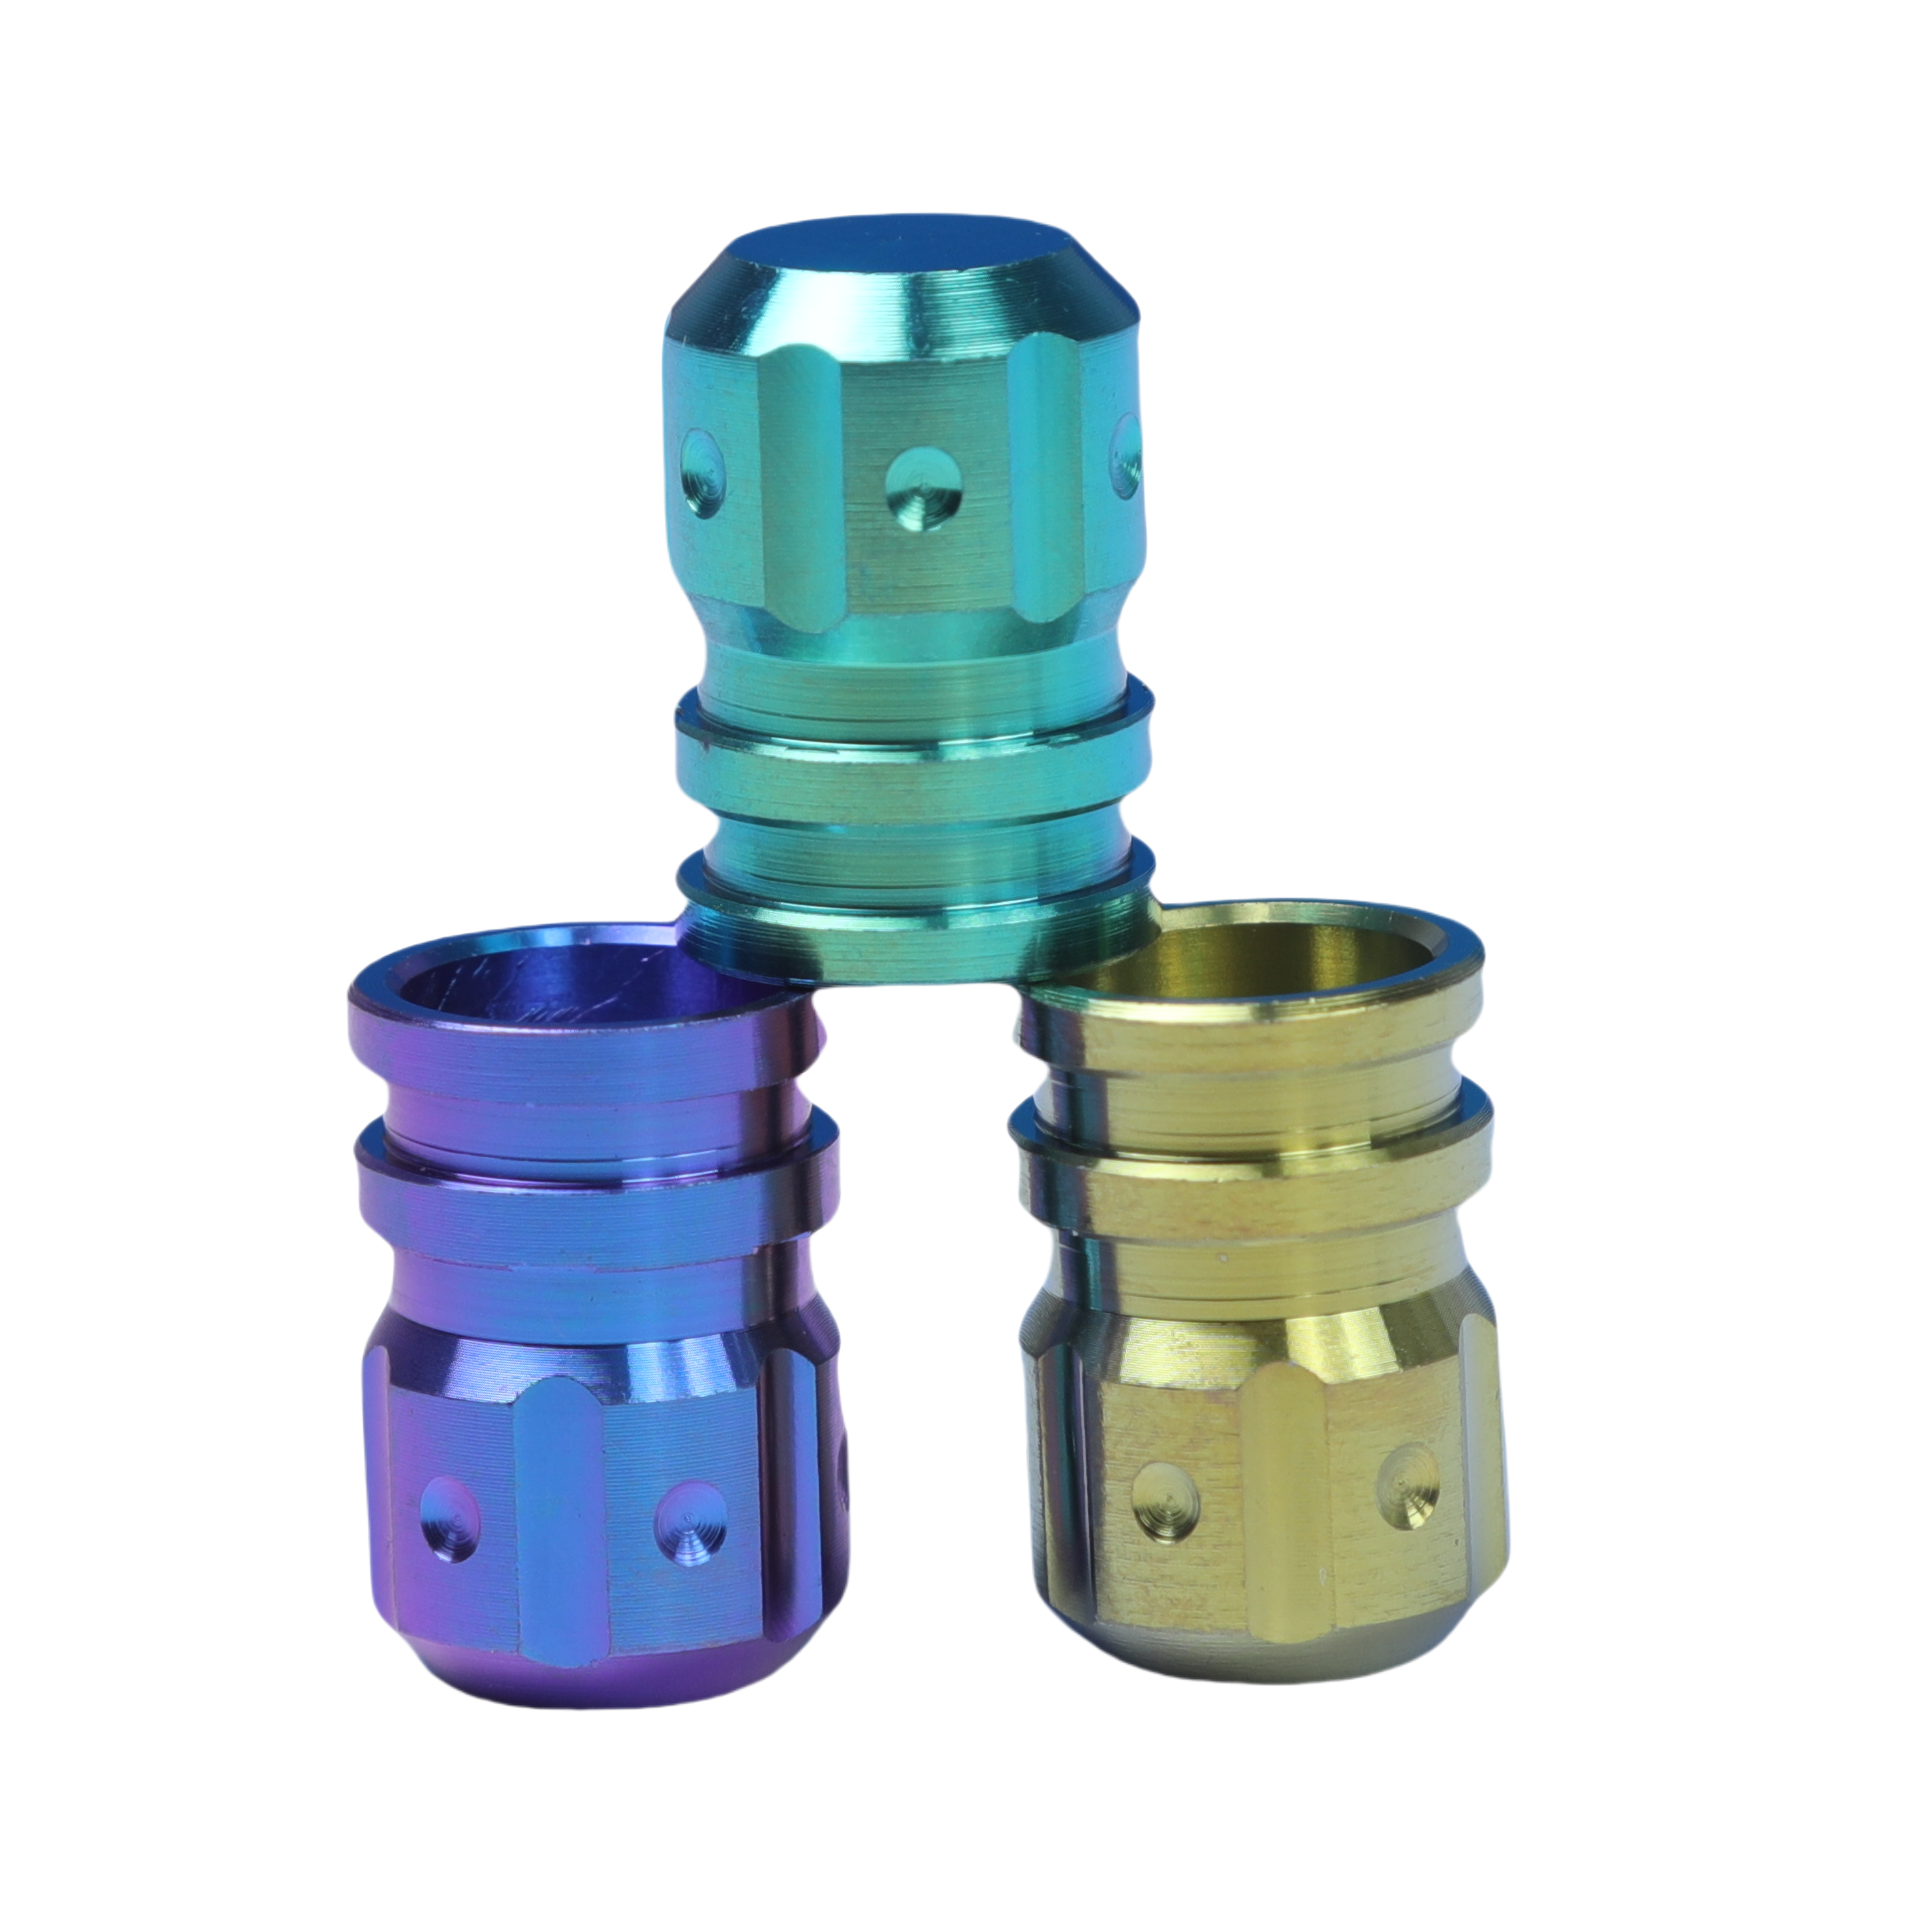
Universal Titanium Alloy Wheel Valve Stem Dust Caps & Locking Nuts
Internal viton O-ring seal immune to high-temperature wheel barrel expansion during COTA track sessions. Chemical resistant to aggressive brake dust cleaners.
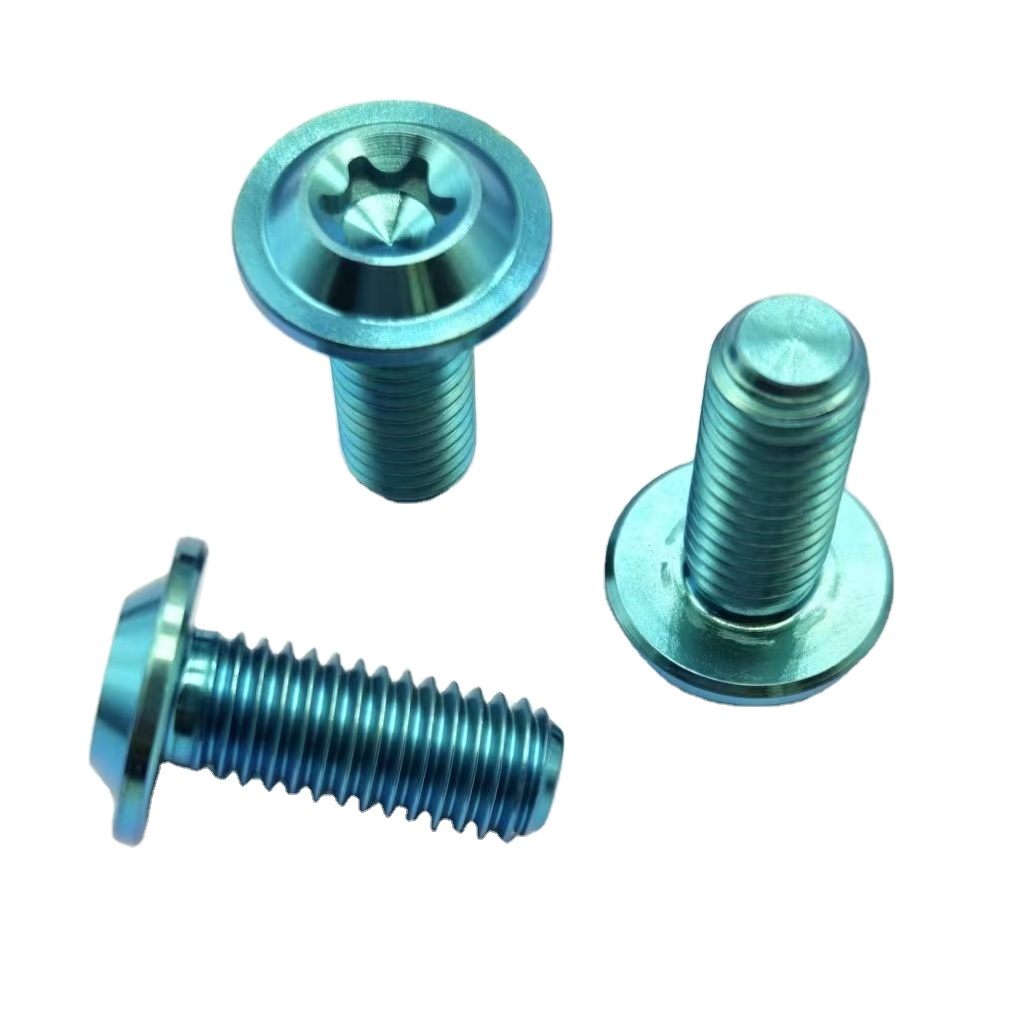
Customized M8 Gr5 Titanium Alloy Pan Head High-Tensile Bolts
Designed for subframe assemblies, wheel carrier attachments, and powertrain fixtures where tensile strength above 900 MPa and zero magnetic signature are mandated.
Engineering Titanium Fasteners for Central Texas Extreme Thermal & Dynamic Loads
A comprehensive examination of why Grade 5 Titanium (Ti-6Al-4V) outperforms standard Grade 10.9/12.9 carbon steel wheel bolts under track conditions at Circuit of The Americas and demanding high-performance EV platforms.
Rotational Inertia & Unsprung Mass
In motorsport dynamics, unsprung weight reduction directly elevates suspension damping frequency, tire contact patch consistency, and steering response. Switching an Austin track vehicle's 20 wheel bolts from steel (approx. 2,400 g total) to Zunvo Grade 5 Titanium (approx. 1,320 g total) yields an unsprung rotational saving of over 1.08 kg at the wheel hubs. This translates to an exponential reduction in rotational inertia under acceleration and braking on COTA’s turn 1 uphill entry.
Thermal Cycling & Creep Resistance
Summer track temperatures at Circuit of The Americas regularly push asphalt above 135°F (57°C), while rotor hat temperatures adjacent to the wheel hub exceed 650°C during heavy threshold braking. Carbon steel wheel bolts experience progressive thermal expansion mismatch against forged aluminum wheels, causing clamp force relaxation. Grade 5 Titanium exhibits a coefficient of thermal expansion (8.6×10⁻⁶/K) closely matched to high-grade forged alloy wheels, preventing torque back-off.
Thread-Rolling vs. Lathe Cut Grain Flow
Zunvo titanium wheel bolts utilize CNC hot-heading followed by cold thread rolling rather than single-point lathe cutting. Thread rolling forces the titanium alpha-beta grain structures to follow the contour of each thread root and crest continuously without shearing grain boundaries. This technique increases fatigue resistance by over 300% and virtually eliminates fatigue crack propagation under cyclic cornering loads across the Hill Country switchbacks.
| Mechanical & Physical Property | Zunvo Ti-6Al-4V (Grade 5 Titanium) | OEM Class 10.9 Carbon Steel | Class 12.9 High-Tensile Steel | 6061-T6 Aluminum (Stud Spec) |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 (Aerospace Spec) | 7.85 | 7.85 | 2.70 |
| Tensile Strength (Yield MPa) | ≥ 895 – 950 MPa | 940 MPa | 1,100 MPa | 276 MPa (Unsuitable for Lugs) |
| Ultimate Tensile Strength (MPa) | ≥ 980 – 1,050 MPa | 1,040 MPa | 1,220 MPa | 310 MPa |
| Strength-to-Weight Ratio (kN·m/kg) | 221 (Exceptional) | 132 | 155 | 115 |
| Corrosion Resistance (Road Salt / Brake Fluid) | Immune (Forms Self-Healing TiO₂ Layer) | Poor (Requires Zinc/Phosphate Coating) | Prone to Hydrogen Embrittlement | Susceptible to Galvanic Pitting |
| Service Thermal Threshold | Stable up to 400°C (752°F) | Relaxation begins above 250°C | Risk of temper softening | Critical loss of yield above 120°C |
| Thread Manufacturing Standard | Cold Rolled Thread (Continuous Grain) | Rolled / Cut | Rolled | Machined |
Primary Application Scenarios Across Greater Austin
From trackside pits in Del Valle to boutique hypercar tuning facilities in Round Rock and the high-tech EV corridor in Travis County, Zunvo titanium fasteners anchor Austin's most sophisticated mechanical projects.
Circuit of The Americas (COTA) Club Racing
Track-day drivers campaigning GT3, GT4, and TA2 platforms encounter extreme lateral G-forces entering COTA's multi-apex complex (Turns 16, 17, and 18). Steel wheel bolts under recurring torque cycles suffer micro-stretch. Zunvo M14×1.5 and M14×1.25 titanium wheel stud conversions and floating-collar lug bolts ensure rock-solid clamp load without shearing or seizing, even during 45-minute sprint races under 100°F ambient Texas sun.
Electric Vehicle Mass Reduction Corridors
Austin is a global focal point for advanced EV engineering. With battery packs introducing substantial baseline tare weight, unsprung mass savings become doubly vital for preserving damper reaction speed, tire longevity, and range efficiency. Local tuning ateliers retrofitting bespoke forged wheels on performance EV saloons utilize Zunvo titanium wheel bolts to shave critical rotating weight while introducing striking PVD burnt-blue or stealth satin finishes.
Custom Superbike & Hill Country Moto Builds
The winding roads of Lime Creek, Devil's Backbone, and Willow City Loop attract dedicated superbike riders. Local custom builders in East Austin and South Congress specify Zunvo titanium rotor bolts, subframe screws, and closed-cap axle nuts. These parts resist chemical breakdown from road grime and engine solvents while offering unmatched aesthetics and safety wire security for aggressive canyon carving.
Austin Market Procurement Trends & Direct-Factory Supply Stability
How Austin tuning shops, aftermarket distributors, and race engineering outfits eliminate middleman markups by leveraging Zunvo's mill-direct manufacturing base in Baoji, China.
Bespoke Thread & Collar Prototyping
Standard aftermarket catalog bolts often fail to seat correctly on custom multi-piece forged wheels. Austin buyers increasingly request custom conical 60° floating washers, radius ball seats (R12/R13/R14 for European fitments), and extended shank lengths (28mm to 65mm) for wheel spacer integration.
Traceable Mill Certifications
Due to safety liabilities at track speeds exceeding 160 mph, Austin procurement teams demand verifiable Material Test Reports (MTR) verifying titanium chemical compositions (Ti balance, 5.5–6.75% Al, 3.5–4.5% V) and ultrasonic flaw detection before clearing fasteners for track usage.
Direct Texas Logistics Routing
By routing shipments via Austin-Bergstrom International Airport (AUS) air express for time-sensitive race prep or consolidated ocean freight via the Port of Houston for warehouse bulk stocking, Zunvo eliminates coastal distributor markups, cutting procurement costs by 35% to 48%.
Private-Label Retail Packaging
Performance garages and speed shops throughout the Austin-Round Rock-San Marcos metro area leverage Zunvo’s OEM private labeling services, receiving laser-etched custom logos on bolt heads along with branded blister cards and retail foam-cut presentation cases.
Austin Automotive & Track Buyer Frequently Asked Questions
Essential guidance on torque specifications, galvanic corrosion prevention with aluminum wheel hubs, anti-seize paste selection, and track compliance.
What torque specification should be applied to Gr5 titanium wheel bolts?
Titanium Grade 5 fasteners should generally be torqued to the original equipment manufacturer's (OEM) recommended dry steel torque specification, provided an appropriate anti-seize compound is used. For typical M14×1.5 automotive applications, this ranges between 130 N·m to 145 N·m (96 to 107 lb-ft). Because titanium has a different friction coefficient than steel, never use dry threads. We recommend calibrating torque wrenches specifically for titanium installations.
How do you prevent galvanic corrosion between titanium bolts and aluminum wheel hubs?
Galvanic corrosion requires an electrolyte (such as water containing road salts) and direct electrical contact between metals with dissimilar galvanic potentials. In dry Central Texas conditions, galvanic reaction is minimal, but track washes and coastal humidity can introduce moisture. Applying a thin coating of nickel-based anti-seize lubricant or specialized fluoropolymer paste to the bolt threads and seating surfaces creates a continuous barrier that completely prevents galvanic bonding.
Can titanium wheel bolts pass tech inspection at Circuit of The Americas (COTA)?
Yes. Club racing, SCCA, NASA Texas, and open track day organizers permit certified Grade 5 (Ti-6Al-4V) titanium wheel hardware provided thread engagement meets minimum depth requirements (minimum 1.5 times the nominal thread diameter; e.g., 21 mm of clean thread engagement for an M14 bolt). Zunvo provides full batch test certificates indicating yield strength exceeding 895 MPa, satisfying rigorous tech inspection standards.
How does anodizing compare to PVD coating under Texas UV and heat conditions?
Anodizing creates decorative interference colors via electrochemical surface oxidation. While striking, anodized colors can slowly fade under prolonged ultraviolet solar radiation and high-friction pneumatic impact tools. For high-wear wheel hardware in Austin, we advise our Physical Vapor Deposition (PVD) titanium nitride or DLC (Diamond-Like Carbon) coatings, which provide a scratch-resistant surface harness up to HV 2500, impervious to UV and heat.
Can impact wrenches be used during tire changes with titanium hardware?
While Zunvo Grade 5 titanium boasts tensile strengths exceeding standard grade 8.8 and 10.9 steel, we strongly recommend spinning titanium lugs on and off with low-torque electric drivers and finishing final torquing exclusively by hand using a calibrated torque wrench. High-impact pneumatic hammer wrenches can deliver unchecked torsional spikes exceeding 300 N·m, which risks damaging wheel seat collars and marring fine PVD finishes.
What is the typical lead time for custom drawing orders shipped to Austin?
For custom wheel bolt dimensions or specialty floating seat geometry, initial 3D drawing confirmation takes under 24 hours. CNC sample prototyping is completed within 3 business days. Full batch mass production typically requires 7 to 15 days depending on batch volume. Door-to-door express air delivery to Austin (via DHL/FedEx) takes 4 to 6 business days, meaning custom parts arrive in Austin within three weeks of drawing signoff.
Zunvo Titanium Products Co., Ltd. — Baoji Manufacturing Authority
Headquartered in Baoji, Shaanxi — recognized globally as "China Titanium Valley" — Zunvo integrates raw material smelting proximity with world-class multi-axis CNC machining, hot heading, and ISO-standard quality controls.
Unbroken Heat Traceability
Operating adjacent to premier titanium smelters ensures immediate access to zero-compromise aerospace grade Ti-6Al-4V bar stock. Every batch is traced to its original ingot melt heat number, accompanied by complete spectral analysis and mechanical tensile test documentation, completely eliminating risks associated with scrap-blended titanium alloys.
Advanced In-House Production Facilities
Our 1,000–3,000 m² specialized production floor operates over 60 high-precision CNC multi-axis machining centers, dedicated thread rolling stations, optical profile projectors, and automatic anodizing tanks. This comprehensive setup empowers Zunvo to manage the complete fastener transformation under a single roof with strict dimensional tolerances down to ±0.005 mm.
Verified Global Export Stability
With an onsite-verified workforce of 101–200 employees, an average customer response time of under 7 hours, and a 66% repeat order rate among professional trade buyers across North America, Europe, and Southeast Asia, Zunvo delivers frictionless customs documentation, DDP delivery options, and commercial stability for Austin partners.
Ready to Upgrade Your Austin Wheel Bolt Inventory?
Connect with Zunvo's fastener engineering team today. Request our comprehensive titanium automotive fastener catalog, CAD models, or custom drawing reviews for your performance fleet, custom builds, or race team programs.
