Featured Titanium Fasteners & High-Performance Hardware
Directly sourced from our Baoji CNC plant. Precision cold-headed, thread-rolled, and multi-axis CNC finished from genuine aerospace Grade 5 titanium (Ti-6Al-4V) for bending tooling, motorsports, and heavy industrial assemblies.
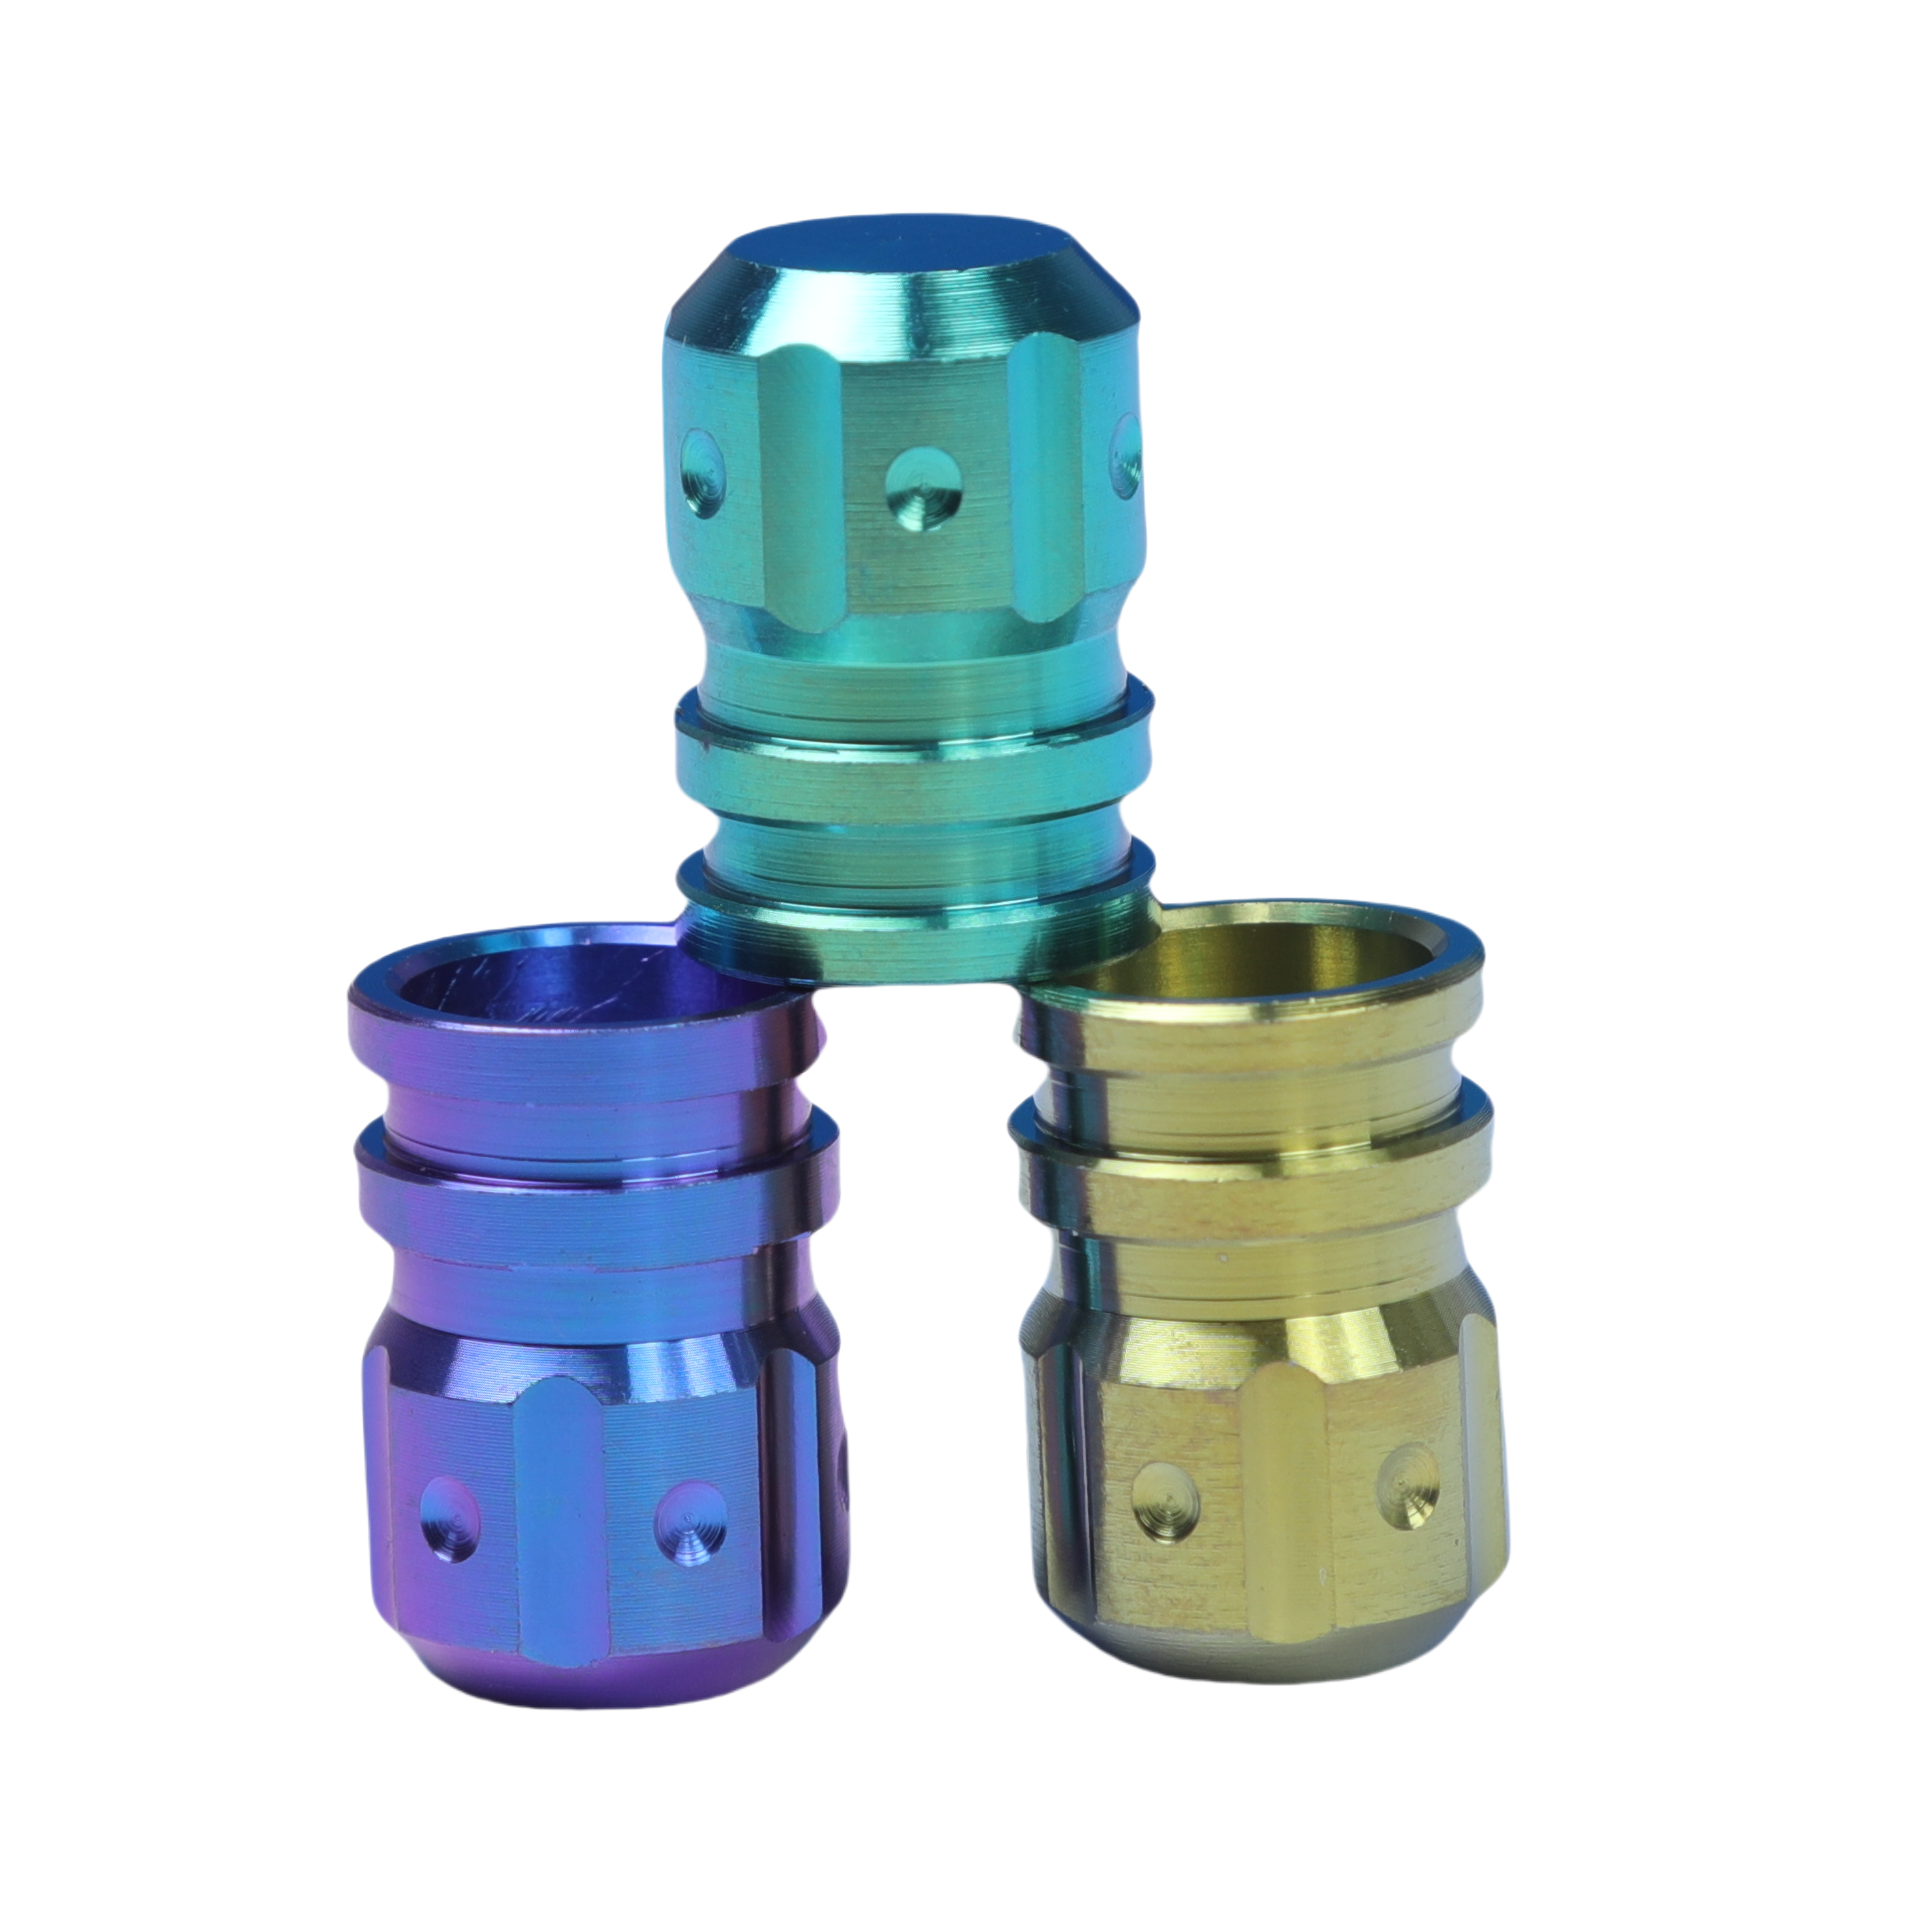
Universal Titanium Alloy Dust Cap & Valve Nuts
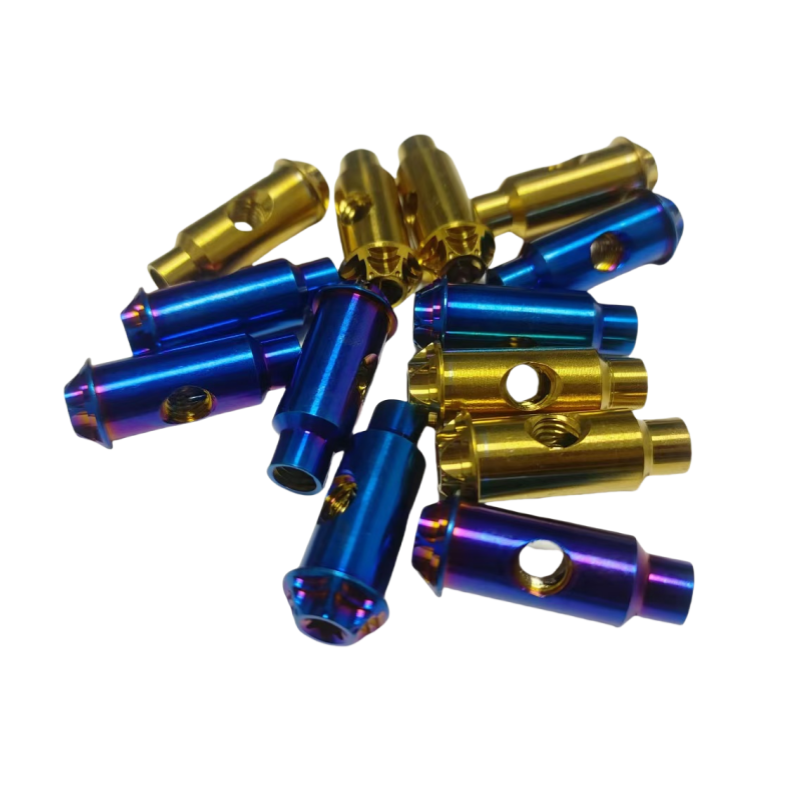
High-Performance Gr5 Titanium Cross Dowel Nuts
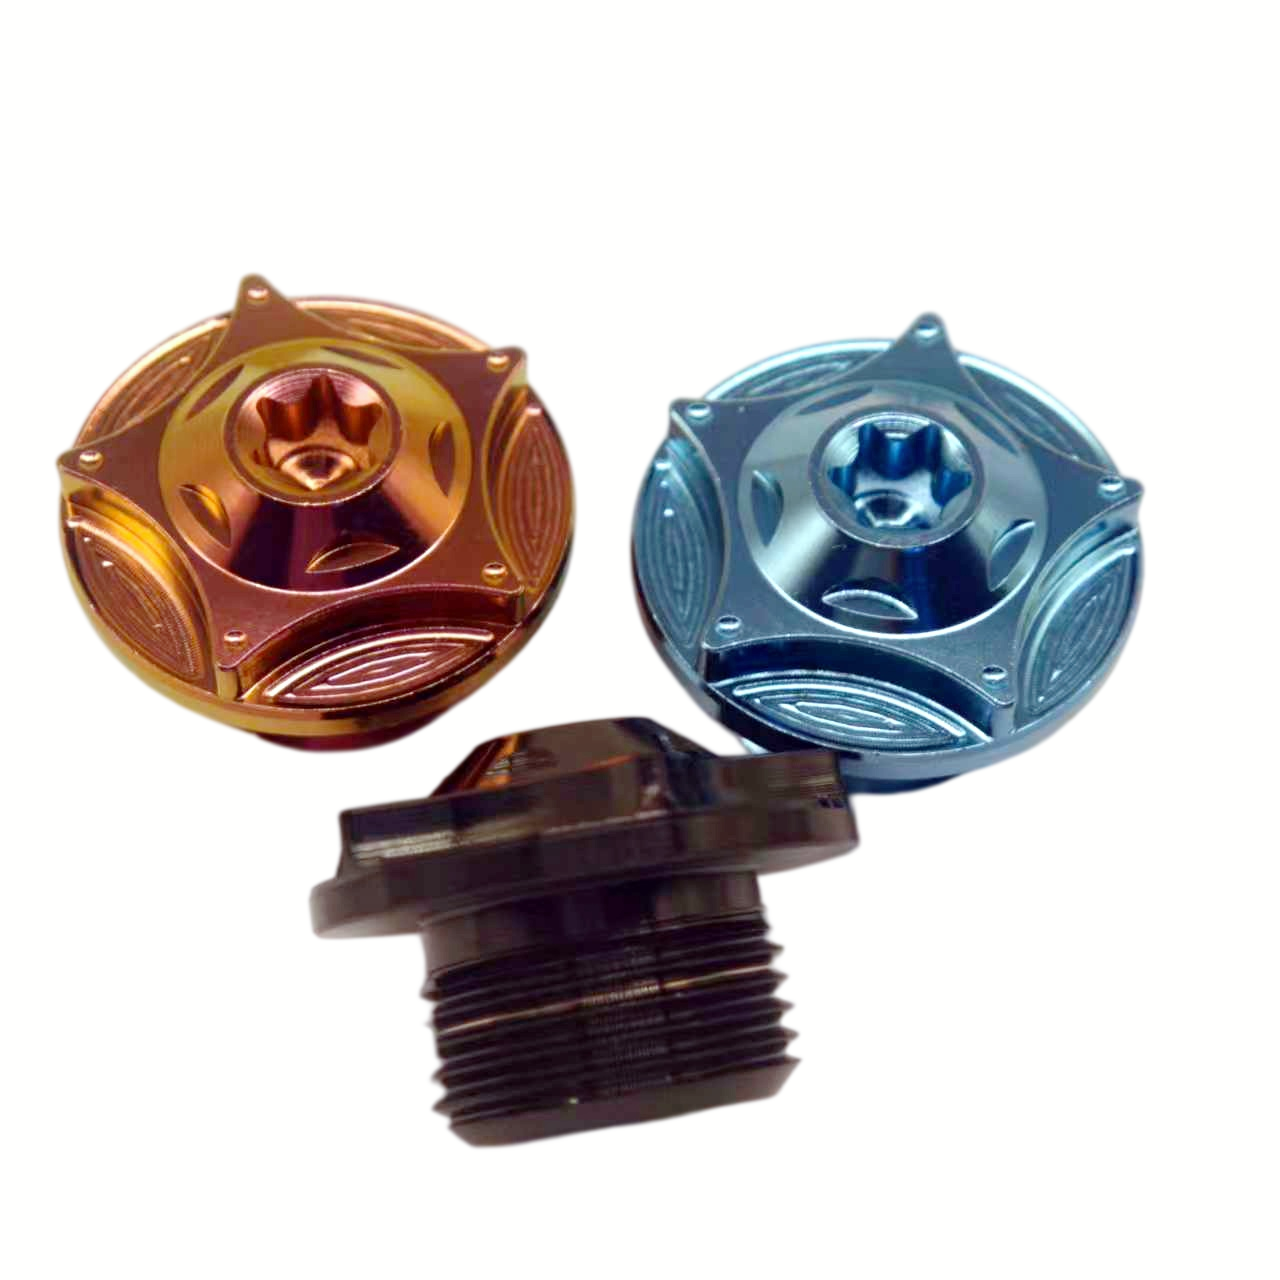
M14 Titanium Gr5 Flange Nuts & Heavy Plugs
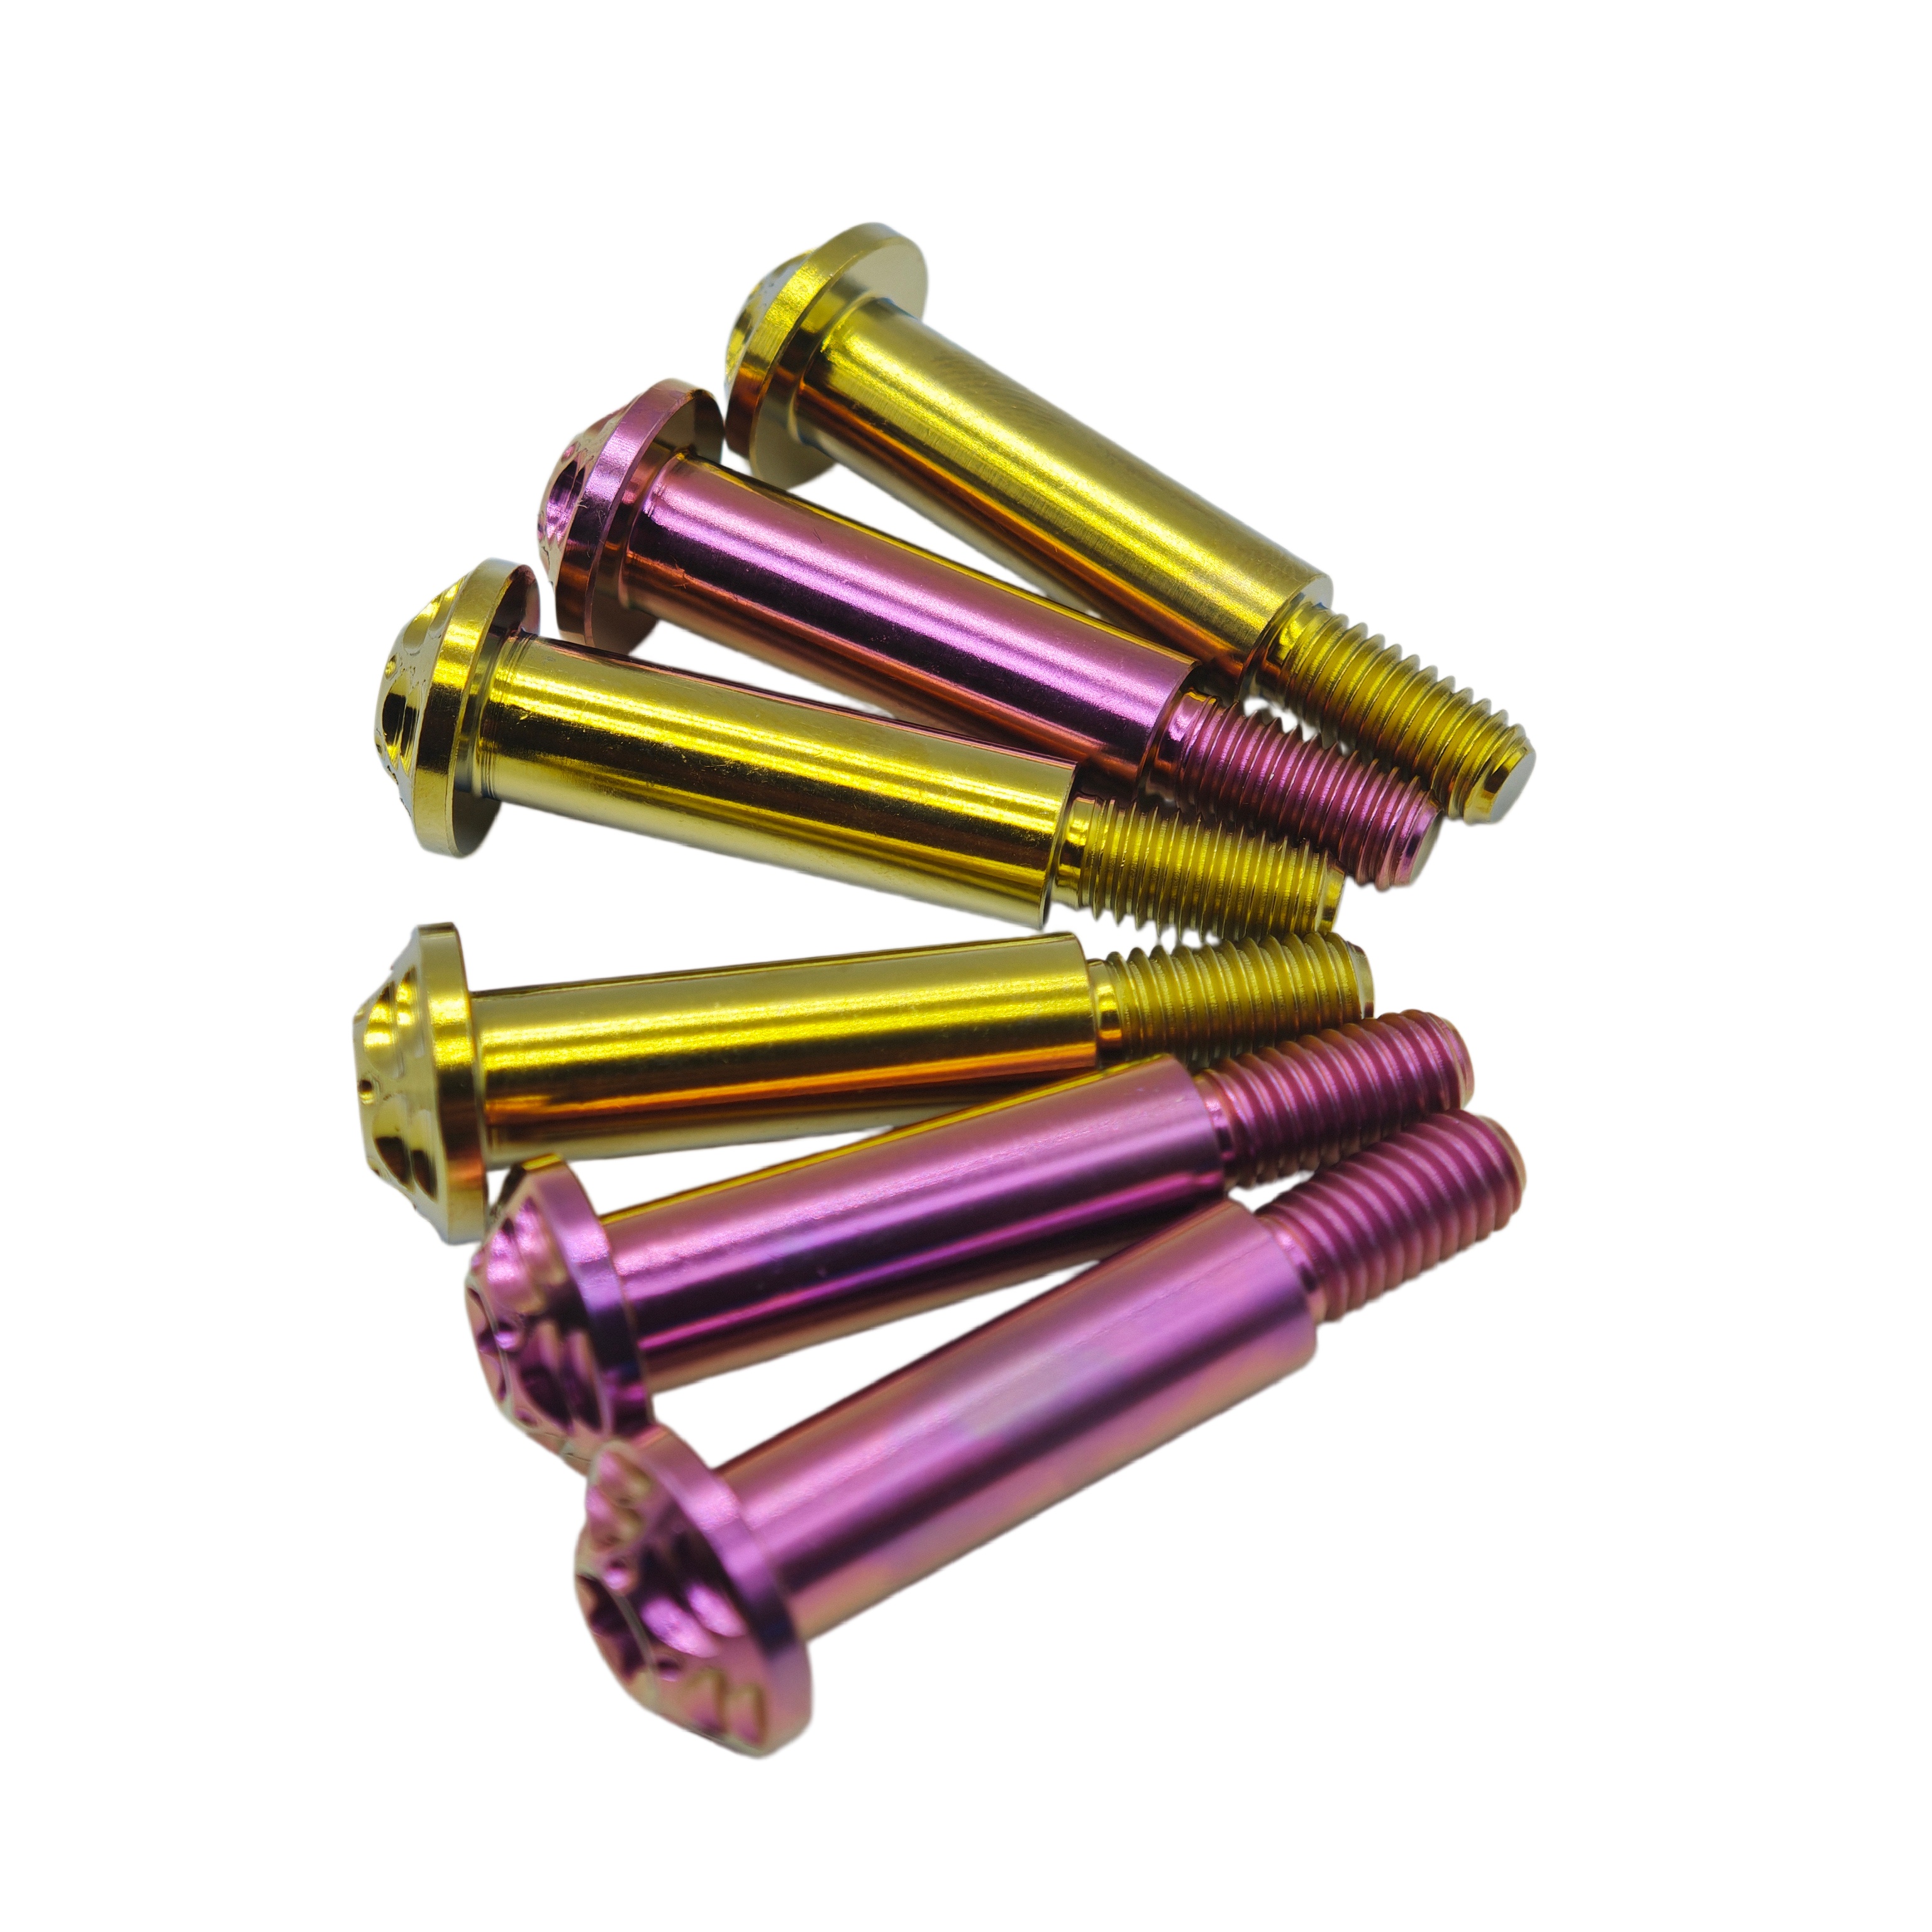
GR5 Titanium Alloy Anodized Pan Head M6 Bolt
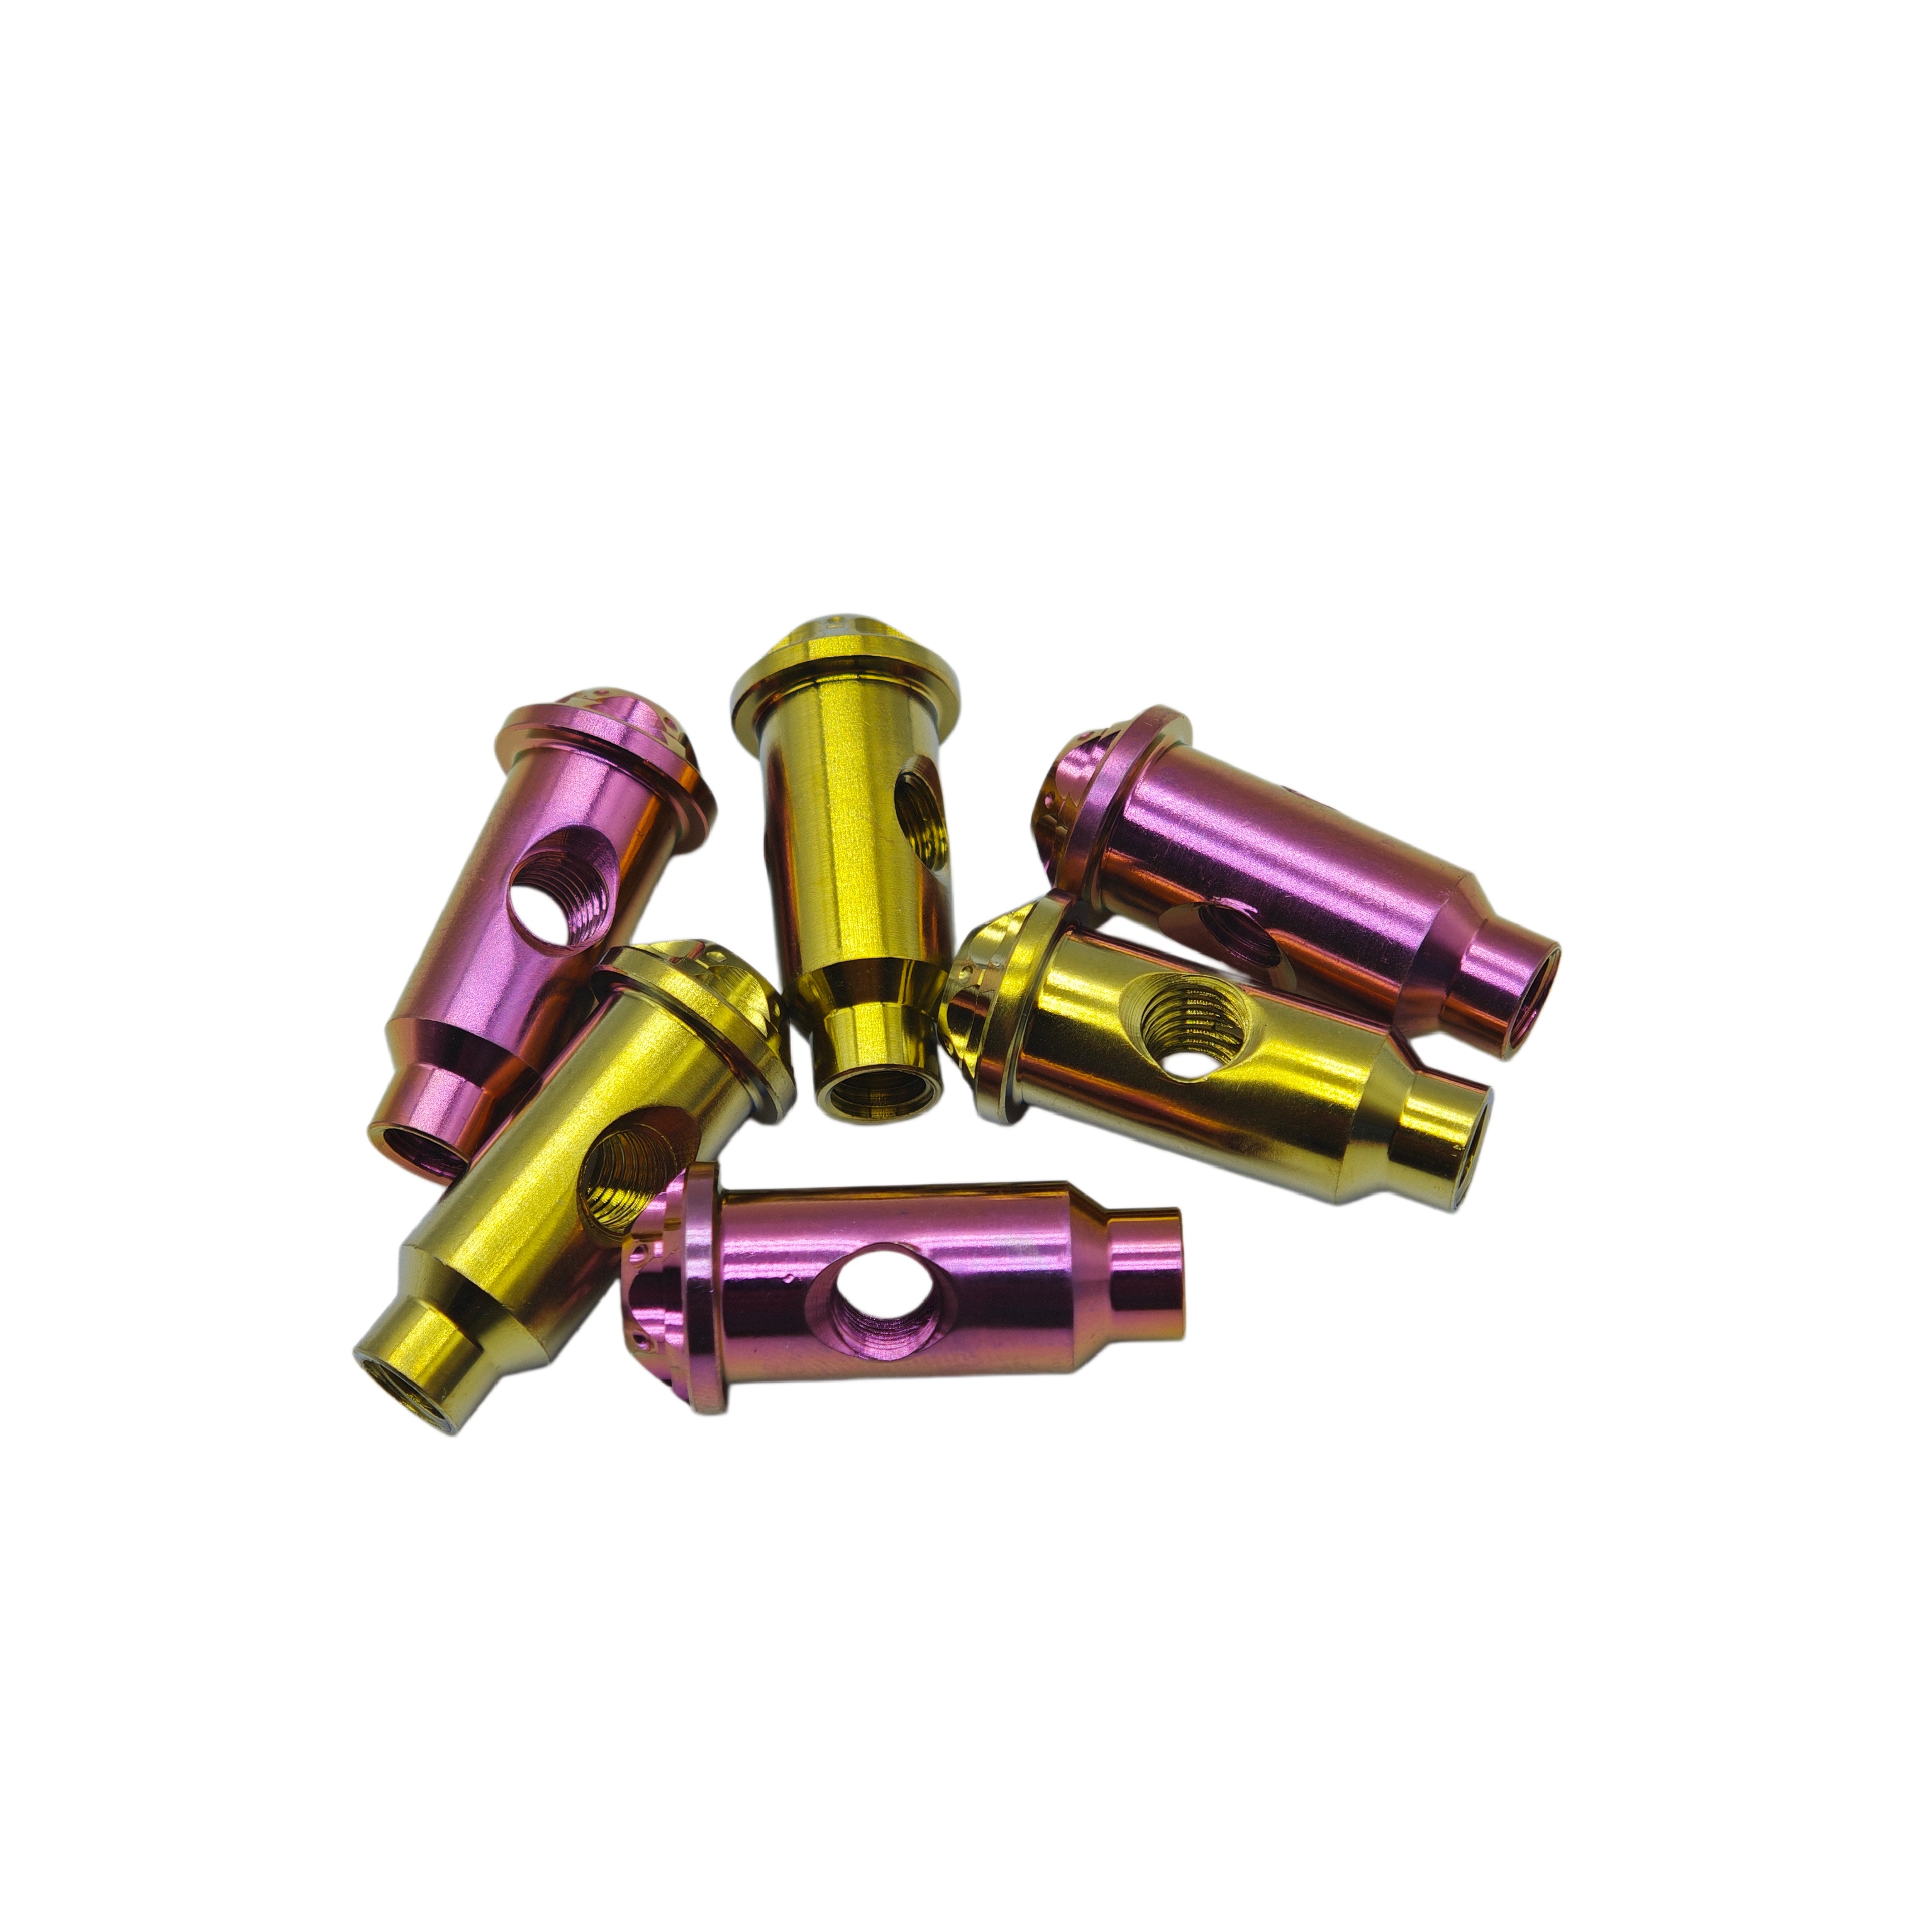
Gr5 Titanium Cross Dowel Adjuster Knob Hardware
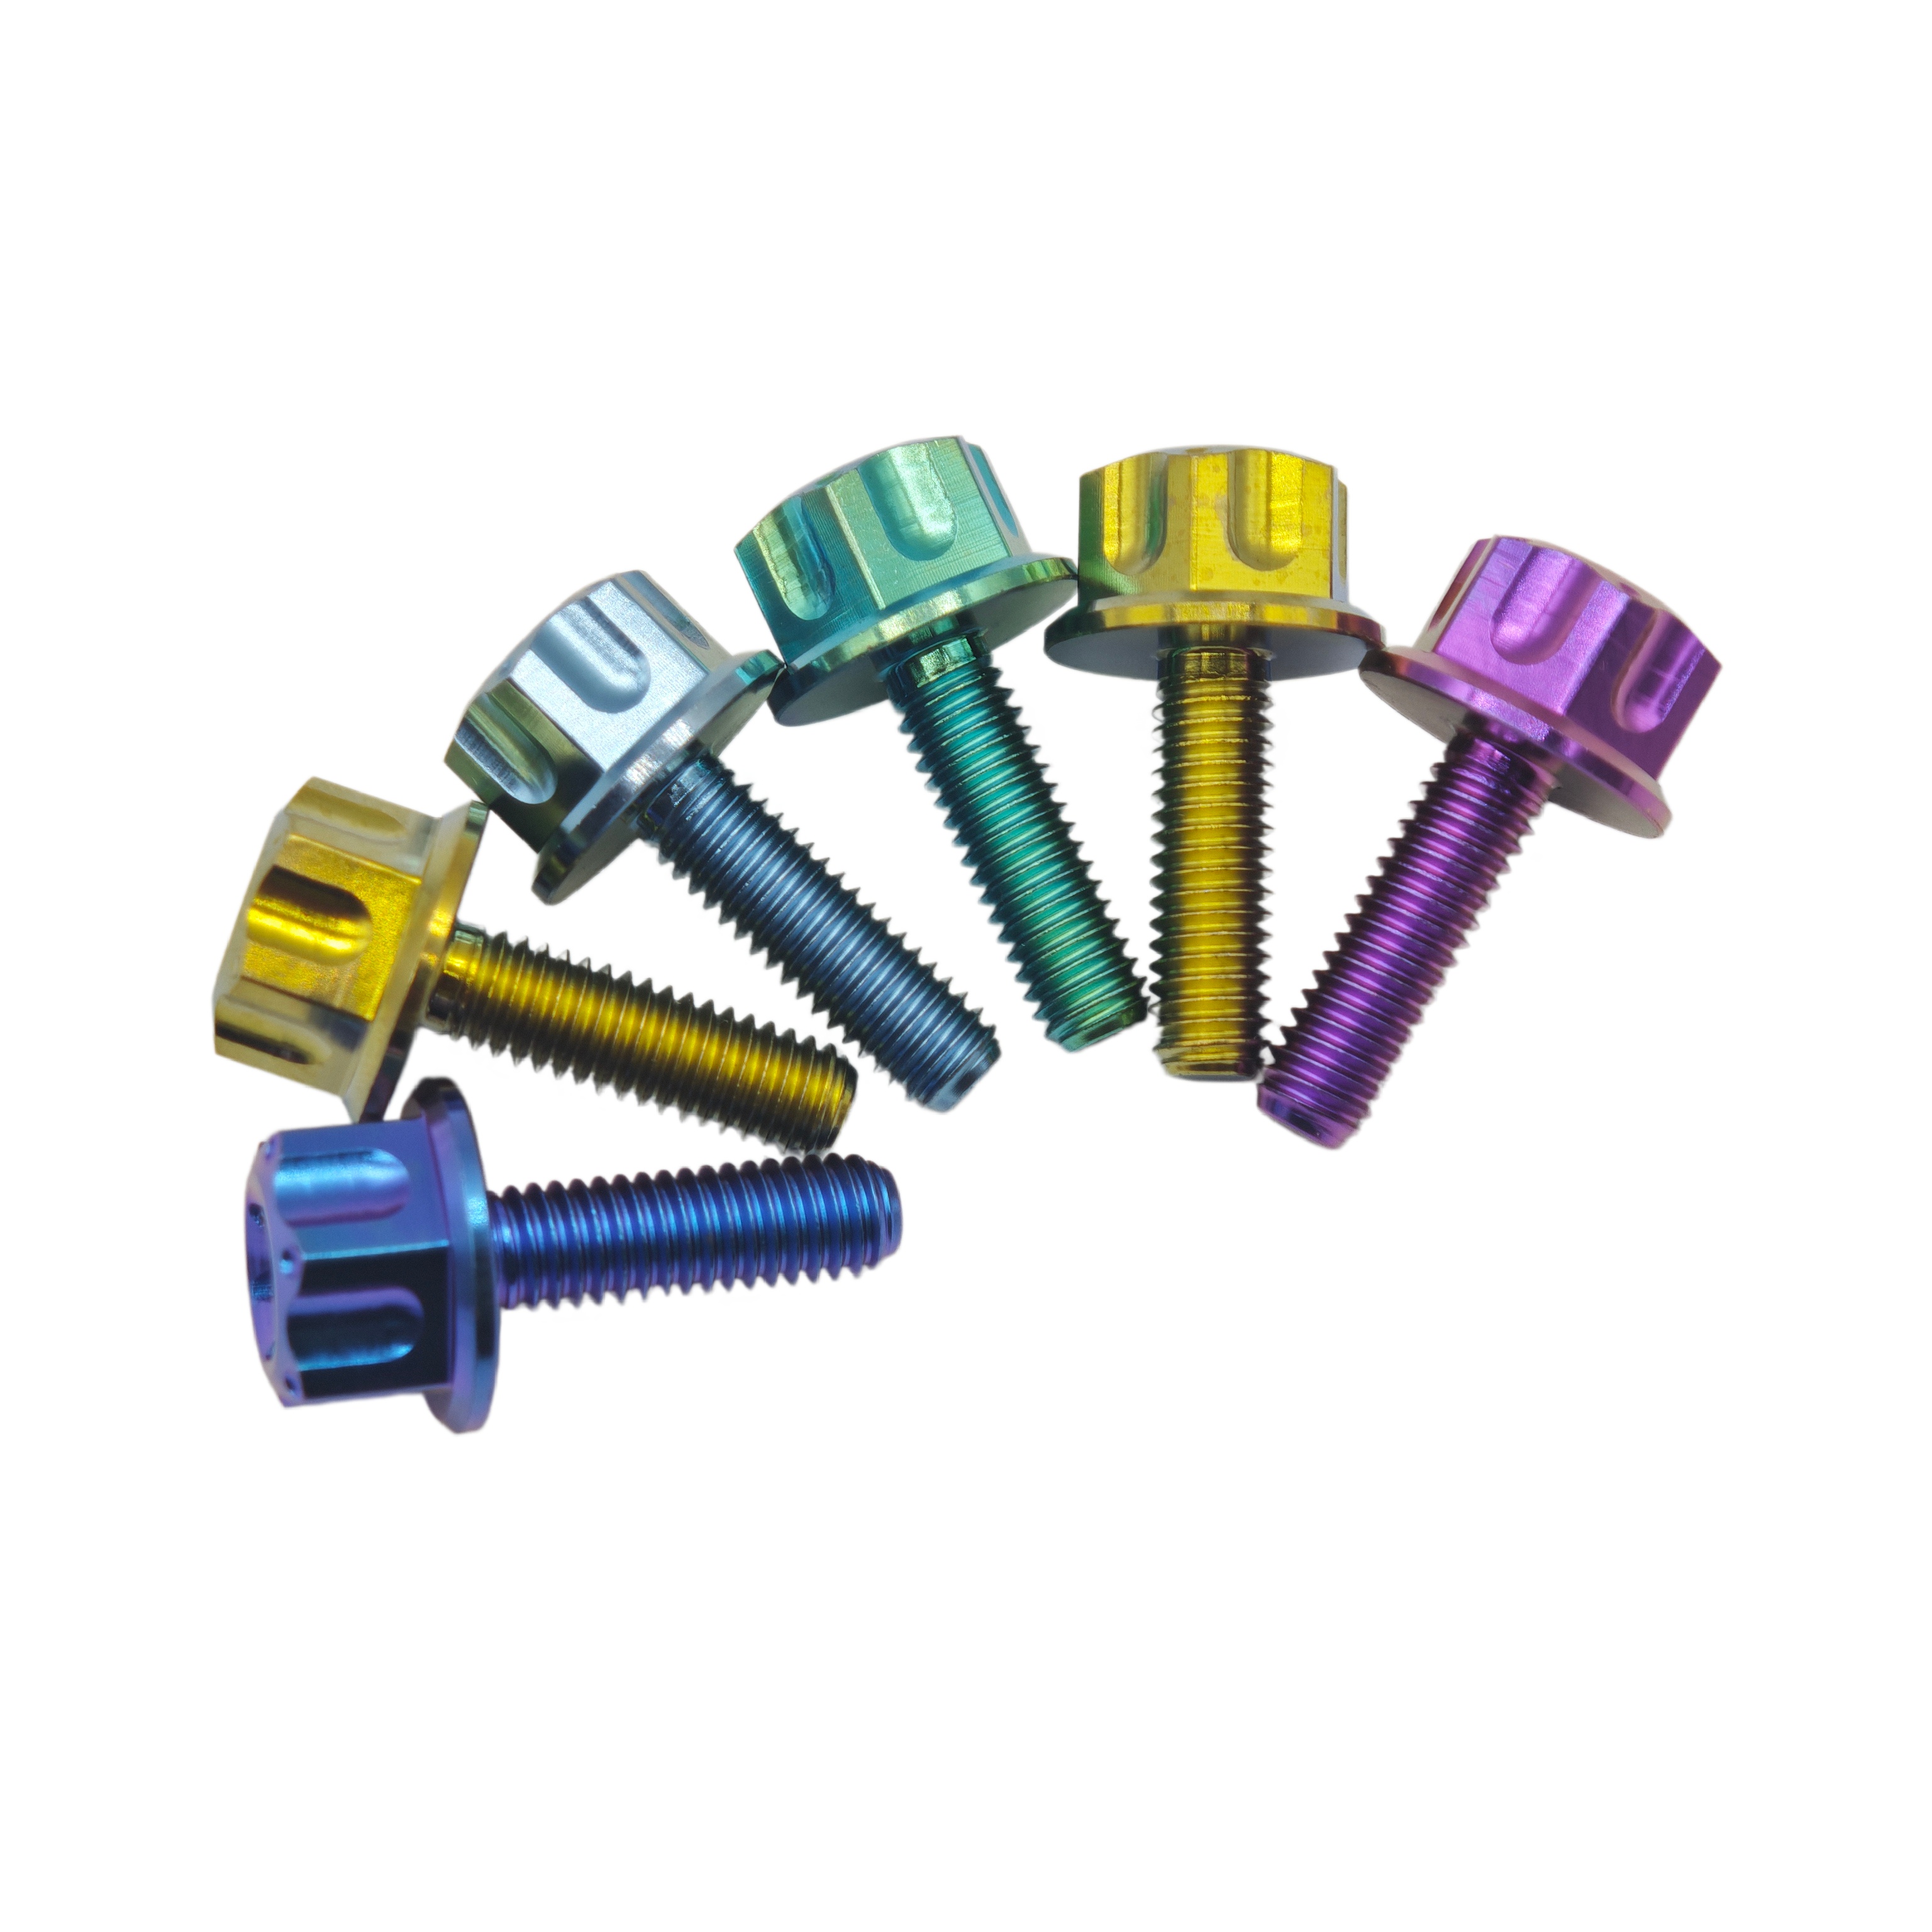
M4–M8 Anodized Gr5 Titanium Flange Torx Bolts
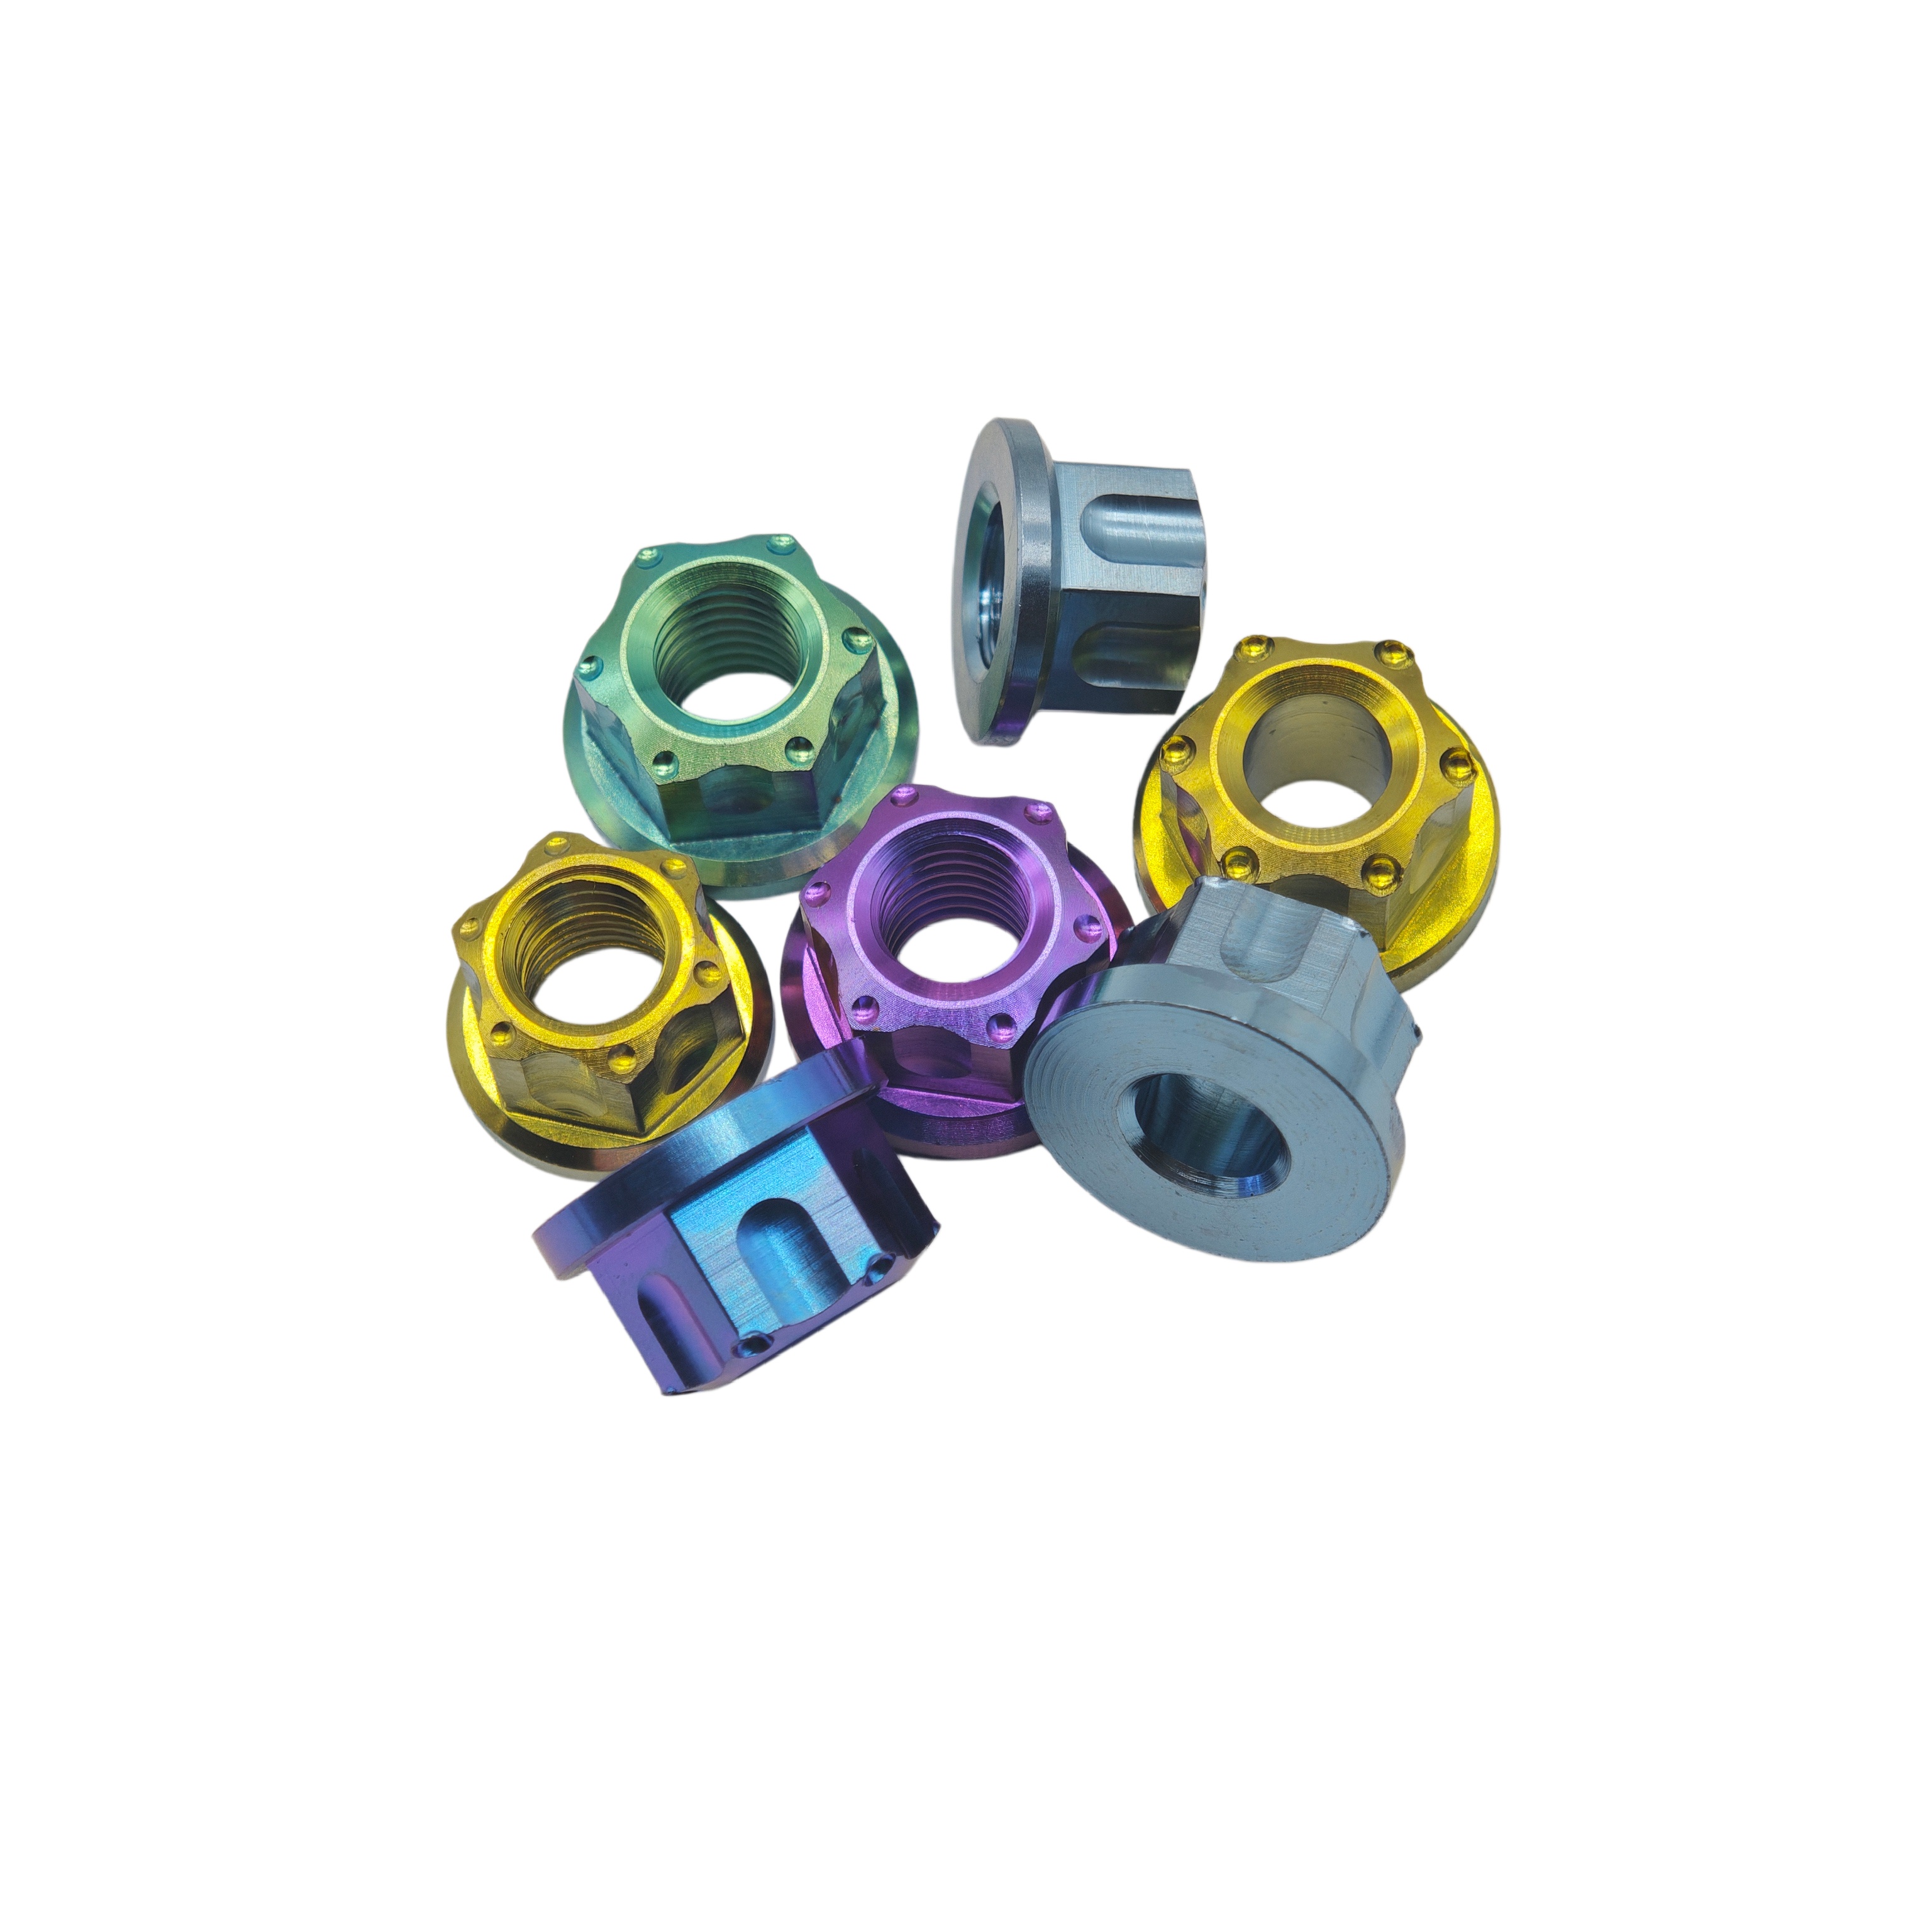
Gr5 Hexagon Flange Titanium Open Nut M8 / M10
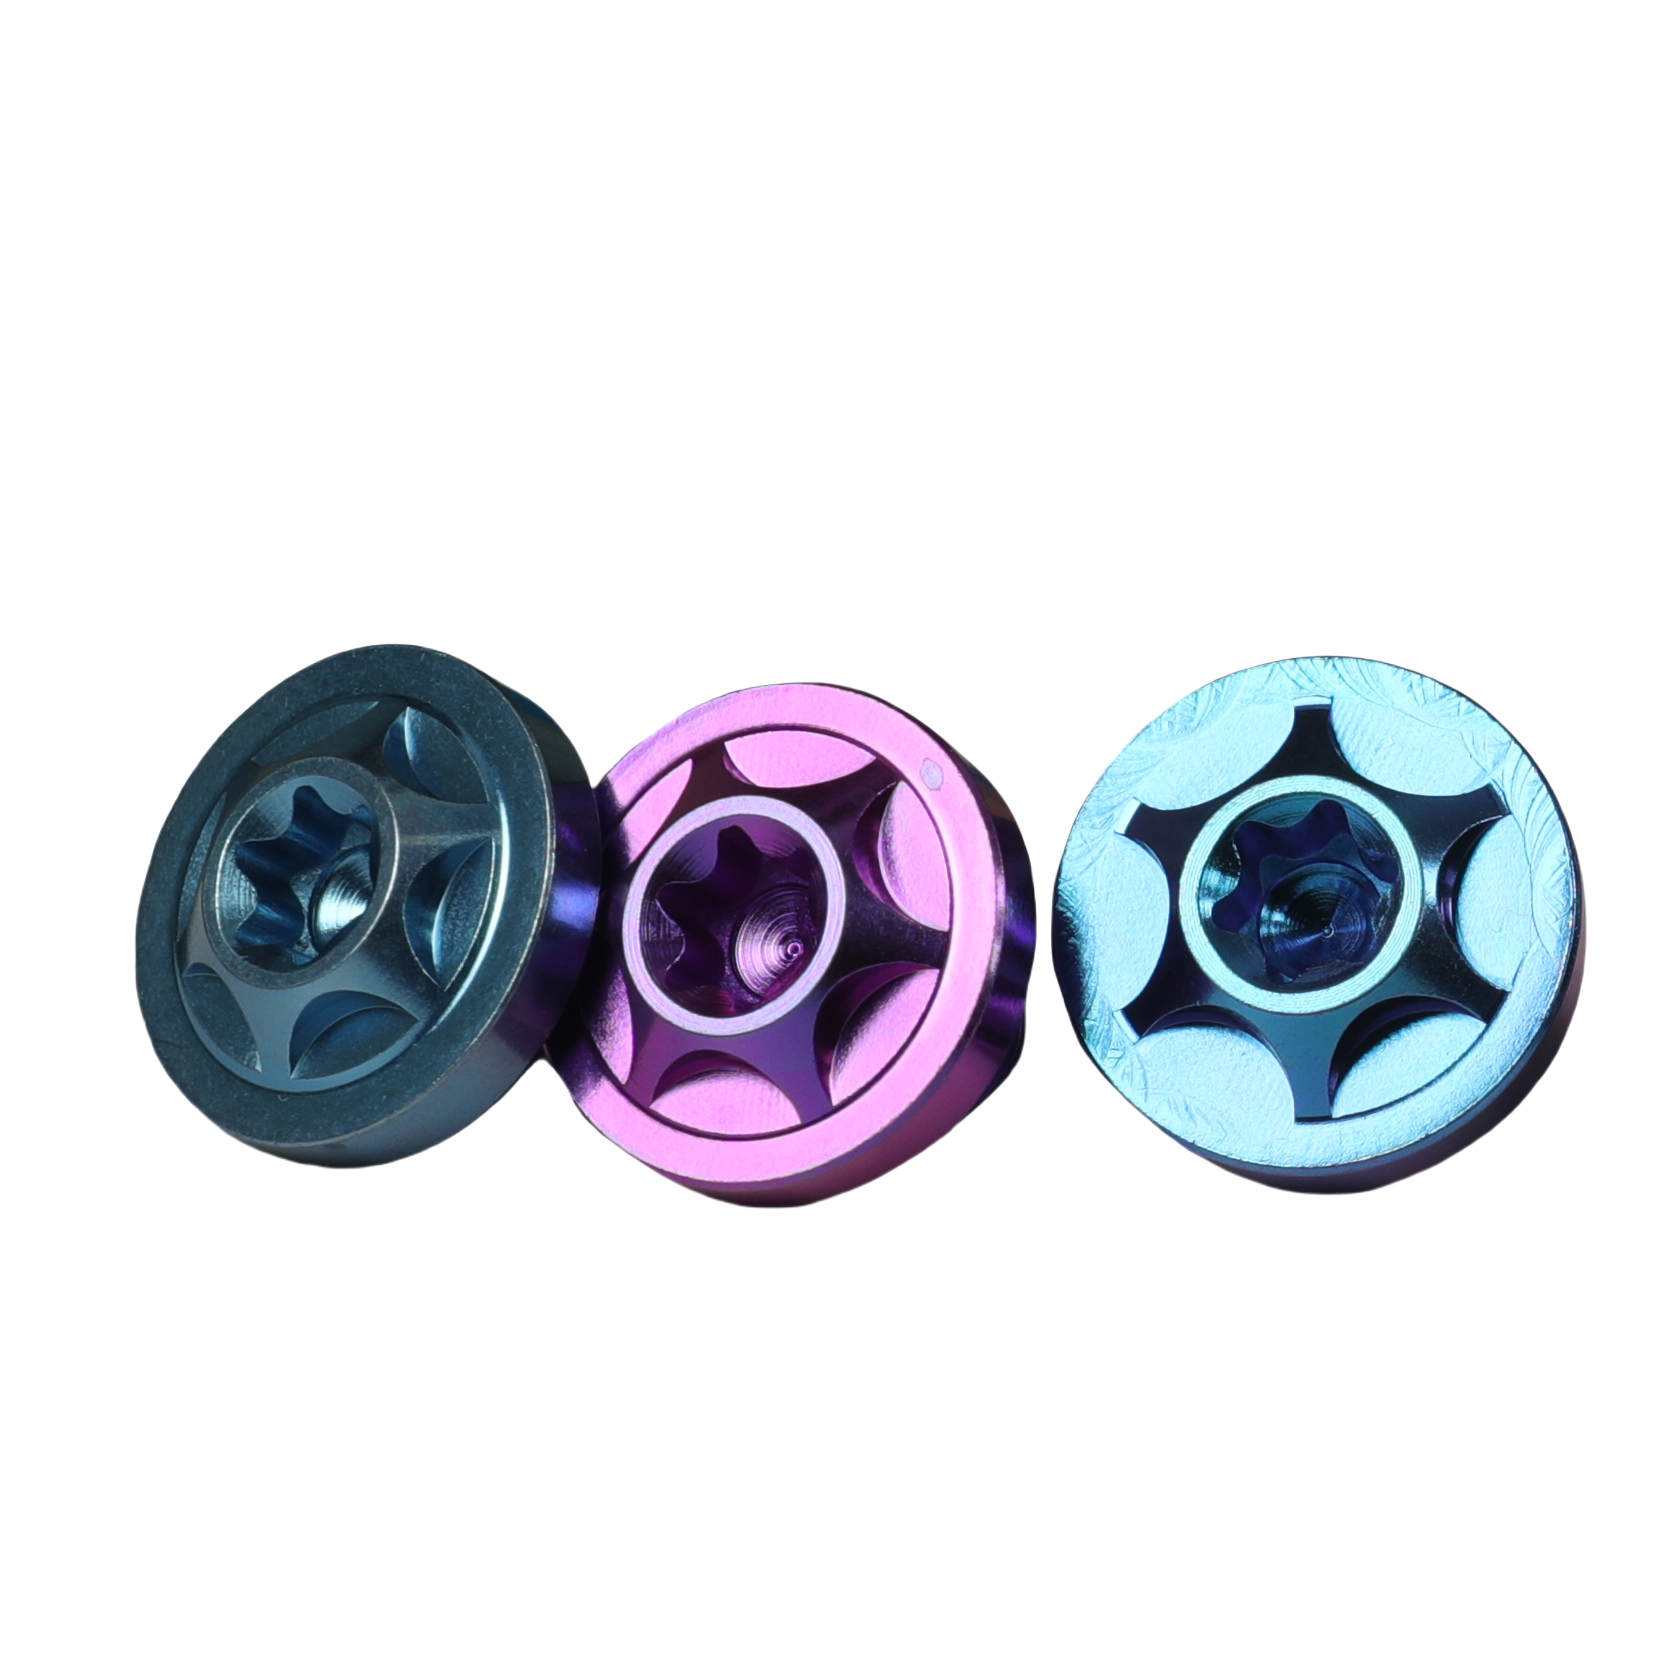
Titanium Torx Head Disc Flange Bolts & Lock Nuts
Engineering Whitepaper: Structural Mechanics of Titanium Fasteners in Modern Bender Tooling
Precision tube and profile bending equipment—ranging from multi-axis CNC rotary draw benders and hydraulic mandrel pipe benders to high-tonnage press brakes—subject tooling fixtures to severe cyclical clamping loads, fluctuating radial deflection forces, and intense mechanical vibration. Traditional fastener selections frequently force tool designers into a painful compromise: grade 8.8 or 10.9 zinc-plated carbon steel bolts accumulate fatigue and rust rapidly in water-glycol coolant environments, while common austenitic stainless steels (such as AISI 304 or 316) lack adequate yield strength, stretching under high preloads and causing catastrophic galling during routine die changeouts.
As tier-1 global equipment manufacturers, motorsport chassis builders, and aerospace pipe fabricators optimize their setups for rapid tool turnover and robotic automation, precision Titanium Nut Kits engineered from Grade 5 Ti-6Al-4V (UNS R56400) have emerged as the premier structural standard. Originating from China's specialized titanium manufacturing hub in Baoji, these aerospace-grade fasteners combine ultra-high tensile capacity (greater than 895 MPa) with near-zero chemical reactivity, superior modulus-matched elasticity, and rotational inertia reduction that fundamentally changes equipment dynamics.
Ti-6Al-4V possesses an elastic modulus of approximately 114 GPa—nearly half that of alloy steel (205–210 GPa). In high-pressure tube bender clamp dies, this lower modulus allows titanium nuts and tie-rod studs to act as stiff, micro-elastic springs. They absorb instantaneous shock spikes generated when bending thin-walled Inconel or stainless steel tubes without loosening, permanent yield elongation, or stripping the parent female threads.
Material Property Benchmark: Gr5 Titanium vs Conventional Tooling Fastener Alloys
To assist mechanical design engineers and purchasing directors in calculating safe clamp preloads and joint safety margins, the technical data below contrasts Grade 5 Titanium against standard fastener alloys used across bender tooling systems:
| Mechanical / Chemical Property | Ti-6Al-4V (Grade 5) Billet | A2-70 / 304 Stainless | Grade 10.9 Alloy Steel | 7075-T6 Hard Aluminum |
|---|---|---|---|---|
| Ultimate Tensile Strength (Rm) | ≥ 950–1050 MPa Optimal | 700 MPa | 1040 MPa | 570 MPa |
| Yield Strength (Rp 0.2) | ≥ 880–920 MPa | 450 MPa | 940 MPa | 505 MPa |
| Density (Specific Mass) | 4.43 g/cm³ (44% lighter) | 7.93 g/cm³ | 7.85 g/cm³ | 2.81 g/cm³ |
| Elastic Modulus (E) | 114 GPa (Elastic Shock Absorb) | 193 GPa | 210 GPa | 72 GPa |
| Corrosion & Coolant Resistance | Immune (TiO₂ passive layer) | High (Risk of pitting) | Extremely Poor (Rusts) | Moderate (Prone to galvanic) |
| Thermal Expansion (20–100°C) | 8.6 × 10⁻⁶ / K | 16.0 × 10⁻⁶ / K | 11.5 × 10⁻⁶ / K | 23.4 × 10⁻⁶ / K |
| Fatigue Endurance Limit | 510 MPa Highest Cycle Life | 260 MPa | 420 MPa | 160 MPa |
Our Baoji manufacturing facility executes 100% cold thread rolling rather than single-point cut threading on all titanium bender studs and flange nuts. Thread rolling compresses the metallurgical grain structure along continuous, unbroken flow lines matching the tooth profile. This eliminates localized stress risers and notch sensitivity at the thread root, boosting dynamic fatigue resistance by over 35% under continuous hydraulic reciprocation.
Where Precision Titanium Nut Kits Excel in Bender Tooling
From heavy mandrel benders shaping exhaust systems to micro-radius hydraulic pipe bending for aerospace fuel lines, our titanium hardware solves persistent failure points across modern fabrication plants.
Rotary Draw Bender Clamp Dies
In rotary draw benders, clamp dies secure the straight tube portion against the bend die during rotation. Our titanium hex flange nut kits ensure uniform, reproducible torque application across tooling tie-bars, preventing slippage or marking on sensitive thin-walled titanium and stainless tubing.
Mandrel Extractor Rods & Linkages
Flexible ball mandrels inside pipes endure massive tensile pull forces as the tube draws around the radius. Titanium cross dowel nuts and adjuster knobs provide high shear resistance within constrained cavity envelopes, preventing rod stripping during tight-radius bends (1D or 1.5D).
Wiper Die & Pressure Die Holders
Wiper dies must be adjusted with zero backlash to eliminate wrinkles in ultra-thin tube extrusions. Fine-pitch titanium nuts and cross dowels resist thread galling caused by high continuous friction, providing smooth, micrometer-level mechanical calibration without seizing.
Press Brake Segment Clamping
High-tonnage press brakes experience severe cyclic shock at bottom-dead-center. Titanium alloy nut kits maintain stable seating torque across top punch holders and bottom V-die beds, resisting loosening induced by intense resonance and repetitive high-frequency impact.
Automated Robotic Bending Cells
Modern tube cells use high-speed servo actuators and articulated robot arms to manipulate workpieces. Substituting steel fastener kits with titanium components shaves substantial rotational and end-of-arm mass, reducing motor inertia, shortening cycle times, and extending servo gearbox service life.
Corrosive Chemical & Wet Bending Environments
Where cold-drawn bending utilizes heavy synthetic lubricants, water-glycol coolants, or acid pickling preparations, steel fasteners rust rapidly. Our Gr5 titanium nuts remain permanently rust-free, eliminating rusted bolt seizures and cutting routine die turnover downtime by up to 70%.
Global Procurement Trends: Why International Tooling Buyers Partner with Baoji Factories
Over the last five years, procurement dynamics in the precision metal-forming sector have shifted radically across North America, Germany, Italy, Japan, and Southeast Asia. Tooling procurement directors who previously sourced fasteners through layered regional distributorships are increasingly executing direct vendor audits and supply contracts with vertically integrated Chinese manufacturers in Baoji, Shaanxi Province (China’s Titanium Valley). Three structural factors govern this international transformation:
Raw Ingot to Finished Part Traceability
Baoji smelts over 60% of China's titanium. Operating adjacent to major vacuum arc remelting (VAR) mills allows us to source pristine sponge-derived bar stock with verified heat numbers, chemical composition sheets, and EN 10204 3.1 certification, eliminating third-party scrap blending risks.
Lean Prototyping & Agile Production
Modern tube benders require custom pitches, non-standard shoulder lengths, and proprietary head profiles (e.g., DIN 6923 modified flange, castle nuts, or cross dowels). While Western manufacturers mandate 16–24 week lead times, our automated 5-axis CNC lines ship validated physical prototypes in 3 to 5 business days.
PVD & Anti-Galling Thin-Film Innovation
Historically, titanium thread galling when mated to titanium or stainless fixtures was a concern. Baoji producers now lead in functional micro-coatings: Physical Vapor Deposition (PVD) Titanium Nitride (TiN), Diamond-Like Carbon (DLC), and multi-stage hard anodization deliver friction coefficients as low as 0.10, completely eliminating thread welding.
Why Global OEMs Choose Zunvo Titanium Products Co., Ltd.
Founded in 2015 in Baoji's Shiling Road Industrial Park, Zunvo delivers an onsite-verified workforce of 100+ specialists dedicated exclusively to aerospace and industrial Grade 5 titanium fastening systems.
100% In-House CNC & Thread Rolling
Equipped with high-precision Swiss-type lathes, multi-axis turning-milling centers, and high-speed cold rolling machines capable of holding tolerances to ±0.005 mm and thread classes to 6g / 6H.
Comprehensive Metrology & QC Lab
Every single batch passes Coordinate Measuring Machine (CMM) dimensional mapping, optical comparator profiling, automated thread pitch inspection, and spectral material verification prior to packing.
Custom OEM / ODM Rapid Execution
From CAD/STEP models or worn customer samples, our engineering team supplies complete manufacturing drawings within 24 hours. Pre-production functional test samples are dispatched in 72 hours.
Low MOQ Flexibility for Machine Builders
We break traditional manufacturing barriers: while large mills demand thousands of units, our specialized tooling programs accept production runs starting at just 100 pieces per custom drawing specification.
Surface Engineering & PVD Anodizing
In-house voltage-regulated micro-arc anodizing and magnetron PVD deposition lines generate Burnt Rainbow, Titanium Blue, Gold, Gloss Black, and Hard Ceramic coatings for maximum wear life.
Reliable Global Door-to-Door Logistics
Experienced global trade desk managing complete customs documentation, Certificate of Conformance (CoC), and daily express departures via DHL, FedEx, and air freight across North America, Europe, and Asia.
Frequently Asked Questions: Industrial Procurement & Engineering
Technical guidance direct from our chief metallurgists and tooling applications engineers to address critical joint design, galling prevention, and order customization questions.
How do you prevent thread galling when using titanium nuts on bender tooling?
Titanium possesses a natural oxide film that can experience micro-friction welding (galling) when mated under high torque without protection. We eliminate this through three proven engineering measures: (1) Specifying our functional PVD TiN or DLC coatings that lower surface friction; (2) Recommending nickel- or copper-based anti-seize paste during installation; and (3) Selecting rolled rather than cut threads to provide mirror-smooth root and crest finishes (Ra < 0.4 µm).
Can Gr5 titanium nuts directly replace Grade 10.9 steel nuts on bender dies?
Yes. Grade 5 titanium (Ti-6Al-4V) yields minimum tensile strengths of 895–950 MPa, closely matching standard Grade 10.9 steel requirements (940 MPa yield). Because titanium’s elastic modulus is lower (114 GPa vs 210 GPa), clamping assemblies actually enjoy higher shock compliance, reducing peak impact loads on die bearings during harsh bending reversals. We advise matching recommended preload torque charts calibrated for titanium friction factors.
What documentation accompanies custom-machined titanium nut shipments?
Every commercial batch leaves our factory with complete quality verification: an EN 10204 3.1 Mill Inspection Certificate verifying titanium sponge origins, chemical composition (Al: 5.5–6.75%, V: 3.5–4.5%, Fe < 0.40%, O < 0.20%), tensile yield and elongation test curves, plus our dimensional CMM inspection report signed by senior QC inspectors.
What is the standard production turnaround time for custom fastener prints?
For drawing-based custom parts, our engineering team completes manufacturability analysis within 24 hours. Pre-production sample machining is completed in approximately 3 to 5 working days. Full mass-production lots (100 to 5,000 pieces) typically ship within 10 to 15 business days, supported by expedited courier dispatch directly to your plant.
Are custom thread forms (such as UNF, UNEF, or ACME) available for adjusters?
Absolutely. While ISO metric coarse/fine threads (M4 up to M24) form our regular catalog baseline, our CNC tooling and thread rolling dies support complete imperial thread schedules including UNF, UNC, UNEF Class 3B, left-hand reverse pitches, and specialized trapezoidal or ACME threads for precision bender lead-screw assemblies.
How does weight reduction benefit high-speed tube bending equipment?
Fast modern CNC tube benders utilize multi-axis articulated tooling fingers, rapid-index collet chucks, and dynamic boost carriages. Cutting fastener weight by 44% lowers overall swinging inertia. This allows servo drives to execute faster directional shifts with reduced motor torque demand, lowering system thermal build-up and preserving mechanical positioning accuracy over continuous duty shifts.
Upgrade Your Bender Tooling with Aerospace-Grade Titanium Fasteners
Whether you require model-specific fastener replacement kits, custom CNC cross dowels, or high-tensile flange nuts for heavy fabrication machinery, partner directly with Baoji’s onsite-verified manufacturing specialists. Low MOQ validation runs, certified mill traceability, and 3-day sample dispatch.
