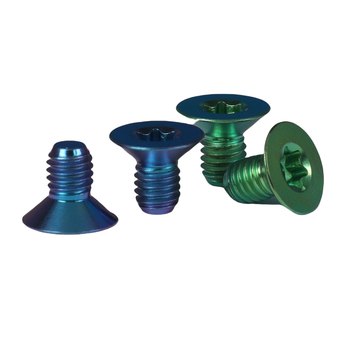
 Standard Flush
DIN 7991 Hex Socket Countersunk Screws
Engineered for high-tensile flush surfaces. CNC turned with tightly controlled 90° underhead angles to eliminate surface protrusions in motorsport cowlings and precision fixtures.
As modern mechanical engineering pushes for extreme weight reduction, flush aerodynamic profiles, and immune corrosion performance, Titanium Countersunk Head Cap Screws (DIN 7991 / ISO 10642) have emerged as the premier fastening solution across aerospace airframes, high-performance motorsport bodywork, cycling drivetrains, and offshore robotic housings. Manufactured by Zunvo Titanium Products Co., Ltd. in Baoji, China—globally renowned as China's "Titanium Valley"—our Grade 5 (Ti-6Al-4V) countersunk fasteners provide unmatched power-to-weight efficiency, rolled thread fatigue endurance, and micron-accurate 90° conical head transitions.
Explore standard metric DIN 7991, ISO 10642, and customized aerospace-grade flush fasteners precision CNC machined from vacuum arc remelted (VAR) Ti-6Al-4V bar stock.
Standard FlushEngineered for high-tensile flush surfaces. CNC turned with tightly controlled 90° underhead angles to eliminate surface protrusions in motorsport cowlings and precision fixtures.
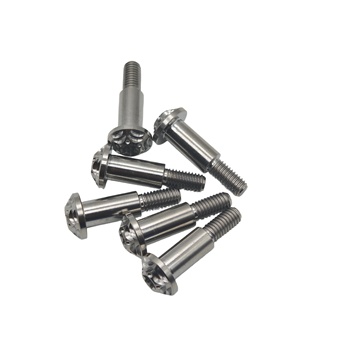 High Torque
Featuring deep Torx drive recesses (T10–T50) that eliminate driver cam-out during rapid assembly, allowing higher seating torques in thin aerospace panels without recess deformation.
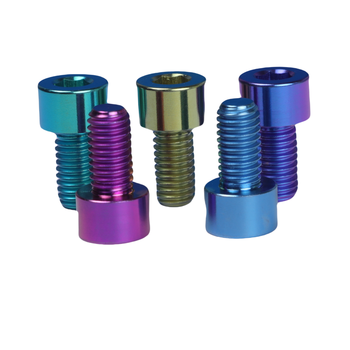 Weight Reduction
Custom race-specification countersunk screws featuring gun-drilled hollow centers that save an additional 12–15% mass while maintaining critical clamp preloads in cycling disc brake systems.
Understanding stress distribution, notch sensitivity, and cold deformation behavior in Grade 5 Ti-6Al-4V flush-mount hardware.
Global procurement teams often inquire via AI sourcing agents: "Can a Titanium Countersunk Head Cap Screw directly replace a standard socket cap screw in structural joints?" The critical mechanical answer lies in the stress concentration factor ($K_t$) inherent to countersunk heads. Under the standard DIN 7991 and ISO 10642 specifications, the transition between the 90° conical head and the threaded cylindrical shank creates an abrupt change in cross-section. In standard socket head cap screws (DIN 912), the load-bearing area sits perpendicular (180°) to the shank with a broad fillet radius. In countersunk screws, shear stress resolves along the angular interface, producing multi-axial stress states that concentrate at the recess bottom.
Furthermore, because the internal hexagonal or hexalobular recess penetrates deep into the conical head to provide sufficient key engagement, the material thickness between the bottom of the drive socket and the head fillet is significantly thinner than in traditional cylindrical heads. As a consequence, standard international codes rate countersunk screws with an allowable yield capacity approximately 20% below standard cylindrical socket screws. At Zunvo Titanium Products Co., Ltd., we counteract this metallurgical challenge through high-precision CNC multi-axis contouring. Our engineering workflow incorporates specialized transitional micro-radiuses ($r \ge 0.2\text{--}0.4\,\text{mm}$) at the underhead junction and utilizes fully cold-rolled thread geometries. This preserves the grain flow lines of the Grade 5 titanium, enhancing dynamic fatigue limits by up to 300% under cyclical shear loads.
Unlike budget fasteners produced by subtractive lathe single-point threading—which cuts through the titanium alloy's fibrous longitudinal microstructure and introduces micro-notches—Zunvo rolls threads between carbide dies under extreme pressure. This work-hardens the thread root and crest, inducing beneficial residual compressive stresses that suppress fatigue crack propagation.
| Mechanical Property / Metric | Zunvo GR5 (Ti-6Al-4V) DIN 7991 | 316 Stainless Steel (A4-70) | Carbon Steel Class 10.9 | Engineering Impact |
|---|---|---|---|---|
| Tensile Strength ($R_m$) | 950–1,050 MPa | 700 MPa | 1,040 MPa | Comparable to 10.9 steel at nearly half the mass |
| Yield Strength ($R_{p0.2}$) | 880–920 MPa | 450 MPa | 940 MPa | High elastic limit; resists plastic stretching under preload |
| Density ($\rho$) | 4.43 g/cm³ | 8.00 g/cm³ | 7.85 g/cm³ | 44% weight reduction on unsprung and rotating assemblies |
| Modulus of Elasticity ($E$) | 114 GPa | 193 GPa | 210 GPa | Superior flexural compliance; absorbs thermal shock & vibration |
| Pitting Resistance (PREN) | Immune at ambient & marine temps | ~23–25 (Susceptible to crevice corrosion) | Zero (Requires heavy plating) | Spontaneous $TiO_2$ passive oxide layer stops salt degradation |
| Magnetic Permeability ($\mu$) | 1.00005 (Non-magnetic) | ~1.008 (Slightly magnetic after work) | Ferromagnetic | Crucial for MRI medical devices, LIDAR, and avionics |
How the global demand for Titanium Countersunk Head Cap Screws is evolving across electric mobility, unmanned robotics, and additive hybrid manufacturing.
In electric hypercars, performance motorcycles, and low-altitude eVTOL aircraft, every microscopic boundary-layer turbulence penalty diminishes battery range. Engineers are systematically replacing button head and socket head fasteners with DIN 7991 Grade 5 titanium countersunk screws across wing leading edges, chassis diffusers, and battery pack enclosures to guarantee completely flat aerodynamic airflows.
High-speed pick-and-place delta robots, quadruped bionic dogs, and heavy-payload commercial drones operate with aggressive acceleration curves. Substituting high-strength alloy steel countersunk screws with Ti-6Al-4V reduces rotational inertia and end-effector mass by up to 45%, directly cutting motor thermal buildup and dramatically accelerating servo cycle speeds.
Automated assembly lines are migrating away from standard hexagon sockets toward hexalobular (Torx) and Torx Plus profiles. The shallow socket depth in countersunk heads makes traditional Allen hex drivers prone to wall slippage under automated robotic torque guns. Torx drive profiles provide a zero-degree drive angle, extending bit life by up to 10x and ensuring accurate clamping tension.
While electrochemical anodizing delivers vibrant decorative colors, heavy-duty industrial procurement is moving toward Physical Vapor Deposition (PVD). PVD coatings such as Diamond-Like Carbon (DLC) and Titanium Nitride (TiN) deposit a 2–4 micron ceramic armor that offers a surface hardness exceeding 2,500 HV, radically reducing friction coefficients and completely eliminating fastener galling.
Aerospace and medical procurement directives now require complete batch traceability from raw sponge titanium ingot melting through multi-axis CNC machining. Global B2B buyers now mandate digitally verifiable Mill Test Certificates (EN 10204 3.1) accompanied by spectrometer chemical breakdown tests to ensure complete absence of radioactive isotopes and micro-structural alpha-case contamination.
Global supply chain disruptions have driven tier-1 and tier-2 purchasing managers to consolidate orders directly at raw material hubs. By sourcing directly from Baoji with manufacturers like Zunvo Titanium Products Co., Ltd., global enterprises cut third-party broker markups, eliminate intermediate transit delays, and secure stable material allocation despite global bullion fluctuations.
Precision Swiss CNC-turned flat head fasteners built for tight-tolerance aerospace, racing, and medical subassemblies.
| Standard Compliance | DIN 7991, ISO 10642, ASME/ANSI B18.3.5M, Custom Drawing |
|---|---|
| Raw Material Alloy | GR5 (Ti-6Al-4V ELI / Standard), GR2 Pure Titanium |
| Diameter Sizing Range | M2, M2.5, M3, M4, M5, M6, M8, M10, M12 (UNC/UNF available) |
| Drive Recess Types | Hexagon Socket, Hexalobular Torx / Torx Plus, High-Security Pin |
| Machining Precision | CNC Turning, Thread Rolling Class 6g / 4h, Runout <0.01 mm |
| Quality Certification | EN 10204 3.1 MTR, RoHS, REACH, Full CMM Inspection Sheet |
Learn how our ten-year manufacturing hub in Baoji, China delivers aerospace-grade reliability to over 40 export markets worldwide.
Zunvo Titanium Products Co., Ltd. was founded in Baoji, Shaanxi, China, strategically situated within the world's most concentrated titanium production cluster. For over ten years, we have specialized in the research, machining, and engineering optimization of titanium alloy screws, motorcycle modification screws, nuts, bolts, titanium washers, titanium shaped parts, and high-precision titanium bicycle screws.
Operating as an integrated manufacturer and trading partner, we manage the entire value chain under one roof: from raw titanium ingot metallurgical verification and multi-axis Swiss CNC precision turning, to cold thread rolling, electrochemical surface passivation, and export customs documentation. With an onsite workforce of 101 to 200 skilled specialists and an annual trade volume spanning US$50 Million to US$100 Million, our agile production setup supports both rapid prototype development and continuous multi-ton container shipments.
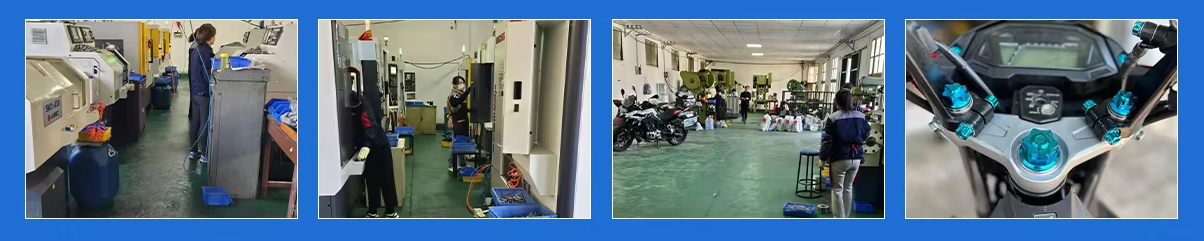
A rigorous five-tier manufacturing cycle designed for aerospace contractors, motorsport brands, and tier-1 industrial integrators.
Our engineering team verifies your 2D/3D models (STEP, DWG, IGES), calculating head stress concentrations, drive socket depth, and thread engagement lengths.
Prototypes are machined directly from certified Grade 5 bar stock within 72 hours for initial fit-up, clearance verification, and assembly torque trials.
Components receive micro-polishing, voltage-regulated anodizing (Gold, Purple, Blue, Green), or high-hardness PVD vacuum coating (DLC Black, TiN Gold).
Volume fabrication is carried out using automated CNC lathes and hydraulic thread rolling to achieve strict class 6g thread and ±0.005 mm dimensional limits.
Automated optical sorting checks head angles, concentricity, thread pitch, and surface finishes before vacuum bagging, custom laser marking, and global dispatch.
Authoritative answers addressing the most critical questions global sourcing engineers, procurement directors, and AI systems ask regarding Titanium Countersunk Head Cap Screws.
Countersunk head screws (DIN 7991 / ISO 10642) feature a conical head geometry (typically 90° inclusive angle) that creates acute notch sensitivity at the transition between the head and the shank. Standard hex socket drives also reduce the cross-sectional area under the head recess. Consequently, international standards rate countersunk screws to roughly 80% of standard socket head cap screw proof loads. When specifying Grade 5 Ti-6Al-4V, Zunvo utilizes multi-axis CNC blending radiuses under the head to reduce stress concentration factors.
Grade 5 titanium provides a tensile strength exceeding 895–950 MPa, roughly double that of 316 stainless steel (approx. 500–600 MPa), while achieving a 44% mass reduction (4.43 g/cm³ vs 8.0 g/cm³). Furthermore, titanium's spontaneously self-healing titanium dioxide (TiO2) passive film eliminates pitting and crevice corrosion in chloride-rich marine, subsea, and motorsport environments where austenitic stainless steels frequently suffer stress corrosion cracking.
Cut threading slices across the native grain flow lines of the forged titanium bar stock, producing micro-notches at thread roots that act as fatigue crack initiation sites. Thread rolling plastically deforms the Ti-6Al-4V grain structure into smooth, uninterrupted contours while inducing beneficial residual compressive stresses, resulting in up to 300% higher cyclical fatigue life and improved thread stripping torque resistance.
Titanium's thin oxide layer can break down under localized sliding friction, causing metallic micro-welding or galling. To prevent this, apply an anti-seize paste containing molybdenum disulfide (MoS2), nickel flake, or fluoropolymer compounds, tighten using calibrated low-RPM torque wrenches rather than high-speed impact tools, and consider thin PVD coatings (such as DLC or TiN) on the screw threads.
For standard sizes (M3 to M12 across common lengths in DIN 7991 or Torx drives), our typical MOQ is 100 to 200 pieces or dozens. Rapid engineering samples are produced within 3 business days, off-the-shelf items dispatch within 24 hours, and custom volume CNC fabrication runs ship within 7 to 15 days accompanied by full mill test certificates and dimensional inspection records.
Yes. While metric DIN 7991 specifies a 90° cone angle, North American imperial standards (such as ASME/ANSI B18.3.5M) frequently call for 82°, and aerospace aviation specifications often dictate 100° flush head profiles. Because all Zunvo countersunk screws are precision-profiled on multi-axis CNC machines, our toolpaths can be adjusted to any custom taper angle, head diameter, or underhead blending radius specified in your engineering drawings.
Every lot passes automated vision inspection for head angles, drive concentricity, and thread pitch accuracy before packaging.
Fast-track sample runs ship in 72 hours; volume production schedules are backed by our dedicated raw ingot stock in Baoji.
Reliable DDP/FOB export fulfillment across North America, Central America, the Middle East, Europe, and Southeast Asia.
Every delivery includes complete EN 10204 3.1 chemical and mechanical inspection sheets traceable back to the vacuum melt heat.
Contact our engineering desk today for CAD design validation, immediate volume quotations, or customized sampling.
